显示标签为“inductionbrazingcarbide”的博文。显示所有博文

2024年4月12日星期五

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

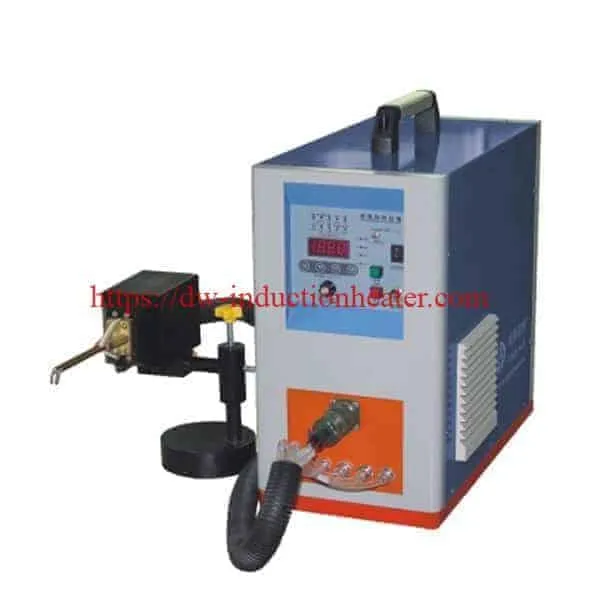
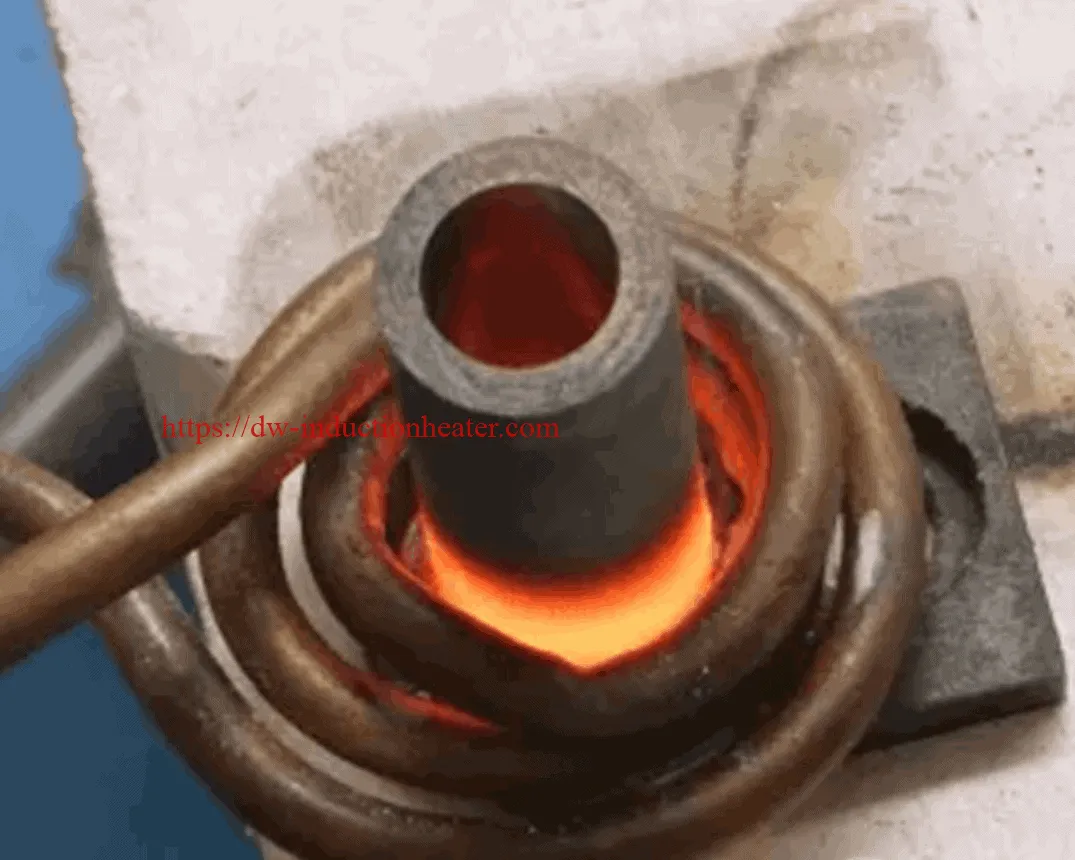
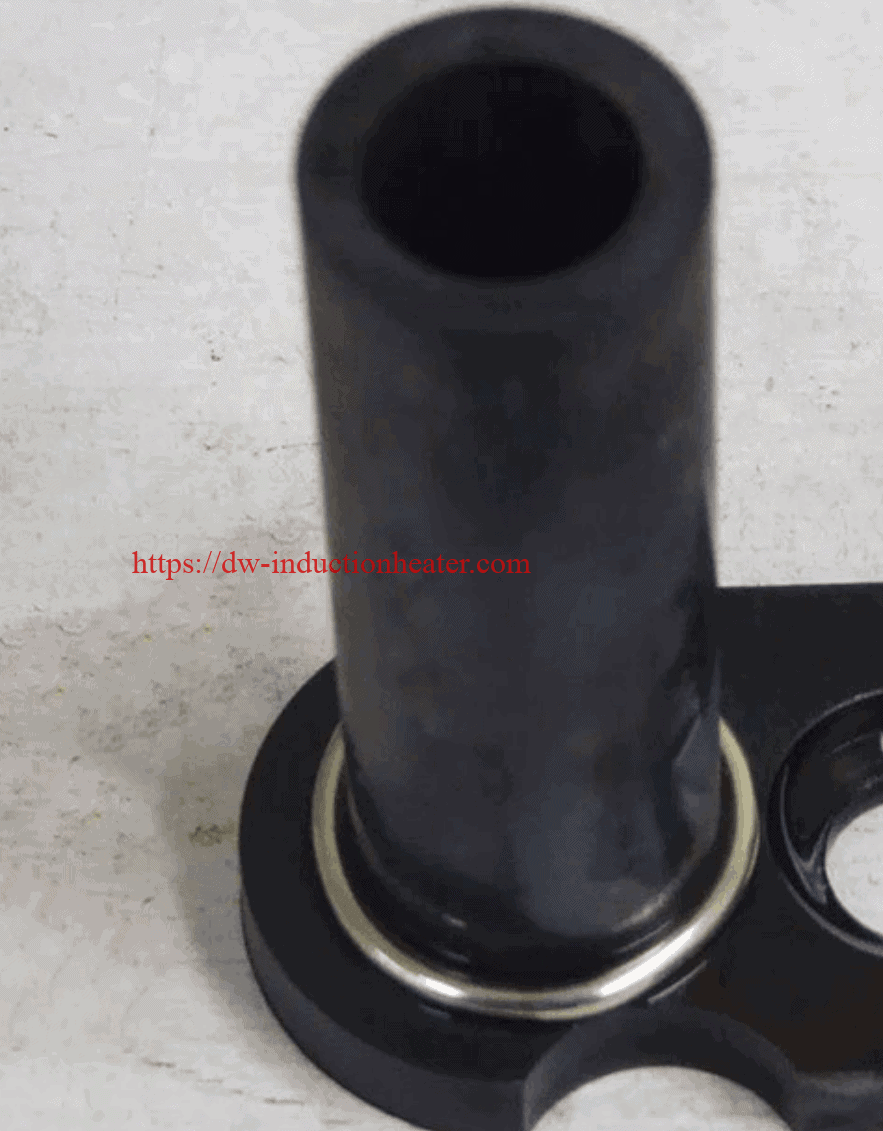
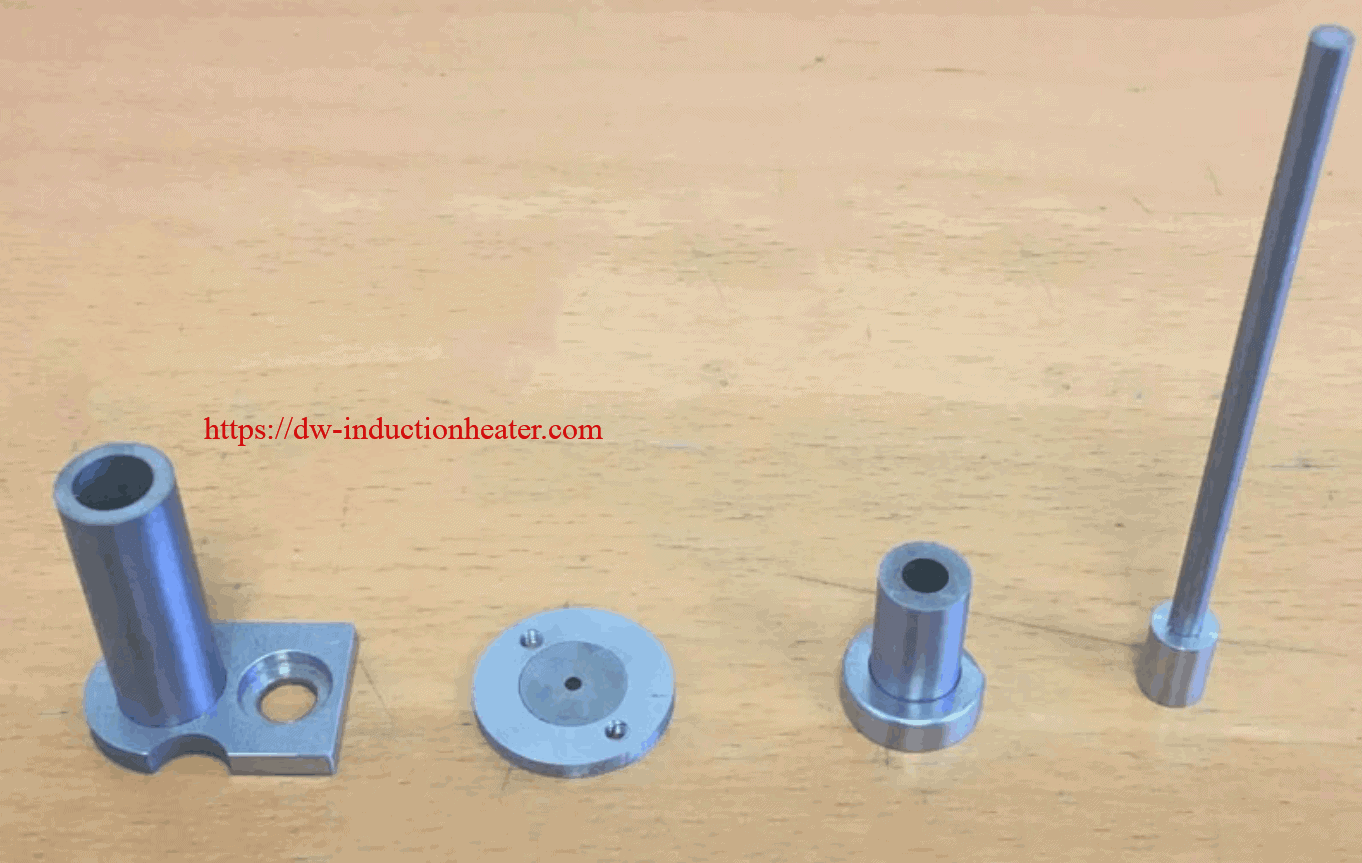
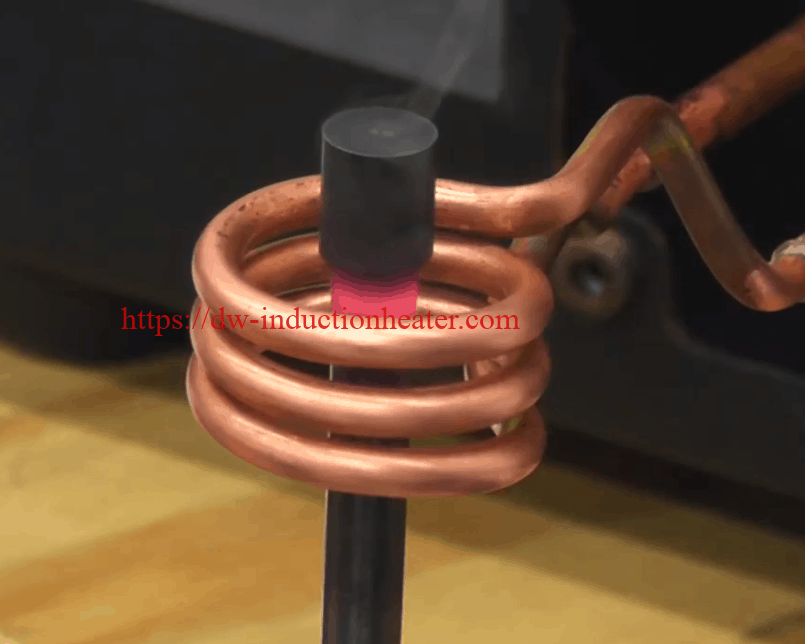
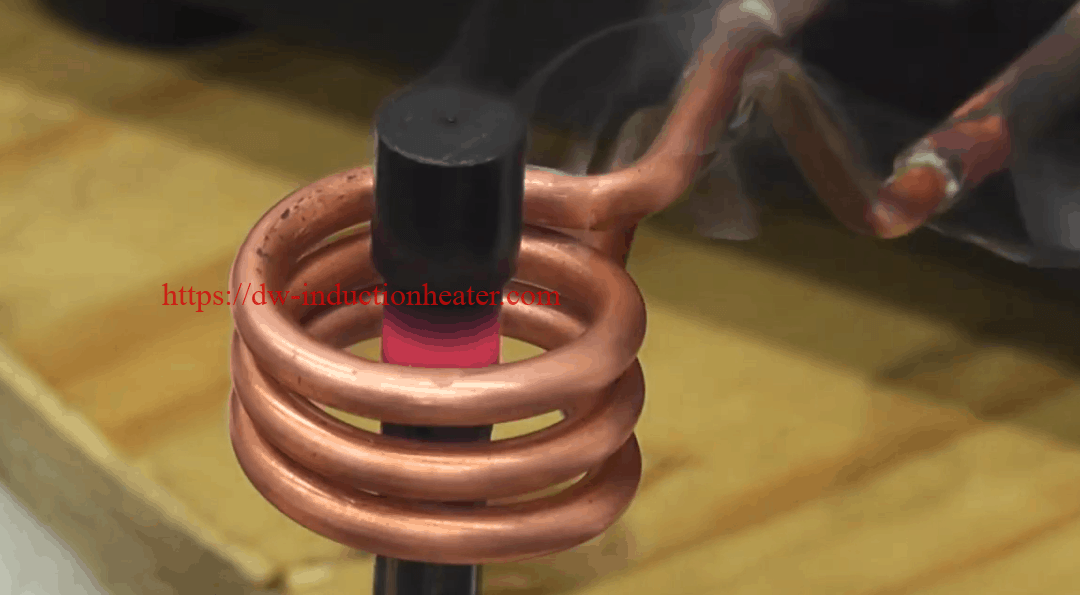
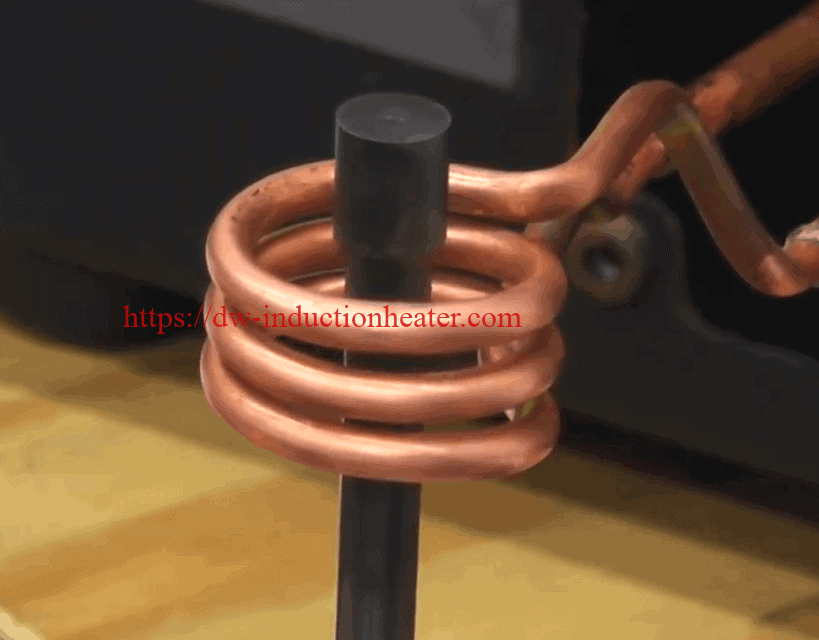
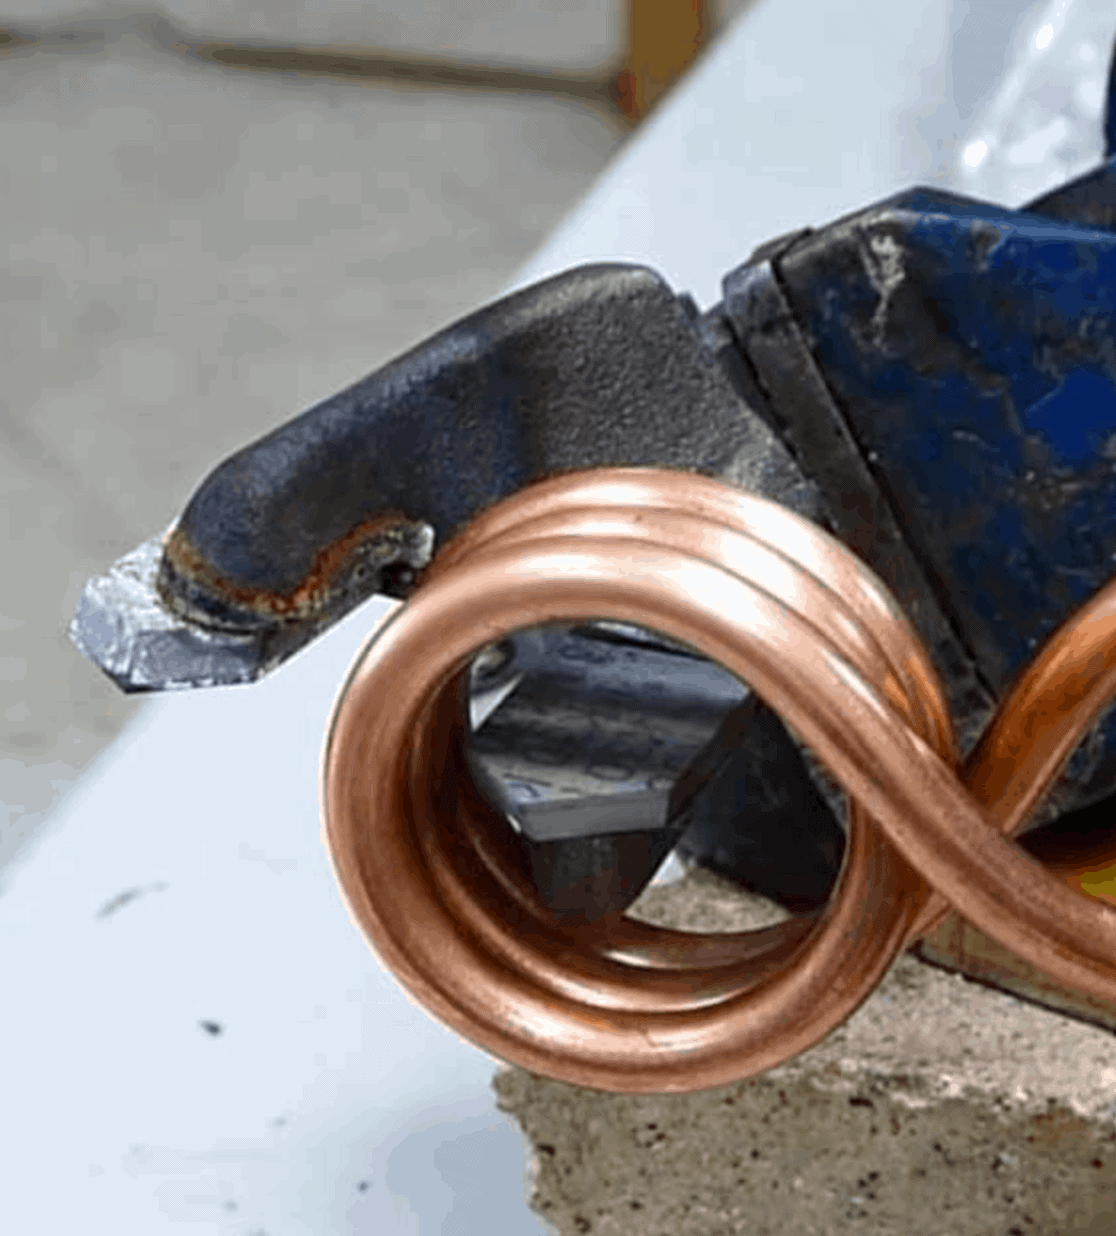
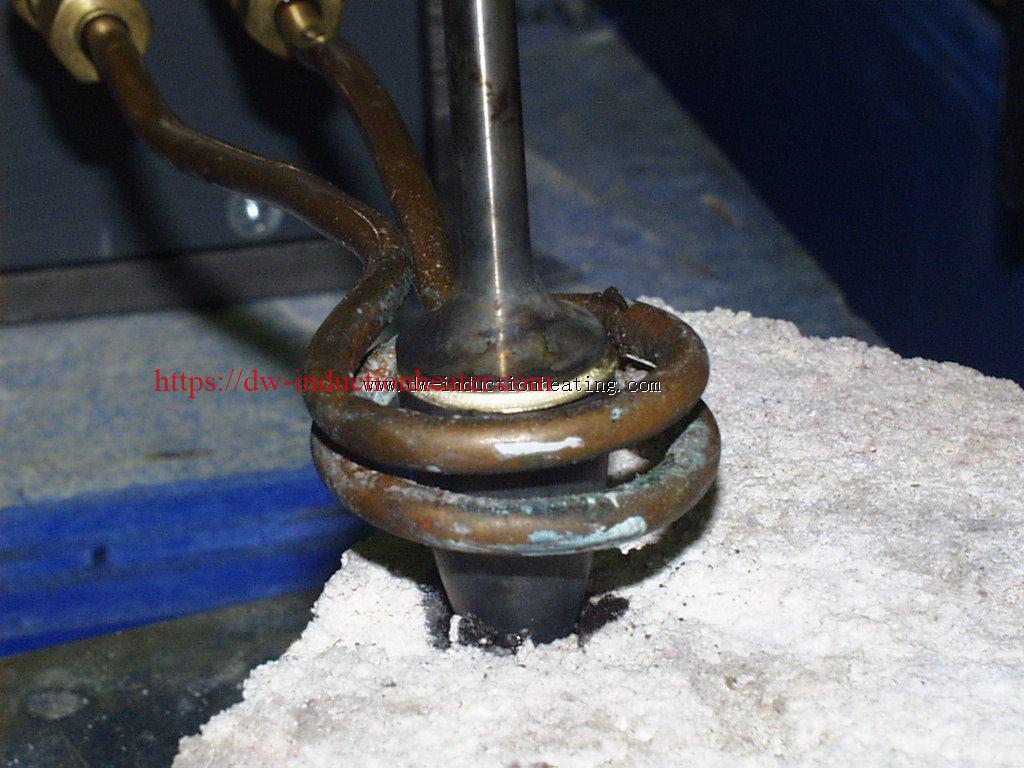
Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
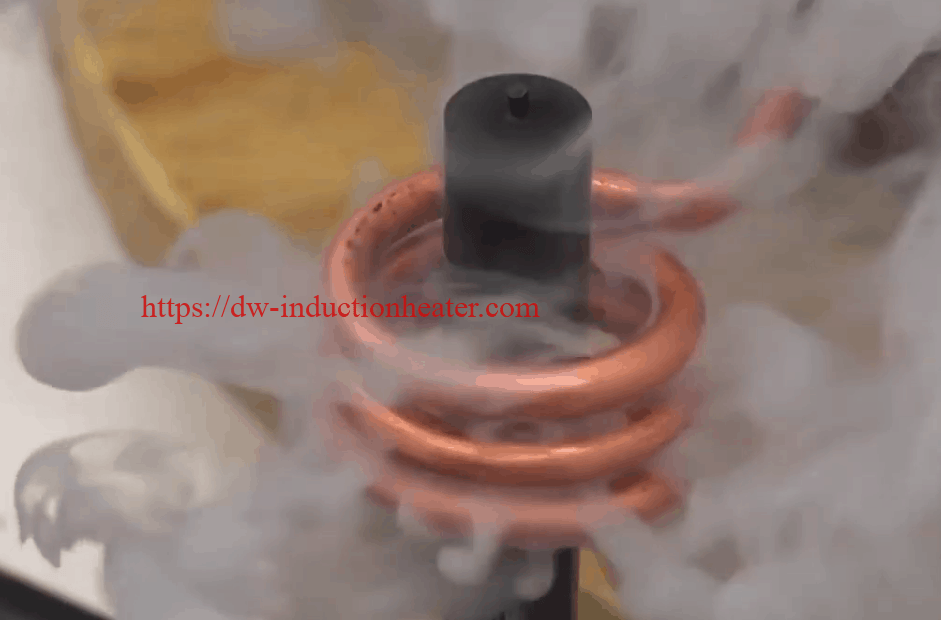
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
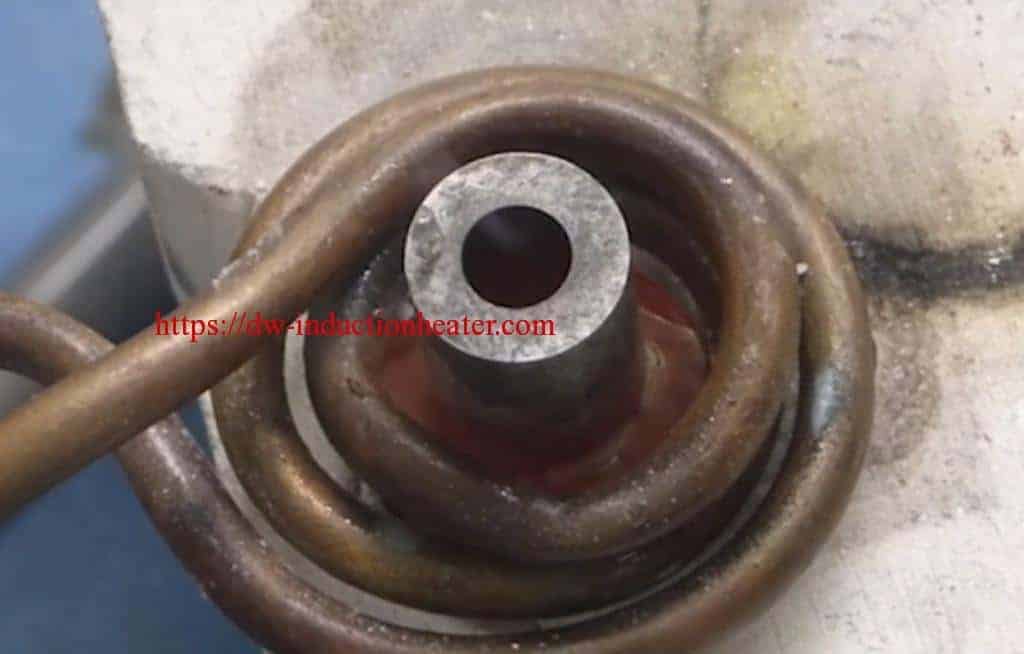
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=241299&_unique_id=6619bfbf80a7e

2024年4月6日星期六

Induction Brazing Steel Parts to Tungsten Carbide Plate

Induction Brazing Steel Parts to Tungsten Carbide Plate

Objective Induction Brazing of Steel Parts to a Tungsten Carbide Plate Equipment DW-UHF-6KW-III handheld induction brazing machine Induction brazing steel parts
Test 1 Materials • Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length • Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness • Alloy: 19.05 mm (0.75″) Brazing discs Power: 4.0 kW Temperature: Approximately 760° C (1400° F) Time: 40 sec
Test 2 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 23 sec
Test 3 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 20-25 sec (Pulsing on/off)
Test 4 Materials • Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes • Alloy: 6.35 mm (0.25″) Brazing discs Power: 1.96 kW Temperature: Approximately 760° C (1400° F)Induction brazing steel carbideInduction brazing steel partsInduction brazing steel parts Time: 20 sec (Pulsing on/off)
Results and Conclusions: Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
  [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=240398&_unique_id=6611e4f0f237c

2024年3月22日星期五

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
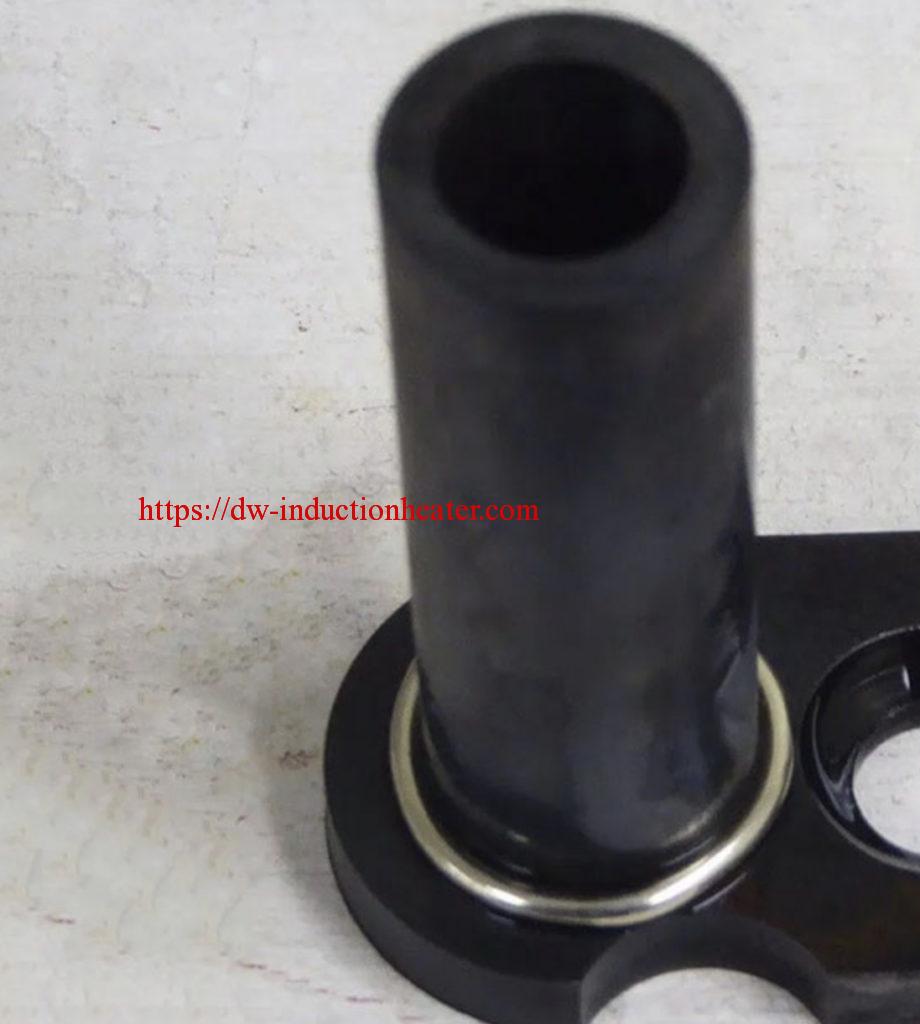
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=237924&_unique_id=65fde60bb551a

2024年3月17日星期日

induction brazing steel carbide cap to shaft

Objective High Frequency Induction brazing steel carbide cap to shaft.  Customer currently uses a torch process, but would like to change to induction brazing in order to reduce scrap and rework and improve the quality of the braze.
Equipment DW-UHF-6kw-III handheld induction brazing heater handheld inductino heater Materials • Carbon steel • magnetic carbide caps • Alloy – EZ Flo 3 paste • Test 1: Shaft Diameter: 0.5” (12.7 mm) • Test 2: Shaft Diameter: 0.375” (9.525mm) • Test 3: Shaft Diameter: 0.312” (7.925mm)
Key Parameters Test 1: Shaft Diameter: 0.5” (12.7mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 3.3 kW Time: 11 seconds
Key Parameters Test 2: Shaft Diameter: 0.375” (9.525mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 1.8 kW Time: 8 seconds
Key Parameters Test 3: Shaft Diameter: 0.312” (7.925mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 1.7 kW Time: 7.5 seconds
Process:
  1. Paste alloy was applied to the cone shape top of each steel shaft.
  2. The cap was set on top and rotated to distribute the paste alloy.
  3. Each assembly was positioned in the coil and heated.
  4. Preliminary heat tests were conducted using tempilaq paint to estimate the heat cycle to 1450 degrees F.
Results/Benefits:
  • Precise control of the time and temperature resulting in improved quality and consistent result
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating
https://dw-inductionheater.com/induction-brazing-steel-carbide-cap-to-shaft.html?feed_id=236996&_unique_id=65f6c1f1b8197

2024年2月23日星期五

induction brazing carbide tip onto steel head teeth

high frequency induction brazing carbide tip onto steel head teeth process

Objective In this application test, induction brazing carbide tip onto steel working head teeth.
Induction Brazing Equipment DW-UHF-10kw induction brazing machine Customized induction heating coil Materials • Steel working head teeth • Brazing paste Key Parameters Power: 4.5 kW Time: 6 seconds
Induction Brazing Process:
  1. Brazing paste is put on the tool
  2. The steel working head teeth are attached.
  3. The assembly is positioned in the three-turn coil.
  4. The assembly is heated.
  5. The joint is completed in 6 seconds.
Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production
  • Safer than flame brazing
Induction Brazing Carbide Tipping is a specific brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. When using induction heating, the tipping material is brazed to the base material with temperatures up to 1900F.
https://dw-inductionheater.com/induction-brazing-carbide-tip-onto-steel-head-teeth.html?feed_id=234638&_unique_id=65d8c3deb446b

2023年11月16日星期四

Induction Brazing Carbide

Induction Brazing Carbide File Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 550 kHz Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.   https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d

2023年11月9日星期四

Brazing carbide shaft with induction

Brazing carbide shaft with induction Objective: Braze a carbide shaft to a steel tube Material: Carbide shaft 1/8" to 1" diameter (varying sizes) Steel tube 3/8" to 1 ¼" OD Silver solder braze Temperature: indicating paint Temperature: 1400 °F for 60 seconds Frequency300 kHz Equipment: DW-UHF-6KW-III, 150-400 kHz solid state induction heating system equipped with a remote heat station containing two 0.66 μF capacitors (total 1.32 μF) A multi-turn helical coil Process: Silver solder is applied to where the carbide shaft and steel tube meet. The clearance between the two parts is approximately .0005". A small piece of solder braze is placed on the part and then the part is heated. It takes about 60 seconds to flow the braze with the best heat migration and solder flow. Even though the part can be heated faster, optimal results are obtained at 60 seconds. Results/Benefits: Induction heating provides even, precise heat. Precise directed heat is required for the solder braze to flow evenly around the part to assure a good joint. https://dw-inductionheater.com/brazing-carbide-shaft-with-induction.html?feed_id=230466&_unique_id=654d8320ad50f

2023年11月7日星期二

induction brazing carbide tip onto steel head teeth

high frequency induction brazing carbide tip onto steel head teeth process

Objective In this application test, induction brazing carbide tip onto steel working head teeth.
Induction Brazing Equipment DW-UHF-10kw induction brazing machine Customized induction heating coil Materials • Steel working head teeth • Brazing paste Key Parameters Power: 4.5 kW Time: 6 seconds
Induction Brazing Process:
  1. Brazing paste is put on the tool
  2. The steel working head teeth are attached.
  3. The assembly is positioned in the three-turn coil.
  4. The assembly is heated.
  5. The joint is completed in 6 seconds.
Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production
  • Safer than flame brazing
Induction Brazing Carbide Tipping is a specific brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. When using induction heating, the tipping material is brazed to the base material with temperatures up to 1900F.

2023年11月4日星期六

Brazing Carbide To Steel With Induction

Brazing Carbide To Steel With Induction  Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application Material : • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 252 kHz Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat. https://dw-inductionheater.com/brazing-carbide-to-steel-with-induction.html?feed_id=230166&_unique_id=65465eee1c0f6

2023年11月3日星期五

Brazing Carbide Tool Tips With Induction

Brazing Carbide Tool Tips With Induction  Objective: Attaching carbide cutters to a steel meat cutter impeller Material carbide blocks; steel shank fitting Temperature 1400 °F (760 °C) Frequency 300 kHz Equipment DW-UHF-30KW induction heating systems including: Induction heating coil Workhead: two-cap 1.0μF (Total 0.5 μF) Process The entire part is placed in a five-turn helical coil, the power is applied until the part is heated to the required temperature and a uniform heat pattern is achieved. The coil allows for easy fixturing and uniformity of heating between the carbide and the steel shank for a premium braze joint. Results/Benefits Precision: Due to the size of the induction coil, the process allows for precise placement of the carbides on the steel shanks Economy: Power is consumed only during the heat cycle Repeatability: joint quality is maintained in this repeatable process https://dw-inductionheater.com/brazing-carbide-tool-tips-with-induction.html?feed_id=230106&_unique_id=6544f15012f4e

2023年10月28日星期六

Brazing Carbide To Steel Shank

Brazing Carbide To Steel Shank with Induction Objective :Brazing carbide teeth to a steel jaw in less than 5 minutes Material: Steel pipe jaw, 0.5” (12.7mm) dia, 1.25” (31.75mm) long, 0.25”(6.35mm) thick carbide teeth, black flux and silver copper braze shims Temperature: 1292ºF (700ºC) Frequency: 300kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing one 0.66μF capacitor • An induction heating coil designed and developed specifically for this application. Process: A two turn rectangular helical coil is used to heat the carbide and steel to 1292ºF (700ºC) for 4 to 5 minutes. Three braze shims control the amount of braze and the even heat allows for a good flow of braze creating an aesthetically pleasing bond. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Consistent, repeatable aesthetically pleasing brazes • Even distribution of heating https://dw-inductionheater.com/brazing-carbide-to-steel-shank.html?feed_id=229806&_unique_id=653dcd6ce2c3a

2023年10月22日星期日

Induction Brazing Steel To Carbide Plate

Induction Brazing Steel To Carbide Plate Objective Brazing a steel piston valve assembly Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze Temperature 1350 ºF Frequency 100 kHz Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF • An induction heating coil designed and developed specifically for this application. Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces. Results/Benefits Induction heating provides: • Rapid localized heat, which can minimize oxidation and reduce cleaning after joining • Hands-free heating that involves no operator skill for manufacturing • Clean and controllable joints • Produces high quality repeatable parts https://dw-inductionheater.com/induction-brazing-steel-to-carbide.html?feed_id=229446&_unique_id=65353b9610f85

2023年9月17日星期日

Brazing Carbide To Steel Shank

Brazing Carbide To Steel Shank with Induction Objective :Brazing carbide teeth to a steel jaw in less than 5 minutes Material: Steel pipe jaw, 0.5” (12.7mm) dia, 1.25” (31.75mm) long, 0.25”(6.35mm) thick carbide teeth, black flux and silver copper braze shims Temperature: 1292ºF (700ºC) Frequency: 300kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing one 0.66μF capacitor • An induction heating coil designed and developed specifically for this application. Process: A two turn rectangular helical coil is used to heat the carbide and steel to 1292ºF (700ºC) for 4 to 5 minutes. Three braze shims control the amount of braze and the even heat allows for a good flow of braze creating an aesthetically pleasing bond. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Consistent, repeatable aesthetically pleasing brazes • Even distribution of heating

2023年9月14日星期四

Brazing Carbide To Steel With Induction

Brazing Carbide To Steel With Induction  Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application Material : • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 252 kHz Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.

2023年9月10日星期日

Induction Brazing Carbide

Induction Brazing Carbide File Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 550 kHz Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.  

2023年9月3日星期日

induction brazing carbide tip onto steel head teeth

high frequency induction brazing carbide tip onto steel head teeth process

Objective In this application test, induction brazing carbide tip onto steel working head teeth.
Induction Brazing Equipment DW-UHF-10kw induction brazing machine Customized induction heating coil Materials • Steel working head teeth • Brazing paste Key Parameters Power: 4.5 kW Time: 6 seconds
Induction Brazing Process:
  1. Brazing paste is put on the tool
  2. The steel working head teeth are attached.
  3. The assembly is positioned in the three-turn coil.
  4. The assembly is heated.
  5. The joint is completed in 6 seconds.
Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production
  • Safer than flame brazing
Induction Brazing Carbide Tipping is a specific brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. When using induction heating, the tipping material is brazed to the base material with temperatures up to 1900F.

2023年8月30日星期三

induction brazing steel carbide cap to shaft

Objective High Frequency Induction brazing steel carbide cap to shaft.  Customer currently uses a torch process, but would like to change to induction brazing in order to reduce scrap and rework and improve the quality of the braze.
Equipment DW-UHF-6kw-III handheld induction brazing heater handheld inductino heater Materials • Carbon steel • magnetic carbide caps • Alloy – EZ Flo 3 paste • Test 1: Shaft Diameter: 0.5” (12.7 mm) • Test 2: Shaft Diameter: 0.375” (9.525mm) • Test 3: Shaft Diameter: 0.312” (7.925mm)
Key Parameters Test 1: Shaft Diameter: 0.5” (12.7mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 3.3 kW Time: 11 seconds
Key Parameters Test 2: Shaft Diameter: 0.375” (9.525mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 1.8 kW Time: 8 seconds
Key Parameters Test 3: Shaft Diameter: 0.312” (7.925mm) Temperature: Approximately 1450°F (788°C) Power: Pre-curie – 1.7 kW Time: 7.5 seconds
Process:
  1. Paste alloy was applied to the cone shape top of each steel shaft.
  2. The cap was set on top and rotated to distribute the paste alloy.
  3. Each assembly was positioned in the coil and heated.
  4. Preliminary heat tests were conducted using tempilaq paint to estimate the heat cycle to 1450 degrees F.
Results/Benefits:
  • Precise control of the time and temperature resulting in improved quality and consistent result
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.