 Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/brazing-carbide-to-steel-with-induction.html?feed_id=230166&_unique_id=65465eee1c0f6
2023年11月4日星期六
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/brazing-carbide-to-steel-with-induction.html?feed_id=230166&_unique_id=65465eee1c0f6

2023年11月1日星期三
Brazing Carbide-Steel Tool with Induction
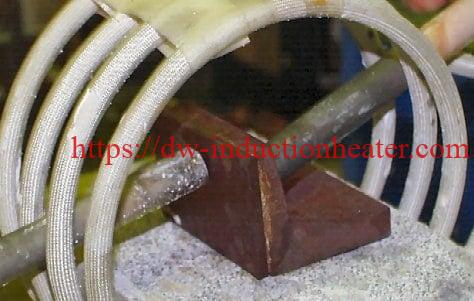 Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
https://dw-inductionheater.com/brazing-carbide-steel-tool-with-induction.html?feed_id=229986&_unique_id=6542162c13fad
2023年9月14日星期四
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年9月12日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年8月13日星期日
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年4月26日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年4月6日星期四
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年3月10日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月31日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月21日星期六
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年1月16日星期一
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月12日星期四
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月6日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年11月9日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年10月30日星期日
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年10月28日星期五
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年7月22日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年7月9日星期六
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年5月25日星期三
Brazing Carbide To Steel With Induction
Brazing Carbide To Steel With Induction
Objective: Braze carbide rotary file assemblies with uniform concentricity in an aerospace application
Material :
• Carbide blank
• High speed steel shank
• Temperature indicating paint
• Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 252 kHz
Equipment DW-UHF-10kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年5月24日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.