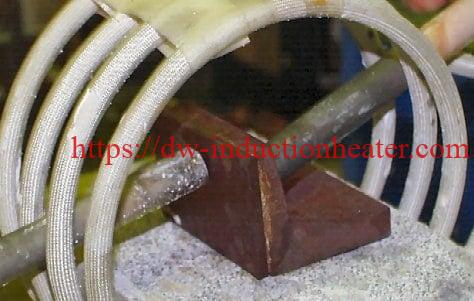
 Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
https://dw-inductionheater.com/brazing-carbide-steel-tool-with-induction.html?feed_id=229986&_unique_id=6542162c13fad
显示标签为“BrazingCarbideSteelToolwithInduction”的博文。显示所有博文
显示标签为“BrazingCarbideSteelToolwithInduction”的博文。显示所有博文
2023年11月1日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
https://dw-inductionheater.com/brazing-carbide-steel-tool-with-induction.html?feed_id=229986&_unique_id=6542162c13fad

2023年9月12日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年4月26日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年3月10日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月31日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月16日星期一
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月12日星期四
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2023年1月6日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年11月9日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年10月30日星期日
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年7月22日星期五
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年7月9日星期六
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年5月24日星期二
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年5月18日星期三
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2022年3月19日星期六
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2021年12月26日星期日
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
2021年12月16日星期四
Brazing Carbide-Steel Tool with Induction
Brazing Carbide-Steel Tool with Induction
Objective: Provide a solution to this steel-carbide brazing application Material • Body 10mm; carbide tip 57 x 35 x 3 mm • Braze shim • Braze flux white
Temperature: 750°C (1382ºF)
Frequency: 150 kHz
Equipment DW-UHF-20KW induction heating system, equipped with a remote heat station containing (2) 1.0 μF capacitors (for a total of 0.5 μF) A 4.5" helical induction heating coil designed and developed specifically for this application.
Process: The body shim and carbide are cleaned and braze flux as applied to the entire surface of the assembly. The parts are placed together in the induction coil. Two ceramic tubes are then placed thru the coil opposing each other to hold the parts during heating. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows in the joint.
Results/Benefits
• targeted heating of the braze joint is efficient
• flameless process is more precise, controllable
• results are reproducible
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.