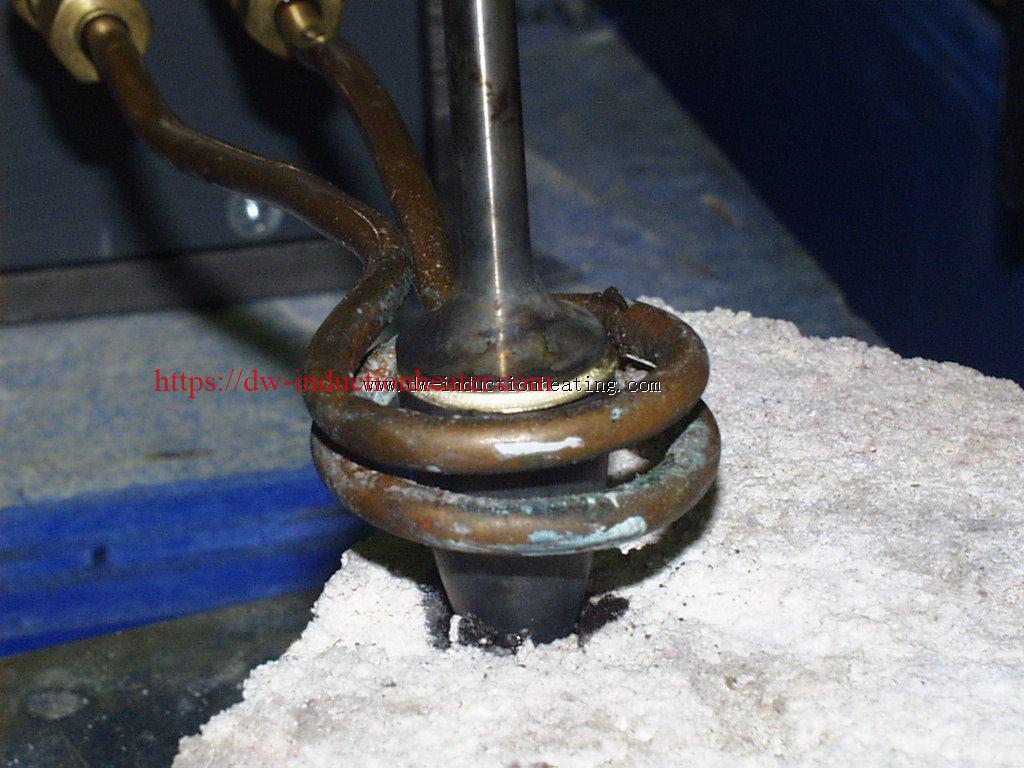
 Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d
2023年11月16日星期四
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d

High Frequency Induction Brazing Diamond Inserts
 High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
https://dw-inductionheater.com/high-frequency-induction-brazing-diamond-inserts.html?feed_id=230826&_unique_id=6556150324734
2023年9月10日星期日
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年6月21日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年5月5日星期五
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2023年3月1日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年1月12日星期四
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年12月14日星期三
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2022年11月16日星期三
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2022年8月19日星期五
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年7月26日星期二
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2022年5月31日星期二
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年5月19日星期四
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2022年4月5日星期二
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2022年2月26日星期六
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年2月16日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年2月15日星期二
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年1月12日星期三
High Frequency Induction Brazing Diamond Inserts
High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
2021年12月23日星期四
High Frequency Brazing Equipment
High Frequency Brazing Equipment
Applications
*Quick quenching *Hardening for small depth *Brazing for tiny workpiece *Heating tiny workpiece *Diamond blade brazing to segments, carbon steel blade brazing, PCBN blade brazing etc.*Glasses steel alloys frame brazing, small bearings quenching, annealing etc.
*Jewelries brazing, watchcase annealing and clock outer quenching.
*Electronics products brazing/welding/heating: fine and expensive products like bulb filaments etc.
*Precise mechanical parts brazing/heating.
*Stainless steel strip annealing etc.
|
Model |
DW-UHF-20KW |
|
|
Input Voltage |
3 phases,380V±10%,50/60Hz |
|
|
Output Power |
20KW |
|
|
Oscillate frequency |
50-250KHz |
|
|
Input Current |
3-30A |
|
|
Cooling Water |
>0.2 MPa, 5 L/Min, |
|
|
Weight |
55KG |
|
|
Size |
Main |
590X300X530mm |
|
Head |
520X255X380MM |
|
Main characteristics:
1. With high frequency up to 50-250KHz.the quenching thickness can be controlled lower than 1mm ,and very tiny parts can be easily heated. 2. IGBT and inverting technologies of third generation been used, higher reliability and lower maintenance cost. 3. 100% duty cycle, continuous working is allowed at Max power output. 4. Light weight,55KG only. Small and portable.
5. Constant current or constant power status can be selected accordingly to achieve higher heating efficiency.
[wpforms id="3947"]
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.