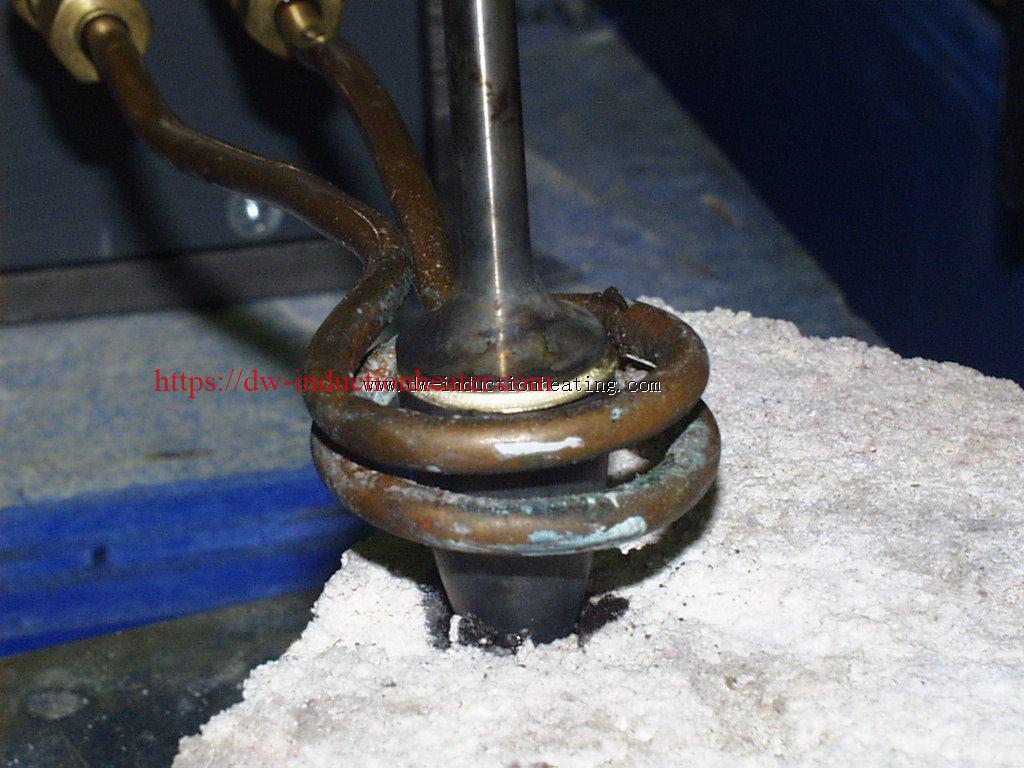
 Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d
2023年11月16日星期四
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d

2023年9月10日星期日
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年6月21日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年3月1日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2023年1月12日星期四
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年8月19日星期五
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年5月31日星期二
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年2月26日星期六
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年2月16日星期三
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
2022年2月15日星期二
Induction Brazing Carbide
Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.