显示标签为“highfrequencybrazingcarbide”的博文。显示所有博文

2024年5月4日星期六

Induction Brazing Carbide To Stainless Steel

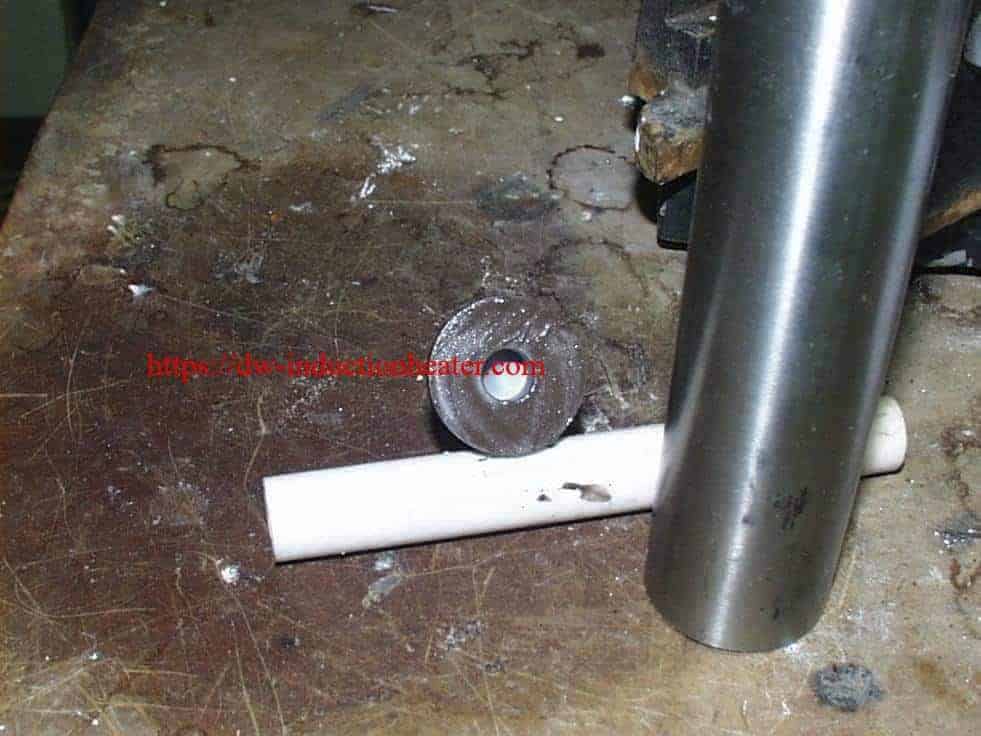
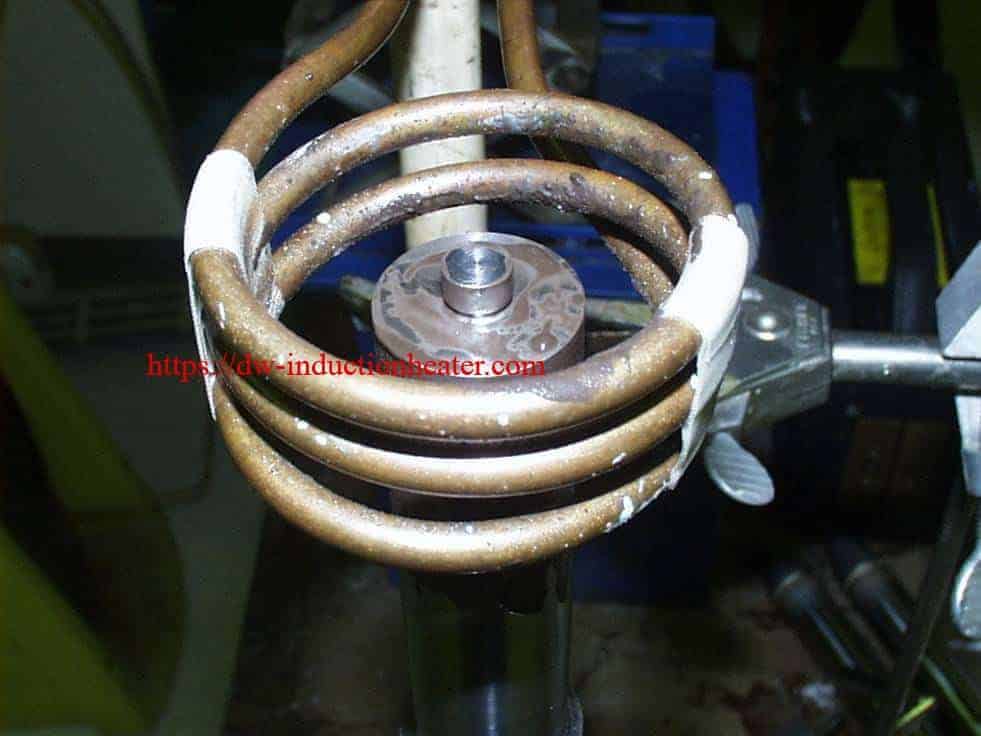
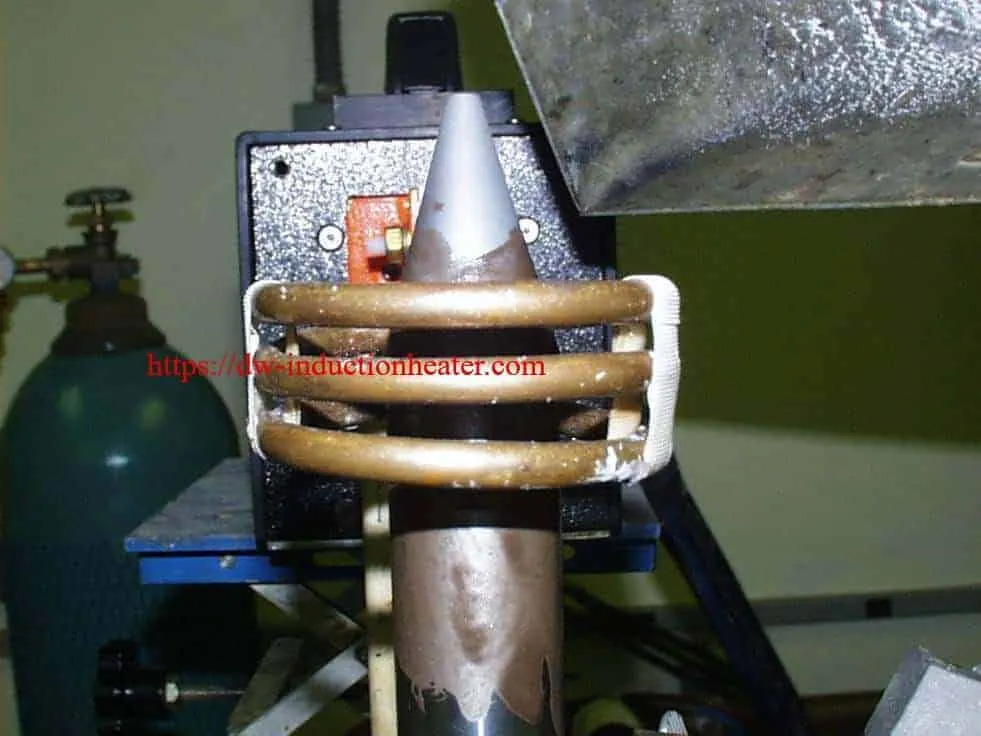
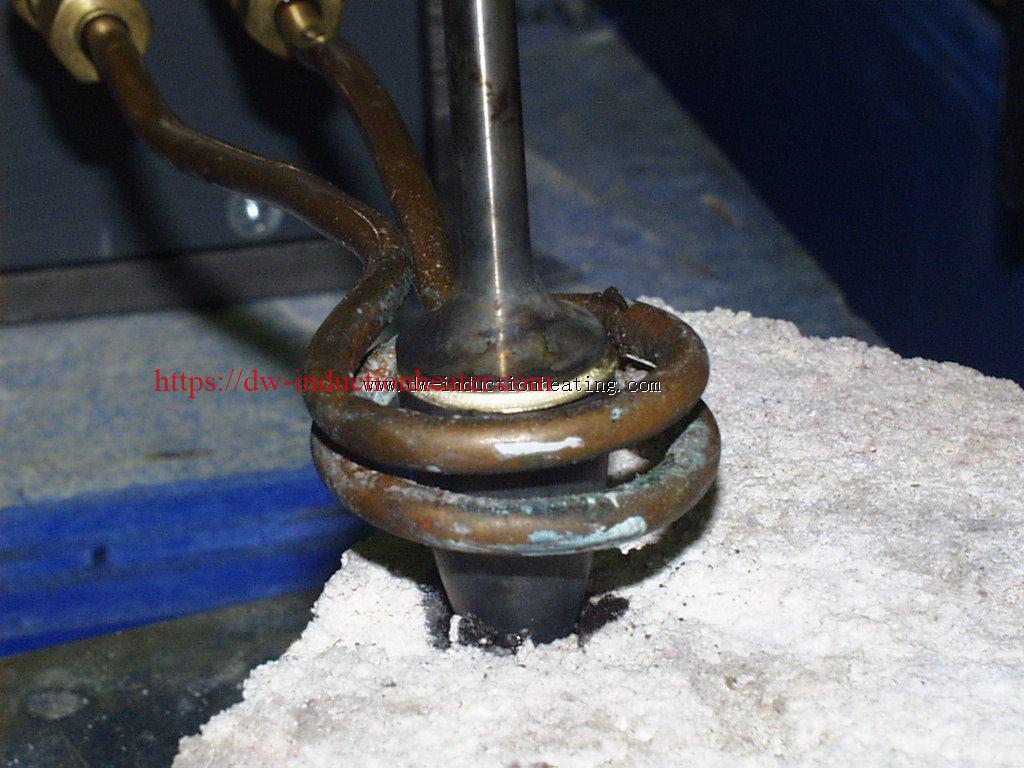
Induction Brazing Carbide To Stainless Steel Shaft With IGBT Heating Units Objective Brazing a cone shaped carbide to a stainless steel shaft for a digger Material Cone shaped carbide 1.12” (28.4mm) dia, 1.5”(38.1mm) tall, stainless steel shaft 1.12” (28.4mm) dia and various length, black brazing flux and braze shims Temperature 1500 ºF (815 ºC) Frequency 277 kHz Equipment • DW-UHF-10 kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to braze the carbide to the shaft. The steel shaft is fluxed and the braze shim placed on top. The carbide tip is fluxed and placed on top of the shim, lining up the countersunk hole in the carbide. The hole is not fluxed because the flux outgases and causes the carbide to build up pressure and attempt to repel from the shaft. Power is applied for 85 seconds for the braze shim to flow and make a good joint. DAWEI’s customer has a customer who is unhappy with the braze quality of their digger so our customer is looking for a better quality brazing process. DAWEI’s customer is very happy with the sample brazed diggers and the help he received from the Ameritherm lab in developing his brazing process. Results/Benefits Induction heating provides: • Rapid localized heating only where needed • Creates clean, controllable joints • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating brazing carbide to shaft             induction brazing carbide to shaft               brazing carbide to stainless steel shaft https://dw-inductionheater.com/induction-brazing-carbide-to-stainless-steel.html?feed_id=244304&_unique_id=6636501477c8b
2024年4月12日星期五

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

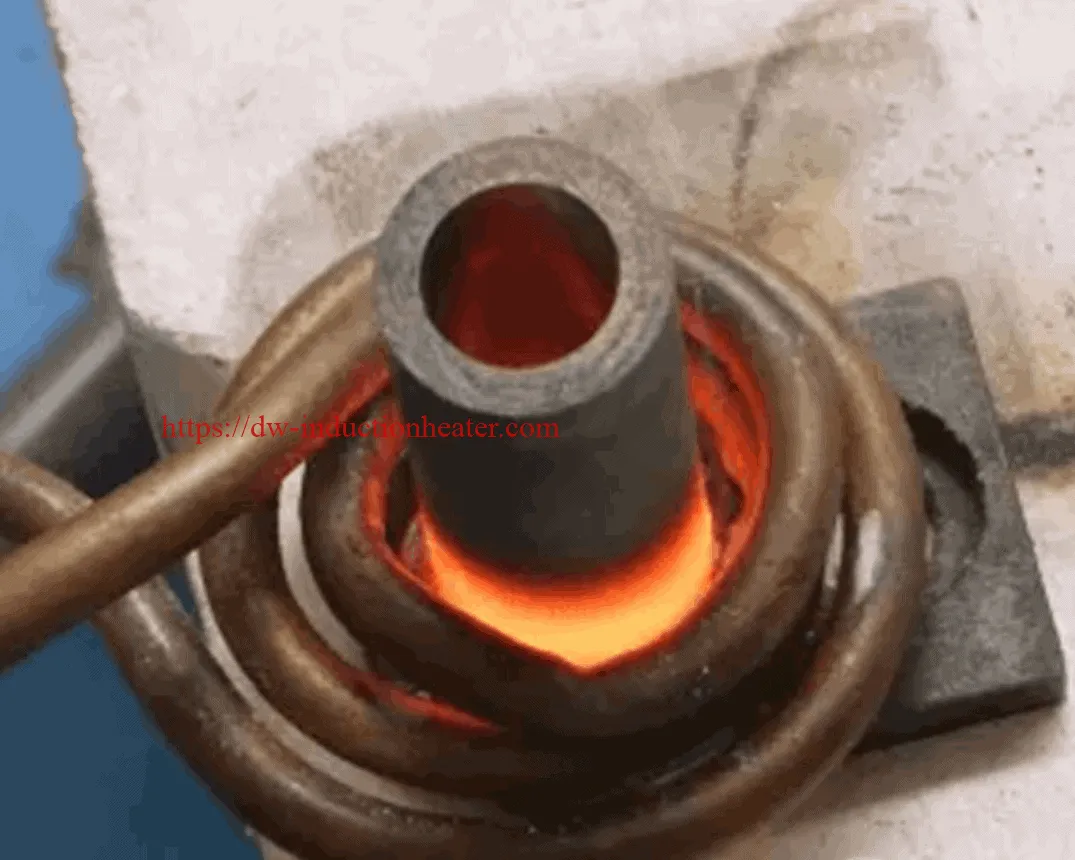
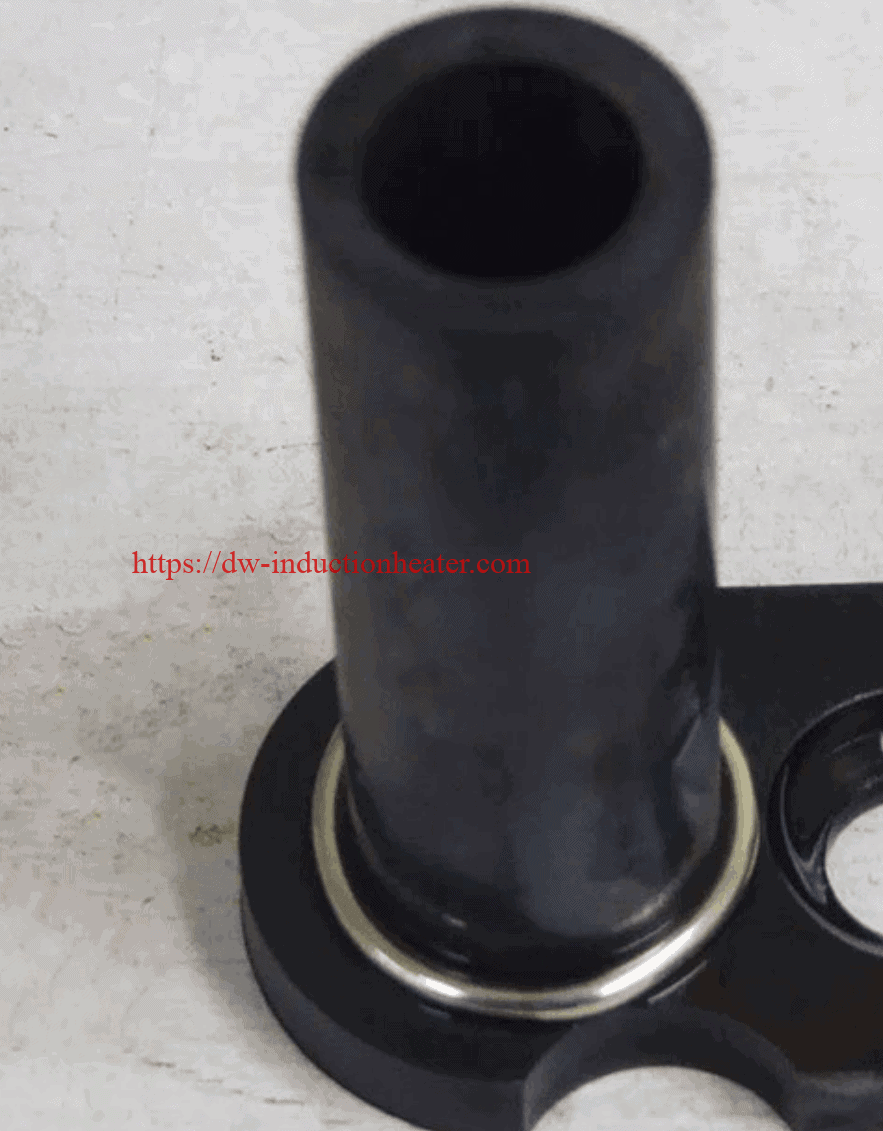
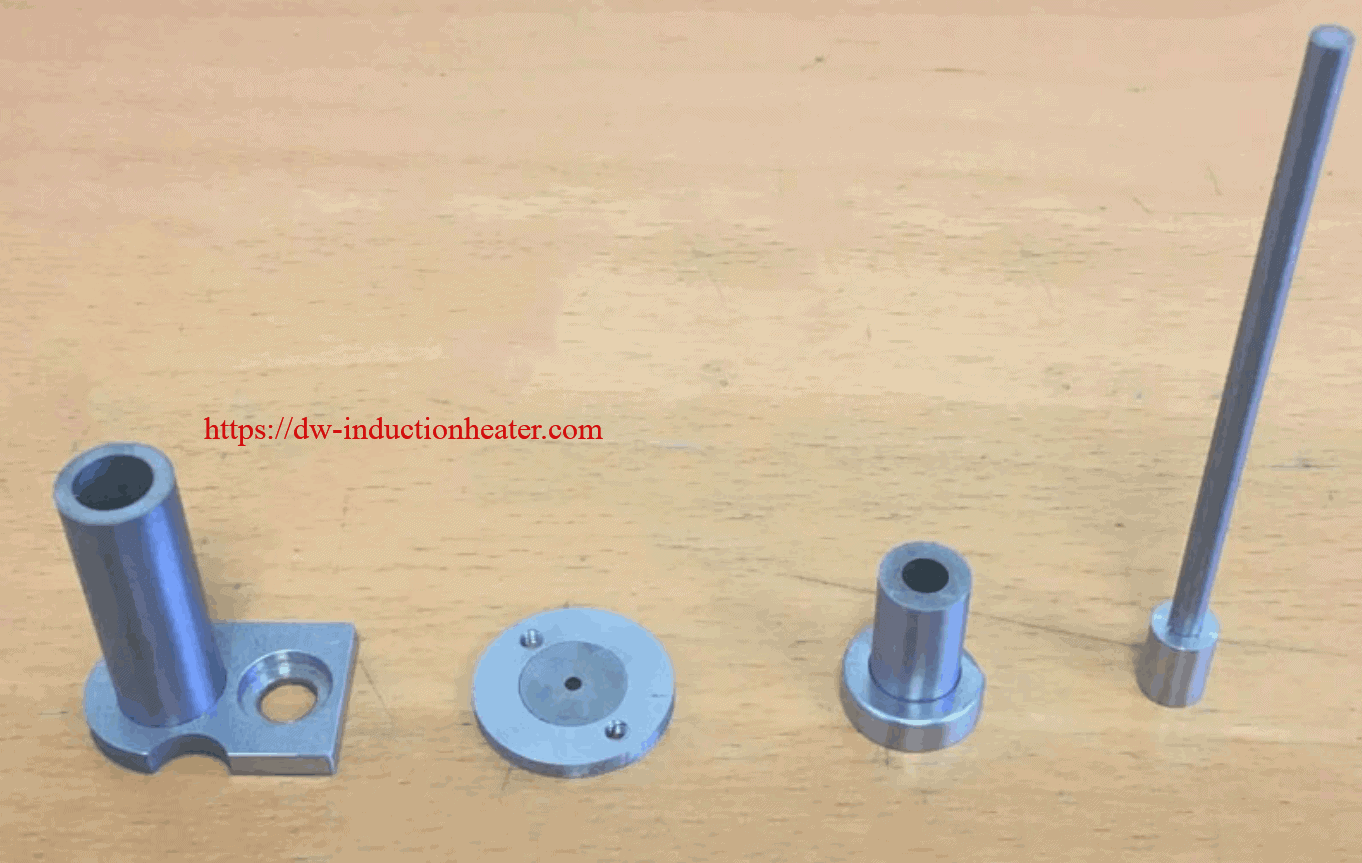
Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=241299&_unique_id=6619bfbf80a7e

2024年3月22日星期五

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=237924&_unique_id=65fde60bb551a

2023年11月16日星期四

Induction Brazing Carbide

Induction Brazing Carbide File Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 550 kHz Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.   https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=230856&_unique_id=6556cbb53479d

2023年10月28日星期六

Brazing Carbide To Steel Shank

Brazing Carbide To Steel Shank with Induction Objective :Brazing carbide teeth to a steel jaw in less than 5 minutes Material: Steel pipe jaw, 0.5” (12.7mm) dia, 1.25” (31.75mm) long, 0.25”(6.35mm) thick carbide teeth, black flux and silver copper braze shims Temperature: 1292ºF (700ºC) Frequency: 300kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing one 0.66μF capacitor • An induction heating coil designed and developed specifically for this application. Process: A two turn rectangular helical coil is used to heat the carbide and steel to 1292ºF (700ºC) for 4 to 5 minutes. Three braze shims control the amount of braze and the even heat allows for a good flow of braze creating an aesthetically pleasing bond. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Consistent, repeatable aesthetically pleasing brazes • Even distribution of heating https://dw-inductionheater.com/brazing-carbide-to-steel-shank.html?feed_id=229806&_unique_id=653dcd6ce2c3a

2023年9月17日星期日

Brazing Carbide To Steel Shank

Brazing Carbide To Steel Shank with Induction Objective :Brazing carbide teeth to a steel jaw in less than 5 minutes Material: Steel pipe jaw, 0.5” (12.7mm) dia, 1.25” (31.75mm) long, 0.25”(6.35mm) thick carbide teeth, black flux and silver copper braze shims Temperature: 1292ºF (700ºC) Frequency: 300kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing one 0.66μF capacitor • An induction heating coil designed and developed specifically for this application. Process: A two turn rectangular helical coil is used to heat the carbide and steel to 1292ºF (700ºC) for 4 to 5 minutes. Three braze shims control the amount of braze and the even heat allows for a good flow of braze creating an aesthetically pleasing bond. Results/Benefits Induction heating provides: • Hands-free heating that involves no operator skill for manufacturing • Consistent, repeatable aesthetically pleasing brazes • Even distribution of heating

2023年9月10日星期日

Induction Brazing Carbide

Induction Brazing Carbide File Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 550 kHz Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.  

2023年8月21日星期一

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=224236&_unique_id=64e316e592f81

2023年8月12日星期六

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature

2023年7月30日星期日

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=221161&_unique_id=64c6749551518

2023年6月21日星期三

Induction Brazing Carbide

Induction Brazing Carbide File Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux Temperature 1400°F (760°C) Frequency 550 kHz Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application. Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved. Results/Benefits • Repeatable, consistent precise heat.  

2023年4月26日星期三

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel

2023年4月1日星期六

Induction Brazing Carbide To Stainless Steel

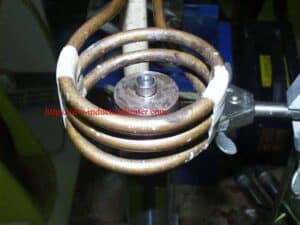
Induction Brazing Carbide To Stainless Steel Shaft With IGBT Heating Units Objective Brazing a cone shaped carbide to a stainless steel shaft for a digger Material Cone shaped carbide 1.12” (28.4mm) dia, 1.5”(38.1mm) tall, stainless steel shaft 1.12” (28.4mm) dia and various length, black brazing flux and braze shims Temperature 1500 ºF (815 ºC) Frequency 277 kHz Equipment • DW-UHF-10 kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to braze the carbide to the shaft. The steel shaft is fluxed and the braze shim placed on top. The carbide tip is fluxed and placed on top of the shim, lining up the countersunk hole in the carbide. The hole is not fluxed because the flux outgases and causes the carbide to build up pressure and attempt to repel from the shaft. Power is applied for 85 seconds for the braze shim to flow and make a good joint. DAWEI’s customer has a customer who is unhappy with the braze quality of their digger so our customer is looking for a better quality brazing process. DAWEI’s customer is very happy with the sample brazed diggers and the help he received from the Ameritherm lab in developing his brazing process. Results/Benefits Induction heating provides: • Rapid localized heating only where needed • Creates clean, controllable joints • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating brazing carbide to shaft             induction brazing carbide to shaft               brazing carbide to stainless steel shaft
2023年3月1日星期三

Induction Brazing Carbide

Induction Brazing Carbide File

Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application

Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux

Temperature 1400°F (760°C)

Frequency 550 kHz

Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.

Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.

Results/Benefits • Repeatable, consistent precise heat.


2023年2月22日星期三

Induction Brazing Carbide To Stainless Steel

Induction Brazing Carbide To Stainless Steel Shaft With IGBT Heating Units

Objective Brazing a cone shaped carbide to a stainless steel shaft for a digger
Material Cone shaped carbide 1.12” (28.4mm) dia, 1.5”(38.1mm) tall, stainless steel shaft 1.12” (28.4mm) dia and various length, black brazing flux and braze shims
Temperature 1500 ºF (815 ºC)
Frequency 277 kHz
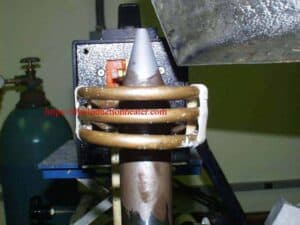
Equipment • DW-UHF-10 kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF
• An induction heating coil designed and developed specifically for this application.
Process A three turn helical coil is used to braze the carbide to the shaft. The steel shaft is fluxed and the braze shim placed on top. The carbide tip is fluxed and placed on top of the shim, lining up the countersunk hole in the carbide. The hole is not fluxed because the flux outgases and causes the carbide to build up pressure and attempt to repel from the shaft. Power is applied for 85 seconds for the braze shim to flow and make a good joint.
DAWEI’s customer has a customer who is unhappy with the braze quality of their digger so our customer is looking for a better quality brazing process. DAWEI’s customer is very happy with the sample brazed diggers and the help he received from the Ameritherm lab in developing his brazing process.
Results/Benefits Induction heating provides:
• Rapid localized heating only where needed
• Creates clean, controllable joints
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
brazing carbide to shaft


induction brazing carbide to shaft


brazing carbide to stainless steel shaft

2023年1月23日星期一

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.