显示标签为“brazingcarbidemachine”的博文。显示所有博文

2024年3月22日星期五

Induction Brazing Carbide To Steel

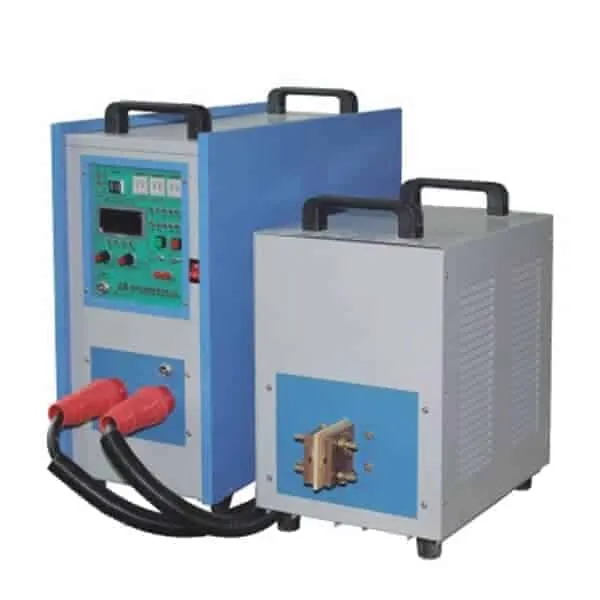
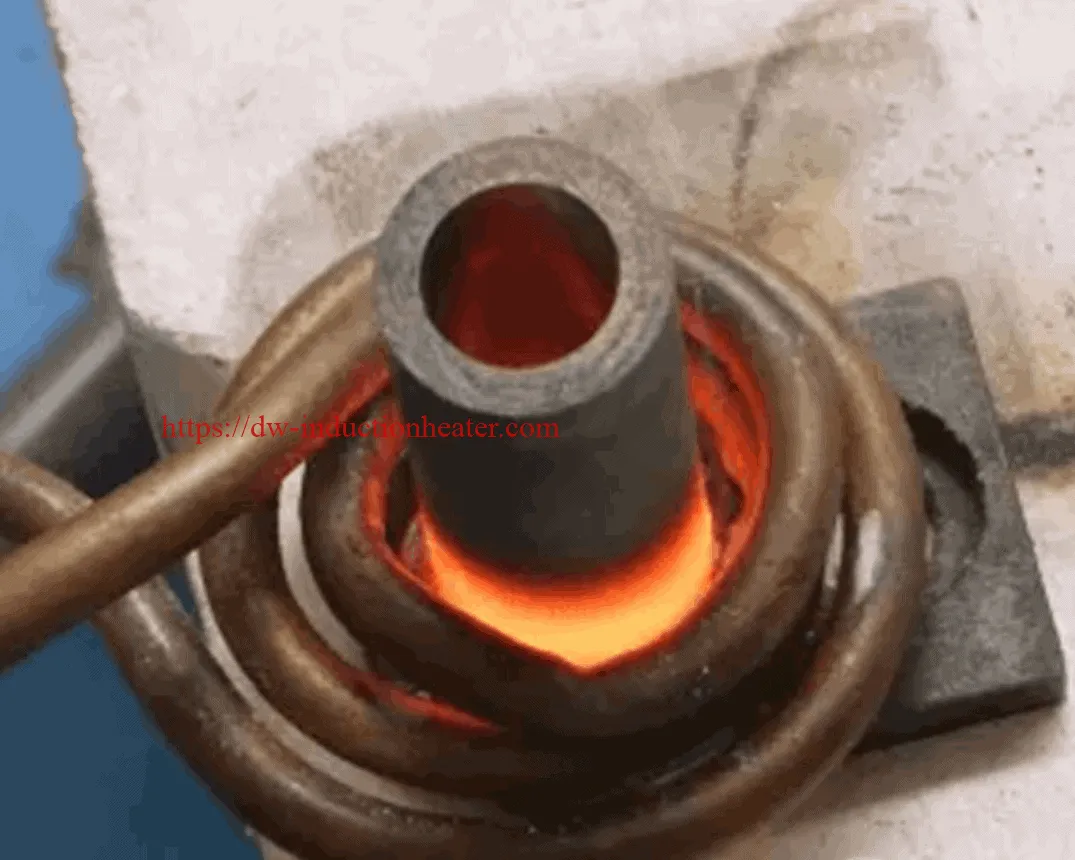
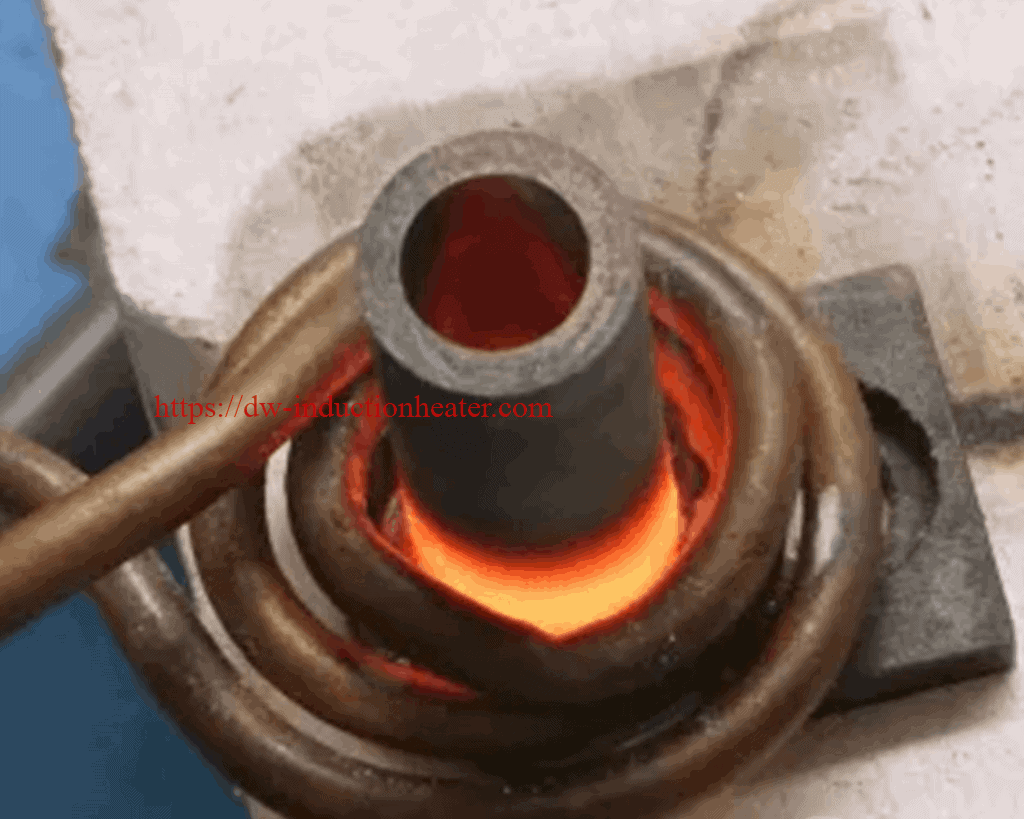
Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=237924&_unique_id=65fde60bb551a

2024年3月18日星期一

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
https://dw-inductionheater.com/induction-brazing-carbide-to-steelbrazing-tungsten-carbide-to-stainless-steel.html?feed_id=237324&_unique_id=65f8e6a800a0b

2023年9月18日星期一

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.

2023年8月12日星期六

Induction Brazing Carbide To Steel

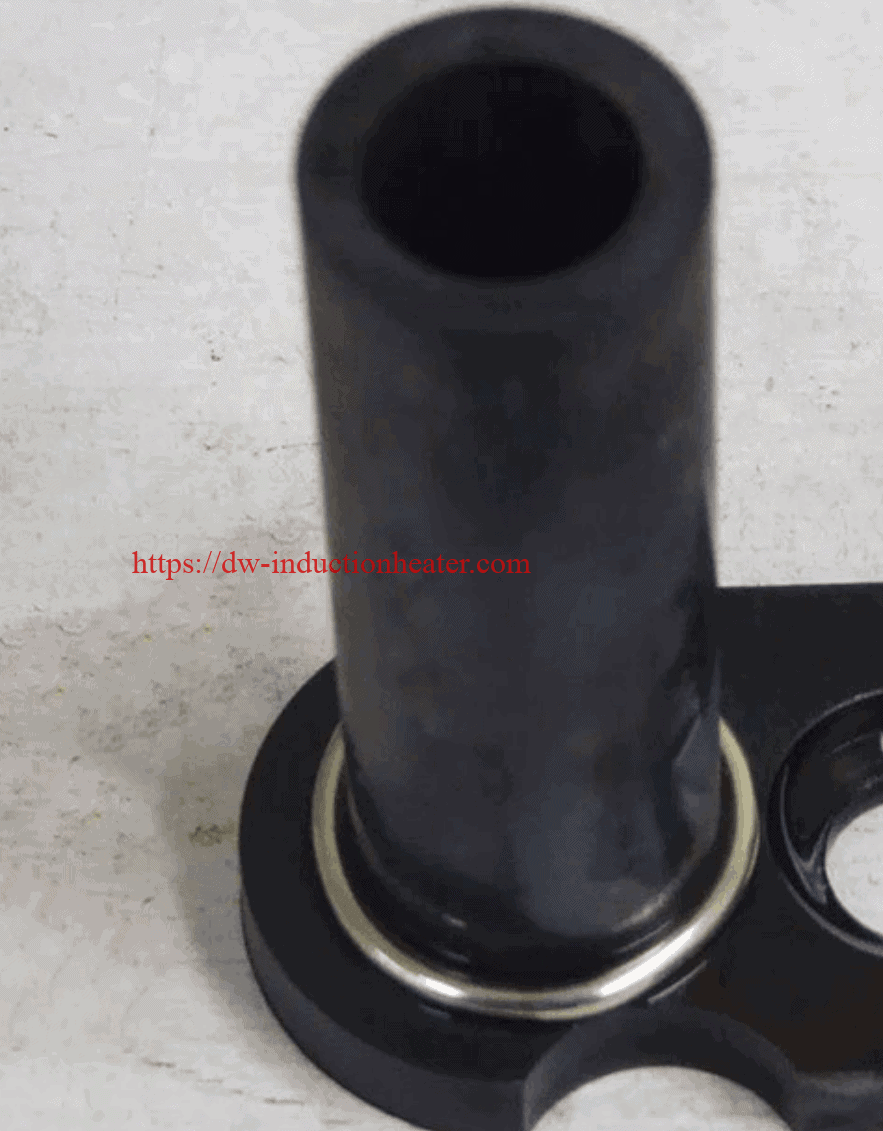
Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
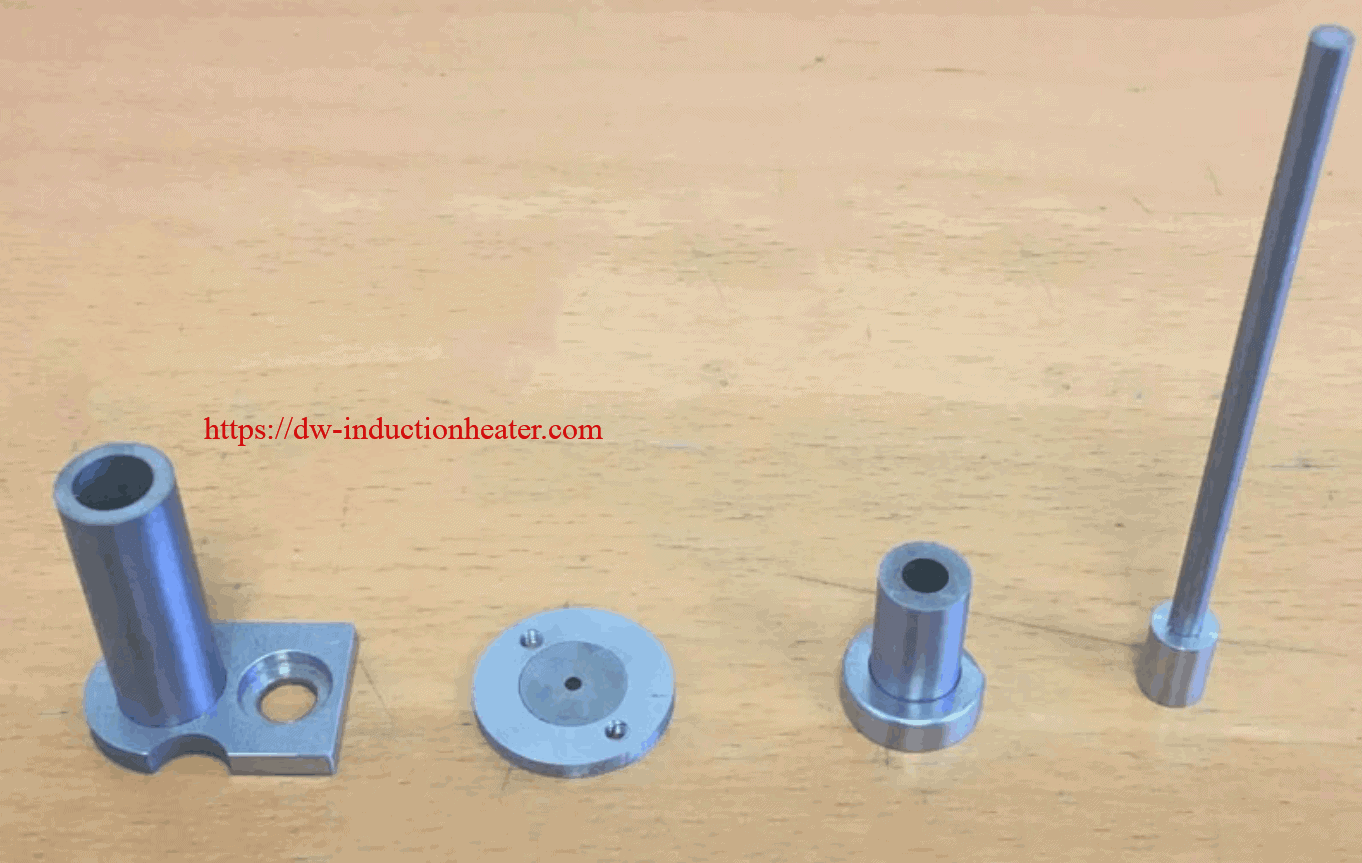
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature

2023年7月30日星期日

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=221161&_unique_id=64c6749551518

2023年7月26日星期三

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
https://dw-inductionheater.com/induction-brazing-carbide-to-steelbrazing-tungsten-carbide-to-stainless-steel.html?feed_id=220561&_unique_id=64c1743521066

2023年4月30日星期日

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.