显示标签为“brazingsteeltocarbide”的博文。显示所有博文

2024年3月18日星期一

Induction Brazing Carbide to Steel

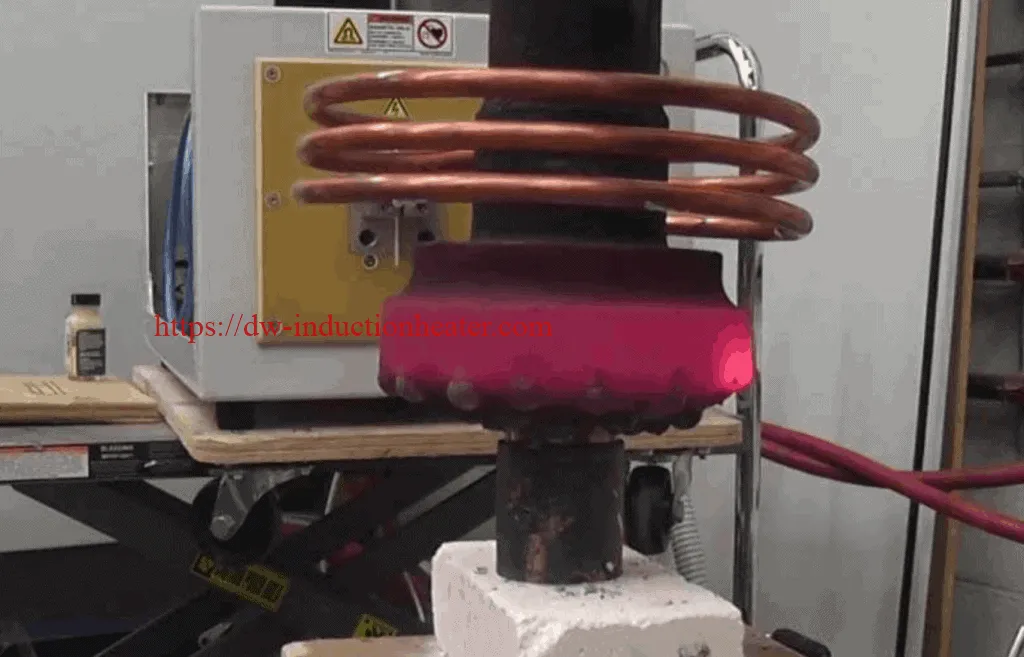
Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
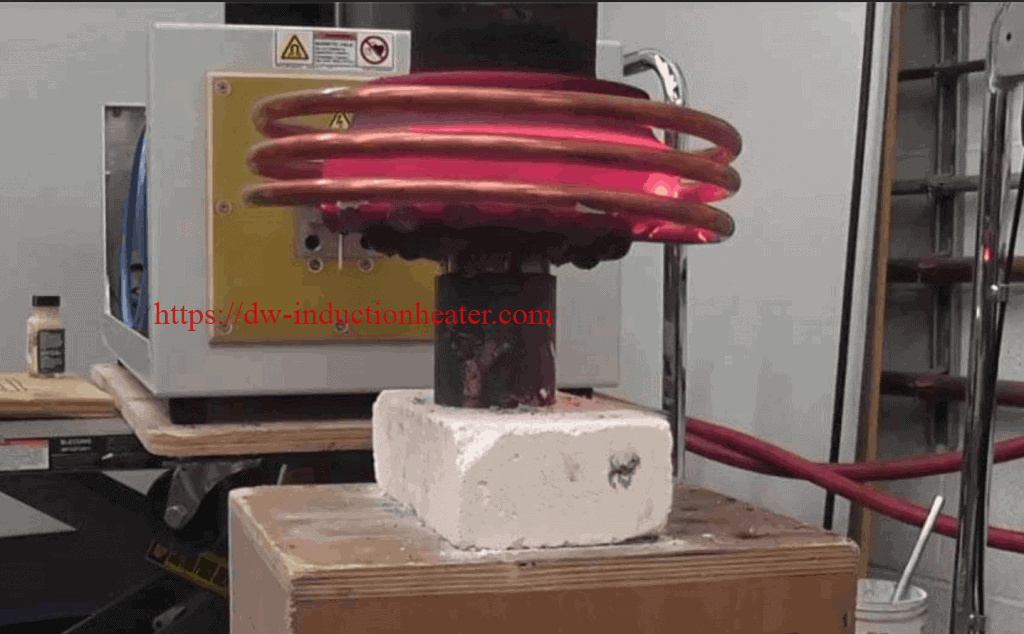
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
https://dw-inductionheater.com/induction-brazing-carbide-to-steelbrazing-tungsten-carbide-to-stainless-steel.html?feed_id=237324&_unique_id=65f8e6a800a0b

2023年9月18日星期一

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
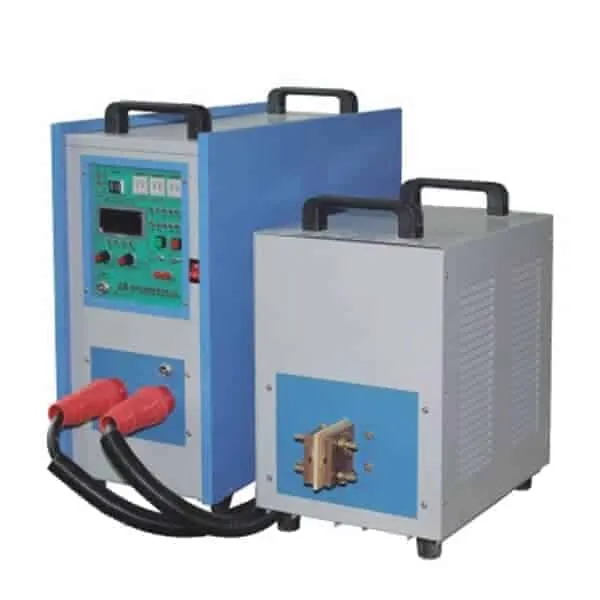
induction brazing machineMaterials:
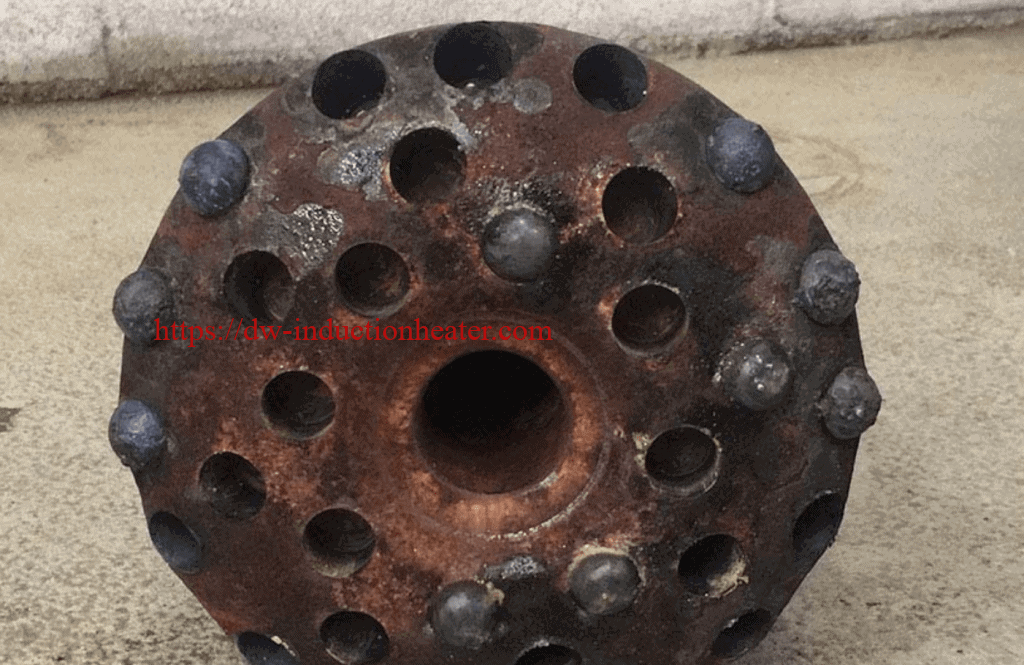
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
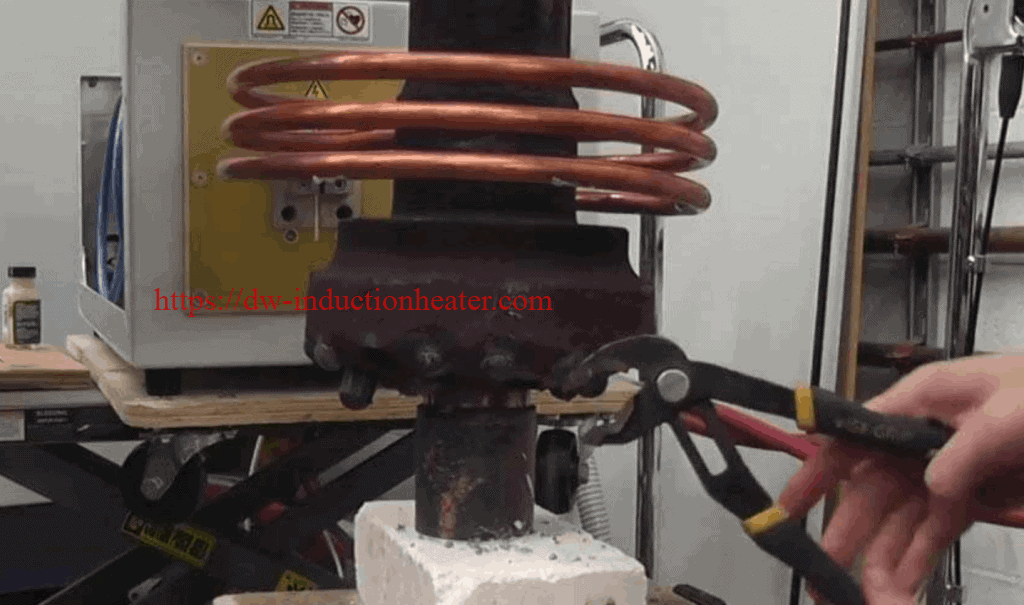
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
2023年7月26日星期三

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
https://dw-inductionheater.com/induction-brazing-carbide-to-steelbrazing-tungsten-carbide-to-stainless-steel.html?feed_id=220561&_unique_id=64c1743521066

2023年4月30日星期日

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
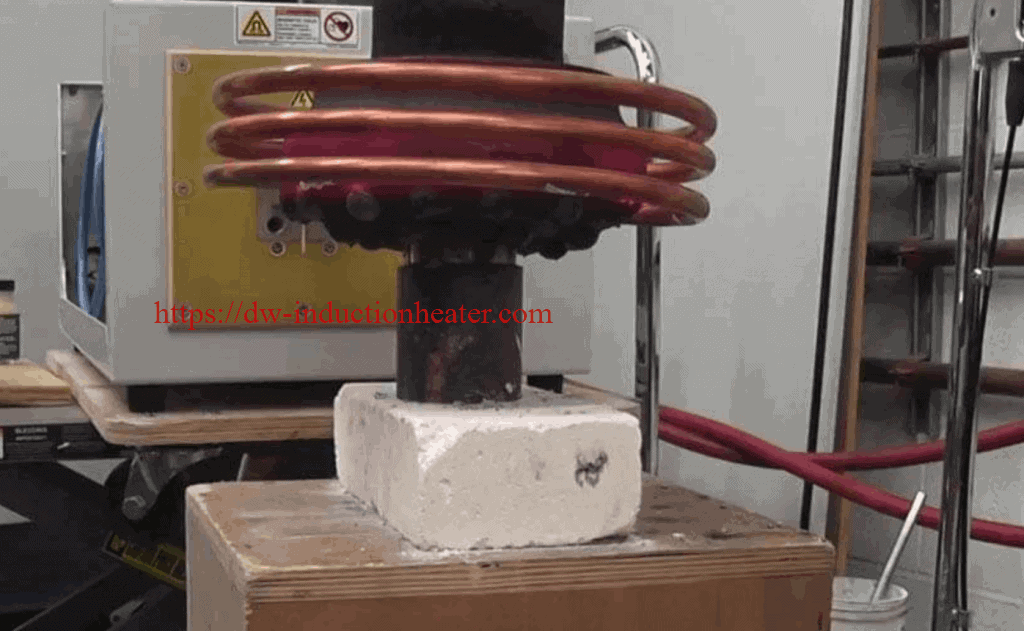
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
2023年4月7日星期五

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.

2023年3月18日星期六

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.