显示标签为“brazingcarbide”的博文。显示所有博文

2024年5月4日星期六

Induction Brazing Carbide To Stainless Steel

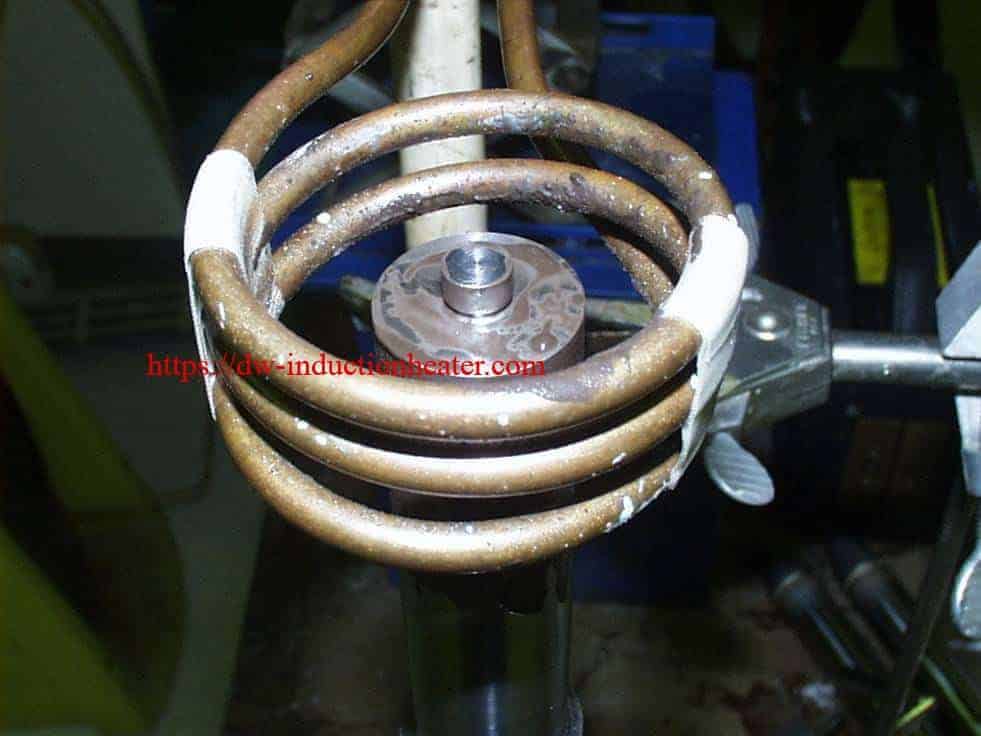
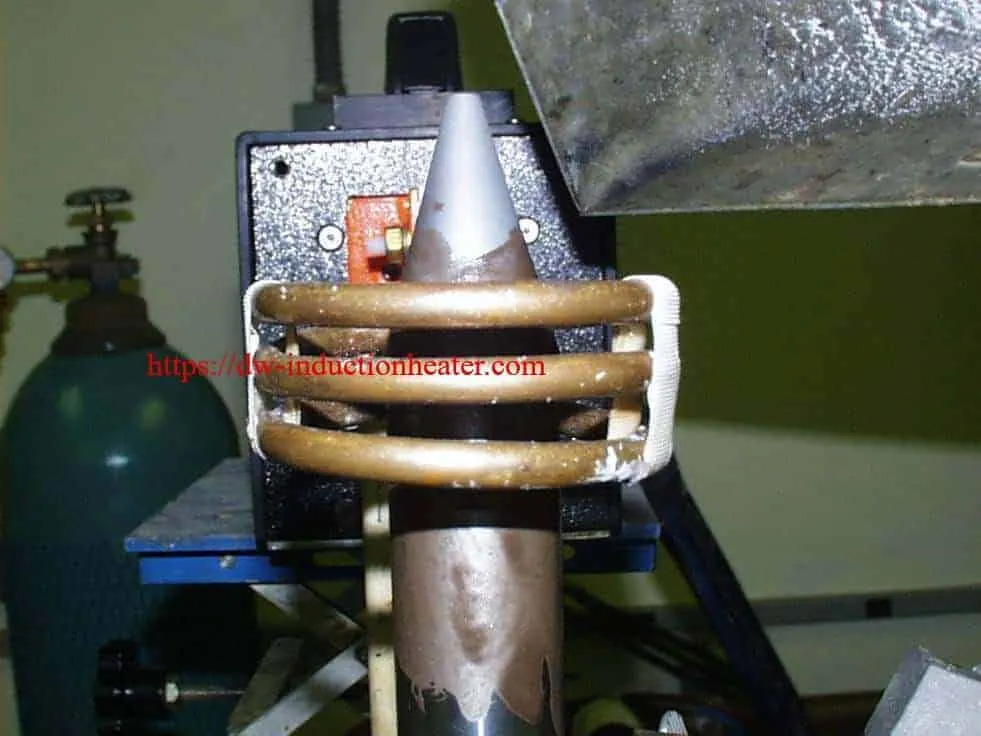
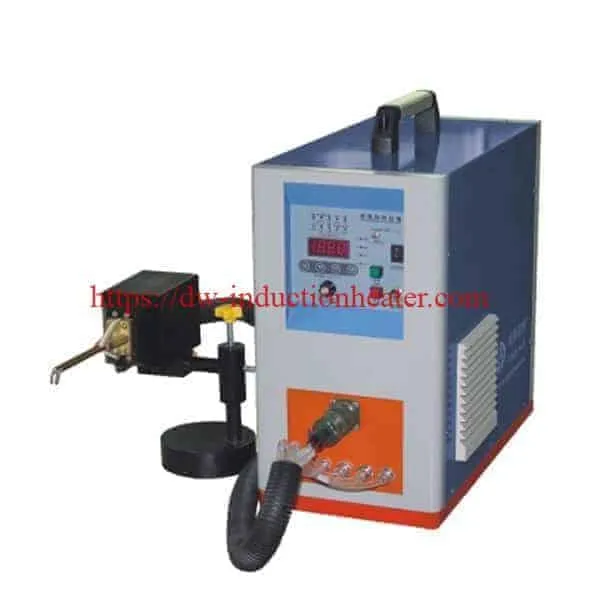
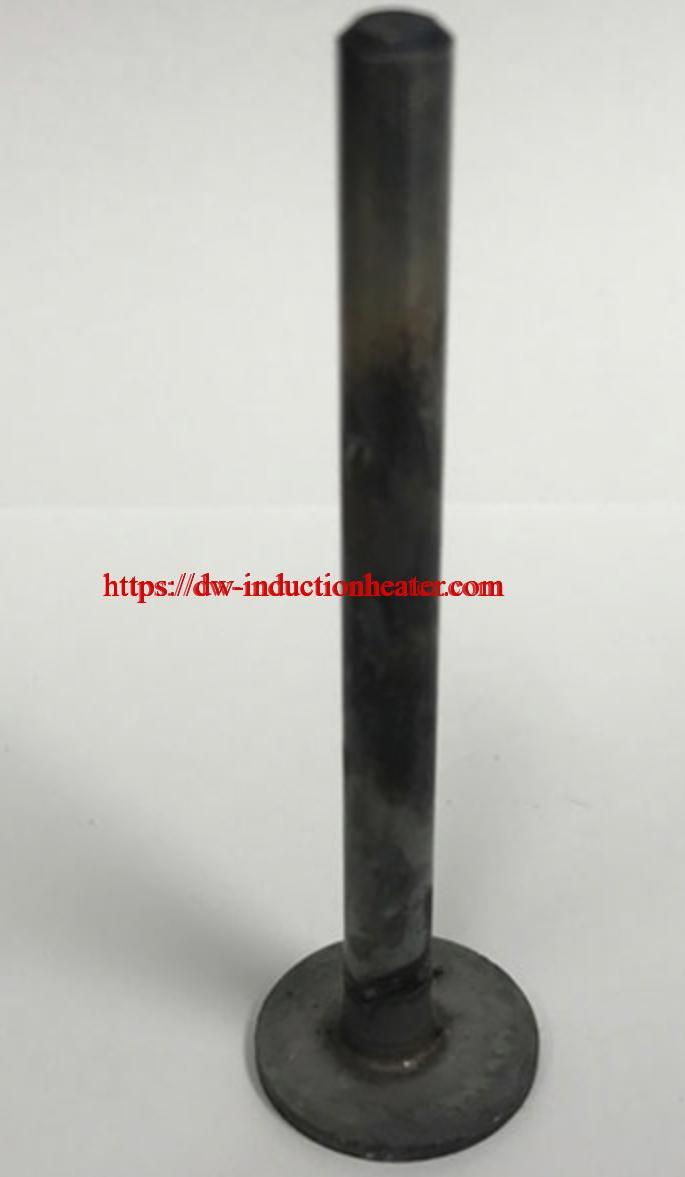
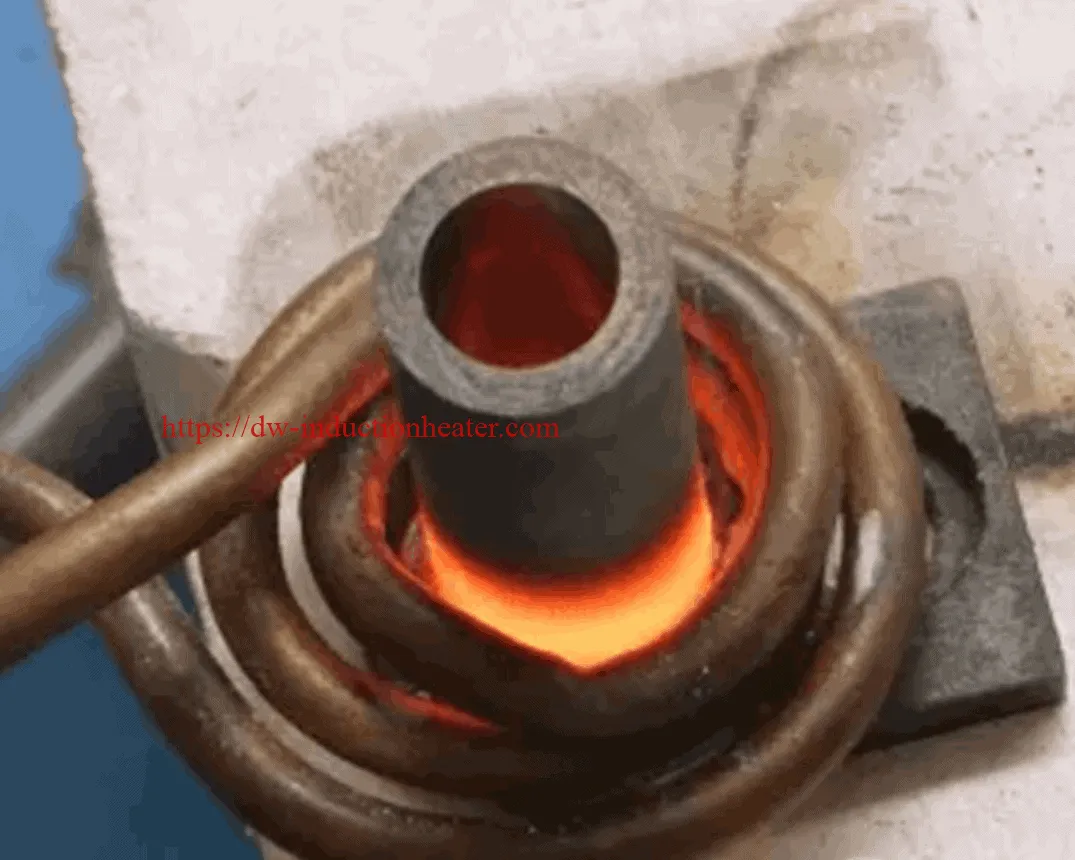
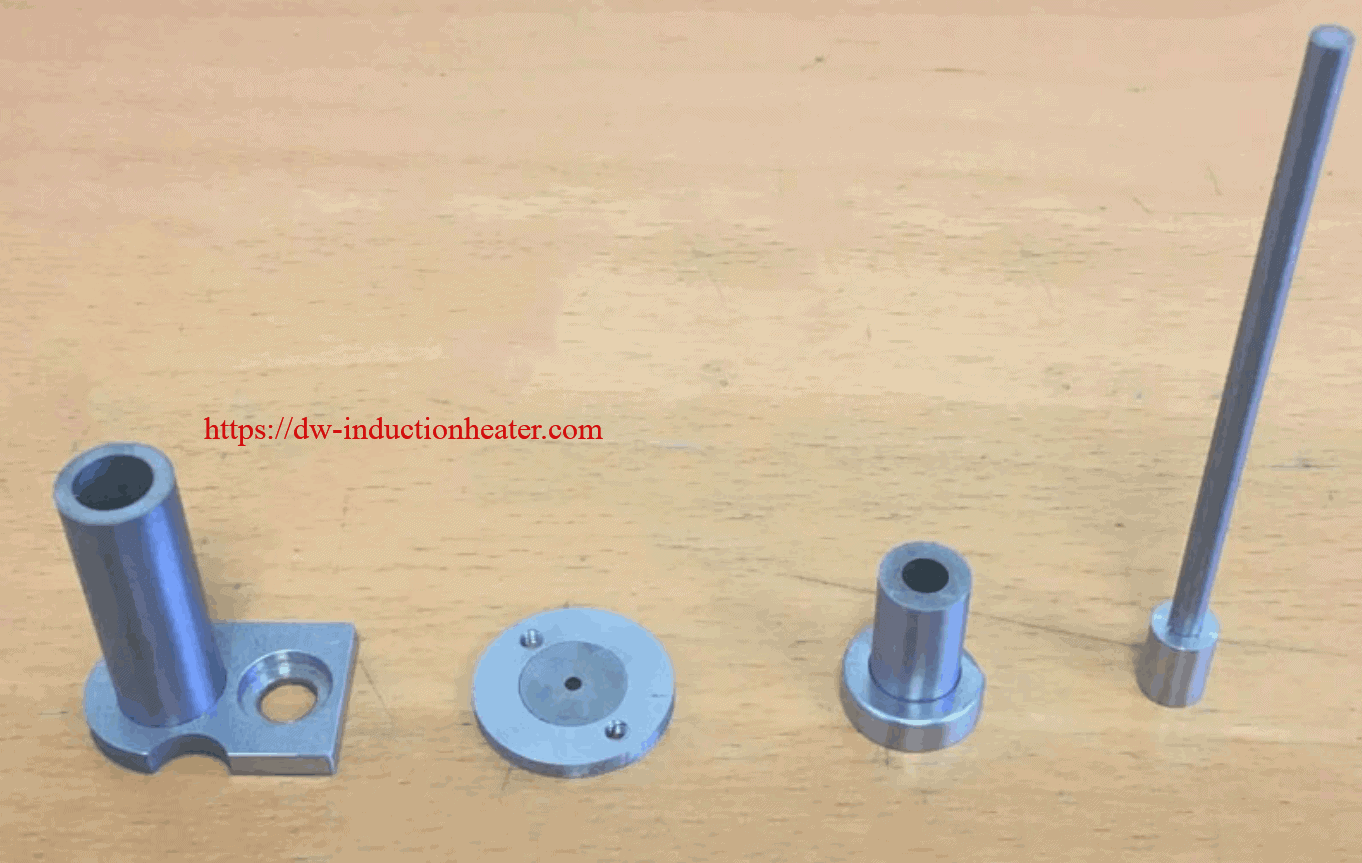
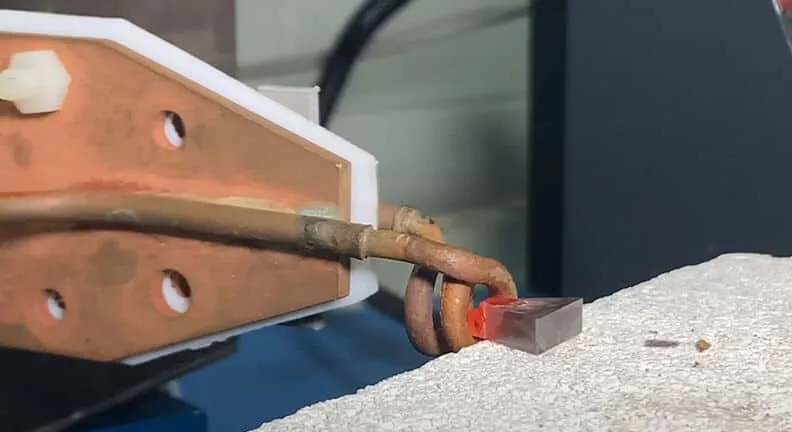
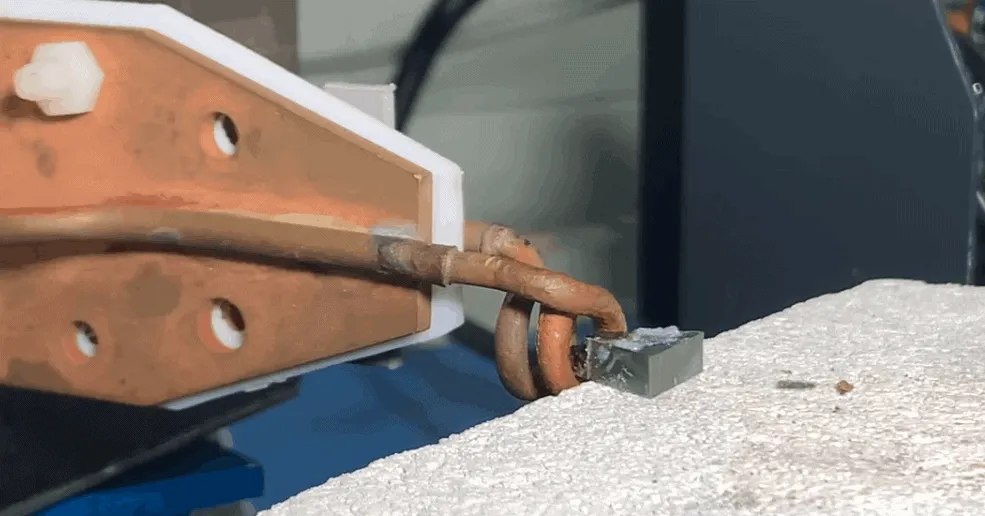
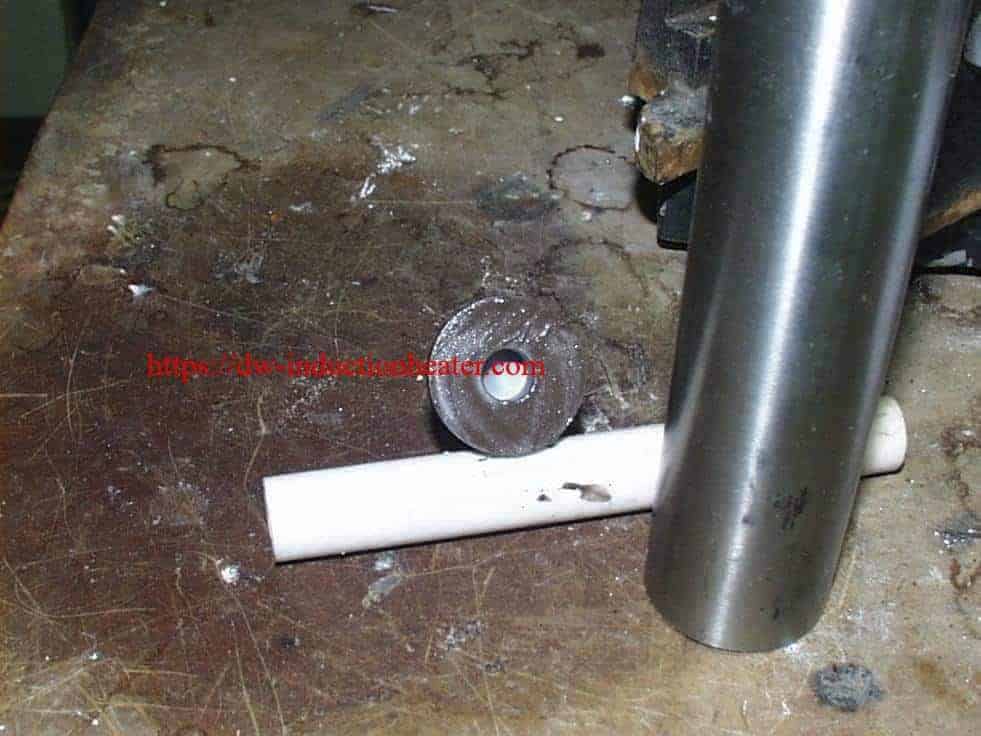
Induction Brazing Carbide To Stainless Steel Shaft With IGBT Heating Units Objective Brazing a cone shaped carbide to a stainless steel shaft for a digger Material Cone shaped carbide 1.12” (28.4mm) dia, 1.5”(38.1mm) tall, stainless steel shaft 1.12” (28.4mm) dia and various length, black brazing flux and braze shims Temperature 1500 ºF (815 ºC) Frequency 277 kHz Equipment • DW-UHF-10 kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF • An induction heating coil designed and developed specifically for this application. Process A three turn helical coil is used to braze the carbide to the shaft. The steel shaft is fluxed and the braze shim placed on top. The carbide tip is fluxed and placed on top of the shim, lining up the countersunk hole in the carbide. The hole is not fluxed because the flux outgases and causes the carbide to build up pressure and attempt to repel from the shaft. Power is applied for 85 seconds for the braze shim to flow and make a good joint. DAWEI’s customer has a customer who is unhappy with the braze quality of their digger so our customer is looking for a better quality brazing process. DAWEI’s customer is very happy with the sample brazed diggers and the help he received from the Ameritherm lab in developing his brazing process. Results/Benefits Induction heating provides: • Rapid localized heating only where needed • Creates clean, controllable joints • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating brazing carbide to shaft             induction brazing carbide to shaft               brazing carbide to stainless steel shaft https://dw-inductionheater.com/induction-brazing-carbide-to-stainless-steel.html?feed_id=244304&_unique_id=6636501477c8b

2024年4月12日星期五

Induction Brazing Carbide Onto Steel Part

Induction Brazing Carbide Onto Steel Part

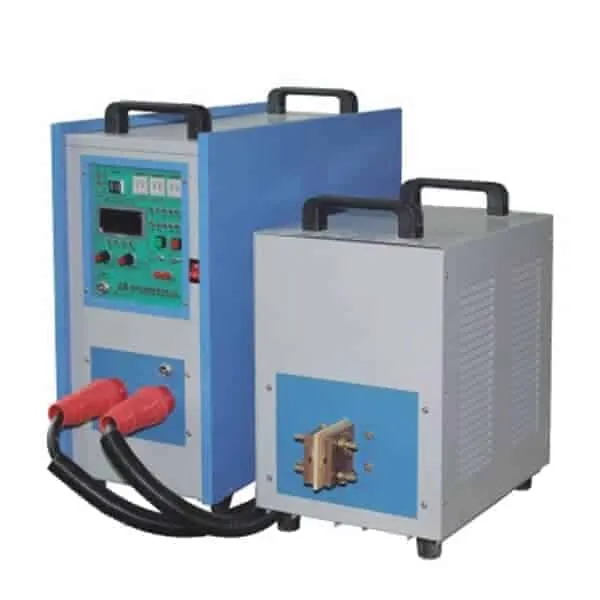
Induction brazing carbide onto steelObjective Brazing carbide onto steel workpiece Equipment DW-UHF-6KW-III Handheld Induction Brazing Heater Handheld induction brazing heaterKey Parameters Power: 4kW Temperature: Approximately 1500°F (815°C) Time: 16 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
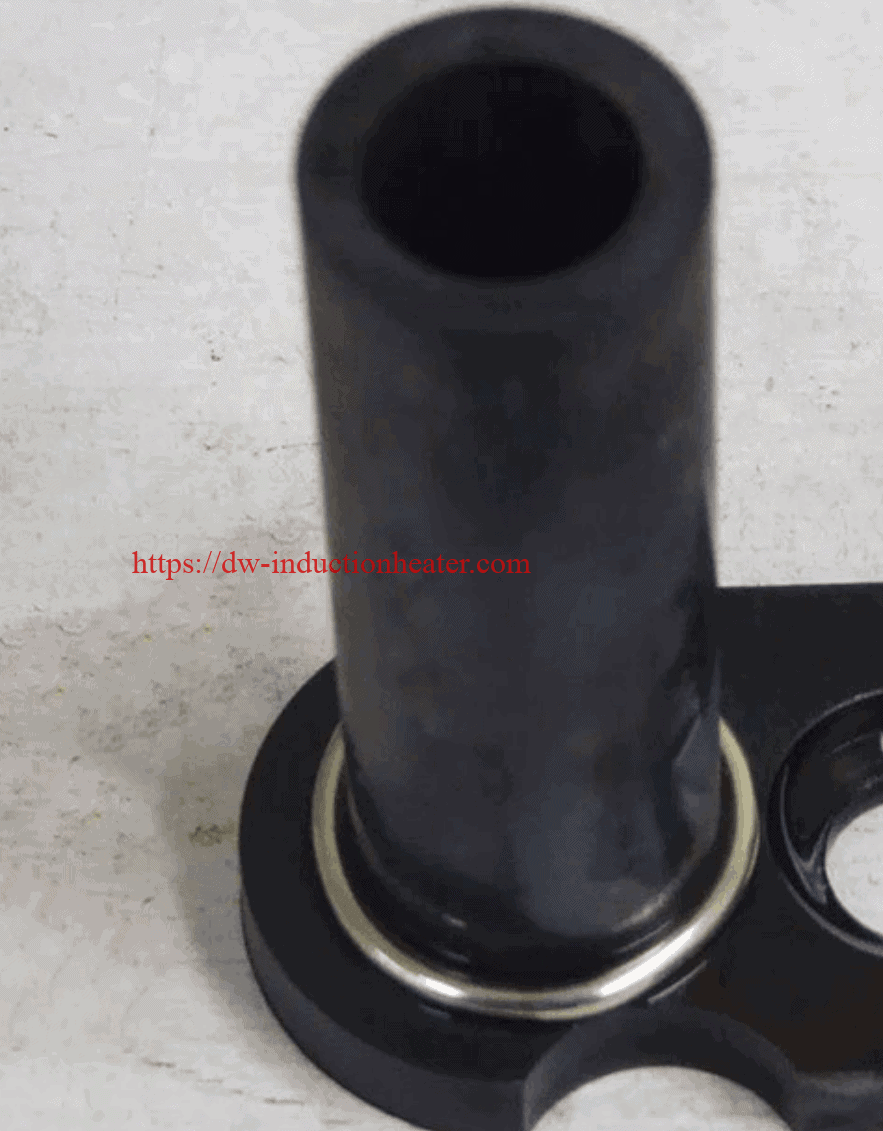
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 3kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
Induction brazing carbide to steelbrazing carbide onto steel
https://dw-inductionheater.com/induction-brazing-carbide-onto-steel-part.html?feed_id=241299&_unique_id=6619bfbf80a7e

2024年4月6日星期六

Induction Brazing Steel Parts to Tungsten Carbide Plate

Induction Brazing Steel Parts to Tungsten Carbide Plate

Objective Induction Brazing of Steel Parts to a Tungsten Carbide Plate Equipment DW-UHF-6KW-III handheld induction brazing machine Induction brazing steel parts
Test 1 Materials • Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length • Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness • Alloy: 19.05 mm (0.75″) Brazing discs Power: 4.0 kW Temperature: Approximately 760° C (1400° F) Time: 40 sec
Test 2 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 23 sec
Test 3 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 20-25 sec (Pulsing on/off)
Test 4 Materials • Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes • Alloy: 6.35 mm (0.25″) Brazing discs Power: 1.96 kW Temperature: Approximately 760° C (1400° F)Induction brazing steel carbideInduction brazing steel partsInduction brazing steel parts Time: 20 sec (Pulsing on/off)
Results and Conclusions: Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
  [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=240398&_unique_id=6611e4f0f237c

2024年3月22日星期五

Induction Brazing Carbide To Steel

Objective Induction Brazing carbide to steel parts Equipment DW-HF-15kw Induction Heating Power Supply HLQ custom coil Key Parameters Power: 5.88 kW Temperature: Approximately 1500°F (815°C) Time: 10 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 10 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Induction Brazing was successful all in under 15 seconds with 8kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/high-frequency-induction-brazing-carbide-to-steel-process.html?feed_id=237924&_unique_id=65fde60bb551a

2024年3月18日星期一

Induction Brazing Carbide to Steel

Objective High frequency induction brazing carbide to steel. Recommended Equipment The recommended equipment for this application is the DW-HF-45KW induction brazing machine with the remote heating station.
induction brazing machineMaterials:
  • Large magnetic steel drill head with carbides. Head is approx. 8” OD x 4” (203.2mm OD x 101.6mm) thick, shaft is 11” (279.4mm) long x 2”(50.8mm) to 5” (127mm) OD.
  • Carbides 1.125” (28.5mm) long x 0.75”(19.05mm) OD with dome shaped top attached to the head, recessed approx. 0.8” (20.3mm) into the head.
Power: Up to 37kW Temperature: 1500°F  + (815°C+) Time: Alloy flows at the outer most carbides in 50 seconds.  The center and inner carbides start to show alloy dripping at 1 minute and 40 seconds.
Results and Conclusions: Tests results show that carbide removal is possible.  Initially, the part needs to be heated and held at temperature to allow the induction brazing alloy to drip out.  It is important to fixture the part with carbides facing down.  An external shock is needed afterwards to shift the carbides out enough to allow them to be grabbed with a set of pliers. Caution: when pulling out the carbides, hot molten induction brazing alloy can flow out of the holes for the carbides when they are pulled out.
https://dw-inductionheater.com/induction-brazing-carbide-to-steelbrazing-tungsten-carbide-to-stainless-steel.html?feed_id=237324&_unique_id=65f8e6a800a0b

2024年2月24日星期六

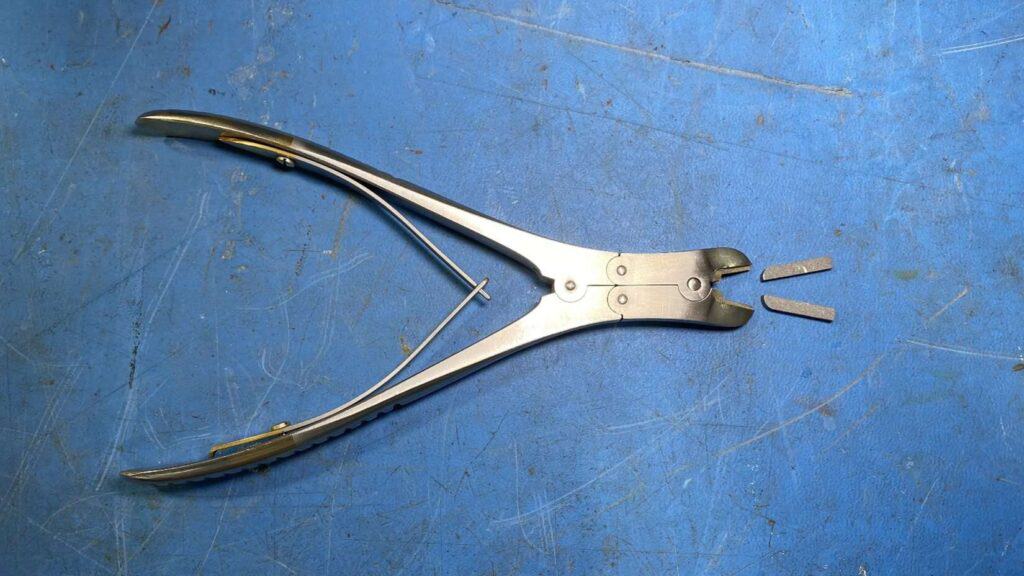
Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

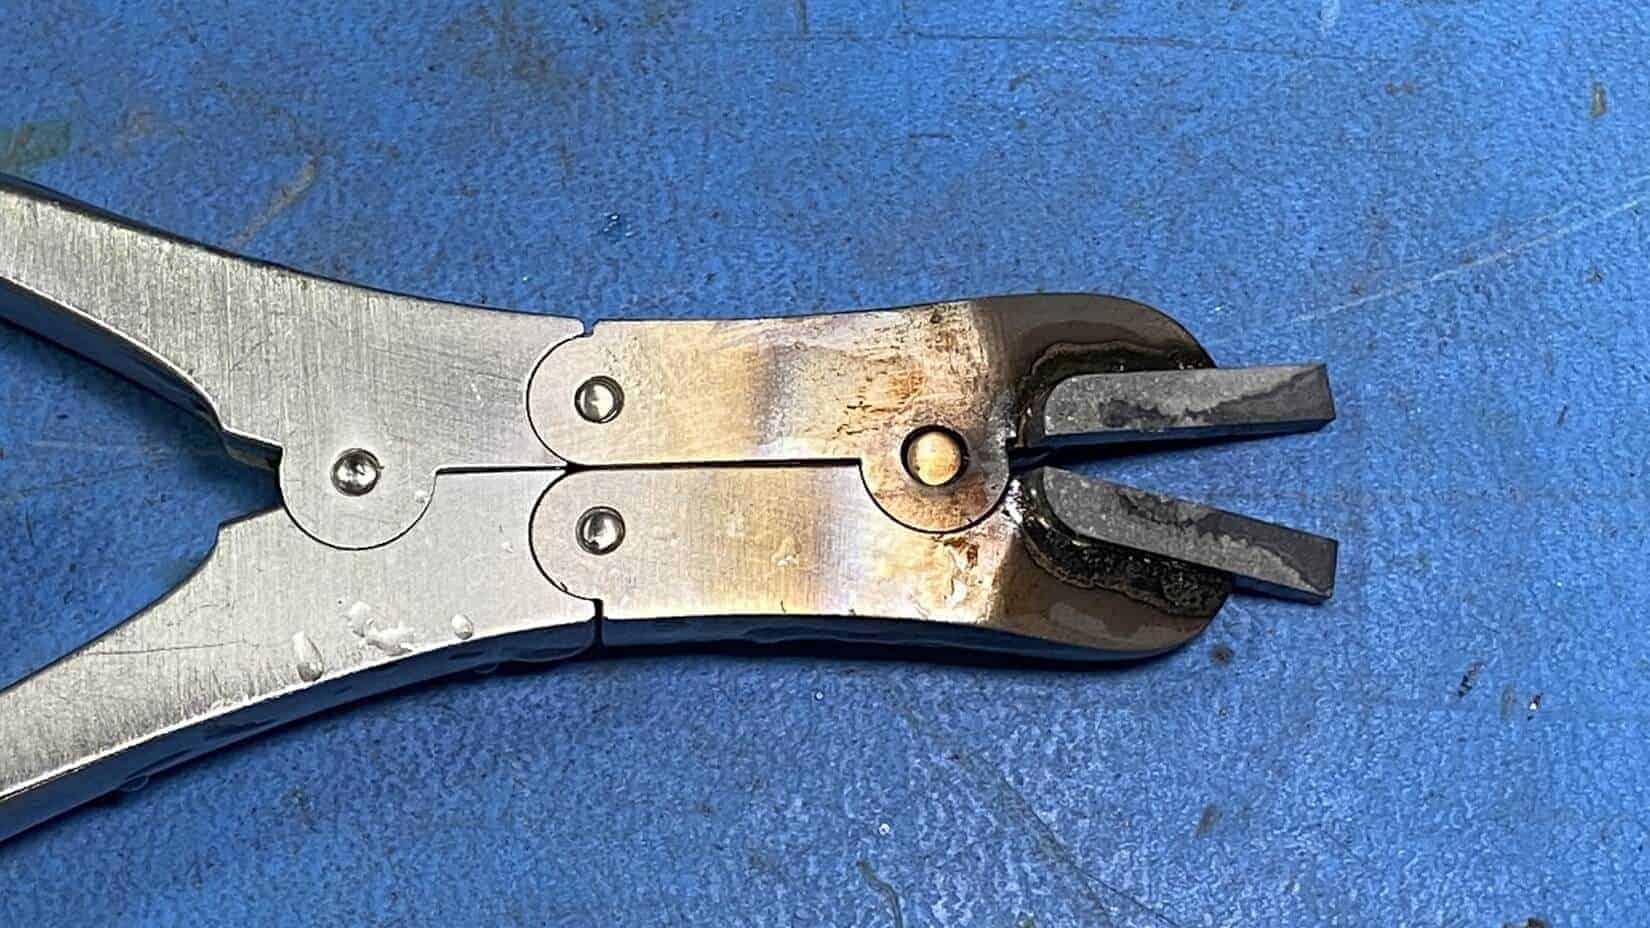
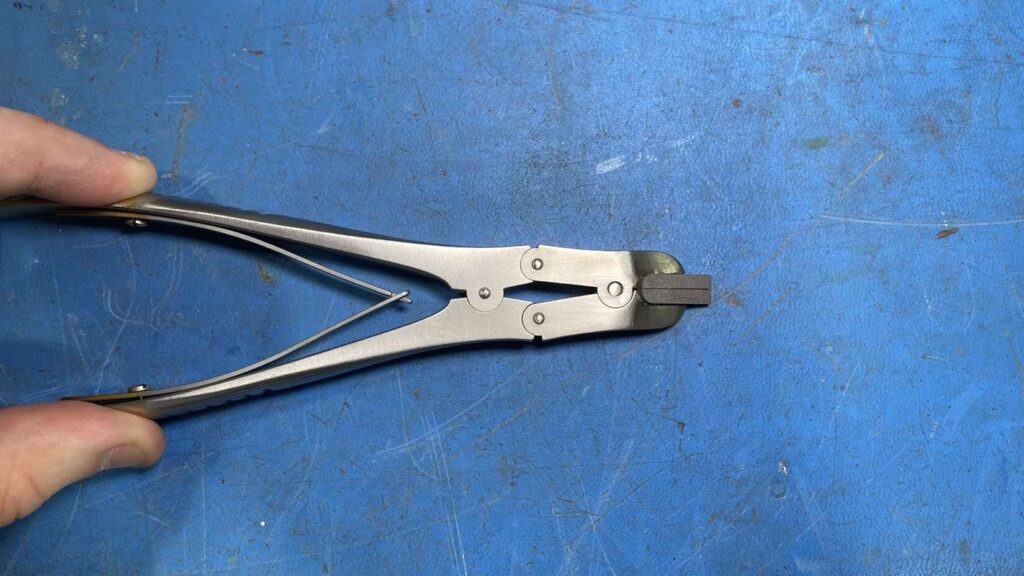
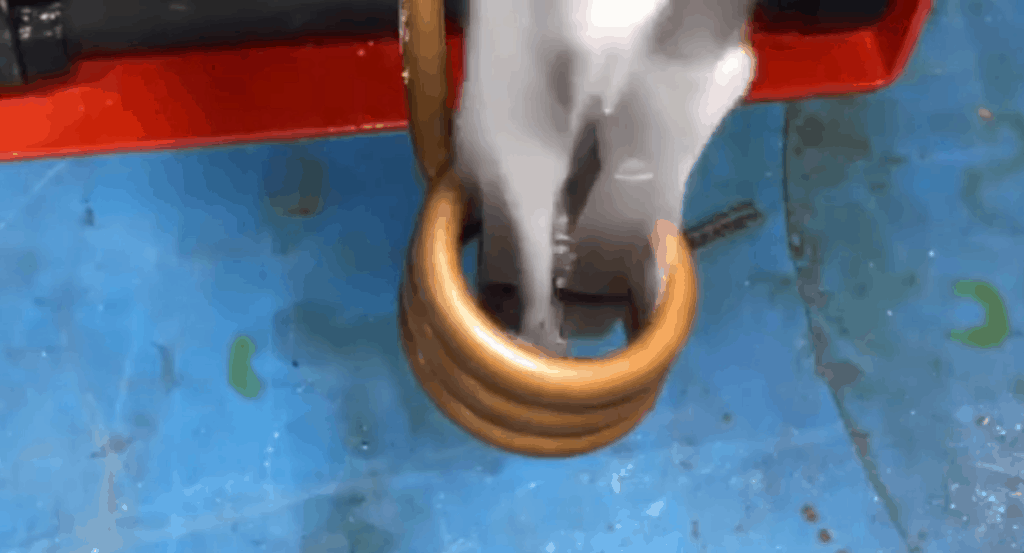
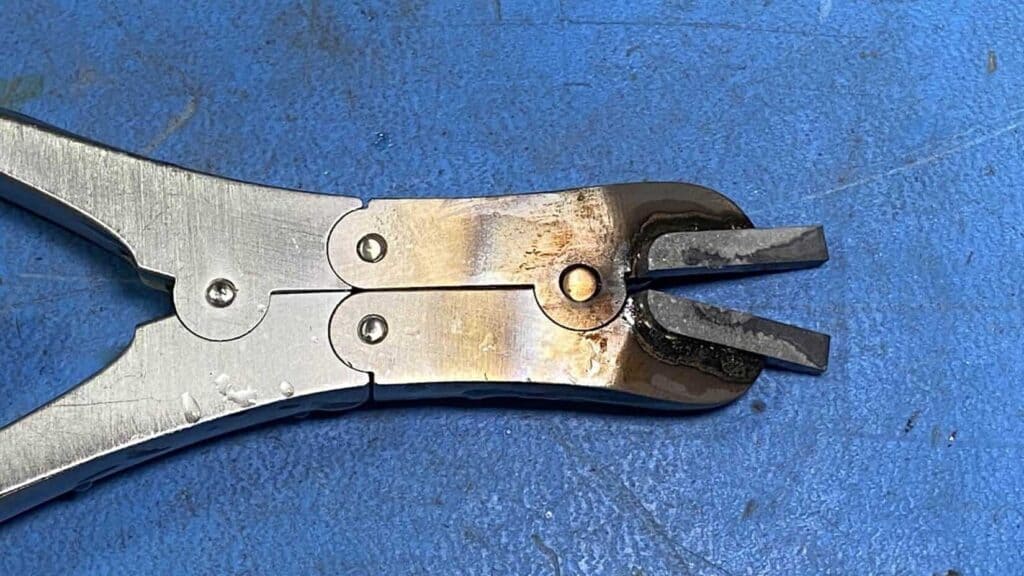
Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental https://dw-inductionheater.com/induction-brazing-carbide-tipping-of-medical-tools.html?feed_id=234808&_unique_id=65dae83c26fa5
Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

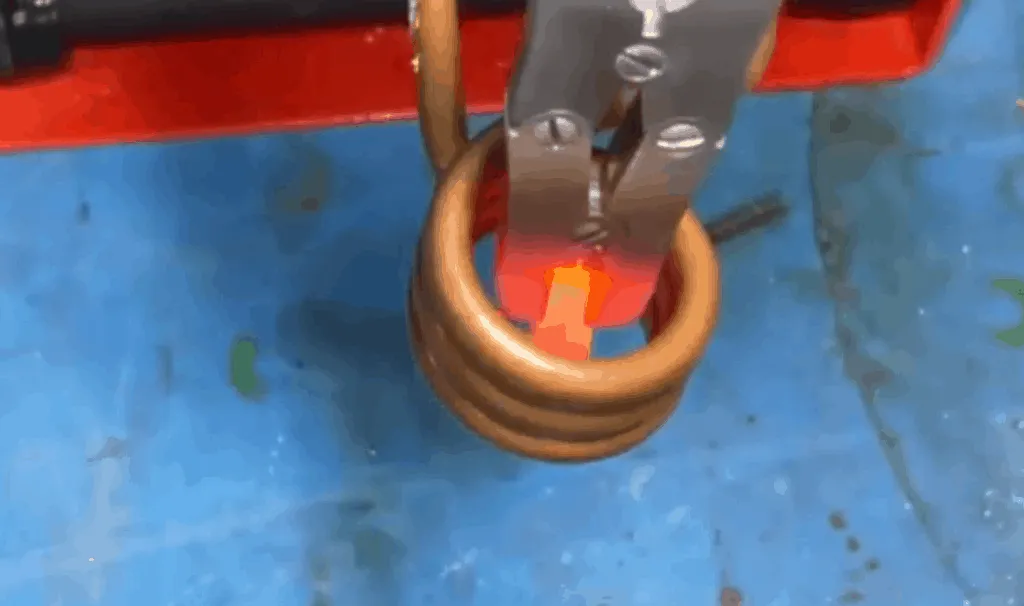
Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment   https://dw-inductionheater.com/induction-brazing-carbide-tipping-on-cutting-steel-tool.html?feed_id=234740&_unique_id=65da3174f13f0

2024年2月23日星期五

Brazing Carbide to Steel Part With Induction Heating

Brazing Carbide to Steel Part With Induction Heating

Objective Brazing carbide to steel part Equipment DW-UHF-6kw Induction Heating Power Supply ultra high frequency custom coil Key Parameters Power: 1.88 kW Temperature: Approximately 1500°F (815°C) Time: 14 sec Materials Coil-  2 helical turns (20 mm ID) 1 planar turn (40 mm OD, 13 mm Height) Carbide-  13 mm OD, 3 mm wall thickness Steel piece– 20 mm OD, 13 mm ID
Induction Brazing Process:
  1. To demonstrate elimination of “hand feeding” the alloy, we formed the alloy into a ring to tightly fit over the center post tube. This method provides a uniform amount for each cycle, resulting in uniform joints and wetting.
  2. The custom made coil was then placed over the steel piece, where is was set for 14 seconds to heat the alloy.
  3. The alloy was heated at approximately 1500°F (815)°C
  4.  The whole piece is left alone and cooled with ambient air
Results/Benefits:
  • Brazing was successful all in under 20 seconds with 2-kW
  • High quality and repeatability of the brazed joints
  • Increased productivity
  • Rings will need to be developed for specific joints to prevent the use of too much alloy
  • Precise control of the time and temperature
https://dw-inductionheater.com/brazing-carbide-to-steel-part-with-induction-heating.html?feed_id=234673&_unique_id=65d97aa9ecfb5

2023年11月9日星期四

Brazing carbide shaft with induction

Brazing carbide shaft with induction Objective: Braze a carbide shaft to a steel tube Material: Carbide shaft 1/8" to 1" diameter (varying sizes) Steel tube 3/8" to 1 ¼" OD Silver solder braze Temperature: indicating paint Temperature: 1400 °F for 60 seconds Frequency300 kHz Equipment: DW-UHF-6KW-III, 150-400 kHz solid state induction heating system equipped with a remote heat station containing two 0.66 μF capacitors (total 1.32 μF) A multi-turn helical coil Process: Silver solder is applied to where the carbide shaft and steel tube meet. The clearance between the two parts is approximately .0005". A small piece of solder braze is placed on the part and then the part is heated. It takes about 60 seconds to flow the braze with the best heat migration and solder flow. Even though the part can be heated faster, optimal results are obtained at 60 seconds. Results/Benefits: Induction heating provides even, precise heat. Precise directed heat is required for the solder braze to flow evenly around the part to assure a good joint. https://dw-inductionheater.com/brazing-carbide-shaft-with-induction.html?feed_id=230466&_unique_id=654d8320ad50f

2023年9月22日星期五

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.