显示标签为“hfbrazing”的博文。显示所有博文

2024年3月16日星期六

induction Brazing copper rods to brass strips

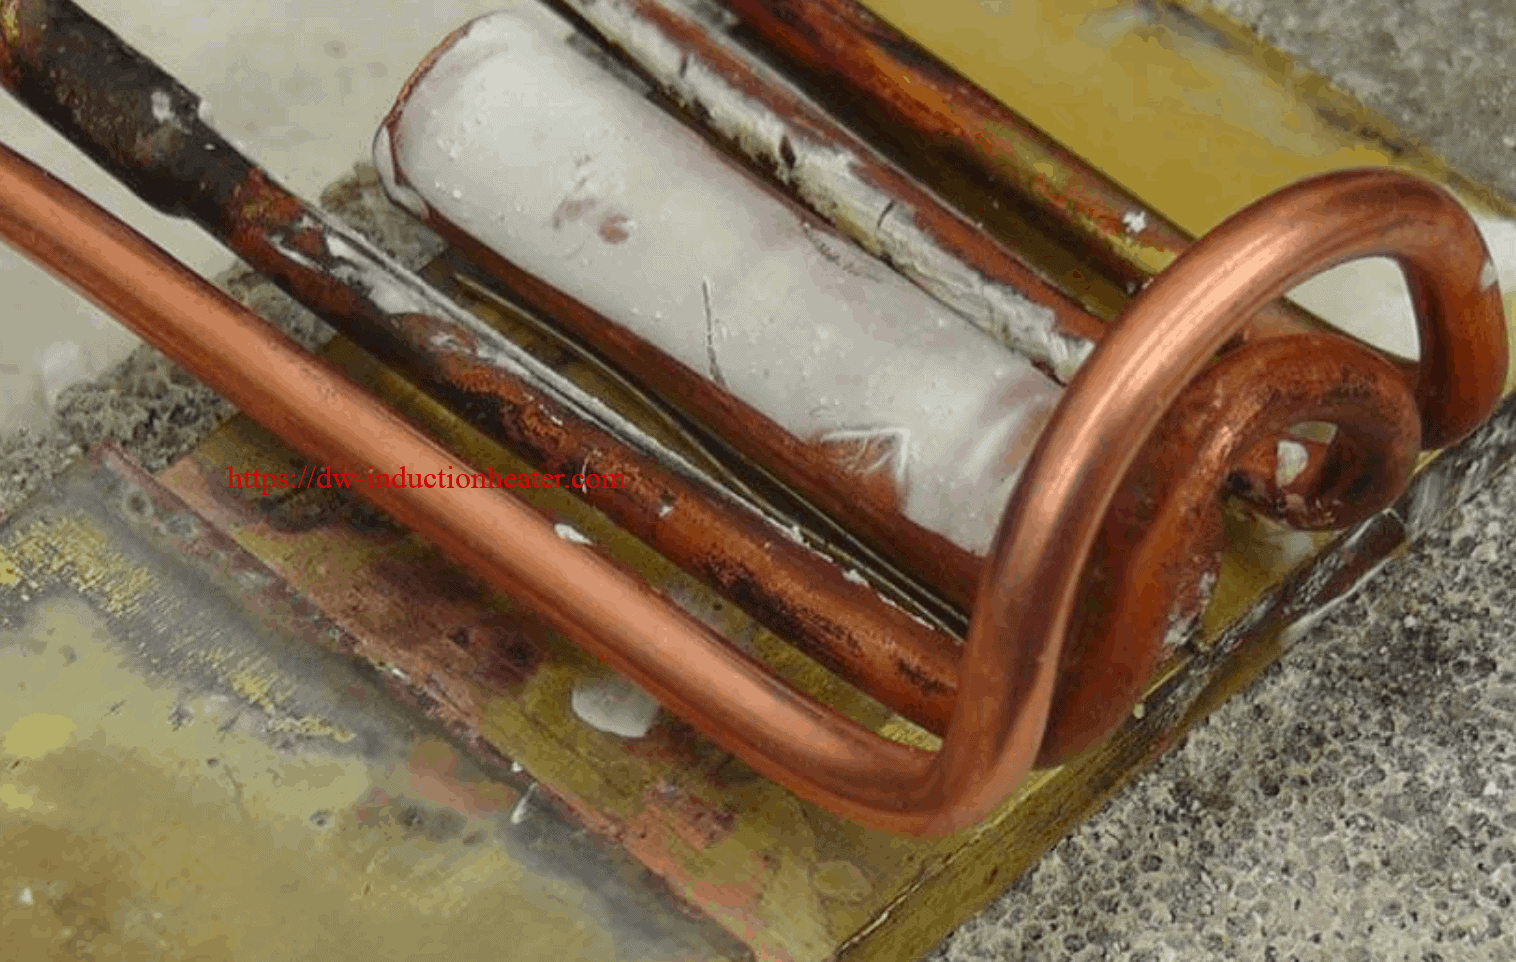
Objective Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.
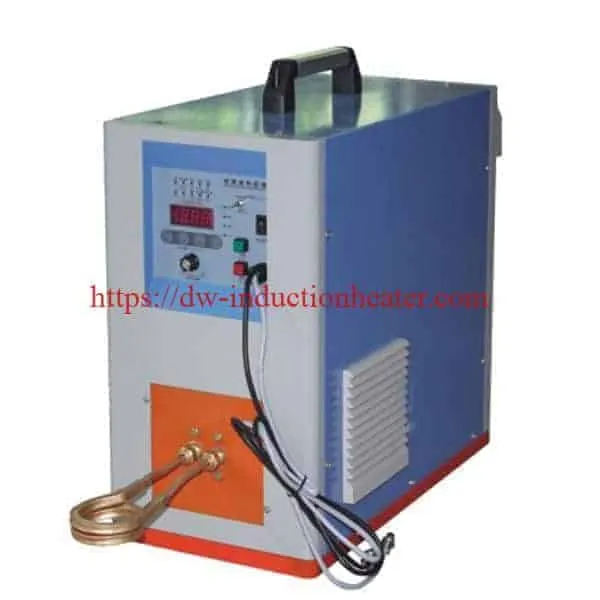
Equipment DW-UHF-10KW INDUCTION BRAZING MACHINE Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 100 seconds Process and Results: For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.
Key Parameters – TEST 1 Power: 6 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2.5 minutes Process and Results: For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2 minutes Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up  and heated for an average time of 2 minutes to flow the alloy and achieve the braze.
Results/Benefits:
  • induction brazing Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/induction-brazing-copper-rods-to-brass-strips.html?feed_id=236928&_unique_id=65f60b623c1e1

2024年2月24日星期六

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

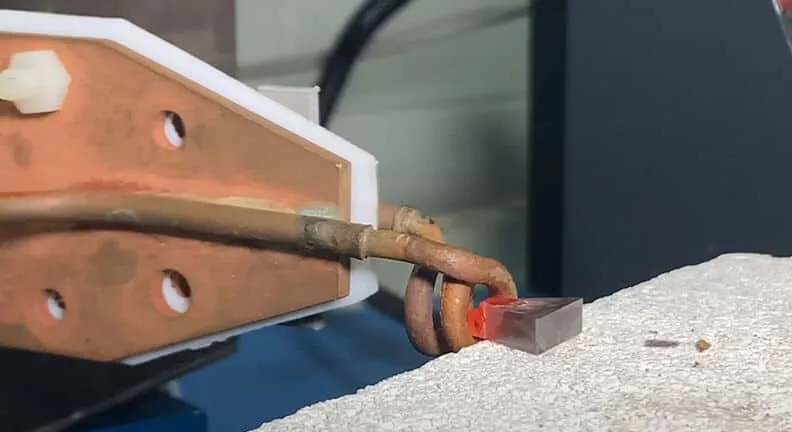
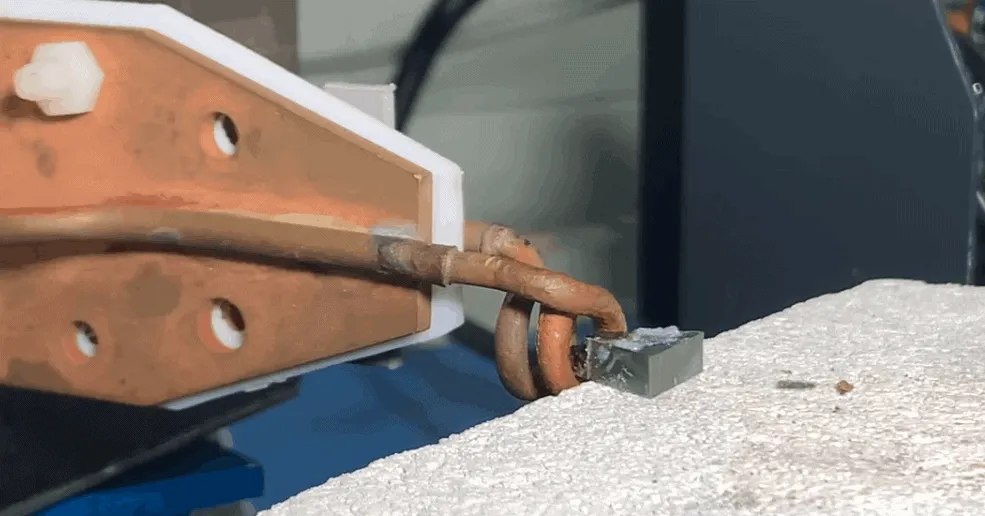
Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment   https://dw-inductionheater.com/induction-brazing-carbide-tipping-on-cutting-steel-tool.html?feed_id=234740&_unique_id=65da3174f13f0

2023年10月28日星期六

induction Brazing copper rods to brass strips

Objective Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.
Equipment DW-UHF-10KW INDUCTION BRAZING MACHINE Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 100 seconds Process and Results: For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.
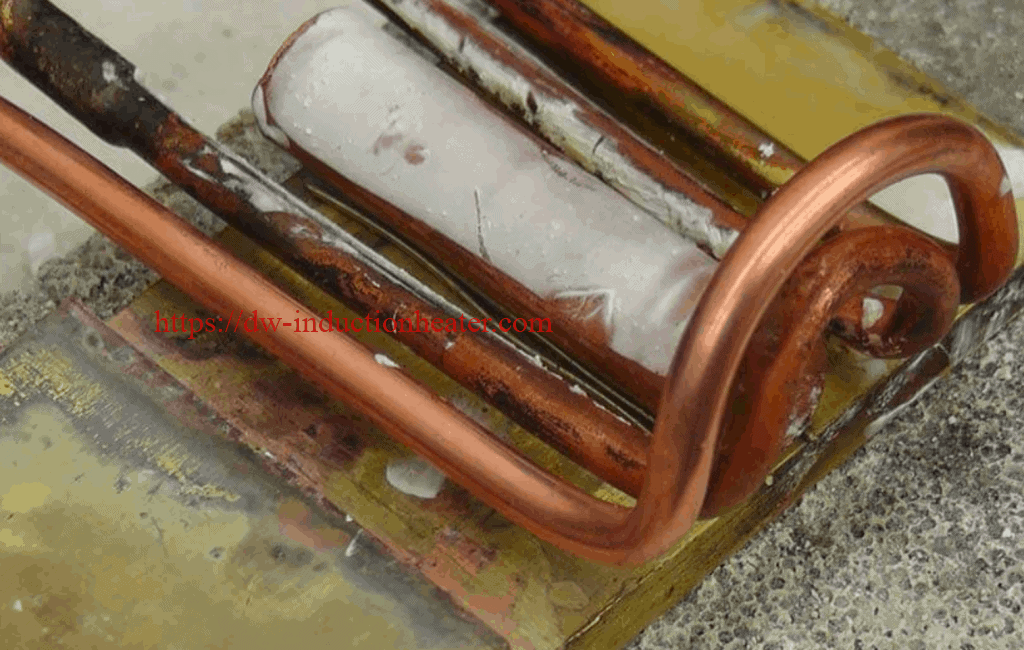
Key Parameters – TEST 1 Power: 6 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2.5 minutes Process and Results: For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2 minutes Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up  and heated for an average time of 2 minutes to flow the alloy and achieve the braze.
Results/Benefits:
  • induction brazing Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2023年9月22日星期五

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment  

2023年8月28日星期一

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment  

2023年7月28日星期五

induction Brazing copper rods to brass strips

Objective Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.
Equipment DW-UHF-10KW INDUCTION BRAZING MACHINE Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 100 seconds Process and Results: For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.
Key Parameters – TEST 1 Power: 6 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2.5 minutes Process and Results: For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2 minutes Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up  and heated for an average time of 2 minutes to flow the alloy and achieve the braze.
Results/Benefits:
  • induction brazing Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2023年7月24日星期一

induction Brazing copper rods to brass strips

Objective Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.
Equipment DW-UHF-10KW INDUCTION BRAZING MACHINE Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 100 seconds Process and Results: For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.
Key Parameters – TEST 1 Power: 6 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2.5 minutes Process and Results: For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2 minutes Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up  and heated for an average time of 2 minutes to flow the alloy and achieve the braze.
Results/Benefits:
  • induction brazing Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/induction-brazing-copper-rods-to-brass-strips.html?feed_id=220261&_unique_id=64be98295fb09

2023年7月21日星期五

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small areain order to decrease heat loss and improve carbide tipping process.   Induction Brazing Process:  The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:  DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry:Tools & Equipment  

2023年7月8日星期六

induction Brazing copper rods to brass strips

Objective Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.
Equipment DW-UHF-10KW INDUCTION BRAZING MACHINE Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 100 seconds Process and Results: For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.
Key Parameters – TEST 1 Power: 6 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2.5 minutes Process and Results: For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1 Power: 7.2 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 2 minutes Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up  and heated for an average time of 2 minutes to flow the alloy and achieve the braze.
Results/Benefits:
  • induction brazing Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.