显示标签为“BrazingCarbideTipping”的博文。显示所有博文

2024年2月24日星期六

Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

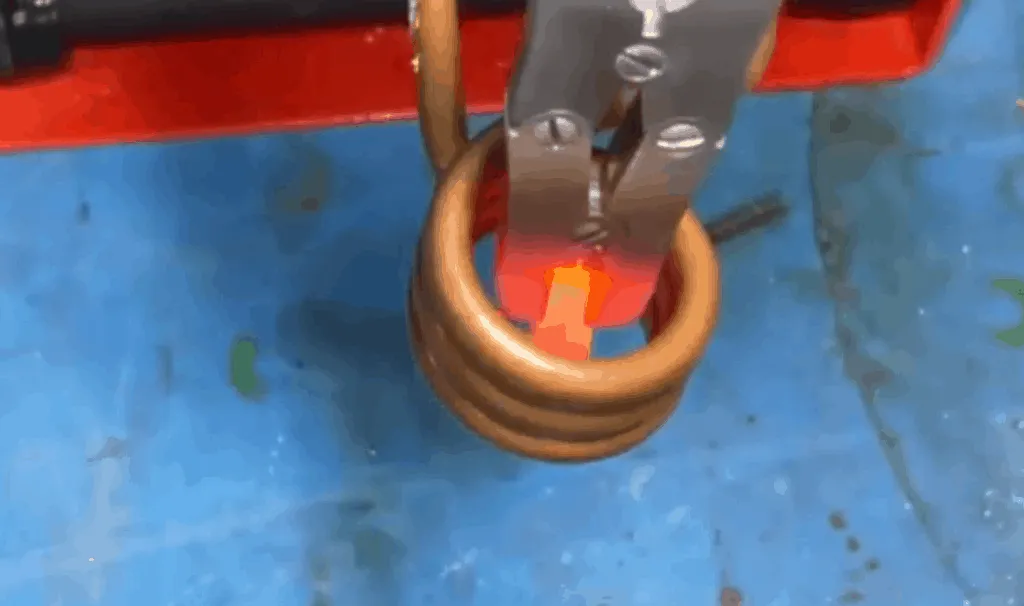
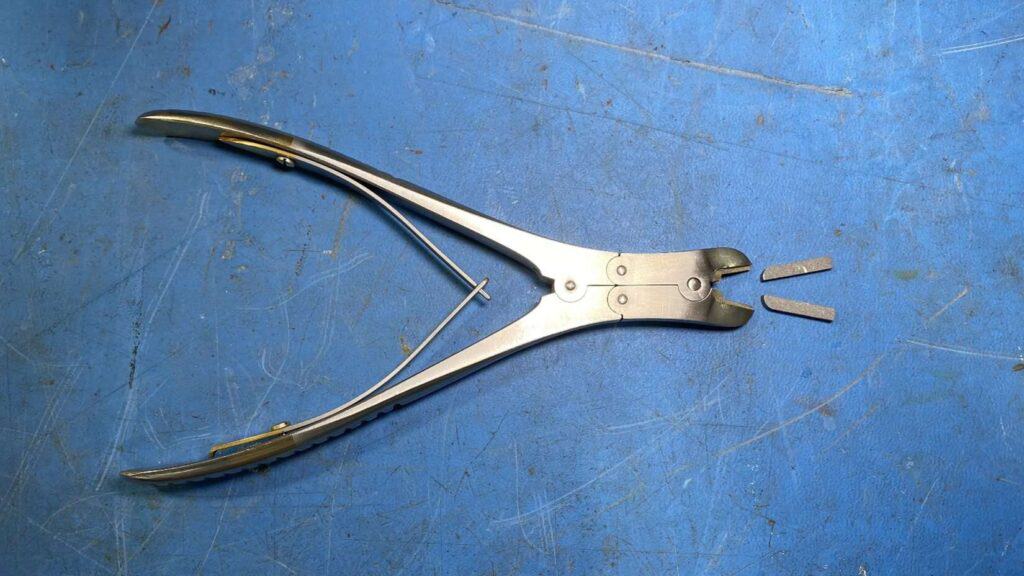
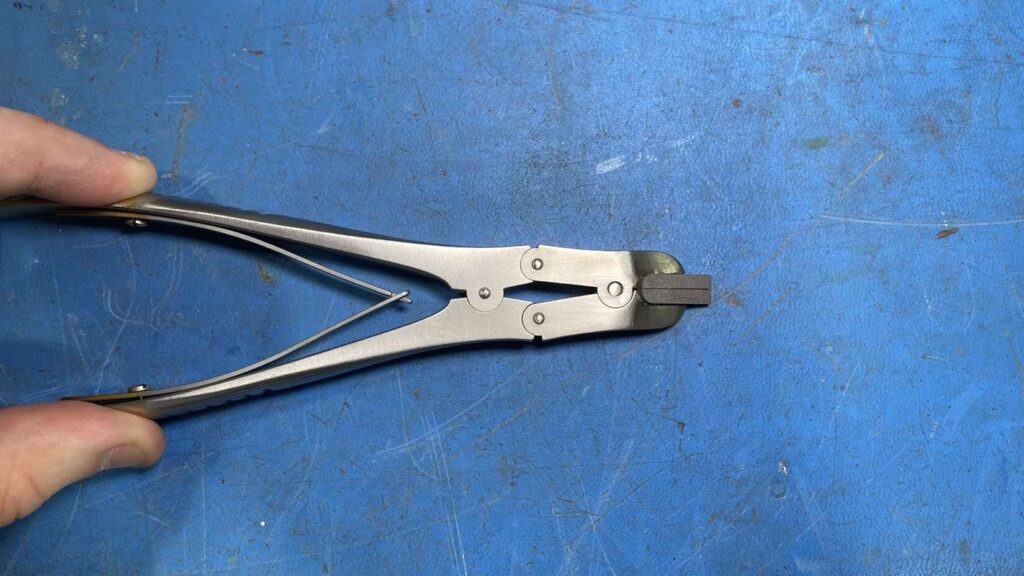
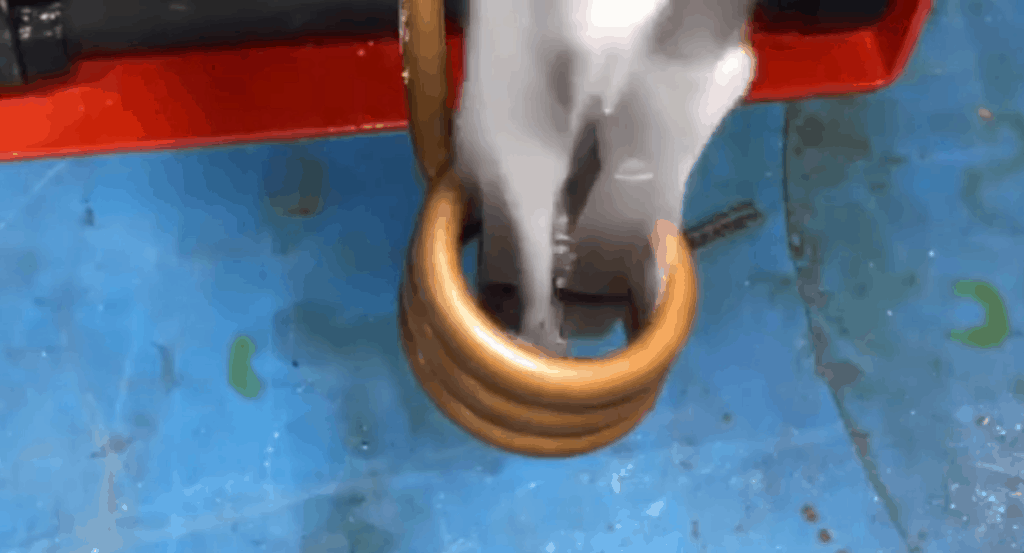
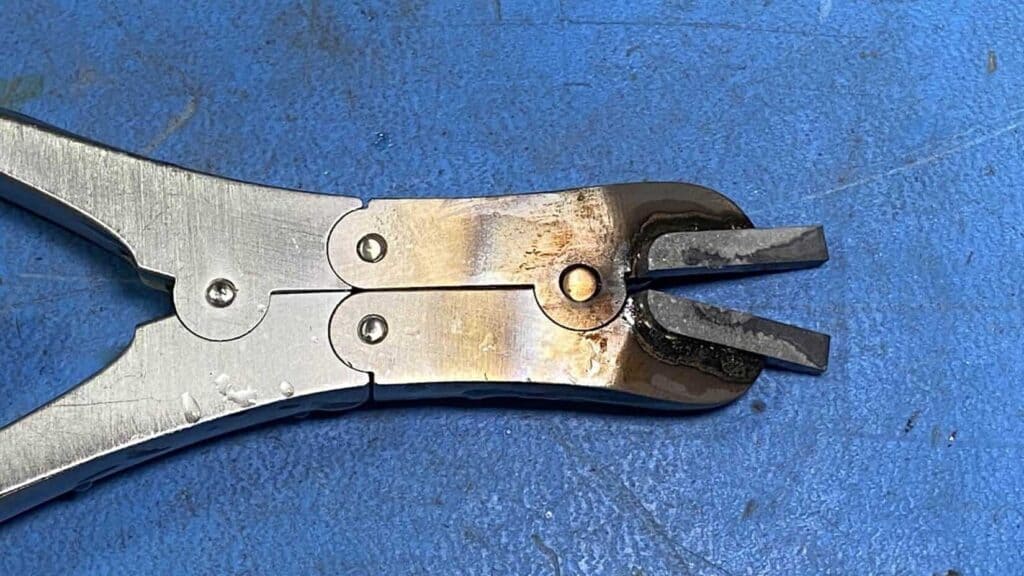
Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental https://dw-inductionheater.com/induction-brazing-carbide-tipping-of-medical-tools.html?feed_id=234808&_unique_id=65dae83c26fa5
Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

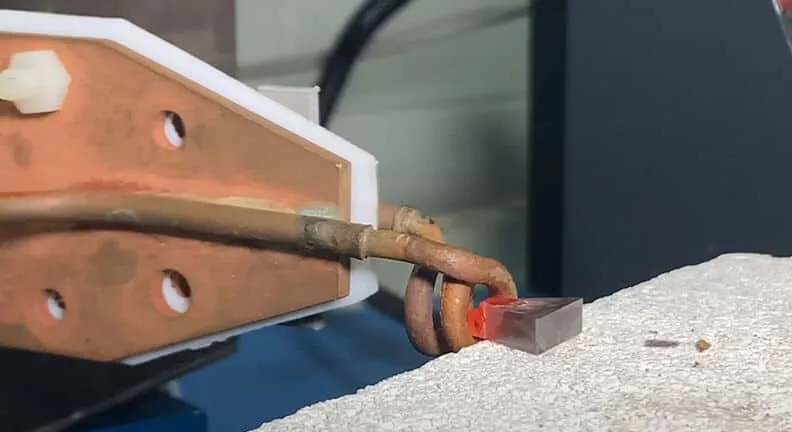
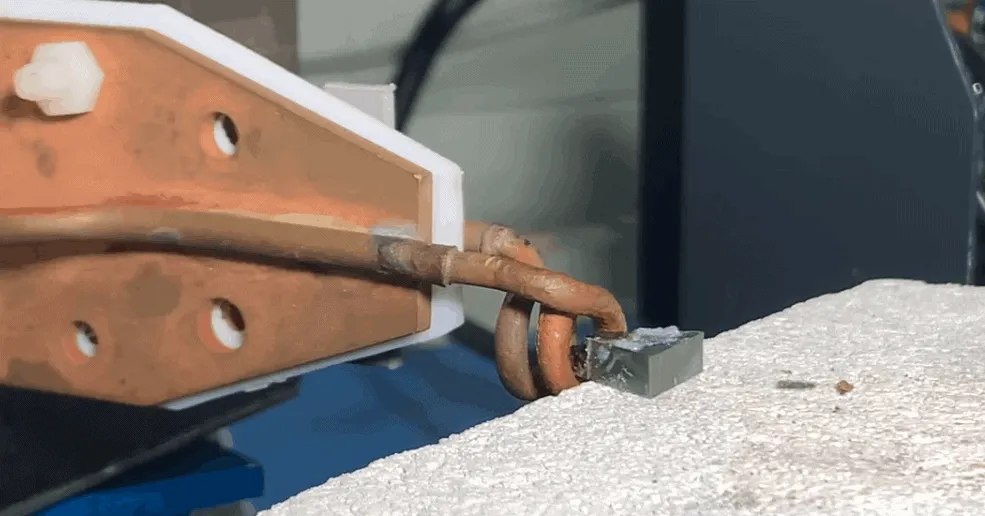
Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment   https://dw-inductionheater.com/induction-brazing-carbide-tipping-on-cutting-steel-tool.html?feed_id=234740&_unique_id=65da3174f13f0

2023年9月22日星期五

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment  

2023年8月28日星期一

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment  

2023年7月21日星期五

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment  

2023年7月3日星期一

Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental https://dw-inductionheater.com/induction-brazing-carbide-tipping-of-medical-tools.html?feed_id=217411&_unique_id=64a3711e8744b

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment   https://dw-inductionheater.com/induction-brazing-carbide-tipping-on-cutting-steel-tool.html?feed_id=217336&_unique_id=64a2ba7dc1281

2023年5月28日星期日

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment  

2023年5月3日星期三

Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental

2023年4月27日星期四

Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental
2023年4月22日星期六

Induction Brazing Carbide Tipping of Medical Tools

High Frequency Induction Brazing Carbide Tipping of Medical Tools Applications

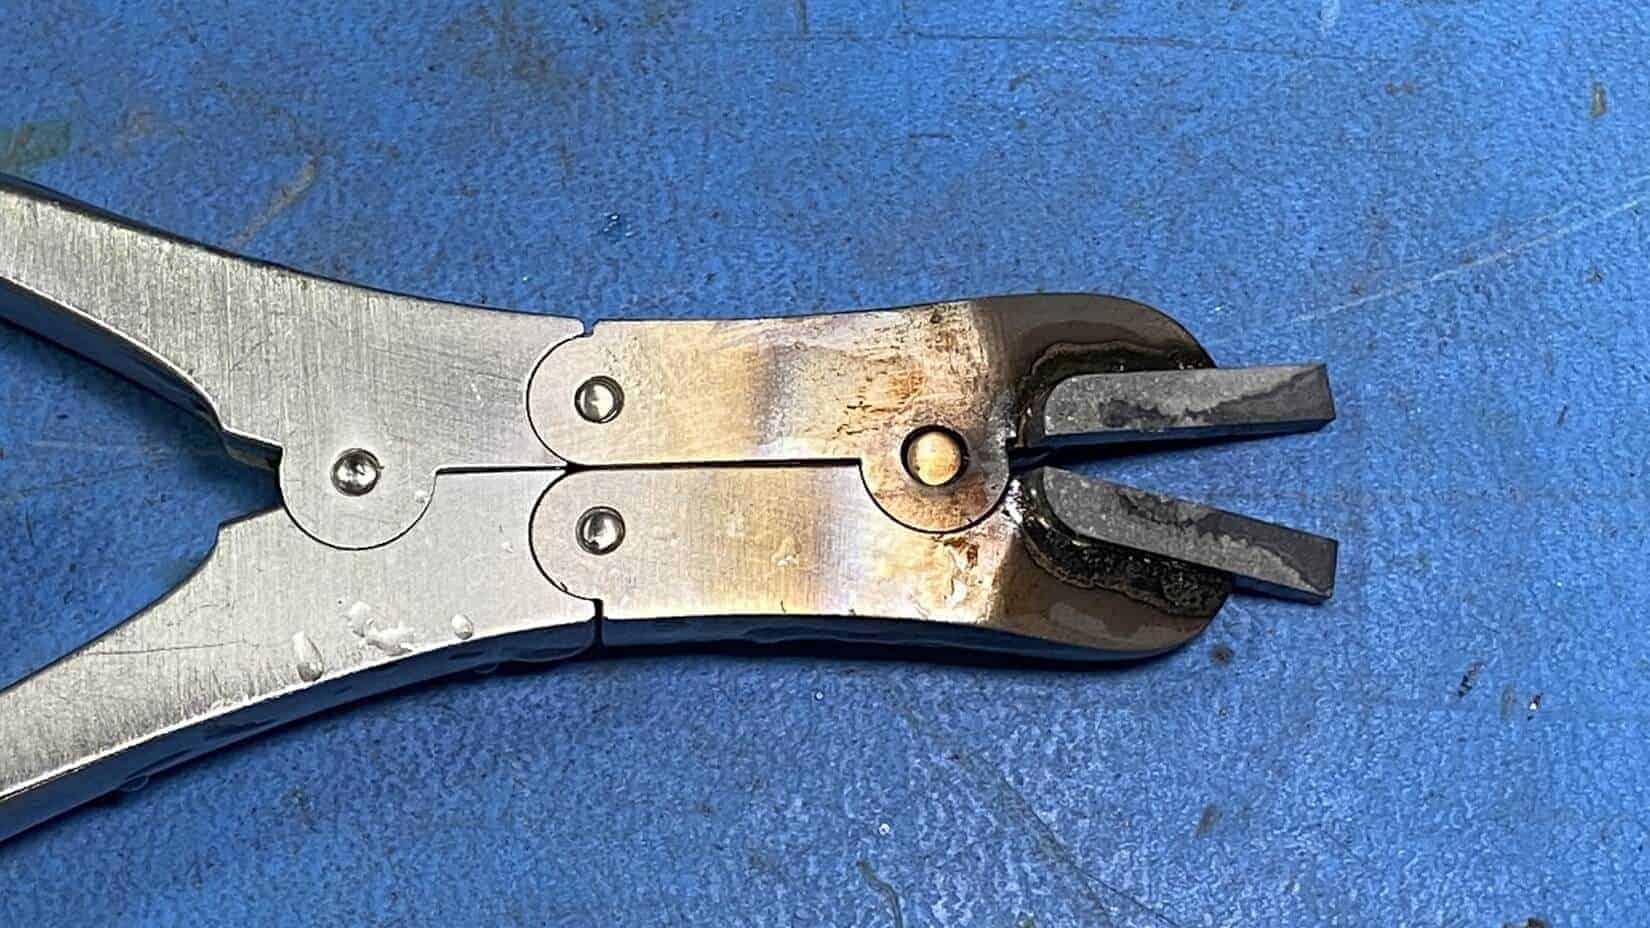
Carbide Tipping is specific induction brazing process by which a hardened tip material is applied to a base material to produce an extremely hard cutting edge. Objective: The objective of this application: Induction brazing carbide tipping of medical tools They would like to use induction heating technology to replace torches and achieve a cleaner brazing process. Induction Brazing Equipment: DW-HF-15 induction brazing equipment was set at 40% to complete the process. The adaptive digital phase control provides efficient operation in a wide frequency range.   Induction Brazing Process: A stainless-steel pin cutter 6 13/16” (17 cm) long with a 0.775” (1.96 cm) wide area for heating had to be brazed with two carbide inserts 25/32”(1.98 cm) long, 1/8” (7.8 mm) wide, 3/32” (2.54 cm) deep. There was an overlap 9/16” (1.42 cm) long, 1/8” (25.4 mm) wide (on each side of cutting head) and 1/16” (1.58 mm) deep. Brazing flux was applied to the joint area. The carbide inserts were then placed in between the pre-forms. The assembly was closed together and brought into the induction heating coil. Heat was applied for 8 seconds reaching the temperature of ~1400°F (760°C). The parts were successfully brazed together. Industry: Medical & Dental

2023年4月15日星期六

Induction Brazing Carbide Tipping on Cutting Steel Tool

Induction Brazing Carbide Tipping on Cutting Steel Tool Applications

Objective :  A leading manufacturer of CBN and PCD cutting tools wants to increase their productivity by focusing heat on a very small area in order to decrease heat loss and improve a carbide tipping process.    Induction Brazing Process:   The customer provided a triangle steel body, each side ~16.5 mm (0.65 inches). The induction brazing carbide tipping must be performed on a 3 mm (0.11 inches) equilateral triangle on the edge. The heating zone of the tool steel body is 43 mm (1.69 inches) OD x 25 mm (0.98 inches) in length.  DW-UHF-6kW-II  induction heating system was utilized to reach 1600 °F (870 °C) and complete the process in 8 seconds. A custom-designed coil concentrated the heat in the carbide tipping zone and minimized cycle time. Induction Brazing Equipment:   DW-UHF-6kW-II induction heating system  with a customized induction brazing coil was used to fit the process requirements. Industry: Tools & Equipment  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.