显示标签为“inductionbrazingsteel”的博文。显示所有博文

2024年4月10日星期三

High frequency induction brazing steel tube to steel fitting

High frequency induction brazing steel tube to steel fitting

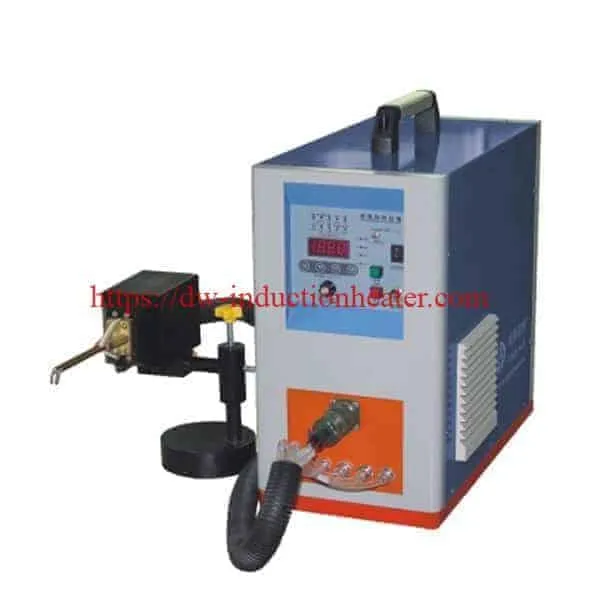
Objective Handheld high frequency induction brazing of a steel tube to a steel fitting Recommended Equipment The recommended equipment for this application is the DW-UHF-6KW-III handheld induction brazing heater heat station.
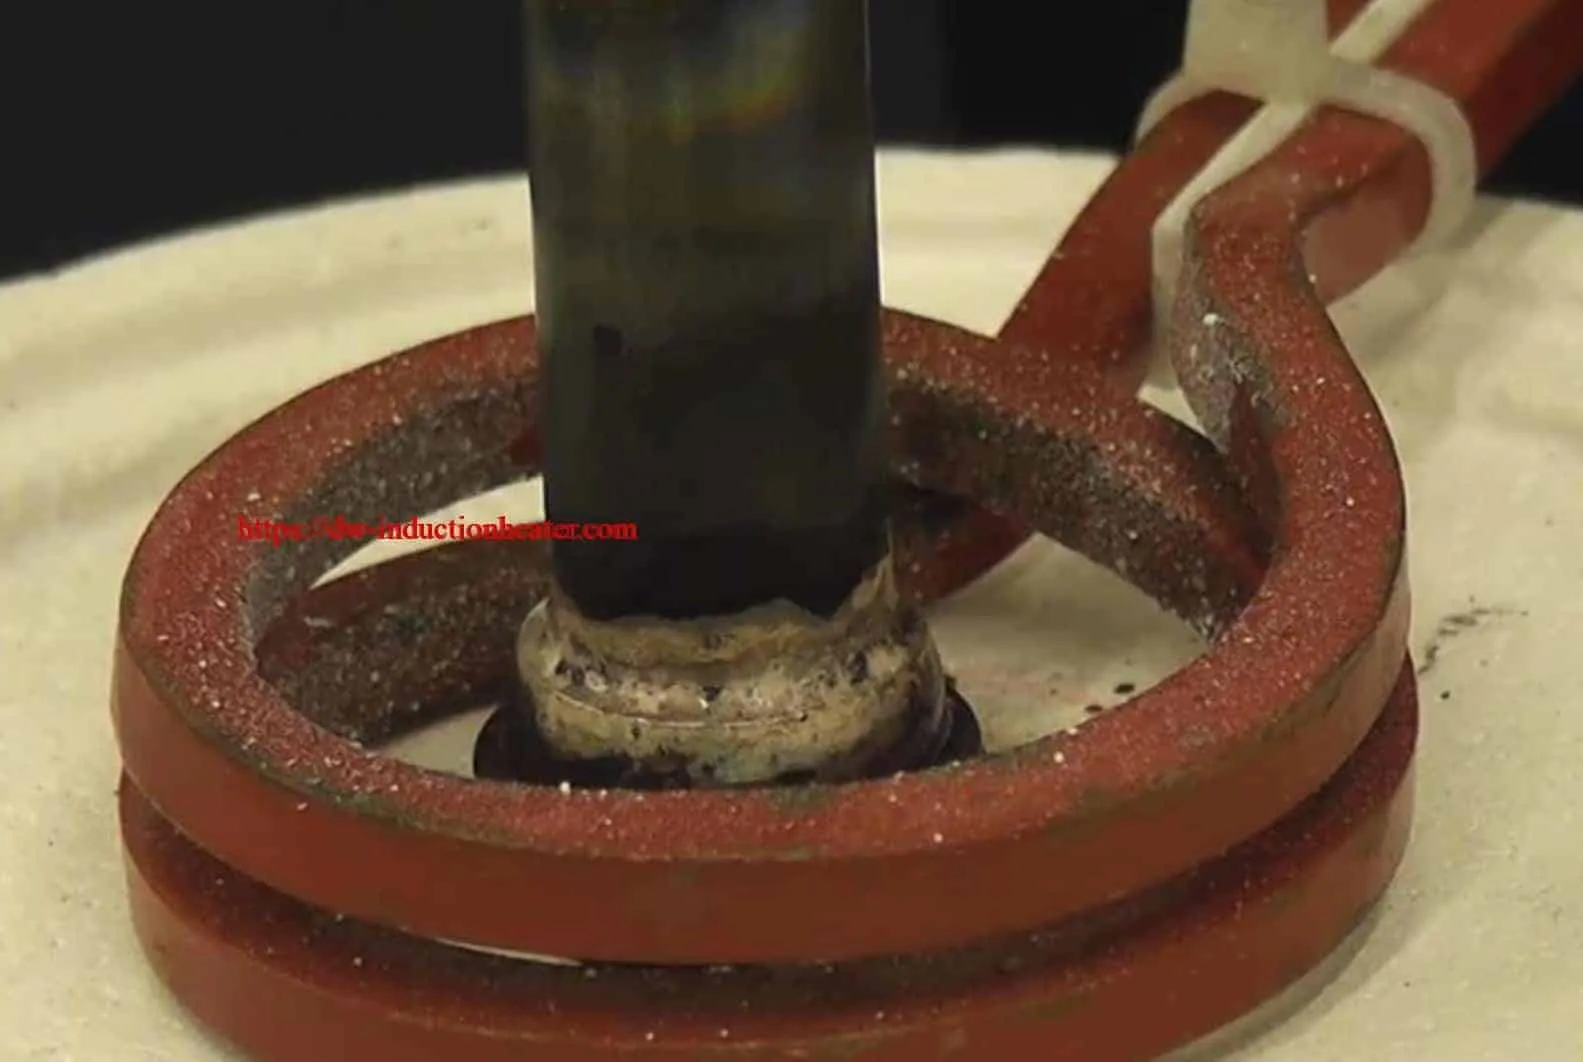
High frequency induction steel tube to steelHigh frequency induction brazing steel tubeHigh frequency induction brazing steel tube
Materials: Steel tube to steel fitting braze using Lucas-Milhaupt Easy FLO 3 brazing alloy rings and Harris Black Brazing Flux. Power: 3.5kW to 6.6kW Temperature: 1300°F to 1400°F (704°C to 760°C ) Time: 6 to 8 SecondsHandheld induction brazing heater  
Induction brazing steel tube to steel
  https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=240961&_unique_id=6616e47156a1e

2024年4月6日星期六

Induction Brazing Steel Parts to Tungsten Carbide Plate

Induction Brazing Steel Parts to Tungsten Carbide Plate

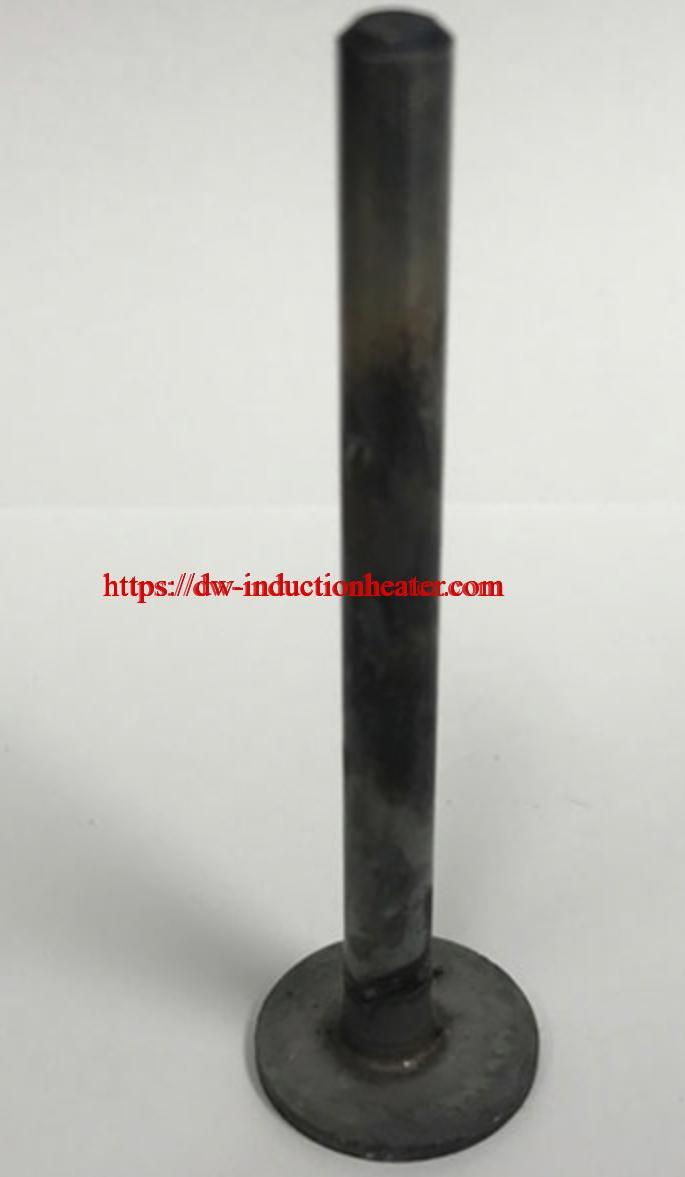
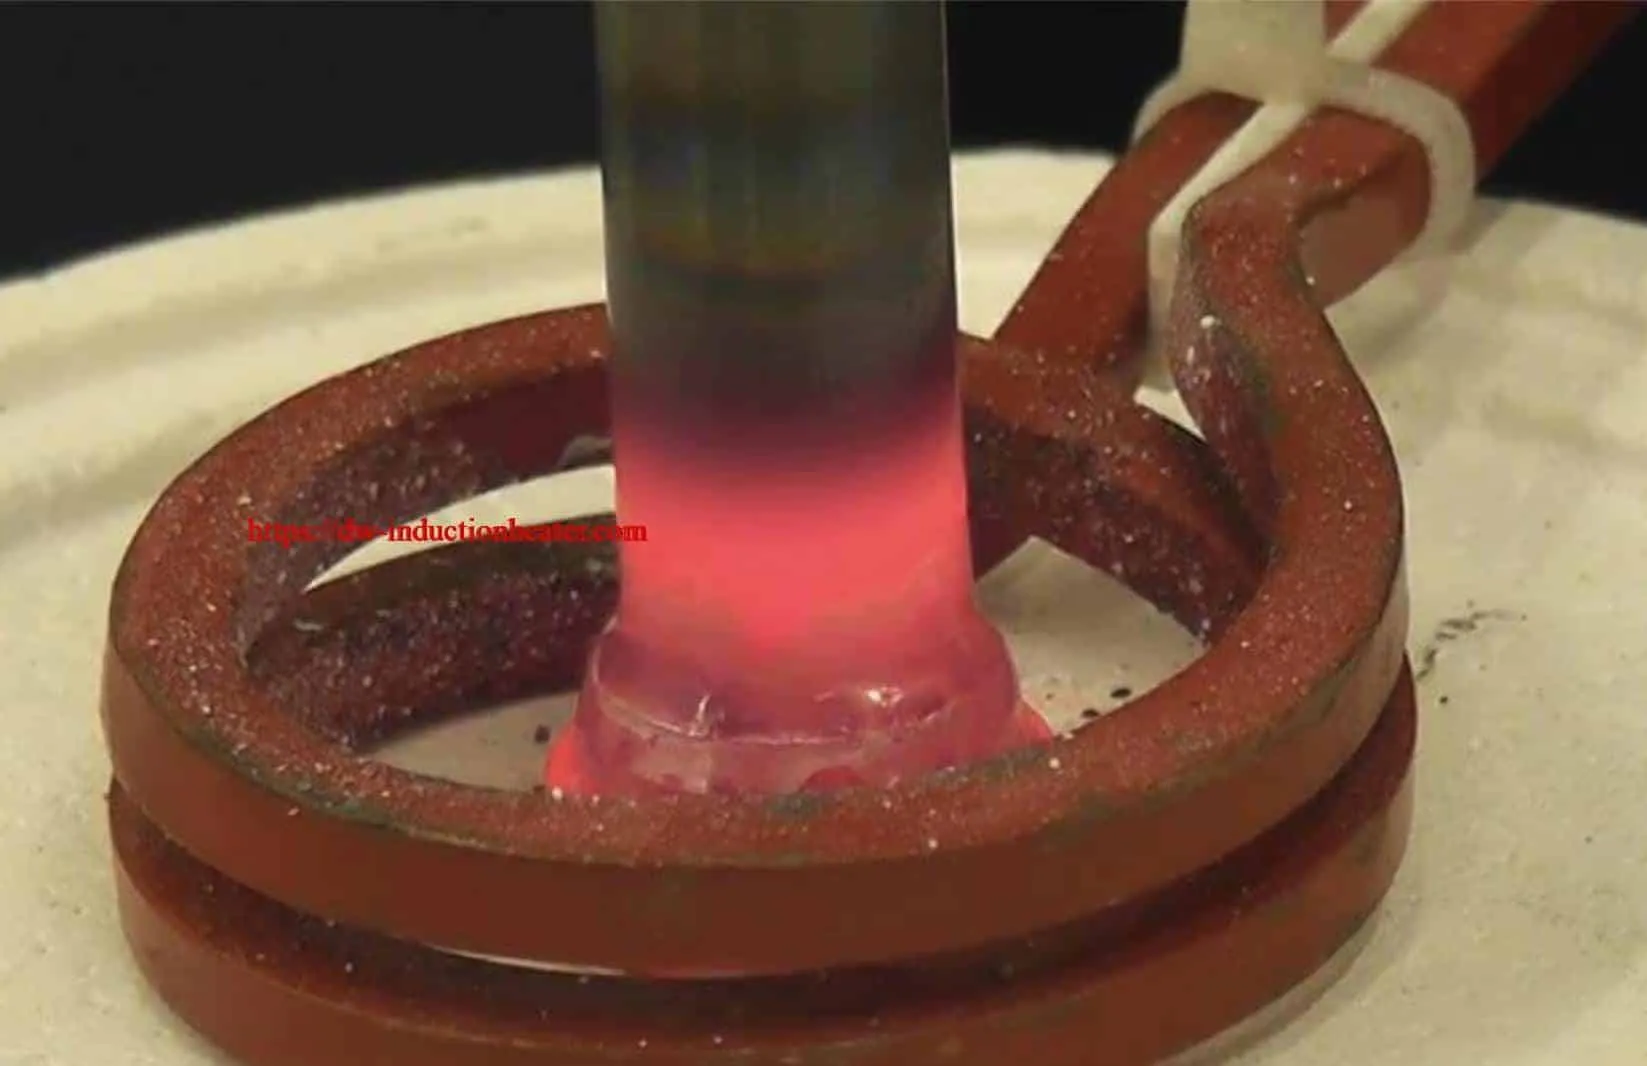
Objective Induction Brazing of Steel Parts to a Tungsten Carbide Plate Equipment DW-UHF-6KW-III handheld induction brazing machine Induction brazing steel parts
Test 1 Materials • Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length • Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness • Alloy: 19.05 mm (0.75″) Brazing discs Power: 4.0 kW Temperature: Approximately 760° C (1400° F) Time: 40 sec
Test 2 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 23 sec
Test 3 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 20-25 sec (Pulsing on/off)
Test 4 Materials • Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes • Alloy: 6.35 mm (0.25″) Brazing discs Power: 1.96 kW Temperature: Approximately 760° C (1400° F)Induction brazing steel carbideInduction brazing steel partsInduction brazing steel parts Time: 20 sec (Pulsing on/off)
Results and Conclusions: Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
  [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=240398&_unique_id=6611e4f0f237c

2023年11月14日星期二

Induction Brazing Steel Pipe

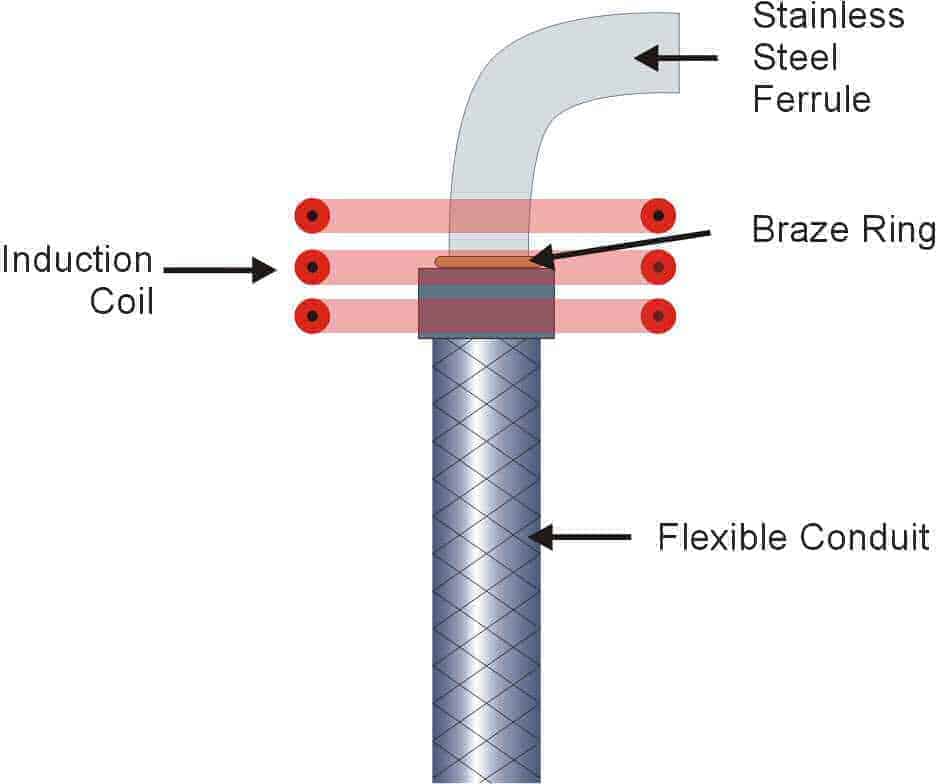
Induction Brazing Steel Pipe Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing. Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter Temperature 1400°F (760°C) Frequency 400 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application. Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow. Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time https://dw-inductionheater.com/induction-brazing-steel-pipe.html?feed_id=230736&_unique_id=6553f062b14a8

2023年10月31日星期二

Brazing Steel To Steel Pipe With Induction

Brazing Steel To Steel Pipe With Induction  Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube. Material • Steel tube, 1 inch (2.54 cm) OD • O-ring Face Seal sleeve and a male connector fittings • Preform braze rings • White SureFlow flux • Steel support mandrel Temperature 1300 ºF (704 ºC) Frequency 200 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF). • An induction heating coil designed and developed specifically for this application. Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows. Results/Benefits Advantages : • Large Inner diameter of coil allows for easy loading and unloading of parts • With efficient energy coupling of the coil to the fittings overheating is avoided. https://dw-inductionheater.com/brazing-steel-to-steel-pipe-with-induction.html?feed_id=229956&_unique_id=65415f6089eec

2023年10月27日星期五

Brazing Golf Ball With Induction

Brazing Golf Ball With Induction Objective: Heating steel golf ball mold to brazing dimple insert Material: Golf ball mold 2” in diameter, braze flux paste, dimple insert Temperature: 1400 ºF (760 ºC) Frequency: 260 kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A four turn helical coil is used to heat the golf ball mold to 1400ºF (760 ºC) in 3 minutes and the dimple insert is brazed to the mold with braze flux paste. Results/Benefits Induction heating provides: • No flame process. • Reliable, repeatable, non contact and energy efficient heat in minimal time. • Even distribution of heating. https://dw-inductionheater.com/brazing-golf-ball-with-induction.html?feed_id=229716&_unique_id=653ba8d7d30e9

2023年10月22日星期日

Induction Brazing Steel To Carbide Plate

Induction Brazing Steel To Carbide Plate Objective Brazing a steel piston valve assembly Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze Temperature 1350 ºF Frequency 100 kHz Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF • An induction heating coil designed and developed specifically for this application. Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces. Results/Benefits Induction heating provides: • Rapid localized heat, which can minimize oxidation and reduce cleaning after joining • Hands-free heating that involves no operator skill for manufacturing • Clean and controllable joints • Produces high quality repeatable parts https://dw-inductionheater.com/induction-brazing-steel-to-carbide.html?feed_id=229446&_unique_id=65353b9610f85

2023年10月20日星期五

Induction Brazing Steel Tips

Induction Brazing Steel Tips with Hihg Frequency Heating System Objective To heat a steel tip and shank assembly to 1300°F (704°C) within 3 seconds for brazing with induction heating instead of torch brazing. Material 0.1” (2.54mm) diameter steel tip & shank, 0.07” (1.78mm) diameter braze ring Temperature 1300°F (704°C) Frequency 800kHz Equipment DW-UHF-4.5kW induction heating system, remote heat station containing one 1.2 microfarad capacitor. Process A two turn helical coil is used to braze the dental parts. The braze ring is placed at the joint area of the steel tip and shank. Black flux is applied to the joint area. RF power is applied for 3 seconds to heat the parts to the established target temperature and the braze paste flows evenly and consistantly. Results/Benefits Induction heating provides: • Fast, accurate, repeatable heat • Ability to heat very small areas within precise production tolerances • Better joint quality, reduced oxidation • Increased production rates and reduced labor costs https://dw-inductionheater.com/induction-brazing-steel-tips.html?feed_id=229326&_unique_id=6532604040597

2023年10月19日星期四

Brazing Steel To Steel Pipe With Induction

Brazing Steel To Steel Pipe With Induction  Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube. Material • Steel tube, 1 inch (2.54 cm) OD • O-ring Face Seal sleeve and a male connector fittings • Preform braze rings • White SureFlow flux • Steel support mandrel Temperature 1300 ºF (704 ºC) Frequency 200 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF). • An induction heating coil designed and developed specifically for this application. Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows. Results/Benefits Advantages : • Large Inner diameter of coil allows for easy loading and unloading of parts • With efficient energy coupling of the coil to the fittings overheating is avoided.

2023年8月28日星期一

Induction Brazing Steel Tips

Induction Brazing Steel Tips with Hihg Frequency Heating System Objective To heat a steel tip and shank assembly to 1300°F (704°C) within 3 seconds for brazing with induction heating instead of torch brazing. Material 0.1” (2.54mm) diameter steel tip & shank, 0.07” (1.78mm) diameter braze ring Temperature 1300°F (704°C) Frequency 800kHz Equipment DW-UHF-4.5kW induction heating system, remote heat station containing one 1.2 microfarad capacitor. Process A two turn helical coil is used to braze the dental parts. The braze ring is placed at the joint area of the steel tip and shank. Black flux is applied to the joint area. RF power is applied for 3 seconds to heat the parts to the established target temperature and the braze paste flows evenly and consistantly. Results/Benefits Induction heating provides: • Fast, accurate, repeatable heat • Ability to heat very small areas within precise production tolerances • Better joint quality, reduced oxidation • Increased production rates and reduced labor costs

2023年8月18日星期五

High frequency induction brazing steel tube to steel fitting

High frequency induction brazing steel tube to steel fitting

Objective Handheld high frequency induction brazing of a steel tube to a steel fitting Recommended Equipment The recommended equipment for this application is the DW-UHF-6KW-III handheld induction brazing heater heat station.
High frequency induction steel tube to steelHigh frequency induction brazing steel tubeHigh frequency induction brazing steel tube
Materials: Steel tube to steel fitting braze using Lucas-Milhaupt Easy FLO 3 brazing alloy rings and Harris Black Brazing Flux. Power: 3.5kW to 6.6kW Temperature: 1300°F to 1400°F (704°C to 760°C ) Time: 6 to 8 SecondsHandheld induction brazing heater  
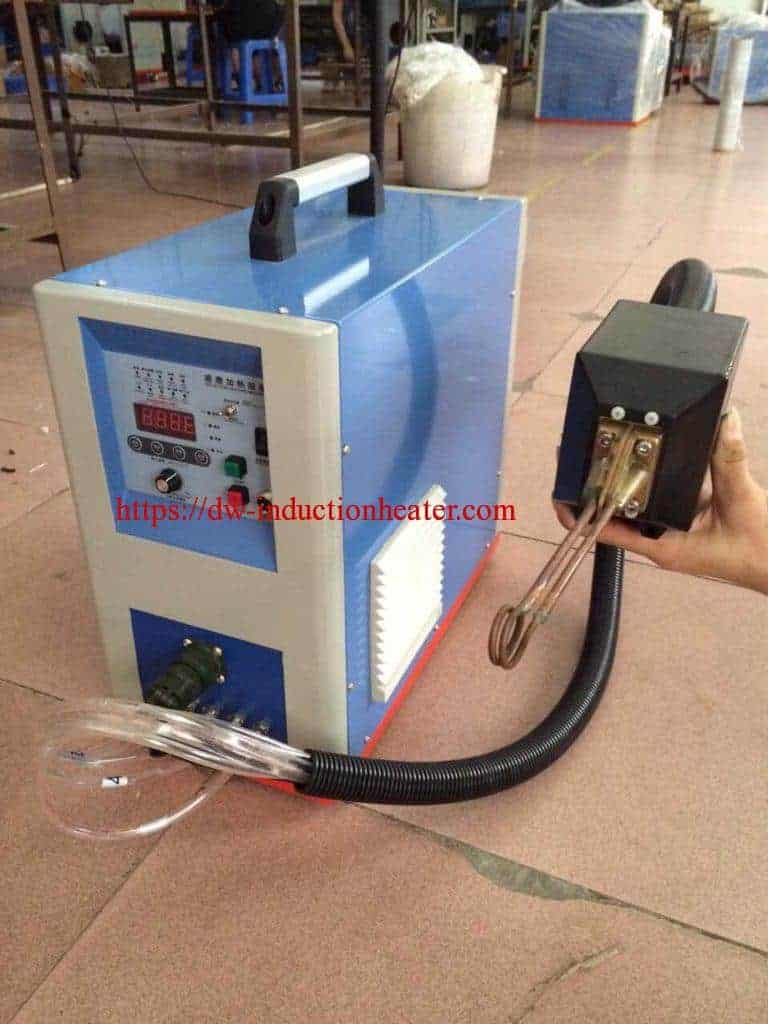
Induction brazing steel tube to steel
  https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=223786&_unique_id=64e03b5596e81

2023年8月15日星期二

Induction Brazing Steel Parts to Tungsten Carbide Plate

Induction Brazing Steel Parts to Tungsten Carbide Plate

Objective Induction Brazing of Steel Parts to a Tungsten Carbide Plate Equipment DW-UHF-6KW-III handheld induction brazing machine Induction brazing steel parts
Test 1 Materials • Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length • Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness • Alloy: 19.05 mm (0.75″) Brazing discs Power: 4.0 kW Temperature: Approximately 760° C (1400° F) Time: 40 sec
Test 2 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 23 sec
Test 3 Materials • Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness • Alloy: 12.7 mm (0.50″) Brazing discs Power: 2.36 kW Temperature: Approximately 760° C (1400° F) Time: 20-25 sec (Pulsing on/off)
Test 4 Materials • Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length • Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes • Alloy: 6.35 mm (0.25″) Brazing discs Power: 1.96 kW Temperature: Approximately 760° C (1400° F)Induction brazing steel carbideInduction brazing steel partsInduction brazing steel parts Time: 20 sec (Pulsing on/off)
Results and Conclusions: Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
  [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=223261&_unique_id=64db3a6f5a9d5

2023年8月9日星期三

Brazing Golf Ball With Induction

Brazing Golf Ball With Induction Objective: Heating steel golf ball mold to brazing dimple insert Material: Golf ball mold 2” in diameter, braze flux paste, dimple insert Temperature: 1400 ºF (760 ºC) Frequency: 260 kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A four turn helical coil is used to heat the golf ball mold to 1400ºF (760 ºC) in 3 minutes and the dimple insert is brazed to the mold with braze flux paste. Results/Benefits Induction heating provides: • No flame process. • Reliable, repeatable, non contact and energy efficient heat in minimal time. • Even distribution of heating.

2023年8月5日星期六

High frequency induction brazing steel tube to steel fitting

High frequency induction brazing steel tube to steel fitting

Objective Handheld high frequency induction brazing of a steel tube to a steel fitting Recommended Equipment The recommended equipment for this application is the DW-UHF-6KW-III handheld induction brazing heater heat station.
High frequency induction steel tube to steelHigh frequency induction brazing steel tubeHigh frequency induction brazing steel tube
Materials: Steel tube to steel fitting braze using Lucas-Milhaupt Easy FLO 3 brazing alloy rings and Harris Black Brazing Flux. Power: 3.5kW to 6.6kW Temperature: 1300°F to 1400°F (704°C to 760°C ) Time: 6 to 8 SecondsHandheld induction brazing heater  
Induction brazing steel tube to steel
 

2023年8月4日星期五

Induction Brazing Steel Tips

Induction Brazing Steel Tips with Hihg Frequency Heating System Objective To heat a steel tip and shank assembly to 1300°F (704°C) within 3 seconds for brazing with induction heating instead of torch brazing. Material 0.1” (2.54mm) diameter steel tip & shank, 0.07” (1.78mm) diameter braze ring Temperature 1300°F (704°C) Frequency 800kHz Equipment DW-UHF-4.5kW induction heating system, remote heat station containing one 1.2 microfarad capacitor. Process A two turn helical coil is used to braze the dental parts. The braze ring is placed at the joint area of the steel tip and shank. Black flux is applied to the joint area. RF power is applied for 3 seconds to heat the parts to the established target temperature and the braze paste flows evenly and consistantly. Results/Benefits Induction heating provides: • Fast, accurate, repeatable heat • Ability to heat very small areas within precise production tolerances • Better joint quality, reduced oxidation • Increased production rates and reduced labor costs

2023年7月19日星期三

Brazing Steel To Steel Pipe With Induction

Brazing Steel To Steel Pipe With Induction  Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube. Material • Steel tube, 1 inch (2.54 cm) OD • O-ring Face Seal sleeve and a male connector fittings • Preform braze rings • White SureFlow flux • Steel support mandrel Temperature 1300 ºF (704 ºC) Frequency 200 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF). • An induction heating coil designed and developed specifically for this application. Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows. Results/Benefits Advantages : • Large Inner diameter of coil allows for easy loading and unloading of parts • With efficient energy coupling of the coil to the fittings overheating is avoided.

2023年7月3日星期一

Induction Brazing Steel To Carbide Plate

Induction Brazing Steel To Carbide Plate Objective Brazing a steel piston valve assembly Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze Temperature 1350 ºF Frequency 100 kHz Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF • An induction heating coil designed and developed specifically for this application. Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces. Results/Benefits Induction heating provides: • Rapid localized heat, which can minimize oxidation and reduce cleaning after joining • Hands-free heating that involves no operator skill for manufacturing • Clean and controllable joints • Produces high quality repeatable parts

2023年7月2日星期日

Induction Brazing Steel Pipe

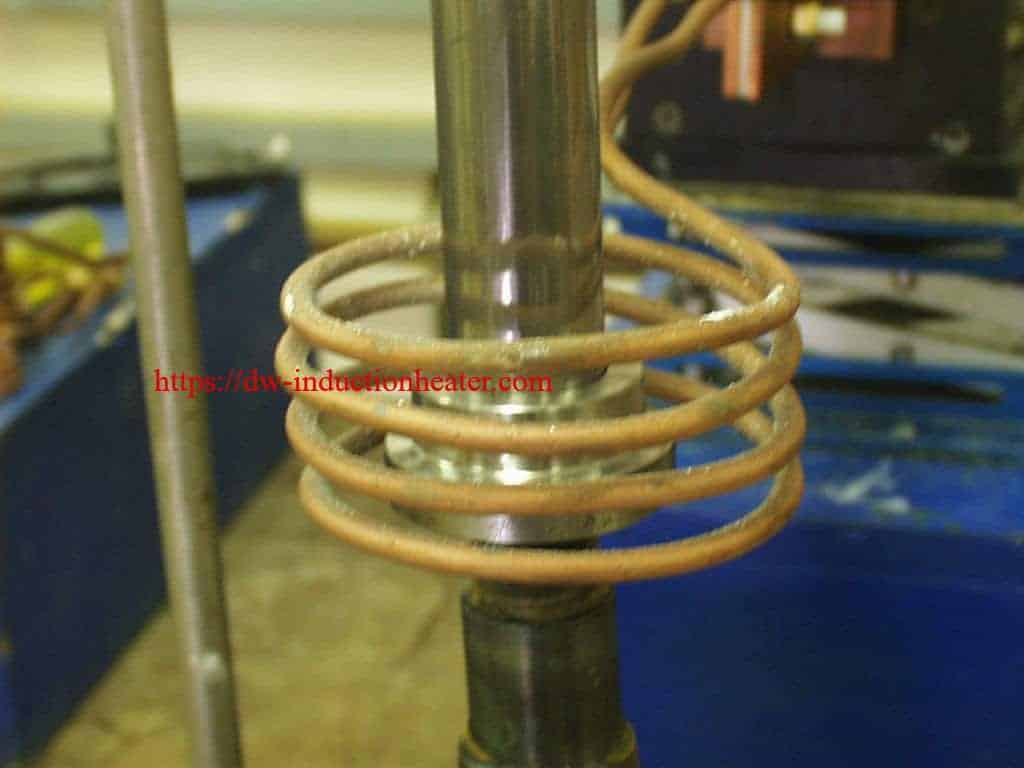
Induction Brazing Steel Pipe Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing. Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter Temperature 1400°F (760°C) Frequency 400 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application. Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow. Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年6月22日星期四

Brazing Steel To Steel Pipe With Induction

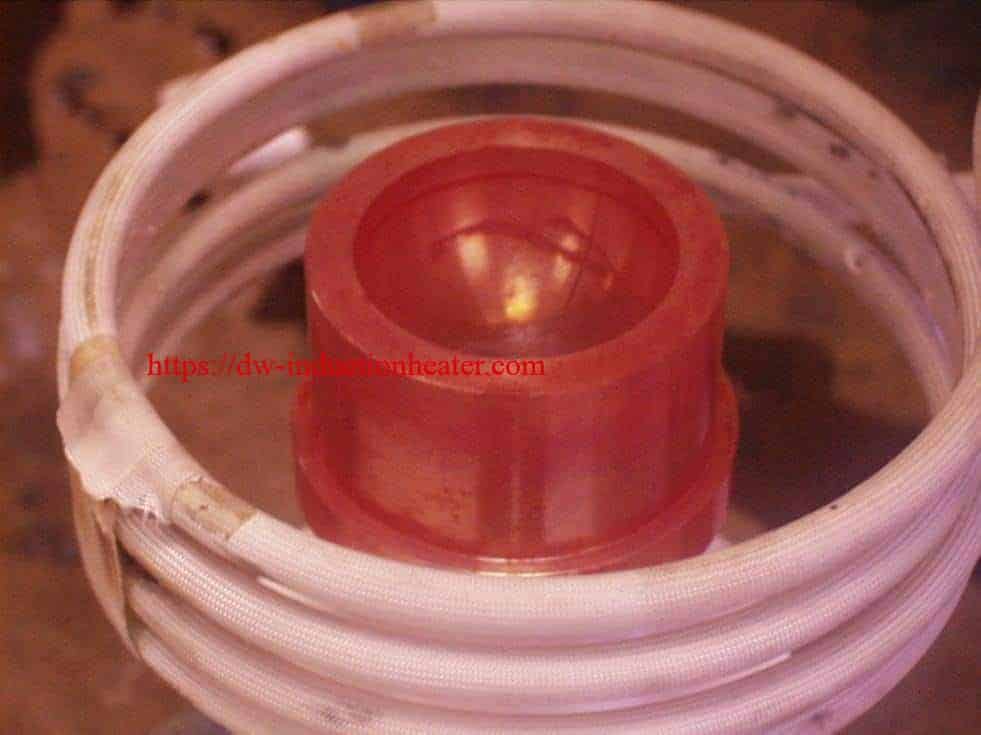
Brazing Steel To Steel Pipe With Induction  Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube. Material • Steel tube, 1 inch (2.54 cm) OD • O-ring Face Seal sleeve and a male connector fittings • Preform braze rings • White SureFlow flux • Steel support mandrel Temperature 1300 ºF (704 ºC) Frequency 200 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF). • An induction heating coil designed and developed specifically for this application. Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows. Results/Benefits Advantages : • Large Inner diameter of coil allows for easy loading and unloading of parts • With efficient energy coupling of the coil to the fittings overheating is avoided.
2023年5月30日星期二

Brazing Golf Ball With Induction

Brazing Golf Ball With Induction Objective: Heating steel golf ball mold to brazing dimple insert Material: Golf ball mold 2” in diameter, braze flux paste, dimple insert Temperature: 1400 ºF (760 ºC) Frequency: 260 kHz Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25 μF • An induction heating coil designed and developed specifically for this application. Process A four turn helical coil is used to heat the golf ball mold to 1400ºF (760 ºC) in 3 minutes and the dimple insert is brazed to the mold with braze flux paste. Results/Benefits Induction heating provides: • No flame process. • Reliable, repeatable, non contact and energy efficient heat in minimal time. • Even distribution of heating.

2023年5月13日星期六

Induction Brazing Steel To Carbide Plate

Induction Brazing Steel To Carbide Plate Objective Brazing a steel piston valve assembly Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze Temperature 1350 ºF Frequency 100 kHz Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF • An induction heating coil designed and developed specifically for this application. Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces. Results/Benefits Induction heating provides: • Rapid localized heat, which can minimize oxidation and reduce cleaning after joining • Hands-free heating that involves no operator skill for manufacturing • Clean and controllable joints • Produces high quality repeatable parts

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.