 Induction Brazing Steel Pipe
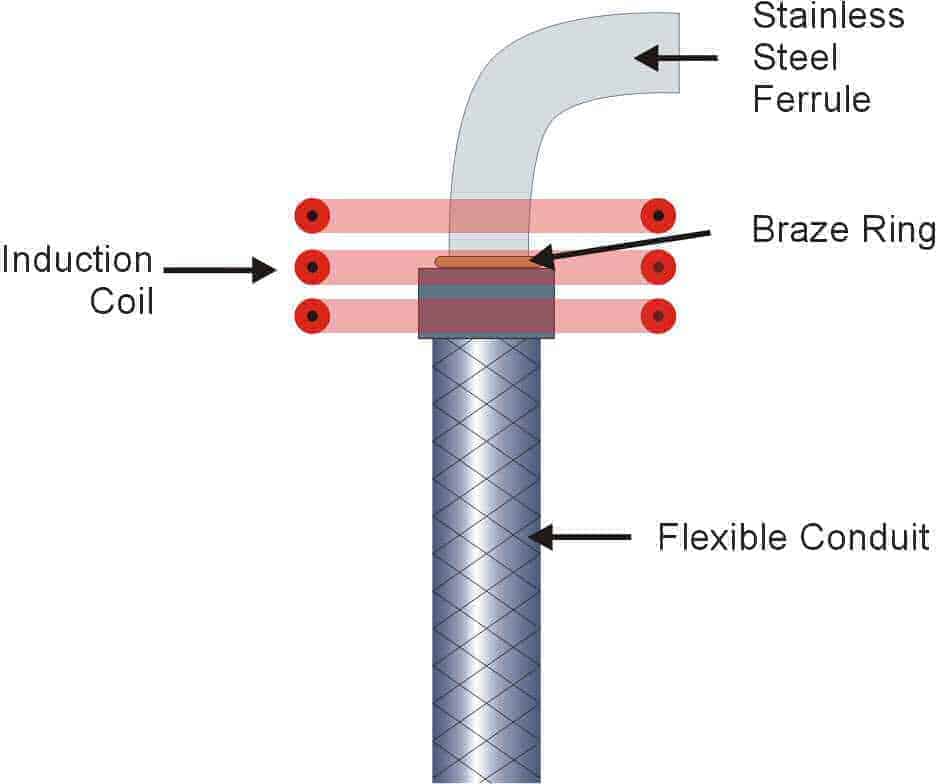
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
https://dw-inductionheater.com/induction-brazing-steel-pipe.html?feed_id=230736&_unique_id=6553f062b14a8
2023年11月14日星期二
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
https://dw-inductionheater.com/induction-brazing-steel-pipe.html?feed_id=230736&_unique_id=6553f062b14a8

2023年11月11日星期六
Brazing Copper Assemblies With Induction
 Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
https://dw-inductionheater.com/brazing-copper-assemblies-with-induction.html?feed_id=230556&_unique_id=654fa79fb26ea
2023年9月19日星期二
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年7月27日星期四
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年7月2日星期日
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年5月10日星期三
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年4月28日星期五
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年4月25日星期二
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年4月7日星期五
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年4月2日星期日
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年4月1日星期六
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年3月25日星期六
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2023年3月17日星期五
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年2月3日星期五
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2023年1月25日星期三
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2022年10月19日星期三
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2022年10月17日星期一
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2022年10月1日星期六
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
2022年7月22日星期五
Brazing Copper Assemblies With Induction
Brazing Copper Assemblies With Induction
Objective:To heat copper ‘T’ assemblies to 1400(760) ºF(ºC) for brazing
Material: Copper ‘T’ assemblies,Silver-copper eutectic braze,White flux
Temperature: 1400(760) ºF(ºC) Frequency: 250 kHz
Equipment: DW-UHF-20KW, 450 kHz solid state induction power supply with a remote heat station containing two 1.32 mF capacitors (total capacitance 0.66 mF). A custom-designed induction heating coil.
Process A custom double-wound pancake-helical coil combination is used to efficiently transfer RF Induction Heating power. Tests were conducted using temperature indicating paint to establish heating profiles and time-to-temperature. After the optimum time-totemperature of 3-5 minutes is established, a braze ring is placed at the joint and white flux applied to the joint area. The first joint on each piece takes 5 minutes with subsequent joints on the same copper piece taking much less time (~3 minutes).
Results/Benefits · Semi-automatic process reduces amount of operator laborinvolved· Easy and effective completion of braze joints
2022年6月28日星期二
Induction Brazing Steel Pipe
Induction Brazing Steel Pipe
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.