显示标签为“highfrequencysoldering”的博文。显示所有博文

2024年5月18日星期六

Induction Soldering Copper Tap

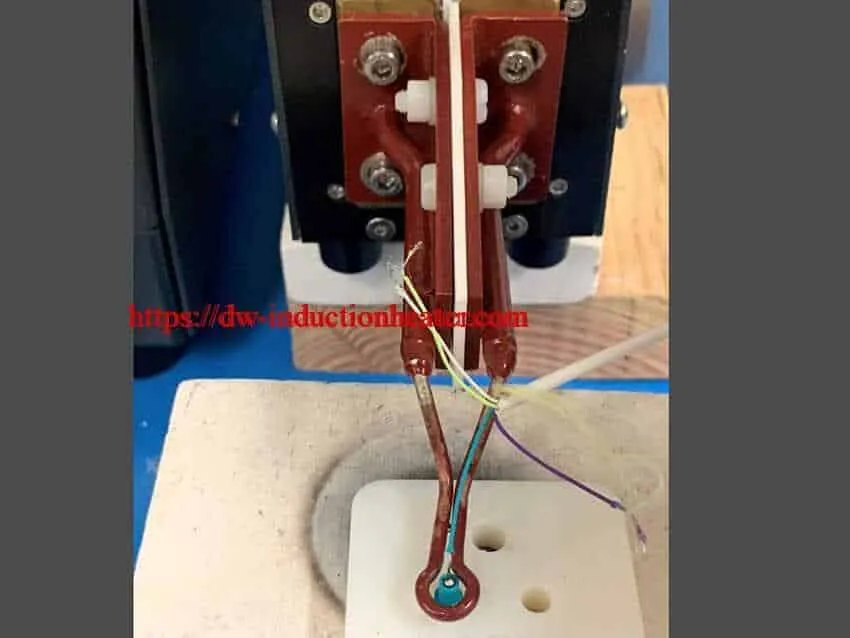
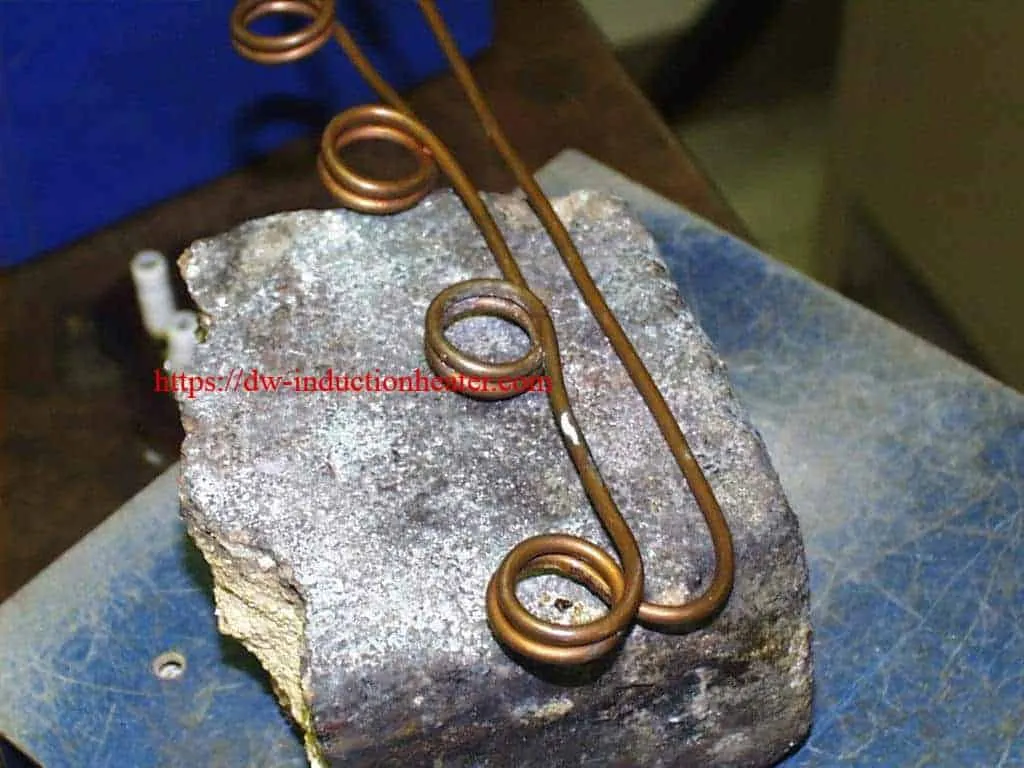
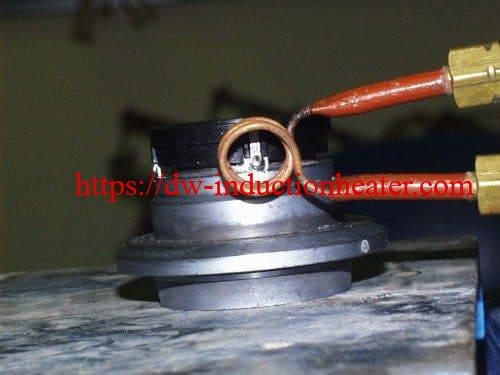
Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper https://dw-inductionheater.com/induction-soldering-copper-tap.html?feed_id=246140&_unique_id=664997f496486

2024年5月13日星期一

Induction Soldering Brass Connector

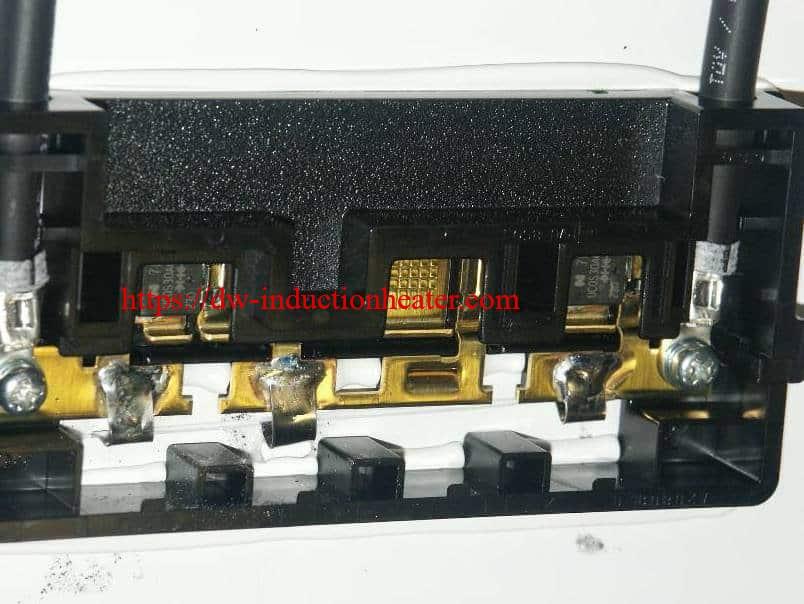
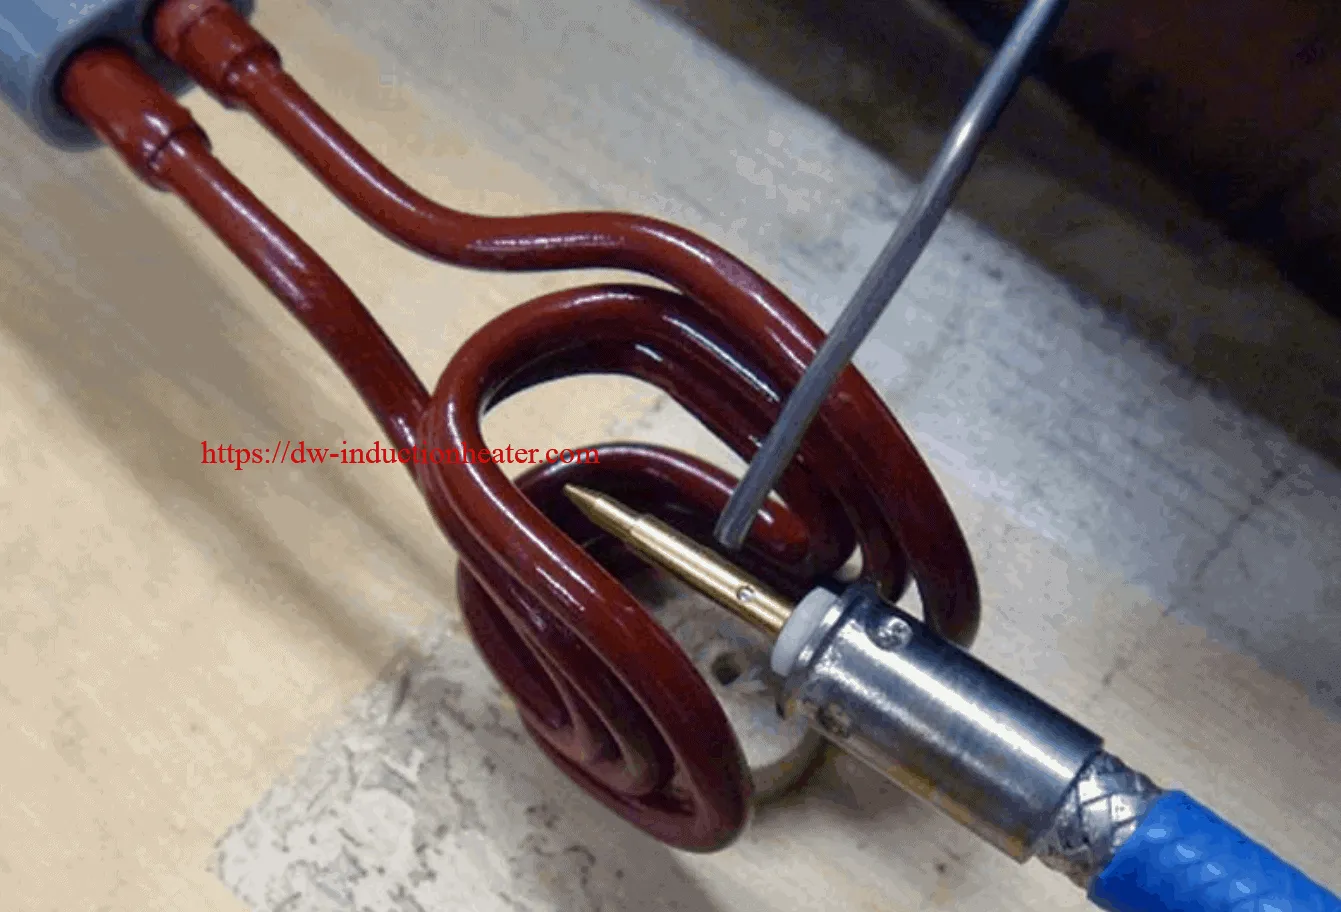
Induction Soldering Brass Connector In Solar Panel With IGBT Induction Heater Objective Solder three brass connectors one at a time in a solar panel junction box without affecting the components in the junction box Material Solar panel junction box, brass connectors, solder wire Temperature 700 ºF (371 ºC) Frequency 344 kHz Equipment • DW-UHF-6 kW induction heating system, equipped with a remote workhead containing one 1.0 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A three turn oval shaped helical coil is used to heat the connectors. A piece of solder wire is placed onto the joint area and each joint is heated separately for 5 seconds to solder the connector. The total process time is 15 seconds for the three joints. Results/Benefits Induction heating provides: • Pinpoint accuracy deliver heating only to joint; does not affect surrounding components • Localized heat produces neat and clean joints • Produces high quality, repeatable results • Even distribution of heating brass connectior               rf soldering brass connector               induction soldering brass connector https://dw-inductionheater.com/induction-soldering-brass-connector.html?feed_id=245392&_unique_id=6641bd1a8f93f

2024年5月12日星期日

Induction Soldering Fuse Caps

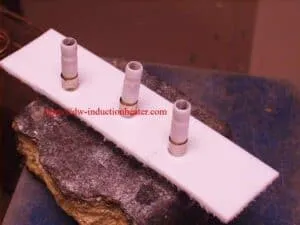
Induction Soldering Fuse Caps With IGBT Induction Heating Units Objective Soldering three fuse caps simultaneously to reflow lead free solder and make a joint between the fuse cap and fuse wire guide Material Plated copper end caps 0.375” (9.5mm) OD x 0.375” (9.5mm) height, ceramic fuse tube 1.5” tall (38.1mm) , lead free solder preforms Temperature 700 ºF (371 ºC) Frequency 286 kHz Equipment • DW-UHF-20 kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF • An induction heating coil designed and developed specifically for this application. Process A three position two turn helical coil is used to solder three fuse caps simultaneously. The fuse assemblies are placed in the coil and the heat is applied in three cycles at 3.5 seconds per cycle to reflow the solder. On the production line the bottom caps are soldered first. The fuses are filled with sand and without flipping the assembly the top cap is soldered. Results/Benefits Induction heating provides: • Consistent, repeatable results • Precise & accurate heat application • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil             Soldering Fuse Caps https://dw-inductionheater.com/induction-soldering-fuse-caps.html?feed_id=245324&_unique_id=66410655105d3
2024年4月2日星期二

Induction Soldering Brass Corner Joint

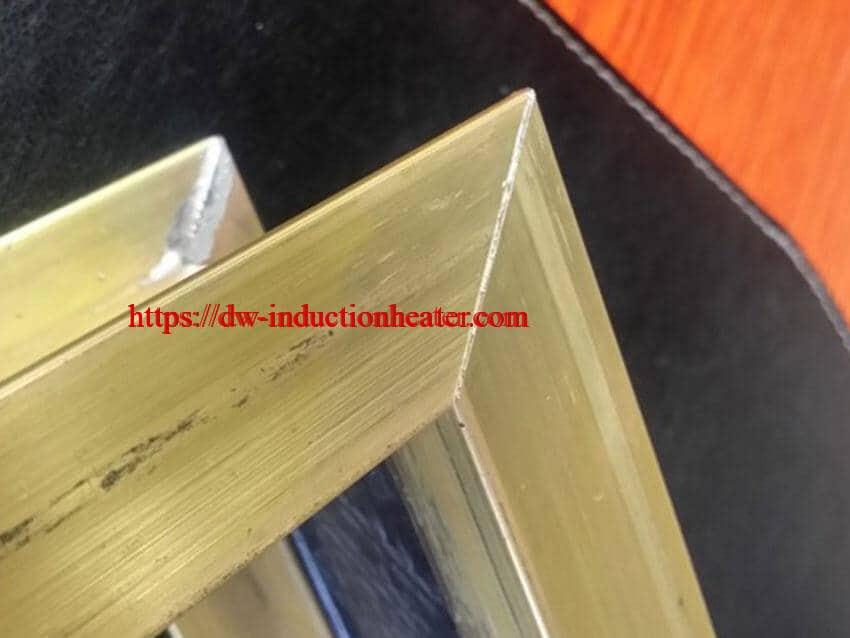
Hig Frequency Induction Soldering Brass Corner Joint

Objective Successfully solder two 45° brass corner joints. Equipment: DW-UHF-10kw induction soldering heater Materials StayBrite #8 silver solder supplied by customer Bridgit solder flux supplied by customer Brass corner joint Pancake coil Key Parameters Power: 5.5 kW Temperature: Approximately 550° F (288° C) Time: 20 sec
Process:
  1. Flux is applied at all joints.
  2. The assembly is positioned into for heating
  3. Induction heating is applied for 15 sec
  4. The brazing rod is applied to the joint
Results/Benefits:
  1. Since the brazing alloy is manually fed, the coil is placed under the joint, facing the visible side of the frame. The visible side of the joint is laying on a flat wooden surface, which does not allow the brazing alloy to leak and spill. This keeps the visible surface nice and clean, while the seam is internally brazed.
  2. If solder paste is used, then the coil can be placed on top of the joint. If special dual coil is used, then both joints (top and bottom) can be done with one shot.
  3. No frame flipping is needed in this case. See the video and zoom the pictures attached for more details.
  4. No special cleaning is needed on either side of the joint. The samples on the pictures have been paper towel wiped only.
https://dw-inductionheater.com/induction-soldering-brass-corner-joint.html?feed_id=239730&_unique_id=660c2e3872b24

2024年3月30日星期六

high frequency induction soldering wire to connector

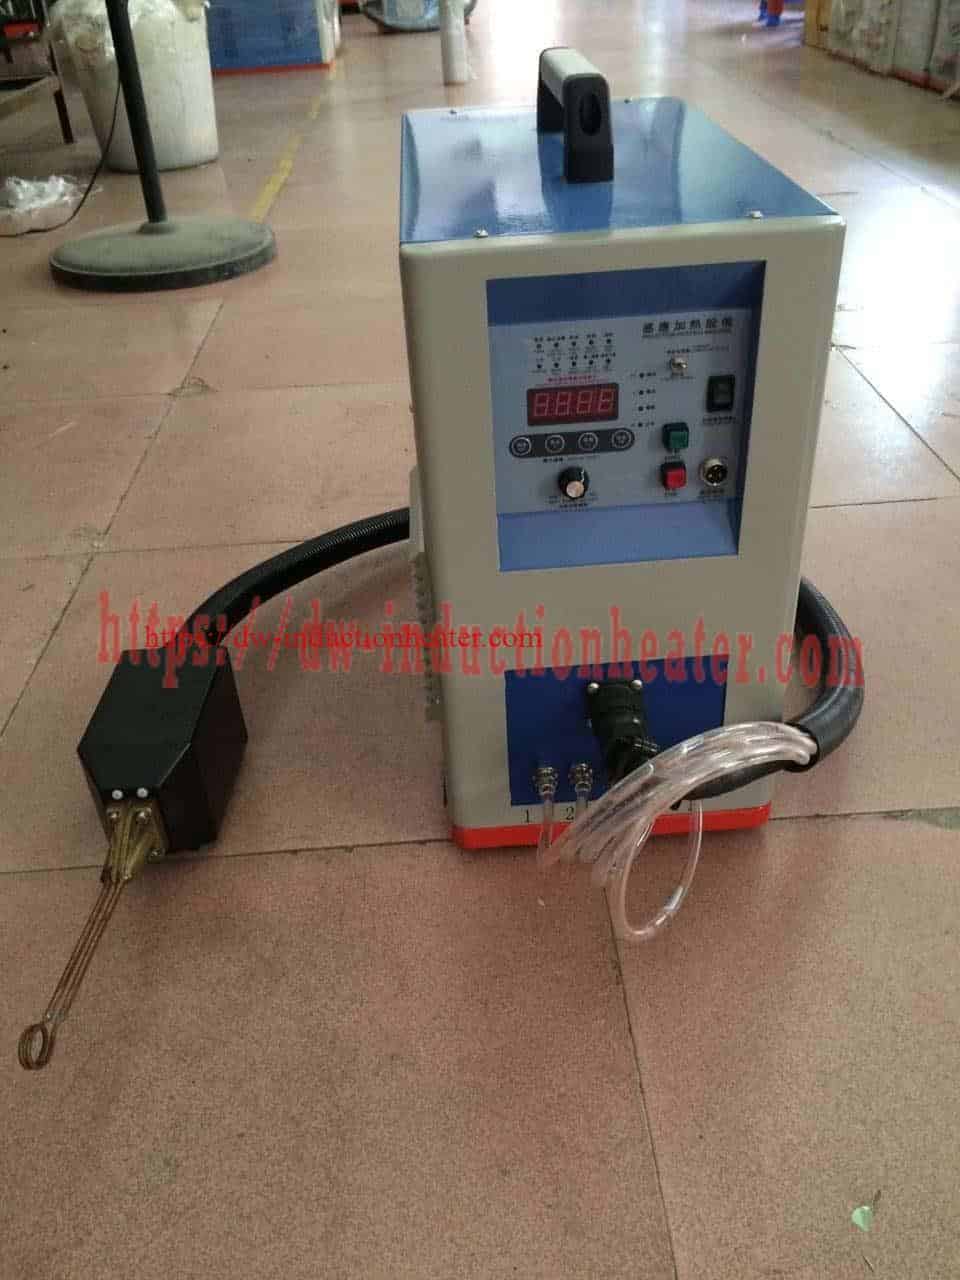
Objective The purpose of this test is to demonstrate the induction soldering wire to connector Recommended Equipment The recommended equipment for this test is the with the customized induction heating coil.  DW-UHF-6KW-I handheld induction heater
Key Parameters Power: Up to 0.48 kW Temperature: 392°F (200°C) Time: 1.5 seconds
Process and Results: This induction soldering wire to connector process was quick yet effective. The unit was run at 985 kHz, the reason for using such a high frequency was to couple into the small diameter of the wires. The whole process from the heat being turned on to the hardening of the solder took 1.5 seconds. Previously a soldering iron was being used to complete this task, however induction soldering was proven to be much faster and more efficient. The process can now be automated on an assembly line, because the system can remotely be turned on.
https://dw-inductionheater.com/high-frequency-induction-soldering-wire-to-connector.html?feed_id=239324&_unique_id=66089c76922a3

2024年3月29日星期五

Induction Soldering Cable to Metallic Plate

Objective The purpose of this test is to demonstrate the induction soldering cable to metallic plate process. Recommended Equipment The recommended equipment for this test is the DW-UHF-6kw-I handheld induction heater.
Key Parameters Power: Up to 0.72 kW Temperature: 482°F (250°C) Time: 4.5 seconds to 14 seconds
Results and Conclusions: The results were satisfactory at 14 seconds. The complete process can be achieved in less than 5 seconds by increasing the frequency from under 200 kHz to over 300 kHz, as well as by increasing the induction heating power
https://dw-inductionheater.com/induction-soldering-cable-to-metallic-plate.html?feed_id=239159&_unique_id=66072ec213f44

2024年3月28日星期四

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
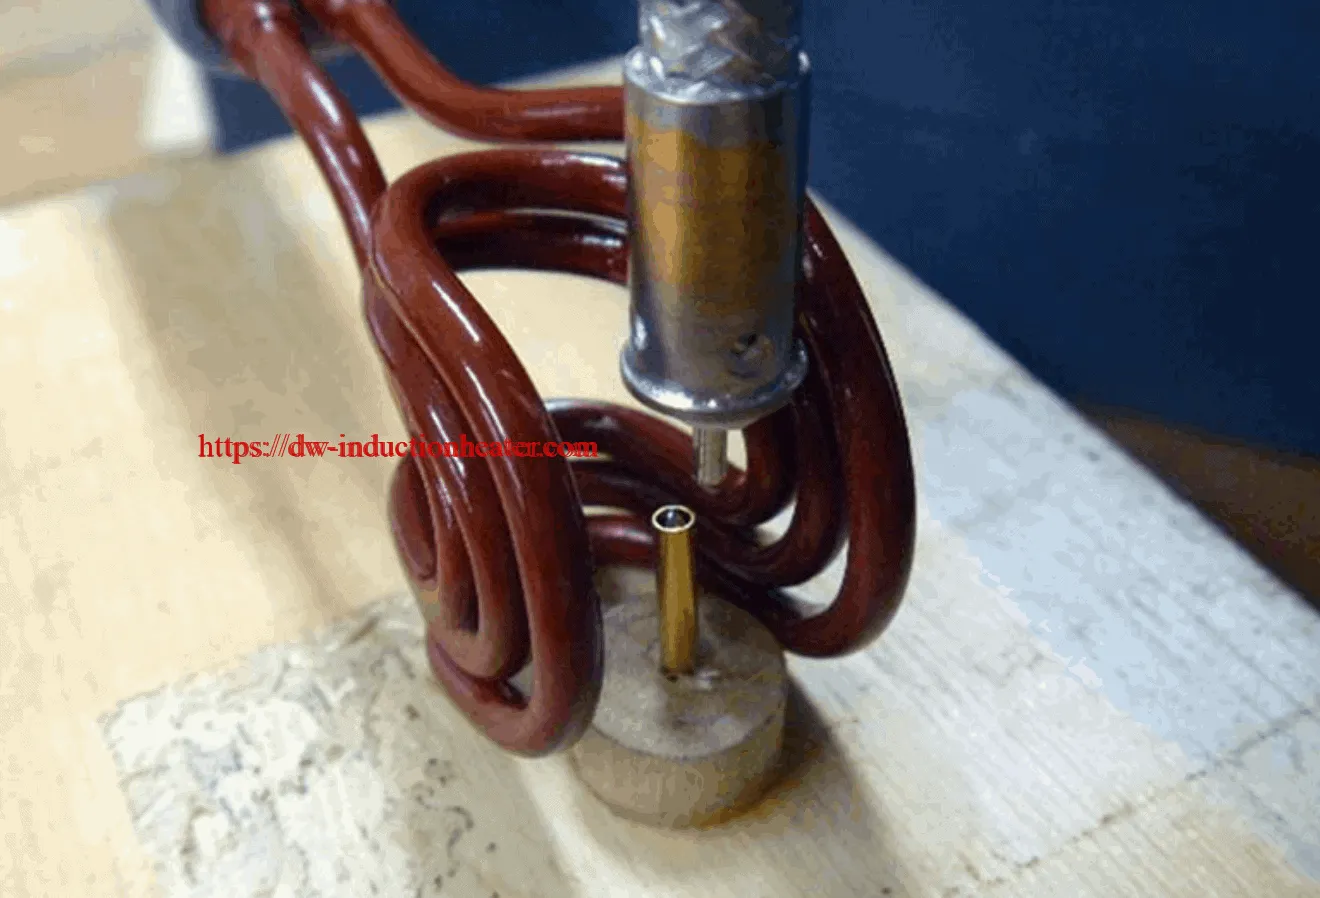
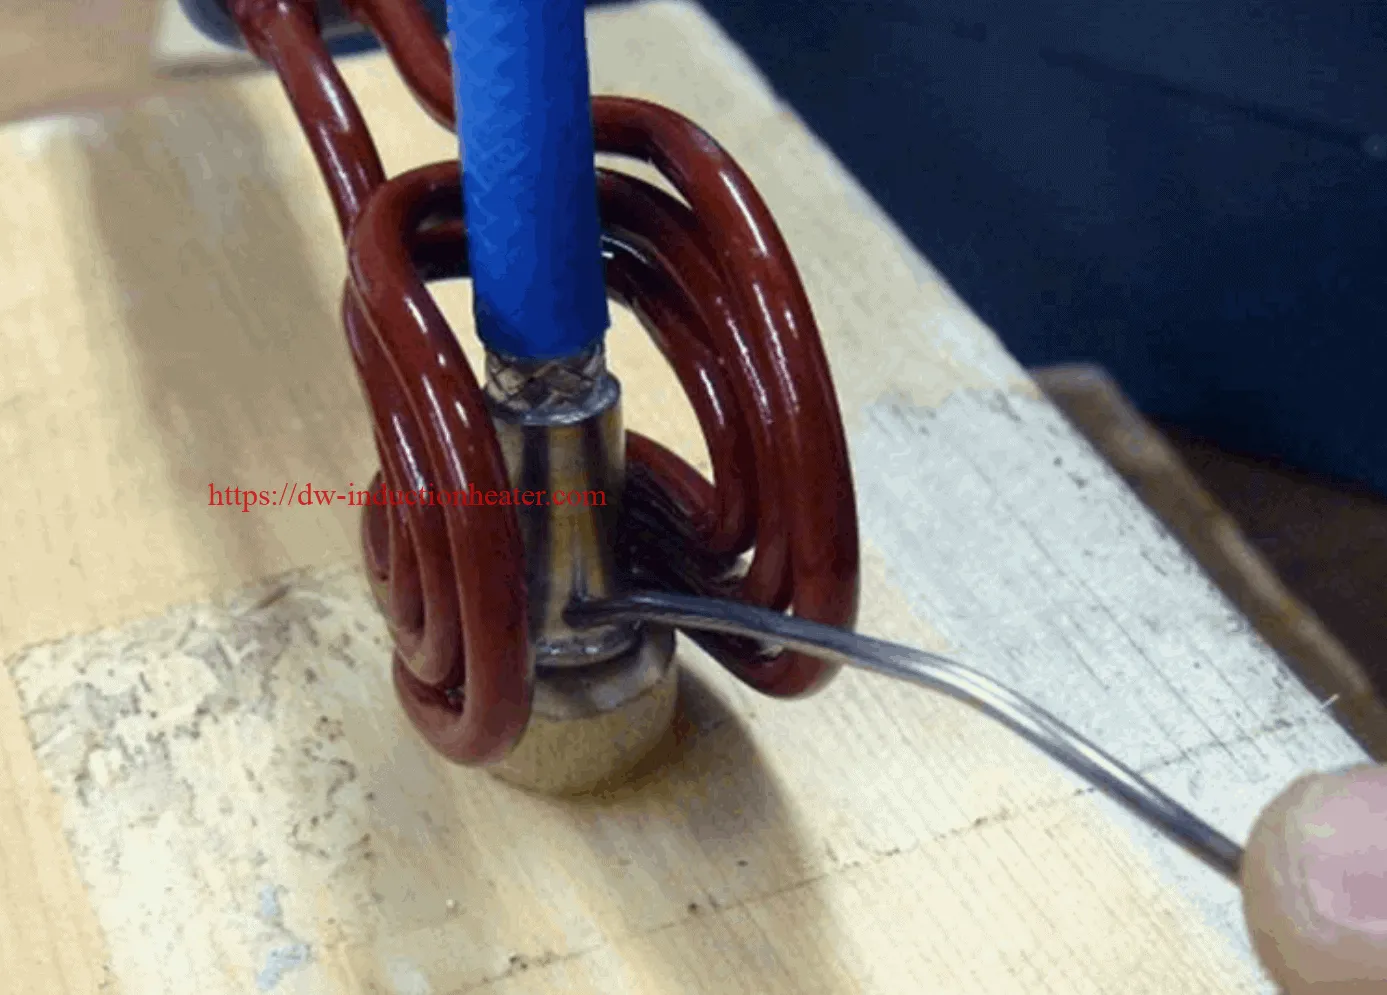
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 
https://dw-inductionheater.com/induction-soldering-coaxial-cable-to-connector-ring.html?feed_id=239023&_unique_id=6605c12449b39

2024年3月10日星期日

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]
https://dw-inductionheater.com/induction-soldering-coaxial-cable.html?feed_id=235992&_unique_id=65ed79a0e0191

2024年3月9日星期六

High frequency Induction Soldering Brass Tubes

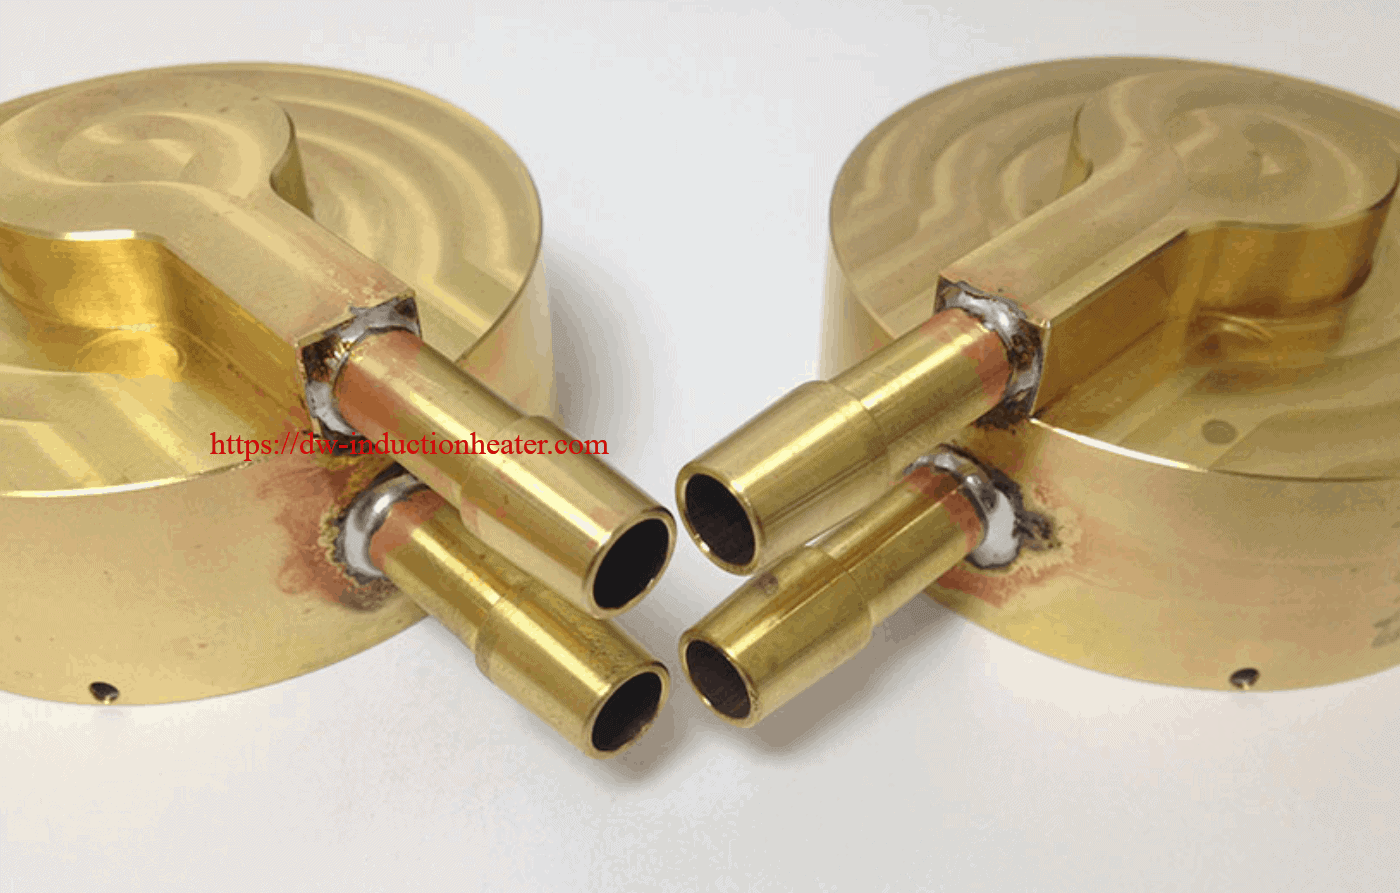
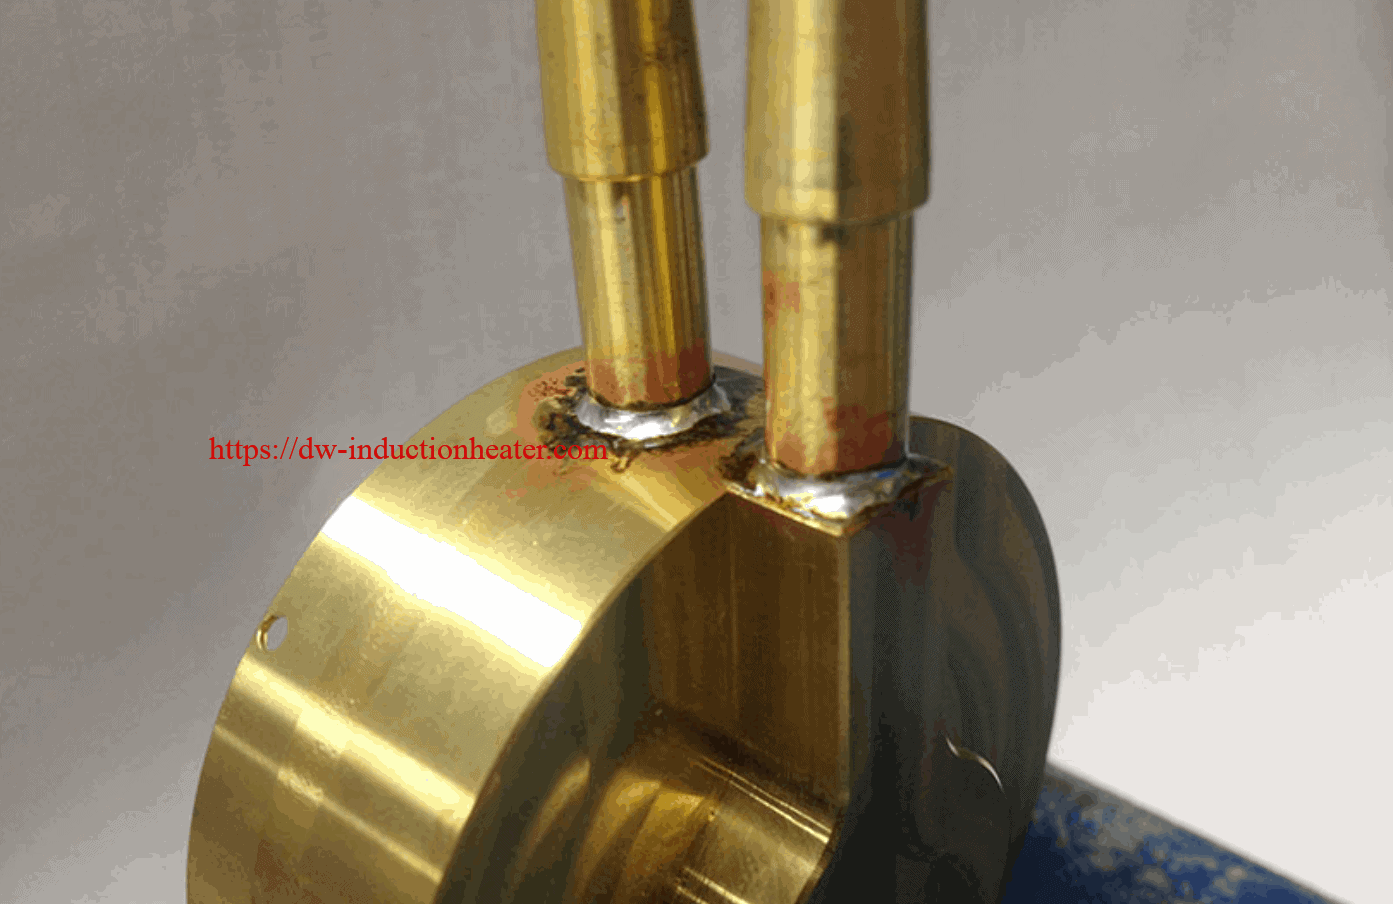
Objective To simultaneously high frequency Induction Soldering Brass Tubessolder to a brass water jacket assembly with induction heating. Equipment DW-HF-15KW Induction Heating Machine induction heating machine Key Parameters Power: 5 kW Temperature: 424°F (217°C) Time: 10 seconds until the alloy flows; 15 seconds to allow alloy to even out around the tube.
TEST 1
Materials • Brass water jacket assembly • Lead-free solder alloy • Utility paste soldering flux
TEST 2
Materials • Brass water jacket assembly • Lead-free solder alloy • Utility paste soldering flux
Results: Brass inlet/outlet tubes were successfully brazed to the brass assembly with induction heating. The piece needs to be positioned so that the tube is close to the end of the coil. The solder joint on the thin wall of the assembly will reach soldering temperature in 10 seconds. The second solder joint will reach soldering temperature an average of 10 seconds later (15 seconds total). An additional 5 seconds of heating might be necessary to allow the solder to flow evenly around the tubes to improve final quality and appearance.
[wpforms id="3947"] https://dw-inductionheater.com/high-frequency-induction-soldering-brass-tubes.html?feed_id=235957&_unique_id=65ecc2a89608e

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.