显示标签为“highfrequencysolderingmachine”的博文。显示所有博文

2024年3月28日星期四

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
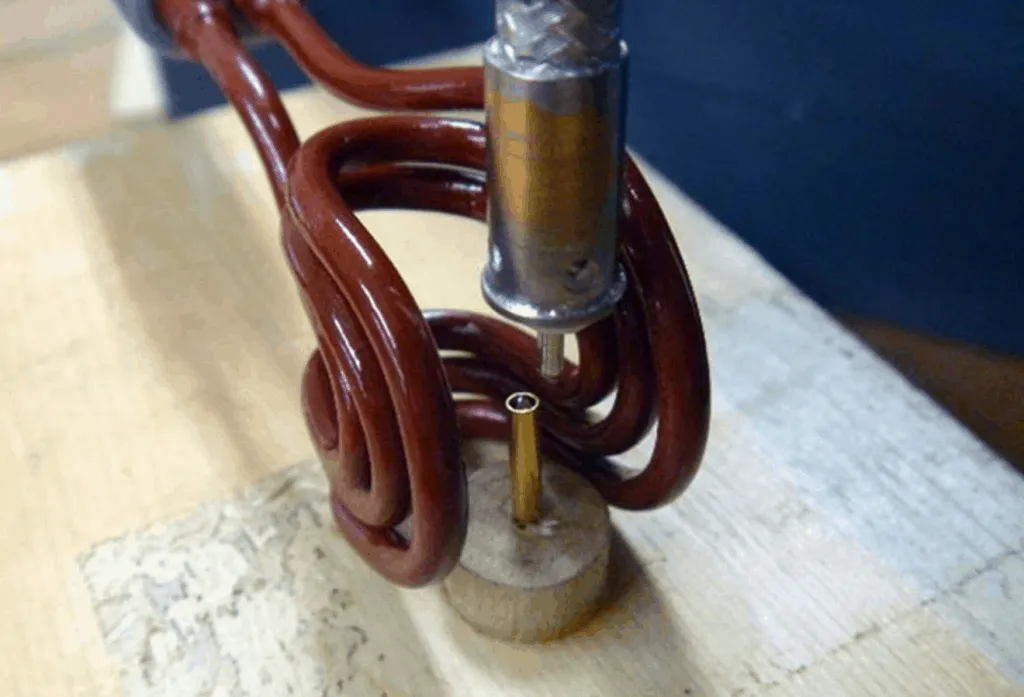
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 
https://dw-inductionheater.com/induction-soldering-coaxial-cable-to-connector-ring.html?feed_id=239023&_unique_id=6605c12449b39

2023年8月5日星期六

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
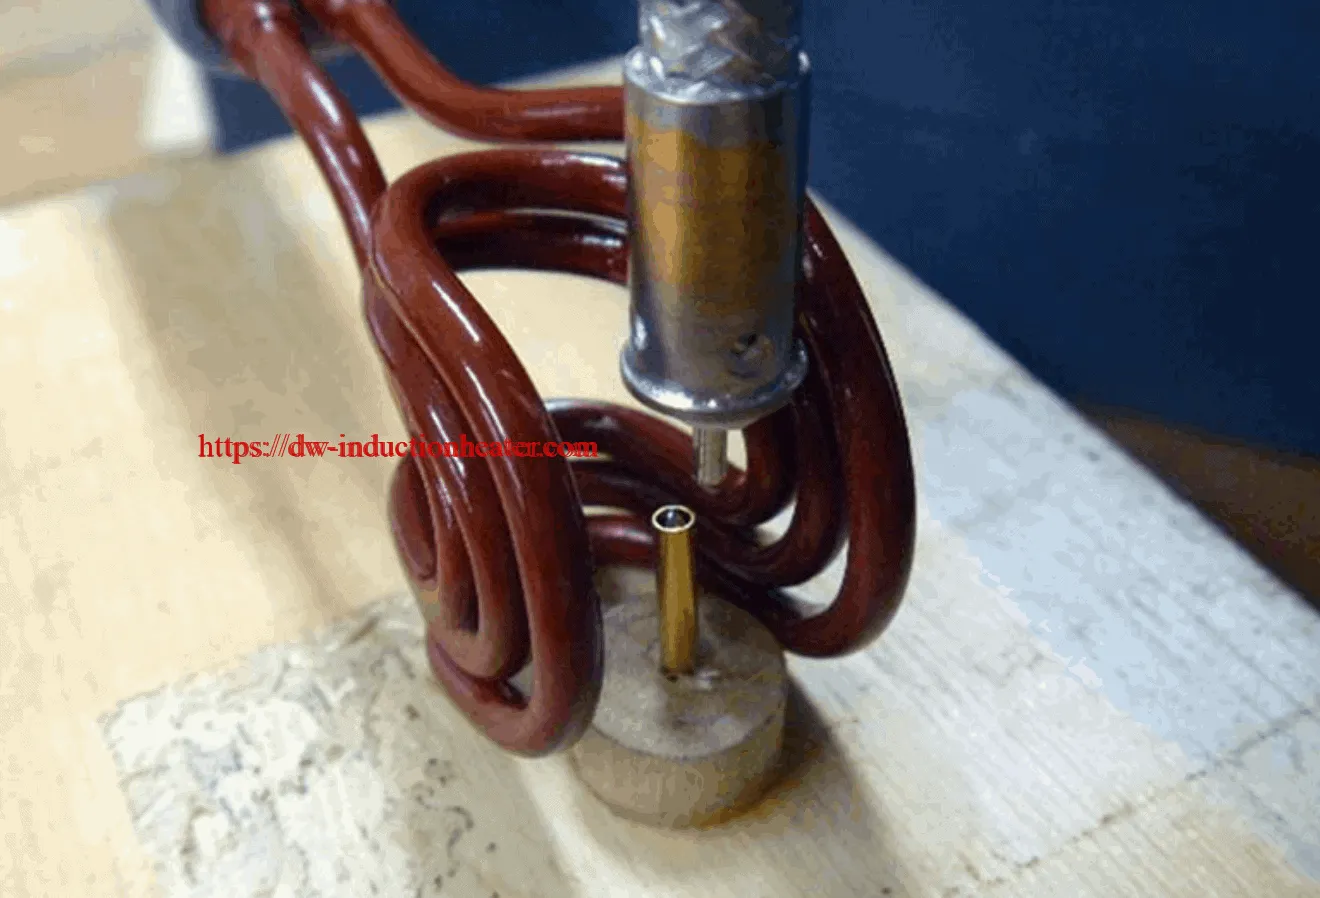
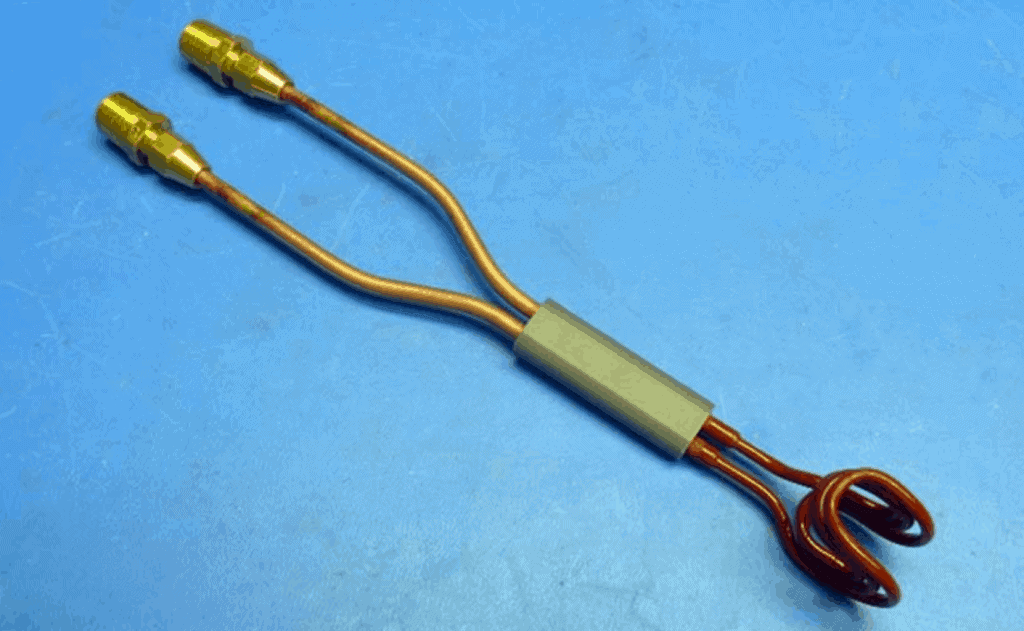
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 
https://dw-inductionheater.com/induction-soldering-coaxial-cable-to-connector-ring.html?feed_id=221986&_unique_id=64cf14d567611

2023年2月24日星期五

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
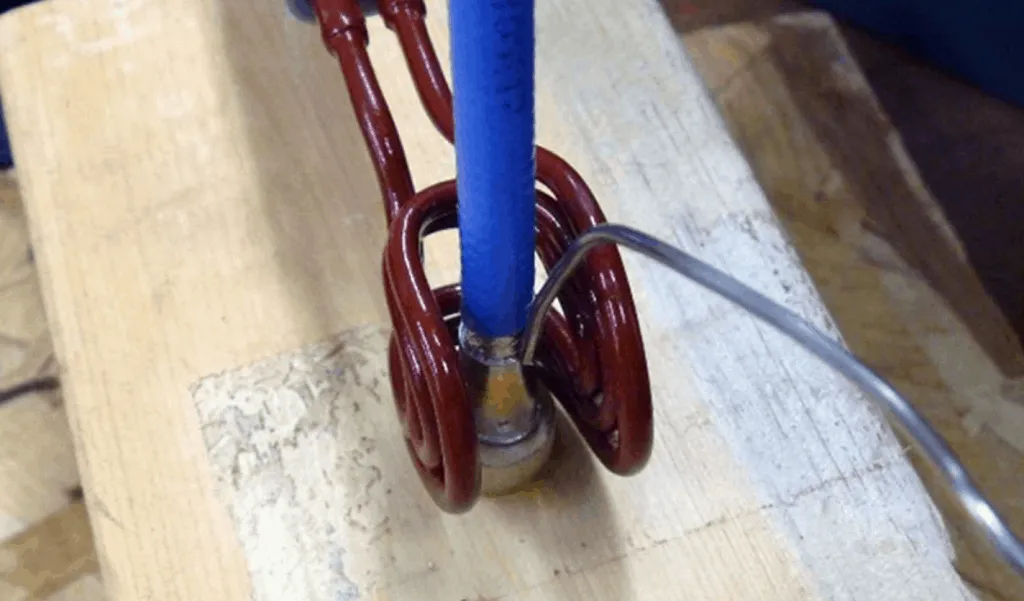
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年12月25日星期日

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年12月24日星期六

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年11月27日星期日

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年9月1日星期四

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年8月5日星期五

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年4月23日星期六

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

2022年3月15日星期二

Induction Soldering Coaxial Cable to Connector Ring

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment  DW-UHF-6KW-I handheld induction Soldering Heater Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 1.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heating was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the induction soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
 

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.