显示标签为“inductionsolderingcopper”的博文。显示所有博文

2024年5月25日星期六

Soldering Steel To Brass With Induction Heater

Soldering Steel To Brass With Induction IGBT Soldering Heater Objective Heat an assembly of small, gold-plated steel connectors to a brass block. Material Approx. 1/8” (3.2mm) diameter gold-plated steel connectors, 1”(25.4mm) square x 1/4” thick brass block Temperature 600°F(315.6ºC) Frequency 240 kHz Equipment • DW-UHF-6kW induction heating system equipped with a remote workhead. • An induction heating coil designed and developed specifically for this application. Process A two-turn helical coil is used to provide uniform heat to parts assembly. Solder paste and flux are applied to the joint area and power is applied for 20 seconds to solder the parts. Proper fixturing is needed to hold the parts in position. Results/Benefits Induction heating provides: • Rapid, localized heating to specific regions of part • Neat and clean joints • Flameless processing induction soldering steel to brass https://dw-inductionheater.com/soldering-steel-to-brass-with-induction-heater.html?feed_id=247175&_unique_id=665229b5a33ef

2024年5月21日星期二

Induction Soldering Copper Tube

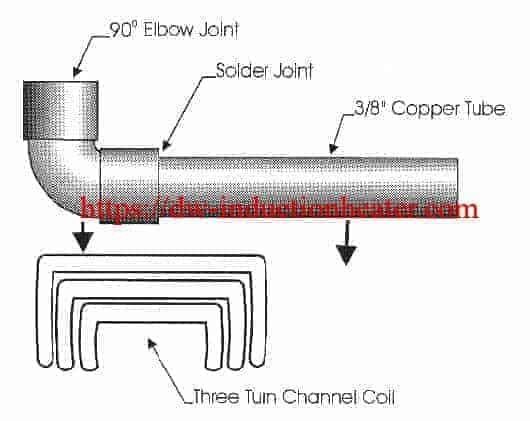
Induction Soldering Copper Tube With High Frequency Heating Units Objective: To heat a section of 3/8" copper tubing along with a 900 elbow for soldering. The copper tubing is to be used in Ice Machine Evaporator Assemblies, and soldering takes place after the tubes have been placed within the assembly. Heating must take place in a channel type coil to provide easy access, once the tubing has been installed. Solder can be manually fed after temperature has been reached. Material: 3/8" Thin Walled Copper Tubing and 900 Elbow Temperature: 6000F Application: Through the use of the DW-UHF-20kW output solid state induction power supply and a unique three (3) turn channel coil, the following results were achieved: 6000F was reached in 10 seconds. A quality solder joint was observed with adequate flow and surface texture. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn channel coil. Frequency: 200 kHz induction soldering copper tube https://dw-inductionheater.com/induction-soldering-copper-tube-pipe.html?feed_id=246441&_unique_id=664c73520bf27

2024年5月18日星期六

Induction Soldering Copper Tap

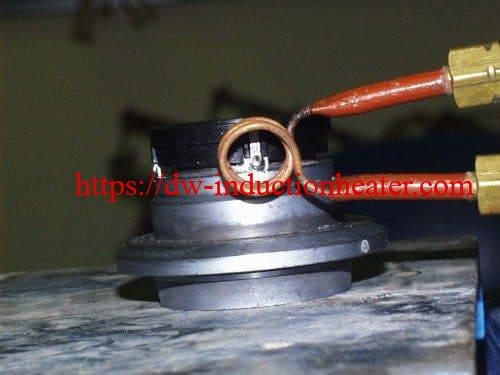
Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper https://dw-inductionheater.com/induction-soldering-copper-tap.html?feed_id=246140&_unique_id=664997f496486

2024年5月14日星期二

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires https://dw-inductionheater.com/induction-soldering-copper-wires.html?feed_id=245596&_unique_id=6643e16e48745

2024年4月2日星期二

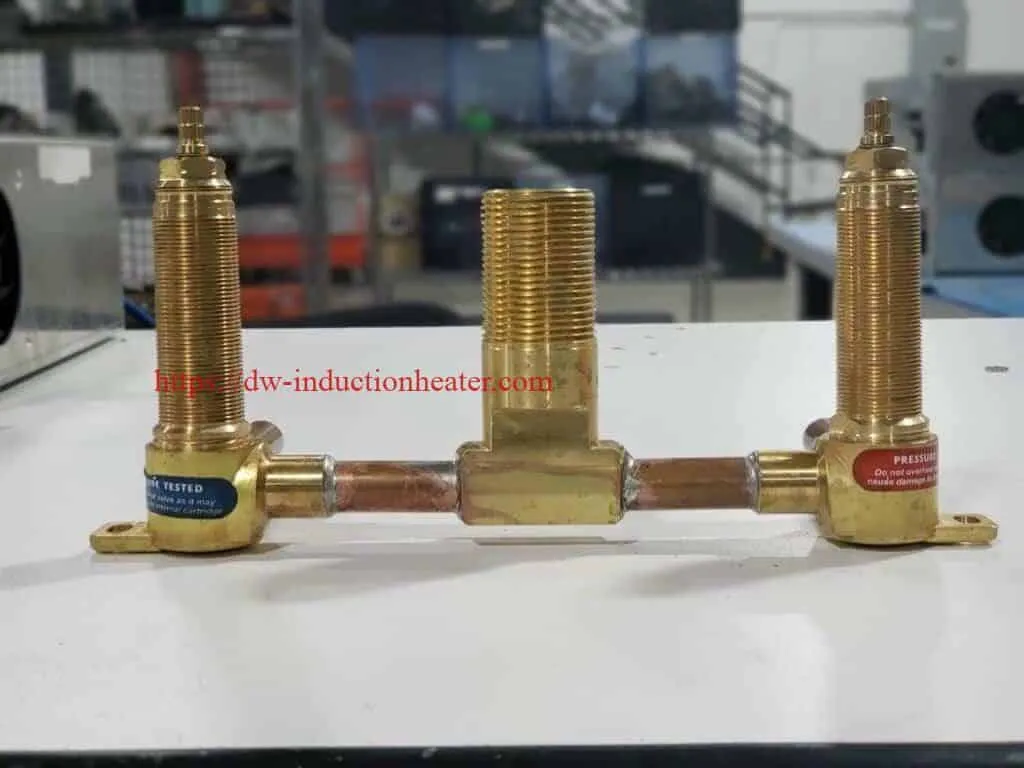
induction soldering copper tubing to brass valves

High frequency induction soldering copper tubing to brass valves

Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine Power: 16 kW Temperature: 932oF (500oC) Time: 20 seconds Coil: Coated custom-made coil.
The Process:
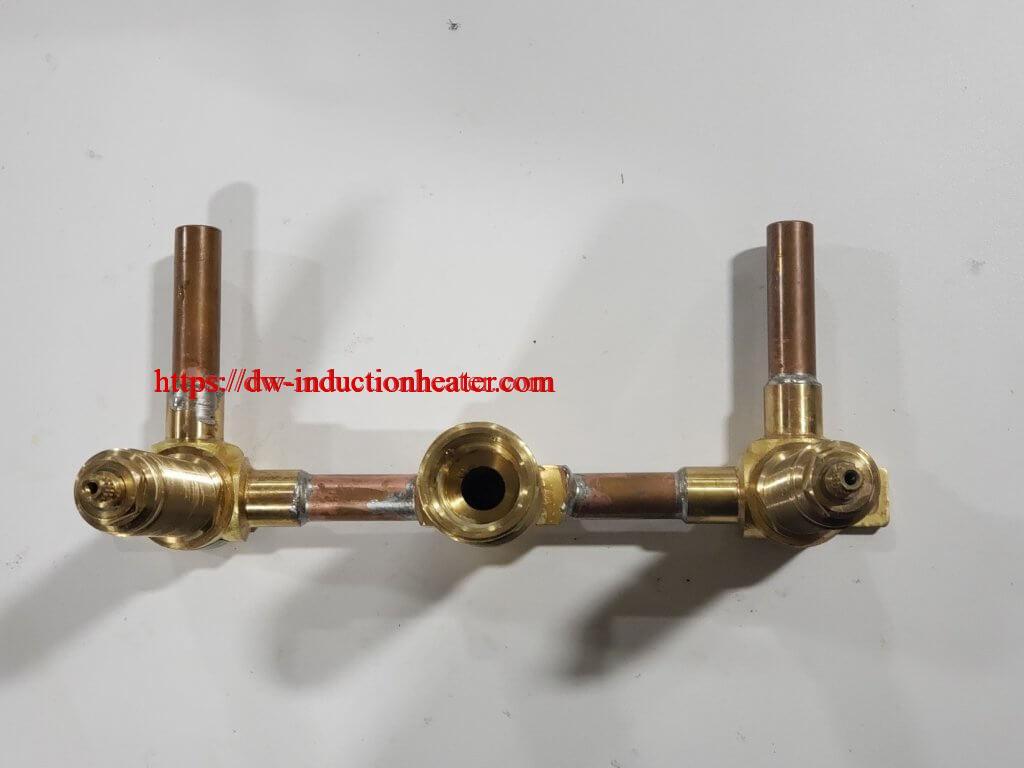
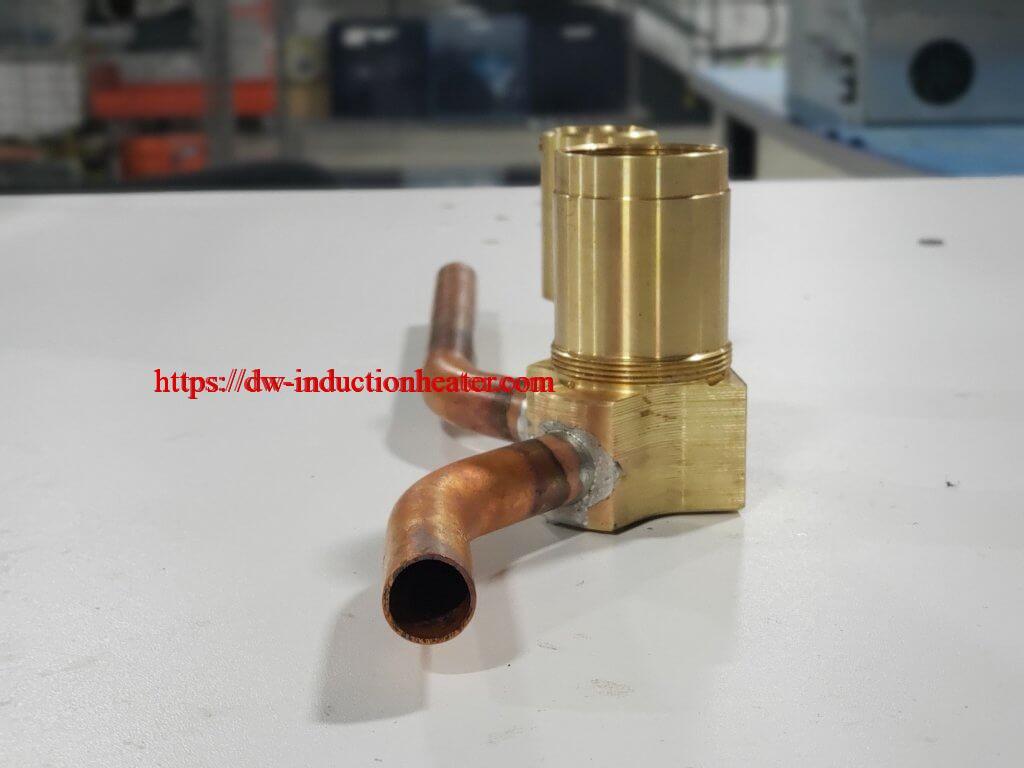
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints.  The use of induction heating was successful in this HVAC application.
https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=239798&_unique_id=660ce5349a514

2024年2月28日星期三

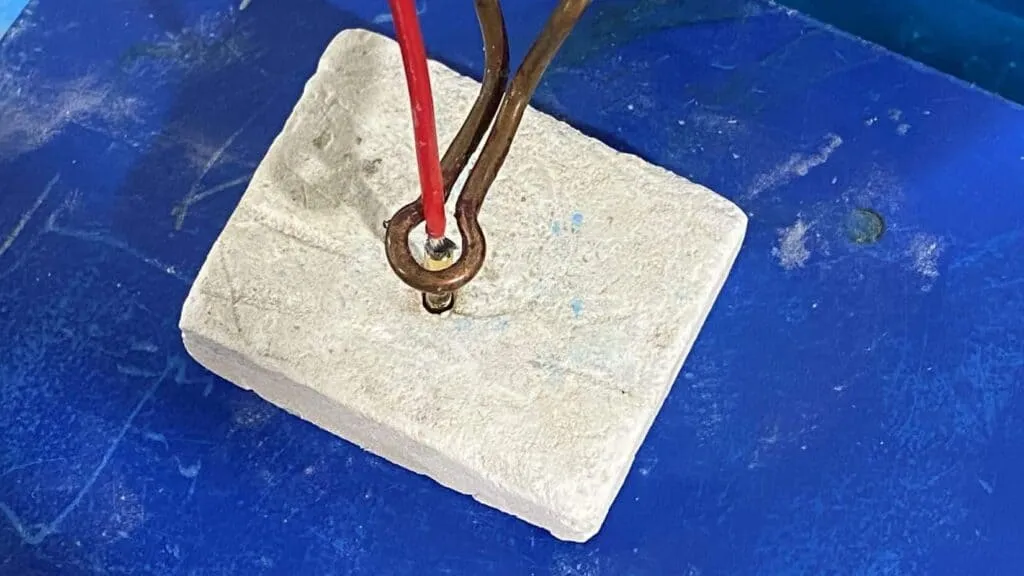
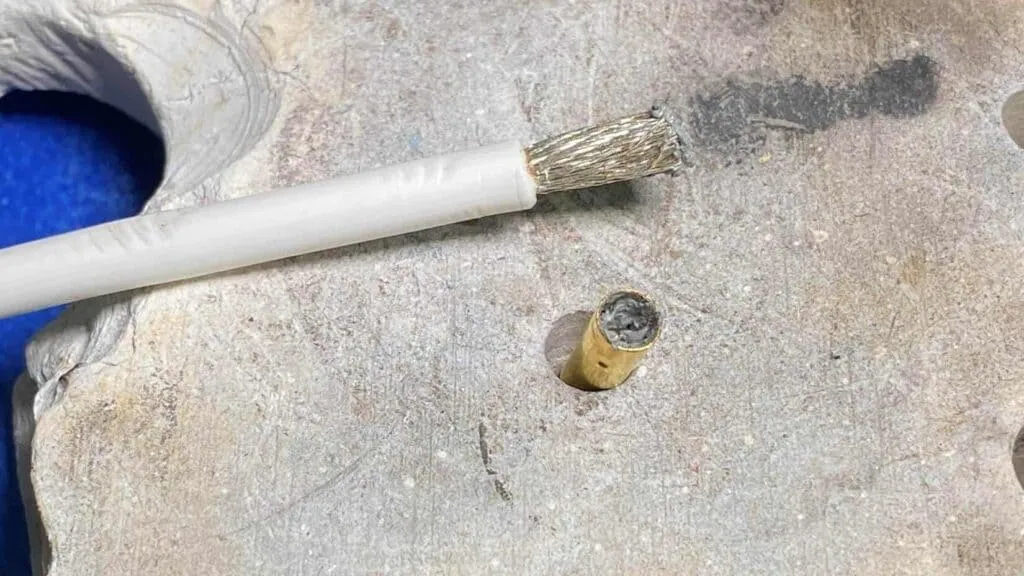
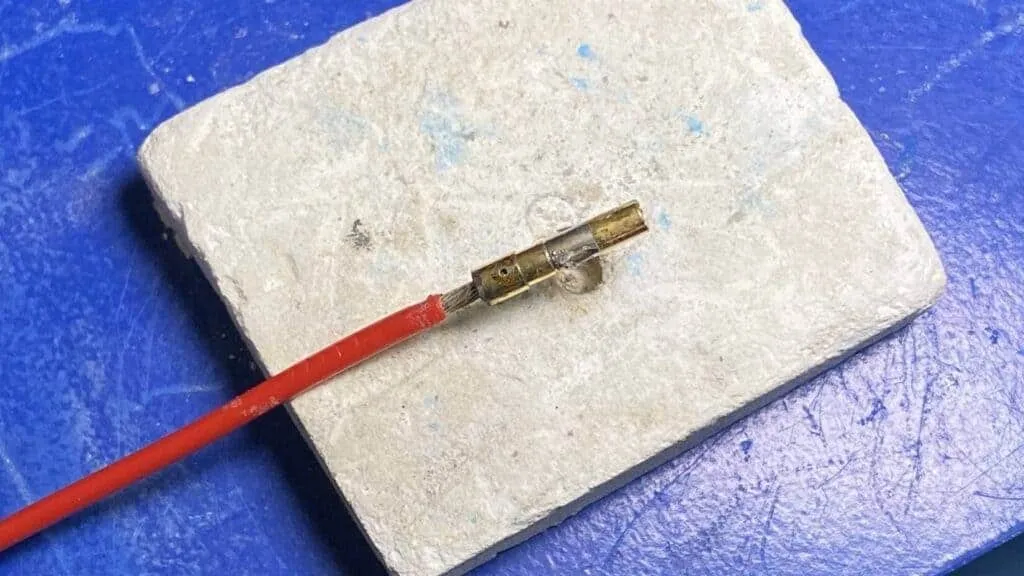
Induction Soldering Copper Cables to Copper Pins

Induction Soldering Copper Cables to Copper Pins

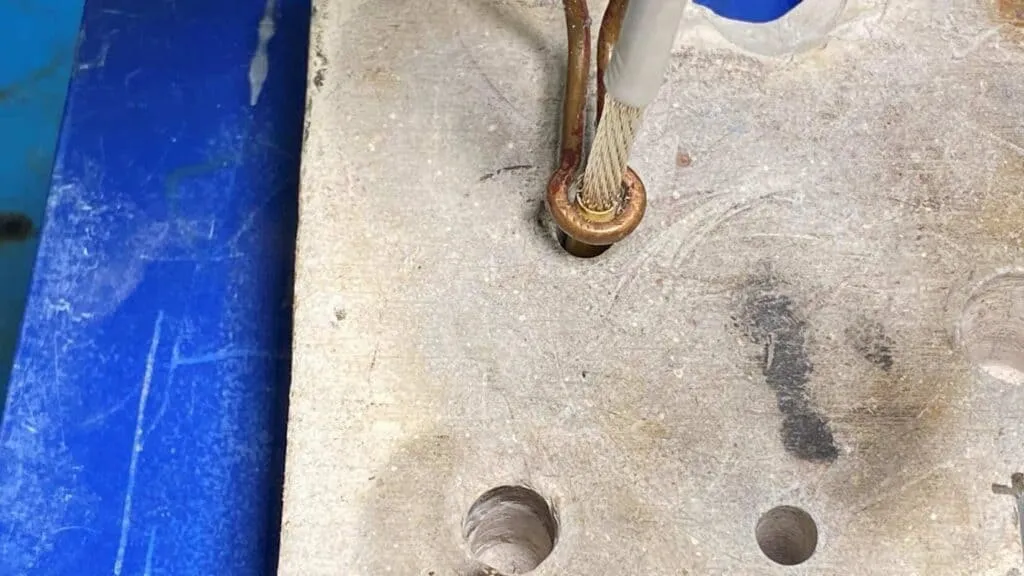
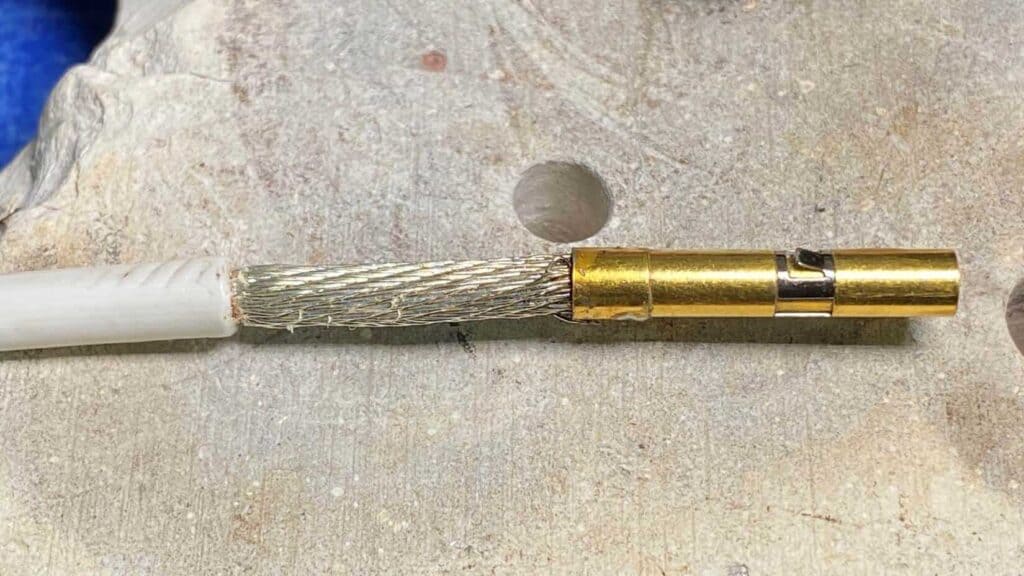
  Objective: The objective of this induction heating application is to solder cables to copper pins for harness manufacturing. The customer is a manufacturer of mission-critical test systems for the Aerospace Industry. The goal is to reduce soldering time from 10 minutes by hand to less than 1 minute with the help of an induction heating system and increase solder quality and repeatability. Equipment: HLQ has a line of induction soldering equipment, typically used in a similar application – DW-UHF series, high frequency induction heating systems for induction soldering and brazing of small components and parts. Process: The customer provided a large cable with 0.2”(5.08 cm) OD and a pin 1”(2.5 cm) long, 0.178” (0.44 cm) OD, a cable receiver 0.2” (5.08 cm) long, 0.169” (0.42 cm) ID, 0.19” OD and a small cable with 0.09” (0.22 cm) OD, as well as, a small pin 0.114”( 0.28 cm) OD and a cable receiver 0.16”( 0.40 cm) long, 0.07”( 0.17 cm) ID. 0.129” (0.32 cm) OD. Induction Soldering paste was applied inside the cable receiver on the pin and to the stripped end of the cable. The pin was then placed in its holder. The induction heating coil entirely covered the cable receiver. Induction soldering with the DW-UHF-6KW-I handheld induction brazing system was completed in 2 seconds at 60% power to a temperature of ~600°F (315°C). Industry: Aerospace & Defense https://dw-inductionheater.com/induction-soldering-copper-cables-to-copper-pins.html?feed_id=235292&_unique_id=65dfe818e45f5
2023年9月28日星期四

Induction Soldering Copper Tube

Induction Soldering Copper Tube With High Frequency Heating Units Objective: To heat a section of 3/8" copper tubing along with a 900 elbow for soldering. The copper tubing is to be used in Ice Machine Evaporator Assemblies, and soldering takes place after the tubes have been placed within the assembly. Heating must take place in a channel type coil to provide easy access, once the tubing has been installed. Solder can be manually fed after temperature has been reached. Material: 3/8" Thin Walled Copper Tubing and 900 Elbow Temperature: 6000F Application: Through the use of the DW-UHF-20kW output solid state induction power supply and a unique three (3) turn channel coil, the following results were achieved: 6000F was reached in 10 seconds. A quality solder joint was observed with adequate flow and surface texture. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn channel coil. Frequency: 200 kHz induction soldering copper tube https://dw-inductionheater.com/induction-soldering-copper-tube-pipe.html?feed_id=228071&_unique_id=6515cfb975c26

2023年9月26日星期二

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper https://dw-inductionheater.com/induction-soldering-copper-tap.html?feed_id=227951&_unique_id=6512f46d8ad53

2023年9月25日星期一

induction soldering copper tubing to brass valves

High frequency induction soldering copper tubing to brass valves

Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine Power: 16 kW Temperature: 932oF (500oC) Time: 20 seconds Coil: Coated custom-made coil.
The Process:
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints.  The use of induction heating was successful in this HVAC application.

2023年9月22日星期五

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires https://dw-inductionheater.com/induction-soldering-copper-wires.html?feed_id=227711&_unique_id=650d3e0d9fa4b

2023年9月1日星期五

Induction Soldering Copper Tube

Induction Soldering Copper Tube With High Frequency Heating Units Objective: To heat a section of 3/8" copper tubing along with a 900 elbow for soldering. The copper tubing is to be used in Ice Machine Evaporator Assemblies, and soldering takes place after the tubes have been placed within the assembly. Heating must take place in a channel type coil to provide easy access, once the tubing has been installed. Solder can be manually fed after temperature has been reached. Material: 3/8" Thin Walled Copper Tubing and 900 Elbow Temperature: 6000F Application: Through the use of the DW-UHF-20kW output solid state induction power supply and a unique three (3) turn channel coil, the following results were achieved: 6000F was reached in 10 seconds. A quality solder joint was observed with adequate flow and surface texture. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn channel coil. Frequency: 200 kHz induction soldering copper tube

2023年8月22日星期二

Soldering Steel To Brass With Induction Heater

Soldering Steel To Brass With Induction IGBT Soldering Heater Objective Heat an assembly of small, gold-plated steel connectors to a brass block. Material Approx. 1/8” (3.2mm) diameter gold-plated steel connectors, 1”(25.4mm) square x 1/4” thick brass block Temperature 600°F(315.6ºC) Frequency 240 kHz Equipment • DW-UHF-6kW induction heating system equipped with a remote workhead. • An induction heating coil designed and developed specifically for this application. Process A two-turn helical coil is used to provide uniform heat to parts assembly. Solder paste and flux are applied to the joint area and power is applied for 20 seconds to solder the parts. Proper fixturing is needed to hold the parts in position. Results/Benefits Induction heating provides: • Rapid, localized heating to specific regions of part • Neat and clean joints • Flameless processing induction soldering steel to brass

2023年8月11日星期五

induction soldering copper tubing to brass valves

High frequency induction soldering copper tubing to brass valves

Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine Power: 16 kW Temperature: 932oF (500oC) Time: 20 seconds Coil: Coated custom-made coil.
The Process:
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints.  The use of induction heating was successful in this HVAC application.
https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=222736&_unique_id=64d639de7c3cb

2023年7月11日星期二

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2023年7月7日星期五

Induction Soldering Copper Cables to Copper Pins

Induction Soldering Copper Cables to Copper Pins

  Objective: The objective of this induction heating application is to solder cables to copper pins for harness manufacturing. The customer is a manufacturer of mission-critical test systems for the Aerospace Industry. The goal is to reduce soldering time from 10 minutes by hand to less than 1 minute with the help of an induction heating system and increase solder quality and repeatability. Equipment: HLQ has a line of induction soldering equipment, typically used in a similar application – DW-UHF series, high frequency induction heating systems for induction soldering and brazing of small components and parts. Process: The customer provided a large cable with 0.2”(5.08 cm) OD and a pin 1”(2.5 cm) long, 0.178” (0.44 cm) OD, a cable receiver 0.2” (5.08 cm) long, 0.169” (0.42 cm) ID, 0.19” OD and a small cable with 0.09” (0.22 cm) OD, as well as, a small pin 0.114”( 0.28 cm) OD and a cable receiver 0.16”( 0.40 cm) long, 0.07”( 0.17 cm) ID. 0.129” (0.32 cm) OD. Induction Soldering paste was applied inside the cable receiver on the pin and to the stripped end of the cable. The pin was then placed in its holder. The induction heating coil entirely covered the cable receiver. Induction soldering with the DW-UHF-6KW-I handheld induction brazing system was completed in 2 seconds at 60% power to a temperature of ~600°F (315°C). Industry: Aerospace & Defense https://dw-inductionheater.com/induction-soldering-copper-cables-to-copper-pins.html?feed_id=217936&_unique_id=64a8716c2d69b
2023年7月2日星期日

Induction Soldering Copper Wires

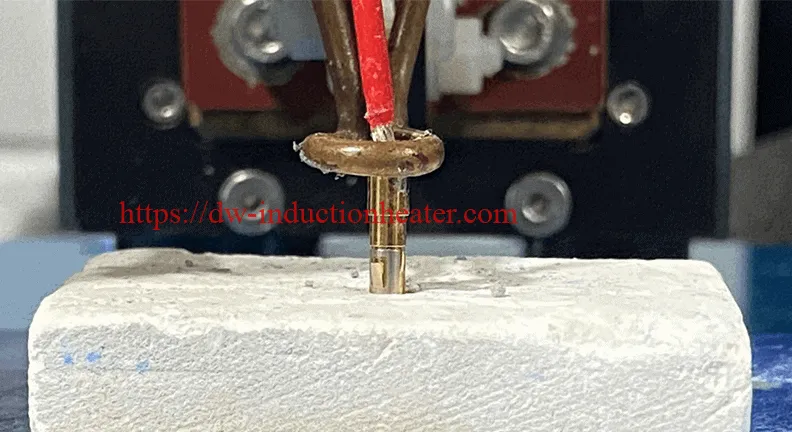
Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2023年6月18日星期日

Induction Soldering Copper Cables to Copper Pins

Induction Soldering Copper Cables to Copper Pins

  Objective: The objective of this induction heating application is to solder cables to copper pins for harness manufacturing. The customer is a manufacturer of mission-critical test systems for the Aerospace Industry. The goal is to reduce soldering time from 10 minutes by hand to less than 1 minute with the help of an induction heating system and increase solder quality and repeatability. Equipment: HLQ has a line of induction soldering equipment, typically used in a similar application – DW-UHF series, high frequency induction heating systems for induction soldering and brazing of small components and parts. Process: The customer provided a large cable with 0.2”(5.08 cm) OD and a pin 1”(2.5 cm) long, 0.178” (0.44 cm) OD, a cable receiver 0.2” (5.08 cm) long, 0.169” (0.42 cm) ID, 0.19” OD and a small cable with 0.09” (0.22 cm) OD, as well as, a small pin 0.114”( 0.28 cm) OD and a cable receiver 0.16”( 0.40 cm) long, 0.07”( 0.17 cm) ID. 0.129” (0.32 cm) OD. Induction Soldering paste was applied inside the cable receiver on the pin and to the stripped end of the cable. The pin was then placed in its holder. The induction heating coil entirely covered the cable receiver. Induction soldering with the DW-UHF-6KW-I handheld induction brazing system was completed in 2 seconds at 60% power to a temperature of ~600°F (315°C). Industry: Aerospace & Defense

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.