显示标签为“highfrequencysolderingcopper”的博文。显示所有博文

2024年5月18日星期六

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper https://dw-inductionheater.com/induction-soldering-copper-tap.html?feed_id=246140&_unique_id=664997f496486

2024年5月14日星期二

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires https://dw-inductionheater.com/induction-soldering-copper-wires.html?feed_id=245596&_unique_id=6643e16e48745

2023年9月26日星期二

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper https://dw-inductionheater.com/induction-soldering-copper-tap.html?feed_id=227951&_unique_id=6512f46d8ad53

2023年9月22日星期五

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires https://dw-inductionheater.com/induction-soldering-copper-wires.html?feed_id=227711&_unique_id=650d3e0d9fa4b

2023年7月11日星期二

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2023年7月2日星期日

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2023年5月29日星期一

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2023年4月21日星期五

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2023年3月8日星期三

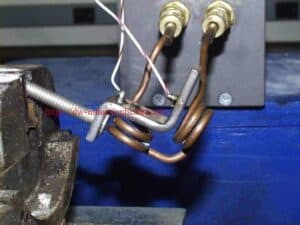
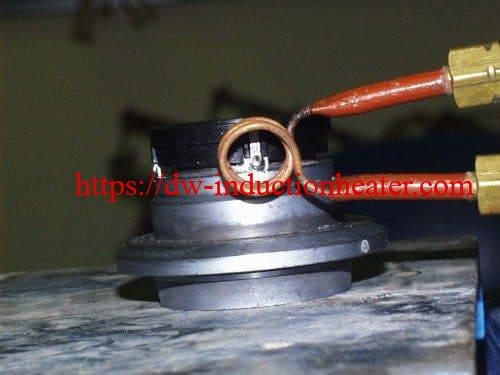
Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units

Objective Soldering two copper wires to pre-installed turrets on a copper buss bar
Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick
Temperature 446 ºF (230 ºC)
Frequency 230 kHz
Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor.
• An induction heating coil designed and developed specifically for this application.
Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint.
Results/Benefits Induction heating provides:
• Reduced solder time
• Even distribution of heating
• Joint to joint consistency
 

induction soldering copper wires

2022年12月26日星期一

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年11月18日星期五

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年10月7日星期五

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2022年9月13日星期二

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2022年9月6日星期二

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年8月6日星期六

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年5月29日星期日

Induction Soldering Copper Wires

Induction Soldering Copper Wires With IGBT High Frequency Heating Units Objective Soldering two copper wires to pre-installed turrets on a copper buss bar Material Solder dipped copper/nickel buss bar, 2 tinned stranded copper wires, brazing stick Temperature 446 ºF (230 ºC) Frequency 230 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1.2μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A four turn split helical coil is used to solder the buss bar assembly. The 2 copper wires are applied to the turrets and power is applied for 30 seconds. The brazing stick is fed by hand to the heated parts and the braze flows evenly, creating the joint. Results/Benefits Induction heating provides: • Reduced solder time • Even distribution of heating • Joint to joint consistency   induction soldering copper wires

2022年4月27日星期三

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年4月17日星期日

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2022年1月23日星期日

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

2021年12月22日星期三

Induction Soldering Copper Tap

Induction Soldering Copper Tap on a Speaker Ring with IGBT Induction Heater Objective Heat copper tab until the solder reflows. Material Copper tab 0.25 X 0.25 inch square about 0.05 inches thick. Lead free solder material (higher melting temperature than regular solder.) Temperature 500 ºF for 1.25 seconds Frequency 286 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz solid state induction heating system equipped with a remote heat station containing one 1.2 μF capacitor and a specially-designed work coil.. A multi-turn helical coil about 3/16 inch internal diameter made out of 1/16 inch diameter tubing. Process Solder wire is fed onto speaker tab area using an automatic wire feeder. It is then heated to re-flow the solder. Results/Benefits With an efficient coil design induction heating easily reaches the desired reflow temperature in a very short amount of time. induction soldering copper

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.