 https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=269343&_unique_id=67ab5f763d81a
2025年2月11日星期二
induction soldering copper tubing to brass valves
induction soldering copper tubing to brass valves
https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=269343&_unique_id=67ab5f763d81a
https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=269343&_unique_id=67ab5f763d81a

2025年2月10日星期一
Induction Soldering Brass Corner Joint
Induction Soldering Brass Corner Joint
 https://dw-inductionheater.com/induction-soldering-brass-corner-joint.html?feed_id=269256&_unique_id=67aa6242be3fe
2025年2月9日星期日
Induction Soldering Copper Pipes to PCB Board
Induction Soldering Copper Pipes to PCB Board
 https://dw-inductionheater.com/induction-soldering-copper-pipes-to-pcb-board.html?feed_id=269111&_unique_id=67a8680b23850
2025年1月26日星期日
induction soldering steel and brass parts process
induction soldering steel and brass parts process
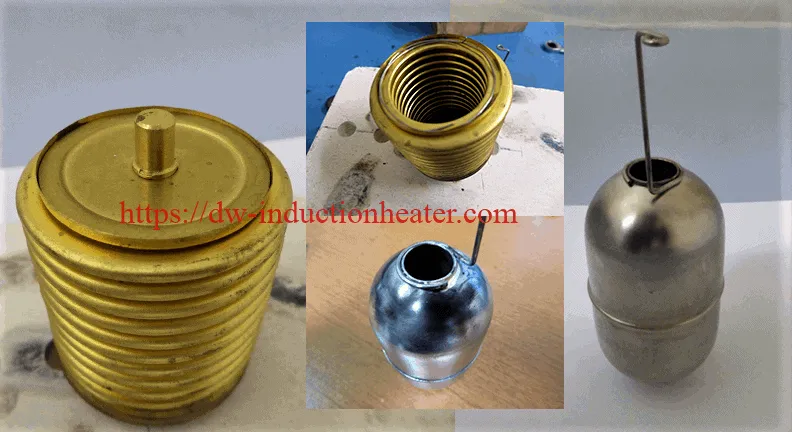 https://dw-inductionheater.com/product/induction-soldering-steel-and-brass-parts-process?feed_id=267835&_unique_id=6796a2a04b23c
2024年12月26日星期四
Induction Soldering Copper Cables to Copper Pins
Induction Soldering Copper Cables to Copper Pins
 https://dw-inductionheater.com/induction-soldering-copper-cables-to-copper-pins.html?feed_id=264645&_unique_id=676d149bb996c
2024年10月1日星期二
High frequency induction soldering machine
High frequency induction soldering machine
 https://dw-inductionheater.com/product/high-frequency-induction-soldering-machine?feed_id=256496&_unique_id=66fc63896fc00
2024年4月2日星期二
induction soldering copper tubing to brass valves
High frequency induction soldering copper tubing to brass valves
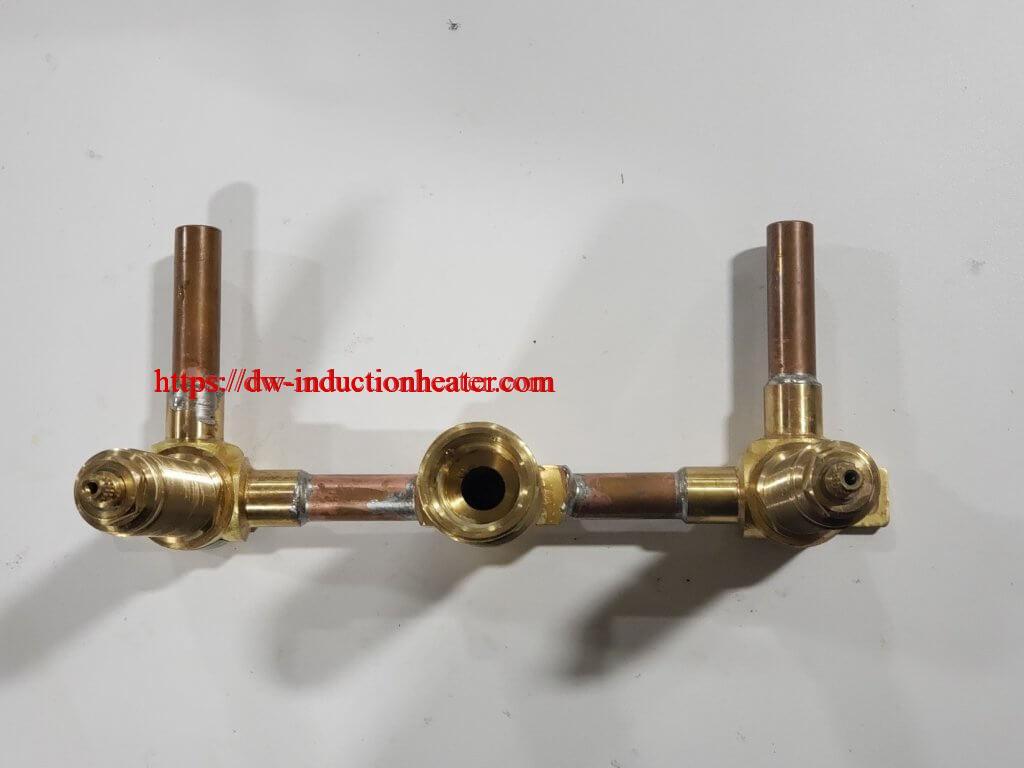
Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine
Power: 16 kW
Temperature: 932oF (500oC)
Time: 20 seconds
Coil: Coated custom-made coil.
The Process:
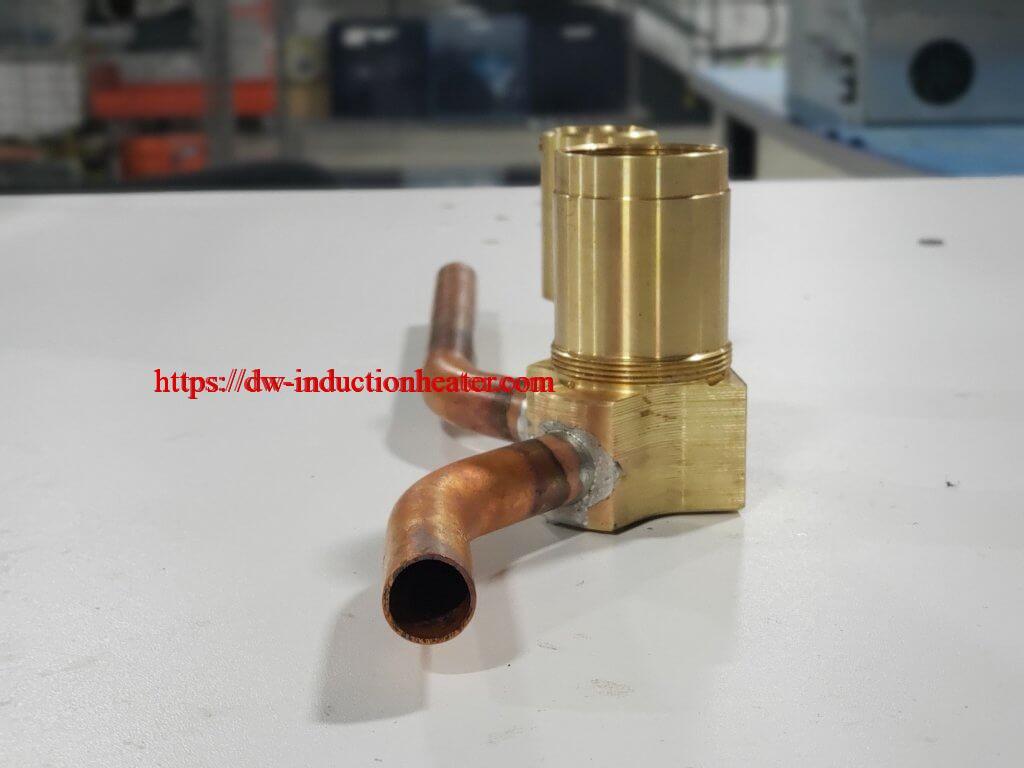
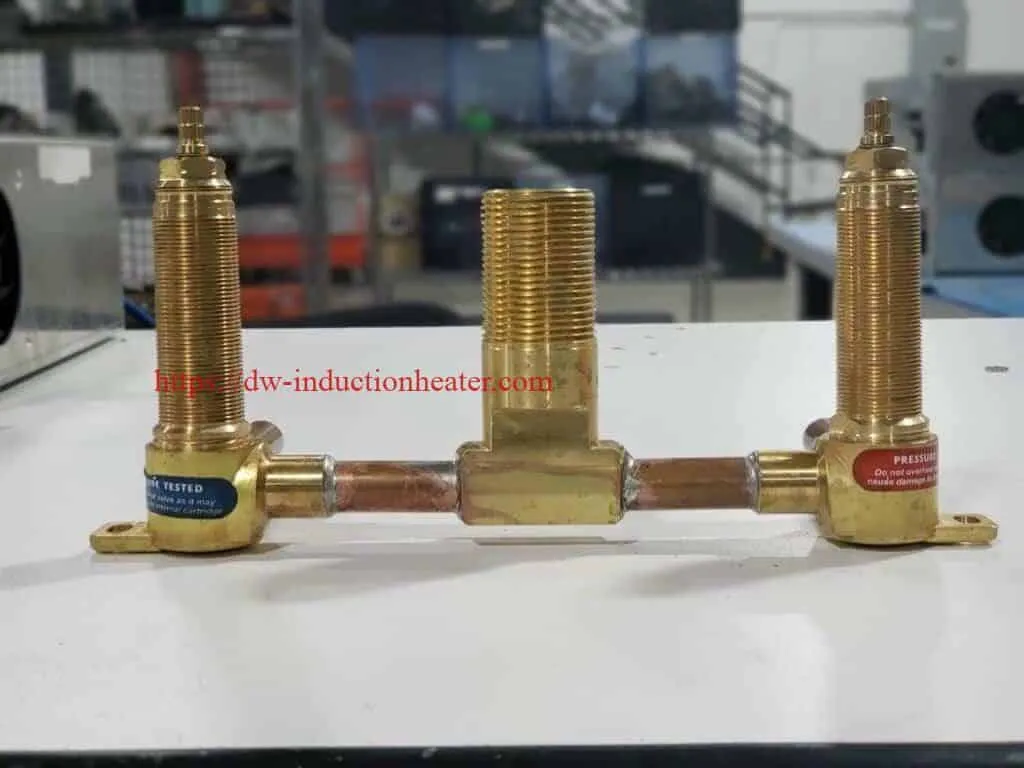
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints. The use of induction heating was successful in this HVAC application.

https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=239798&_unique_id=660ce5349a514

Induction Soldering Brass Corner Joint
Hig Frequency Induction Soldering Brass Corner Joint
Objective
Successfully solder two 45° brass corner joints.
Equipment:
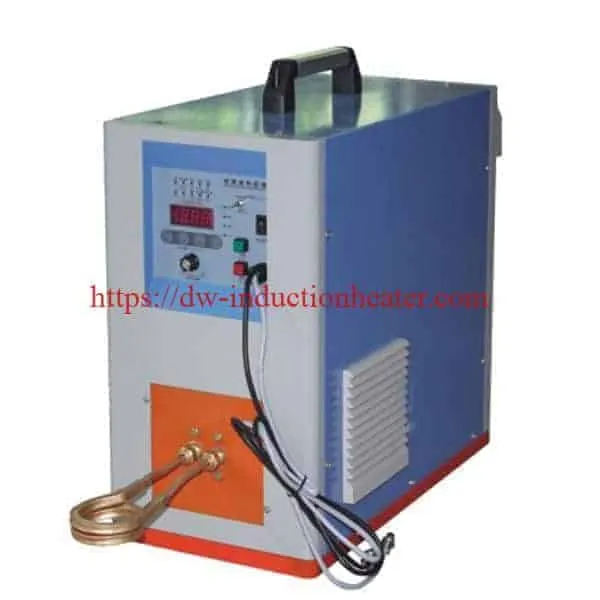
DW-UHF-10kw induction soldering heater
 Materials
StayBrite #8 silver solder supplied by customer
Bridgit solder flux supplied by customer
Brass corner joint
Pancake coil
Key Parameters
Power: 5.5 kW
Temperature: Approximately 550° F (288° C)
Time: 20 sec
Materials
StayBrite #8 silver solder supplied by customer
Bridgit solder flux supplied by customer
Brass corner joint
Pancake coil
Key Parameters
Power: 5.5 kW
Temperature: Approximately 550° F (288° C)
Time: 20 sec
Process:
 Results/Benefits:
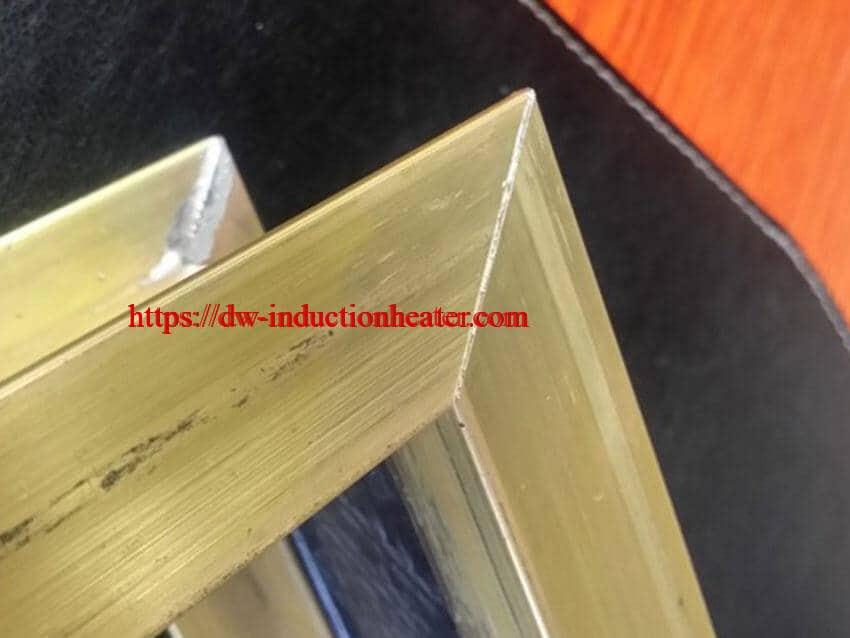
- Flux is applied at all joints.
- The assembly is positioned into for heating
- Induction heating is applied for 15 sec
- The brazing rod is applied to the joint
Results/Benefits:
- Since the brazing alloy is manually fed, the coil is placed under the joint, facing the visible side of the frame. The visible side of the joint is laying on a flat wooden surface, which does not allow the brazing alloy to leak and spill. This keeps the visible surface nice and clean, while the seam is internally brazed.
- If solder paste is used, then the coil can be placed on top of the joint. If special dual coil is used, then both joints (top and bottom) can be done with one shot.
- No frame flipping is needed in this case. See the video and zoom the pictures attached for more details.
- No special cleaning is needed on either side of the joint. The samples on the pictures have been paper towel wiped only.
2024年4月1日星期一
Induction Soldering Copper Pipes to PCB Board
Objective:
Test –Induction Soldering Copper Pipes to PCB Board
Industry: Medical & Dental
Materials: Flat copper pipes, PCB board
Alloy: Low-temperature solder paste
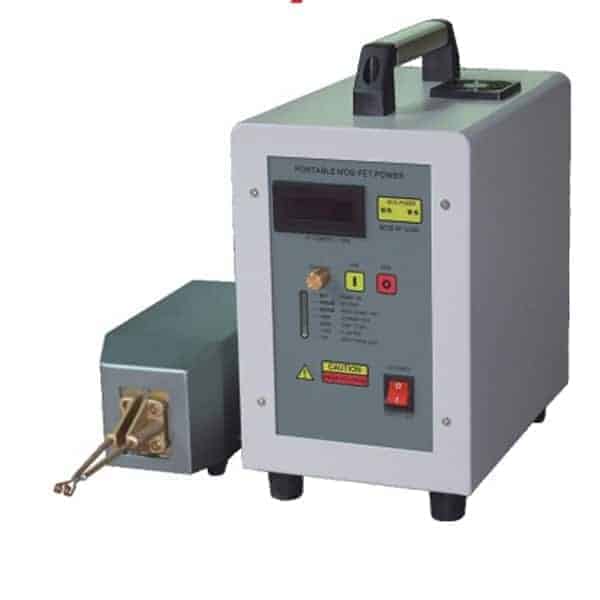
Equipment: DW-UHF-6KW-I Handheld Induction Heater
 Power: 1.88 kW
Time: 15 secs.
Coil: Coated custom-made coil.
The Process:
HLQ was contacted by a leading manufacturer of clinical diagnostic equipment who is striving to drive innovation in the Magnetic Resonance Imaging (MRI) technology.
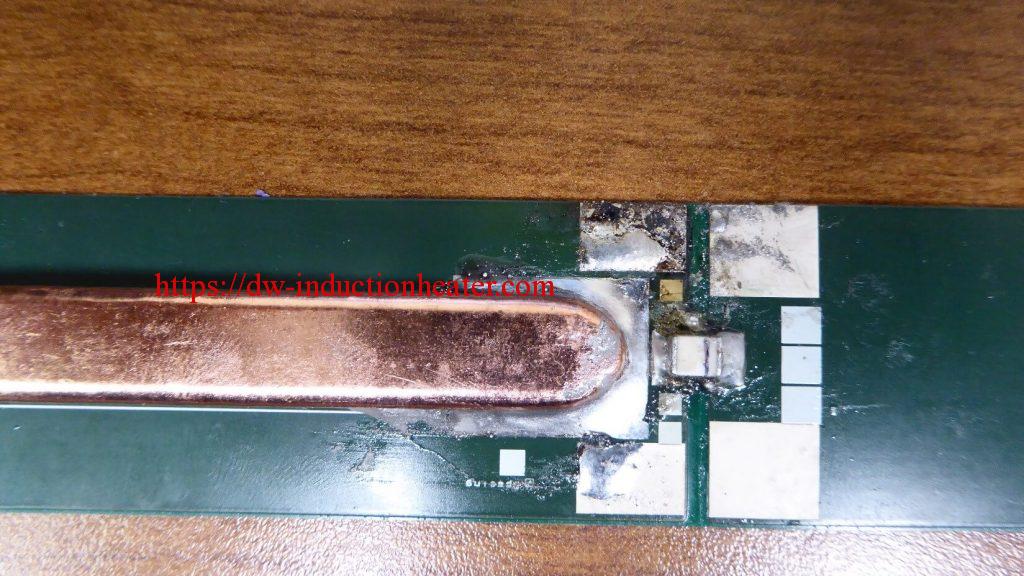
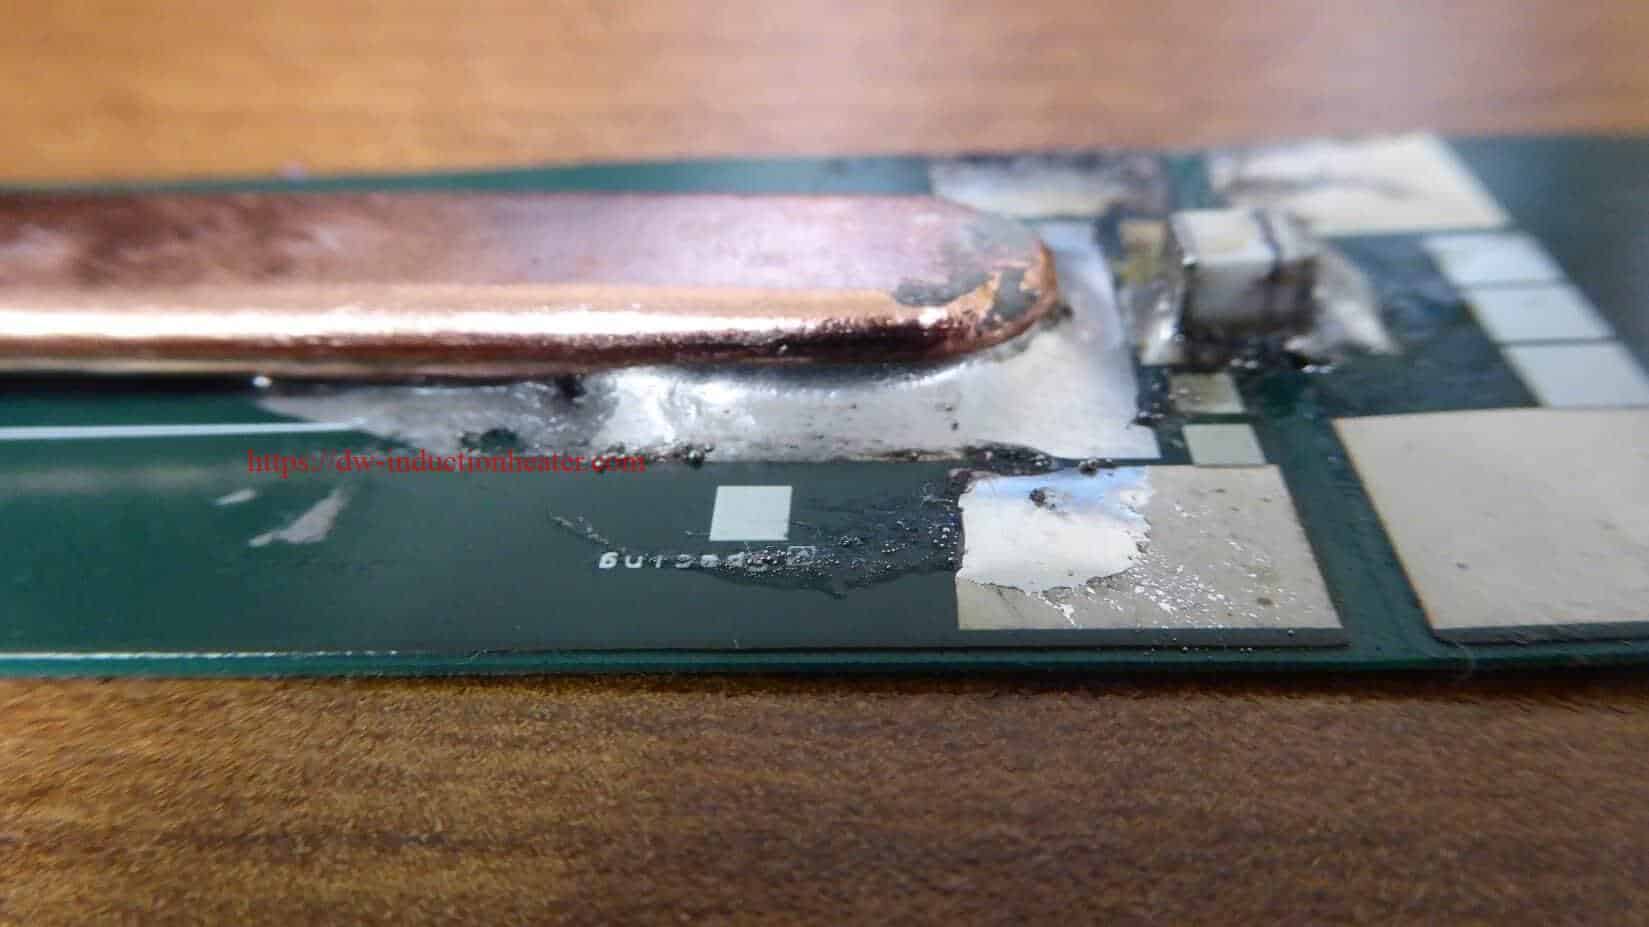
The flat pipes, featured in this heating application, are used to transfer heat with minimal temperature difference or spread the heat across a surface.
Our induction heating solution helped the client to cut manufacturing time which previously took 1 hour to produce 16 soldered copper heat pipes.
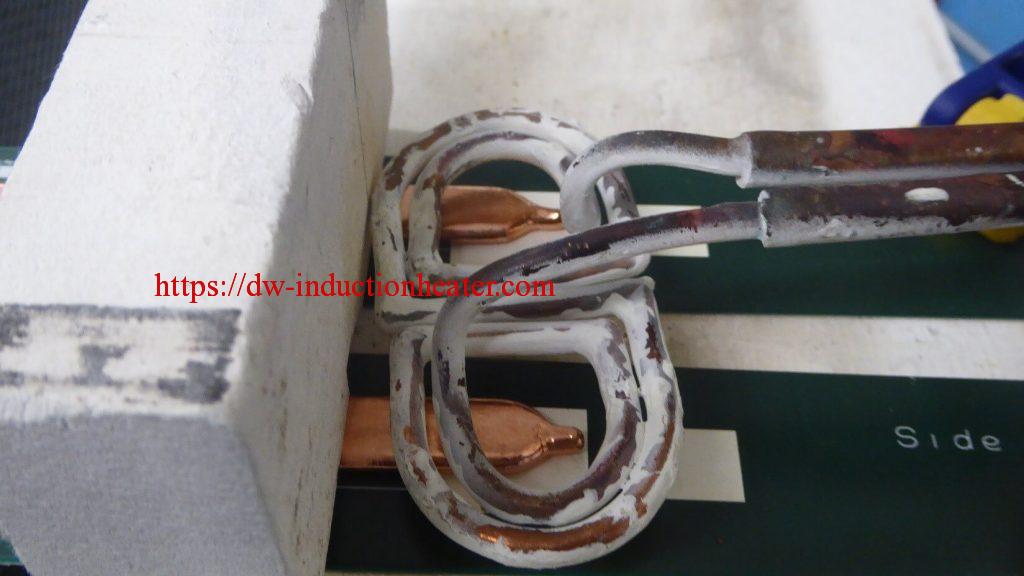
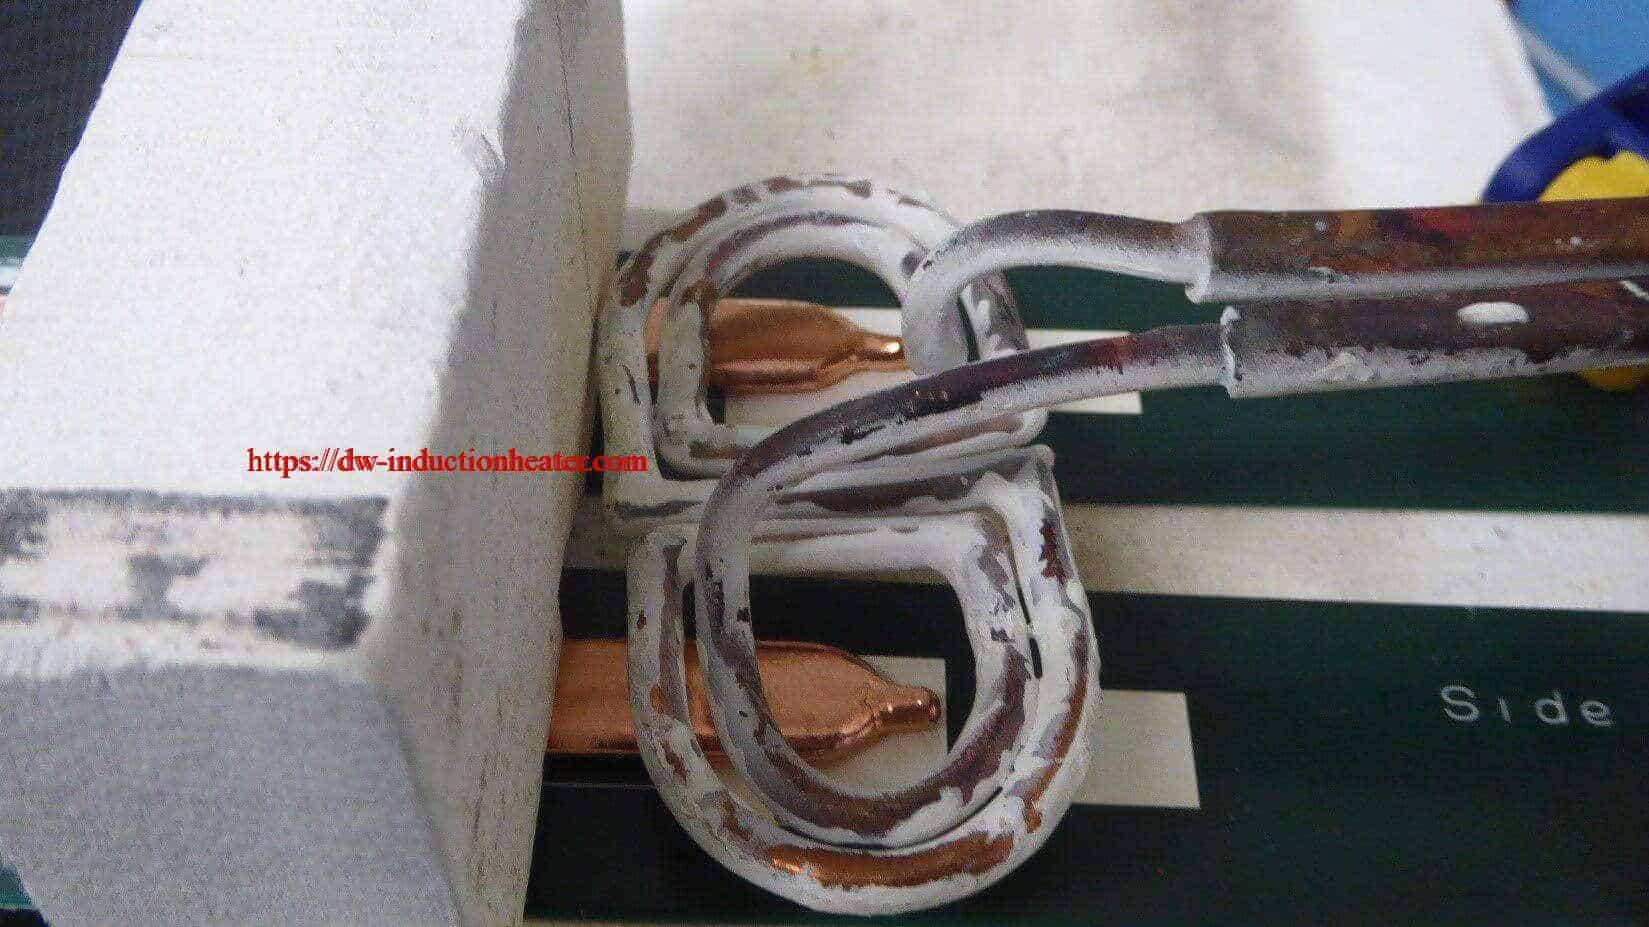
The DW-UHF-6KW-I handheld induction heating power supply along with a heat station successfully performed the soldering process in approximately 15 seconds. We also used one of our custom-made induction coils with cement coasting to ensure that the coil will not suffer mechanical damage.
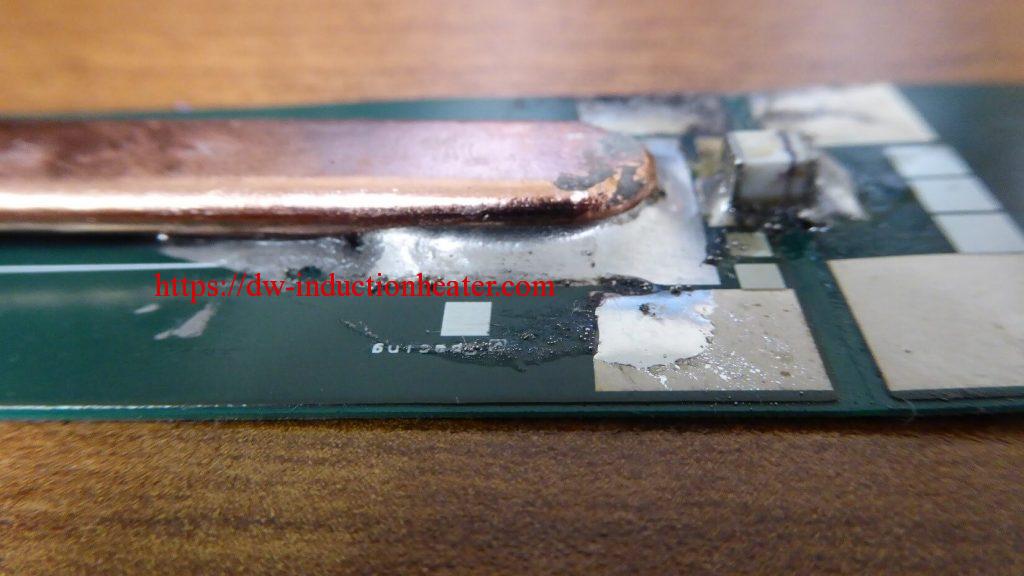
To perform the test, we positioned the induction soldering copper pipes onto two flat pads containing low-temperature solder paste. Induction heating ensures complete repeatability. There is a significant reduction in cycle time and increased efficiency as now multiple parts can be soldered simultaneously.
https://dw-inductionheater.com/induction-soldering-copper-pipes-to-pcb-board.html?feed_id=239594&_unique_id=660ac11a870da
Power: 1.88 kW
Time: 15 secs.
Coil: Coated custom-made coil.
The Process:
HLQ was contacted by a leading manufacturer of clinical diagnostic equipment who is striving to drive innovation in the Magnetic Resonance Imaging (MRI) technology.
The flat pipes, featured in this heating application, are used to transfer heat with minimal temperature difference or spread the heat across a surface.
Our induction heating solution helped the client to cut manufacturing time which previously took 1 hour to produce 16 soldered copper heat pipes.
The DW-UHF-6KW-I handheld induction heating power supply along with a heat station successfully performed the soldering process in approximately 15 seconds. We also used one of our custom-made induction coils with cement coasting to ensure that the coil will not suffer mechanical damage.
To perform the test, we positioned the induction soldering copper pipes onto two flat pads containing low-temperature solder paste. Induction heating ensures complete repeatability. There is a significant reduction in cycle time and increased efficiency as now multiple parts can be soldered simultaneously.

2024年3月9日星期六
High frequency Induction Soldering Brass Tubes

Objective
To simultaneously high frequency Induction Soldering Brass Tubessolder to a brass water jacket assembly with induction heating.
 Equipment
DW-HF-15KW Induction Heating Machine
 Key Parameters
Power: 5 kW
Temperature: 424°F (217°C)
Time: 10 seconds until the alloy flows; 15 seconds to allow alloy to even out around the tube.
Equipment
DW-HF-15KW Induction Heating Machine
Key Parameters
Power: 5 kW
Temperature: 424°F (217°C)
Time: 10 seconds until the alloy flows; 15 seconds to allow alloy to even out around the tube.

TEST 1
Materials
• Brass water jacket assembly
• Lead-free solder alloy
• Utility paste soldering flux

TEST 2
Materials
• Brass water jacket assembly
• Lead-free solder alloy
• Utility paste soldering flux
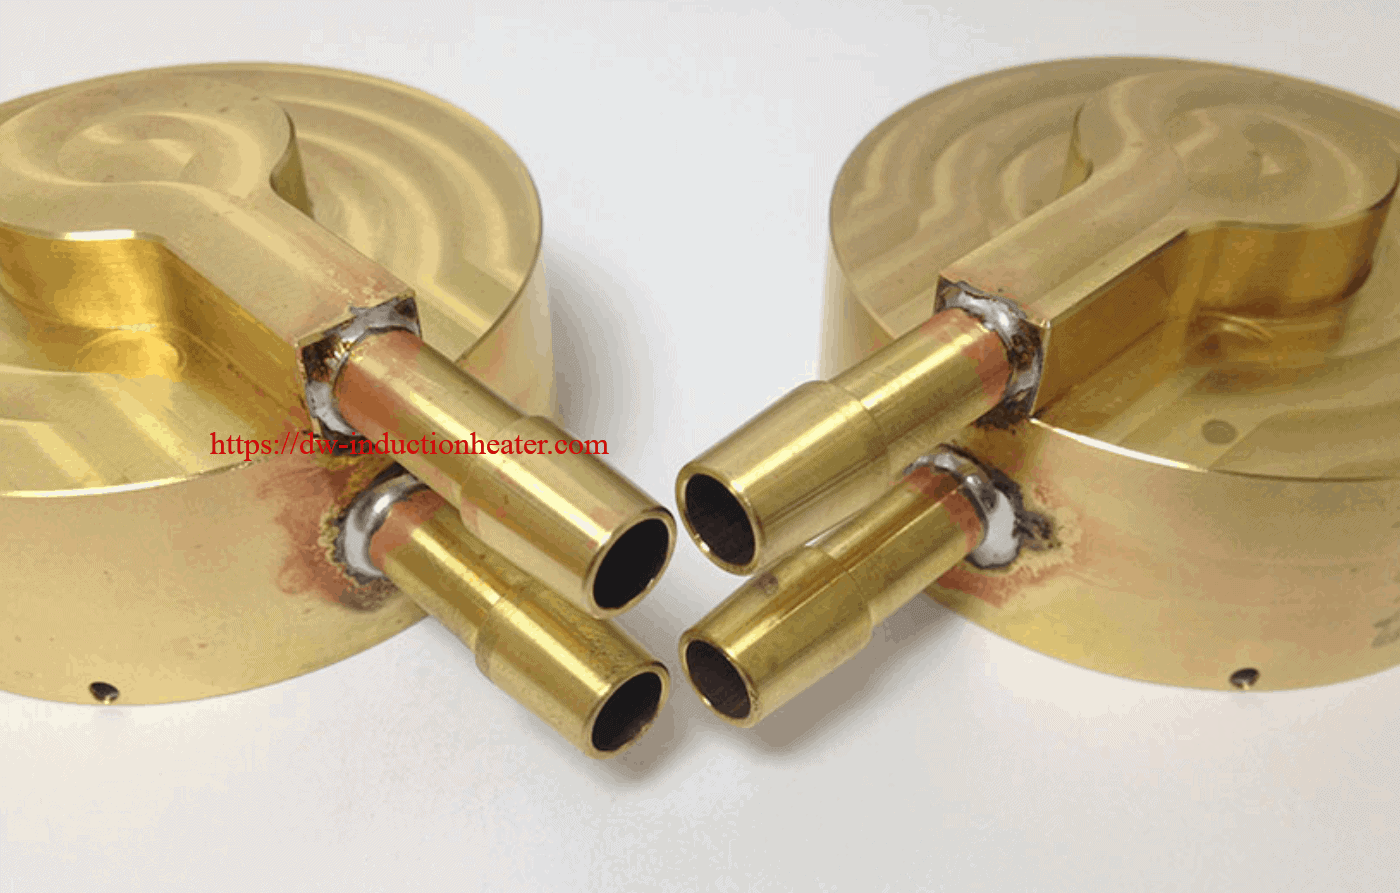
Results:
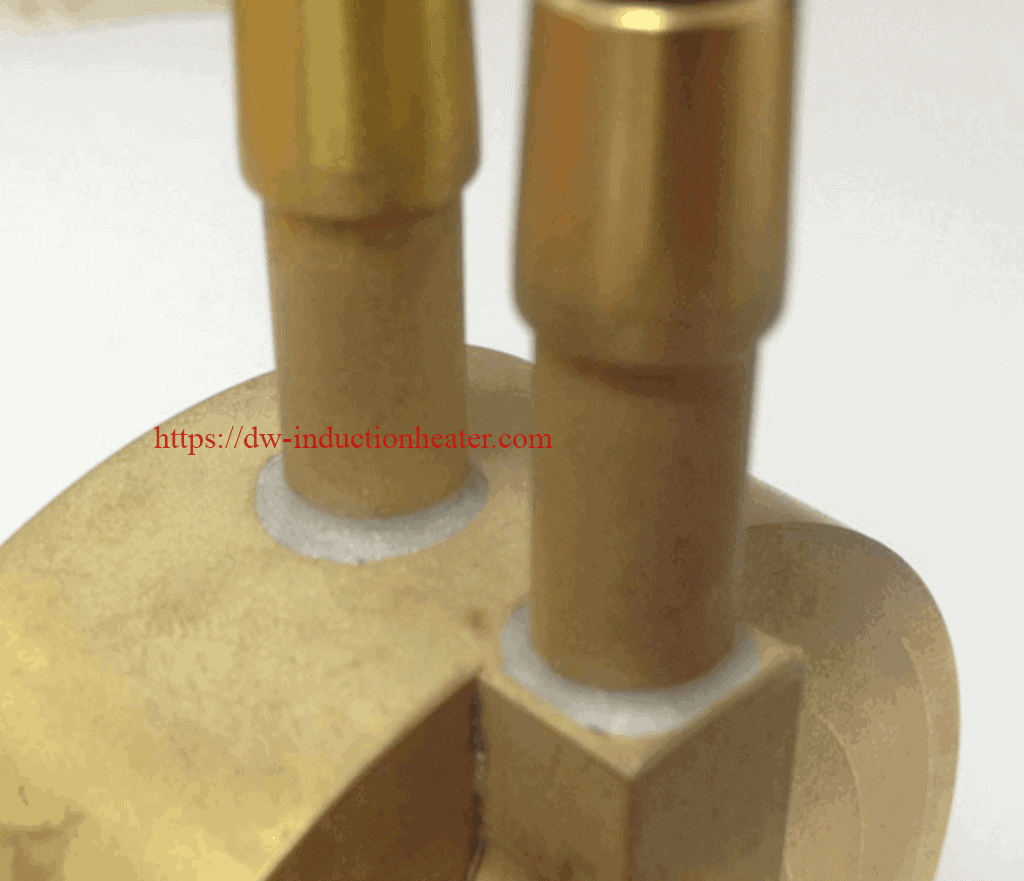
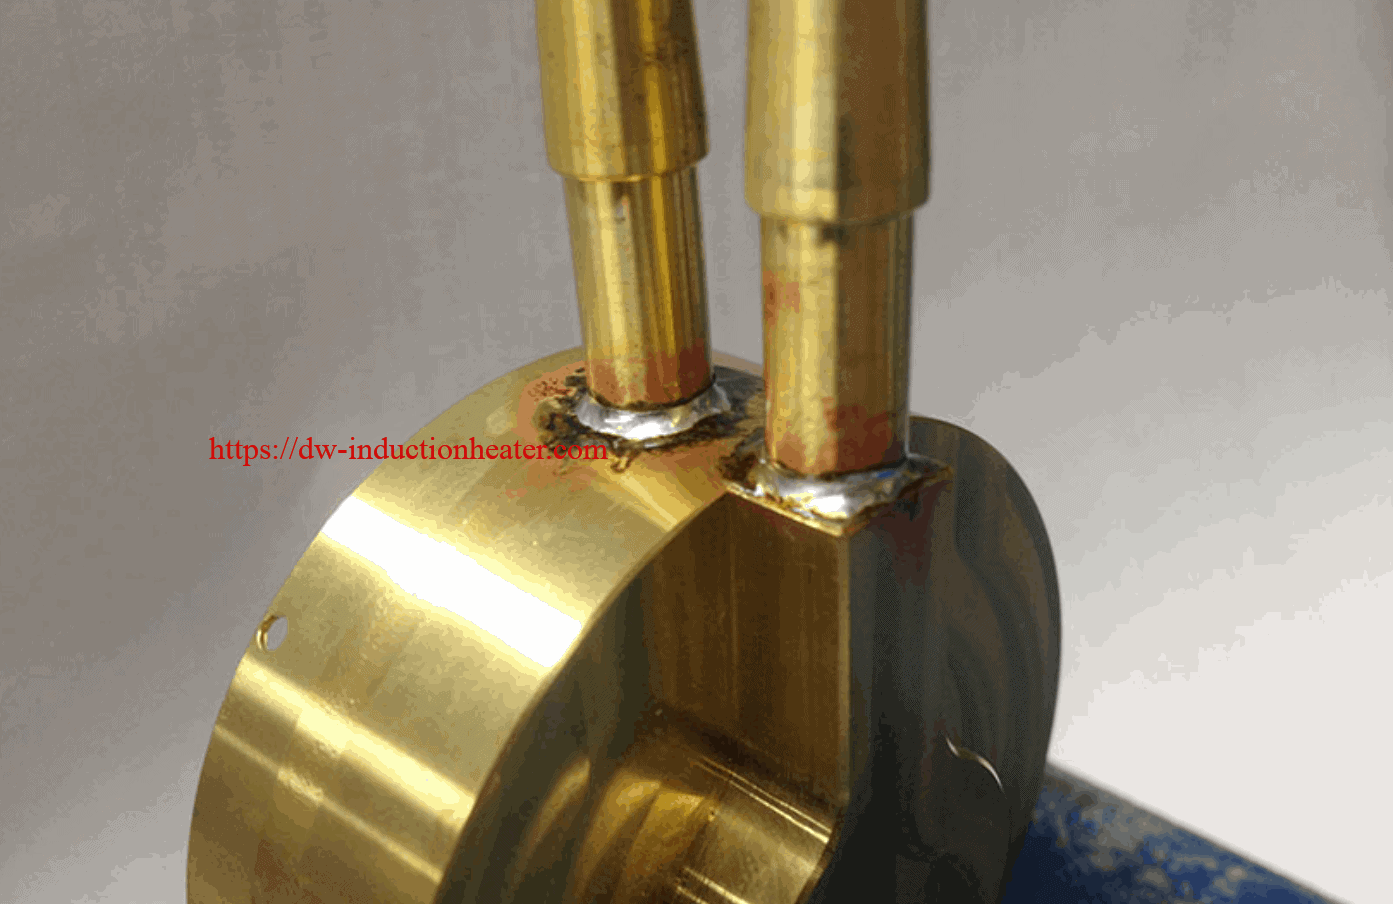
Brass inlet/outlet tubes were successfully brazed to the brass assembly with induction heating. The piece needs to be positioned so that the tube is close to the end of the coil. The solder joint on the thin wall of the assembly will reach soldering temperature in 10 seconds. The second solder joint will reach soldering temperature an average of 10 seconds later (15 seconds total). An additional 5 seconds of heating might be necessary to allow the solder to flow evenly around the tubes to improve final quality and appearance.




2024年2月28日星期三
Induction Soldering Copper Cables to Copper Pins
Induction Soldering Copper Cables to Copper Pins
Objective:
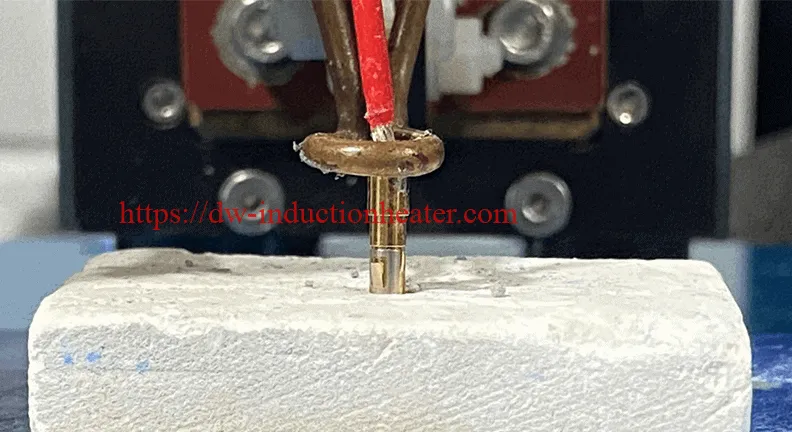
The objective of this induction heating application is to solder cables to copper pins for harness manufacturing. The customer is a manufacturer of mission-critical test systems for the Aerospace Industry. The goal is to reduce soldering time from 10 minutes by hand to less than 1 minute with the help of an induction heating system and increase solder quality and repeatability.
 Equipment:
HLQ has a line of induction soldering equipment, typically used in a similar application – DW-UHF series, high frequency induction heating systems for induction soldering and brazing of small components and parts.
 Process:
The customer provided a large cable with 0.2”(5.08 cm) OD and a pin 1”(2.5 cm) long, 0.178” (0.44 cm) OD, a cable receiver 0.2” (5.08 cm) long, 0.169” (0.42 cm) ID, 0.19” OD and a small cable with 0.09” (0.22 cm) OD, as well as, a small pin 0.114”( 0.28 cm) OD and a cable receiver 0.16”( 0.40 cm) long, 0.07”( 0.17 cm) ID. 0.129” (0.32 cm) OD.
 Induction Soldering paste was applied inside the cable receiver on the pin and to the stripped end of the cable. The pin was then placed in its holder. The induction heating coil entirely covered the cable receiver. Induction soldering with the DW-UHF-6KW-I handheld induction brazing system was completed in 2 seconds at 60% power to a temperature of ~600°F (315°C).
 Industry: Aerospace & Defense

 https://dw-inductionheater.com/induction-soldering-copper-cables-to-copper-pins.html?feed_id=235292&_unique_id=65dfe818e45f5
2023年9月25日星期一
induction soldering copper tubing to brass valves
High frequency induction soldering copper tubing to brass valves
Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine
Power: 16 kW
Temperature: 932oF (500oC)
Time: 20 seconds
Coil: Coated custom-made coil.
The Process:
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints. The use of induction heating was successful in this HVAC application.
2023年8月11日星期五
induction soldering copper tubing to brass valves
High frequency induction soldering copper tubing to brass valves
Objective: Test: Induction Soldering copper tubing to brass valves Industry: HVAC Materials: Copper and brass pipes
Equipment: DW-HF-25kw induction heating machine
Power: 16 kW
Temperature: 932oF (500oC)
Time: 20 seconds
Coil: Coated custom-made coil.
The Process:
This application request was brought to HLQ Induction Heating Power’s attention by a HVAC company. Their goal was to eliminate their current use of the torch method, as well as remove defects and improve the safety for operators. To start the test, our applications engineer assembled the setup of copper tubing and brass valves. After applying flux to each joint the engineer heated them for 20 seconds. Solder was manually applied after the joints reached 932oF (500o C), and created an even solder around the joints. The use of induction heating was successful in this HVAC application.
https://dw-inductionheater.com/induction-soldering-copper-tubing-to-brass-valves.html?feed_id=222736&_unique_id=64d639de7c3cb
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.