显示标签为“solderingbrass”的博文。显示所有博文

2024年5月22日星期三

Induction Soldering Brass Rings

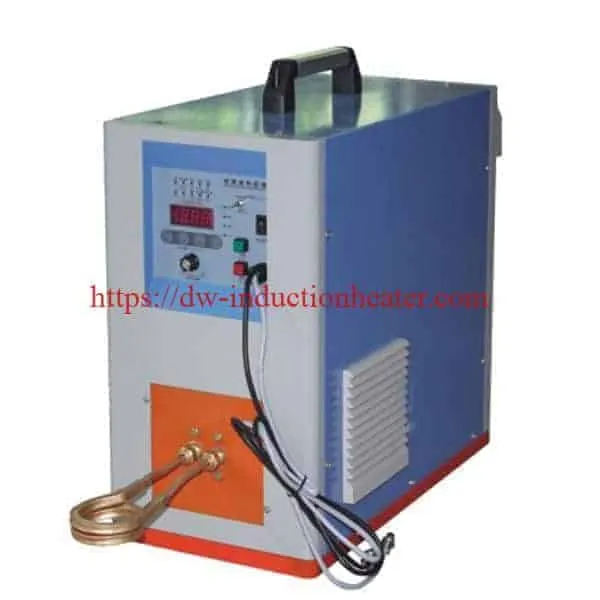
Induction Soldering Brass Rings With High Frequency IGBT Induction Heater Objective: To heat 1 3/4", 3" and 6" diameter brass slip rings and a sheathed copper wire assembly to 3600 F for soldering within three (3) to six (6) seconds. Currently production is accomplished by using a soldering iron and stick feeding rosin cored solder. This process leaves unwanted solder on the side of the slip ring where the soldering iron makes contact. The customer would like to see an increase in joint quality without sacrificing time. Material: 303 Brass Slip Rings of 1 3/4", 3" and 6" diameters. Sheathed Copper Wire Assembly. Resin Core Solder, 37% Pb, 63% Sn. Temperature: 3750F Application: Through laboratory testing, the DW-UHF-20kW output solid state induction power supply along with a unique four (4) turn "ear muff" type coil produced the following results: Times to reach 3750 F are as listed below: - 1 3/4" in 3 seconds - 3" in 3-4 seconds - 6" in 5 seconds Adequate solder flow was observed producing a clean joint. Solder preforms are recommended to speed up production. Side loading was facilitated by the unique four (4) turn "ear muff" style coil. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.0 μFcapacitor, a 4-20mA input for fast ramp simulation, and a unique four (4) turn "ear muff" style coil. Frequency: 265 kHz induction soldering brass ring https://dw-inductionheater.com/induction-soldering-brass-rings.html?feed_id=246606&_unique_id=664de0d1bbef6

2024年5月21日星期二

Induction Soldering Brass Assembly

Induction Soldering Brass Assembly With High Frequency Soldering Units Objective: To heat a brass bellows and end cap assembly to 4500F for soldering within 20 seconds. Presently, a soldering iron is used to produce the joint between the bellows and cap. The customer requests a quality solder joint with minimal heating of the bellows to prevent annealing and performance losses. Solder preforms, in the form of flat washers, are to be used to complete this application. Material: Brass Bellows measuring 2" in diameter Solder Preforms Cadmium Free Flux Temperature: 4500F Application: The DW-UHF-20kW output solid state induction power supply along with a unique three (3) turn double wound helical coil was utilized to achieve the following results: 4500F was reached and solder flow completed in 6.3 seconds. A quality repeatable solder joint was observed. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn double wound helical coil with an inside diameter of 0.4". Frequency: 307 kHz Induction Soldering Brass https://dw-inductionheater.com/induction-soldering-brass-assembly.html?feed_id=246509&_unique_id=664d2a1346aa0

2024年5月20日星期一

Induction Soldering Brass Tube-Pipe

Induction Soldering Brass Tube-Pipe-Tubing With RF Soldering Heating System Objective: Soldering two brass tubes measuring 3/4" and 1/4" together for use as cellular phone antennas. The lengths of tubes range from four (4) feet to twelve (12) feet, and must be soldered along the axial side. The joint is to be made using 60/40 Tin Lead Solder and Kestor Rosin paste flux. Material: Brass Tubes measuring 3/4" and 1/4" 60/40 Tin Lead Solder Kestor Rosin Flux Temperature: 3750F Application: Through the use of the the DW-UHF-40KW output solid state induction power supply along with a unique five (5) turn 12" long channel coil, the following results were achieved: 3750 F was reached and the solder flowed after a heating period of 35 seconds. A production rate of 24" per minute was determined to be adequate. A quality solder fillet was observed after heating and cooling Equipment: DW-UHF-40kW output solid state induction power supply including one (1) remote heat station containing two (2) capacitors, and a unique five (5) turn channel coil made from 3/16" copper tubing and measuring 1 1/4" by 12". Frequency: 385 kHz induction soldering brass tube     https://dw-inductionheater.com/induction-soldering-brass-tube-pipe.html?feed_id=246344&_unique_id=664bbc671ac0e

2024年5月17日星期五

Induction Soldering Brass Heating Exchanger

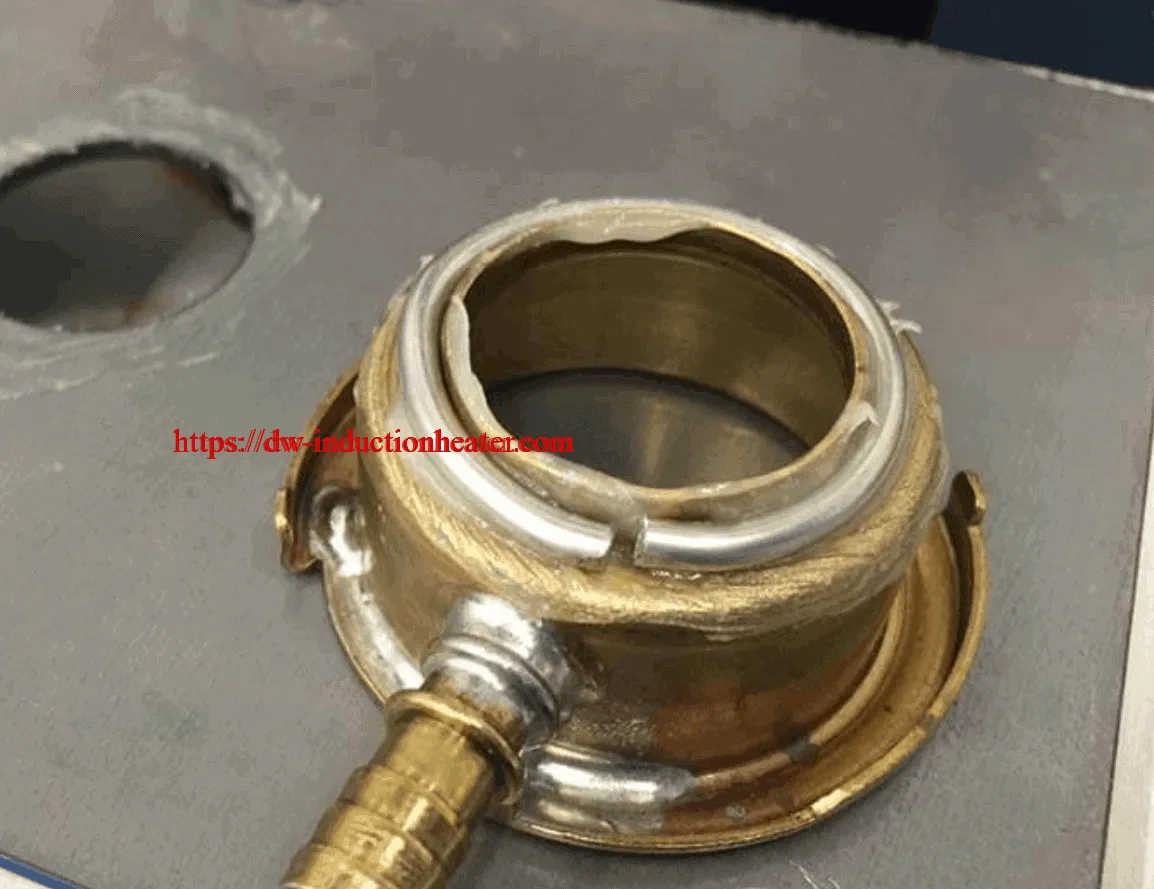
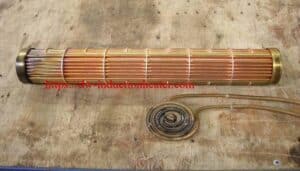
Induction Soldering Brass Heating Exchanger Of a Series Copper Pipe  Objective To solder a brass end cap to a series of copper tubes Material Preassembled heat exchanger with copper tubes and 2 brass end caps 2.36” (60mm) OD, 0.08” to 0.12” (2 to 3mm) thick at both ends, liquid solder Temperature 302ºF (150ºC) 482ºF (250ºC) Frequency 237kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor • An induction heating coil designed and developed specifically for this application. Process A dual four turn pancake coil is used to solder 2 brass caps per cycle. Liquid solder is squirted onto the end cap and is heated for 18 seconds at 302ºF (150ºC) to burn off the flux. Then the heat is increased to 482ºF (250ºC) for 15 seconds to solder the parts. Results Induction heating provides: • Even distribution of heating • Compared to hot plate, induction heating is able to heat two parts in 30 seconds vs. one part in 60 seconds • Increased production • No discoloration with the slow heating process induction soldering brass heating exchanger             induction soldering brass end                   soldering brass pipe https://dw-inductionheater.com/induction-soldering-brass-heating-exchanger.html?feed_id=245936&_unique_id=664773ac3c930
2024年5月13日星期一

Induction Soldering Brass Connector

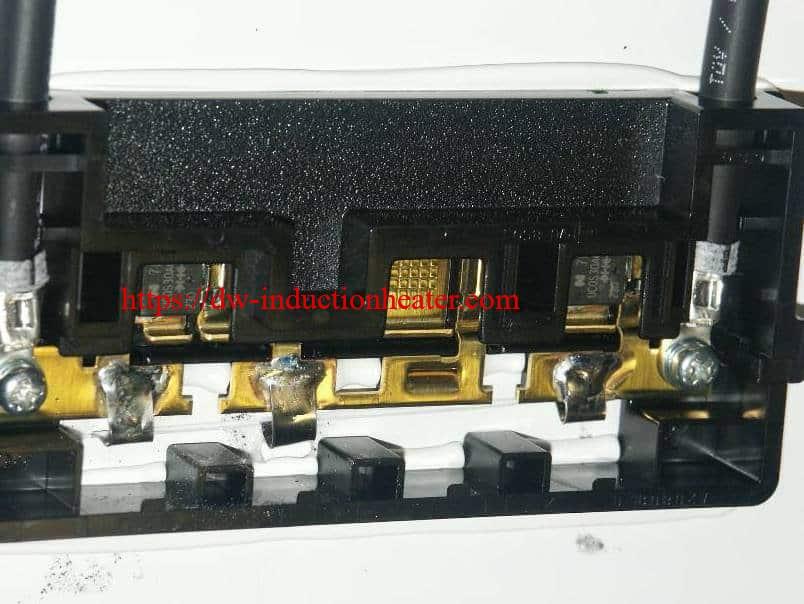
Induction Soldering Brass Connector In Solar Panel With IGBT Induction Heater Objective Solder three brass connectors one at a time in a solar panel junction box without affecting the components in the junction box Material Solar panel junction box, brass connectors, solder wire Temperature 700 ºF (371 ºC) Frequency 344 kHz Equipment • DW-UHF-6 kW induction heating system, equipped with a remote workhead containing one 1.0 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A three turn oval shaped helical coil is used to heat the connectors. A piece of solder wire is placed onto the joint area and each joint is heated separately for 5 seconds to solder the connector. The total process time is 15 seconds for the three joints. Results/Benefits Induction heating provides: • Pinpoint accuracy deliver heating only to joint; does not affect surrounding components • Localized heat produces neat and clean joints • Produces high quality, repeatable results • Even distribution of heating brass connectior               rf soldering brass connector               induction soldering brass connector https://dw-inductionheater.com/induction-soldering-brass-connector.html?feed_id=245392&_unique_id=6641bd1a8f93f

2024年4月2日星期二

Induction Soldering Brass Corner Joint

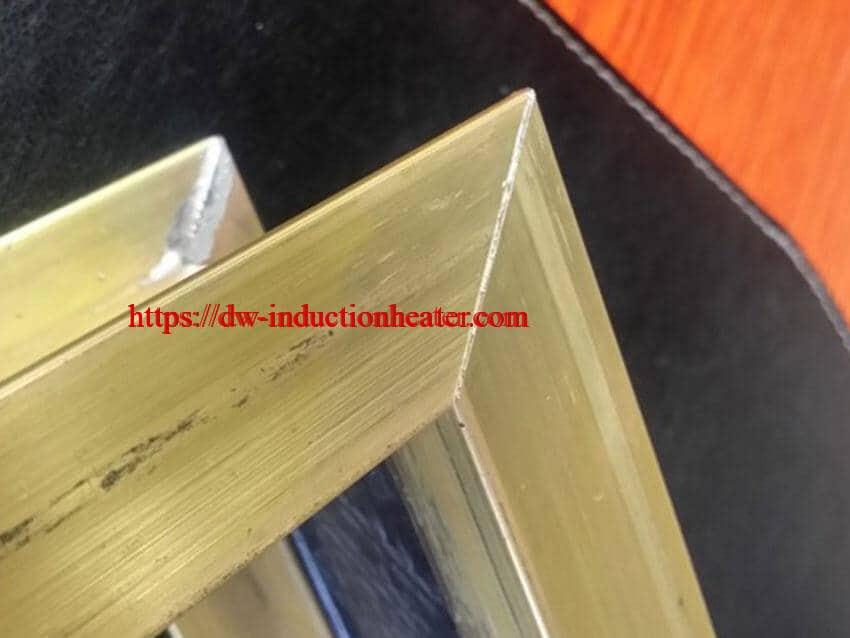
Hig Frequency Induction Soldering Brass Corner Joint

Objective Successfully solder two 45° brass corner joints. Equipment: DW-UHF-10kw induction soldering heater Materials StayBrite #8 silver solder supplied by customer Bridgit solder flux supplied by customer Brass corner joint Pancake coil Key Parameters Power: 5.5 kW Temperature: Approximately 550° F (288° C) Time: 20 sec
Process:
  1. Flux is applied at all joints.
  2. The assembly is positioned into for heating
  3. Induction heating is applied for 15 sec
  4. The brazing rod is applied to the joint
Results/Benefits:
  1. Since the brazing alloy is manually fed, the coil is placed under the joint, facing the visible side of the frame. The visible side of the joint is laying on a flat wooden surface, which does not allow the brazing alloy to leak and spill. This keeps the visible surface nice and clean, while the seam is internally brazed.
  2. If solder paste is used, then the coil can be placed on top of the joint. If special dual coil is used, then both joints (top and bottom) can be done with one shot.
  3. No frame flipping is needed in this case. See the video and zoom the pictures attached for more details.
  4. No special cleaning is needed on either side of the joint. The samples on the pictures have been paper towel wiped only.
https://dw-inductionheater.com/induction-soldering-brass-corner-joint.html?feed_id=239730&_unique_id=660c2e3872b24

2024年3月30日星期六

Induction Soldering Brass to Steel Plate

High Frequency Induction Soldering Brass to Steel Plate Technology

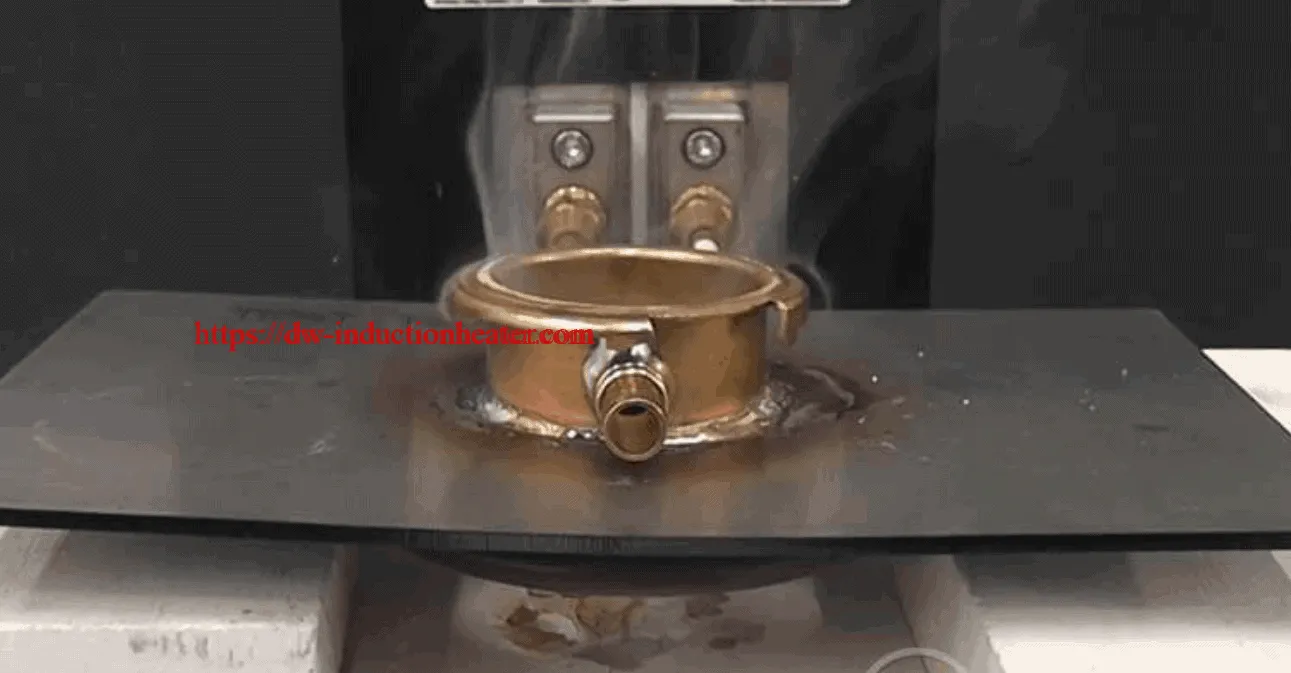
Objective High Frequency Induction Soldering brass to steel plate Equipment DW-UHF-6KW-I handheld induction brazing heater
Materials Steel plate to brass part induction soldering using Harris Stay-Brite #8 Silver Bearing Solder and Harris Bridgit Lead Free Soldering Flux. Key Parameters Power: 2kW Temperature: 535°F to 585°F (279°C to 307°C) Time: 21 Seconds  
https://dw-inductionheater.com/induction-soldering-brass-to-steel-plate.html?feed_id=239227&_unique_id=6607e5b4e654f

2023年11月11日星期六

Induction Soldering Brass Heating Exchanger

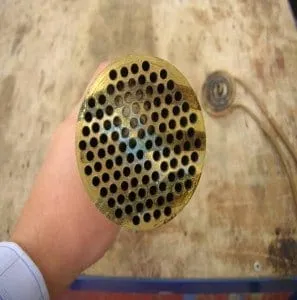
Induction Soldering Brass Heating Exchanger Of a Series Copper Pipe  Objective To solder a brass end cap to a series of copper tubes Material Preassembled heat exchanger with copper tubes and 2 brass end caps 2.36” (60mm) OD, 0.08” to 0.12” (2 to 3mm) thick at both ends, liquid solder Temperature 302ºF (150ºC) 482ºF (250ºC) Frequency 237kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor • An induction heating coil designed and developed specifically for this application. Process A dual four turn pancake coil is used to solder 2 brass caps per cycle. Liquid solder is squirted onto the end cap and is heated for 18 seconds at 302ºF (150ºC) to burn off the flux. Then the heat is increased to 482ºF (250ºC) for 15 seconds to solder the parts. Results Induction heating provides: • Even distribution of heating • Compared to hot plate, induction heating is able to heat two parts in 30 seconds vs. one part in 60 seconds • Increased production • No discoloration with the slow heating process induction soldering brass heating exchanger             induction soldering brass end                   soldering brass pipe
2023年10月25日星期三

Induction Soldering Brass Heating Exchanger

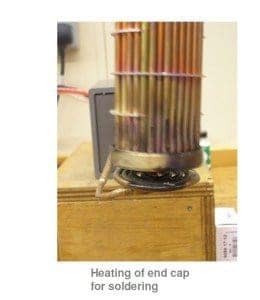
Induction Soldering Brass Heating Exchanger Of a Series Copper Pipe  Objective To solder a brass end cap to a series of copper tubes Material Preassembled heat exchanger with copper tubes and 2 brass end caps 2.36” (60mm) OD, 0.08” to 0.12” (2 to 3mm) thick at both ends, liquid solder Temperature 302ºF (150ºC) 482ºF (250ºC) Frequency 237kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor • An induction heating coil designed and developed specifically for this application. Process A dual four turn pancake coil is used to solder 2 brass caps per cycle. Liquid solder is squirted onto the end cap and is heated for 18 seconds at 302ºF (150ºC) to burn off the flux. Then the heat is increased to 482ºF (250ºC) for 15 seconds to solder the parts. Results Induction heating provides: • Even distribution of heating • Compared to hot plate, induction heating is able to heat two parts in 30 seconds vs. one part in 60 seconds • Increased production • No discoloration with the slow heating process induction soldering brass heating exchanger             induction soldering brass end                   soldering brass pipe
2023年9月29日星期五

Induction Soldering Brass Rings

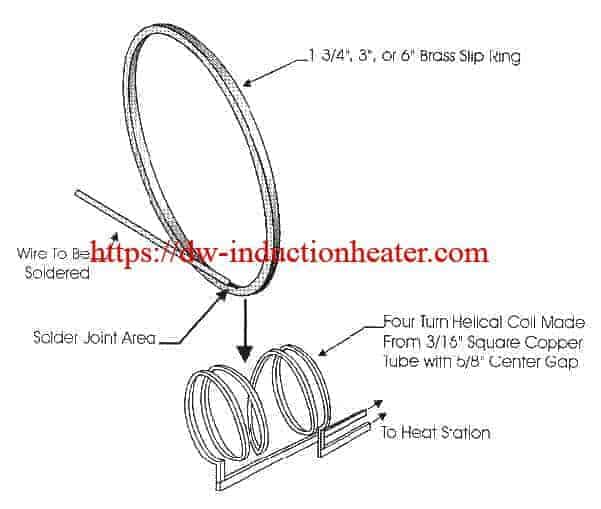
Induction Soldering Brass Rings With High Frequency IGBT Induction Heater Objective: To heat 1 3/4", 3" and 6" diameter brass slip rings and a sheathed copper wire assembly to 3600 F for soldering within three (3) to six (6) seconds. Currently production is accomplished by using a soldering iron and stick feeding rosin cored solder. This process leaves unwanted solder on the side of the slip ring where the soldering iron makes contact. The customer would like to see an increase in joint quality without sacrificing time. Material: 303 Brass Slip Rings of 1 3/4", 3" and 6" diameters. Sheathed Copper Wire Assembly. Resin Core Solder, 37% Pb, 63% Sn. Temperature: 3750F Application: Through laboratory testing, the DW-UHF-20kW output solid state induction power supply along with a unique four (4) turn "ear muff" type coil produced the following results: Times to reach 3750 F are as listed below: - 1 3/4" in 3 seconds - 3" in 3-4 seconds - 6" in 5 seconds Adequate solder flow was observed producing a clean joint. Solder preforms are recommended to speed up production. Side loading was facilitated by the unique four (4) turn "ear muff" style coil. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.0 μFcapacitor, a 4-20mA input for fast ramp simulation, and a unique four (4) turn "ear muff" style coil. Frequency: 265 kHz induction soldering brass ring https://dw-inductionheater.com/induction-soldering-brass-rings.html?feed_id=228131&_unique_id=65173d4827183

Induction Soldering Brass Assembly

Induction Soldering Brass Assembly With High Frequency Soldering Units Objective: To heat a brass bellows and end cap assembly to 4500F for soldering within 20 seconds. Presently, a soldering iron is used to produce the joint between the bellows and cap. The customer requests a quality solder joint with minimal heating of the bellows to prevent annealing and performance losses. Solder preforms, in the form of flat washers, are to be used to complete this application. Material: Brass Bellows measuring 2" in diameter Solder Preforms Cadmium Free Flux Temperature: 4500F Application: The DW-UHF-20kW output solid state induction power supply along with a unique three (3) turn double wound helical coil was utilized to achieve the following results: 4500F was reached and solder flow completed in 6.3 seconds. A quality repeatable solder joint was observed. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn double wound helical coil with an inside diameter of 0.4". Frequency: 307 kHz Induction Soldering Brass https://dw-inductionheater.com/induction-soldering-brass-assembly.html?feed_id=228101&_unique_id=651686a978c6b

2023年9月27日星期三

Induction Soldering Brass to Steel Plate

High Frequency Induction Soldering Brass to Steel Plate Technology

Objective High Frequency Induction Soldering brass to steel plate Equipment DW-UHF-6KW-I handheld induction brazing heater
Materials Steel plate to brass part induction soldering using Harris Stay-Brite #8 Silver Bearing Solder and Harris Bridgit Lead Free Soldering Flux. Key Parameters Power: 2kW Temperature: 535°F to 585°F (279°C to 307°C) Time: 21 Seconds  

2023年9月24日星期日

Induction Soldering Brass Heating Exchanger

Induction Soldering Brass Heating Exchanger Of a Series Copper Pipe  Objective To solder a brass end cap to a series of copper tubes Material Preassembled heat exchanger with copper tubes and 2 brass end caps 2.36” (60mm) OD, 0.08” to 0.12” (2 to 3mm) thick at both ends, liquid solder Temperature 302ºF (150ºC) 482ºF (250ºC) Frequency 237kHz Equipment • DW-UHF-20kW induction heating system, equipped with a remote workhead containing one 1.0μF capacitor • An induction heating coil designed and developed specifically for this application. Process A dual four turn pancake coil is used to solder 2 brass caps per cycle. Liquid solder is squirted onto the end cap and is heated for 18 seconds at 302ºF (150ºC) to burn off the flux. Then the heat is increased to 482ºF (250ºC) for 15 seconds to solder the parts. Results Induction heating provides: • Even distribution of heating • Compared to hot plate, induction heating is able to heat two parts in 30 seconds vs. one part in 60 seconds • Increased production • No discoloration with the slow heating process induction soldering brass heating exchanger             induction soldering brass end                   soldering brass pipe https://dw-inductionheater.com/induction-soldering-brass-heating-exchanger.html?feed_id=227861&_unique_id=6510d03dcfd25
2023年9月20日星期三

Induction Soldering Brass Connector

Induction Soldering Brass Connector In Solar Panel With IGBT Induction Heater Objective Solder three brass connectors one at a time in a solar panel junction box without affecting the components in the junction box Material Solar panel junction box, brass connectors, solder wire Temperature 700 ºF (371 ºC) Frequency 344 kHz Equipment • DW-UHF-6 kW induction heating system, equipped with a remote workhead containing one 1.0 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A three turn oval shaped helical coil is used to heat the connectors. A piece of solder wire is placed onto the joint area and each joint is heated separately for 5 seconds to solder the connector. The total process time is 15 seconds for the three joints. Results/Benefits Induction heating provides: • Pinpoint accuracy deliver heating only to joint; does not affect surrounding components • Localized heat produces neat and clean joints • Produces high quality, repeatable results • Even distribution of heating brass connectior               rf soldering brass connector               induction soldering brass connector https://dw-inductionheater.com/induction-soldering-brass-connector.html?feed_id=227621&_unique_id=650b19623607d

Induction Soldering Brass Assembly

Induction Soldering Brass Assembly With High Frequency Soldering Units Objective: To heat a brass bellows and end cap assembly to 4500F for soldering within 20 seconds. Presently, a soldering iron is used to produce the joint between the bellows and cap. The customer requests a quality solder joint with minimal heating of the bellows to prevent annealing and performance losses. Solder preforms, in the form of flat washers, are to be used to complete this application. Material: Brass Bellows measuring 2" in diameter Solder Preforms Cadmium Free Flux Temperature: 4500F Application: The DW-UHF-20kW output solid state induction power supply along with a unique three (3) turn double wound helical coil was utilized to achieve the following results: 4500F was reached and solder flow completed in 6.3 seconds. A quality repeatable solder joint was observed. Equipment: DW-UHF-20kW output solid state induction power supply including one (1) remote heat station containing one (1) 1.2 μF capacitor, and a unique three (3) turn double wound helical coil with an inside diameter of 0.4". Frequency: 307 kHz Induction Soldering Brass

2023年9月16日星期六

Induction Soldering Brass Connector

Induction Soldering Brass Connector In Solar Panel With IGBT Induction Heater Objective Solder three brass connectors one at a time in a solar panel junction box without affecting the components in the junction box Material Solar panel junction box, brass connectors, solder wire Temperature 700 ºF (371 ºC) Frequency 344 kHz Equipment • DW-UHF-6 kW induction heating system, equipped with a remote workhead containing one 1.0 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A three turn oval shaped helical coil is used to heat the connectors. A piece of solder wire is placed onto the joint area and each joint is heated separately for 5 seconds to solder the connector. The total process time is 15 seconds for the three joints. Results/Benefits Induction heating provides: • Pinpoint accuracy deliver heating only to joint; does not affect surrounding components • Localized heat produces neat and clean joints • Produces high quality, repeatable results • Even distribution of heating brass connectior               rf soldering brass connector               induction soldering brass connector
关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.