显示标签为“highfrquencyinductionsoldering”的博文。显示所有博文

2024年3月10日星期日

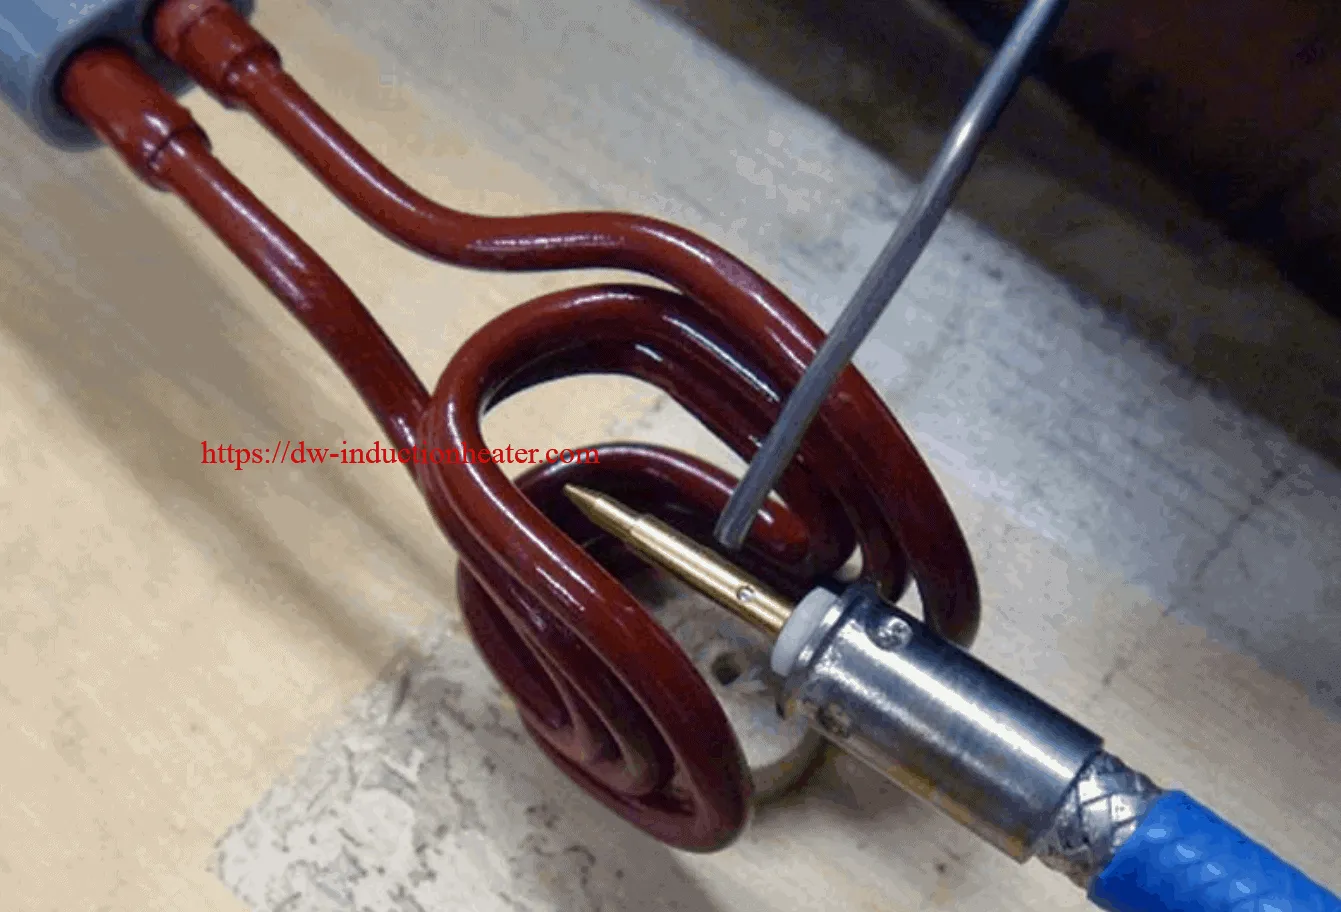
Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
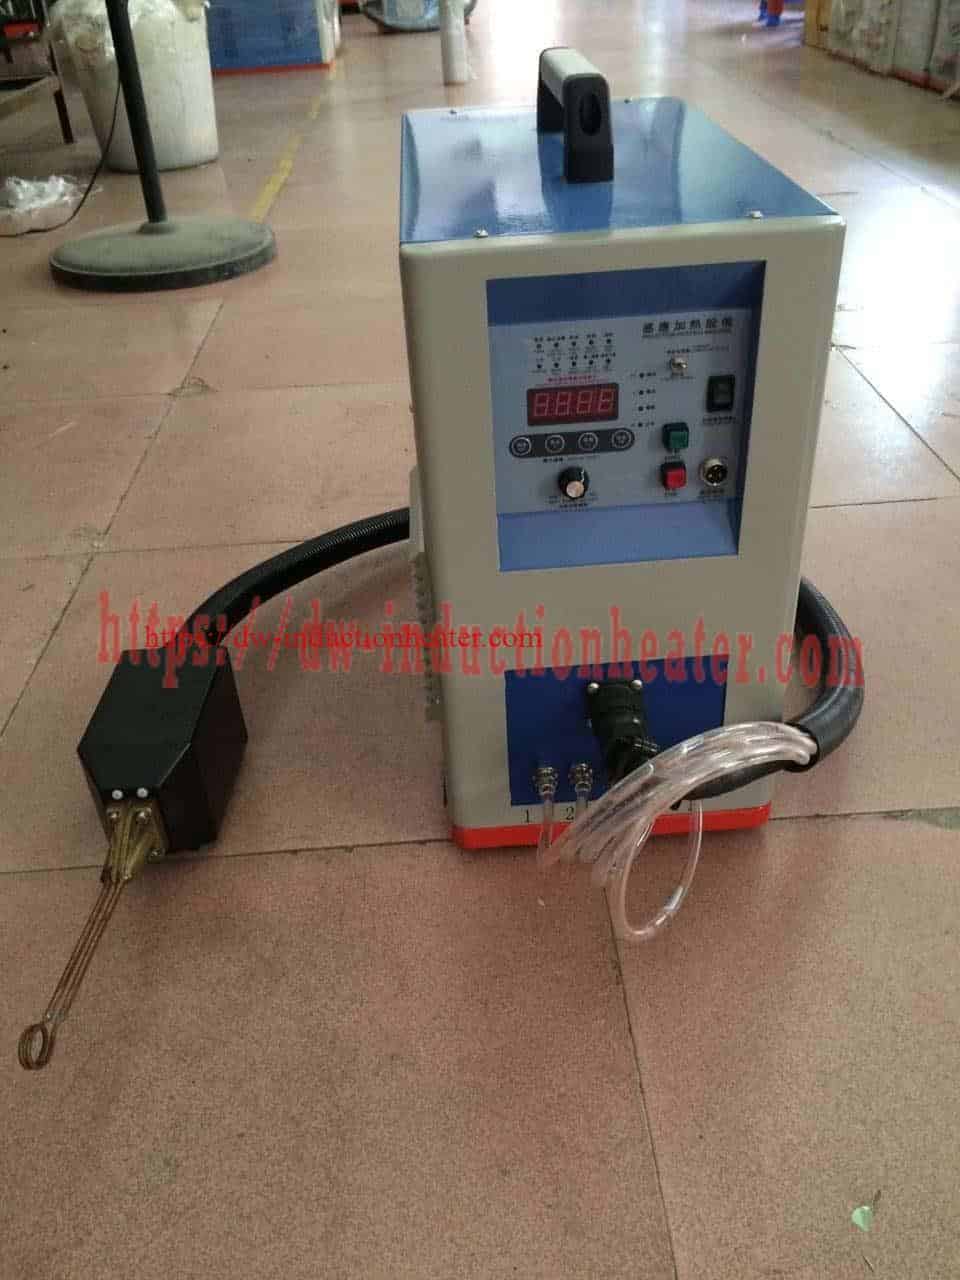
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
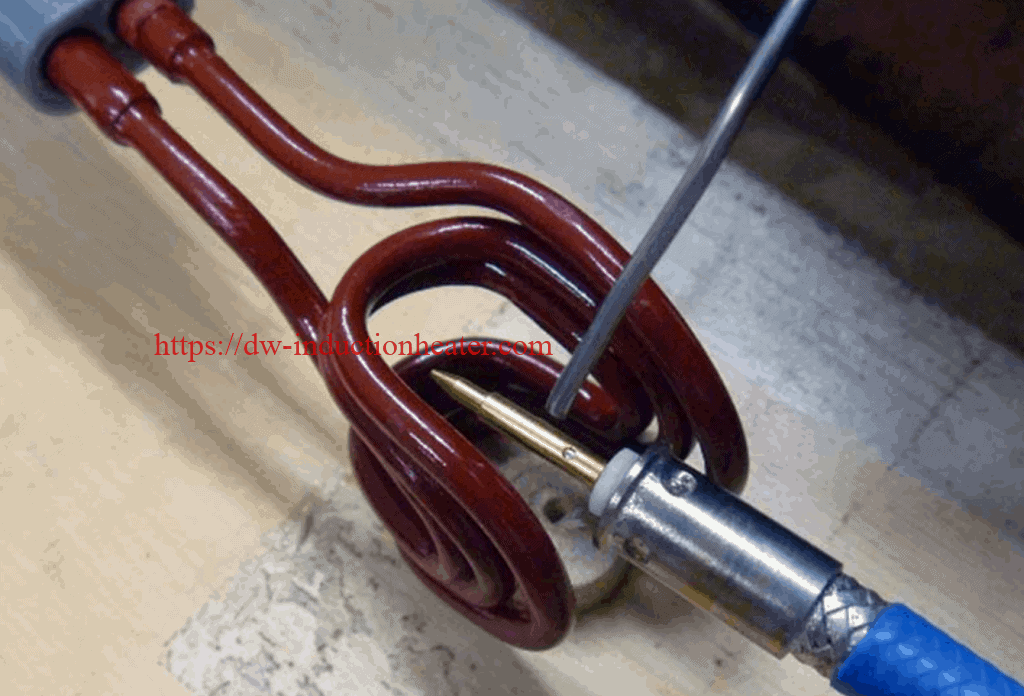
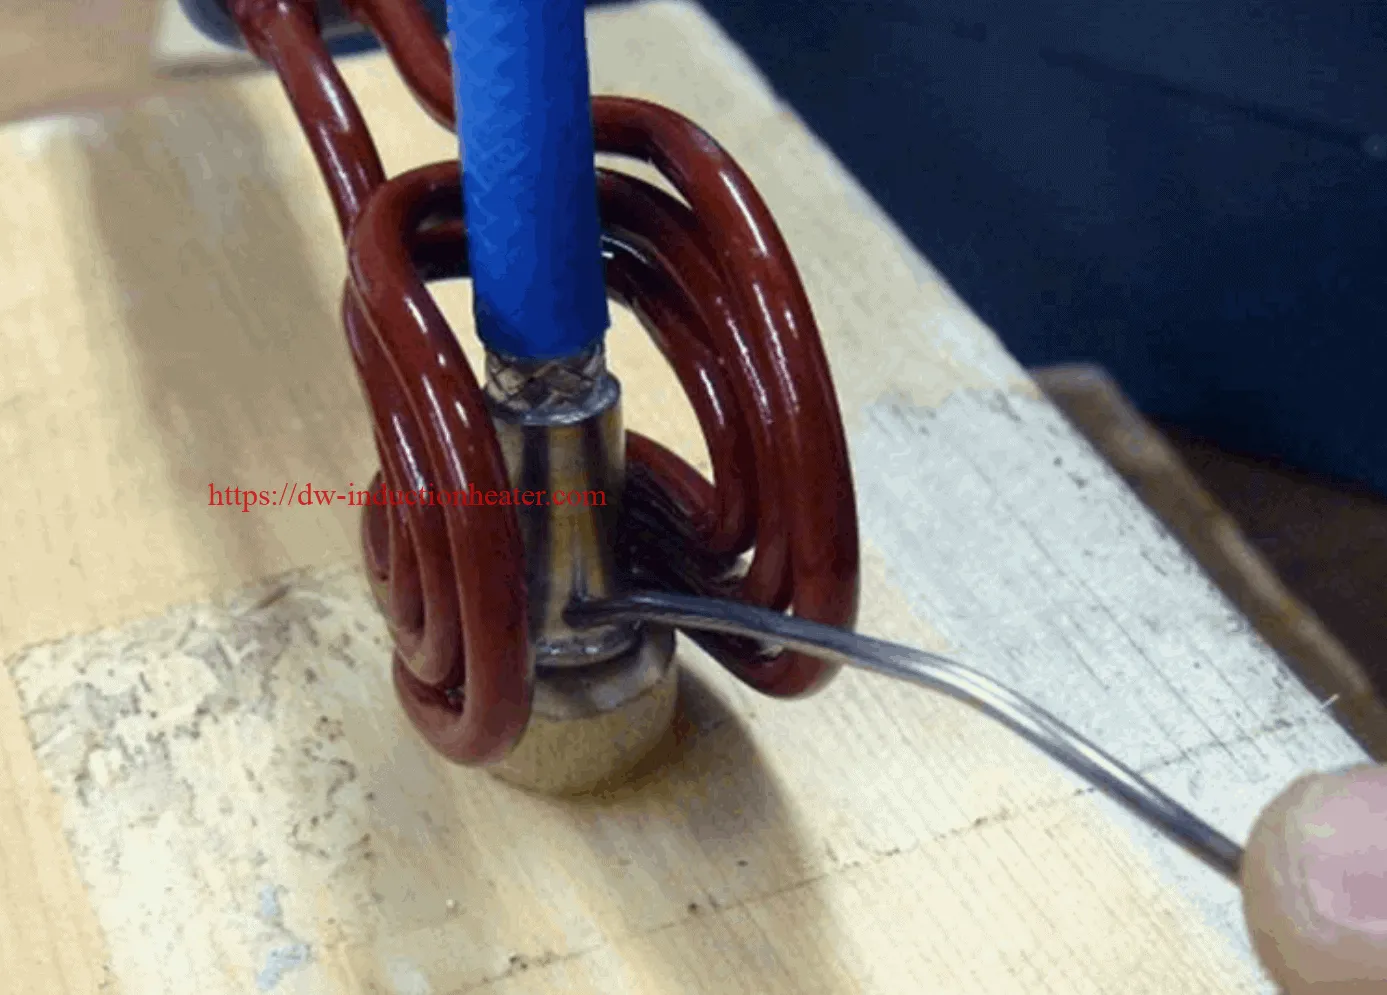
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
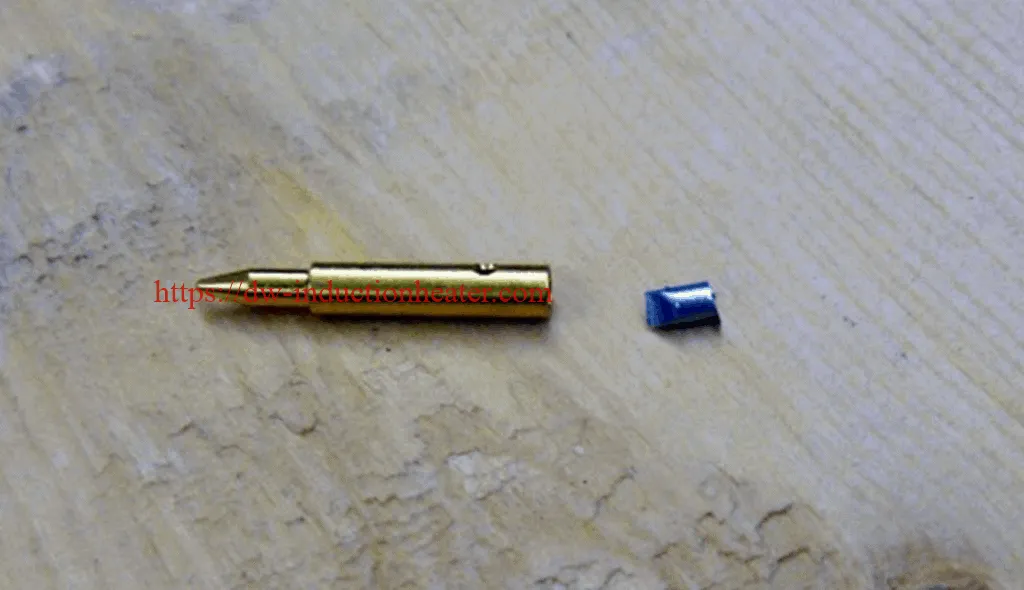
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]
https://dw-inductionheater.com/induction-soldering-coaxial-cable.html?feed_id=235992&_unique_id=65ed79a0e0191

2023年7月17日星期一

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]
https://dw-inductionheater.com/induction-soldering-coaxial-cable.html?feed_id=219361&_unique_id=64b604f0ea570

2023年1月4日星期三

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]

2022年11月30日星期三

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]

2022年11月23日星期三

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]

2022年5月30日星期一

Induction Soldering Coaxial Cable

Objective Induction Soldering coaxial cable to connector ring and pin in two steps in under 5 seconds by reaching a temperature of 500°F (260°C) with induction heating.
Equipment DW-UHF-6KW-III handheld induction heater Handheld induction brazing heater Channel coil Materials • No-flux solder wire • Coaxial cable • Cable connector • Center pin Key Parameters Power: 3.0kW Temperature: 662°F (350°C) Time: 5 sec
Process:
  1. The coaxial cable and connector were placed vertically inside the coil.
  2. Induction heating was applied for 3 seconds, at which point the part is hot enough for soldering.
  3. The induction soldering wire was fed between the cable braid and connector.
  4. Solder wire was inserted into the center pin, and the center pin was placed in the coil.
  5. The cable with connector was placed above the pin.
  6. Induction heat was applied for 1.5 seconds, after which the part was hot enough for soldering.
  7. The center conductor was inserted into the pin.
  8. The assembly was inspected to ensure that the soldering was successful.
Results/Benefits:
  • Strong durable joints and faster heating cycles
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Technology without pollution, which is both clean and safe
[wpforms id="3947"]

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.