 https://dw-inductionheater.com/product/rail-high-frequency-induction-hardening-machine?feed_id=271518&_unique_id=67c6c16e9073b
2025年3月4日星期二
Rail high frequency induction hardening machine
Rail high frequency induction hardening machine
https://dw-inductionheater.com/product/rail-high-frequency-induction-hardening-machine?feed_id=271518&_unique_id=67c6c16e9073b
https://dw-inductionheater.com/product/rail-high-frequency-induction-hardening-machine?feed_id=271518&_unique_id=67c6c16e9073b

2025年2月22日星期六
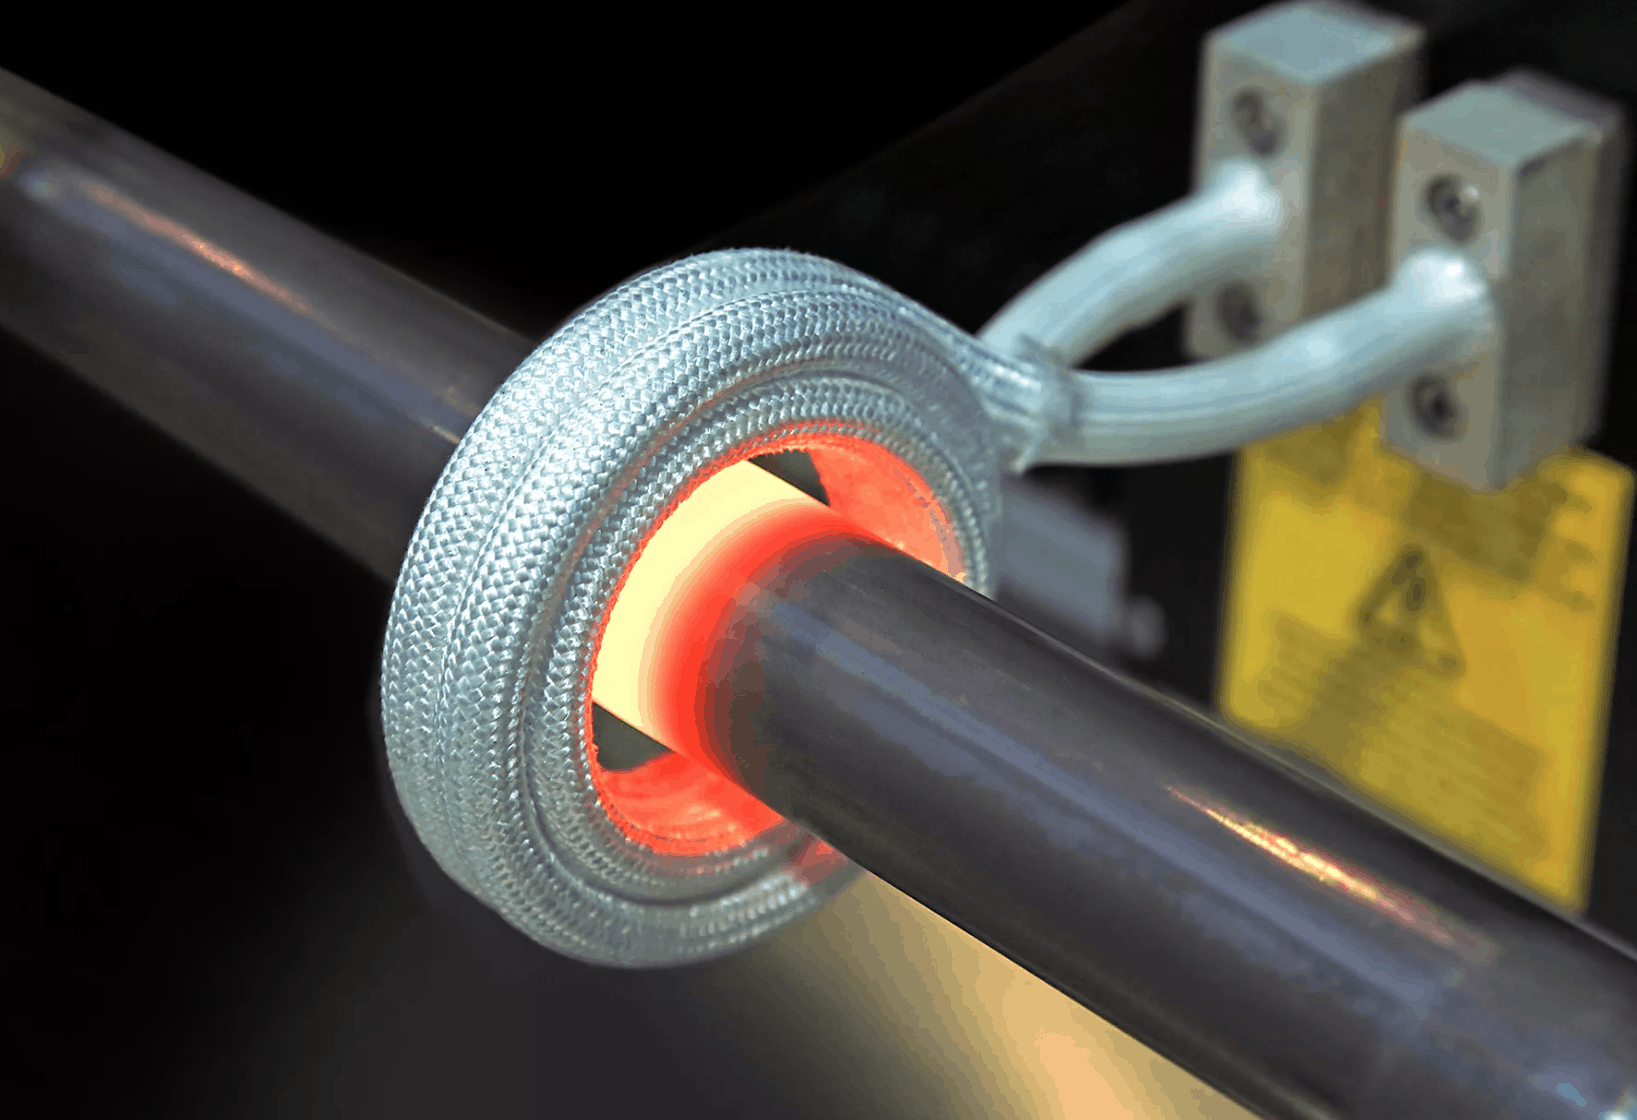
Induction Hardening Steel Pipe Surface
Induction Hardening Steel Pipe Surface
 https://dw-inductionheater.com/product/induction-hardening-steel-pipe-surface?feed_id=270532&_unique_id=67ba3b313d891
2025年2月15日星期六
induction Hardening Steel Cam Assembly
induction Hardening Steel Cam Assembly
 https://dw-inductionheater.com/product/induction-hardening-steel-cam-assembly?feed_id=269720&_unique_id=67b057e582e3d
2025年2月13日星期四
induction hardening the teeth of saw blade
induction hardening the teeth of saw blade
 https://dw-inductionheater.com/product/induction-hardening-the-teeth-of-saw-blade?feed_id=269575&_unique_id=67ae64763473d
Induction Hardening Steel Part with High Frequency Hardening Machine
Induction Hardening Steel Part with High Frequency Hardening Machine
 https://dw-inductionheater.com/induction-hardening-steel-part-with-high-frequency-hardening-machine.html?feed_id=269546&_unique_id=67ae5d75cc089
2025年1月25日星期六
high frequency induction hardening magnetic steel part process
high frequency induction hardening magnetic steel part process
 https://dw-inductionheater.com/product/high-frequency-induction-hardening-magnetic-steel-part-process?feed_id=267719&_unique_id=6795513752233
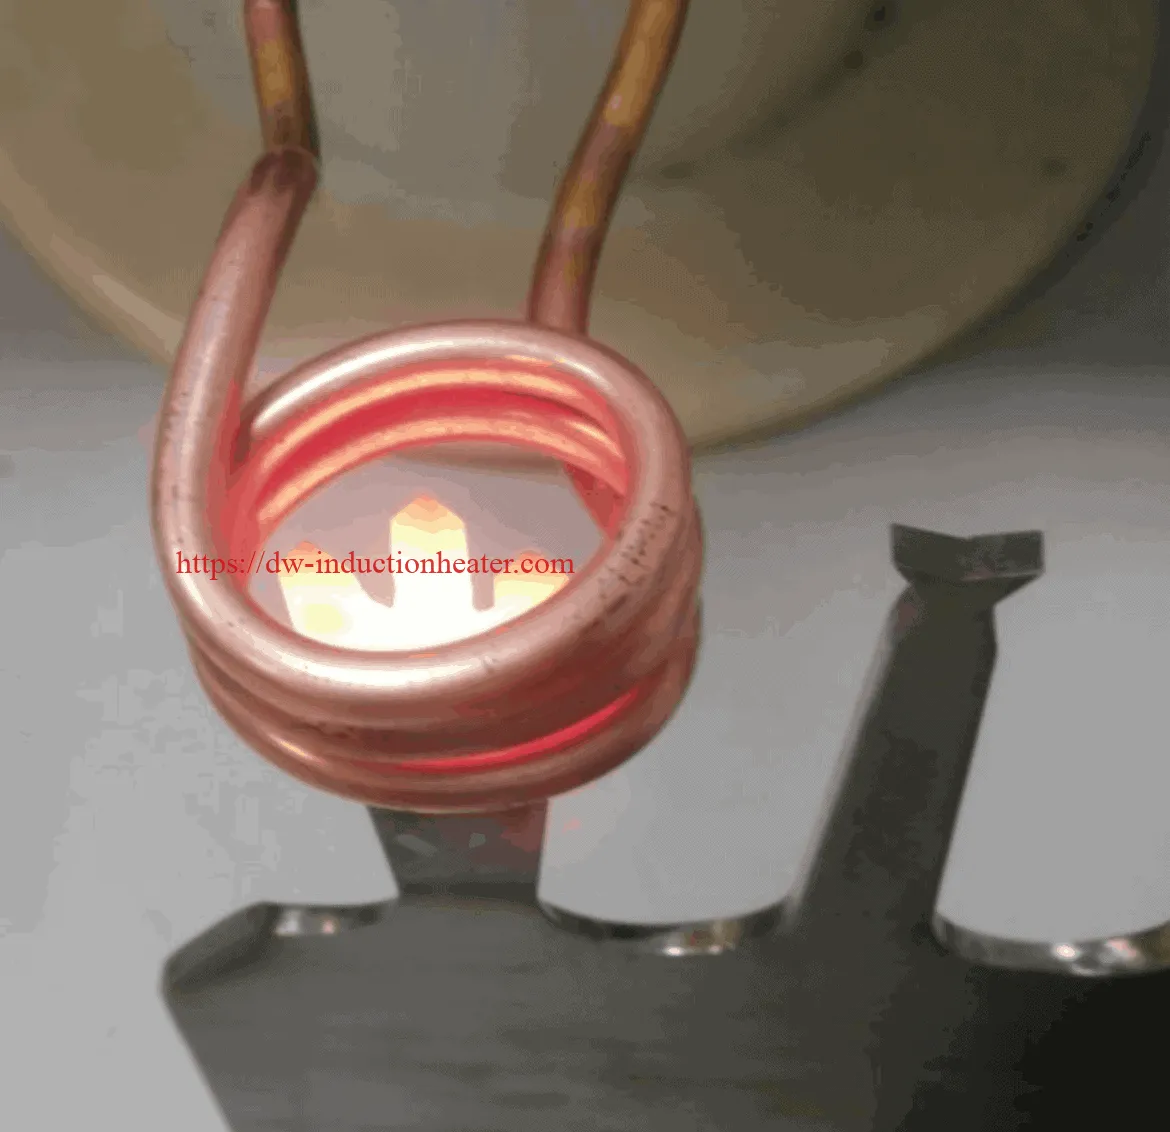
Induction hardening Jaw Teeth of Carbon Steel
Induction hardening Jaw Teeth of Carbon Steel
 https://dw-inductionheater.com/product/induction-hardening-jaw-teeth-of-carbon-steel?feed_id=267690&_unique_id=6794a8641892d
2025年1月24日星期五
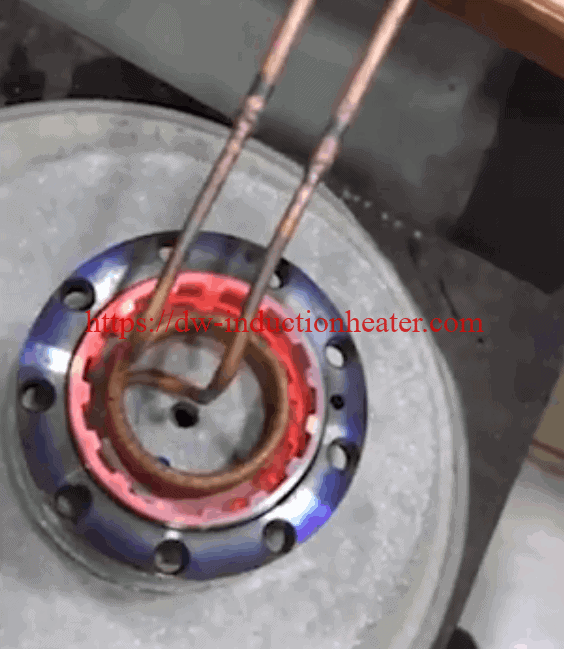
High frequency induction hardening flange groove process
High frequency induction hardening flange groove process
 https://dw-inductionheater.com/product/high-frequency-induction-hardening-flange-groove-process?feed_id=267632&_unique_id=6793ffadc4c00
2024年12月28日星期六
induction hardening steel handheld stamps
induction hardening steel handheld stamps
 https://dw-inductionheater.com/induction-hardening-steel-handheld-stamps.html?feed_id=264906&_unique_id=67700bd89df0e
2024年12月16日星期一
Induction Hardening Surface Process
Induction Hardening Surface Process
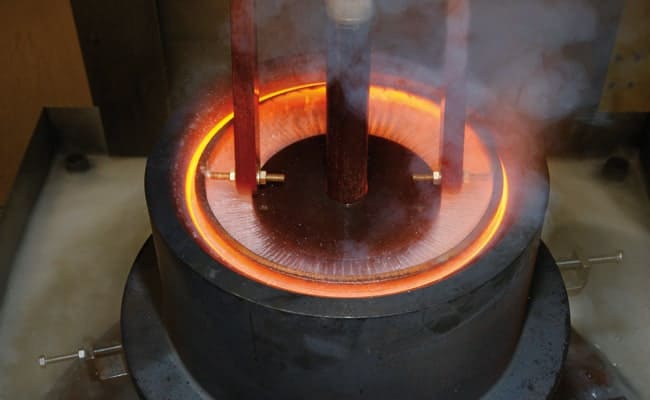 https://dw-inductionheater.com/induction-hardening-surface-process.html?feed_id=263688&_unique_id=676039f500cce
2024年12月9日星期一
2024年12月7日星期六
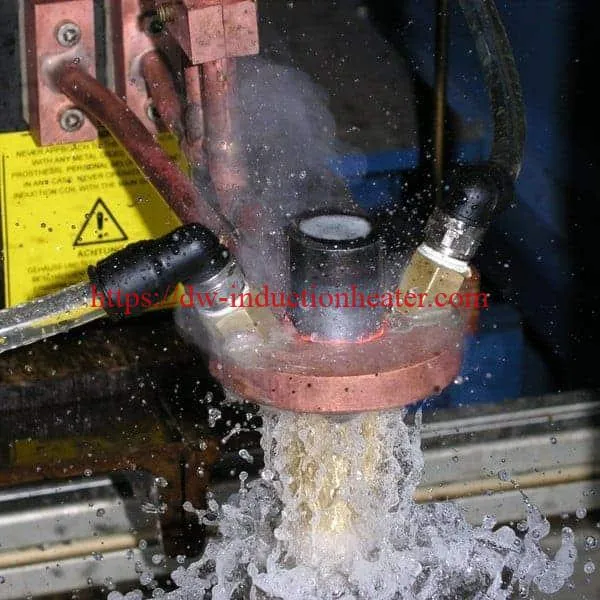
2024年12月5日星期四

2024年11月29日星期五
2024年4月4日星期四
Induction Hardening Steel Part with High Frequency Hardening Machine
Induction Hardening Steel Part with High Frequency Hardening Machine
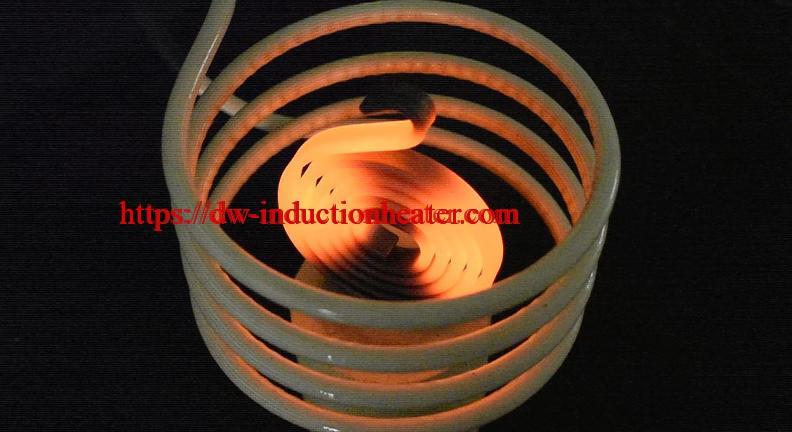
The goal of this induction heating application is to heat complex shape steel tools for hardening and integrate the process on a conveyor line to increase productivity.
 Industry: Manufacturing
Equipment: DW-UHF-10KW induction hardening machine
Materials: Steel tool parts
Power: 9.71kW
Time: 17 secs
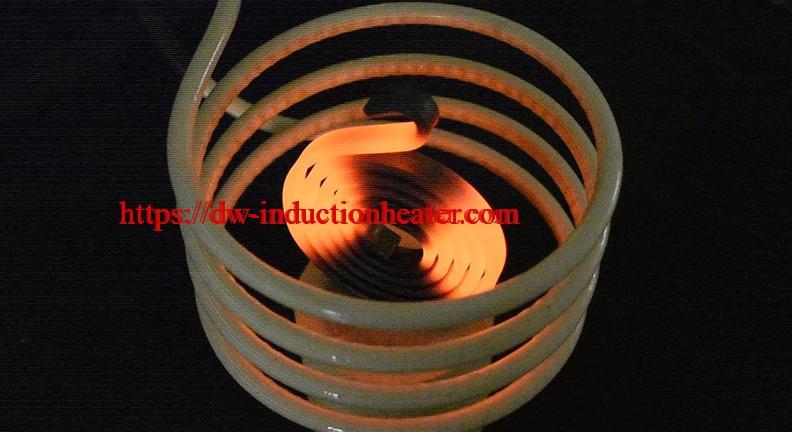
Coil: Custom designed 4 turn helical coil.
The Process:
The induction coil is designed to provide uniform heat to the entire part. The induction heat is applied to the entire part. The sample is then quenched into water. The exact time and power of the induction heat have to be determined based on the specific hardening and production requirements. The benefits of induction hardening for tools parts include fast heating, increased production rates, increased energy efficiency, automation and repeatability.
DW-UHF induction heating systems are widely used for similar induction hardening applications.
 [wpforms id="3947"]
https://dw-inductionheater.com/induction-hardening-steel-part-with-high-frequency-hardening-machine.html?feed_id=240031&_unique_id=660f097968e6a
Industry: Manufacturing
Equipment: DW-UHF-10KW induction hardening machine
Materials: Steel tool parts
Power: 9.71kW
Time: 17 secs
Coil: Custom designed 4 turn helical coil.
The Process:
The induction coil is designed to provide uniform heat to the entire part. The induction heat is applied to the entire part. The sample is then quenched into water. The exact time and power of the induction heat have to be determined based on the specific hardening and production requirements. The benefits of induction hardening for tools parts include fast heating, increased production rates, increased energy efficiency, automation and repeatability.
DW-UHF induction heating systems are widely used for similar induction hardening applications.
[wpforms id="3947"]
2024年3月1日星期五
induction hardening steel handheld stamps
induction hardening steel handheld stamps
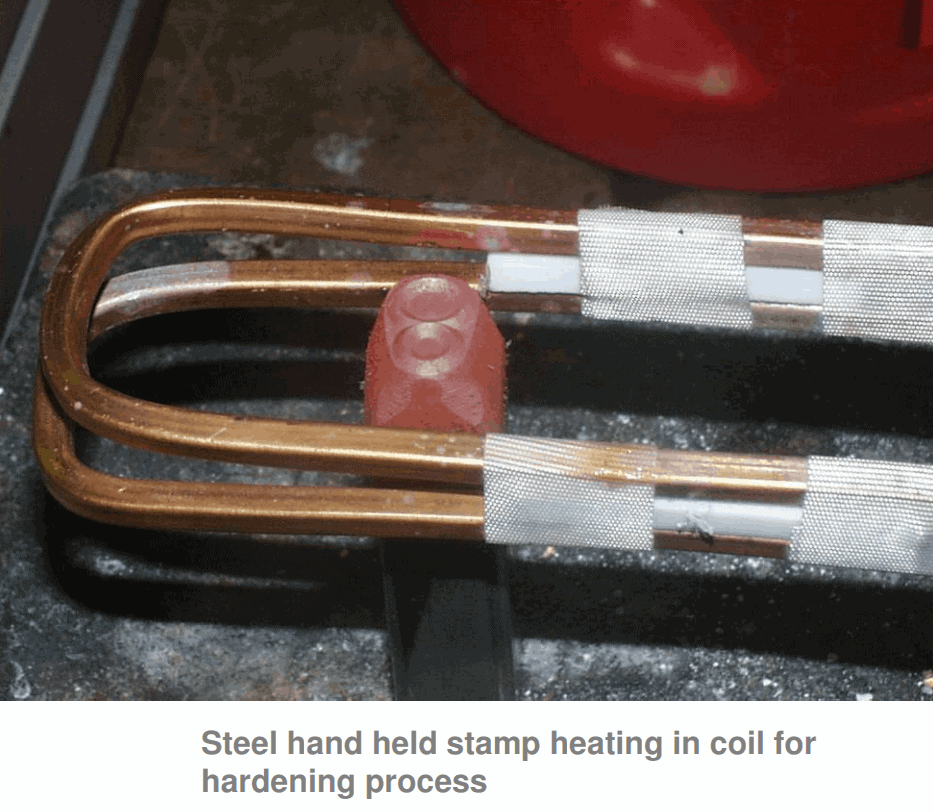
Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application.Induction Hardening Process:
A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily.
Results/Benefits
Induction heating provides:
• Faster process time and production rates
• Hands-free heating that involves no operator skill for manufacturing
• Controlled precise application of heat
 https://dw-inductionheater.com/induction-hardening-steel-handheld-stamps.html?feed_id=235397&_unique_id=65e20c4fb4fdb
2024年2月21日星期三
Induction Hardening Surface Process
Induction Hardening Surface Process Applicatons
What is induction hardening ?
Induction hardening is a form of heat treatment in which a metal part with sufficient carbon content is heated in the induction field and then rapidly cooled. This increases both the hardness and brittleness of the part. Induction heating allows you to have localized heating to a pre-determined temperature and enables you to precisely control the hardening process. Process repeatability is thus guaranteed. Usually, induction hardening is applied to metal parts which need to have great surface wear resistance, while at the same time retaining their mechanical properties. After the induction hardening process is achieved, the metal workpiece needs to be quenched in water, oil or air inorder to obtain specific properties of the surface layer.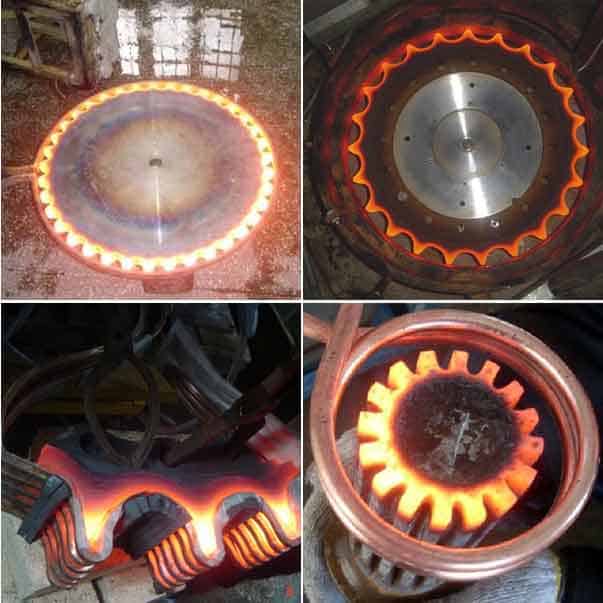 Induction hardening is a method of quickly and selectively hardening the surface of a metal part. A copper coil carrying a significant level of alternating current is placed near (not touching) the part. Heat is generated at, and near the surface by eddy current and hysteresis losses. Quench, usually water-based with an addition such as a polymer, is directed at the part or it is submerged. This transforms the structure to martensite, which is much harder than the prior structure.
A popular, modern type of induction hardening equipment is called a scanner. The part is held between centers, rotated, and passed through a progressive coil which provides both heat and quench. The quench is directed below the coil, so any given area of the part is rapidly cooled immediately following heating. Power level, dwell time, scan (feed) rate and other process variables are precisely controlled by a computer.
Case hardening process used to increase wear resistance, surface hardness and fatigue life through creation of a hardened surface layer while maintaining an unaffected core microstructure.

Processes and Industries that can benefit from induction hardening:
-
Heat-treatment
-
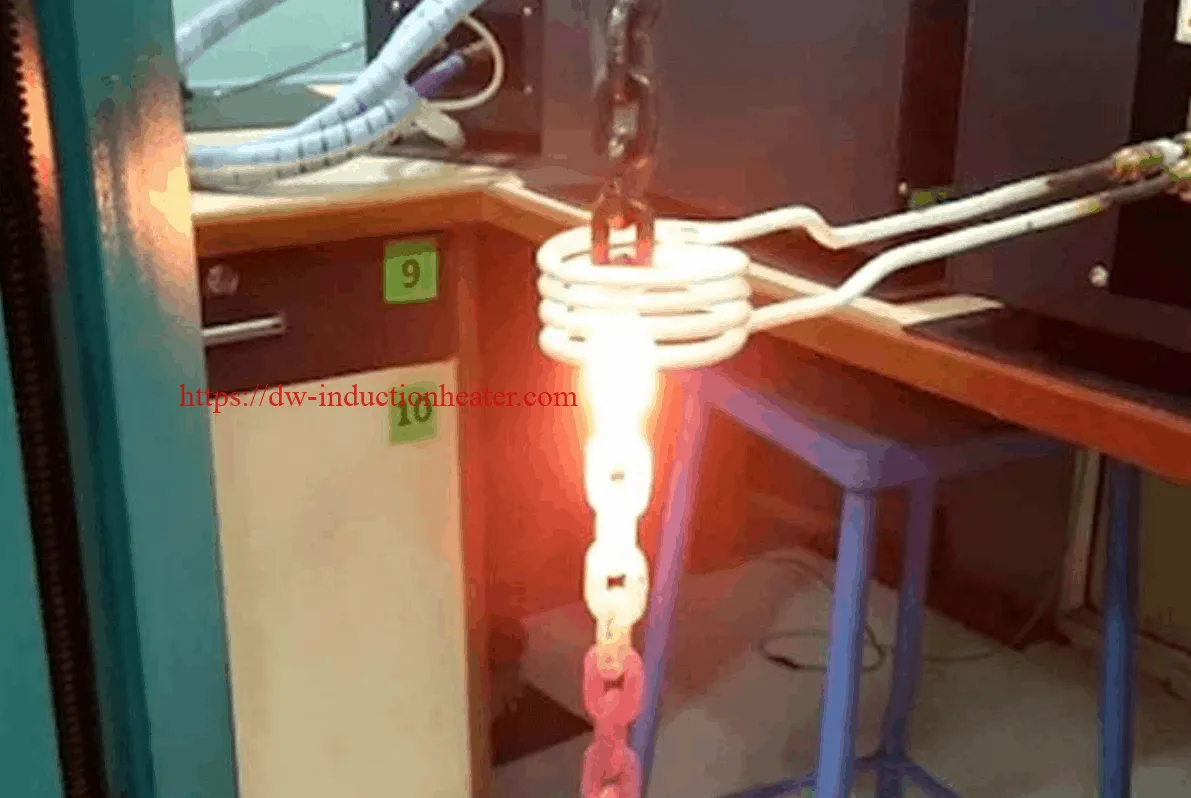
Chain hardening
-
Tube & Pipe Hardening
-
Shipbuilding
-
Aerospace
-
Railway
-
Automotive
-
Renewable energies
Benefits of Induction Hardening:
Favoured for components that are subjected to heavy loading. Induction imparts a high surface hardness with a deep case capable of handling extremely high loads. Fatigue strength is increased by the development of a soft core surrounded by an extremely tough outer layer. These properties are desirable for parts that experience torsional loading and surfaces that experience impact forces. Induction processing is performed one part at a time allowing for very predictable dimensional movement from part to part.-
Precise control over temperature and hardening depth
-
Controlled and localized heating
-
Easily integrated into production lines
-
Fast and repeatable process
-
Each workpiece can be hardened by precise optimized parameters
-
Energy-efficient process
Steel and stainless-steel components that can be hardened with induction:
Fasteners, flanges, gears, bearings, tube, inner and outer races, crankshafts, camshafts, yokes, drive shafts, output shafts, spindles, torsion bars, slewing rings, wire, valves, rock drills, etc.

Increased Wear Resistance
There is a direct correlation between hardness and wear resistance. The wear resistance of a part increases significantly with induction hardening, assuming the initial state of the material was either annealed, or treated to a softer condition.Increased Strength & Fatigue Life due to the Soft Core & Residual Compressive Stress at the Surface
The compressive stress (usually considered a positive attribute) is a result of the hardened structure near the surface occupying slightly more volume than the core and prior structure.Parts may be Tempered after Induction Hardening to Adjust Hardness Level, as desired
As with any process producing a martensitic structure, tempering will lower hardness while decreasing brittleness.Deep Case with Tough Core
Typical case depth is .030” - .120” which is deeper on average than processes such as carburizing, carbonitriding, and various forms of nitriding performed at sub-critical temperatures. For certain projects such as axels, or parts which are still useful even after much material has worn away, case depth may be up to ½ inch or greater.Selective Hardening Process with No Masking Required
Areas with post-welding or post-machining stay soft - very few other heat treat processes are able to achieve this.Relatively Minimal Distortion
Example: a shaft 1” Ø x 40” long, which has two evenly spaced journals, each 2” long requiring support of a load and wear resistance. Induction hardening is performed on just these surfaces, a total of 4” length. With a conventional method (or if we induction hardened the entire length for that matter), there would be significantly more warpage.Allows use of Low Cost Steels such as 1045
The most popular steel utilized for parts to be induction hardened is 1045. It is readily machinable, low cost, and due to a carbon content of 0.45% nominal, it may be induction hardened to 58 HRC +. It also has a relatively low risk of cracking during treatment. Other popular materials for this process are 1141/1144, 4140, 4340, ETD150, and various cast irons.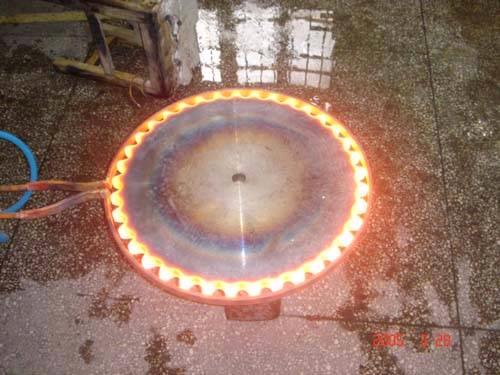
Limitations of Induction Hardening
Requires an Induction Coil and Tooling which relates to the Part’s Geometry
Since the part-to-coil coupling distance is critical to heating efficiency, the coil’s size and contour must be carefully selected. While most treaters have an arsenal of basic coils to heat round shapes such as shafts, pins, rollers etc., some projects may require a custom coil, sometimes costing thousands of dollars. On medium to high volume projects, the benefit of reduced treatment cost per part may easily offset coil cost. In other cases, the engineering benefits of the process may outweigh cost concerns. Otherwise, for low volume projects the coil and tooling cost usually makes the process impractical if a new coil must be built. The part must also be supported in some manner during the treatment. Running between centers is a popular method for shaft type parts, but in many other cases custom tooling must be utilized.Greater Likelihood of Cracking Compared to most Heat Treatment Processes
This is due to the rapid heating and quenching, also the tendency to create hot spots at features/edges such as: keyways, grooves, cross holes, threads.Distortion with Induction Hardening
Distortion levels do tend to be greater than processes such as ion or gas nitriding, due to the rapid heat/quench and resultant martensitic transformation. That being said, induction hardening may produce less distortion than conventional heat treat, particularly when it’s only applied to a selected area.Material Limitations with Induction Hardening
Since the induction hardening process does not normally involve diffusion of carbon or other elements, the material must contain enough carbon along with other elements to provide hardenability supporting martensitic transformation to the level of hardness desired. This typically means carbon is in the 0.40%+ range, producing hardness of 56 – 65 HRC. Lower carbon materials such as 8620 may be used with a resultant reduction in achievable hardness (40-45 HRC in this case). Steels such as 1008, 1010, 12L14, 1117 are typically not used due to the limited increase in hardness achievable.Induction Hardening Surface Process details
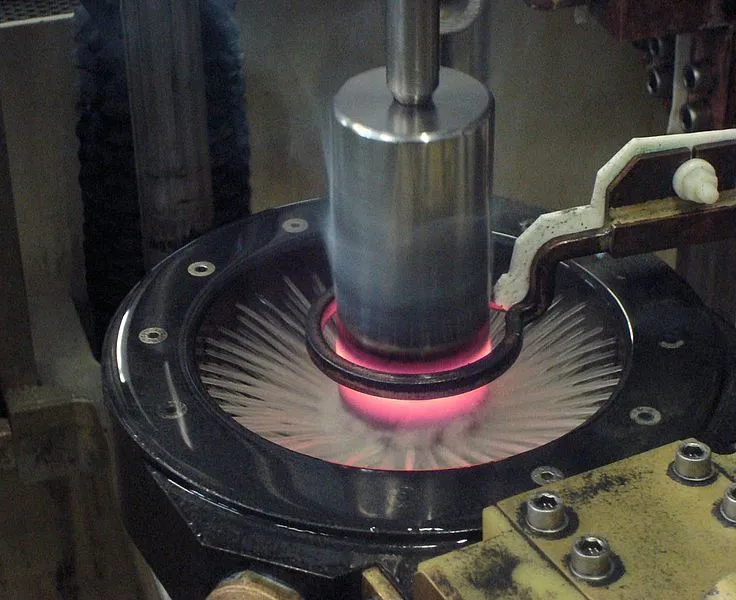
Induction hardening is a process used for the surface hardening of steel and other alloy components. The parts to be heat treated are placed inside a copper coil and then heated above their transformation temperature by applying an alternating current to the coil. The alternating current in the coil induces an alternating magnetic field within the work piece which causes the outer surface of the part to heat to a temperature above the transformation range. The components are heated by means of an alternating magnetic field to a temperature within or above the transformation range followed by immediate quenching. It is an electromagnetic process using a copper inductor coil, which is fed a current at a specific frequency and power level.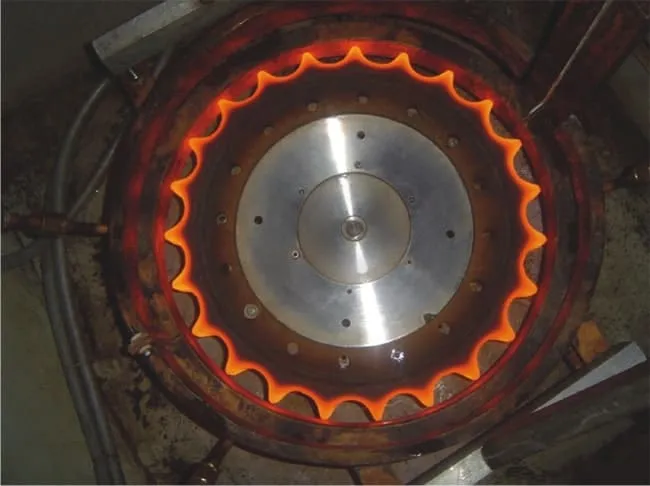 https://dw-inductionheater.com/induction-hardening-surface-process.html?feed_id=234490&_unique_id=65d69f3639d3d
2024年2月16日星期五
induction hardening process

High Frequency Induction Hardening Process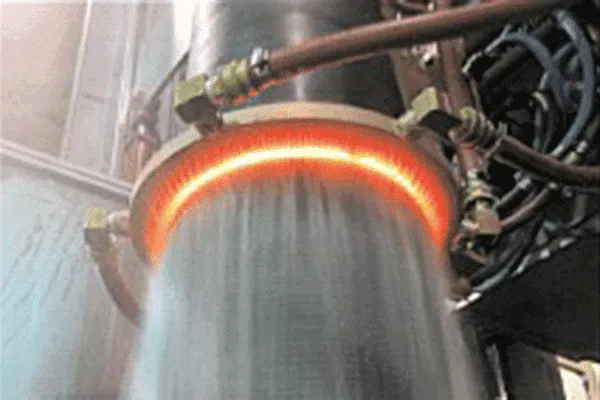
Induction hardening is used in particular for the hardening/quenching of bearing surfaces and shafts as well as intricately shaped parts where only a specific area needs to be heated.
Through the choice of the operating frequency of the induction heating system, the resulting depth of penetration is defined.
Additionally, it can be decided if the area is to be hardened in the air, with water or with a special hardening emulsion. Depending on the cooling medium, different degrees of hardness are achieved.
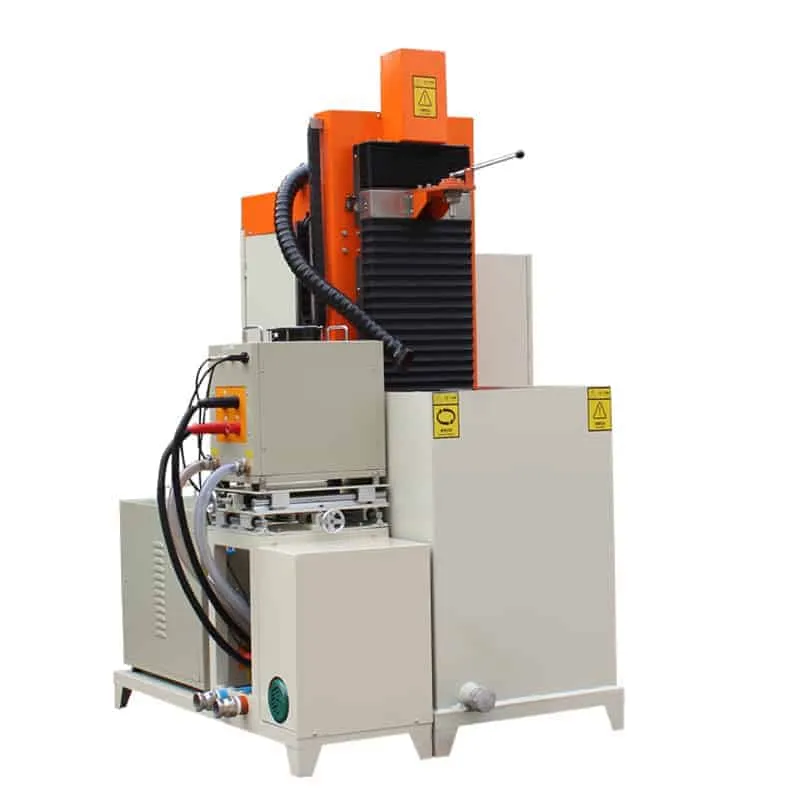 Induction hardening can be realized as a manual or automated solution. There is also the possibility to harden in a continuous process.
- Suitable for hardening and tempering of various workpieces, such as induction hardening of shafts, gears, guide rails, discs, pins, and other parts;
- It has the functions of continuous hardening, simultaneous hardening, segmented continuous hardening, and segmented simultaneous hardening;
- Use numerical control system or PLC and frequency conversion speed regulation system to realize workpiece positioning and scanning, and connect PLC and induction heating power supply to realize fully automated production.
- Vertical (hardening of shaft parts) + horizontal (hardening of gear ring parts)
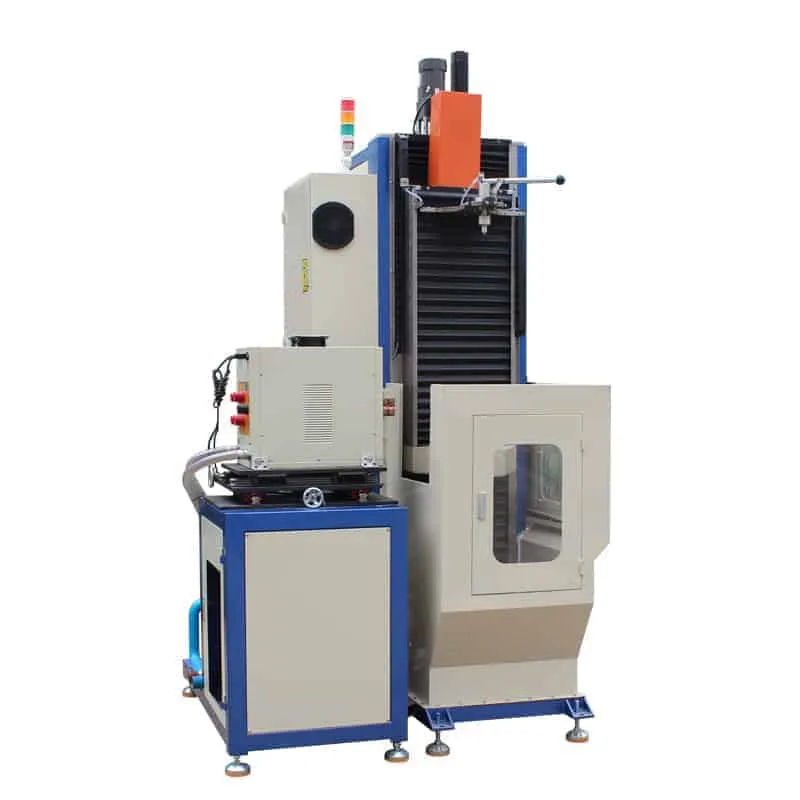 The answer is that induction is phenomenal at generating heat fast. This, in turn, means you can integrate hardening in the production process. Hardening in a furnace, on the other hand, is more time-consuming (greater heat loss) and requires moving the components either to your own furnace or to that of a subcontractor.
In-line integration of hardening reduces your lead times considerably.
You get full control over quality, delivery times and costs. There's no need to transport kilos of components back and forward, which saves energy and the environment.And last but not least, you cut down the amount of administration to a minimum.
HLQ Induction Heating Power Systems has many years of experience in inductive hardening and tempering of diverse workpieces. At the heart of each Hardening system is HLQ Induction Heating Power Systems Induction Heat Power Source, the industry's most advanced induction frequency converter. These acclaimed converters help ensure optimum hardening results—day in day out, year after year
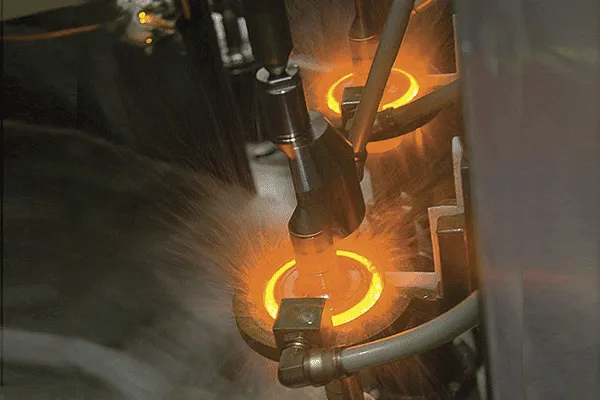 The induction hardening machine includes Vertical Scanning , Horizontal (centerless) Scanning and customized machines—and serial and/or parallel compensated induction power sources with a wide range of output power and frequencies.
- This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine.
- CNC quenching/hardening machine tool feature:
- CNC system:The high-frequency quenching machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements.
- HMI: programming type and human machine interface displays in English and Chinese.
- Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed.
- Lathe: adopt welded structure with good rust-proof functions.
- Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece.
- Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning.
- Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted.
- Electric control part: the machine tool has power-loosing protection function, has high safety and reliability.
- Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor hardening process.
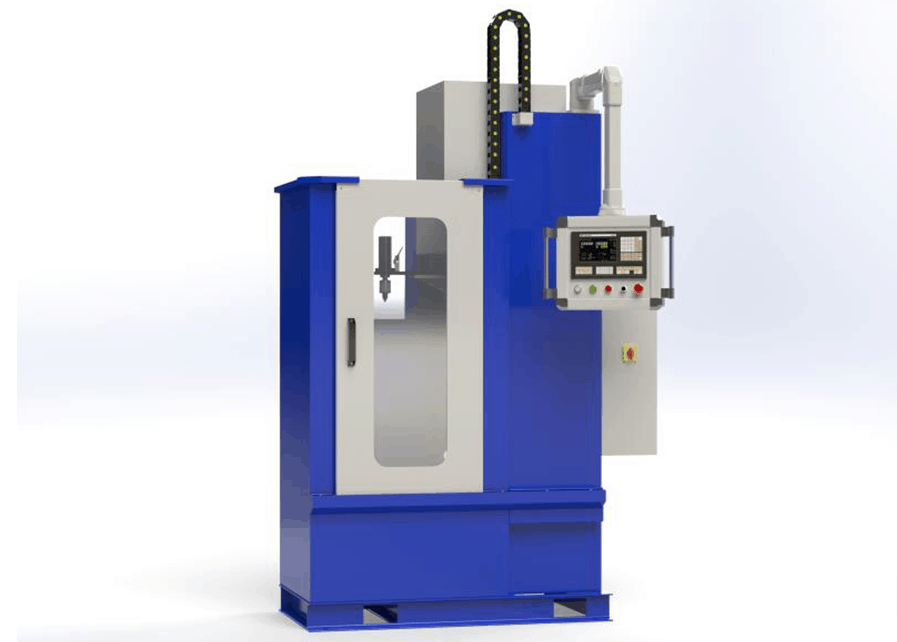 CNC vertical hardening/quenching machine tool
This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine.
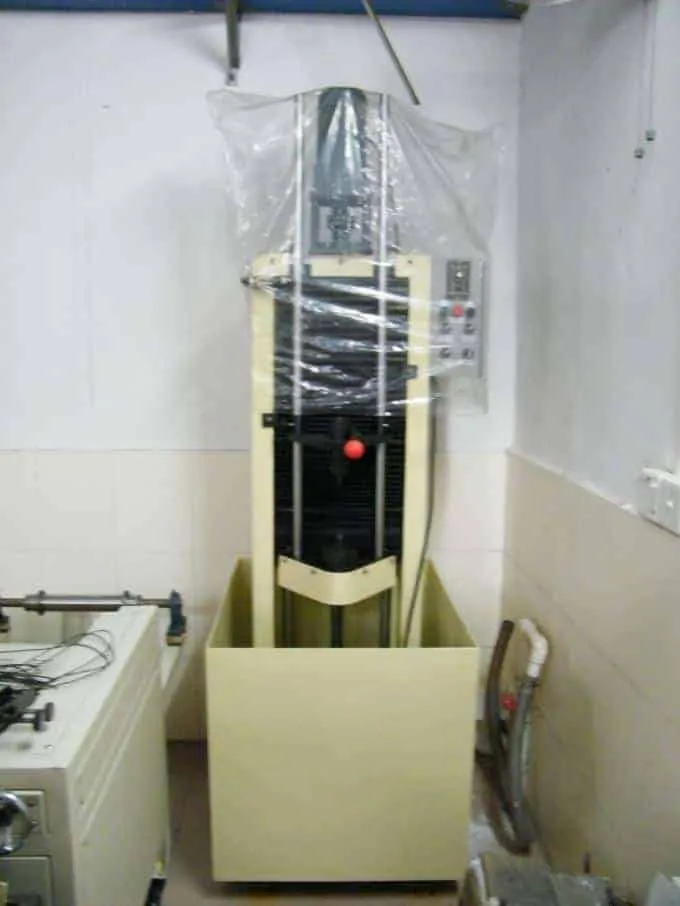 According to the different of workpiece, there are vertical type, horizontal type,closed type, customized type, etc.
1.Standard SK-500/1000/1200/1500 workpiece moving type For shafts, discs, pins and gears hardening
2.SK-2000/2500/3000/4000 Transformer moving type , Used for heating length more than 1500mm shaft
3.Closed type : Customized for big shaft ,More clean work environment.
4.Horizontal hardening machine tool
SK-500/1000/1200/1500/2000/2500/3000/4000 Used for smooth shaft
5.Customized type
Technical Parameter
| Model | SK-500 | SK-1000 | SK-1200 | SK-1500 |
| Max heating length(mm) | 500 | 1000 | 1200 | 1500 |
| Max heating diameter(mm) | 500 | 500 | 600 | 600 |
| Max holding length(mm) | 600 | 1100 | 1300 | 1600 |
| Max weight of workpiece(Kg) | 100 | 100 | 100 | 100 |
| Workpiece rotation speed(r/min) | 0-300 | 0-300 | 0-300 | 0-300 |
| workpiece moving speed(mm/min) | 6-3000 | 6-3000 | 6-3000 | 6-3000 |
| Cooling method | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling |
| Input voltage | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz |
| Motor power | 1.1KW | 1.1KW | 1.2KW | 1.5KW |
| Dimension LxWxH (mm) | 1600 x800 x2000 | 1600 x800 x2400 | 1900 x900 x2900 | 1900 x900 x3200 |
| weight(Kg) | 800 | 900 | 1100 | 1200 |
| Model | SK-2000 | SK-2500 | SK-3000 | SK-4000 |
| Max heating length(mm) | 2000 | 2500 | 3000 | 4000 |
| Max heating diameter(mm) | 600 | 600 | 600 | 600 |
| Max holding length(mm) | 2000 | 2500 | 3000 | 4000 |
| Max weight of workpiece(Kg) | 800 | 1000 | 1200 | 1500 |
| workpiece rotation speed(r/min) | 0-300 | 0-300 | 0-300 | 0-300 |
| workpiece moving speed(mm/min) | 6-3000 | 6-3000 | 6-3000 | 6-3000 |
| Cooling method | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling | Hydrojet cooling |
| Input voltage | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz | 3P 380V 50Hz |
| Motor power | 2KW | 2.2KW | 2.5KW | 3KW |
| Dimension LxWxH (mm) | 1900 x900 x2400 | 1900 x900 x2900 | 1900 x900 x3400 | 1900 x900 x4300 |
| weight(Kg) | 1200 | 1300 | 1400 | 1500 |
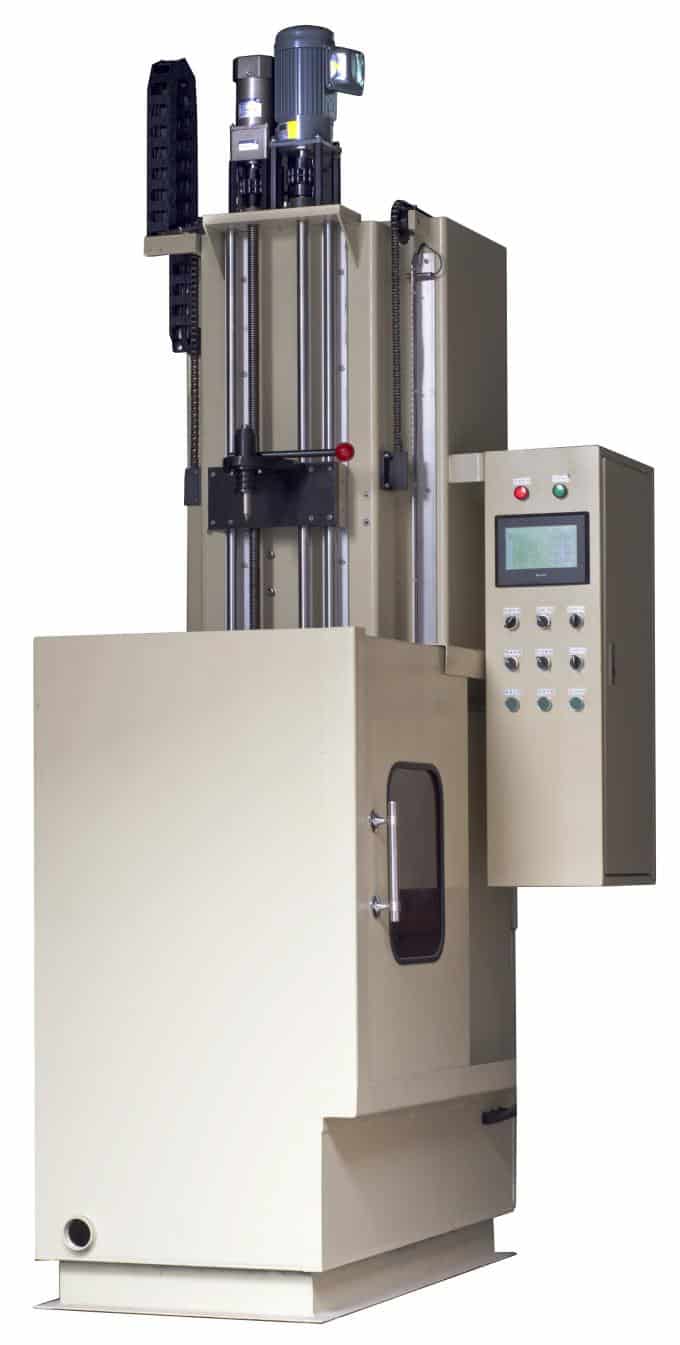 CNC hardening/quenching machine tool feature:
1.CNC system:The high-frequency hardening machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements.
2.HMI: programming type and human machine interface displays in English and Chinese.
3.Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed.
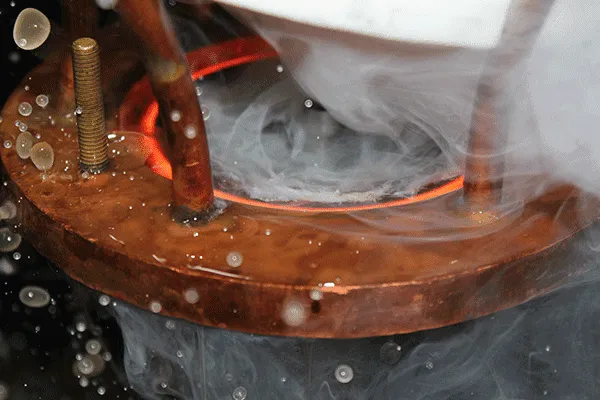 4.Lathe: adopt welded structure with good rust-proof functions.
5.Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece.
6.Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning.
7.Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted.
8.Electric control part: the machine tool has power-loosing protection function, has high safety and reliability.
9.Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor induction hardening process.
[caption id="attachment_6788" align="alignnone" width="600"] [/caption]
https://dw-inductionheater.com/induction-hardening-process.html?feed_id=234193&_unique_id=65d032023f48a
2024年2月10日星期六
Induction Hardening and tempering
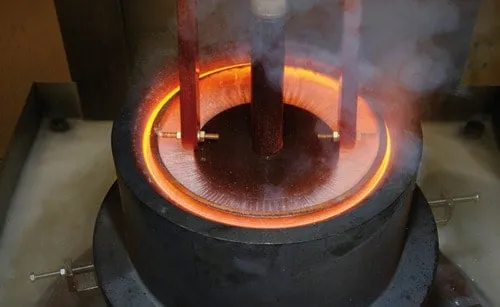
Induction Hardening and tempering Surface Process
Induction Hardening
Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel.
To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc.
There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc.
The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).
Induction heating advantages:
- It treats a specific part of the piece (hardening profile)
- Frequency Control and heating times
- Cooling control
- Energy saving
- No physical contact
- Control and located heat
- Can be integrated in production lines
- Increase performance and saves space
- Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
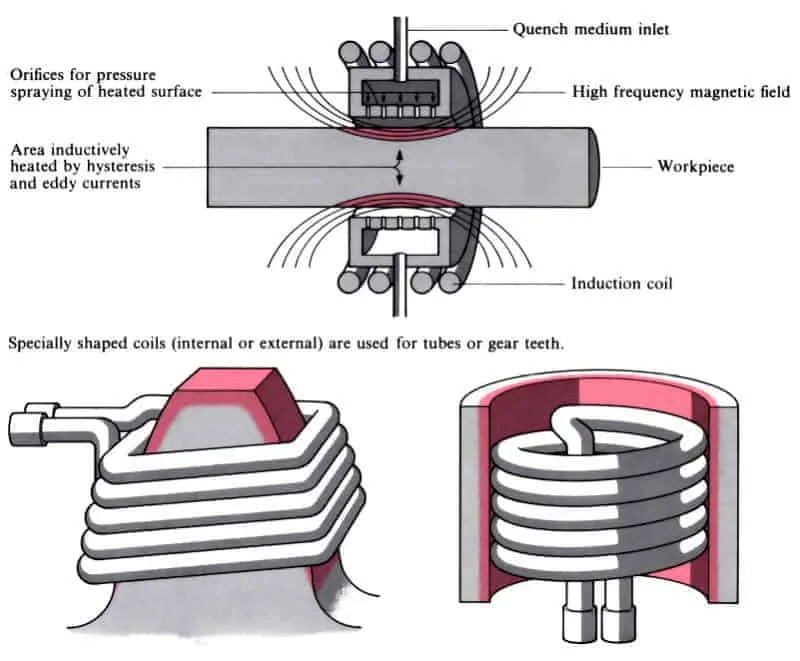
- Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
Induction Tempering
Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.Induction heating advantages:
- Shorter times in the process
- Temperature control
- Integration in production lines
- Energy saving
- Immediate availability of parts
- Saves floor space
- Improved environmental conditions
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.