显示标签为“highfrequencyquenching”的博文。显示所有博文

2024年2月16日星期五

induction hardening process

High Frequency Induction Hardening  Process

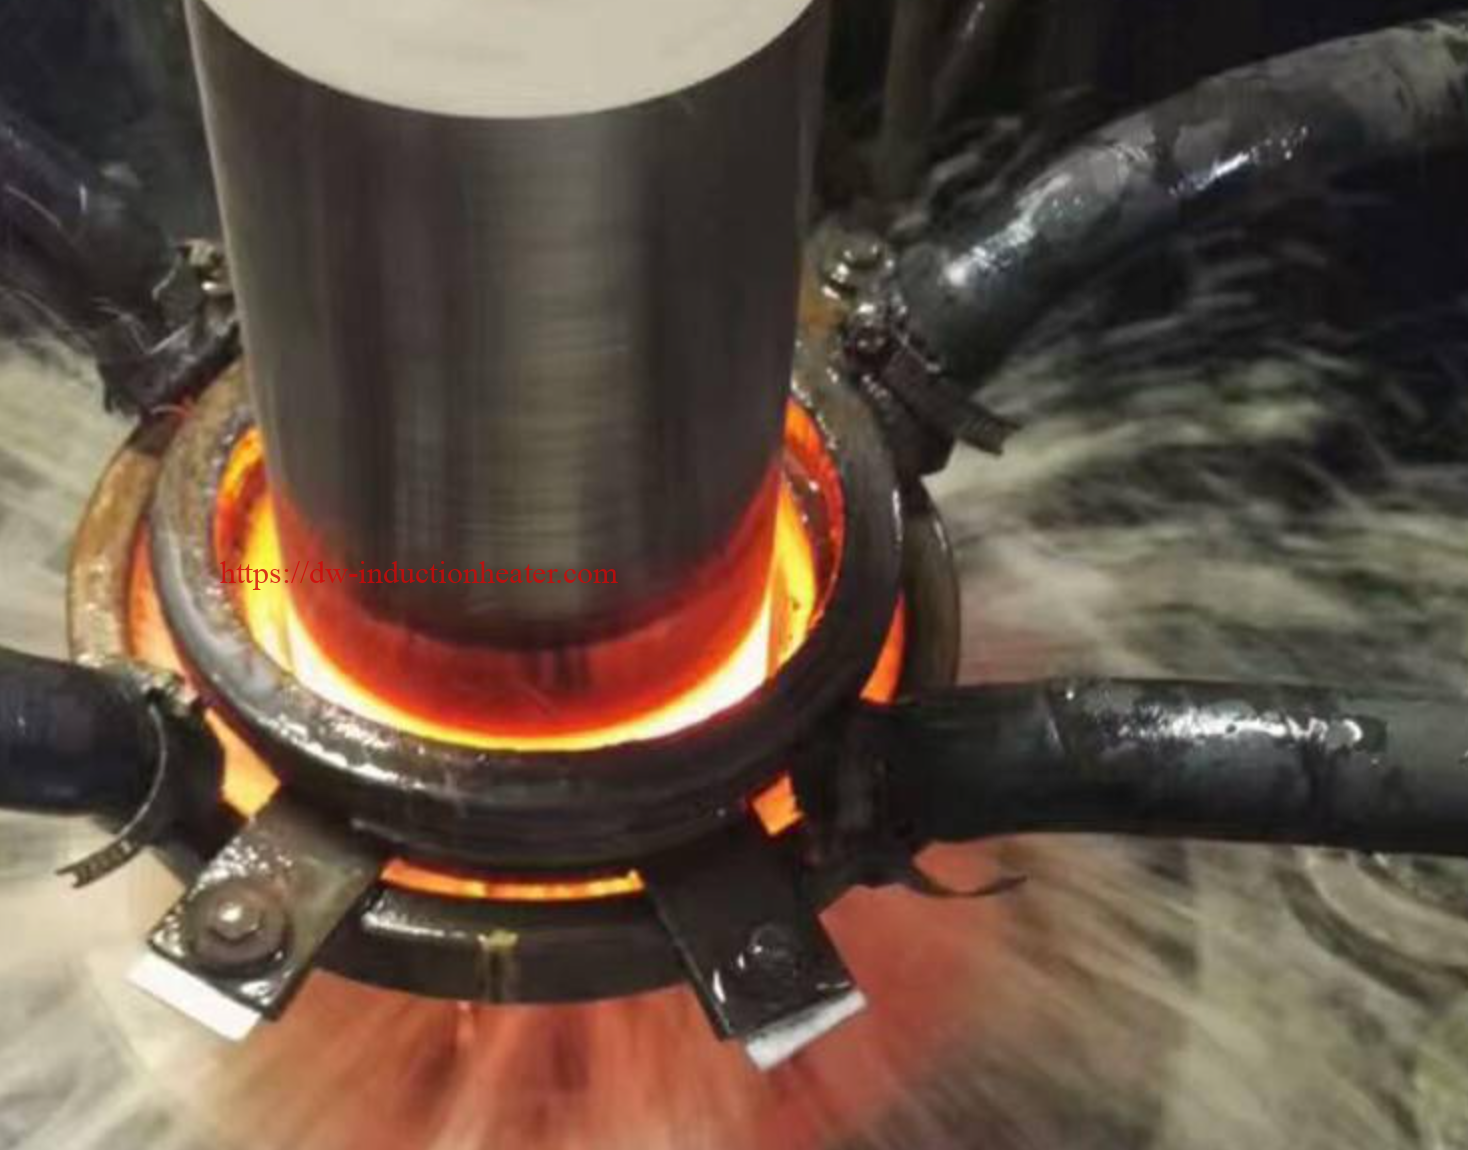
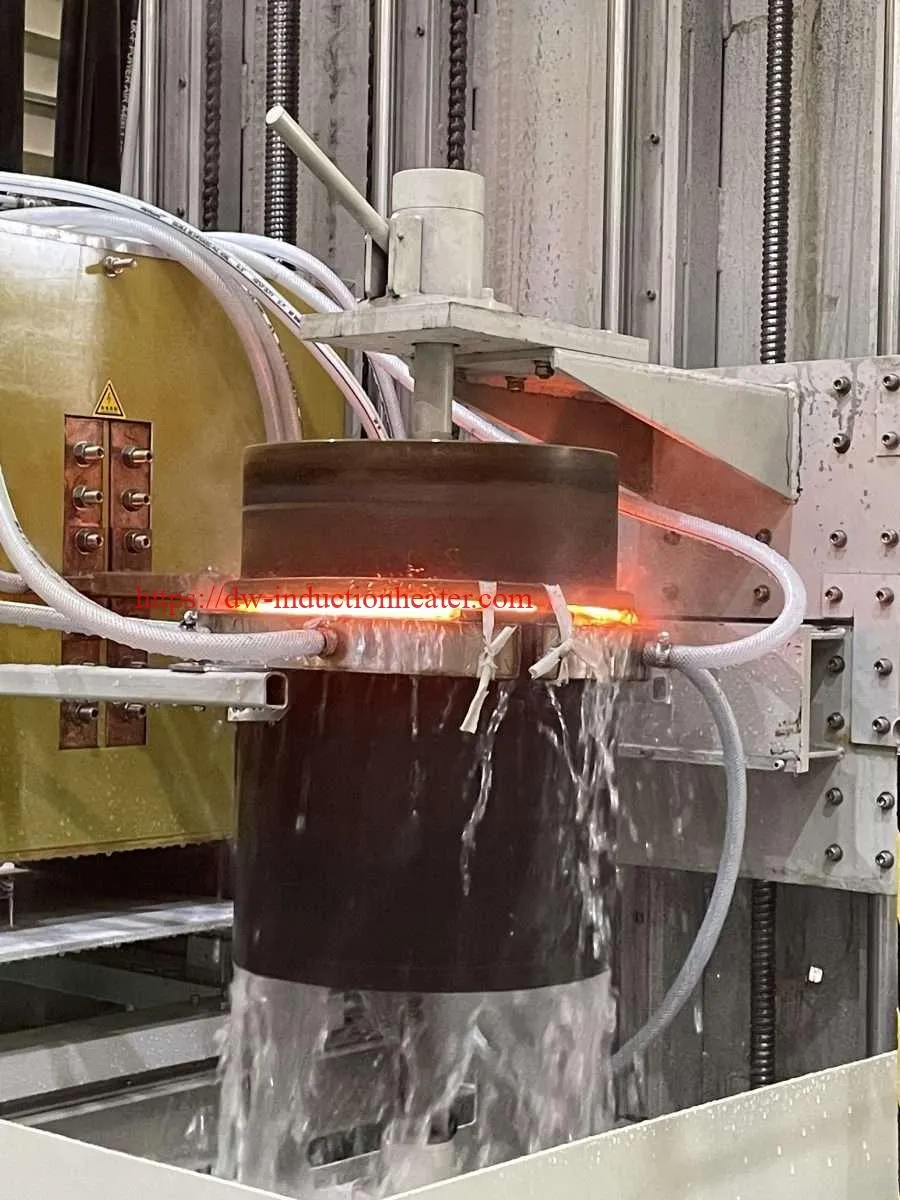
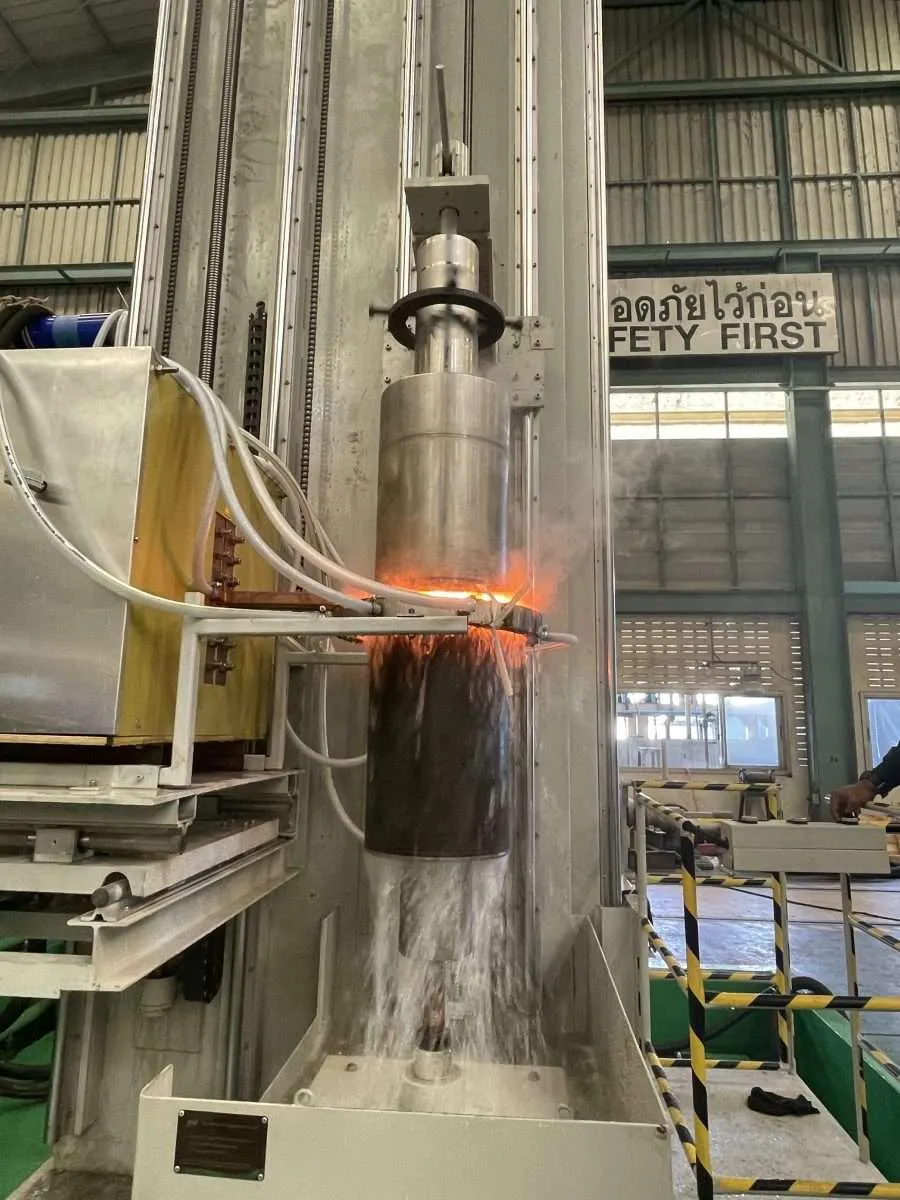
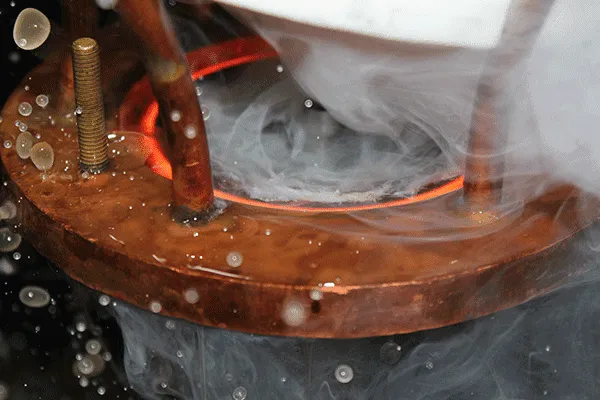
Induction hardening is used in particular for the hardening/quenching of bearing surfaces and shafts as well as intricately shaped parts where only a specific area needs to be heated. Through the choice of the operating frequency of the induction heating system, the resulting depth of penetration is defined. Additionally, it can be decided if the area is to be hardened in the air, with water or with a special hardening emulsion. Depending on the cooling medium, different degrees of hardness are achieved. Induction hardening can be realized as a manual or automated solution. There is also the possibility to harden in a continuous process.
  • Suitable for hardening and tempering of various workpieces, such as induction hardening of shafts, gears, guide rails, discs, pins, and other parts;
  • It has the functions of continuous hardening, simultaneous hardening, segmented continuous hardening, and segmented simultaneous hardening;
  • Use numerical control system or PLC and frequency conversion speed regulation system to realize workpiece positioning and scanning, and connect PLC and induction heating power supply to realize fully automated production.
  • Vertical (hardening of shaft parts) + horizontal (hardening of gear ring parts)
Hardening is one of HLQ induction heating power systems's main application areas. Hundreds of our hardening solutions are at work around the world—many of them within the automotive industry. The main benefit of induction heating for hardening is that it takes just a few seconds. In a furnace, the same process can take hours or even days. How is that possible? The answer is that induction is phenomenal at generating heat fast. This, in turn, means you can integrate hardening in the production process. Hardening in a furnace, on the other hand, is more time-consuming (greater heat loss) and requires moving the components either to your own furnace or to that of a subcontractor. In-line integration of hardening reduces your lead times considerably. You get full control over quality, delivery times and costs. There's no need to transport kilos of components back and forward, which saves energy and the environment.And last but not least, you cut down the amount of administration to a minimum. HLQ Induction Heating Power Systems has many years of experience in inductive hardening and tempering of diverse workpieces. At the heart of each Hardening system is HLQ Induction Heating Power Systems Induction Heat Power Source, the industry's most advanced induction frequency converter. These acclaimed converters help ensure optimum hardening results—day in day out, year after year The induction hardening machine includes Vertical Scanning , Horizontal (centerless) Scanning and customized machines—and serial and/or parallel compensated induction power sources with a wide range of output power and frequencies.
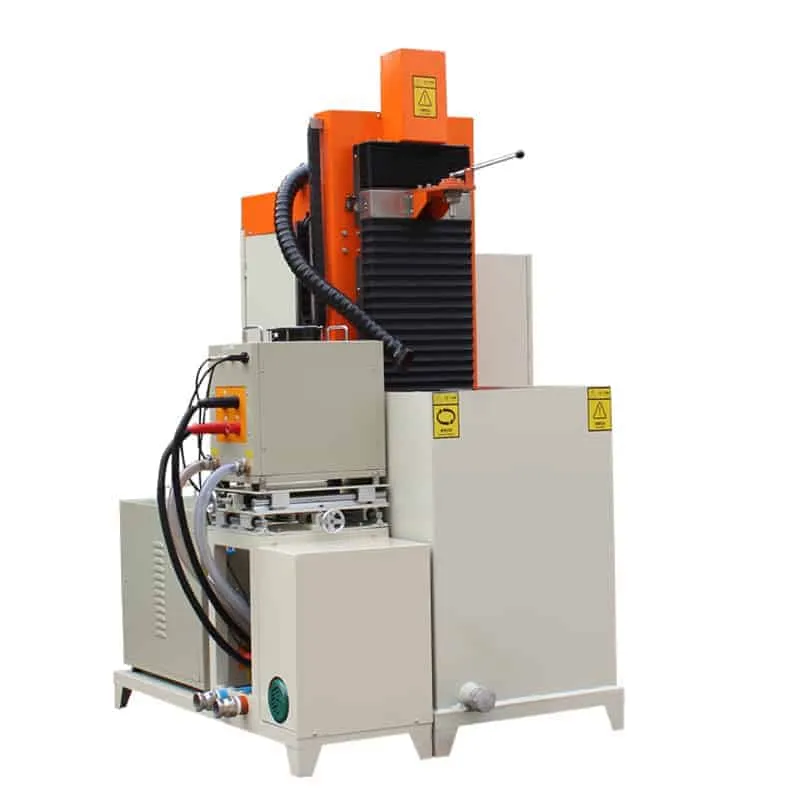
  • This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine.
  • CNC quenching/hardening machine tool feature:
  • CNC system:The high-frequency quenching machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements.
  • HMI: programming type and human machine interface displays in English and Chinese.
  • Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed.
  • Lathe: adopt welded structure with good rust-proof functions.
  • Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece.
  • Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning.
  • Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted.
  • Electric control part: the machine tool has power-loosing protection function, has high safety and reliability.
  • Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor hardening process.
CNC vertical hardening/quenching machine tool This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine. According to the different of workpiece, there are vertical type, horizontal type,closed type, customized type, etc. 1.Standard SK-500/1000/1200/1500 workpiece moving type For shafts, discs, pins and gears hardening 2.SK-2000/2500/3000/4000 Transformer moving type , Used for heating length more than 1500mm shaft 3.Closed type : Customized for big shaft ,More clean work environment. 4.Horizontal hardening machine tool SK-500/1000/1200/1500/2000/2500/3000/4000  Used for smooth shaft 5.Customized type Technical Parameter
Model SK-500 SK-1000 SK-1200 SK-1500
Max heating length(mm) 500 1000 1200 1500
Max heating diameter(mm) 500 500 600 600
Max holding length(mm) 600 1100 1300 1600
Max weight of workpiece(Kg) 100 100 100 100
Workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 1.1KW 1.1KW 1.2KW 1.5KW
Dimension LxWxH (mm) 1600 x800 x2000 1600 x800 x2400 1900 x900 x2900 1900 x900 x3200
weight(Kg) 800 900 1100 1200
 
Model SK-2000 SK-2500 SK-3000 SK-4000
Max heating length(mm) 2000 2500 3000 4000
Max heating diameter(mm) 600 600 600 600
Max holding length(mm) 2000 2500 3000 4000
Max weight of workpiece(Kg) 800 1000 1200 1500
workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 2KW 2.2KW 2.5KW 3KW
Dimension LxWxH (mm) 1900 x900 x2400 1900 x900 x2900 1900 x900 x3400 1900 x900 x4300
weight(Kg) 1200 1300 1400 1500
CNC hardening/quenching machine tool feature: 1.CNC system:The high-frequency hardening machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements. 2.HMI: programming type and human machine interface displays in English and Chinese. 3.Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed. 4.Lathe: adopt welded structure with good rust-proof functions. 5.Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece. 6.Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning. 7.Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted. 8.Electric control part: the machine tool has power-loosing protection function, has high safety and reliability. 9.Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor induction hardening process.     [caption id="attachment_6788" align="alignnone" width="600"]  [/caption] https://dw-inductionheater.com/induction-hardening-process.html?feed_id=234193&_unique_id=65d032023f48a

2024年1月9日星期二

The Benefits of Induction Quenching Surface Process for Manufacturing

The Benefits of Induction Quenching Surface Process for Manufacturing.

Manufacturing is an industry that thrives on innovation and efficiency. When it comes to surface treatment processes, induction quenching is quickly becoming the method of choice for a variety of manufacturing applications. Unlike traditional heat treatment methods, induction quenching offers several unique benefits such as high production rates, increased precision, and improved part quality. In this article, we'll look at some of the key benefits of induction quenching surface process and why it's quickly becoming a popular choice for manufacturers across a range of industries. So, if you're looking to improve the efficiency and quality of your manufacturing process, or you're simply interested in the latest surface treatment techniques, keep reading to learn more about the benefits of induction quenching.

1. What is Induction Quenching Surface Process?

Induction quenching surface process is a type of surface hardening process that uses electrical induction to rapidly heat and cool metal parts. This process is commonly used in manufacturing because it offers a number of benefits over other types of surface hardening processes. In induction quenching, an induction coil is used to generate a high-frequency magnetic field that rapidly heats the metal part. Once the part is heated to the desired temperature, a quenching medium, such as water or oil, is used to rapidly cool the part. This rapid heating and cooling process causes the surface of the metal part to harden, which makes it more wear-resistant and less likely to crack or deform under stress. Induction quenching is also a very precise process that allows for accurate control of the surface hardness of the metal part. This precision makes it an ideal process for manufacturing parts that require high levels of wear resistance, such as gears, shafts, and bearings. Additionally, induction quenching is a very efficient process that can be completed quickly, which makes it ideal for high-volume production environments. Overall, induction quenching is a highly effective surface hardening process that offers many benefits for manufacturers looking to produce high-quality, durable metal parts.

2. Benefits of Induction Quenching Surface Process

Induction quenching surface process is a highly efficient manufacturing technique that offers numerous benefits over traditional surface treatment methods. One of the most significant benefits of this process is that it is incredibly fast and efficient. With the ability to deliver heat at a rate of up to 25,000 degrees per second, induction quenching can heat treat parts in seconds, instead of hours or days, as is the case with other heat treatment methods. This means that manufacturers can produce more parts in less time, without sacrificing quality or reliability. Another significant benefit of induction quenching surface process is that it produces a superior product.

The process uses localized heating, which means that the heat is only applied where it is needed, resulting in less distortion, less scrap, and fewer defects. This makes induction quenching a great choice for manufacturers who are looking to produce high-quality parts quickly and efficiently. Induction quenching surface process is also a more environmentally-friendly option than other surface treatment methods. Since the process uses less energy and generates less waste, it is a more sustainable option for manufacturers who are looking to reduce their carbon footprint and be more environmentally responsible. In addition to these benefits, induction quenching surface process also offers a more controlled and precise heat treatment. The process allows manufacturers to control the depth of the heat treatment and the hardness achieved, which is a significant advantage over other surface treatment methods. With this level of control, manufacturers can produce parts that are exact in their specifications and meet the needs of their customers. Overall, the benefits of induction quenching surface process make it an ideal choice for manufacturers who are looking to improve their production processes, reduce waste, and produce high-quality parts quickly and efficiently.

3. Applications of Induction Quenching Surface Process in Manufacturing

Induction quenching is a surface hardening process that uses induction heating to heat the surface of a material to a high temperature and then rapidly cools it down by quenching it with water, oil or a polymer solution. This process creates a surface that is harder, more wear-resistant, and more durable than the original material. Induction quenching has many applications in manufacturing, including the hardening of gears, shafts, and bearings. It is also used in the automotive industry to harden engine components, such as camshafts, rocker arms, and valve lifters. The aerospace industry uses induction quenching to harden turbine components, and the energy industry uses it to harden drilling and mining components. The medical industry also uses induction quenching to harden surgical instruments and dental tools.

The process is also used in the production of cutting tools and molds. Induction quenching can produce a surface that is up to 10 times harder than the original material, making it an ideal choice for manufacturing applications where durability and wear resistance are critical. Additionally, the process is efficient and cost-effective, making it an attractive option for many manufacturers.

4. Conclusion.

Induction quenching surface process is a type of heat treatment process that is used to harden metal parts. The induction process involves passing a high-frequency electrical current through a coil, which creates a magnetic field. The metal part is then placed inside the coil, where the magnetic field induces an electrical current in the metal. This current causes the metal to heat up quickly, which then allows for the surface of the metal to be rapidly quenched by an appropriate cooling medium. This process creates a hardened surface that is more resistant to wear and tear, making it ideal for use in a wide variety of industrial applications.

  https://dw-inductionheater.com/the-benefits-of-induction-quenching-surface-process-for-manufacturing.html?feed_id=231850&_unique_id=659e350253175

2024年1月2日星期二

CNC Induction Hardening Surface of Shafts, Rollers, Pins

Ultimate Guide to Induction Hardening: Enhancing the Surface of Shafts, Rollers, and Pins.

induction hardening processInduction hardening is a specialized heat treatment process that can significantly enhance the surface properties of various components, including shafts, rollers, and pins. This advanced technique involves selectively heating the surface of the material using high-frequency induction coils and then rapidly quenching it to achieve optimal hardness and wear resistance. In this comprehensive guide, we will explore the intricacies of induction hardening, from the science behind the process to the benefits it offers in terms of improving the durability and performance of these crucial industrial components. Whether you are a manufacturer looking to optimize your production processes or simply curious about the fascinating world of heat treatments, this article will provide you with the ultimate insights into induction hardening. [embed]https://youtu.be/fD89qj5t9Ig[/embed] 1. What is induction hardening? Induction hardening is a heat treatment process used to enhance the surface properties of various components such as shafts, rollers, and pins. It involves heating the surface of the component using high-frequency electrical currents, which are generated by an induction coil. The intense heat generated quickly raises the temperature of the surface, while the core remains relatively cool. This rapid heating and cooling process results in a hardened surface with improved wear resistance, hardness, and strength. The induction hardening process begins by positioning the component within the induction coil. The coil is connected to a power source, which produces an alternating current that flows through the coil, creating a magnetic field. When the component is placed within this magnetic field, eddy currents are induced in its surface. These eddy currents generate heat due to the resistance of the material. As the surface temperature increases, it reaches the austenitizing temperature, which is the critical temperature required for transformation to occur. At this point, the heat is quickly removed, usually through the use of a water spray or quenching medium. The rapid cooling causes the austenite to transform into martensite, a hard and brittle phase that contributes to the enhanced surface properties. Induction hardening offers several advantages over traditional hardening methods. It is a highly localized process, focusing only on the areas that require hardening, which minimizes distortion and reduces energy consumption. The precise control over the heating and cooling process allows for customization of hardness profiles according to specific requirements. Additionally, induction hardening is a fast and efficient process that can be easily automated for high-volume production. In summary, induction hardening is a specialized heat treatment technique that selectively improves the surface properties of components like shafts, rollers, and pins. By harnessing the power of high-frequency electrical currents, this process provides enhanced wear resistance, hardness, and strength, making it a valuable method for enhancing the performance and durability of various industrial components. 2. The science behind induction hardening Induction hardening is a fascinating process that involves enhancing the surface of shafts, rollers, and pins to increase their durability and strength. To understand the science behind induction hardening, we must first delve into the principles of induction heating. The process of induction heating utilizes an alternating magnetic field generated by an induction coil. When an electric current passes through the coil, it generates the magnetic field, which creates eddy currents within the workpiece. These eddy currents produce heat due to the resistance of the material, leading to localized heating. During induction hardening, the workpiece is rapidly heated to a specific temperature above its transformation point, known as the austenitizing temperature. This temperature varies depending on the material being hardened. Once the desired temperature is reached, the workpiece is quenched, typically using water or oil, to rapidly cool it down. The science behind induction hardening lies in the transformation of the material's microstructure. By rapidly heating and cooling the surface, the material undergoes a phase change from its initial state to a hardened state. This phase change results in the formation of martensite, a hard and brittle structure that significantly enhances the surface's mechanical properties. The depth of hardened layer, known as the case depth, can be controlled by adjusting various parameters such as the frequency of the magnetic field, power input, and quenching medium. These variables directly influence the heating rate, cooling rate, and ultimately, the final hardness and wear resistance of the hardened surface. It's important to note that induction hardening is a highly precise process, offering excellent control over localized heating. By selectively heating only the desired areas, such as shafts, rollers, and pins, manufacturers can achieve optimal hardness and wear resistance while maintaining the core's toughness and ductility. In conclusion, the science behind induction hardening lies in the principles of induction heating, the transformation of microstructure, and the control of various parameters. This process enables the enhancement of the surface properties of shafts, rollers, and pins, resulting in improved durability and performance in various industrial applications. 3. Benefits of induction hardening for shafts, rollers, and pins Induction hardening is a widely used heat treatment process that offers numerous benefits for enhancing the surface of shafts, rollers, and pins. The primary advantage of induction hardening is its ability to selectively heat treat specific areas, resulting in a hardened surface while maintaining the core's desired properties. This process improves the durability and wear resistance of these components, making them ideal for heavy-duty applications. One of the key benefits of induction hardening is the significant increase in hardness achieved on the surface of shafts, rollers, and pins. This enhanced hardness helps to prevent surface damage, such as abrasion and deformation, extending the lifespan of the components. The hardened surface also provides improved resistance to fatigue, ensuring that these parts can withstand high-stress conditions without compromising their performance. In addition to hardness, induction hardening improves the overall strength of shafts, rollers, and pins. The localized heating and rapid quenching process during induction hardening results in a transformation of the microstructure, leading to increased tensile strength and toughness. This makes the components more resistant to bending, breaking, and deformation, enhancing their reliability and longevity. Another significant advantage of induction hardening is its efficiency and speed. The process is known for its rapid heating and quenching cycles, enabling high production rates and cost-effective manufacturing. Compared to traditional methods such as case hardening or through-hardening, induction hardening offers shorter cycle times, reducing energy consumption and improving productivity. Furthermore, induction hardening allows for precise control over the hardened depth. By adjusting the power and frequency of the induction heating, manufacturers can achieve the desired hardened depth specific to their application requirements. This flexibility ensures that the surface hardness is optimized while maintaining the appropriate core properties. Overall, the benefits of induction hardening make it an ideal choice for enhancing the surface of shafts, rollers, and pins. From increased hardness and strength to improved durability and efficiency, induction hardening offers manufacturers a reliable and cost-effective method to enhance the performance and longevity of these critical components in various industries. 4. The induction hardening process explained Induction hardening is a widely used technique in the manufacturing industry to enhance the surface properties of various components, such as shafts, rollers, and pins. This process involves heating the selected areas of the component using high-frequency induction heating, followed by rapid quenching to achieve a hardened surface layer. The induction hardening process begins with the positioning of the component in the induction coil, which generates a high-frequency alternating magnetic field. This magnetic field induces eddy currents in the workpiece, leading to rapid and localized heating of the surface. The depth of the hardened layer can be controlled by adjusting the frequency, power, and time of the induction heating. As the surface temperature rises above the critical transformation temperature, the austenite phase is formed. This phase is then rapidly quenched using a suitable medium, such as water or oil, to transform it into martensite. The martensitic structure provides excellent hardness, wear resistance, and strength to the treated surface, while the core of the component retains its original properties. One of the significant advantages of induction hardening is its ability to achieve precise and controlled hardening patterns. By carefully designing the shape and configuration of the induction coil, specific areas of the component can be targeted for hardening. This selective heating minimizes distortion and ensures that only the required surface areas are hardened, preserving the desired mechanical properties of the core. Induction hardening is highly efficient and can be integrated into automated production lines, ensuring consistent and repeatable results. It offers several benefits over other surface hardening methods, such as flame hardening or carburizing, including shorter heating times, reduced energy consumption, and minimal material distortion. However, it is crucial to note that the induction hardening process requires careful process design and parameter optimization to ensure optimal results. Factors such as the component material, geometry, and desired hardening depth must be taken into consideration. In conclusion, induction hardening is a versatile and effective method for enhancing the surface properties of shafts, rollers, and pins. Its ability to provide localized and controlled hardening makes it ideal for various industrial applications where wear resistance, hardness, and strength are essential. By understanding the induction hardening process, manufacturers can harness its benefits to produce high-quality and durable components. 5. Induction Hardening  Power  Supplier
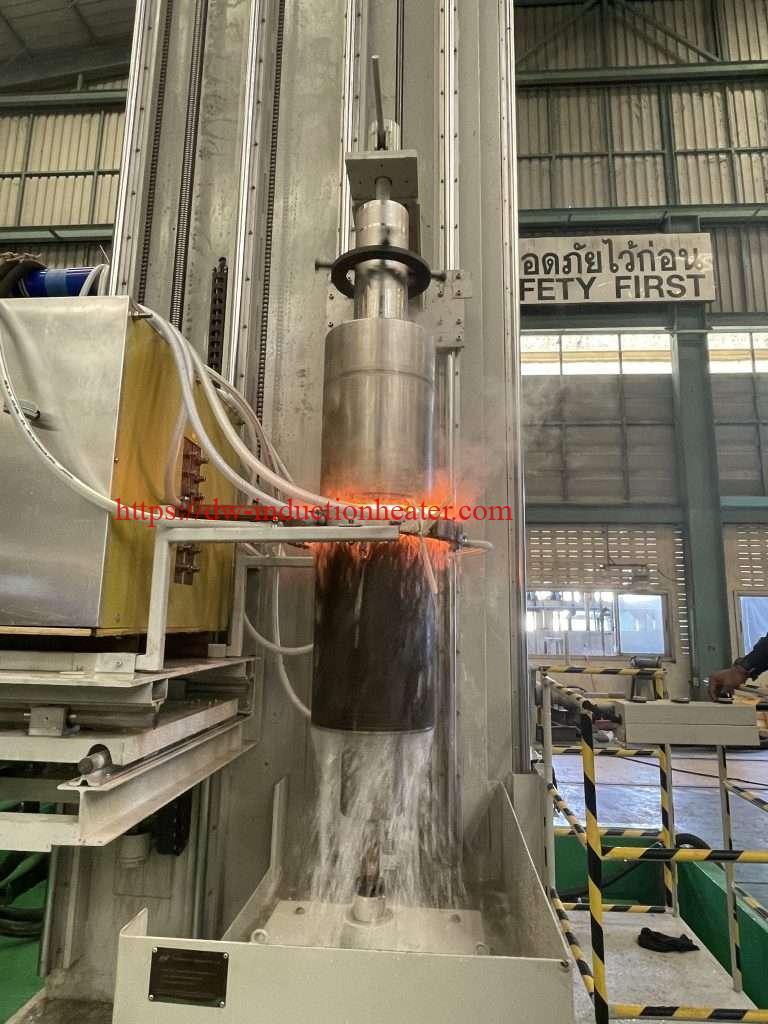
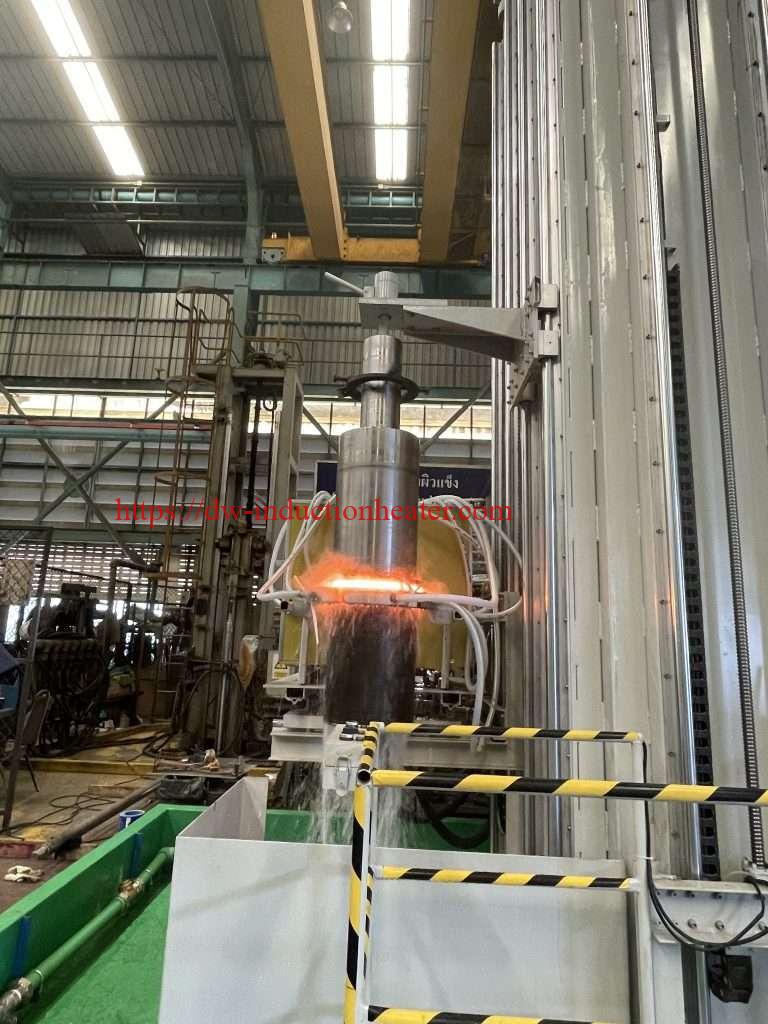
Models Rated output power Frequency rage Input current Input voltage Duty cycle Water flow weight Dimension
MFS-100 100KW 0.5-10KHz 160A 3phase 380V 50Hz 100% 10-20m³/h 175KG 800x650x1800mm
MFS-160 160KW 0.5-10KHz 250A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-200 200KW 0.5-10KHz 310A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-250 250KW 0.5-10KHz 380A 10-20m³/h 192KG 800x 650 x 1800mm
MFS-300 300KW 0.5-8KHz 460A 25-35m³/h 198KG 800x 650 x 1800mm
MFS-400 400KW 0.5-8KHz 610A 25-35m³/h 225KG 800x 650 x 1800mm
MFS-500 500KW 0.5-8KHz 760A 25-35m³/h 350KG 1500 x 800 x 2000mm
MFS-600 600KW 0.5-8KHz 920A 25-35m³/h 360KG 1500 x 800 x 2000mm
MFS-750 750KW 0.5-6KHz 1150A 50-60m³/h 380KG 1500 x 800 x 2000mm
MFS-800 800KW 0.5-6KHz 1300A 50-60m³/h 390KG 1500 x 800 x 2000mm
6.  CNC Hardening / Quenching Machine Tools Technical Parameter
Model SK-500 SK-1000 SK-1200 SK-1500
Max heating length(mm) 500 1000 1200 1500
Max heating diameter(mm) 500 500 600 600
Max holding length(mm) 600 1100 1300 1600
Max weight of workpiece(Kg) 100 100 100 100
Workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 1.1KW 1.1KW 1.2KW 1.5KW
Dimension LxWxH (mm) 1600 x800 x2000 1600 x800 x2400 1900 x900 x2900 1900 x900 x3200
weight(Kg) 800 900 1100 1200
Model SK-2000 SK-2500 SK-3000 SK-4000
Max heating length(mm) 2000 2500 3000 4000
Max heating diameter(mm) 600 600 600 600
Max holding length(mm) 2000 2500 3000 4000
Max weight of workpiece(Kg) 800 1000 1200 1500
workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 2KW 2.2KW 2.5KW 3KW
Dimension LxWxH (mm) 1900 x900 x2400 1900 x900 x2900 1900 x900 x3400 1900 x900 x4300
weight(Kg) 1200 1300 1400 1500
7. Conclusion The specific parameters of the induction hardening process, such as heating time, frequency, power, and quenching medium, are determined based on the material composition, component geometry, desired hardness, and application requirements. Induction hardening provides localized hardening, which allows for a combination of a hard and wear-resistant surface with a tough and ductile core. This makes it suitable for components like shafts, rollers, and pins that require high surface hardness and wear resistance while maintaining sufficient strength and toughness in the core.   https://dw-inductionheater.com/cnc-induction-hardening-surface-of-shafts-rollers-pins.html?feed_id=231406&_unique_id=6594ec8d6a8d6

2023年10月8日星期日

CNC Induction Hardening Surface of Shafts, Rollers, Pins

Ultimate Guide to Induction Hardening: Enhancing the Surface of Shafts, Rollers, and Pins.

induction hardening processInduction hardening is a specialized heat treatment process that can significantly enhance the surface properties of various components, including shafts, rollers, and pins. This advanced technique involves selectively heating the surface of the material using high-frequency induction coils and then rapidly quenching it to achieve optimal hardness and wear resistance. In this comprehensive guide, we will explore the intricacies of induction hardening, from the science behind the process to the benefits it offers in terms of improving the durability and performance of these crucial industrial components. Whether you are a manufacturer looking to optimize your production processes or simply curious about the fascinating world of heat treatments, this article will provide you with the ultimate insights into induction hardening. [embed]https://youtu.be/fD89qj5t9Ig[/embed] 1. What is induction hardening? Induction hardening is a heat treatment process used to enhance the surface properties of various components such as shafts, rollers, and pins. It involves heating the surface of the component using high-frequency electrical currents, which are generated by an induction coil. The intense heat generated quickly raises the temperature of the surface, while the core remains relatively cool. This rapid heating and cooling process results in a hardened surface with improved wear resistance, hardness, and strength. The induction hardening process begins by positioning the component within the induction coil. The coil is connected to a power source, which produces an alternating current that flows through the coil, creating a magnetic field. When the component is placed within this magnetic field, eddy currents are induced in its surface. These eddy currents generate heat due to the resistance of the material. As the surface temperature increases, it reaches the austenitizing temperature, which is the critical temperature required for transformation to occur. At this point, the heat is quickly removed, usually through the use of a water spray or quenching medium. The rapid cooling causes the austenite to transform into martensite, a hard and brittle phase that contributes to the enhanced surface properties. Induction hardening offers several advantages over traditional hardening methods. It is a highly localized process, focusing only on the areas that require hardening, which minimizes distortion and reduces energy consumption. The precise control over the heating and cooling process allows for customization of hardness profiles according to specific requirements. Additionally, induction hardening is a fast and efficient process that can be easily automated for high-volume production. In summary, induction hardening is a specialized heat treatment technique that selectively improves the surface properties of components like shafts, rollers, and pins. By harnessing the power of high-frequency electrical currents, this process provides enhanced wear resistance, hardness, and strength, making it a valuable method for enhancing the performance and durability of various industrial components. 2. The science behind induction hardening Induction hardening is a fascinating process that involves enhancing the surface of shafts, rollers, and pins to increase their durability and strength. To understand the science behind induction hardening, we must first delve into the principles of induction heating. The process of induction heating utilizes an alternating magnetic field generated by an induction coil. When an electric current passes through the coil, it generates the magnetic field, which creates eddy currents within the workpiece. These eddy currents produce heat due to the resistance of the material, leading to localized heating. During induction hardening, the workpiece is rapidly heated to a specific temperature above its transformation point, known as the austenitizing temperature. This temperature varies depending on the material being hardened. Once the desired temperature is reached, the workpiece is quenched, typically using water or oil, to rapidly cool it down. The science behind induction hardening lies in the transformation of the material's microstructure. By rapidly heating and cooling the surface, the material undergoes a phase change from its initial state to a hardened state. This phase change results in the formation of martensite, a hard and brittle structure that significantly enhances the surface's mechanical properties. The depth of hardened layer, known as the case depth, can be controlled by adjusting various parameters such as the frequency of the magnetic field, power input, and quenching medium. These variables directly influence the heating rate, cooling rate, and ultimately, the final hardness and wear resistance of the hardened surface. It's important to note that induction hardening is a highly precise process, offering excellent control over localized heating. By selectively heating only the desired areas, such as shafts, rollers, and pins, manufacturers can achieve optimal hardness and wear resistance while maintaining the core's toughness and ductility. In conclusion, the science behind induction hardening lies in the principles of induction heating, the transformation of microstructure, and the control of various parameters. This process enables the enhancement of the surface properties of shafts, rollers, and pins, resulting in improved durability and performance in various industrial applications. 3. Benefits of induction hardening for shafts, rollers, and pins Induction hardening is a widely used heat treatment process that offers numerous benefits for enhancing the surface of shafts, rollers, and pins. The primary advantage of induction hardening is its ability to selectively heat treat specific areas, resulting in a hardened surface while maintaining the core's desired properties. This process improves the durability and wear resistance of these components, making them ideal for heavy-duty applications. One of the key benefits of induction hardening is the significant increase in hardness achieved on the surface of shafts, rollers, and pins. This enhanced hardness helps to prevent surface damage, such as abrasion and deformation, extending the lifespan of the components. The hardened surface also provides improved resistance to fatigue, ensuring that these parts can withstand high-stress conditions without compromising their performance. In addition to hardness, induction hardening improves the overall strength of shafts, rollers, and pins. The localized heating and rapid quenching process during induction hardening results in a transformation of the microstructure, leading to increased tensile strength and toughness. This makes the components more resistant to bending, breaking, and deformation, enhancing their reliability and longevity. Another significant advantage of induction hardening is its efficiency and speed. The process is known for its rapid heating and quenching cycles, enabling high production rates and cost-effective manufacturing. Compared to traditional methods such as case hardening or through-hardening, induction hardening offers shorter cycle times, reducing energy consumption and improving productivity. Furthermore, induction hardening allows for precise control over the hardened depth. By adjusting the power and frequency of the induction heating, manufacturers can achieve the desired hardened depth specific to their application requirements. This flexibility ensures that the surface hardness is optimized while maintaining the appropriate core properties. Overall, the benefits of induction hardening make it an ideal choice for enhancing the surface of shafts, rollers, and pins. From increased hardness and strength to improved durability and efficiency, induction hardening offers manufacturers a reliable and cost-effective method to enhance the performance and longevity of these critical components in various industries. 4. The induction hardening process explained Induction hardening is a widely used technique in the manufacturing industry to enhance the surface properties of various components, such as shafts, rollers, and pins. This process involves heating the selected areas of the component using high-frequency induction heating, followed by rapid quenching to achieve a hardened surface layer. The induction hardening process begins with the positioning of the component in the induction coil, which generates a high-frequency alternating magnetic field. This magnetic field induces eddy currents in the workpiece, leading to rapid and localized heating of the surface. The depth of the hardened layer can be controlled by adjusting the frequency, power, and time of the induction heating. As the surface temperature rises above the critical transformation temperature, the austenite phase is formed. This phase is then rapidly quenched using a suitable medium, such as water or oil, to transform it into martensite. The martensitic structure provides excellent hardness, wear resistance, and strength to the treated surface, while the core of the component retains its original properties. One of the significant advantages of induction hardening is its ability to achieve precise and controlled hardening patterns. By carefully designing the shape and configuration of the induction coil, specific areas of the component can be targeted for hardening. This selective heating minimizes distortion and ensures that only the required surface areas are hardened, preserving the desired mechanical properties of the core. Induction hardening is highly efficient and can be integrated into automated production lines, ensuring consistent and repeatable results. It offers several benefits over other surface hardening methods, such as flame hardening or carburizing, including shorter heating times, reduced energy consumption, and minimal material distortion. However, it is crucial to note that the induction hardening process requires careful process design and parameter optimization to ensure optimal results. Factors such as the component material, geometry, and desired hardening depth must be taken into consideration. In conclusion, induction hardening is a versatile and effective method for enhancing the surface properties of shafts, rollers, and pins. Its ability to provide localized and controlled hardening makes it ideal for various industrial applications where wear resistance, hardness, and strength are essential. By understanding the induction hardening process, manufacturers can harness its benefits to produce high-quality and durable components. 5. Induction Hardening  Power  Supplier
Models Rated output power Frequency rage Input current Input voltage Duty cycle Water flow weight Dimension
MFS-100 100KW 0.5-10KHz 160A 3phase 380V 50Hz 100% 10-20m³/h 175KG 800x650x1800mm
MFS-160 160KW 0.5-10KHz 250A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-200 200KW 0.5-10KHz 310A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-250 250KW 0.5-10KHz 380A 10-20m³/h 192KG 800x 650 x 1800mm
MFS-300 300KW 0.5-8KHz 460A 25-35m³/h 198KG 800x 650 x 1800mm
MFS-400 400KW 0.5-8KHz 610A 25-35m³/h 225KG 800x 650 x 1800mm
MFS-500 500KW 0.5-8KHz 760A 25-35m³/h 350KG 1500 x 800 x 2000mm
MFS-600 600KW 0.5-8KHz 920A 25-35m³/h 360KG 1500 x 800 x 2000mm
MFS-750 750KW 0.5-6KHz 1150A 50-60m³/h 380KG 1500 x 800 x 2000mm
MFS-800 800KW 0.5-6KHz 1300A 50-60m³/h 390KG 1500 x 800 x 2000mm
6.  CNC Hardening / Quenching Machine Tools Technical Parameter
Model SK-500 SK-1000 SK-1200 SK-1500
Max heating length(mm) 500 1000 1200 1500
Max heating diameter(mm) 500 500 600 600
Max holding length(mm) 600 1100 1300 1600
Max weight of workpiece(Kg) 100 100 100 100
Workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 1.1KW 1.1KW 1.2KW 1.5KW
Dimension LxWxH (mm) 1600 x800 x2000 1600 x800 x2400 1900 x900 x2900 1900 x900 x3200
weight(Kg) 800 900 1100 1200
Model SK-2000 SK-2500 SK-3000 SK-4000
Max heating length(mm) 2000 2500 3000 4000
Max heating diameter(mm) 600 600 600 600
Max holding length(mm) 2000 2500 3000 4000
Max weight of workpiece(Kg) 800 1000 1200 1500
workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 2KW 2.2KW 2.5KW 3KW
Dimension LxWxH (mm) 1900 x900 x2400 1900 x900 x2900 1900 x900 x3400 1900 x900 x4300
weight(Kg) 1200 1300 1400 1500
7. Conclusion The specific parameters of the induction hardening process, such as heating time, frequency, power, and quenching medium, are determined based on the material composition, component geometry, desired hardness, and application requirements. Induction hardening provides localized hardening, which allows for a combination of a hard and wear-resistant surface with a tough and ductile core. This makes it suitable for components like shafts, rollers, and pins that require high surface hardness and wear resistance while maintaining sufficient strength and toughness in the core.   https://dw-inductionheater.com/cnc-induction-hardening-surface-of-shafts-rollers-pins.html?feed_id=228669&_unique_id=6522eeb509cba

CNC Induction Hardening Surface of Shafts, Rollers, Pins

Ultimate Guide to Induction Hardening: Enhancing the Surface of Shafts, Rollers, and Pins.

induction hardening processInduction hardening is a specialized heat treatment process that can significantly enhance the surface properties of various components, including shafts, rollers, and pins. This advanced technique involves selectively heating the surface of the material using high-frequency induction coils and then rapidly quenching it to achieve optimal hardness and wear resistance. In this comprehensive guide, we will explore the intricacies of induction hardening, from the science behind the process to the benefits it offers in terms of improving the durability and performance of these crucial industrial components. Whether you are a manufacturer looking to optimize your production processes or simply curious about the fascinating world of heat treatments, this article will provide you with the ultimate insights into induction hardening. [embed]https://youtu.be/fD89qj5t9Ig[/embed] 1. What is induction hardening? Induction hardening is a heat treatment process used to enhance the surface properties of various components such as shafts, rollers, and pins. It involves heating the surface of the component using high-frequency electrical currents, which are generated by an induction coil. The intense heat generated quickly raises the temperature of the surface, while the core remains relatively cool. This rapid heating and cooling process results in a hardened surface with improved wear resistance, hardness, and strength. The induction hardening process begins by positioning the component within the induction coil. The coil is connected to a power source, which produces an alternating current that flows through the coil, creating a magnetic field. When the component is placed within this magnetic field, eddy currents are induced in its surface. These eddy currents generate heat due to the resistance of the material. As the surface temperature increases, it reaches the austenitizing temperature, which is the critical temperature required for transformation to occur. At this point, the heat is quickly removed, usually through the use of a water spray or quenching medium. The rapid cooling causes the austenite to transform into martensite, a hard and brittle phase that contributes to the enhanced surface properties. Induction hardening offers several advantages over traditional hardening methods. It is a highly localized process, focusing only on the areas that require hardening, which minimizes distortion and reduces energy consumption. The precise control over the heating and cooling process allows for customization of hardness profiles according to specific requirements. Additionally, induction hardening is a fast and efficient process that can be easily automated for high-volume production. In summary, induction hardening is a specialized heat treatment technique that selectively improves the surface properties of components like shafts, rollers, and pins. By harnessing the power of high-frequency electrical currents, this process provides enhanced wear resistance, hardness, and strength, making it a valuable method for enhancing the performance and durability of various industrial components. 2. The science behind induction hardening Induction hardening is a fascinating process that involves enhancing the surface of shafts, rollers, and pins to increase their durability and strength. To understand the science behind induction hardening, we must first delve into the principles of induction heating. The process of induction heating utilizes an alternating magnetic field generated by an induction coil. When an electric current passes through the coil, it generates the magnetic field, which creates eddy currents within the workpiece. These eddy currents produce heat due to the resistance of the material, leading to localized heating. During induction hardening, the workpiece is rapidly heated to a specific temperature above its transformation point, known as the austenitizing temperature. This temperature varies depending on the material being hardened. Once the desired temperature is reached, the workpiece is quenched, typically using water or oil, to rapidly cool it down. The science behind induction hardening lies in the transformation of the material's microstructure. By rapidly heating and cooling the surface, the material undergoes a phase change from its initial state to a hardened state. This phase change results in the formation of martensite, a hard and brittle structure that significantly enhances the surface's mechanical properties. The depth of hardened layer, known as the case depth, can be controlled by adjusting various parameters such as the frequency of the magnetic field, power input, and quenching medium. These variables directly influence the heating rate, cooling rate, and ultimately, the final hardness and wear resistance of the hardened surface. It's important to note that induction hardening is a highly precise process, offering excellent control over localized heating. By selectively heating only the desired areas, such as shafts, rollers, and pins, manufacturers can achieve optimal hardness and wear resistance while maintaining the core's toughness and ductility. In conclusion, the science behind induction hardening lies in the principles of induction heating, the transformation of microstructure, and the control of various parameters. This process enables the enhancement of the surface properties of shafts, rollers, and pins, resulting in improved durability and performance in various industrial applications. 3. Benefits of induction hardening for shafts, rollers, and pins Induction hardening is a widely used heat treatment process that offers numerous benefits for enhancing the surface of shafts, rollers, and pins. The primary advantage of induction hardening is its ability to selectively heat treat specific areas, resulting in a hardened surface while maintaining the core's desired properties. This process improves the durability and wear resistance of these components, making them ideal for heavy-duty applications. One of the key benefits of induction hardening is the significant increase in hardness achieved on the surface of shafts, rollers, and pins. This enhanced hardness helps to prevent surface damage, such as abrasion and deformation, extending the lifespan of the components. The hardened surface also provides improved resistance to fatigue, ensuring that these parts can withstand high-stress conditions without compromising their performance. In addition to hardness, induction hardening improves the overall strength of shafts, rollers, and pins. The localized heating and rapid quenching process during induction hardening results in a transformation of the microstructure, leading to increased tensile strength and toughness. This makes the components more resistant to bending, breaking, and deformation, enhancing their reliability and longevity. Another significant advantage of induction hardening is its efficiency and speed. The process is known for its rapid heating and quenching cycles, enabling high production rates and cost-effective manufacturing. Compared to traditional methods such as case hardening or through-hardening, induction hardening offers shorter cycle times, reducing energy consumption and improving productivity. Furthermore, induction hardening allows for precise control over the hardened depth. By adjusting the power and frequency of the induction heating, manufacturers can achieve the desired hardened depth specific to their application requirements. This flexibility ensures that the surface hardness is optimized while maintaining the appropriate core properties. Overall, the benefits of induction hardening make it an ideal choice for enhancing the surface of shafts, rollers, and pins. From increased hardness and strength to improved durability and efficiency, induction hardening offers manufacturers a reliable and cost-effective method to enhance the performance and longevity of these critical components in various industries. 4. The induction hardening process explained Induction hardening is a widely used technique in the manufacturing industry to enhance the surface properties of various components, such as shafts, rollers, and pins. This process involves heating the selected areas of the component using high-frequency induction heating, followed by rapid quenching to achieve a hardened surface layer. The induction hardening process begins with the positioning of the component in the induction coil, which generates a high-frequency alternating magnetic field. This magnetic field induces eddy currents in the workpiece, leading to rapid and localized heating of the surface. The depth of the hardened layer can be controlled by adjusting the frequency, power, and time of the induction heating. As the surface temperature rises above the critical transformation temperature, the austenite phase is formed. This phase is then rapidly quenched using a suitable medium, such as water or oil, to transform it into martensite. The martensitic structure provides excellent hardness, wear resistance, and strength to the treated surface, while the core of the component retains its original properties. One of the significant advantages of induction hardening is its ability to achieve precise and controlled hardening patterns. By carefully designing the shape and configuration of the induction coil, specific areas of the component can be targeted for hardening. This selective heating minimizes distortion and ensures that only the required surface areas are hardened, preserving the desired mechanical properties of the core. Induction hardening is highly efficient and can be integrated into automated production lines, ensuring consistent and repeatable results. It offers several benefits over other surface hardening methods, such as flame hardening or carburizing, including shorter heating times, reduced energy consumption, and minimal material distortion. However, it is crucial to note that the induction hardening process requires careful process design and parameter optimization to ensure optimal results. Factors such as the component material, geometry, and desired hardening depth must be taken into consideration. In conclusion, induction hardening is a versatile and effective method for enhancing the surface properties of shafts, rollers, and pins. Its ability to provide localized and controlled hardening makes it ideal for various industrial applications where wear resistance, hardness, and strength are essential. By understanding the induction hardening process, manufacturers can harness its benefits to produce high-quality and durable components. 5. Induction Hardening  Power  Supplier
Models Rated output power Frequency rage Input current Input voltage Duty cycle Water flow weight Dimension
MFS-100 100KW 0.5-10KHz 160A 3phase 380V 50Hz 100% 10-20m³/h 175KG 800x650x1800mm
MFS-160 160KW 0.5-10KHz 250A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-200 200KW 0.5-10KHz 310A 10-20m³/h 180KG 800x 650 x 1800mm
MFS-250 250KW 0.5-10KHz 380A 10-20m³/h 192KG 800x 650 x 1800mm
MFS-300 300KW 0.5-8KHz 460A 25-35m³/h 198KG 800x 650 x 1800mm
MFS-400 400KW 0.5-8KHz 610A 25-35m³/h 225KG 800x 650 x 1800mm
MFS-500 500KW 0.5-8KHz 760A 25-35m³/h 350KG 1500 x 800 x 2000mm
MFS-600 600KW 0.5-8KHz 920A 25-35m³/h 360KG 1500 x 800 x 2000mm
MFS-750 750KW 0.5-6KHz 1150A 50-60m³/h 380KG 1500 x 800 x 2000mm
MFS-800 800KW 0.5-6KHz 1300A 50-60m³/h 390KG 1500 x 800 x 2000mm
6.  CNC Hardening / Quenching Machine Tools Technical Parameter
Model SK-500 SK-1000 SK-1200 SK-1500
Max heating length(mm) 500 1000 1200 1500
Max heating diameter(mm) 500 500 600 600
Max holding length(mm) 600 1100 1300 1600
Max weight of workpiece(Kg) 100 100 100 100
Workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 1.1KW 1.1KW 1.2KW 1.5KW
Dimension LxWxH (mm) 1600 x800 x2000 1600 x800 x2400 1900 x900 x2900 1900 x900 x3200
weight(Kg) 800 900 1100 1200
Model SK-2000 SK-2500 SK-3000 SK-4000
Max heating length(mm) 2000 2500 3000 4000
Max heating diameter(mm) 600 600 600 600
Max holding length(mm) 2000 2500 3000 4000
Max weight of workpiece(Kg) 800 1000 1200 1500
workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 2KW 2.2KW 2.5KW 3KW
Dimension LxWxH (mm) 1900 x900 x2400 1900 x900 x2900 1900 x900 x3400 1900 x900 x4300
weight(Kg) 1200 1300 1400 1500
7. Conclusion The specific parameters of the induction hardening process, such as heating time, frequency, power, and quenching medium, are determined based on the material composition, component geometry, desired hardness, and application requirements. Induction hardening provides localized hardening, which allows for a combination of a hard and wear-resistant surface with a tough and ductile core. This makes it suitable for components like shafts, rollers, and pins that require high surface hardness and wear resistance while maintaining sufficient strength and toughness in the core.   https://dw-inductionheater.com/cnc-induction-hardening-surface-of-shafts-rollers-pins.html?feed_id=228604&_unique_id=652277de4e2b1

2023年6月25日星期日

induction hardening process

High Frequency Induction Hardening  Process

Induction hardening is used in particular for the hardening/quenching of bearing surfaces and shafts as well as intricately shaped parts where only a specific area needs to be heated. Through the choice of the operating frequency of the induction heating system, the resulting depth of penetration is defined. Additionally, it can be decided if the area is to be hardened in the air, with water or with a special hardening emulsion. Depending on the cooling medium, different degrees of hardness are achieved. Induction hardening can be realized as a manual or automated solution. There is also the possibility to harden in a continuous process.
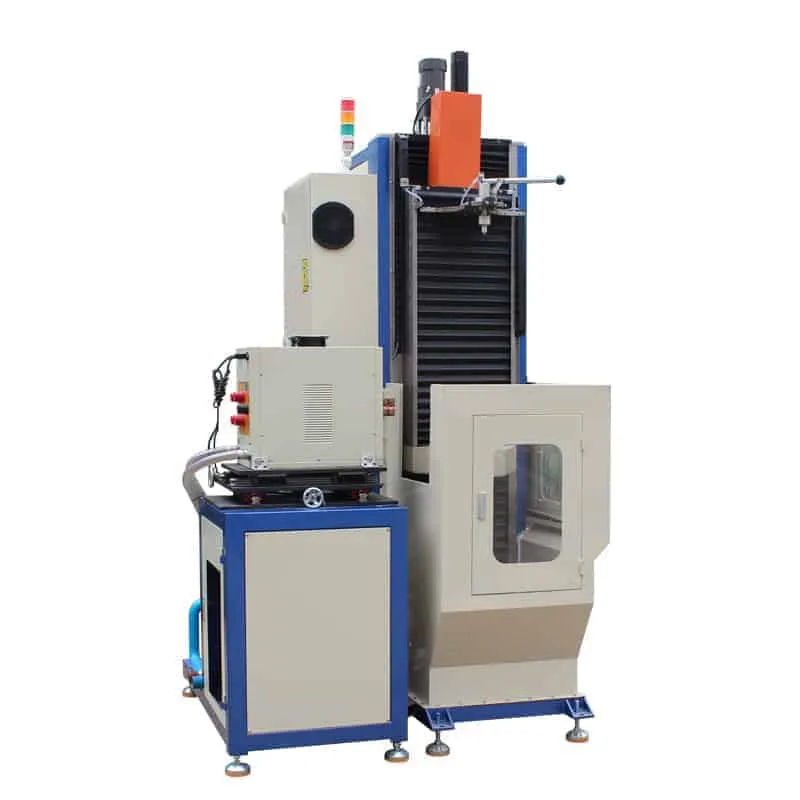
  • Suitable for hardening and tempering of various workpieces, such as induction hardening of shafts, gears, guide rails, discs, pins, and other parts;
  • It has the functions of continuous hardening, simultaneous hardening, segmented continuous hardening, and segmented simultaneous hardening;
  • Use numerical control system or PLC and frequency conversion speed regulation system to realize workpiece positioning and scanning, and connect PLC and induction heating power supply to realize fully automated production.
  • Vertical (hardening of shaft parts) + horizontal (hardening of gear ring parts)
Hardening is one of HLQ induction heating power systems's main application areas. Hundreds of our hardening solutions are at work around the world—many of them within the automotive industry. The main benefit of induction heating for hardening is that it takes just a few seconds. In a furnace, the same process can take hours or even days. How is that possible? The answer is that induction is phenomenal at generating heat fast. This, in turn, means you can integrate hardening in the production process. Hardening in a furnace, on the other hand, is more time-consuming (greater heat loss) and requires moving the components either to your own furnace or to that of a subcontractor. In-line integration of hardening reduces your lead times considerably. You get full control over quality, delivery times and costs. There's no need to transport kilos of components back and forward, which saves energy and the environment.And last but not least, you cut down the amount of administration to a minimum. HLQ Induction Heating Power Systems has many years of experience in inductive hardening and tempering of diverse workpieces. At the heart of each Hardening system is HLQ Induction Heating Power Systems Induction Heat Power Source, the industry's most advanced induction frequency converter. These acclaimed converters help ensure optimum hardening results—day in day out, year after year The induction hardening machine includes Vertical Scanning , Horizontal (centerless) Scanning and customized machines—and serial and/or parallel compensated induction power sources with a wide range of output power and frequencies.
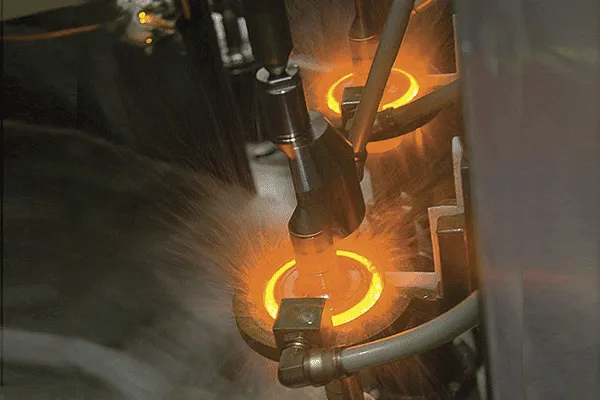
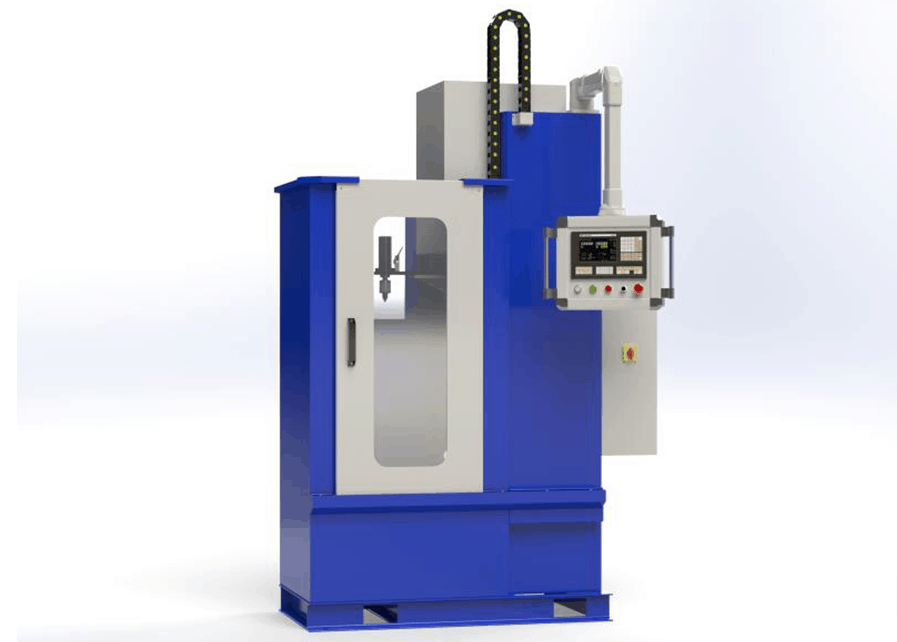
  • This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine.
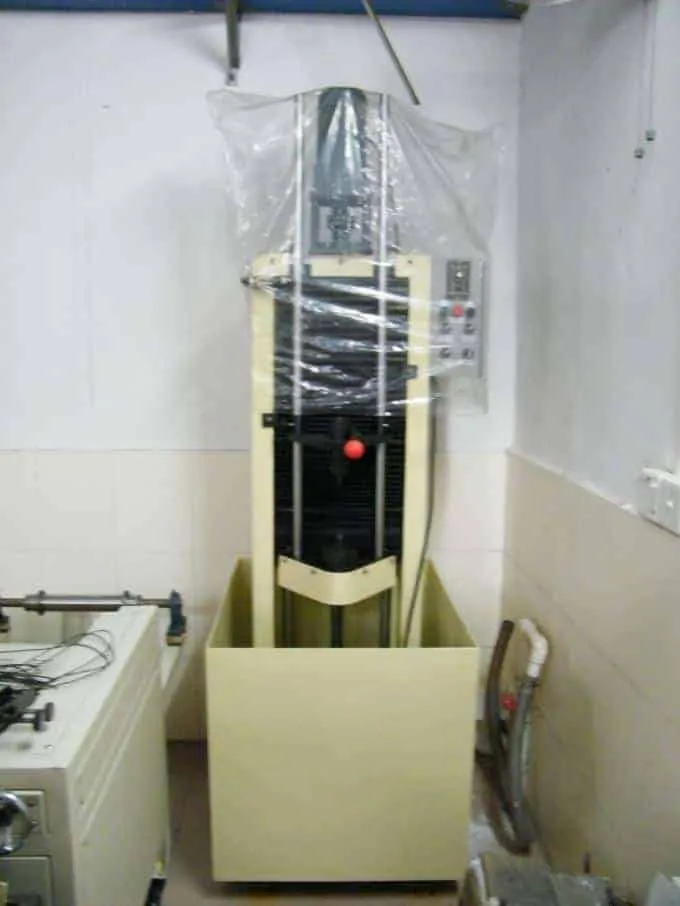
  • CNC quenching/hardening machine tool feature:
  • CNC system:The high-frequency quenching machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements.
  • HMI: programming type and human machine interface displays in English and Chinese.
  • Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed.
  • Lathe: adopt welded structure with good rust-proof functions.
  • Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece.
  • Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning.
  • Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted.
  • Electric control part: the machine tool has power-loosing protection function, has high safety and reliability.
  • Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor hardening process.
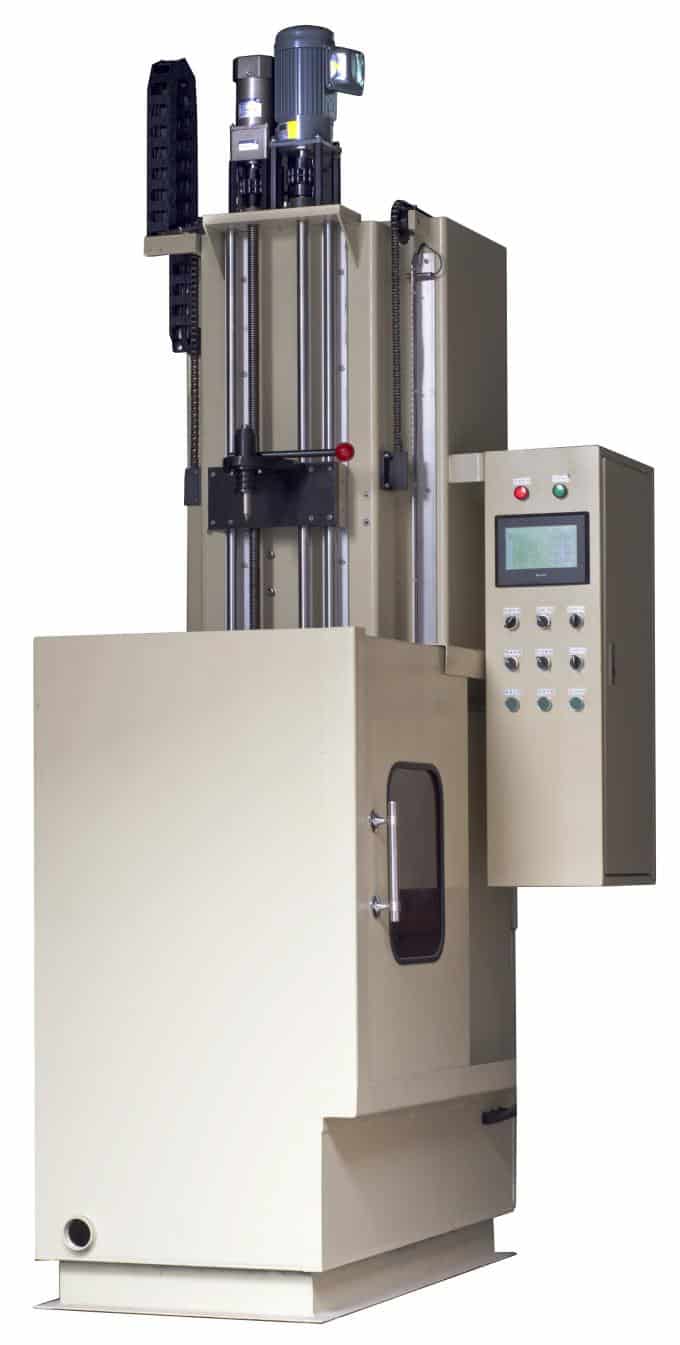
CNC vertical hardening/quenching machine tool This series hardening machine tool uses numberic control technology, has continuous, simultaneous, sectionally-continuous and sectionally-silultaneous quenching functions, it is mainly used for induction quenching of shafts, discs, pins and gears, and featured by high quenching precision. hardening machine tool used by connecting with medium frequency, superaudio frequency, high frequency and ultrahigh frequency induction heating machine. According to the different of workpiece, there are vertical type, horizontal type,closed type, customized type, etc. 1.Standard SK-500/1000/1200/1500 workpiece moving type For shafts, discs, pins and gears hardening 2.SK-2000/2500/3000/4000 Transformer moving type , Used for heating length more than 1500mm shaft 3.Closed type : Customized for big shaft ,More clean work environment. 4.Horizontal hardening machine tool SK-500/1000/1200/1500/2000/2500/3000/4000  Used for smooth shaft 5.Customized type Technical Parameter
Model SK-500 SK-1000 SK-1200 SK-1500
Max heating length(mm) 500 1000 1200 1500
Max heating diameter(mm) 500 500 600 600
Max holding length(mm) 600 1100 1300 1600
Max weight of workpiece(Kg) 100 100 100 100
Workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 1.1KW 1.1KW 1.2KW 1.5KW
Dimension LxWxH (mm) 1600 x800 x2000 1600 x800 x2400 1900 x900 x2900 1900 x900 x3200
weight(Kg) 800 900 1100 1200
 
Model SK-2000 SK-2500 SK-3000 SK-4000
Max heating length(mm) 2000 2500 3000 4000
Max heating diameter(mm) 600 600 600 600
Max holding length(mm) 2000 2500 3000 4000
Max weight of workpiece(Kg) 800 1000 1200 1500
workpiece rotation speed(r/min) 0-300 0-300 0-300 0-300
workpiece moving speed(mm/min) 6-3000 6-3000 6-3000 6-3000
Cooling method Hydrojet cooling Hydrojet cooling Hydrojet cooling Hydrojet cooling
Input voltage 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz 3P 380V 50Hz
Motor power 2KW 2.2KW 2.5KW 3KW
Dimension LxWxH (mm) 1900 x900 x2400 1900 x900 x2900 1900 x900 x3400 1900 x900 x4300
weight(Kg) 1200 1300 1400 1500
CNC hardening/quenching machine tool feature: 1.CNC system:The high-frequency hardening machine CNC system can compile and store a variety of quenching process programs according to different workpiece requirements. 2.HMI: programming type and human machine interface displays in English and Chinese. 3.Control adjust: it can control the heating power to start, stop, parts heating and cooling time, rotation speed and movement speed. 4.Lathe: adopt welded structure with good rust-proof functions. 5.Top adjustment parts: adopt electric adjustment, to realize clamping of different length work piece. 6.Work table system: adopt ball screw and servo motor to drive, driving light, high guide precision and accurate positioning. 7.Main shaft rotation system: adopt variable frequency regulating to realize parts rotation speed continuous adjusted. 8.Electric control part: the machine tool has power-loosing protection function, has high safety and reliability. 9.Frame: made by thick steel plates, with window and sliding doors, prevent water splash, easy to load parts and monitor induction hardening process.     [caption id="attachment_6788" align="alignnone" width="600"]  [/caption] https://dw-inductionheater.com/induction-hardening-process.html?feed_id=216136&_unique_id=6498b93607922
2023年6月18日星期日

The Benefits of Induction Quenching Surface Process for Manufacturing

The Benefits of Induction Quenching Surface Process for Manufacturing.

Manufacturing is an industry that thrives on innovation and efficiency. When it comes to surface treatment processes, induction quenching is quickly becoming the method of choice for a variety of manufacturing applications. Unlike traditional heat treatment methods, induction quenching offers several unique benefits such as high production rates, increased precision, and improved part quality. In this article, we'll look at some of the key benefits of induction quenching surface process and why it's quickly becoming a popular choice for manufacturers across a range of industries. So, if you're looking to improve the efficiency and quality of your manufacturing process, or you're simply interested in the latest surface treatment techniques, keep reading to learn more about the benefits of induction quenching.

1. What is Induction Quenching Surface Process?

Induction quenching surface process is a type of surface hardening process that uses electrical induction to rapidly heat and cool metal parts. This process is commonly used in manufacturing because it offers a number of benefits over other types of surface hardening processes. In induction quenching, an induction coil is used to generate a high-frequency magnetic field that rapidly heats the metal part. Once the part is heated to the desired temperature, a quenching medium, such as water or oil, is used to rapidly cool the part. This rapid heating and cooling process causes the surface of the metal part to harden, which makes it more wear-resistant and less likely to crack or deform under stress. Induction quenching is also a very precise process that allows for accurate control of the surface hardness of the metal part. This precision makes it an ideal process for manufacturing parts that require high levels of wear resistance, such as gears, shafts, and bearings. Additionally, induction quenching is a very efficient process that can be completed quickly, which makes it ideal for high-volume production environments. Overall, induction quenching is a highly effective surface hardening process that offers many benefits for manufacturers looking to produce high-quality, durable metal parts.

2. Benefits of Induction Quenching Surface Process

Induction quenching surface process is a highly efficient manufacturing technique that offers numerous benefits over traditional surface treatment methods. One of the most significant benefits of this process is that it is incredibly fast and efficient. With the ability to deliver heat at a rate of up to 25,000 degrees per second, induction quenching can heat treat parts in seconds, instead of hours or days, as is the case with other heat treatment methods. This means that manufacturers can produce more parts in less time, without sacrificing quality or reliability. Another significant benefit of induction quenching surface process is that it produces a superior product.

The process uses localized heating, which means that the heat is only applied where it is needed, resulting in less distortion, less scrap, and fewer defects. This makes induction quenching a great choice for manufacturers who are looking to produce high-quality parts quickly and efficiently. Induction quenching surface process is also a more environmentally-friendly option than other surface treatment methods. Since the process uses less energy and generates less waste, it is a more sustainable option for manufacturers who are looking to reduce their carbon footprint and be more environmentally responsible. In addition to these benefits, induction quenching surface process also offers a more controlled and precise heat treatment. The process allows manufacturers to control the depth of the heat treatment and the hardness achieved, which is a significant advantage over other surface treatment methods. With this level of control, manufacturers can produce parts that are exact in their specifications and meet the needs of their customers. Overall, the benefits of induction quenching surface process make it an ideal choice for manufacturers who are looking to improve their production processes, reduce waste, and produce high-quality parts quickly and efficiently.

3. Applications of Induction Quenching Surface Process in Manufacturing

Induction quenching is a surface hardening process that uses induction heating to heat the surface of a material to a high temperature and then rapidly cools it down by quenching it with water, oil or a polymer solution. This process creates a surface that is harder, more wear-resistant, and more durable than the original material. Induction quenching has many applications in manufacturing, including the hardening of gears, shafts, and bearings. It is also used in the automotive industry to harden engine components, such as camshafts, rocker arms, and valve lifters. The aerospace industry uses induction quenching to harden turbine components, and the energy industry uses it to harden drilling and mining components. The medical industry also uses induction quenching to harden surgical instruments and dental tools.

The process is also used in the production of cutting tools and molds. Induction quenching can produce a surface that is up to 10 times harder than the original material, making it an ideal choice for manufacturing applications where durability and wear resistance are critical. Additionally, the process is efficient and cost-effective, making it an attractive option for many manufacturers.

4. Conclusion.

Induction quenching surface process is a type of heat treatment process that is used to harden metal parts. The induction process involves passing a high-frequency electrical current through a coil, which creates a magnetic field. The metal part is then placed inside the coil, where the magnetic field induces an electrical current in the metal. This current causes the metal to heat up quickly, which then allows for the surface of the metal to be rapidly quenched by an appropriate cooling medium. This process creates a hardened surface that is more resistant to wear and tear, making it ideal for use in a wide variety of industrial applications.

  https://dw-inductionheater.com/the-benefits-of-induction-quenching-surface-process-for-manufacturing.html?feed_id=214111&_unique_id=648f184ecd6e5

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.