显示标签为“Inductionhardeningheater”的博文。显示所有博文

2024年3月1日星期五

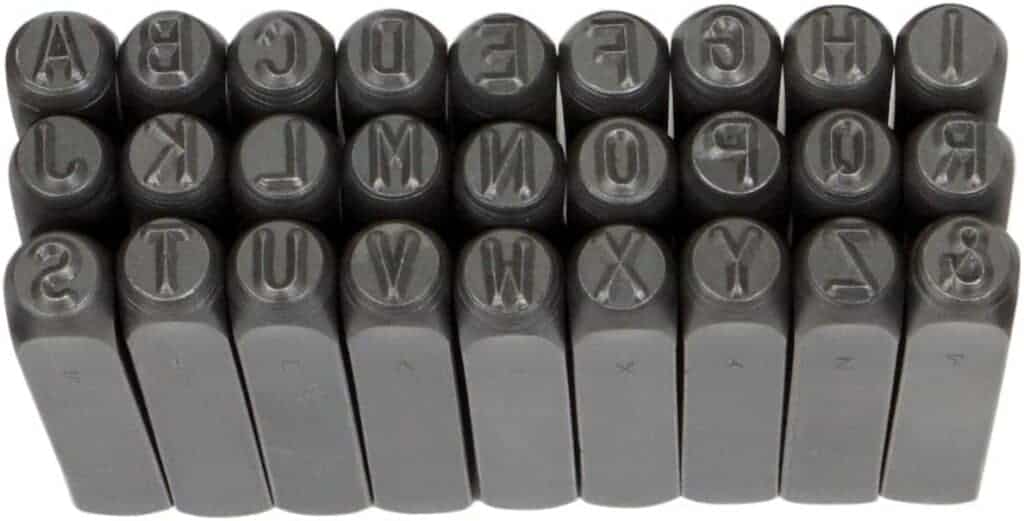
induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat https://dw-inductionheater.com/induction-hardening-steel-handheld-stamps.html?feed_id=235397&_unique_id=65e20c4fb4fdb

2024年2月10日星期六

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

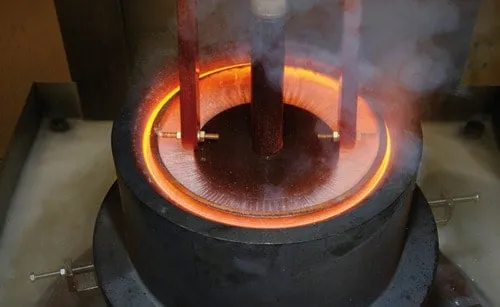
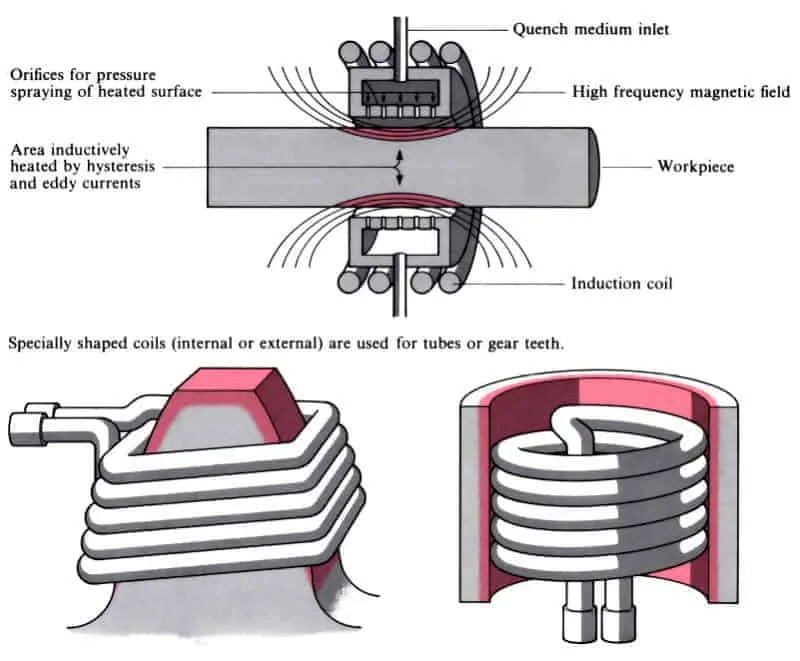
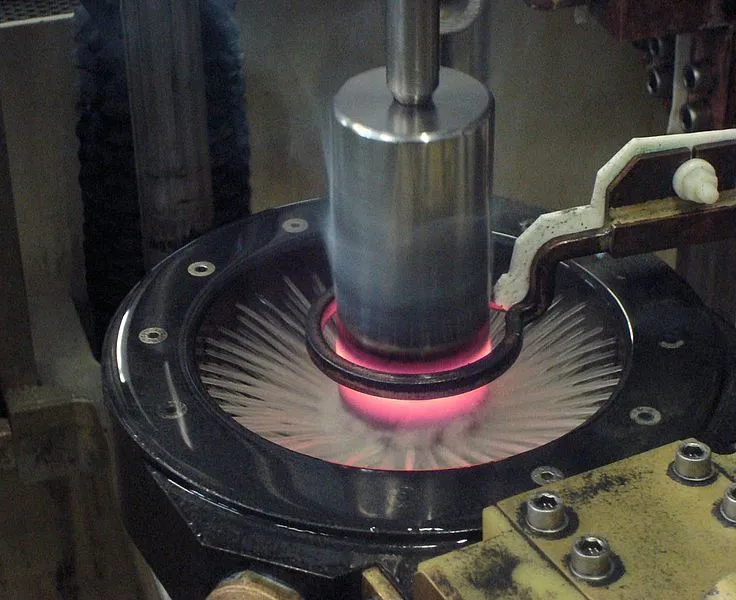
Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  
https://dw-inductionheater.com/induction-hardening-and-tempering.html?feed_id=233836&_unique_id=65c856f96ed5b

2023年9月30日星期六

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年8月27日星期日

induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat

2023年7月26日星期三

induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat

2023年7月16日星期日

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年7月9日星期日

induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat https://dw-inductionheater.com/induction-hardening-steel-handheld-stamps.html?feed_id=218161&_unique_id=64aa965f36bb0

2023年6月19日星期一

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  
https://dw-inductionheater.com/induction-hardening-and-tempering.html?feed_id=214561&_unique_id=6490dd0e137d3

2023年6月15日星期四

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年5月5日星期五

induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat

2023年5月1日星期一

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年4月17日星期一

induction hardening steel handheld stamps

induction hardening steel handheld stamps

Objective Induction hardening various size ends of handheld marking stamps. The area to be hardened is 3/4” (19mm) up the shank. Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square Temperature :1550 ºF (843 ºC) Frequency 99 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF • An induction heating coil designed and developed specifically for this application. Induction Hardening Process: A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily. Results/Benefits Induction heating provides: • Faster process time and production rates • Hands-free heating that involves no operator skill for manufacturing • Controlled precise application of heat

2023年3月12日星期日

Induction Hardening and tempering

Induction Hardening and tempering Surface Process


Induction Hardening


Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel.


To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc.

There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc.

The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:


  • It treats a specific part of the piece (hardening profile)

  • Frequency Control and heating times

  • Cooling control

  • Energy saving

  • No physical contact

  • Control and located heat

  • Can be integrated in production lines

  • Increase performance and saves space


Induction hardening can be done in two different ways:

  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.


  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.


For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering


Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness.

The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:


  • Shorter times in the process

  • Temperature control

  • Integration in production lines

  • Energy saving

  • Immediate availability of parts

  • Saves floor space

  • Improved environmental conditions


The process of hardening and tempering is a treatment for various components in many industrial sectors.


2023年3月11日星期六

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年3月7日星期二

Induction Hardening and tempering

Induction Hardening and tempering Surface Process

Induction Hardening

Induction Hardening is a process of heating followed by cooling generally fast for increase hardness and mechanical strength of steel. To this end, the steel is heated to a temperature slightly higher than the upper critical (between 850-900ºC) and then cooled more or less quickly (depending on the characteristics of steel) in a medium such as oil, air, water, water mixed with soluble polymers, etc. There are different methods for heating such as electric oven, gas cooker, salt, flame, induction, etc. The steels that are normally used in induction hardening contain from 0.3% to 0.7% carbon (hypoeutectic steels).

Induction heating advantages:

  • It treats a specific part of the piece (hardening profile)
  • Frequency Control and heating times
  • Cooling control
  • Energy saving
  • No physical contact
  • Control and located heat
  • Can be integrated in production lines
  • Increase performance and saves space
Induction hardening can be done in two different ways:
  • Static: consists of setting the part in front of the inductor and carrying out the operation without moving either the part or the inductor. This type of operation is very fast, requires only simple mechanics and enables a very accurate localisation of the treated area, even with parts with complicated geometry.
  • Progressive (by scanning): consists of going over the part with a continuous operation, moving either the part or the inductor. This kind of operation means that parts with large surfaces and large sizes can be treated.
For the same kind of part the scanning treatment requires less power with longer treatment time in compare to static treatment.

Induction Tempering

Induction Tempering is a process able to decrease the hardness, strength and increases the toughness of hardened steels, while removes the tensions created in the temple, leaving the steel with the required hardness. The traditional tempering system consists of heating the parts at relatively low temperatures (from 150ºC to 500°C, always below the lineAC1) for a while and then let them cool slowly.

Induction heating advantages:

  • Shorter times in the process
  • Temperature control
  • Integration in production lines
  • Energy saving
  • Immediate availability of parts
  • Saves floor space
  • Improved environmental conditions
The process of hardening and tempering is a treatment for various components in many industrial sectors.  

2023年3月6日星期一

induction hardening steel handheld stamps

induction hardening steel handheld stamps


Objective

Induction hardening various size ends of handheld marking stamps.
The area to be hardened is 3/4” (19mm) up the shank.

Material : Steel stamps 1/4” (6.3mm), 3/8” (9.5mm), 1/2” (12.7mm) and 5/8” (15.8mm) square

Temperature :1550 ºF (843 ºC)

Frequency 99 kHz

Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing eight 1.0µF capacitors for a total of 2.0µF
• An induction heating coil designed and developed specifically for this application.
Induction Hardening Process:

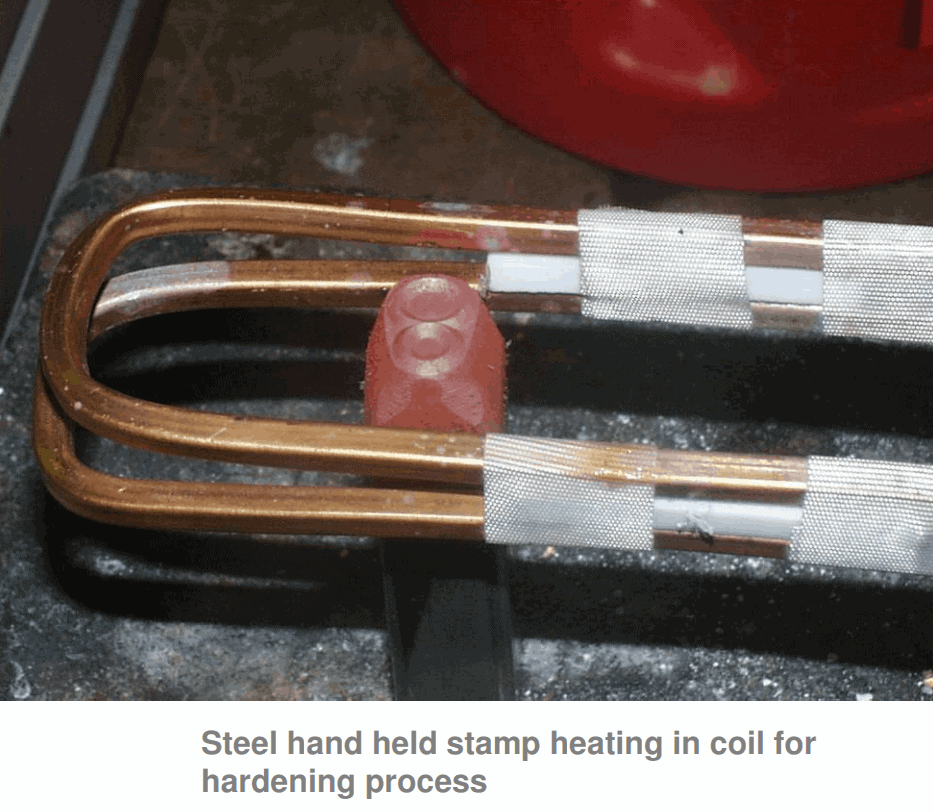
A two turn channel coil is used to cover the range of steel stamps being heated. The 5/8” steel stamp is heated for 60 seconds to reach 1550 ºF (843 ºC) and the desired hardness. Smaller parts will also heat easily.

Results/Benefits

Induction heating provides:
• Faster process time and production rates
• Hands-free heating that involves no operator skill for manufacturing
• Controlled precise application of heat
关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.