 https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61
2025年2月18日星期二
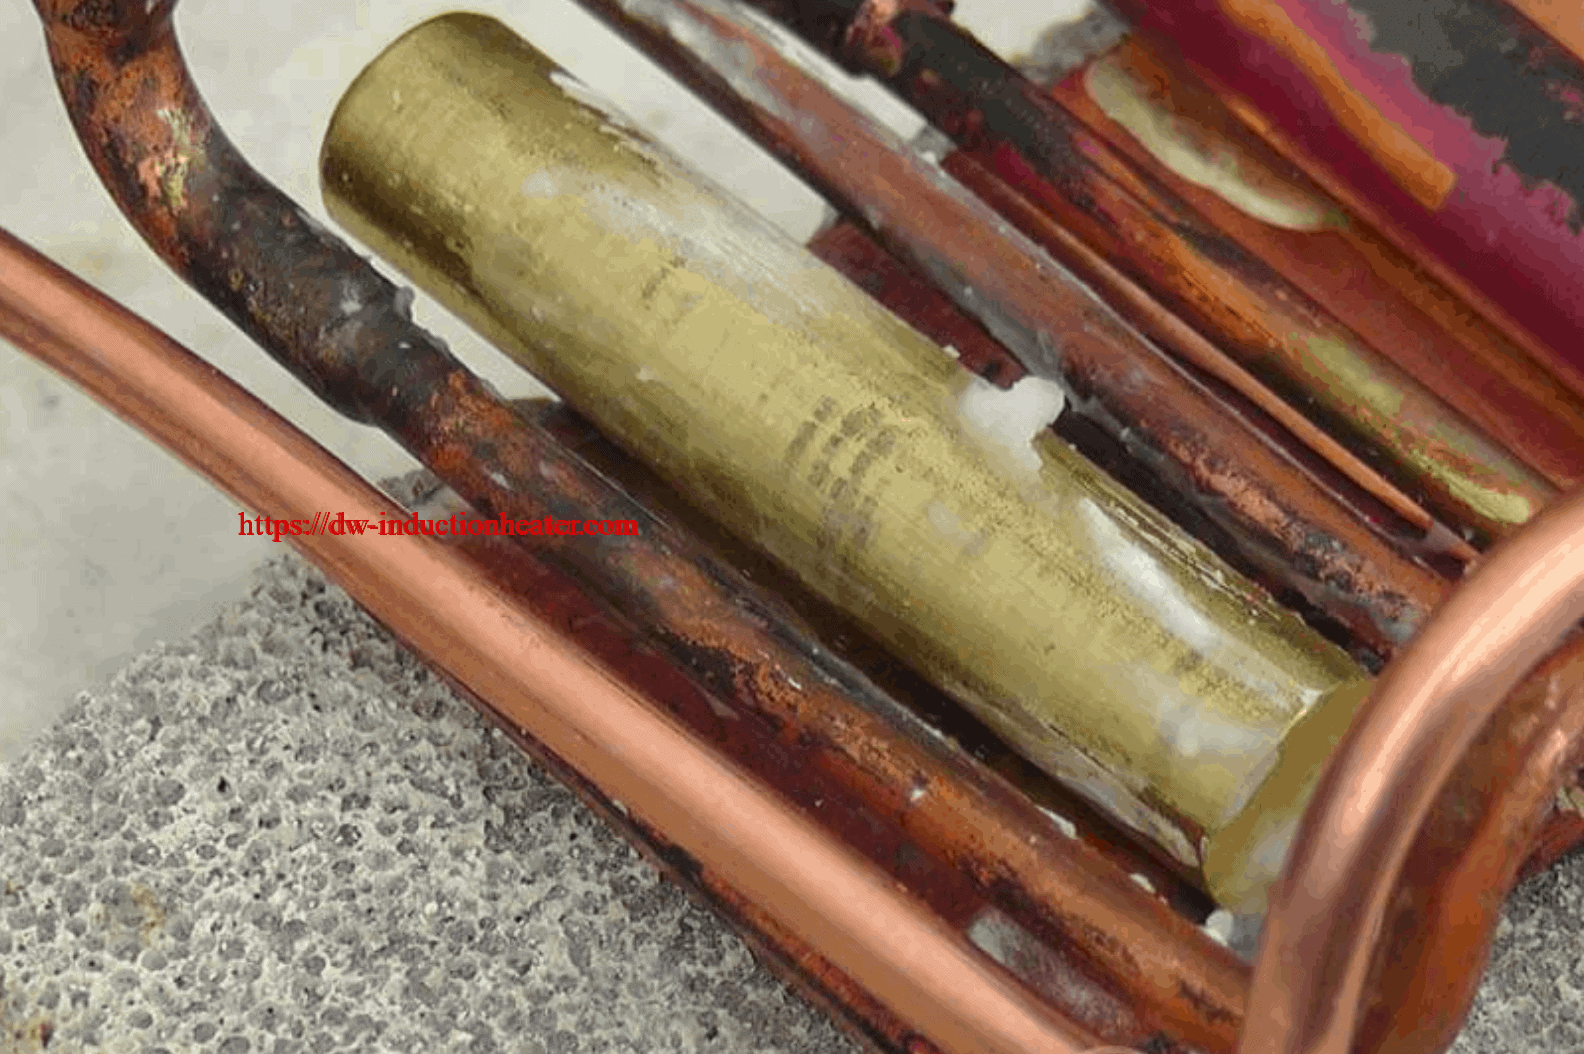
induction brazing copper and brass rods
induction brazing copper and brass rods
https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61
https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61

2025年1月29日星期三
Induction Brazing copper to copper pipes
Induction Brazing copper to copper pipes
 https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html?feed_id=268096&_unique_id=679a9050d61c9
2025年1月22日星期三
induction brazing stainless steel to copper
induction brazing stainless steel to copper
 https://dw-inductionheater.com/induction-brazing-stainless-steel-to-copper.html?feed_id=267458&_unique_id=6791aa44c7849
Induction Brazing Copper To Copper Parts
Induction Brazing Copper To Copper Parts
 https://dw-inductionheater.com/induction-brazing-copper-to-copper-parts.html?feed_id=267371&_unique_id=6790ad14138c7
2024年11月26日星期二
2024年10月8日星期二
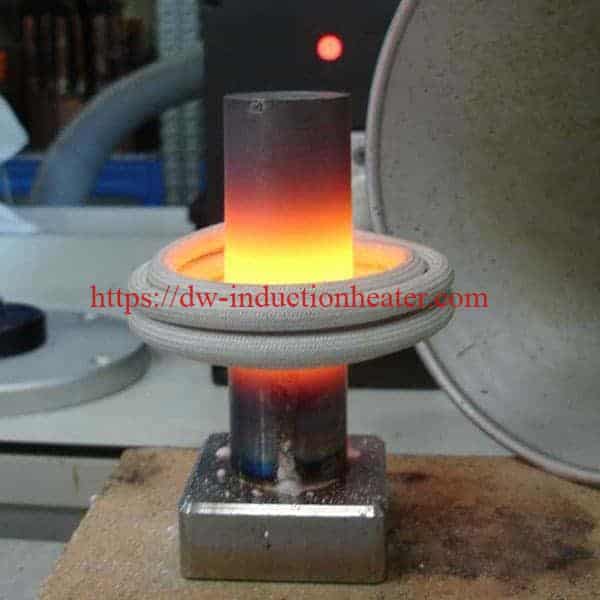
Induction Brazing Copper Lap Joints: A Reliable and Efficient Joining Method
Induction Brazing Copper Lap Joints: A Reliable and Efficient Joining Method
 https://dw-inductionheater.com/induction-brazing-copper-lap-joints-a-reliable-and-efficient-joining-method.html?feed_id=257134&_unique_id=67054340e8fab
2024年7月5日星期五
Brazing Copper Tube with Induction
 Brazing Copper Tube with Induction
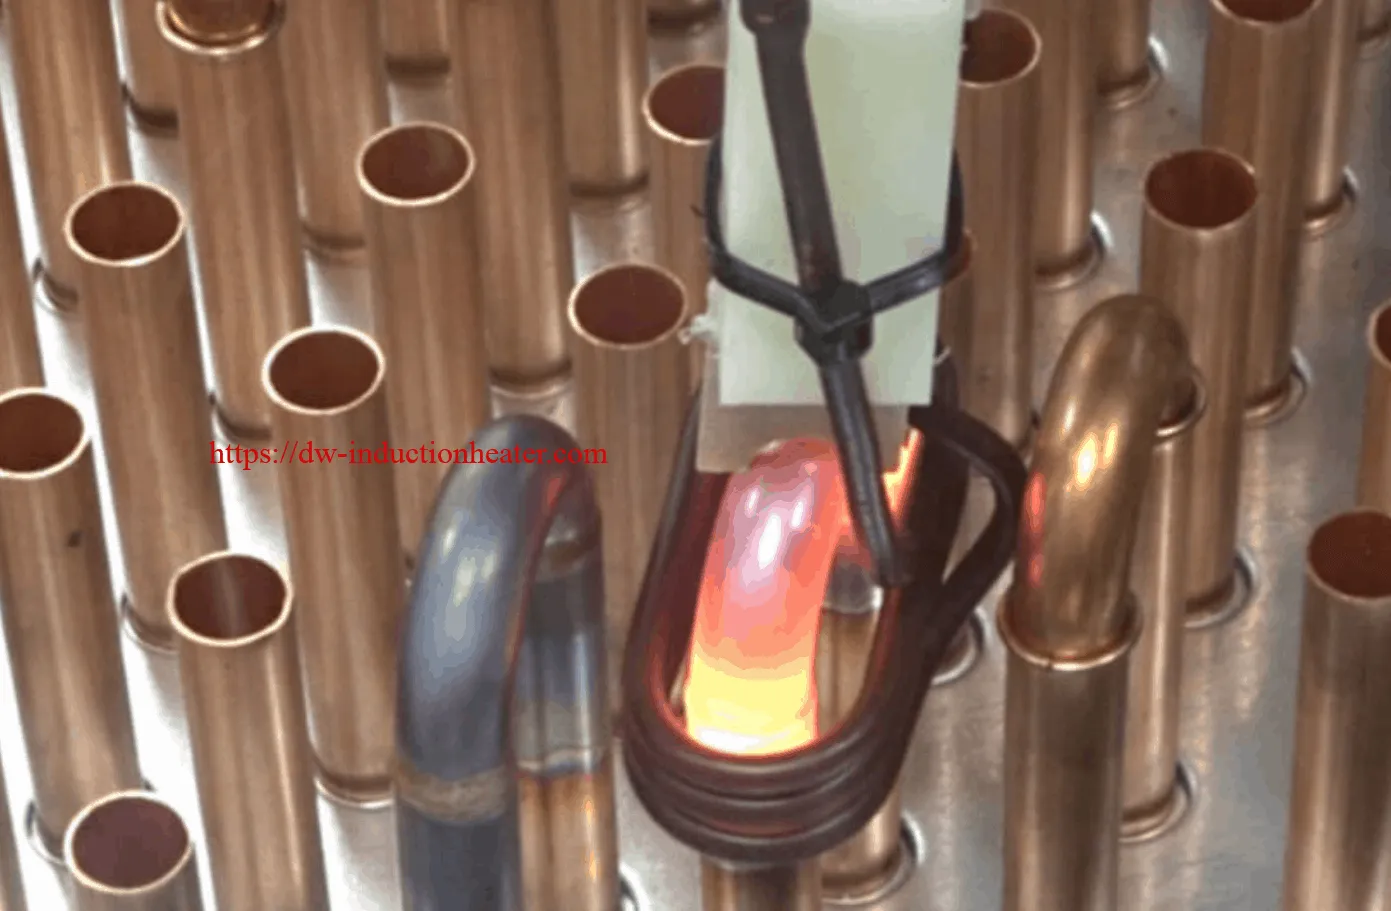
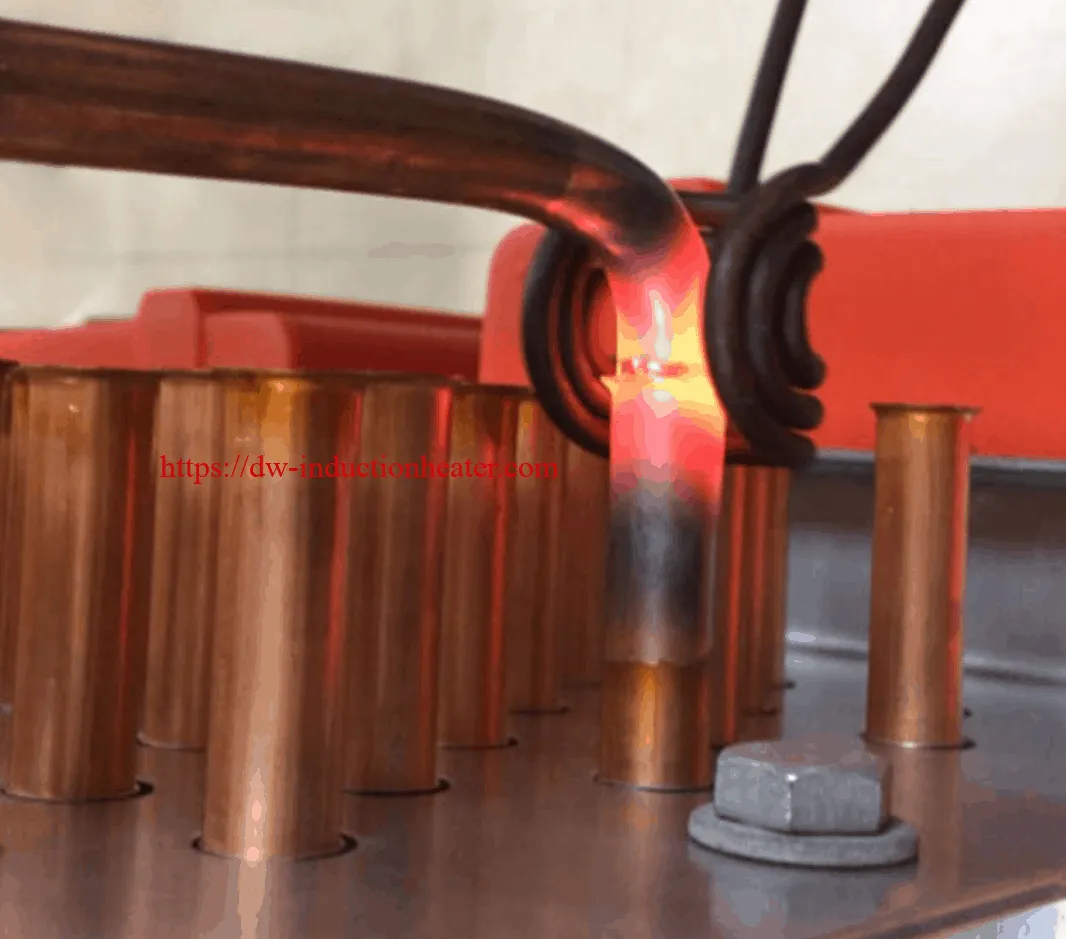
Objective: To braze a copper tube ( 3/8" OD by 2-4" long) into a 3/8" fitting in less than 10 seconds. Heating must take place in a channel type coil to allow for easy loading of parts.
Material Copper Tubing and Fitting with Braze and Stay Silv White Flux
Temperature 1300°F
Frequency 215 kHz
Equipment DW-UHF-10kw output solid state induction power supply equipped with a standard heat station containing eight 0.33 μF capacitors for a total of 0.66μF, a step down transformer, and a specifically designed induction heating coil.
Process DW-UHF-10kw solid state induction power supply was setup to achieve the following results: · 2.0 kW of power was directly loaded into the copper tube resulting in a heating time of 7.2 seconds to reach the necessary 13000F for brazing.
Results& Processing ease was achieved through the design of a unique channel type coil comprised of three turns of 1/8" copper.
 https://dw-inductionheater.com/brazing-copper-tube-with-induction.html?feed_id=252766&_unique_id=66886faf6bfe7
2024年7月4日星期四
Brazing Copper Tube to Brass Fitting With Induction
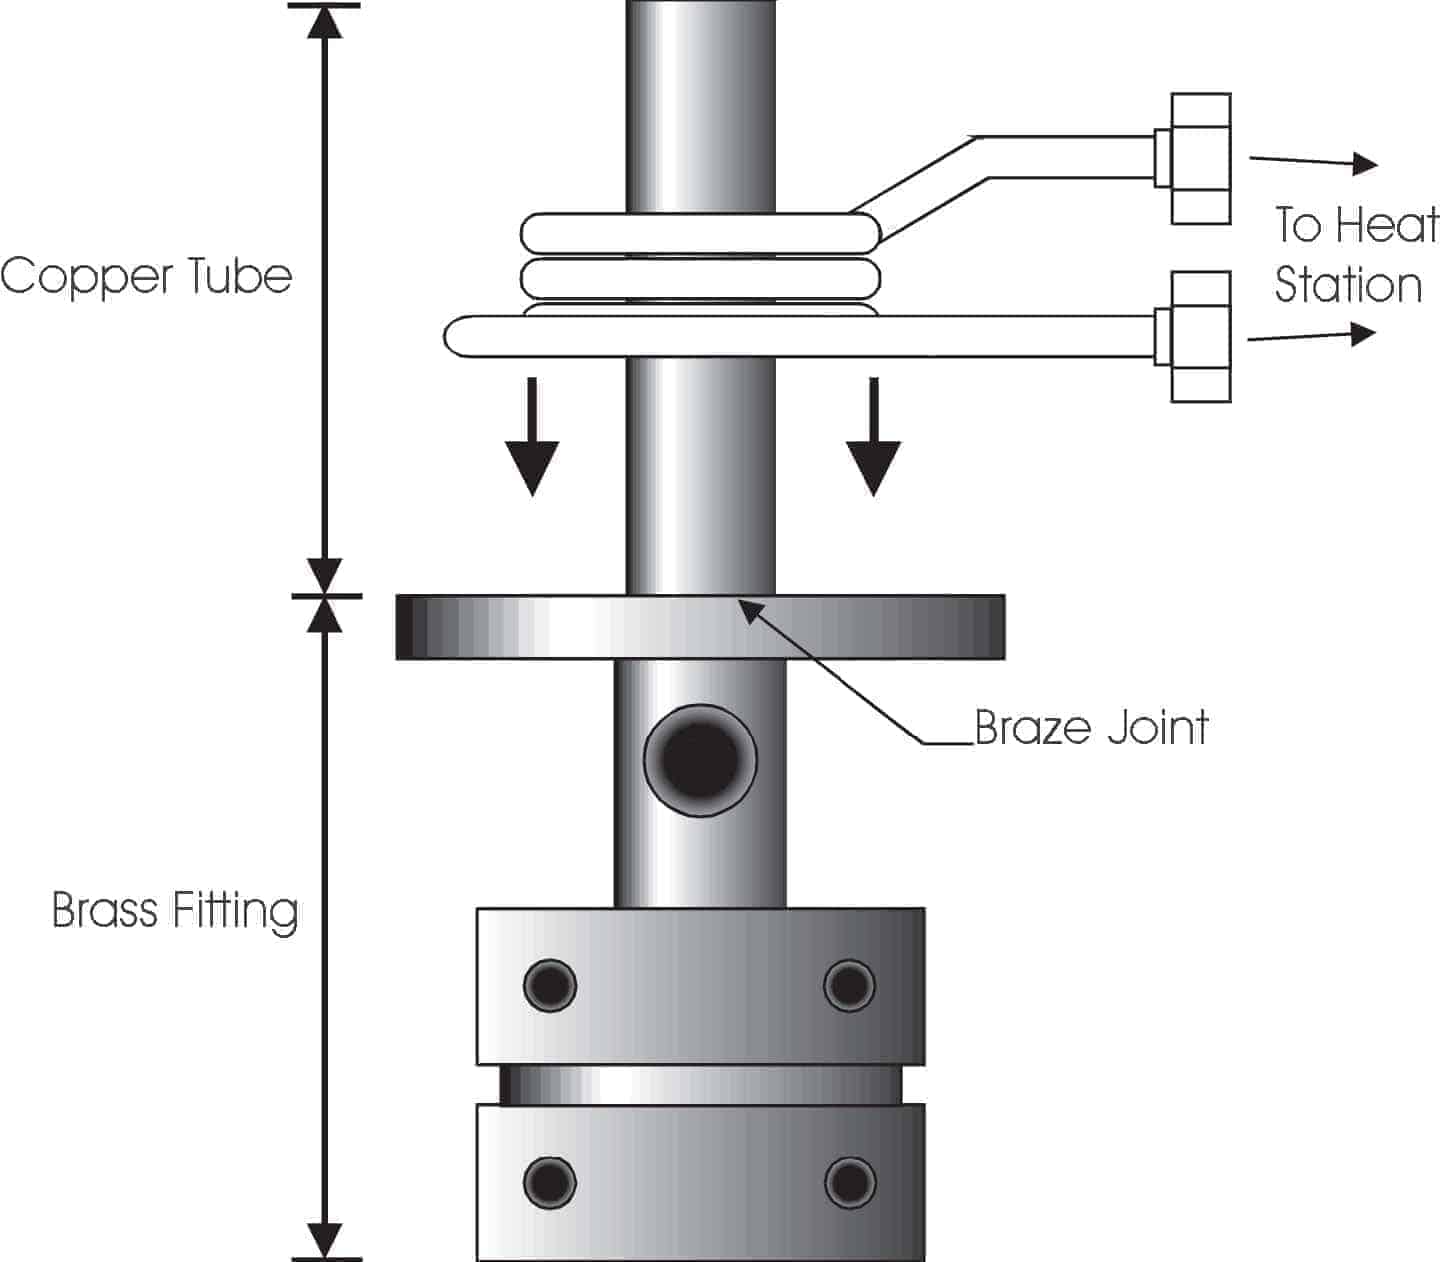 Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=252630&_unique_id=668702447dc78
2024年6月22日星期六
Brazing Copper Bars with Induction
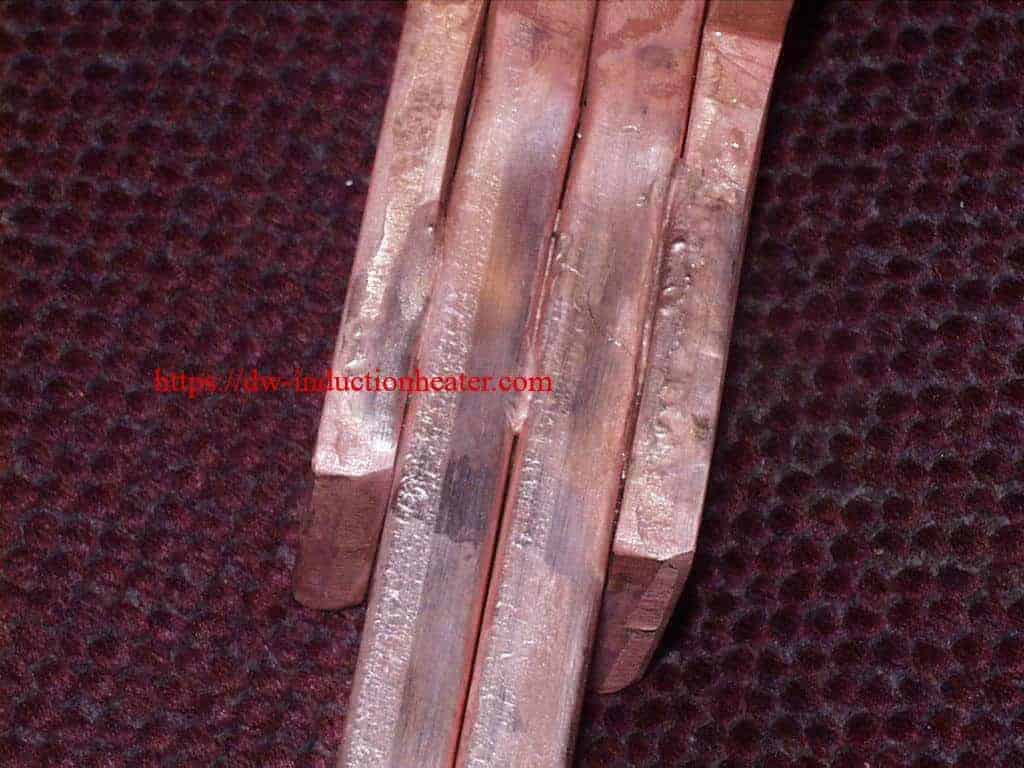 Brazing Copper Bars with Induction
Objective: To braze bus bar assemblies together
Material: • 2 copper bus bars 6" (152.4mm) wide, 2' (609.6mm)long, 2
copper bars 6"(152.4mm) wide, 18" (457.2)long & 3/8" (9.65mm) thick • braze shim preforms and white flux
Temperature: 1292 ºF (700 ºC)
Frequency: 80 kHz
Equipment • DW-UHF-60KW induction heating system, equipped with a
remote workhead containing eight 1.0 μF capacitors for a total of 2.0 μF.
• An induction heating coil, designed and developed specifically for this application
Process: A three-turn helical coil is used to heat the assembly. Three braze shim preforms are placed between the plates and white flux is applied to the assembly. It is heated for 5 minutes to evenly flow the braze alloy. A high current capable, aesthetic looking braze zone is produced.
Results/Benefits Induction heating provides:
• Consistently produced, quality parts
• Heat into the part that is divided equally between the copper pieces, allowing for even flow and consistent use of braze
• Hands-free operation that doesn't require skilled operators
https://dw-inductionheater.com/brazing-copper-bars-with-induction.html?feed_id=250876&_unique_id=6676957123c3e
2024年6月12日星期三
Induction Brazing Copper Assembly
 Induction Brazing Copper Assembly With High Frequency Heating Equipment
Objective Brazing a copper pivot assembly
Material Two copper uprights 2” (5cm) wide x 4” (10.2cm) high, copper base 3” (7.6cm) x 2” (5cm) and .5” (1.3mm) thick with 2 channels for the uprights to the slide into, braze shims and black flux
Temperature 1350 ºF (732 ºC)
Frequency 200 kHz
Equipment •DW-UHF-20kW induction heating system, equipped with a remote workhead containing two 1.0μF capacitors for a total of 0.5μF
• An induction heating coil designed and developed specifically for this application.
Process A three turn helical coil is used to heat the base of the assembly. The copper uprights and two braze shims are placed in the grooves in the base and black flux is applied. The assembly is placed in the coil and power is applied for 4 minutes to braze both the uprights in place.
Results/Benefits Induction heating provides:
• Rapid localized heat which can minimize oxidation and reduce cleaning after joining
• Consistent and repeatable joints
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
https://dw-inductionheater.com/induction-brazing-copper.html?feed_id=249677&_unique_id=666a7153614d4
2020年5月6日星期三
Induction Brazing Copper To Copper Parts
Objective
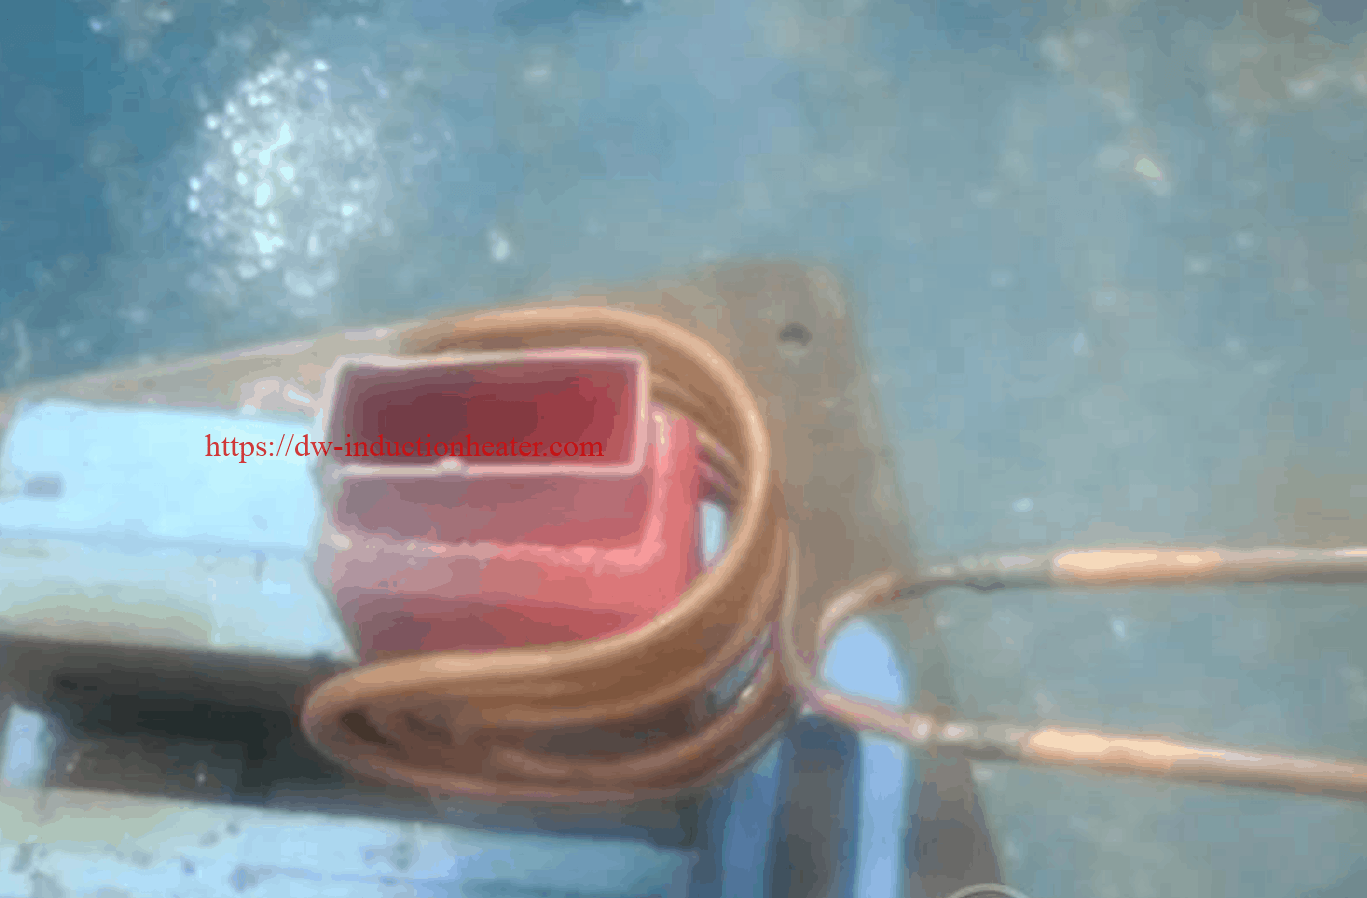
Induction Brazing Copper to Copper parts Spacer. The workpieces were heated to 2012˚F (1100˚C) in 1 minutes.

Recommended Equipment
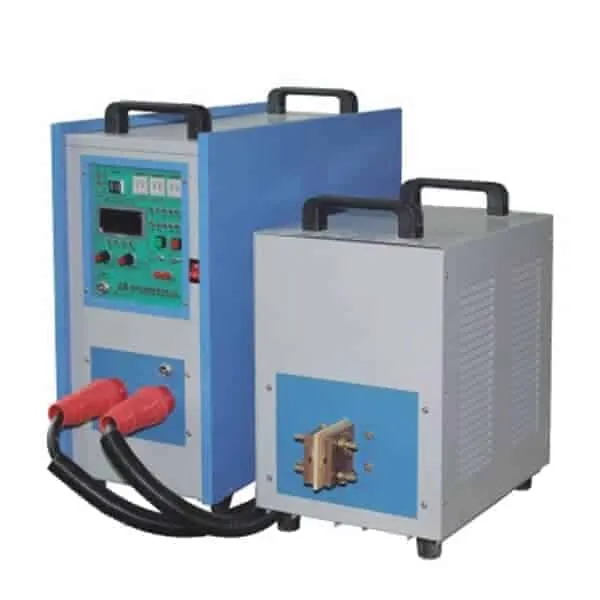
The recommended equipment for this application is the DW-HF-45kw induction heating machine
 Materials:
- Copper section: 0.55” thick x 1.97” long x 1.18” wide x 0.2” long (14 mm thick & 50 mm long x 30 mm wide x 5 mm long)
- Copper spacer: 0.55” thick x 1.57” long x 0.79” wide x 0.08” long (14 mm thick & 40 mm long x 20 mm wide x 2 mm long)
- Brazing alloy: 5% silver brazing rod
Power: induction heating power supplies up to 30 kW
Temperature: 2012˚F (1100˚C)
Time: 1 minutes

https://dw-inductionheater.com/wp-content/uploads/2020/05/High-frequency-Induction-Brazing-Copper-To-Copper-Parts.png?v=1588728728
https://dw-inductionheater.com/induction-brazing-copper-to-copper-parts.html
brazing, brazing copper, brazing induction, brazing machine manufacturer, High frequency Brazing copper, induction brazing, induction brazing copper, induction brazing copper to copper, induction brazing machine, induction brazing process, induction soldering
2020年5月2日星期六
induction brazing stainless steel to copper
Objective
Induction Brazing stainless steel to copper tubing. Objective is to evaluate induction brazing solution. Customer is looking to reduce defects and for a cleaner brazing environment.

Due to different pipe size and lower volume – evaluation is performed with a UBraze system.
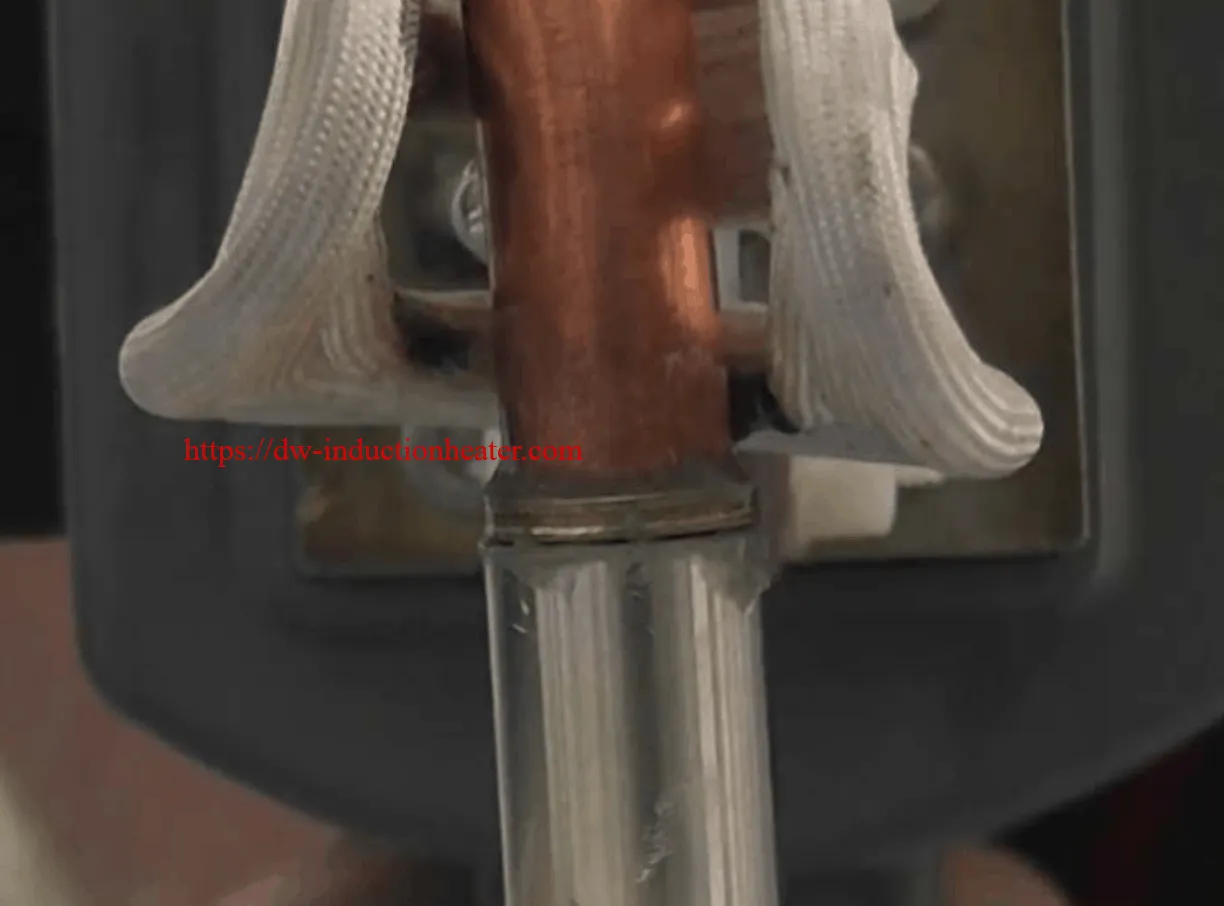
Test1
Equipment
DW-HF-25kw induction brazing machine
Materials
Copper to Stainless steel tube
Power: 12.5kW
Temperature: 1400ºF to 1600ºF (760ºC to 871ºC)
Time: 9 to 11 seconds
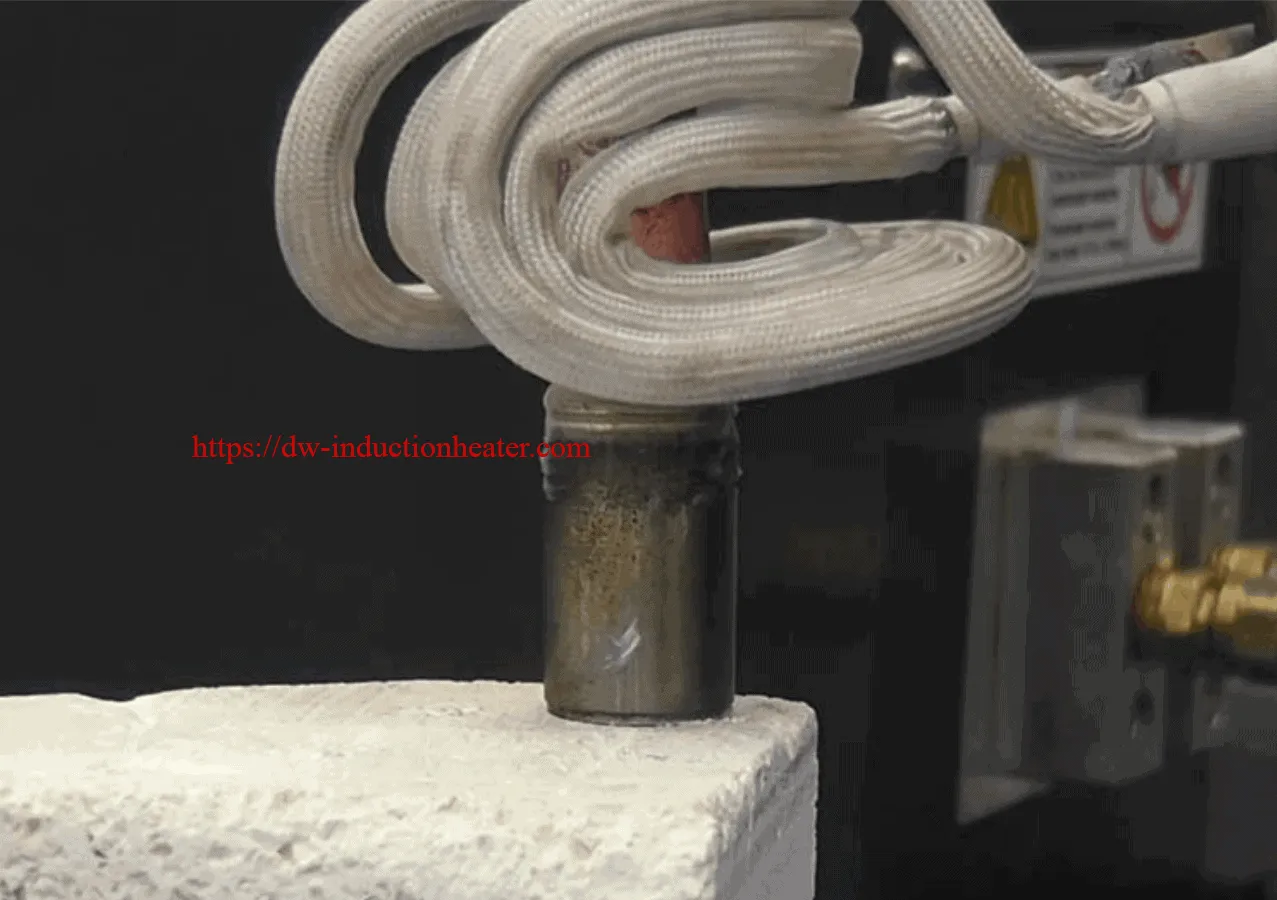
Test2
Equipment
DW-HF-25kw induction brazing machine
Materials
Copper to Stainless steel
Power: 12.5kW
Temperature: 1400ºF to 1600ºF (760ºC to 871ºC)
Time: 9 to 11 seconds
Results and Conclusions:
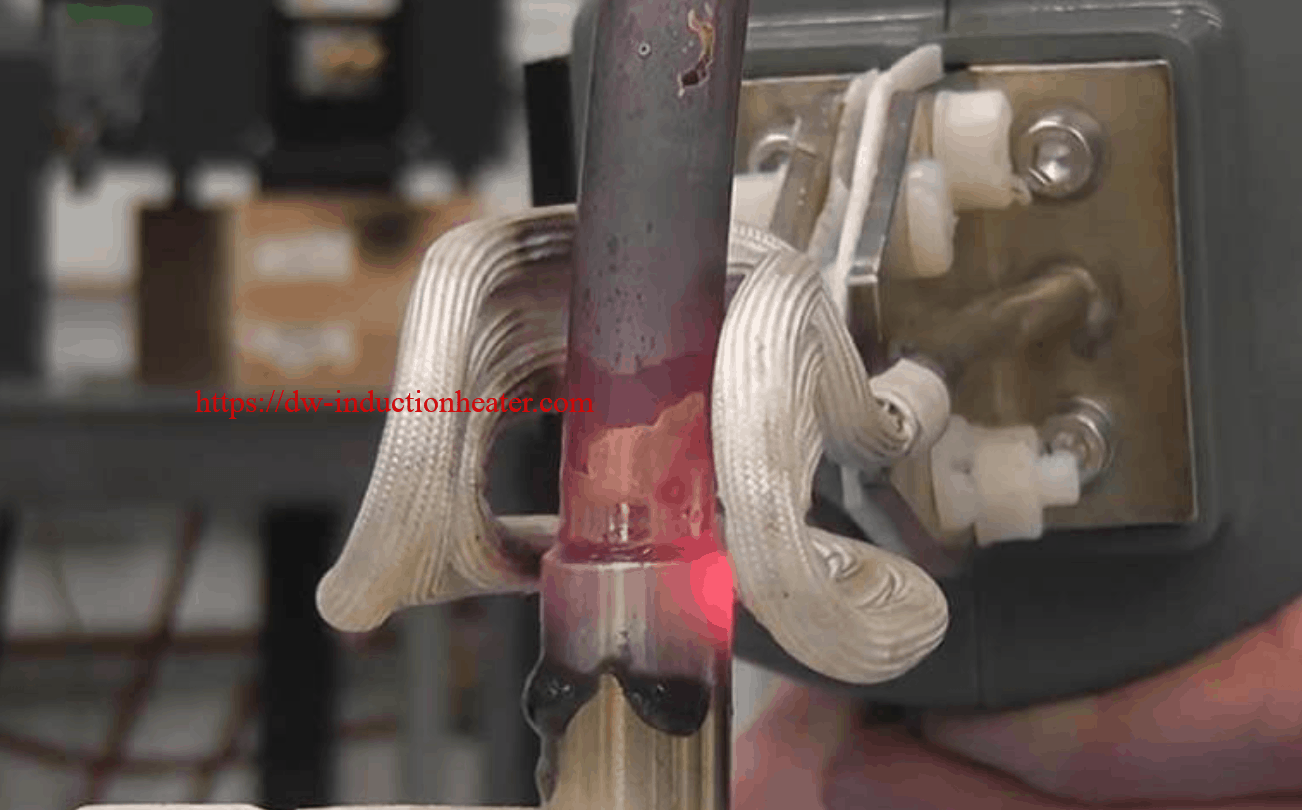
Induction brazing test with U open coil was able to braze the parts in 9 to 11 seconds for the full braze cycle.
Operator training with this setup will be minimal.


https://dw-inductionheater.com/wp-content/uploads/2020/05/induction-brazing-stainless-steel-to-coppr-pipes.png?v=1588384073
https://dw-inductionheater.com/induction-brazing-stainless-steel-to-copper.html
brazing copper system, brazing stainless steel, brazing stainless steel to copper, brazing stainless steel tube, handheld brazing copper, High frequency Brazing copper, High Frequency brazing stainless steel, induction brazing equipment, induction brazing machine, induction brazing stainless steel, induction brazing stainless steel unit, induction brazing system, induction brazing units, RF brazing stainless steel
2020年4月15日星期三
Induction Brazing copper to copper pipes
High Frequency Induction Brazing copper to copper pipes Process
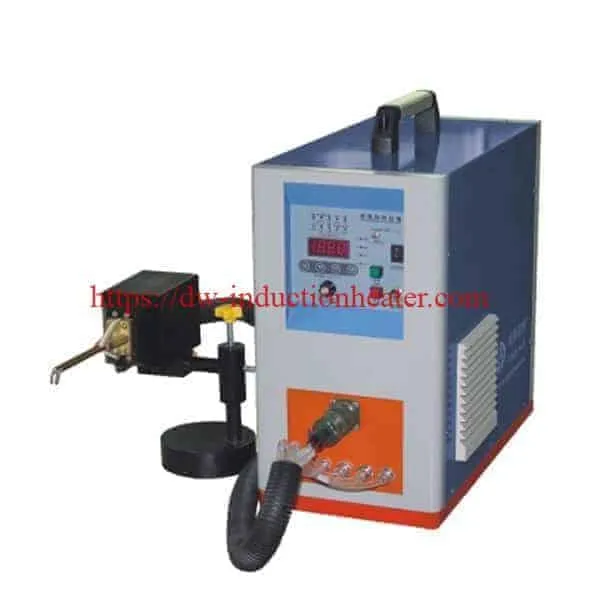
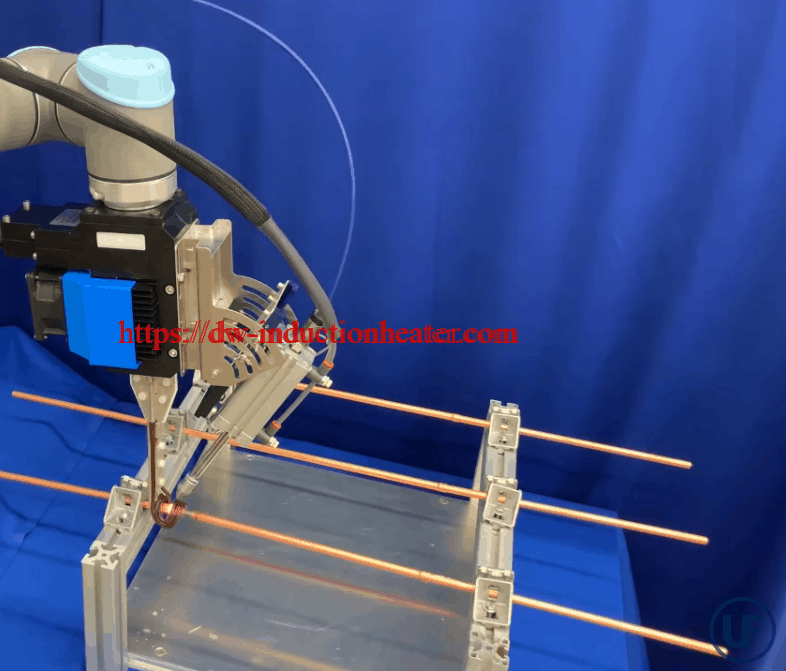
Objective: Induction Brazing copper to copper pipes
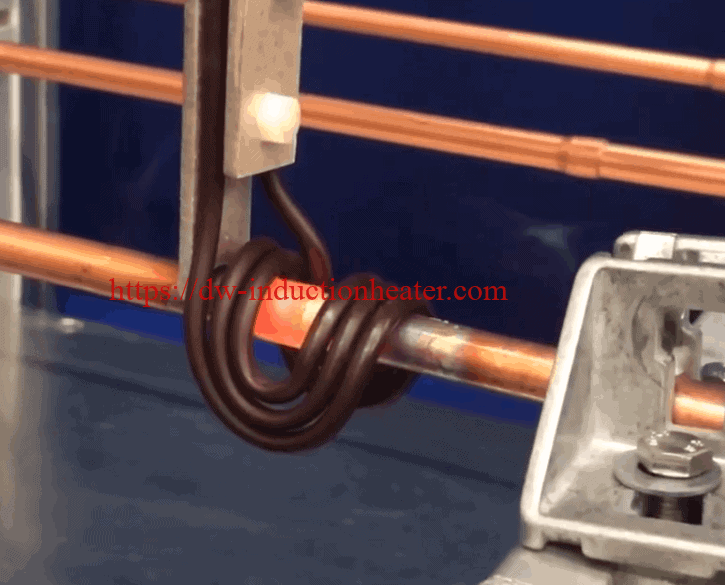
Equipment: DW-UHF-6KW-III handheld induction brazing heater
Materials: Six Copper pipes (9.5 mm)
Power: 6 kW
Temperature: 1475 °F/ 800°C
Time: 20 seconds
Process:
The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F.
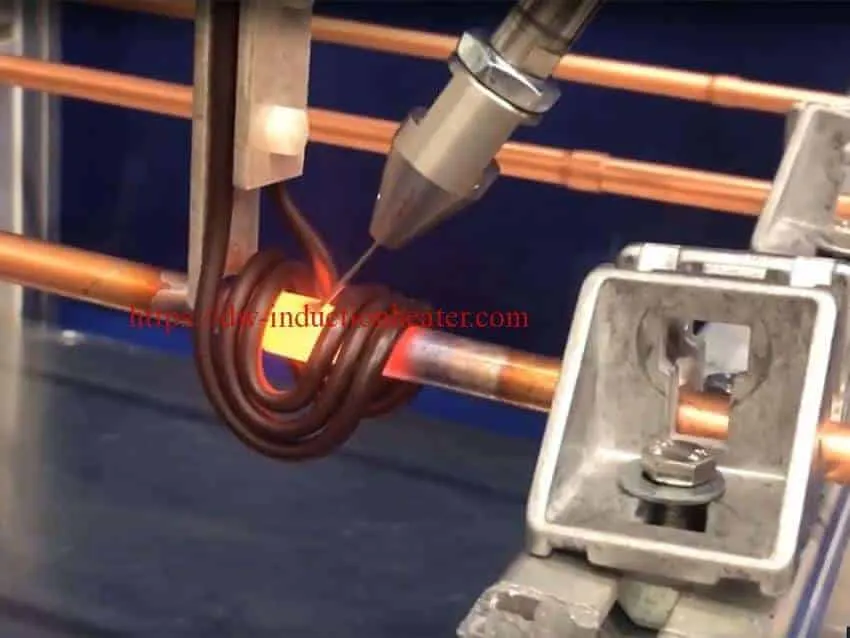 The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.
https://dw-inductionheater.com/wp-content/uploads/2020/04/Induction-Brazing-of-copper-to-copper-pipes-2.png?v=1586935463
https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html
brazing copper, Brazing copper heater, brazing copper system, copper brazing machine, copper pipes induction brazer, copper pipes induction brazing, High frequency Brazing copper, high frequency brazing copper tube, induction brazing copper, induction brazing copper pipes, induction copper brazing machine, RF brazing copper pipes
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.