 https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html?feed_id=267748&_unique_id=67959eabde320
2025年1月25日星期六
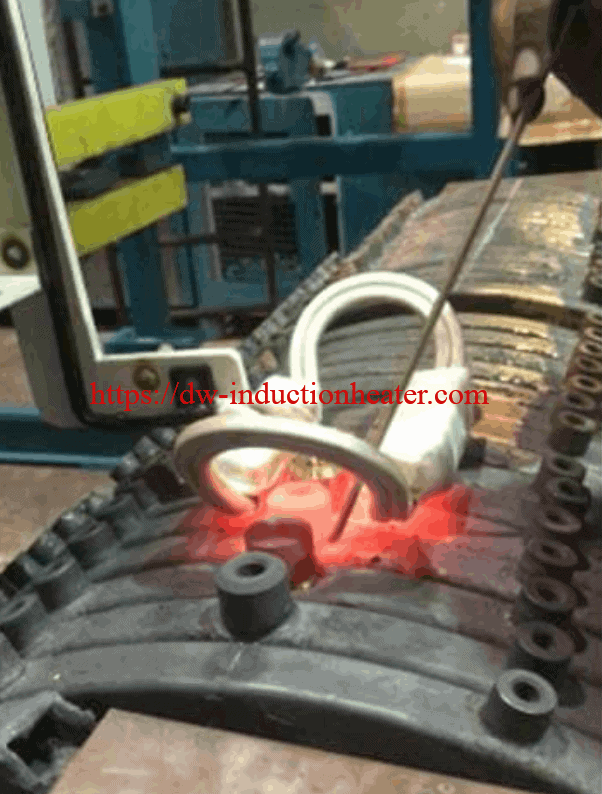
Induction Brazing Brass Studs to Copper Pipes
Induction Brazing Brass Studs to Copper Pipes
https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html?feed_id=267748&_unique_id=67959eabde320
https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html?feed_id=267748&_unique_id=67959eabde320

2024年10月8日星期二
Induction Brazing Copper Lap Joints: A Reliable and Efficient Joining Method
Induction Brazing Copper Lap Joints: A Reliable and Efficient Joining Method
 https://dw-inductionheater.com/induction-brazing-copper-lap-joints-a-reliable-and-efficient-joining-method.html?feed_id=257134&_unique_id=67054340e8fab
2024年7月4日星期四
Brazing Copper Tube to Brass Fitting With Induction
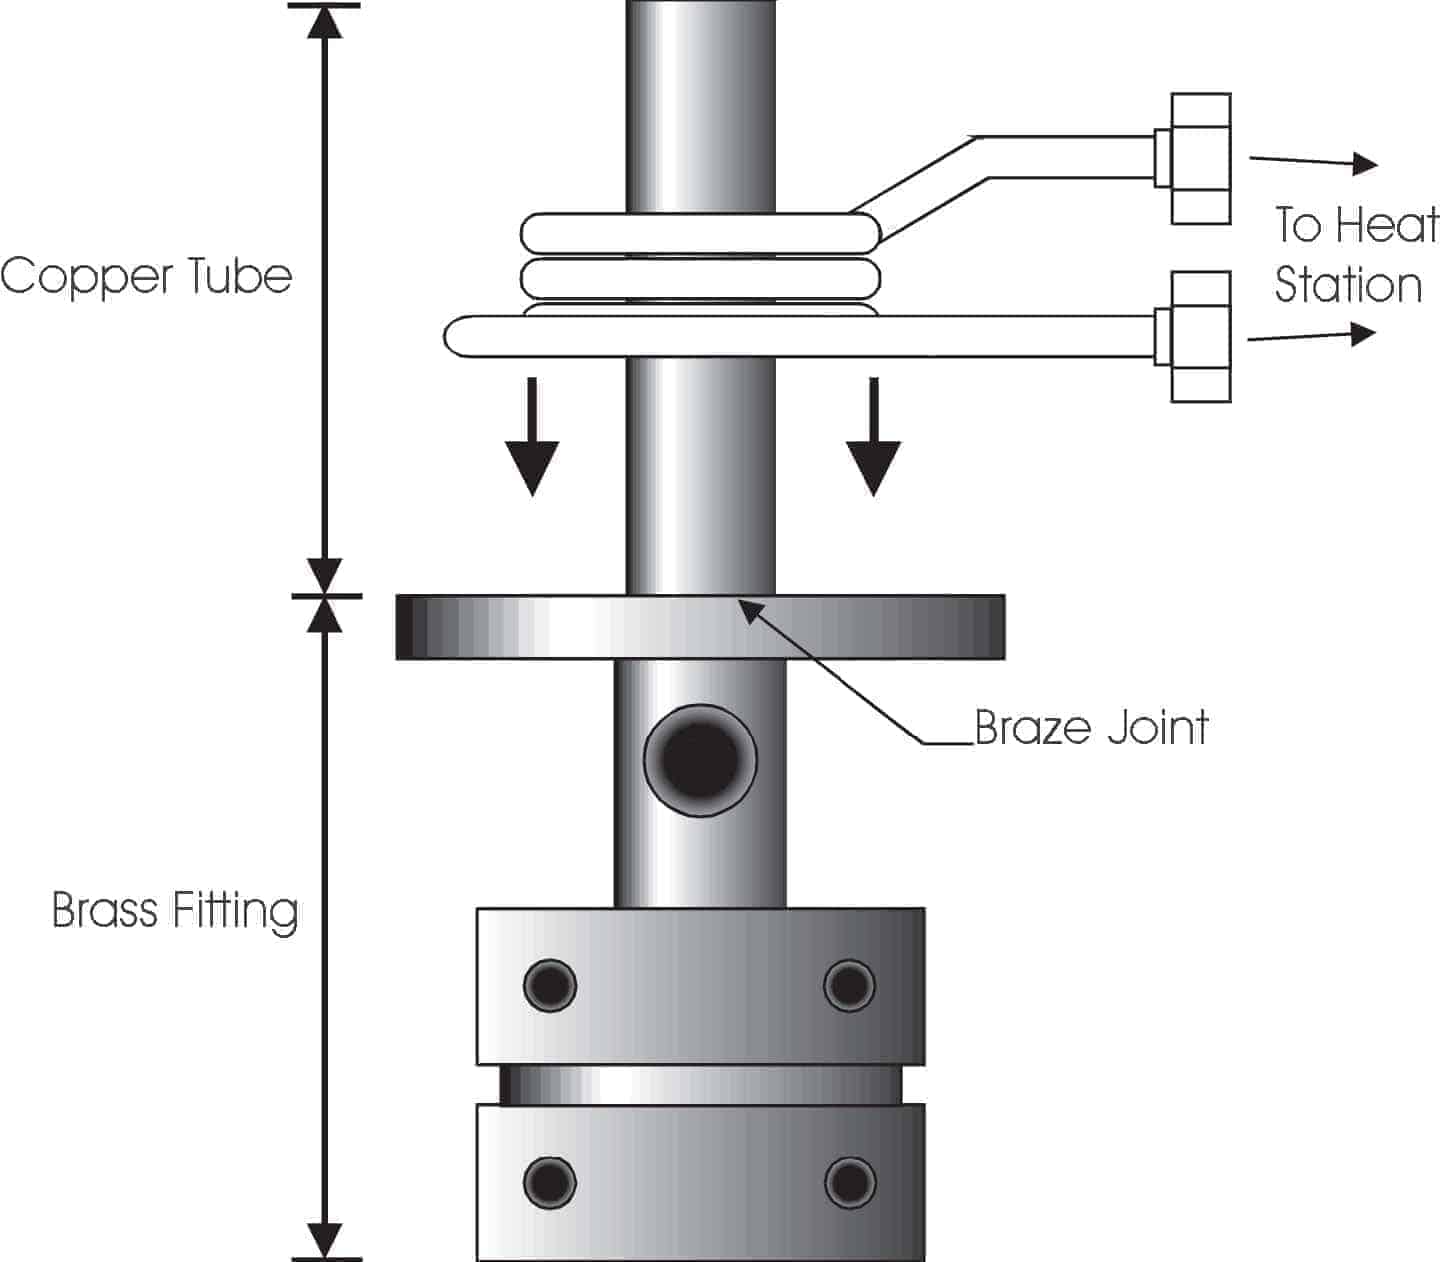 Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=252630&_unique_id=668702447dc78
2024年7月2日星期二
Brazing Brass Fittings With Induction
 Brazing Brass Fittings With Induction
Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm)
Material: Brass tubing Brass flange Braze rings Braze flux
Temperature :1382°F (750°C)
Frequency 200 kHz
Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application.
Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter.
Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes.
https://dw-inductionheater.com/brazing-brass-fittings-with-induction.html?feed_id=252426&_unique_id=6684ddcf51384
2024年6月25日星期二
Brazing Brass To Copper With Induction
 Brazing Brass To Copper With Induction
Objective: To braze brass end-connectors to copper tubes used in aircraft assembly air lines Material brass end connectors, copper tubes of different diameters
Temperature 1400 ºF 750°C
Frequency 350 kHz
Equipment DW-UHF-4.5KW induction heating system, including a three turn helical induction coil using two 0.33μF capacitors (total 0.66μF)
Process For smaller diameter parts, flux is applied to the entire part and the copper tube to brass joint is assembled using brazing preforms (allowing for the same amount of braze in each joint). The assembly is placed in the coil and heated for 20-30 seconds reaching a temperature of 1400°F. For larger copper tube assemblies, the same process is used, but the braze alloy is stick-fed to the joint to prevent the alloy from flowing out of the joint. A foot switch control is recommended to enable better control of the process.
Results/Benefits
Economy: Power is consumed during the heating only
Consistency: the results of braze joints are repeatable and uniform
https://dw-inductionheater.com/brazing-brass-to-copper-with-induction.html?feed_id=251408&_unique_id=667ade3ae905e
2024年6月13日星期四
Induction Brazing Brass Faucet
 Induction Brazing Brass Faucet
Objective Brazing two joints on a brass bathroom faucet assembly
Material Brass bathroom fittings 1” OD, brazing rings, flux
Temperature 1148 ºF (620 ºC)
Frequency 90 kHz
Equipment • DW-UHF-30 kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8.0 μF
• An induction heating coil designed and developed specifically for this application.
Process A two turn C shaped coil is used to braze the faucet assembly.
The braze rings are placed at the joint, the parts assembled and fluxed. The first braze joint is heated for 30 seconds and the braze ring flows. The assembly is rotated & the second joint is heated for 30 seconds to flow the braze ring. The two brazes are completed in 60 seconds.
Results/Benefits Induction heating provides:
• Faster, repeatable and consistent results
• Localized heat produces neat and clean joints
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
https://dw-inductionheater.com/induction-brazing-brass.html?feed_id=249745&_unique_id=666b28403ce61
2020年4月23日星期四
Induction Brazing Brass Studs to Copper Pipes
Induction Brazing Brass Studs to Copper Pipes
Objective:
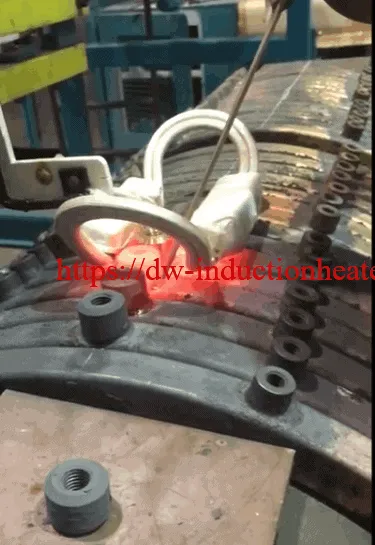
Induction brazing brass studs to copper pipes
The Client:
A manufacturer of coils for industrial heating applications.
Equipment:
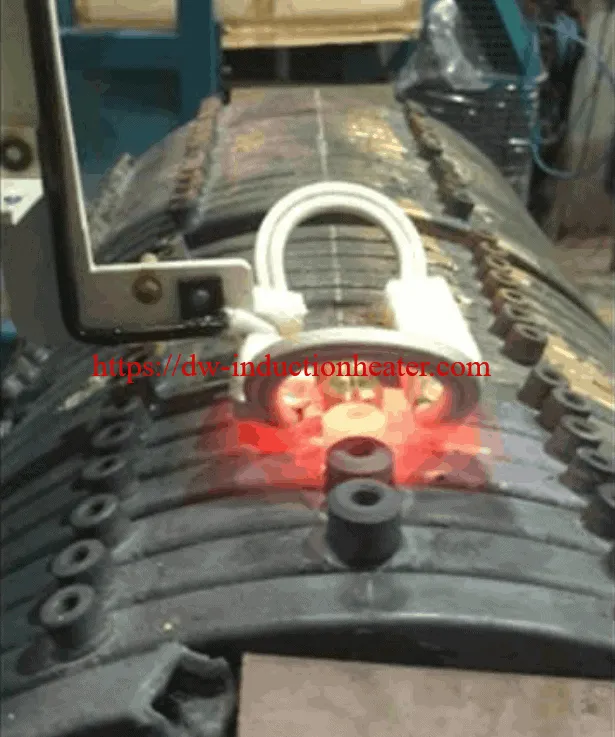
DW-UHF-40KW Induction Brazing Systems – two modules.
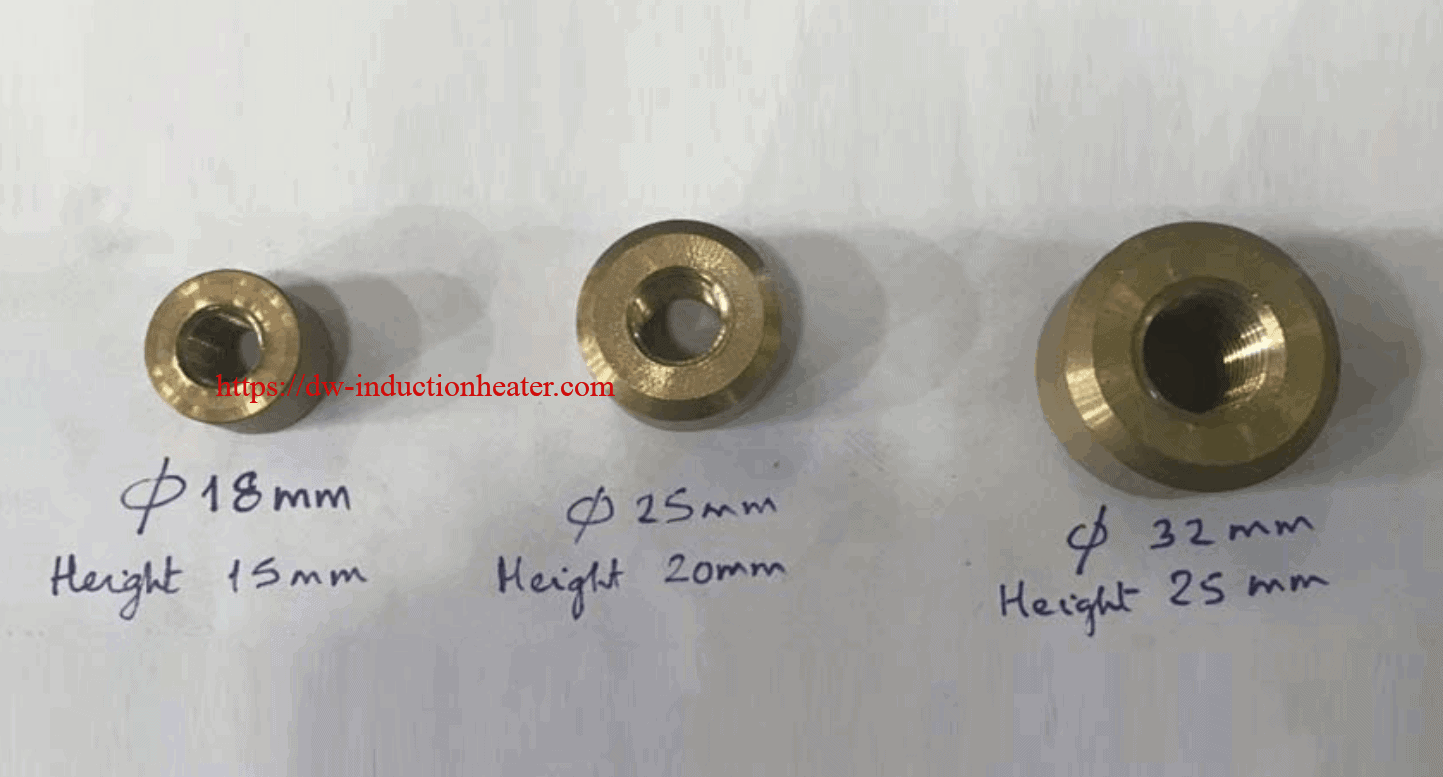
Materials: Brass stud ( size: 25mm diameter, 20 mm height )
Power: 30 kW
 The Process:
The main challenge during this induction brazing process is to ensure that the design of the coil is one that eases the technician to position it in the most convenient way. The induction coil should allow for the second stud to be pre-heated without melting the first one.
First, the electrolytic copper section is wound on a steel former by a gas torch while an equal spacing between the turns is maintained. Then, the copper turn is heated close to the required temperature and while the power is ON, the technician should make sure to manually position the brass stud with the brazing ring at the designated centre. During the process of brazing, the induction coil is moving at a speed of 58 mm per minute – 33 kW.
If the power is increased, the speed changes accordingly.
Results and Conclusions:
- A fast, clean and safe induction brazing process
- Guaranteed repeatability
- Precise control of time and temperature
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-brass-studs-to-copper.png?v=1587644202
https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html
brass studs brazing, brazing brass, brazing brass studs, brazing brass to copper, High Frequency Brazing brass, induction brazer, induction brazing brass, induction brazing copper, induction brazing copper system, induction brazing equipment, induction brazing system, induction brazing units
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.