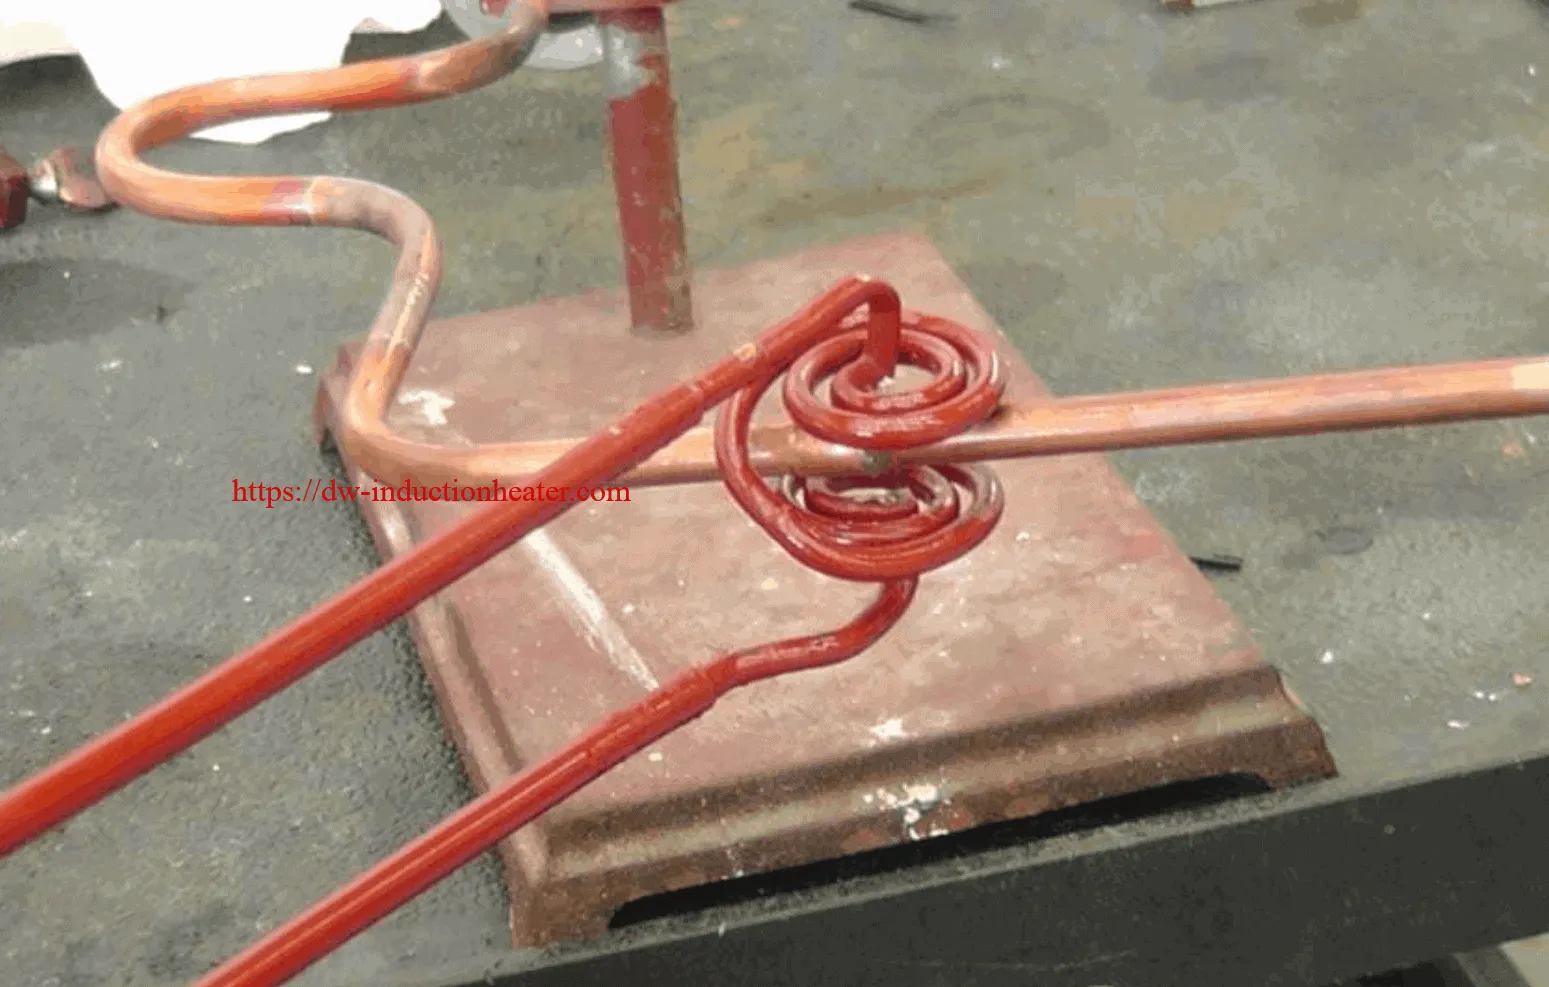
 https://dw-inductionheater.com/product/brazing-copper-tubing-with-induction?feed_id=269314&_unique_id=67ab120973c92
2025年2月11日星期二
Brazing Copper Tubing with Induction
Brazing Copper Tubing with Induction
https://dw-inductionheater.com/product/brazing-copper-tubing-with-induction?feed_id=269314&_unique_id=67ab120973c92
https://dw-inductionheater.com/product/brazing-copper-tubing-with-induction?feed_id=269314&_unique_id=67ab120973c92

2024年10月4日星期五
Electricmagnetic induction copper brazing machine
Electricmagnetic induction copper brazing machine
 https://dw-inductionheater.com/product/electricmagnetic-induction-copper-brazing-machine?feed_id=256728&_unique_id=66ffaf5ab436d
2024年7月9日星期二
Induction Brazing Copper Pipe Fittings
 Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
https://dw-inductionheater.com/induction-brazing-copper-pipe-fittings.html?feed_id=253405&_unique_id=668e2619682c9
2024年7月4日星期四
Brazing Copper Tube to Brass Fitting With Induction
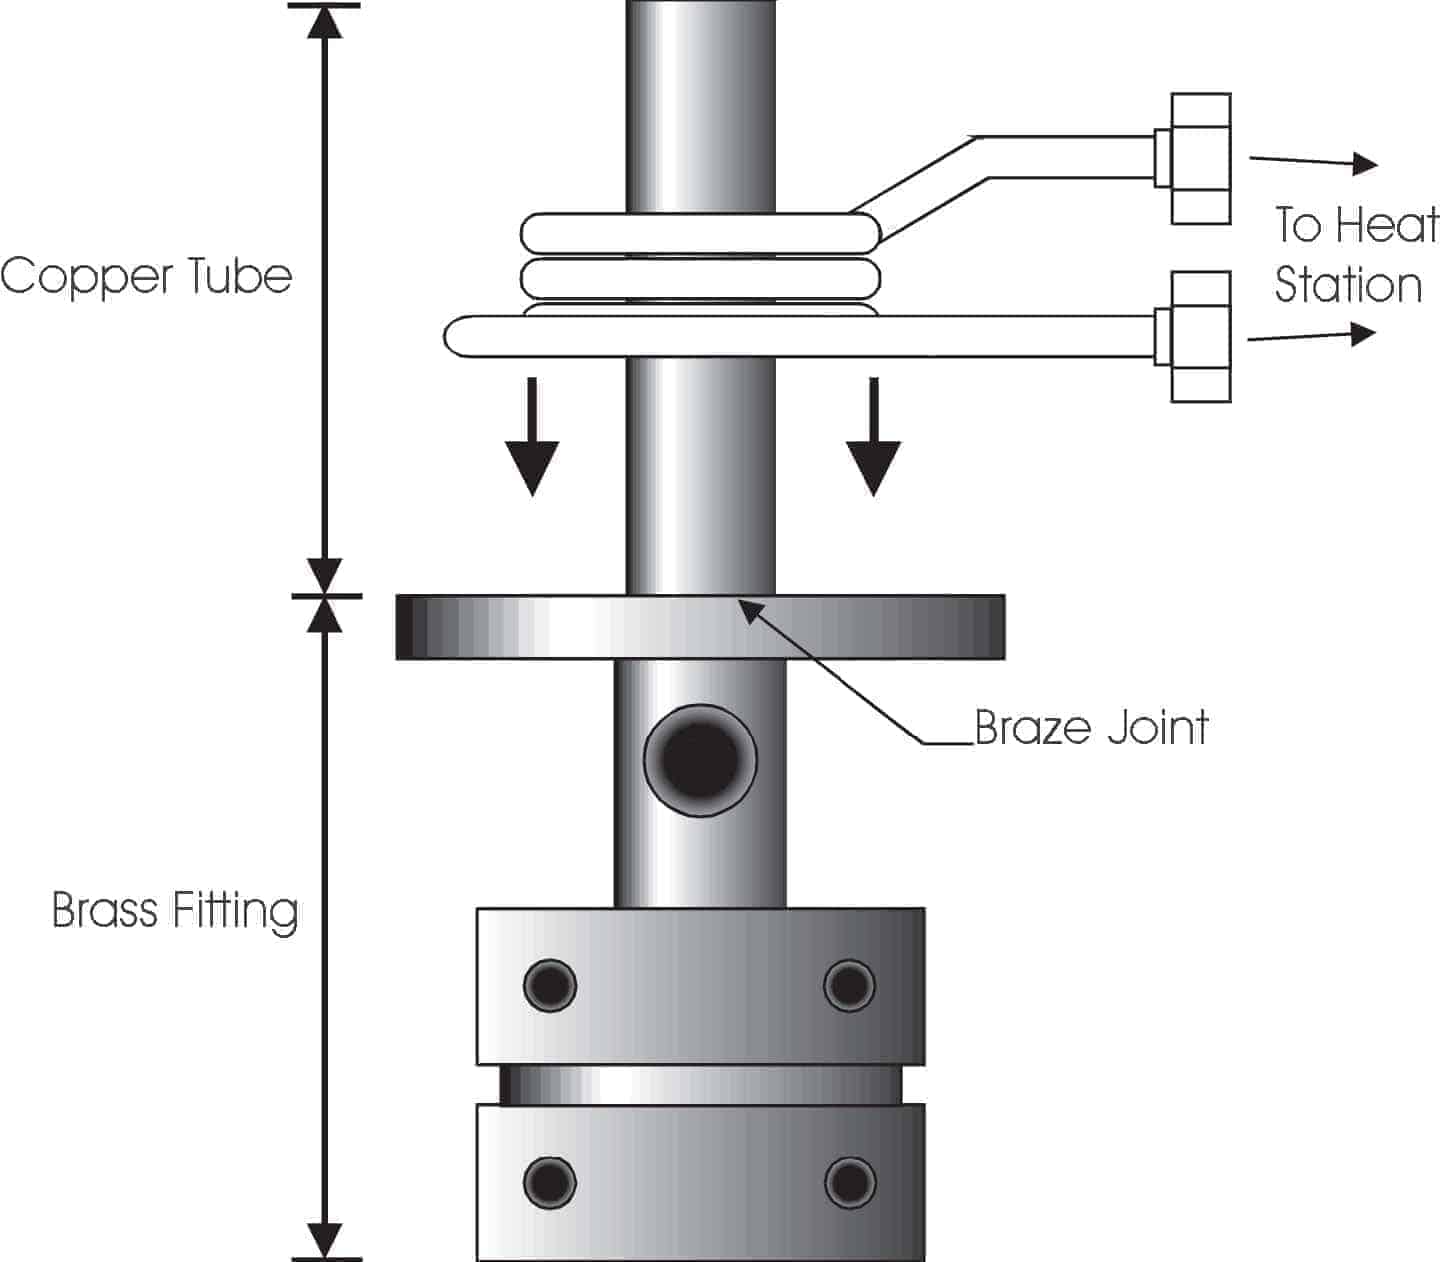 Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=252630&_unique_id=668702447dc78
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.