 https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=272794&_unique_id=67d6e793b2d58
2025年3月16日星期日
Brazing copper tube to brass fitting
Brazing copper tube to brass fitting
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=272794&_unique_id=67d6e793b2d58
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=272794&_unique_id=67d6e793b2d58

2025年2月25日星期二
Induction Brazing Copper Tube of Heat Exchanger
Induction Brazing Copper Tube of Heat Exchanger
 https://dw-inductionheater.com/induction-brazing-copper-tube-of-heat-exchanger.html?feed_id=270822&_unique_id=67be28da7d6f7
2025年2月21日星期五
Induction Brazing Copper Tube For Refrigeration
Induction Brazing Copper Tube For Refrigeration
 https://dw-inductionheater.com/induction-brazing-copper-tube-for-refrigeration.html?feed_id=270358&_unique_id=67b839f53075d
2025年2月18日星期二
Induction Handheld Brazing Copper To Steel Tube
Induction Handheld Brazing Copper To Steel Tube
 https://dw-inductionheater.com/induction-handheld-brazing-copper-to-steel-tube.html?feed_id=270097&_unique_id=67b542963dcc2
induction brazing copper and brass rods
induction brazing copper and brass rods
 https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61
2025年2月11日星期二
Brazing Copper Tubing with Induction
Brazing Copper Tubing with Induction
 https://dw-inductionheater.com/product/brazing-copper-tubing-with-induction?feed_id=269314&_unique_id=67ab120973c92
2025年1月29日星期三
Induction Brazing copper to copper pipes
Induction Brazing copper to copper pipes
 https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html?feed_id=268096&_unique_id=679a9050d61c9
2025年1月28日星期二
Induction Brazing Copper to Stainless Steel Process
Induction Brazing Copper to Stainless Steel Process
 https://dw-inductionheater.com/high-frequency-induction-brazing-copper-to-stainless-steel-process.html?feed_id=267951&_unique_id=6798963684669
2025年1月22日星期三
Induction Brazing Copper To Copper Parts
Induction Brazing Copper To Copper Parts
 https://dw-inductionheater.com/induction-brazing-copper-to-copper-parts.html?feed_id=267371&_unique_id=6790ad14138c7
2025年1月18日星期六
induction Brazing copper rods to brass strips
induction Brazing copper rods to brass strips
 https://dw-inductionheater.com/induction-brazing-copper-rods-to-brass-strips.html?feed_id=267023&_unique_id=678bbb8201bea
2024年11月27日星期三
2024年11月25日星期一

2020年5月23日星期六
induction Brazing copper rods to brass strips
Objective
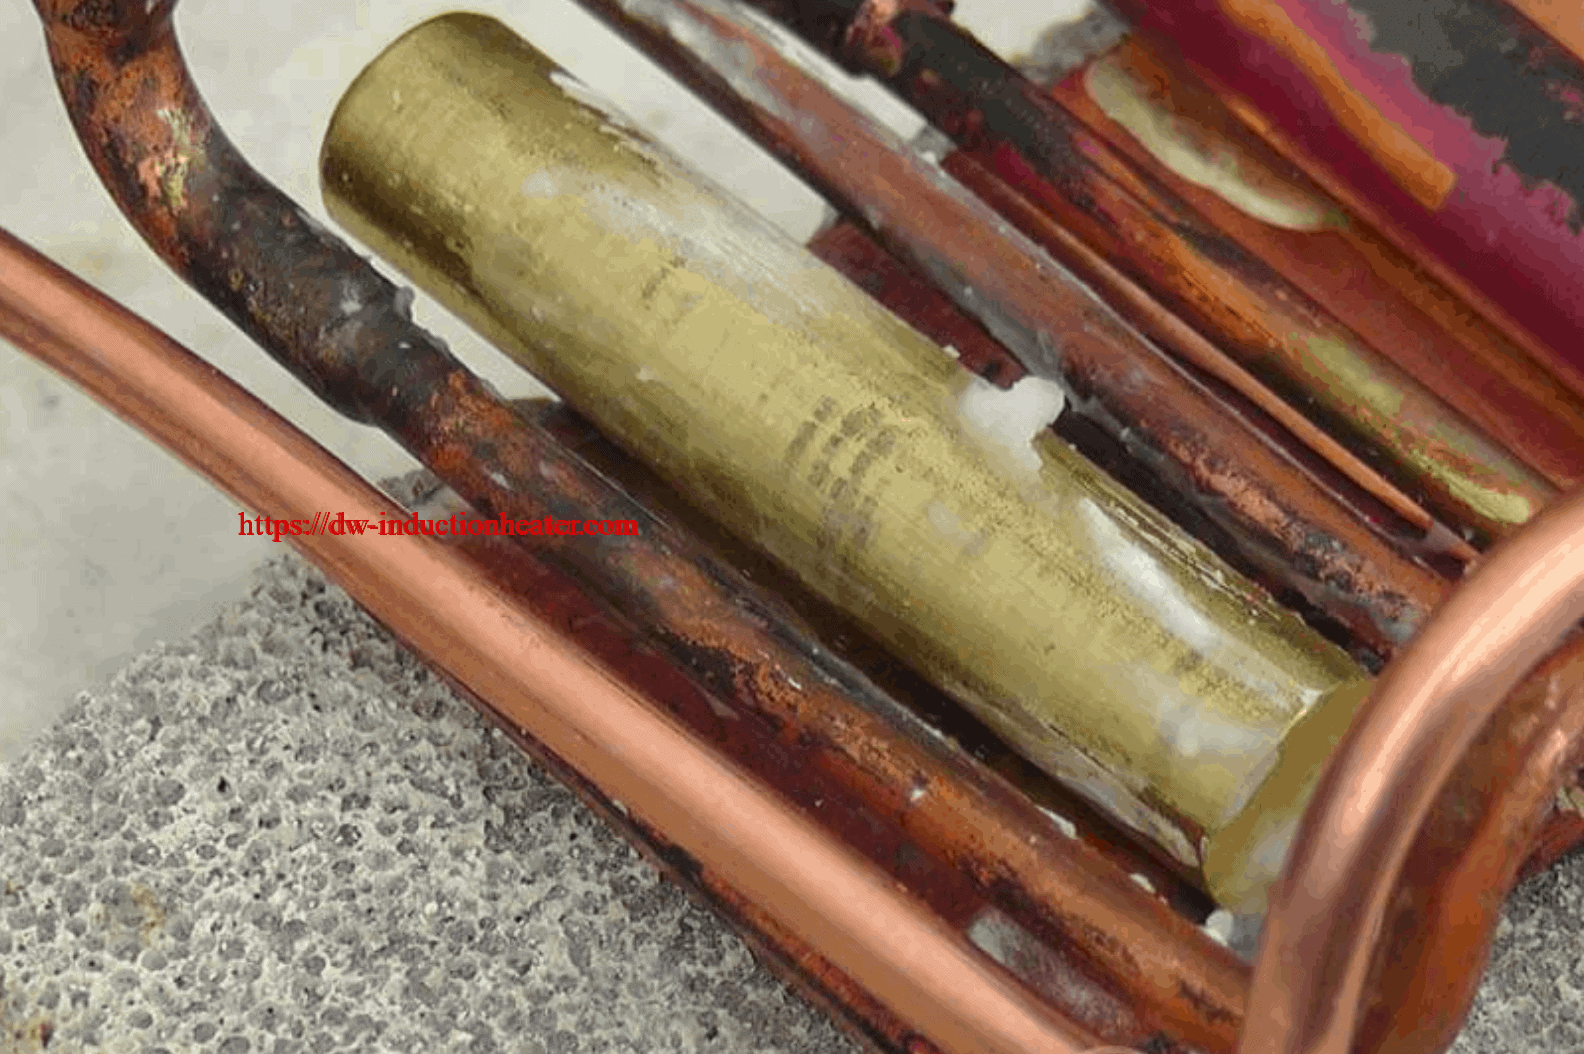
Induction Brazing copper rods to brass strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the induction brazing operation.

Equipment
DW-UHF-10KW INDUCTION BRAZING MACHINE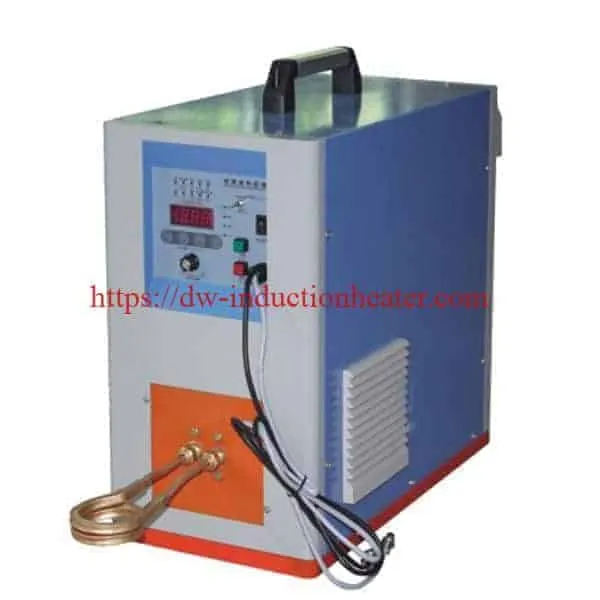
Two turn open end conveyor coil
Materials
• Copper coupon plate and copper rod
• Braze wire – EZ Flo 45
• Braze alloy – 45% Silver, 1/32 DIA

Key Parameters – TEST 1
Power: 7.2 kW
Temperature: Approximately 1350° F (732° C)
Time: Average time – 100 seconds
Process and Results:
For Induction brazing copper plate to copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up and heated for an average time of 100 seconds to flow the alloy and achieve the braze.

Key Parameters – TEST 1
Power: 6 kW
Temperature: Approximately 1350° F (732° C)
Time: Average time – 2.5 minutes
Process and Results:
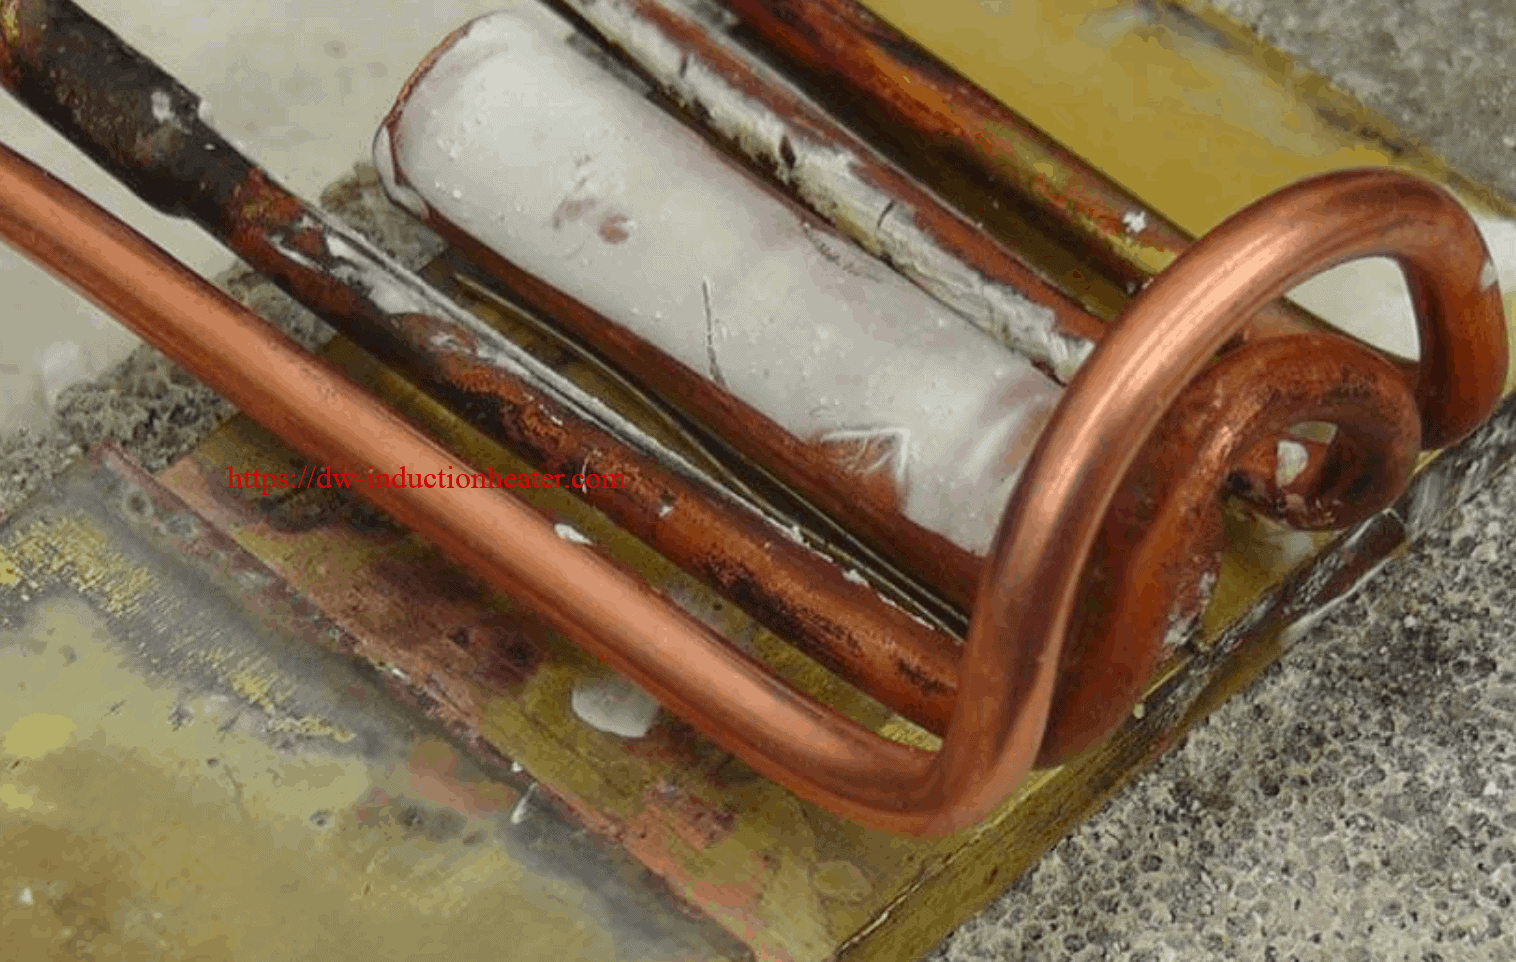
For Induction brazing copper rod to brass plate,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 2.5 minutes to flow the alloy and achieve the braze.
Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The induction heating coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Key Parameters – TEST 1
Power: 7.2 kW
Temperature: Approximately 1350° F (732° C)
Time: Average time – 2 minutes
Process and Results:
For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended.
The assemblies were set up and heated for an average time of 2 minutes to flow the alloy and achieve the braze.

Results/Benefits:
- induction brazing Strong durable joints
- Selective and precise heat zone, resulting in less part distortion and joint stress than welding
- Less oxidation
- Faster heating cycles
- More consistent results and suitability for large volume production, without the need for batch processing
- Safer than flame brazing
https://dw-inductionheater.com/wp-content/uploads/2020/05/induction-Brazing-copper-rods-to-brass-strips-1.png?v=1590226201
https://dw-inductionheater.com/induction-brazing-copper-rods-to-brass-strips.html
brass induction brazing machine, brass plate induction brazing, brazing copper, Brazing copper rods to brass, Brazing copper rods to brass machine, copper and brass brazing, copper rod brazing, hf brazing, induction brazing copper system
2020年5月6日星期三
Induction Brazing Copper To Copper Parts
Objective
Induction Brazing Copper to Copper parts Spacer. The workpieces were heated to 2012˚F (1100˚C) in 1 minutes.

Recommended Equipment
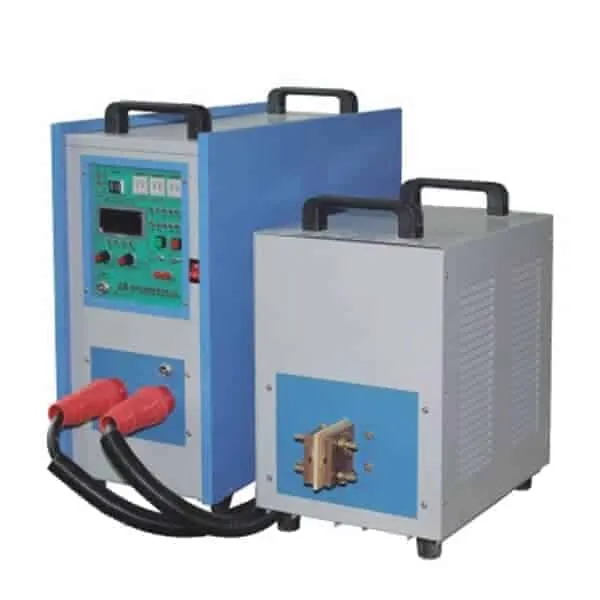
The recommended equipment for this application is the DW-HF-45kw induction heating machine
 Materials:
- Copper section: 0.55” thick x 1.97” long x 1.18” wide x 0.2” long (14 mm thick & 50 mm long x 30 mm wide x 5 mm long)
- Copper spacer: 0.55” thick x 1.57” long x 0.79” wide x 0.08” long (14 mm thick & 40 mm long x 20 mm wide x 2 mm long)
- Brazing alloy: 5% silver brazing rod
Power: induction heating power supplies up to 30 kW
Temperature: 2012˚F (1100˚C)
Time: 1 minutes

https://dw-inductionheater.com/wp-content/uploads/2020/05/High-frequency-Induction-Brazing-Copper-To-Copper-Parts.png?v=1588728728
https://dw-inductionheater.com/induction-brazing-copper-to-copper-parts.html
brazing, brazing copper, brazing induction, brazing machine manufacturer, High frequency Brazing copper, induction brazing, induction brazing copper, induction brazing copper to copper, induction brazing machine, induction brazing process, induction soldering
2020年4月18日星期六
Induction Brazing Copper to Stainless Steel Process
High Frequency Induction Brazing Copper to Stainless Steel Process Technology
Objective
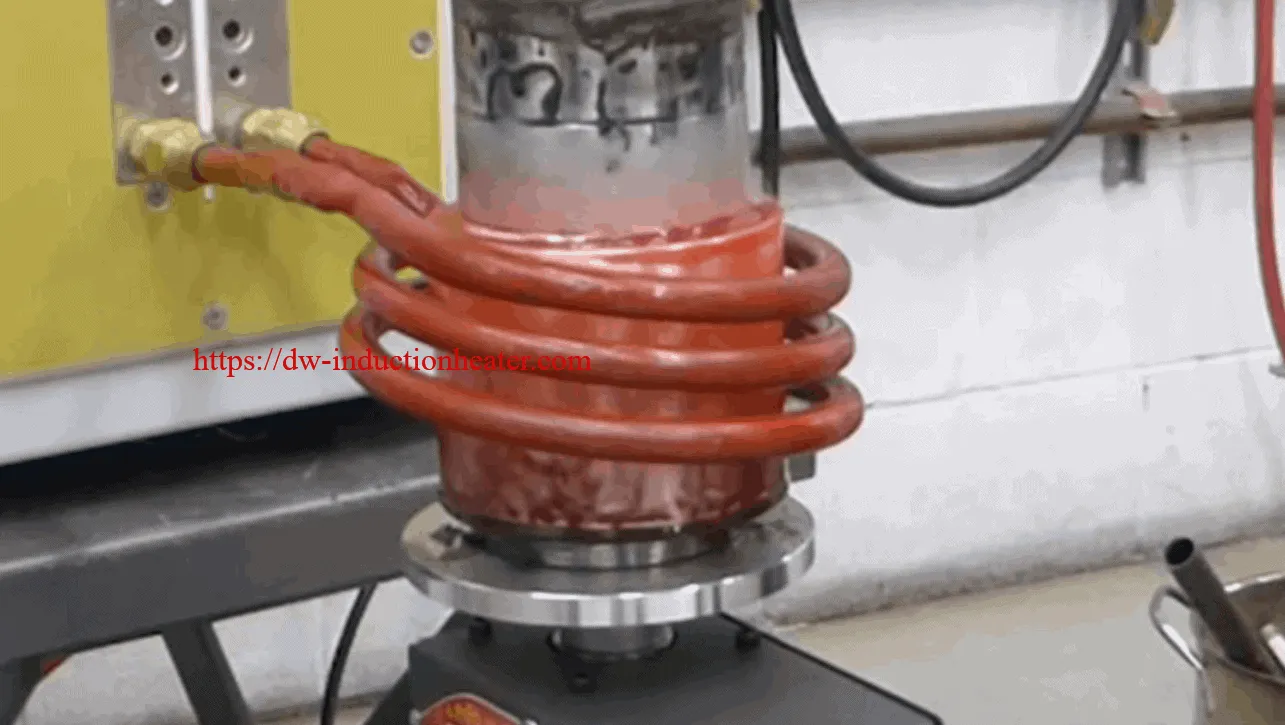
The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station
Equipment
DW-UHF-40KW Induction Heating Power Supply
HLQ custom coil
Key Parameters
Power: 23.65 kW
Temperature: Approximately 1300°F (704)°C
Time: 3.5 mins
 Materials
Cooper
4.5″ OD
0.5″ Wall Thickness
Stainless Steel 4″ OD
Braze Joint 2″

Process:
In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits:
The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-copper-to-stainless-steel.jpg?v=1587209214
https://dw-inductionheater.com/induction-brazing-copper-to-stainless-steel-process.html
brazing copper, brazing copper system, brazing copper to stainless steel, copper to stainless steel brazing, copper to stainless steel HF brazing, HF brazing machine, HF induction brazing, high frequency brazing, High frequency Brazing copper, induction brazing
Induction Brazing Copper to Stainless Steel Process
High Frequency Induction Brazing Copper to Stainless Steel Process Technology
Objective
The objective of this induction brazing copper to stainless steel using a DW-UHF-40kw induction heating power supply with a custom heating station
Equipment
DW-UHF-40KW Induction Heating Power Supply
HLQ custom coil
Key Parameters
Power: 23.65 kW
Temperature: Approximately 1300°F (704)°C
Time: 3.5 mins
Materials
Cooper
4.5″ OD
0.5″ Wall Thickness
Stainless Steel 4″ OD
Braze Joint 2″
Process:
In order to start the induction brazing of copper to stainless steel the part was centered on a turntable. The induction brazing coil was then positioned around the copper because it is less efficiently heated than stainless steel. As the part was rotating, approximately 25kW were being applied to the coil. Once the brazed joint was close to the ideal brazing temperature, the alloy was hand fed onto the joint. The induction brazing of cooper to stainless steel was completed and successful.
Results/Benefits:
The result of the induction brazing copper to stainless steel application testing was a positive one, the induction brazing was completed and the copper to stainless steel was done seamlessly. This test resulted in high quality and repeatability of the brazed joints, increased productivity and control of the time and temperature.
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-copper-to-stainless-steel.jpg?v=1587209214
https://dw-inductionheater.com/induction-brazing-copper-to-stainless-steel-process.html
brazing copper, brazing copper system, brazing copper to stainless steel, copper to stainless steel brazing, copper to stainless steel HF brazing, HF brazing machine, HF induction brazing, high frequency brazing, High frequency Brazing copper, induction brazing
2020年4月15日星期三
Induction Brazing copper to copper pipes
High Frequency Induction Brazing copper to copper pipes Process
Objective: Induction Brazing copper to copper pipes
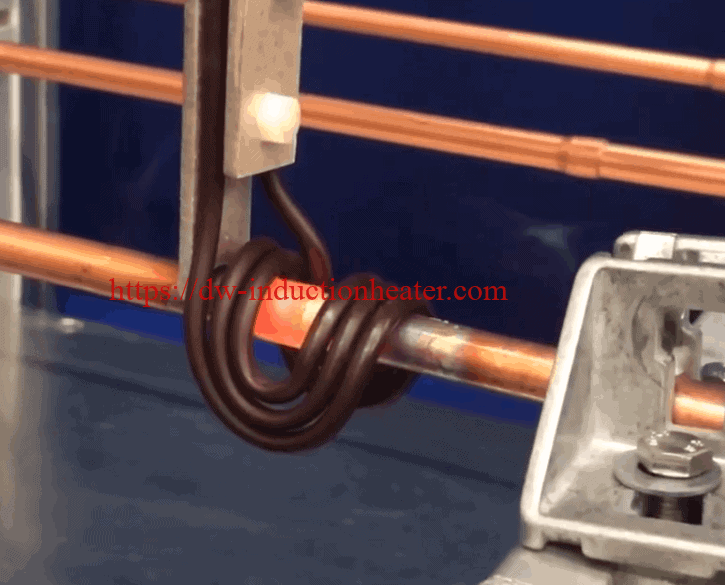
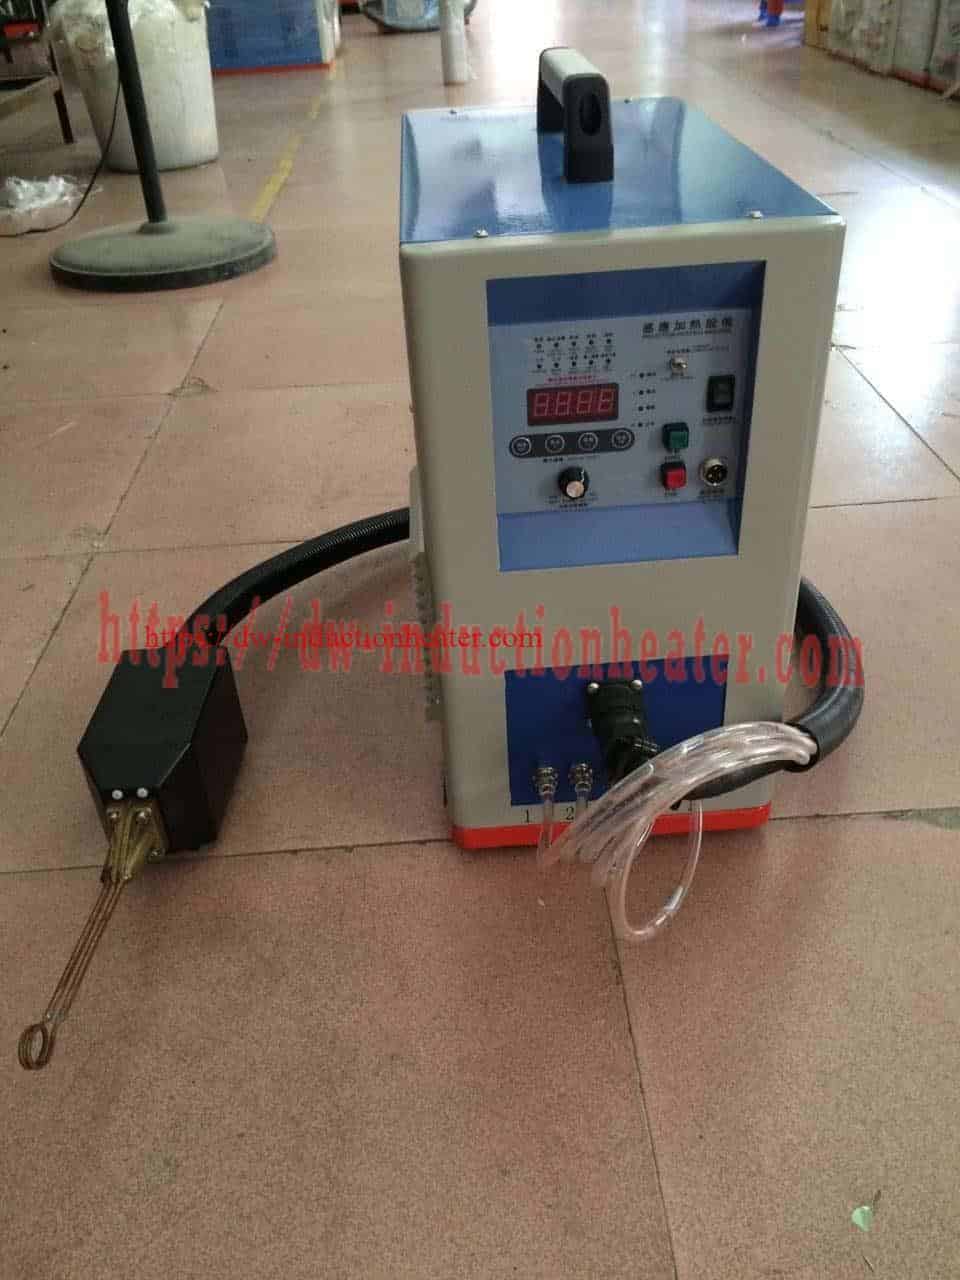
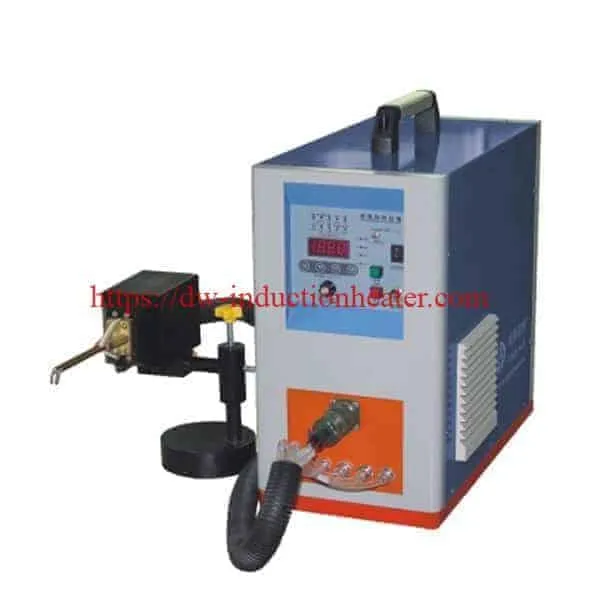
Equipment: DW-UHF-6KW-III handheld induction brazing heater
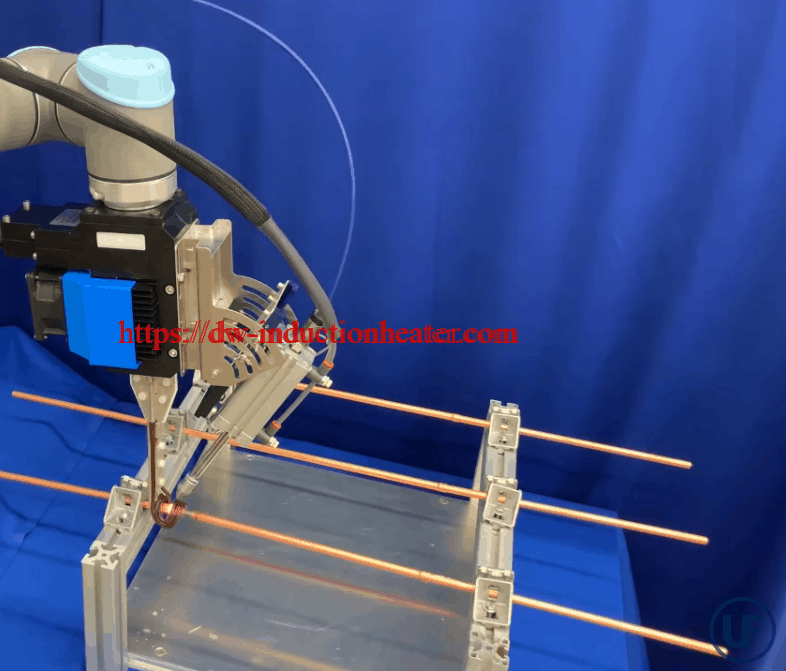
Materials: Six Copper pipes (9.5 mm)
Power: 6 kW
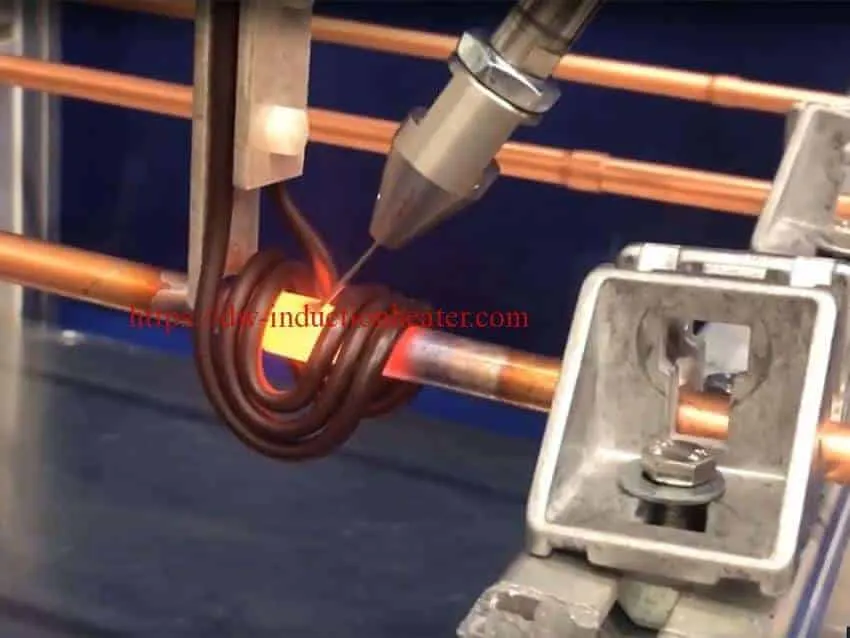
Temperature: 1475 °F/ 800°C
Time: 20 seconds
Process:
The DW-UHF-6KW-III handheld induction brazing system with robot can automatically induction braze multiple joints located in predefined positions. For this brazing application a wire feeder was mounted to the DW-UHF-6KW-III induction brazing heater, which feds the alloy onto the copper joints. A nitrogen nozzle was also added to reduce oxidization of the joints, this helps minimize the brazed joints cleaning procedure. The robotic system is programmed to move to each joint and apply power for a pre-programmed amount of time. This ensures a repeatable and reliable brazing process. The induction brazing of copper to copper was performed successfully within 20 seconds per joint at 1475 °F.
 The DW-UHF-6KW-III handheld induction brazing heater is ideal for flameless brazing of refrigerator compressors, heat exchangers, home appliance components and complex HVAC assemblies.
https://dw-inductionheater.com/wp-content/uploads/2020/04/Induction-Brazing-of-copper-to-copper-pipes-2.png?v=1586935463
https://dw-inductionheater.com/induction-brazing-copper-to-copper-pipes.html
brazing copper, Brazing copper heater, brazing copper system, copper brazing machine, copper pipes induction brazer, copper pipes induction brazing, High frequency Brazing copper, high frequency brazing copper tube, induction brazing copper, induction brazing copper pipes, induction copper brazing machine, RF brazing copper pipes
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.