 https://dw-inductionheater.com/induction-brazing-basics.html?feed_id=273287&_unique_id=67ddcc8c394db
2025年3月21日星期五
Induction Brazing Basics
Induction Brazing Basics
https://dw-inductionheater.com/induction-brazing-basics.html?feed_id=273287&_unique_id=67ddcc8c394db
https://dw-inductionheater.com/induction-brazing-basics.html?feed_id=273287&_unique_id=67ddcc8c394db

2025年3月20日星期四

2025年3月16日星期日
Brazing copper tube to brass fitting
Brazing copper tube to brass fitting
 https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=272794&_unique_id=67d6e793b2d58
2025年3月3日星期一
Brazing Copper T-Pipes with Induction Heating
Brazing Copper T-Pipes with Induction Heating
 https://dw-inductionheater.com/brazing-copper-t-pipes-with-induction-heating.html?feed_id=271487&_unique_id=67c67b64b06ce
2025年2月21日星期五
High frequency induction brazing steel tube to steel fitting
High frequency induction brazing steel tube to steel fitting
 https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90
2025年2月20日星期四
Induction Brazing Copper T Pipe With Induction Heating Machine
Induction Brazing Copper T Pipe With Induction Heating Machine
 https://dw-inductionheater.com/induction-brazing-copper-t-pipe-with-induction-heating-machine.html?feed_id=270300&_unique_id=67b73cd74f87b
2025年1月22日星期三
2025年1月20日星期一
induction brazing and soldering technology
induction brazing and soldering technology
 https://dw-inductionheater.com/induction-brazing-and-soldering-technology.html?feed_id=267226&_unique_id=678eb2eef02ec
2024年12月18日星期三
induction brazing carbide tip onto steel head teeth
induction brazing carbide tip onto steel head teeth
 https://dw-inductionheater.com/induction-brazing-carbide-tip-onto-steel-head-teeth.html?feed_id=263891&_unique_id=6763315409583
2024年11月26日星期二
Induction Brazing Stainless Steel Tools
Induction Brazing Stainless Steel Tools
 https://dw-inductionheater.com/product/induction-brazing-stainless-steel-tools?feed_id=261890&_unique_id=67463739e8521
2024年10月2日星期三

2024年10月1日星期二

2024年7月8日星期一
High Frequency Induction Brazing Diamond Inserts
 High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
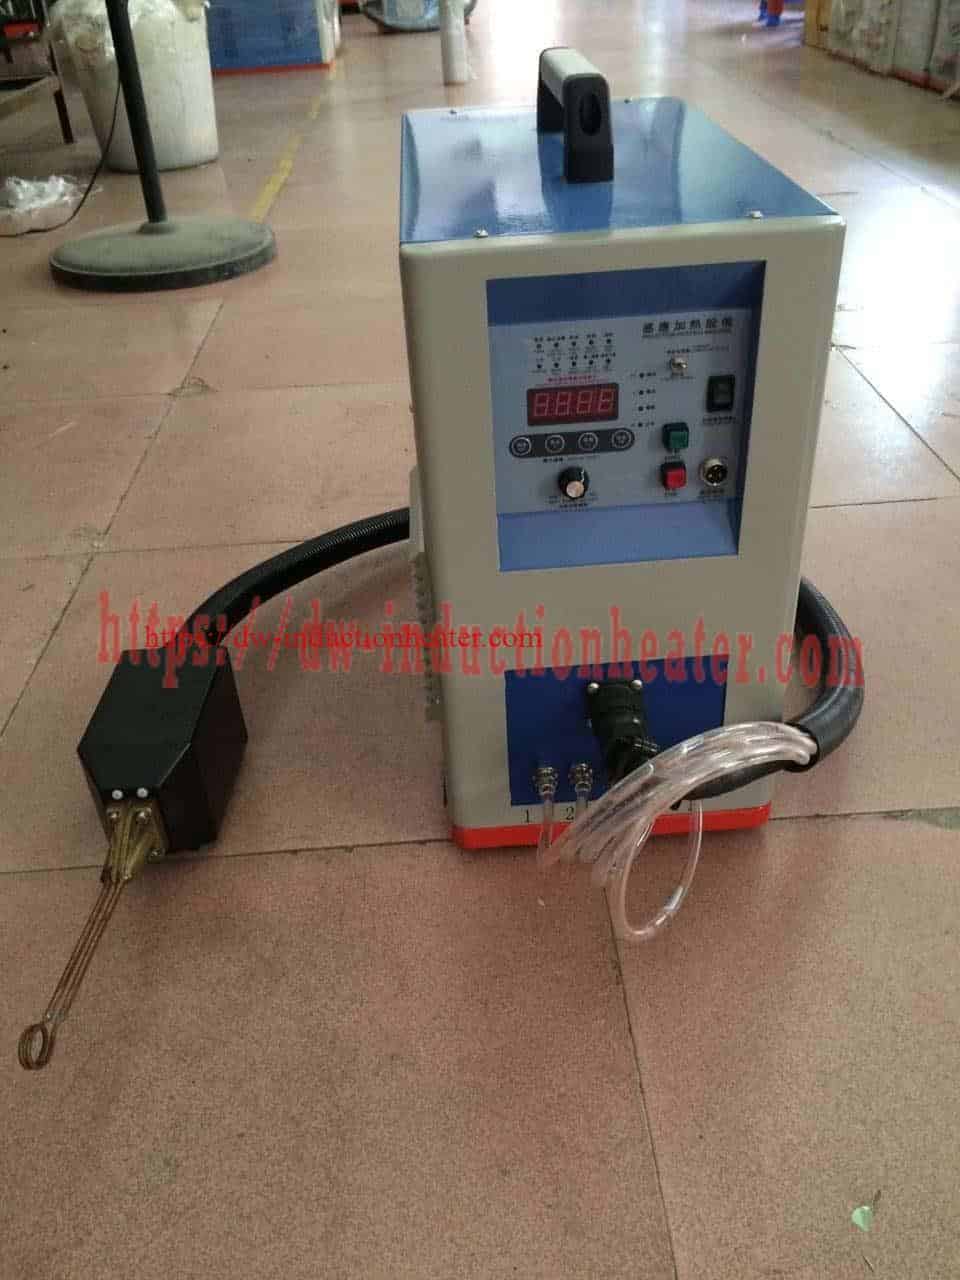
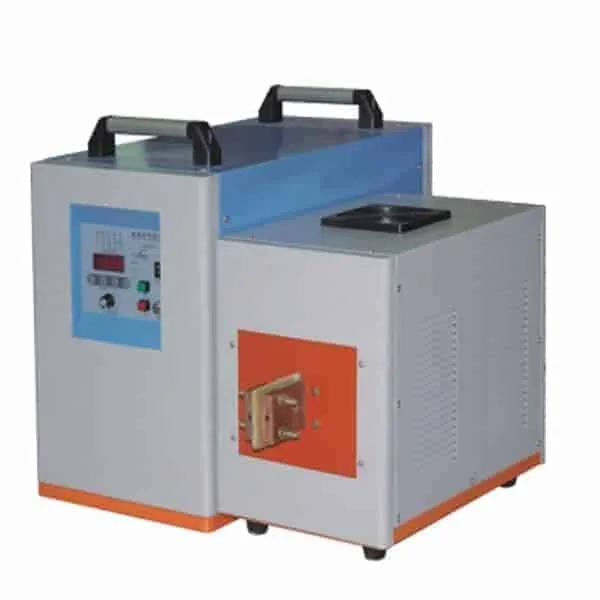
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
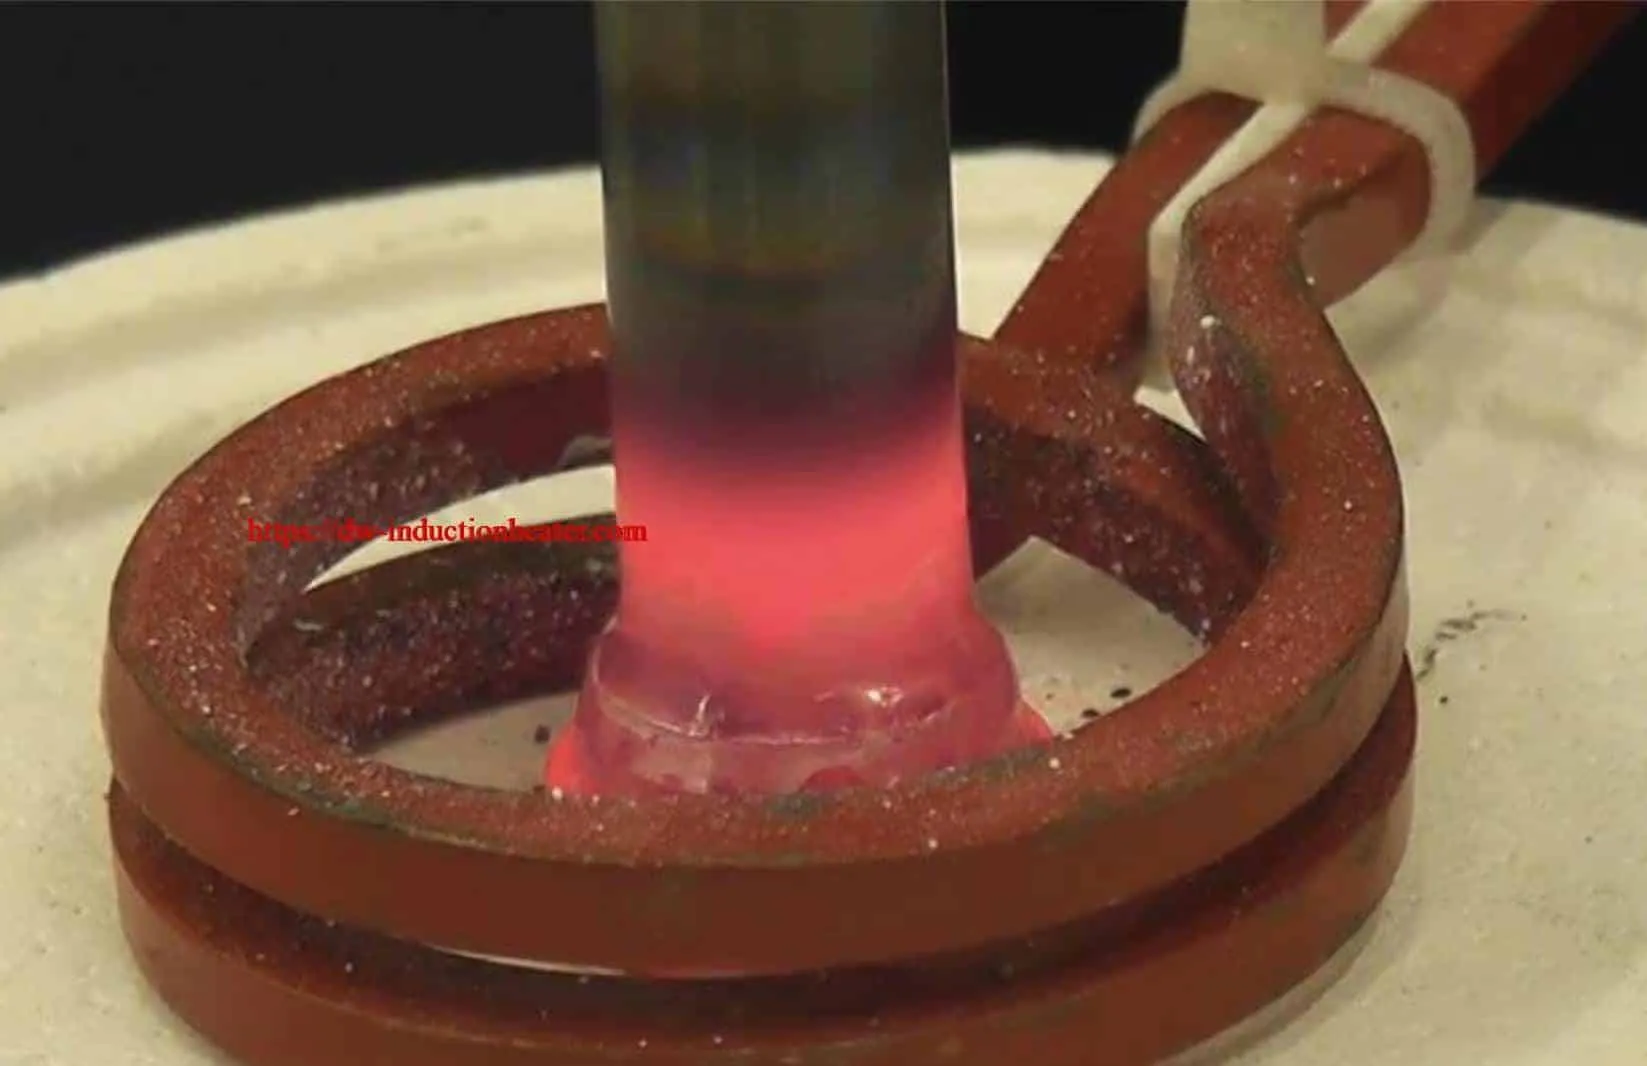
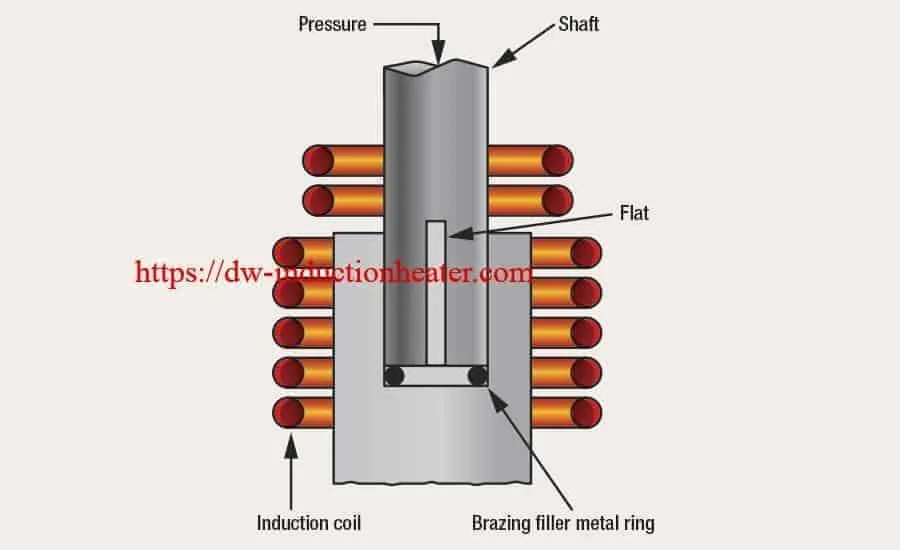
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
https://dw-inductionheater.com/high-frequency-induction-brazing-diamond-inserts.html?feed_id=253269&_unique_id=668cb891a1675
2024年6月25日星期二
Brazing Brass To Copper With Induction
 Brazing Brass To Copper With Induction
Objective: To braze brass end-connectors to copper tubes used in aircraft assembly air lines Material brass end connectors, copper tubes of different diameters
Temperature 1400 ºF 750°C
Frequency 350 kHz
Equipment DW-UHF-4.5KW induction heating system, including a three turn helical induction coil using two 0.33μF capacitors (total 0.66μF)
Process For smaller diameter parts, flux is applied to the entire part and the copper tube to brass joint is assembled using brazing preforms (allowing for the same amount of braze in each joint). The assembly is placed in the coil and heated for 20-30 seconds reaching a temperature of 1400°F. For larger copper tube assemblies, the same process is used, but the braze alloy is stick-fed to the joint to prevent the alloy from flowing out of the joint. A foot switch control is recommended to enable better control of the process.
Results/Benefits
Economy: Power is consumed during the heating only
Consistency: the results of braze joints are repeatable and uniform
https://dw-inductionheater.com/brazing-brass-to-copper-with-induction.html?feed_id=251408&_unique_id=667ade3ae905e
2020年5月10日星期日
induction brazing and soldering technology
HLQ Induction heating systems are value added systems that can fit directly into the manufacturing cell, reducing scrap, waste, and without the need for torches. The systems can be configured for manual control, semi-automated, and all the way up to fully automated systems. HLQ induction brazing and soldering systems repeatedly provide clean, leak-free joints for a wide range of parts including fuel lines, heat exchangers, gas distributors, manifolds, carbide tooling, and more.
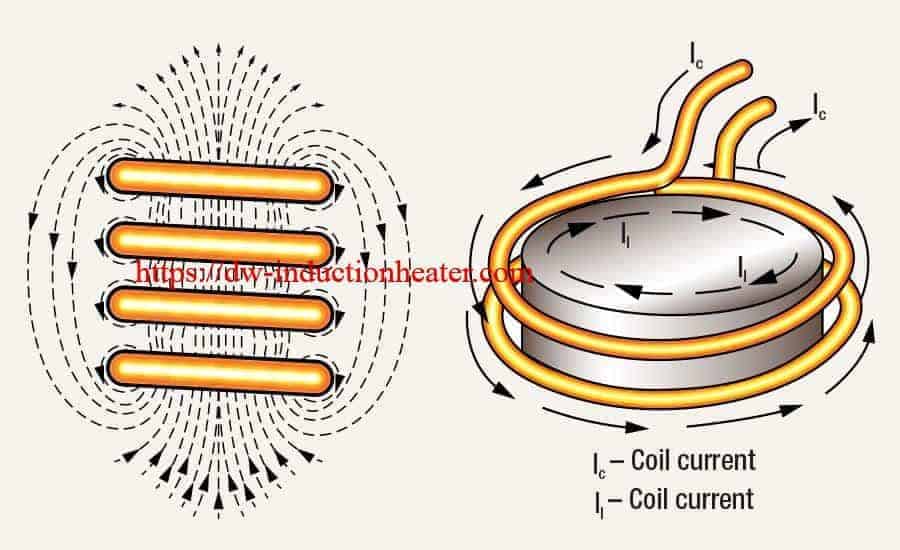
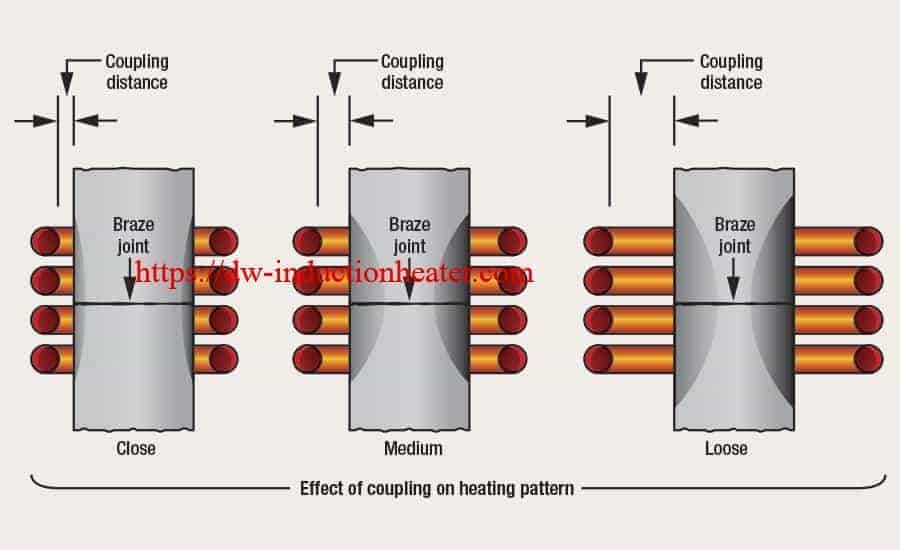
Principles of Induction Brazing & Soldering
Brazing and soldering are processes of joining similar or dissimilar materials using a compatible a filler material. Filler metals include lead, tin, copper, silver, nickel and their alloys. Only the alloy melts and solidifies during these processes to join the work piece base materials. The filler metal is pulled into the joint by capillary action. Soldering processes are conducted below 840°F (450°C) while brazing applications are conducted at temperatures above 840°F (450°C) up to 2100°F (1150°C).
 The success of these processes depends upon the assembly’s design, clearance between the surfaces to be joined, cleanliness, process control and the correct selection of equipment needed to perform a repeatable process.
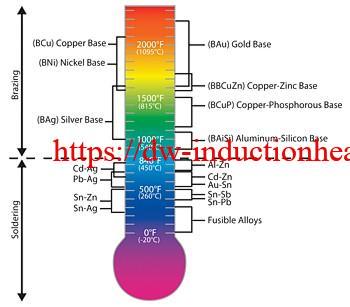
Cleanliness is ordinarily obtained by introducing a flux which covers and dissolves dirt or oxides displacing them from the braze joint.
Induction Brazing Filler Materials
Induction Brazing filler metals can come in a variety of forms, shapes, sizes and alloys depending on their intended use. Ribbon, preformed rings, paste, wire and preformed washers are just a few of the shapes and forms alloys that can be found.

The decision to use a particular alloy and/or shape is largely dependent on the parent materials to be joined, placement during processing and the service environment for which the final product is intended.
Many operations are now conducted in a controlled atmosphere with a blanket of inert gas or combination of inert / active gasses to shield the operation and eliminate the need for a flux. These methods have been proven on a wide variety of material and part configurations replacing or complimenting atmosphere furnace technology with a just in time – single piece flow process.
Clearance Affects Strength
Clearance between the faying surfaces to be joined determines the amount of braze alloy, capillary action / penetration of the alloy and subsequently the strength of the finished joint. The best fit up condition for conventional silver brazing applications are 0.002 inches (0.050 mm) to 0.005 inches (0.127 mm) total clearance. Aluminum is typically 0.004 inches (0.102 mm) to 0.006 inches (0.153 mm). Larger clearances up to 0.015 inches (0.380 mm) usually lack sufficient capillary action for a successful braze.
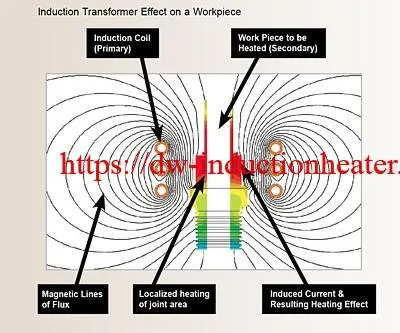
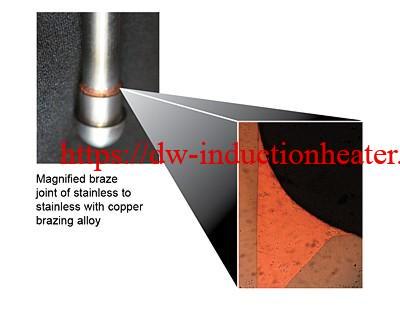
Brazing with copper (above 1650°F / 900°C) requires the joint tolerance kept to an absolute minimum and in some cases press fit at ambient temperatures to assure minimum joint tolerances while at the brazing temperature.
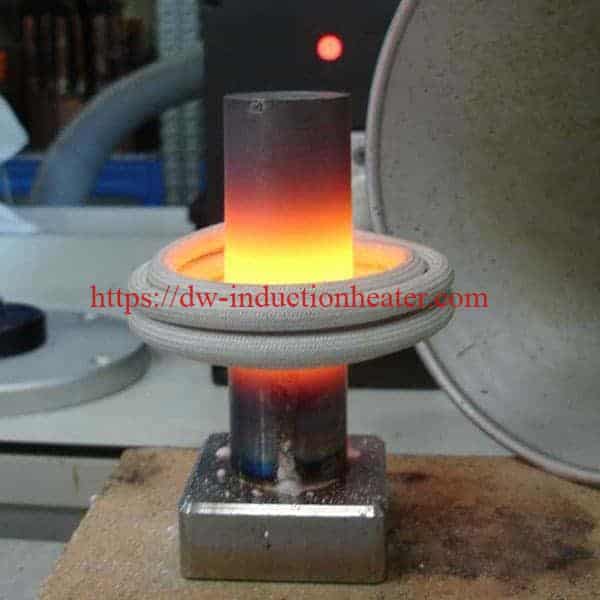
Induction heating has proven to be a valuable aid in the joining process for many reasons. Rapid heading and precise heat control offers the possibility of localized heating of high strength components without significantly changing the material properties. It also allows for the brazing of difficult materials such as aluminum and sequential, multi-alloy brazing and soldering of close proximity joints.
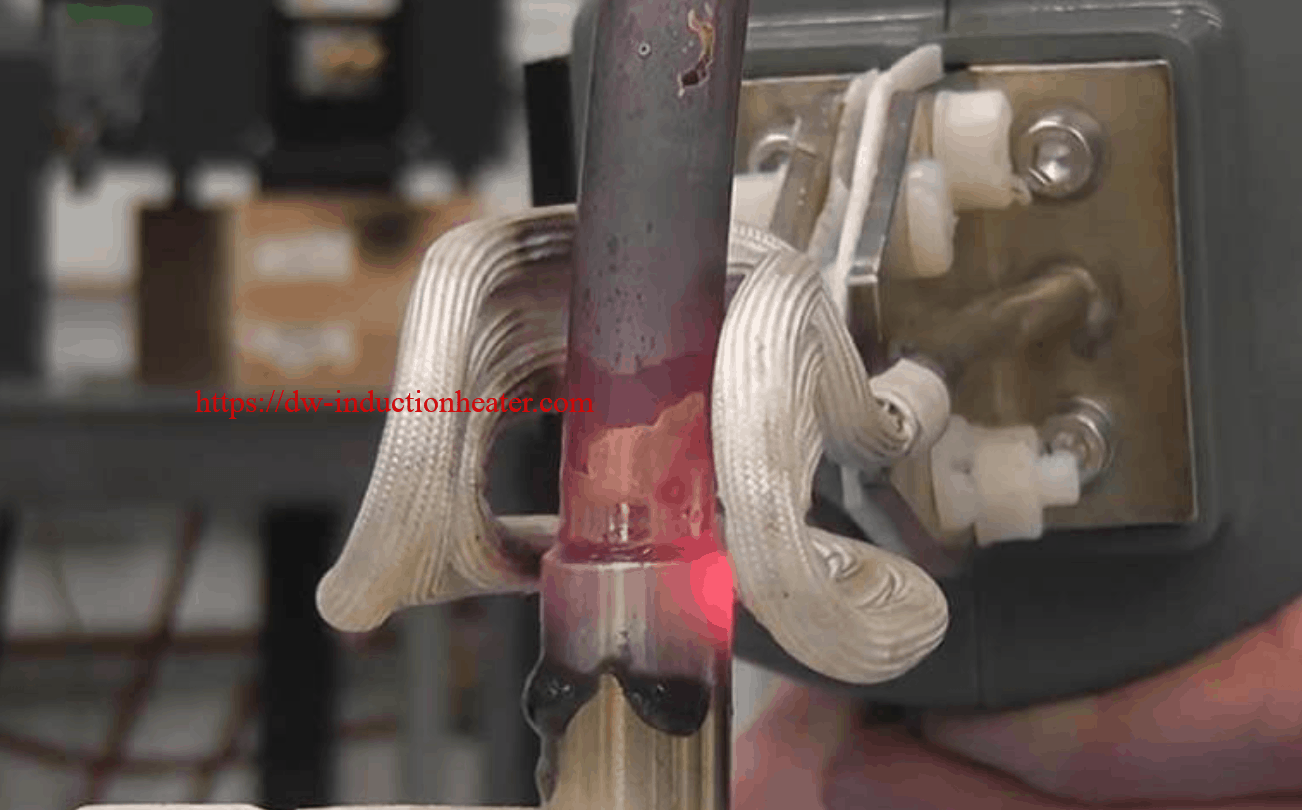
Induction heating in brazing and soldering applications is readily adaptable to production line methods, permitting strategic arrangement of the equipment in an assembly line, and if necessary, heating by remote control. Frequently, induction brazing and soldering permits a reduction in the require number of part fixtures, with the minimal heating of the fixtures increasing life span and maintaining accuracy in alignment of the components to be joined. Since operators need not guide the induction heating source, both hands are left free to prepare assemblies for joining.
 HLQ induction brazing equipment delivers quality, consistency, configurable throughput, and quick change-over tooling for various production needs. The Radyne induction brazing and soldering product line offers standard solutions for brazing:
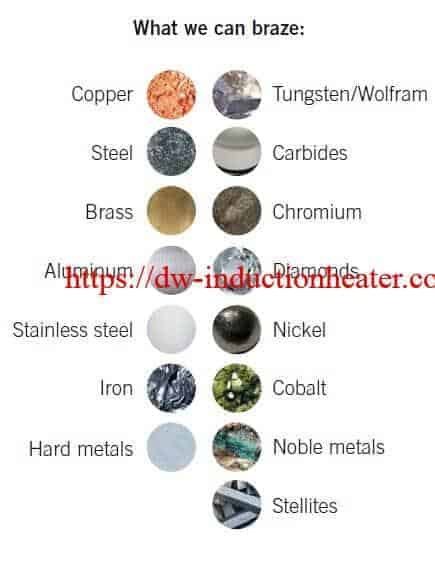
Aluminum
Copper
Brass
Stainless steel
Carbide
And more…
https://dw-inductionheater.com/wp-content/uploads/2020/05/induction-brazing-soldering-technology.jpg?v=1589092485
https://dw-inductionheater.com/induction-brazing-and-soldering-technology.html
high frequency brazing, induction brazer, induction brazing, induction brazing copper system, induction brazing machine, induction brazing manufacturer, induction brazing system, induction brazing units, induction soldering, MF brazing, MF brazing machine, radio frequency brazing, radio frequency soldering, RF induction brazing
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.