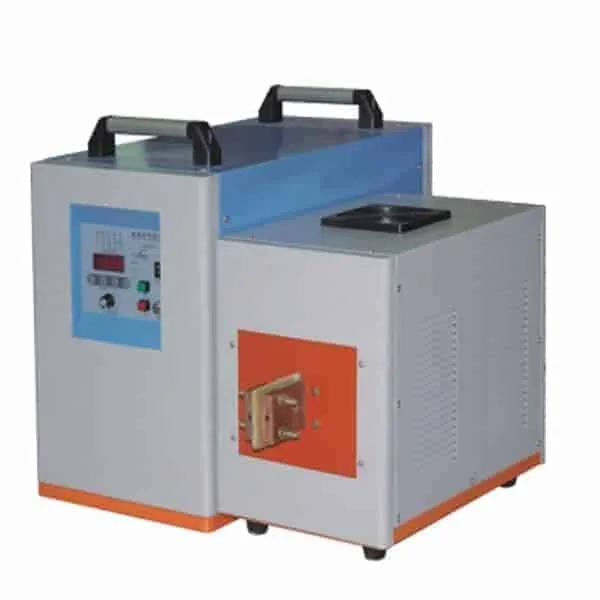
 https://dw-inductionheater.com/product/high-frequency-brazing-equipment?feed_id=267429&_unique_id=67915ca0cb74b
2025年1月22日星期三
High Frequency Brazing Equipment
High Frequency Brazing Equipment
https://dw-inductionheater.com/product/high-frequency-brazing-equipment?feed_id=267429&_unique_id=67915ca0cb74b
https://dw-inductionheater.com/product/high-frequency-brazing-equipment?feed_id=267429&_unique_id=67915ca0cb74b

2024年7月9日星期二
Induction Brazing Carbide
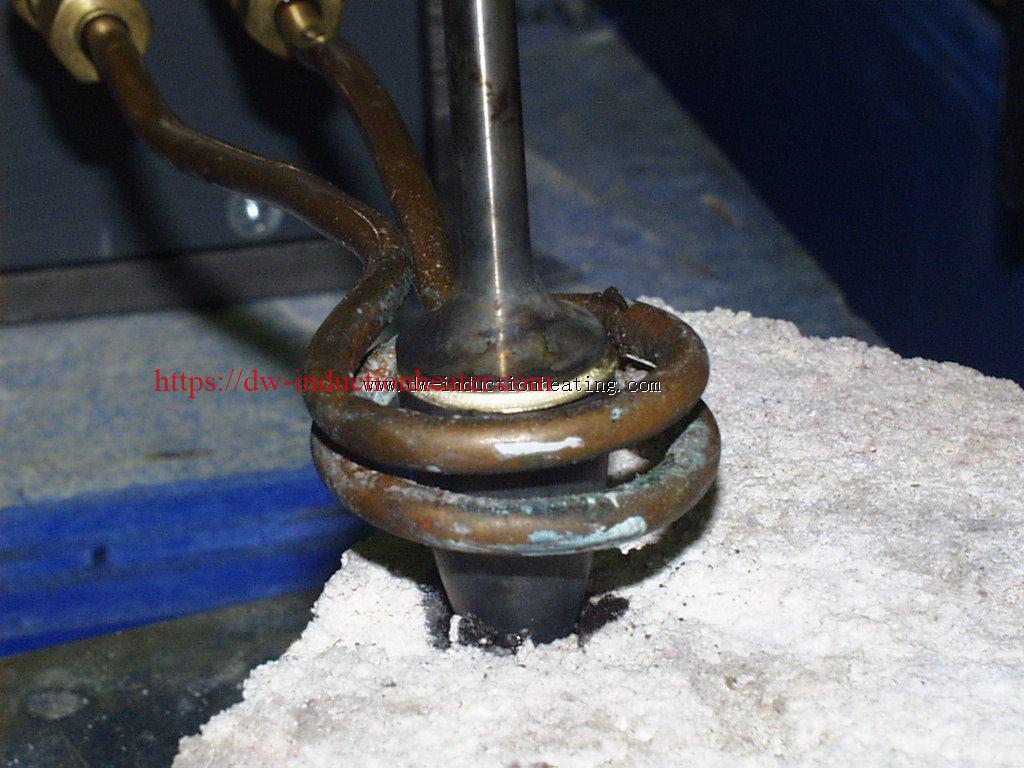 Induction Brazing Carbide File
Objective: Induction Brazing carbide rotary file assemblies with uniform concentricity in an aerospace application
Material • Carbide blank • High speed steel shank • Temperature indicating paint • Braze shim and black flux
Temperature 1400°F (760°C)
Frequency 550 kHz
Equipment: DW-UHF-4.5kw induction heating system, equipped with a remote heat station containing two 0.33 μF capacitors (total 0.66 μF) An induction heating coil designed and developed specifically for this application.
Process A multi-turn helical coil is used. The part is heated to determine the time required to reach the desired temperature and required heat pattern. It takes approximately 30 - 45 seconds to reach 1400°F (760°C) depending on the various part sizes. Flux is applied to the entire part. A braze shim is sandwiched between the steel shank and carbide. Induction heating power is applied until the braze flows. With proper fixturing, concentricity of the part can be achieved.
Results/Benefits • Repeatable, consistent precise heat.
https://dw-inductionheater.com/induction-brazing-carbide-file.html?feed_id=253337&_unique_id=668d6f6a2c054
2024年7月8日星期一
High Frequency Induction Brazing Diamond Inserts
 High Frequency Induction Brazing Diamond Inserts
Objective: Induction Brazing diamond inserts to a steel drilling ring
Material : • steel ring and diamond inserts • Braze shim preform • Flux
Temperature :1300 – 1350 (700 – 730) °F (°C)
Frequency :78 kHz
Equipment: DW-HF-15kW, induction heating system, equipped with a remote heat station containing two 0.5 μF capacitors (total 0.25 μF) An induction heating coil designed and developed specifically for this application.
Process: A multi-turn, internal-external helical coil (A) is used to generate the required heating pattern. Initial tests on the ring alone determine system tuning. Flux is applied to the part and the braze shims are inserted into the counter-bored holes (B). This is followed by the synthetic diamonds. The part is loaded into the coil and weight is placed onto the diamonds (C). RF Induction Heating power is applied until the braze flows. The power is turned off and the part air cools to room temperature.
Results/Benefits • reduced ring warping compared to furnace induction heating • decreased cycle time due to reduced ramp-up and cooldown times
https://dw-inductionheater.com/high-frequency-induction-brazing-diamond-inserts.html?feed_id=253269&_unique_id=668cb891a1675
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.