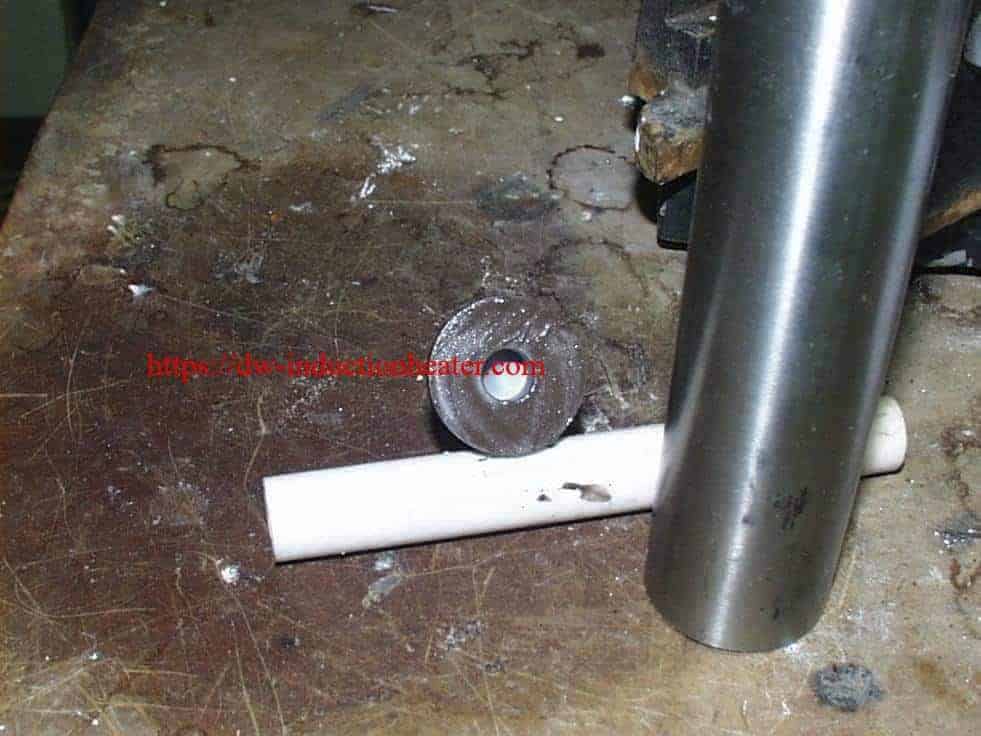
 https://dw-inductionheater.com/induction-brazing-carbide-to-stainless-steel.html?feed_id=273809&_unique_id=67e4b8875b247
2025年3月26日星期三
Induction Brazing Carbide To Stainless Steel
Induction Brazing Carbide To Stainless Steel
https://dw-inductionheater.com/induction-brazing-carbide-to-stainless-steel.html?feed_id=273809&_unique_id=67e4b8875b247
https://dw-inductionheater.com/induction-brazing-carbide-to-stainless-steel.html?feed_id=273809&_unique_id=67e4b8875b247

2025年3月15日星期六
Brazing stainless steel with induction
Brazing stainless steel with induction
 https://dw-inductionheater.com/brazing-stainless-steel-with-induction.html?feed_id=272707&_unique_id=67d5e3a52460f
2025年2月22日星期六
Handheld Brazing Stainless Steel Tube
Handheld Brazing Stainless Steel Tube
 https://dw-inductionheater.com/handheld-brazing-stainless-steel-tube.html?feed_id=270503&_unique_id=67ba34252eb11
2025年2月17日星期一
High Frequency Brazing Stainless Steel Fittings
High Frequency Brazing Stainless Steel Fittings
 https://dw-inductionheater.com/high-frequency-brazing-stainless-steel-fittings-machine.html?feed_id=269952&_unique_id=67b3484dc80ed
2025年1月28日星期二
2025年1月25日星期六
induction brazing stainless steel tubing process
induction brazing stainless steel tubing process
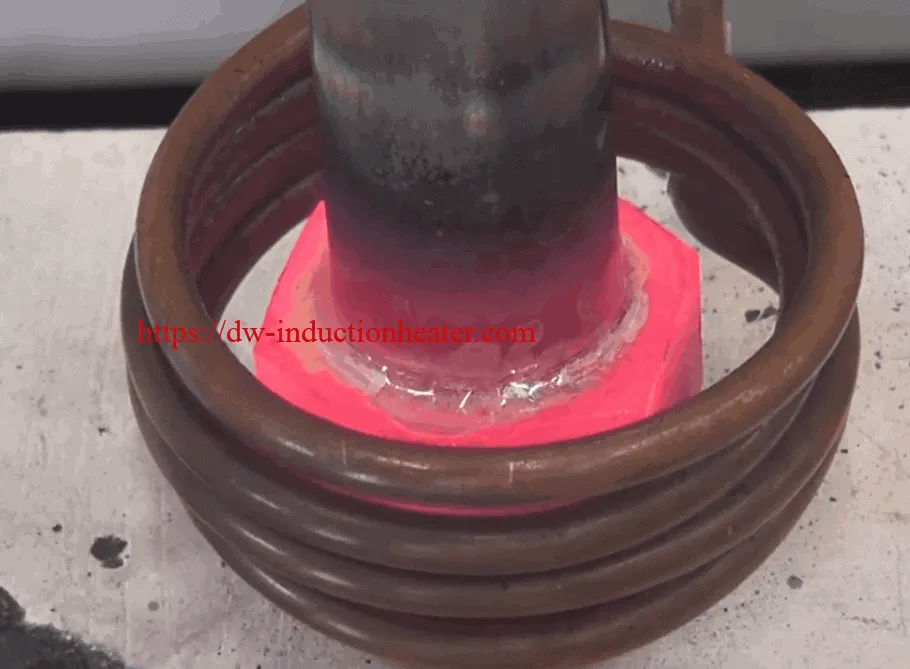 https://dw-inductionheater.com/induction-brazing-stainless-steel-tubing-process.html?feed_id=267661&_unique_id=6794a19459353
2025年1月22日星期三
induction brazing stainless steel to copper
induction brazing stainless steel to copper
 https://dw-inductionheater.com/induction-brazing-stainless-steel-to-copper.html?feed_id=267458&_unique_id=6791aa44c7849
2024年11月26日星期二
Induction Brazing Stainless Steel Tools
Induction Brazing Stainless Steel Tools
 https://dw-inductionheater.com/product/induction-brazing-stainless-steel-tools?feed_id=261890&_unique_id=67463739e8521
2024年6月21日星期五
Induction Brazing Stainless Steel
 Induction Brazing Stainless Steel
Objective
1st Application: Braze hub assembly to needle holder
2nd Application: Braze Large tube to ring joint
Material: 1st Application: Steel hub assembly and needle 0.1" dia(2.5mm) 2nd Application: Steel tube 1" OD (25.4 mm) and ring
Temperature 1400 ºF (760 ºC)
Frequency 325 kHz for brazing the needle 0.1" dia (2.5mm) 259 kHz for brazing ring to steel tube 1" OD (25.4 mm)
Equipment • DW-UHF-4.5KW induction heating system, equipped with a
remote workhead containing two .66 μF capacitors for a total of 1.32 μF
• Two induction heating coils, designed and developed specifically for this dual application.
Process 1st application: A two-turn helical coil is used to heat the hub assembly on the needle holder for 10 seconds. The coil concentrates the heat on the hub only, as the needle is magnetic and the hub material is non-magnetic. A small
diameter braze wire is used to supply sufficient amount of braze creating a strong aesthetically pleasing bond. 2nd application: A three-turn helical coil is used for brazing the large tube to the ring joint for 3-5 minutes. A braze ring is
used to supply sufficient amount of braze to create an aesthetically pleasing bond.
Results/Benefits Induction heating provides:
• Even distribution of heating, provides even flow of braze alloy for an aesthetically pleasing bond
• System flexibility allows for the same unit to be used for two different applications which is a cost saving.
https://dw-inductionheater.com/induction-brazing-stainless-steel.html?feed_id=250808&_unique_id=6675de8883b88
2024年6月17日星期一
Induction Brazing Stainless Steel
 Induction Brazing Stainless Steel Car grill
Objective Braze an end plug on a stainless steel car grill before powder coating application
Material Stainless steel car grill 0.5” x 0.19” (12.7mm x 4.8mm), end plugs and braze ring
Temperature: 1350 ºF (732°C)
Frequency:400 kHz
Equipment •DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing one 0.66μF capacitor.
• An induction heating coil designed and developed specifically for this application.
Process A three turn square shaped helical coil is used to heat the end of the grill. End plugs are inserted into the grill and the assembly is inserted into the coil for 30 seconds. The braze flows to create a neat and clean leak-proof joint.
Results/Benefits Induction heating provides:
• Rapid localized heat to joint area only
• Minimized oxidation reduces cleaning time
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
https://dw-inductionheater.com/induction-brazing-stainless-steel-car-grill.html?feed_id=250303&_unique_id=6670df1a69964
Brazing Stainless Steel To Copper With Induction
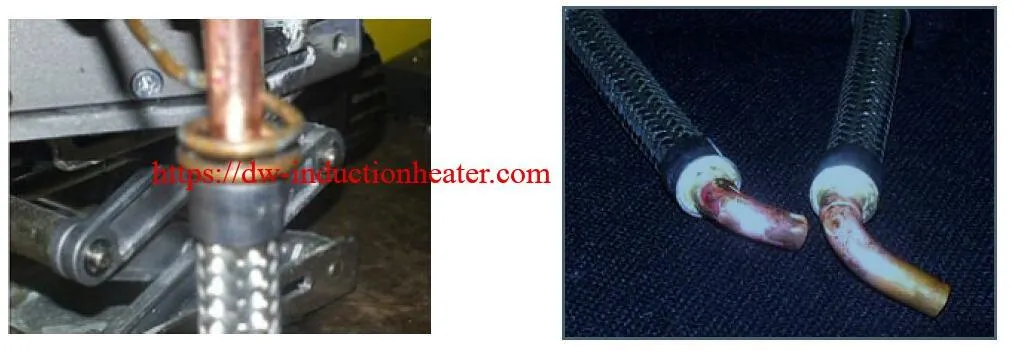 Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
https://dw-inductionheater.com/brazing-stainless-steel-to-copper-with-induction.html?feed_id=250235&_unique_id=667028143e122
Brazing Stainless Steel To Copper With Induction
Brazing Stainless Steel To Copper With Induction Heater
Objective Braze a stainless steel braided hose to copper elbows for a braided hose assembly.
Material Stainless steel braided hose 3/8” (9.5mm) OD, copper elbow 1/4” (6.3mm) OD, braze preform rings and black flux
Temperature 1400 ºF (760 ºC)
Frequency 300 kHz
Equipment • DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing two 0.33μF capacitors for a total of 0.66μF
• An induction heating coil designed and developed specifically for this application.
Process: A two turn helical coil is used to heat the braided hose assembly. Braze rings are placed at the joint on the copper elbow and flux is applied to the entire surface of the assembly.
The assembly is placed in the heating coil and the braze flows within 30-45 seconds. This creates a liquid and gas tight braze between the copper and stainless steel braided hose.
Results/Benefits Induction heating provides:
• Liquid and gas-tight braze
• Energy efficient heat in a minimal amount of time
• Controllable braze flow through the use of braze rings
• Even distribution of heating
https://dw-inductionheater.com/brazing-stainless-steel-to-copper-with-induction.html?feed_id=250235&_unique_id=6670281402b10
2020年5月2日星期六
induction brazing stainless steel to copper
Objective
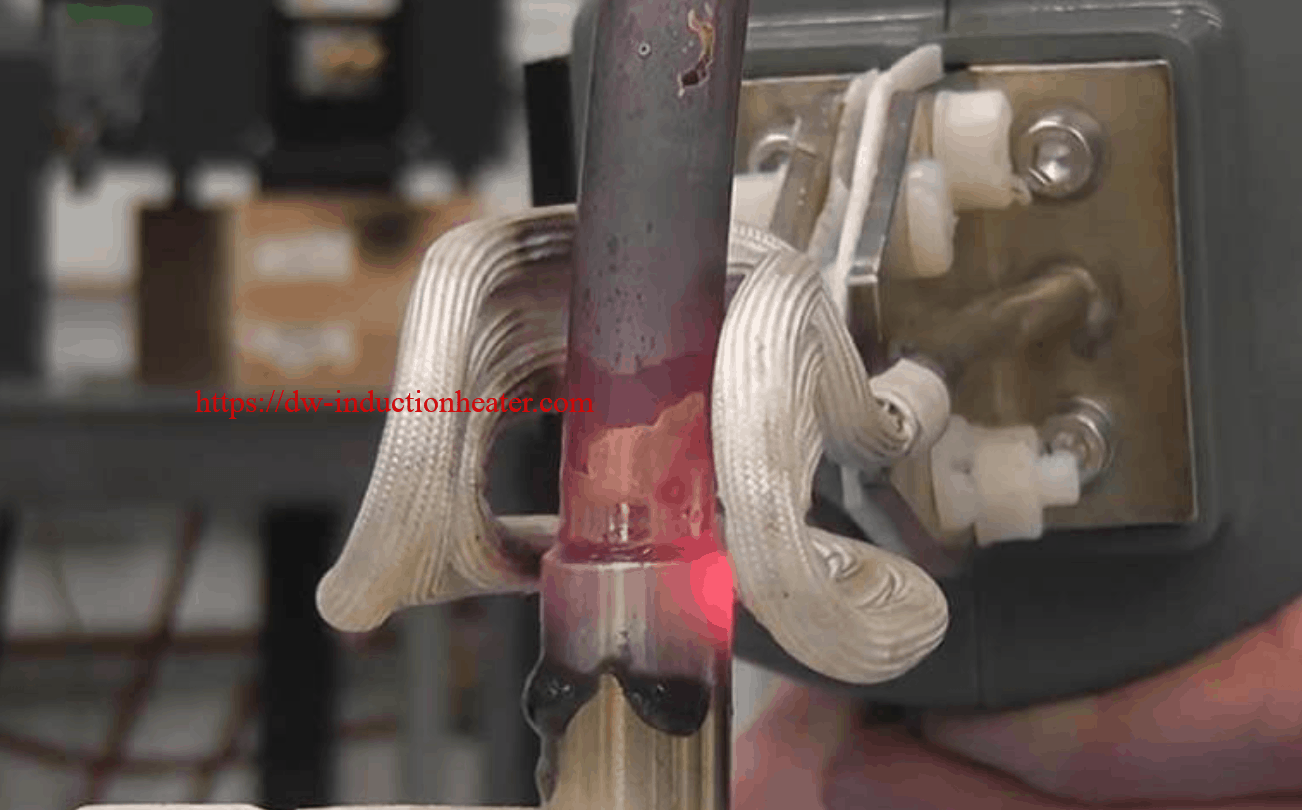
Induction Brazing stainless steel to copper tubing. Objective is to evaluate induction brazing solution. Customer is looking to reduce defects and for a cleaner brazing environment.

Due to different pipe size and lower volume – evaluation is performed with a UBraze system.
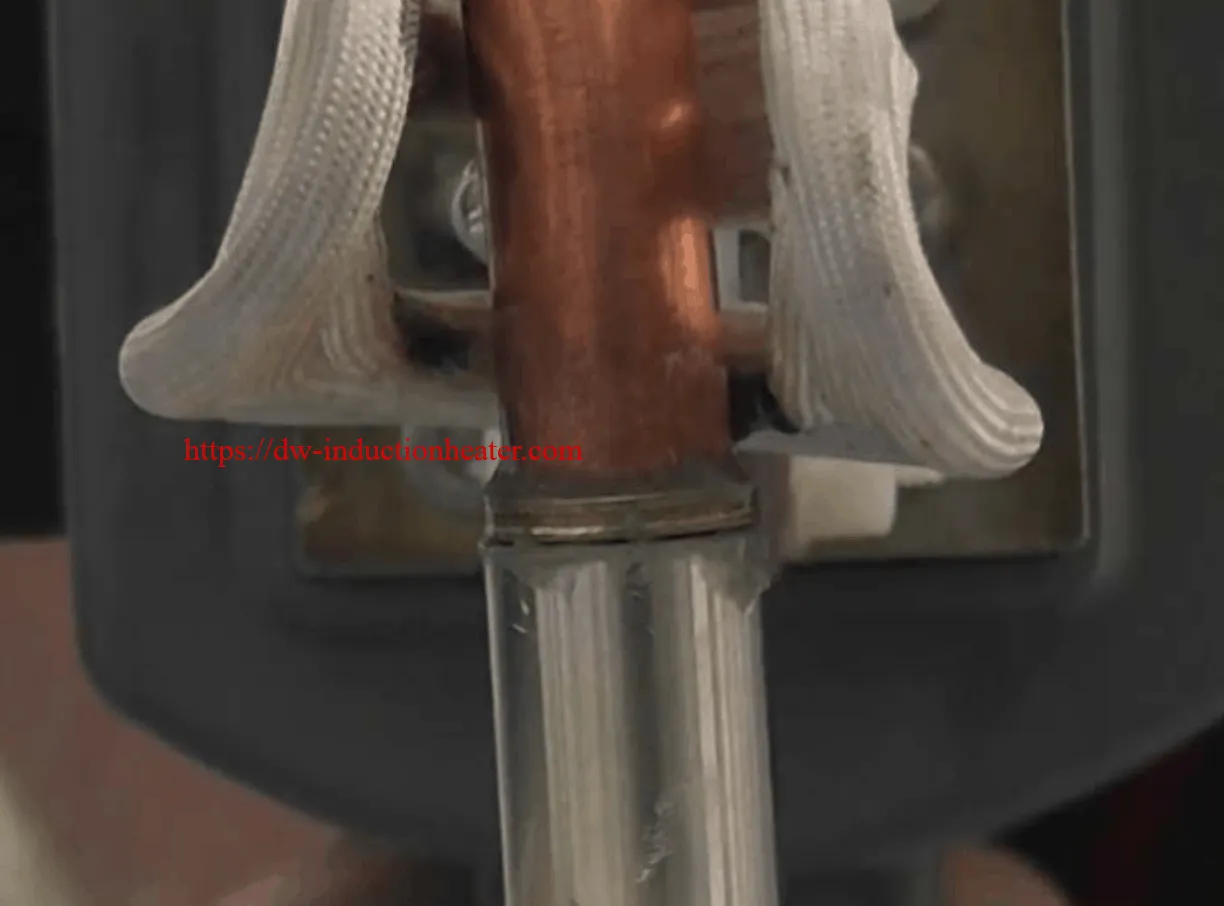
Test1
Equipment
DW-HF-25kw induction brazing machine
Materials
Copper to Stainless steel tube
Power: 12.5kW
Temperature: 1400ºF to 1600ºF (760ºC to 871ºC)
Time: 9 to 11 seconds
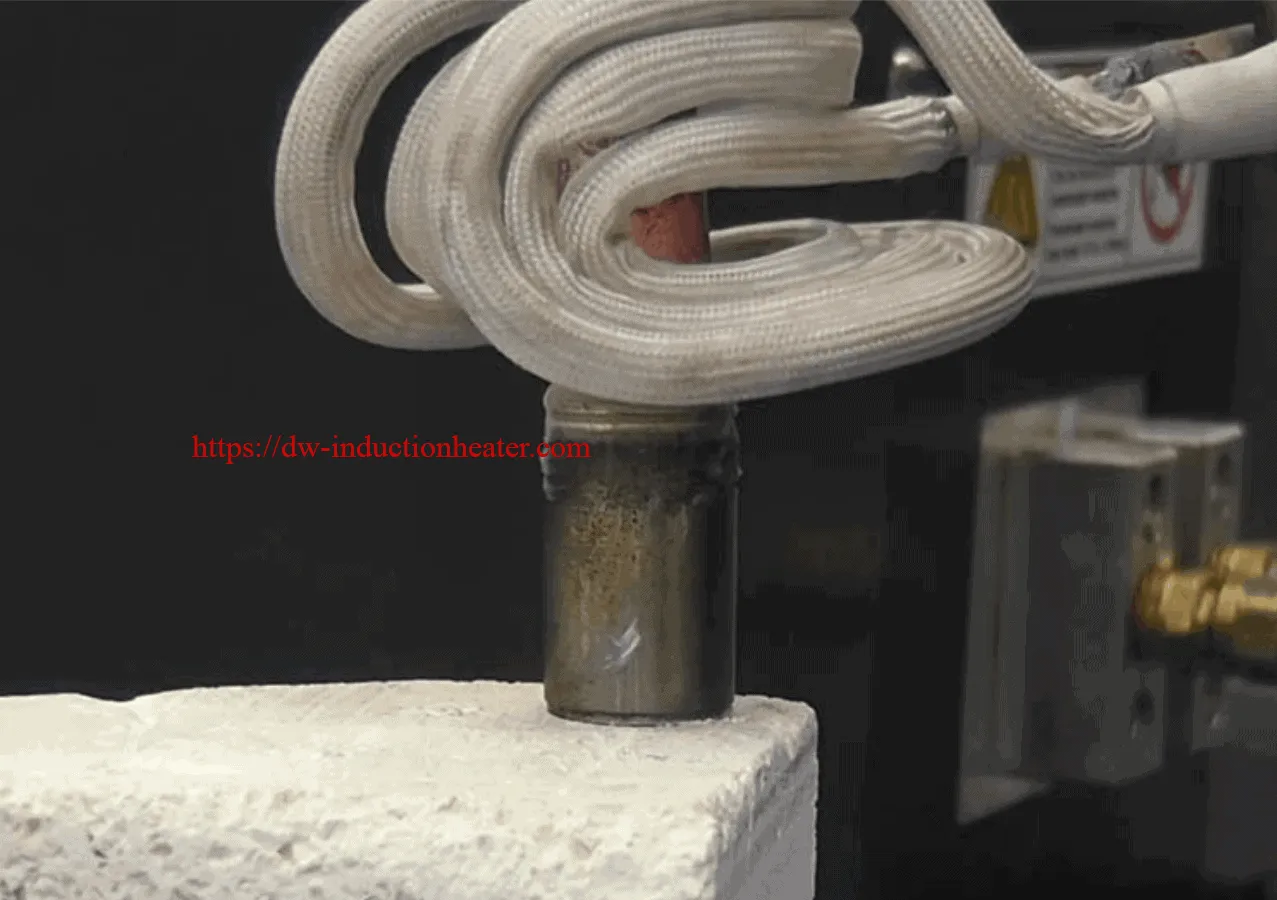
Test2
Equipment
DW-HF-25kw induction brazing machine
Materials
Copper to Stainless steel
Power: 12.5kW
Temperature: 1400ºF to 1600ºF (760ºC to 871ºC)
Time: 9 to 11 seconds
Results and Conclusions:
Induction brazing test with U open coil was able to braze the parts in 9 to 11 seconds for the full braze cycle.
Operator training with this setup will be minimal.


https://dw-inductionheater.com/wp-content/uploads/2020/05/induction-brazing-stainless-steel-to-coppr-pipes.png?v=1588384073
https://dw-inductionheater.com/induction-brazing-stainless-steel-to-copper.html
brazing copper system, brazing stainless steel, brazing stainless steel to copper, brazing stainless steel tube, handheld brazing copper, High frequency Brazing copper, High Frequency brazing stainless steel, induction brazing equipment, induction brazing machine, induction brazing stainless steel, induction brazing stainless steel unit, induction brazing system, induction brazing units, RF brazing stainless steel
2020年4月25日星期六
induction brazing stainless steel tubing process
Induction Brazing stainless steel tubing and stainless steel fittings Technology

Objective
Induction Brazing stainless steel tubing and stainless steel fittings
Equipment
DW-UHF-20kw induction brazing machine
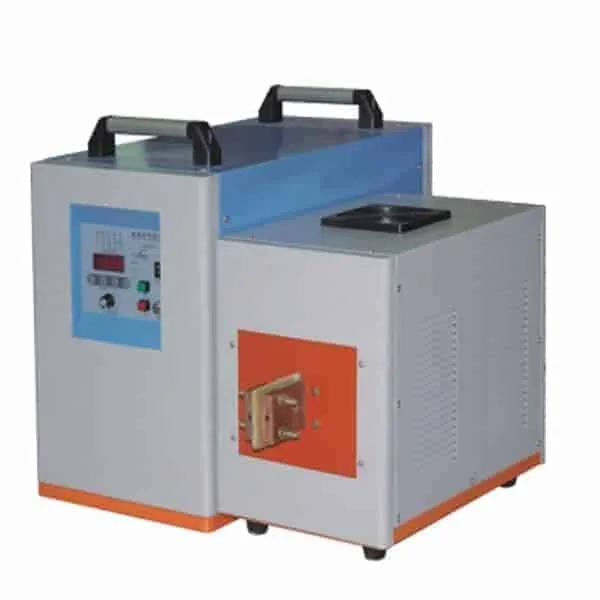
Materials
1.75″ (44.45mm) Hexagon fitting
Power: 10.52 kW
Temperature: 1300°F (704°C)
Time: 30 seconds
 Results and Conclusions:
- Induction heating pinpoints the heat to the desired area of the part
- Improved process control for precise heating to a desired temperature
- Power on demand and rapid, consistent heat cycles
- Technology without pollution, which is both clean and safe


https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-Brazing-stainless-steel-tubing-process.png?v=1587783934
https://dw-inductionheater.com/induction-brazing-stainless-steel-tubing-process.html
brazing stainless steel, brazing stainless steel system, high frquency brazing stainless steel, high frquency brazing tubing, induction brazing stainless steel, induction brazing tubing, induction brazing tubing system, RF brazing stainless steel, RF brazing tubing, stainless steel, stainless steel tubing
2020年4月18日星期六
induction brazing stainless steel to steel
High frequency magnetic induction brazing stainless steel to steel process
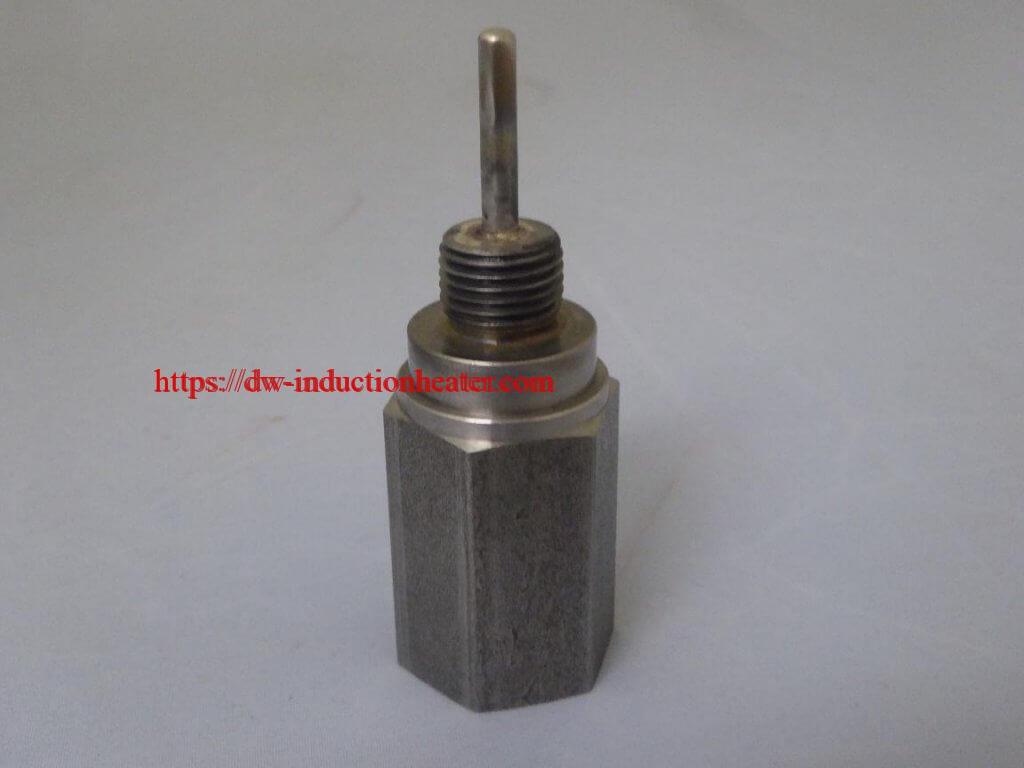
HLQ team was provided with 2 different parts to be brazed in our test laboratory.
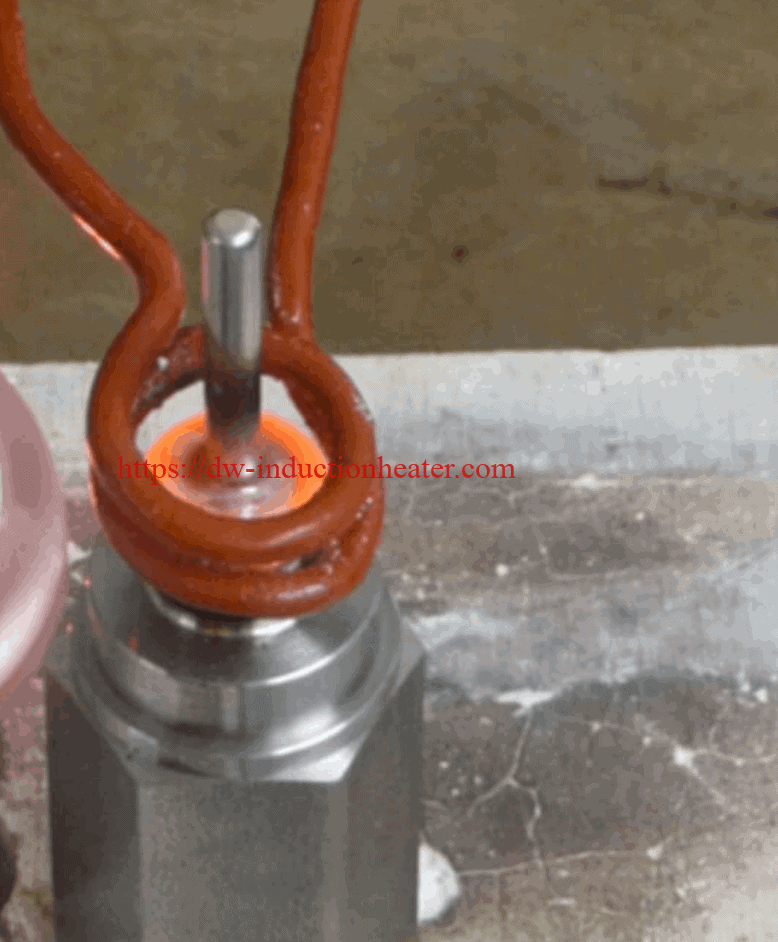
Objective: Induction Brazing of a 0.15’’/ 3.81mm stainless steel pin to a steel base.
Equipment: DW-UHF-6KW-III handheld induction brazing system
Industry: Appliances & HVAC
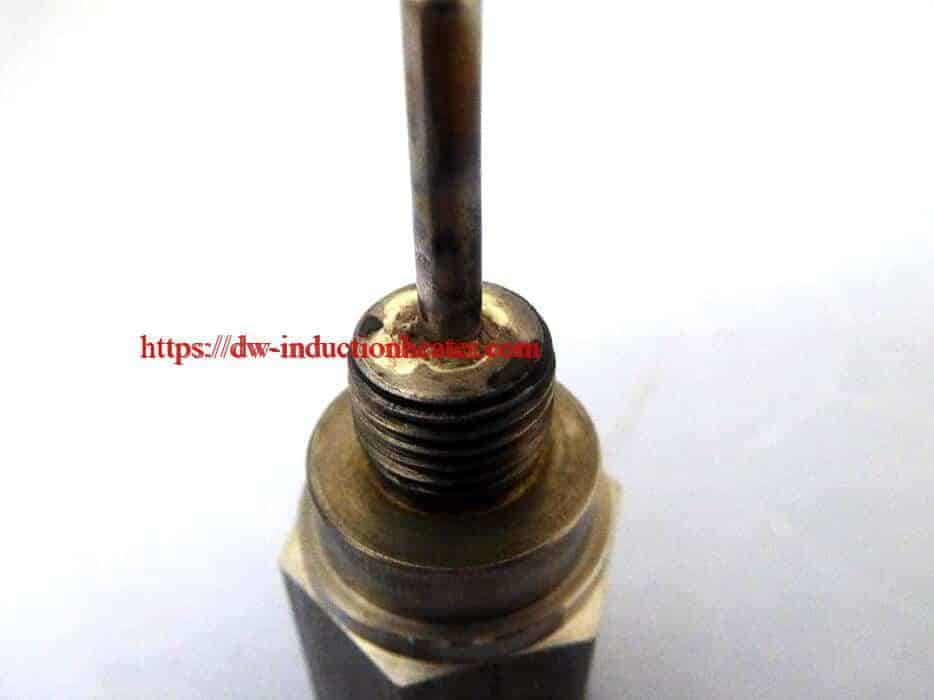
Materials:
Steel hexagon (base 1’’/ 25.4 mm diameter; 0.1’’/ 2.54 mm wall thickness)
A stainless steel pin (0.15’’/ 3.81 mm)
Other Materials:
All-purpose black brazing flux
Power: 1.43 kW
Temperature: 1400 °F/ 760°C
Time: 8 seconds
Process:
The two workpieces were carefully positioned together. All-purpose induction brazing black flux was added because it is ideal for high-temperature applications where rapid, localized heating is needed. The process of induction brazing was performed successfully within 8 seconds by using the DW-UHF-6KW-III handheld induction brazing system, producing the induction heating power of 1.43 kW at 1400 °F/ 760°C.
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-stainless-steel-to-steel-process.png?v=1587196467
https://dw-inductionheater.com/high-frequency-magnetic-induction-brazing-stainless-steel-to-steel-process.html
brazing stainless steel, brazing stainless steel to steel, HF brazing stainless steel, High Frequency Brazing steel, induction brazing, induction brazing machine, induction brazing stainless steel, induction brazing stainless steel to steel
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.