 https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90
2025年2月21日星期五
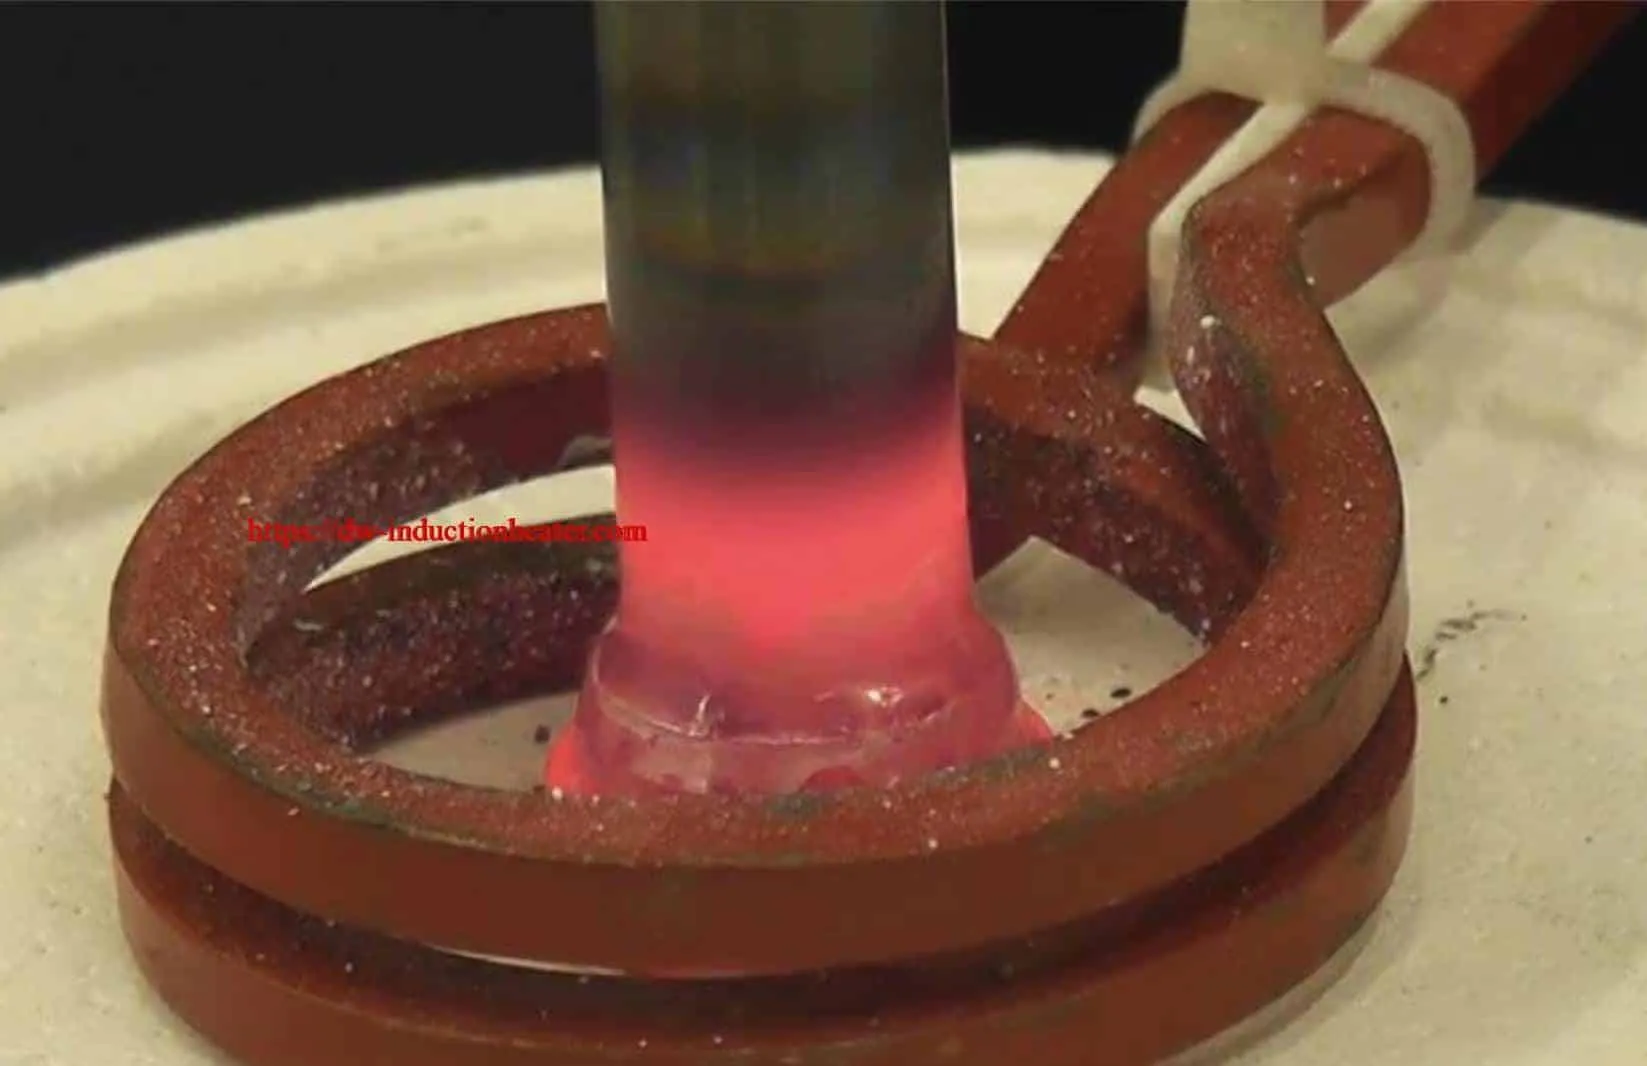
High frequency induction brazing steel tube to steel fitting
High frequency induction brazing steel tube to steel fitting
https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90
https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90

2025年2月17日星期一
High Frequency Brazing Stainless Steel Fittings
High Frequency Brazing Stainless Steel Fittings
 https://dw-inductionheater.com/high-frequency-brazing-stainless-steel-fittings-machine.html?feed_id=269952&_unique_id=67b3484dc80ed
2025年2月16日星期日
Induction Brazing Steel Parts to Tungsten Carbide Plate
Induction Brazing Steel Parts to Tungsten Carbide Plate
 https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=269865&_unique_id=67b24b1830232
2025年1月28日星期二
2024年11月27日星期三
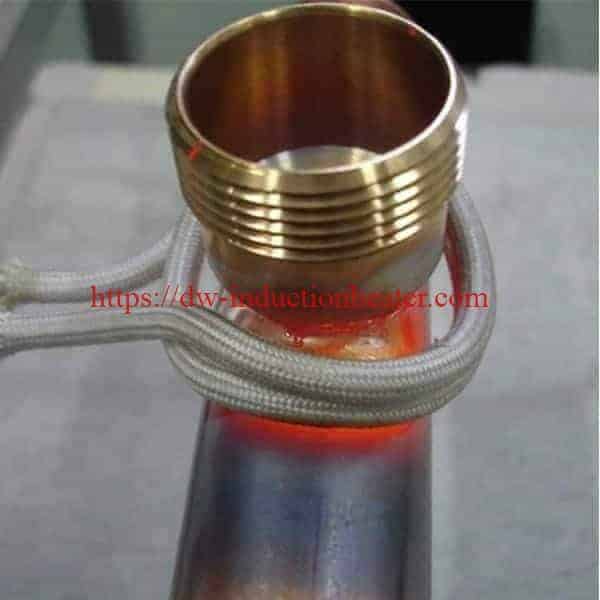
Induction Brazing Stainless Steel To Brass
Induction Brazing Stainless Steel To Brass
 https://dw-inductionheater.com/product/induction-brazing-stainless-steel-to-brass?feed_id=262006&_unique_id=674788a06f3bc
2024年7月7日星期日
Induction Brazing Steel Pipe
 Induction Brazing Steel Pipe
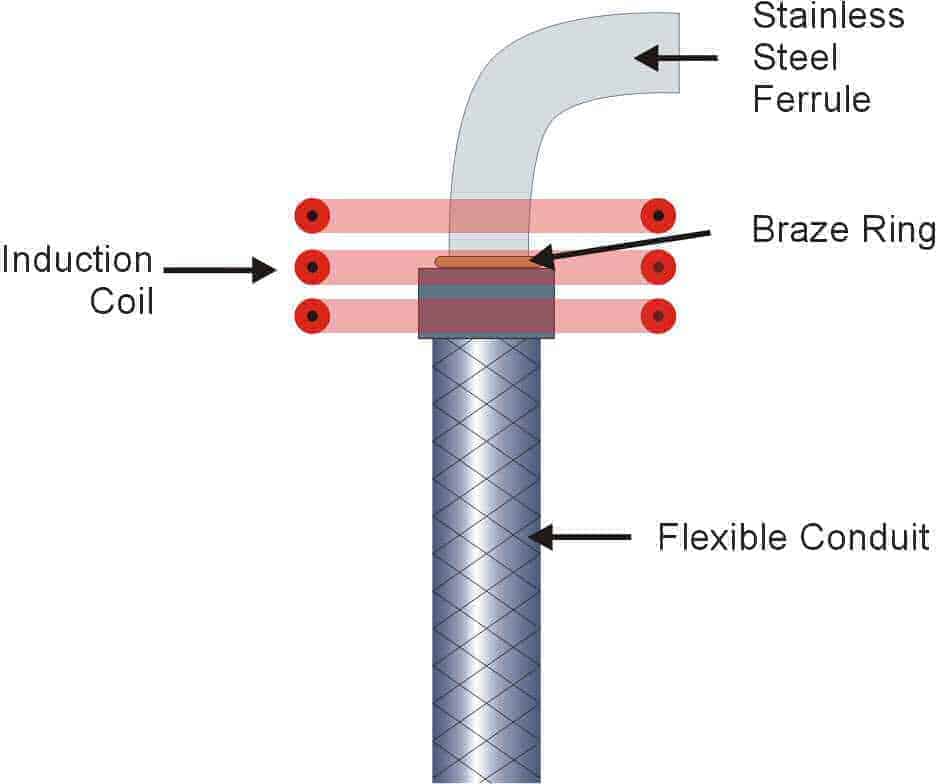
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
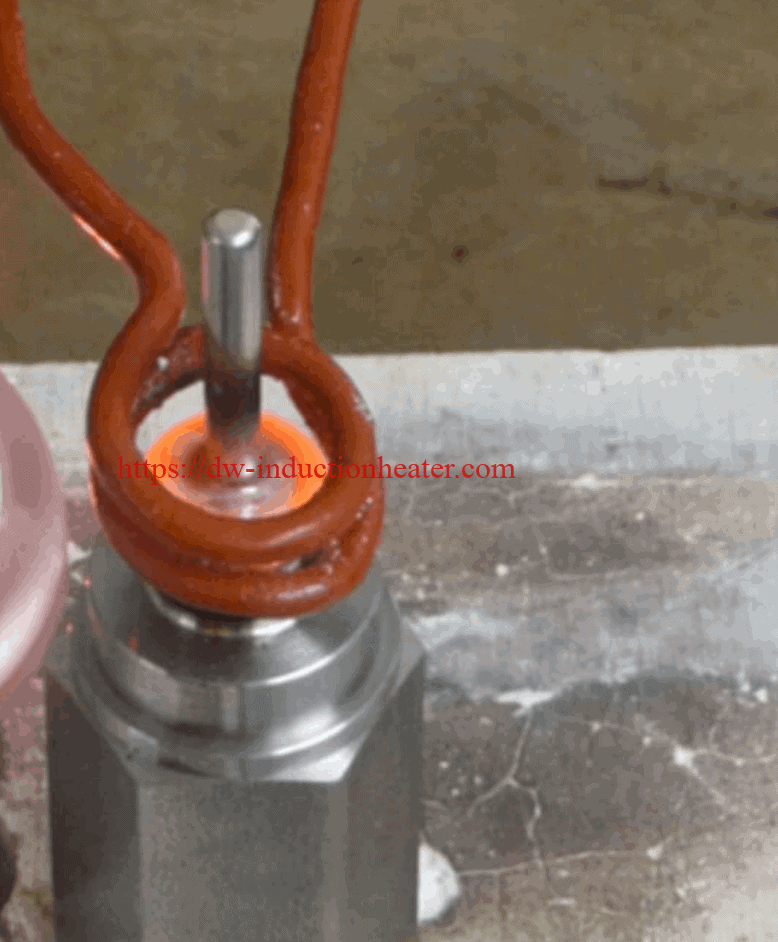
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
https://dw-inductionheater.com/induction-brazing-steel-pipe.html?feed_id=253065&_unique_id=668a9431e0f3d
2024年6月13日星期四
Induction Brazing Steel To Carbide Plate
 Induction Brazing Steel To Carbide Plate
Objective Brazing a steel piston valve assembly
Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze
Temperature 1350 ºF
Frequency 100 kHz
Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF
• An induction heating coil designed and developed specifically for this application.
Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces.
Results/Benefits Induction heating provides:
• Rapid localized heat, which can minimize oxidation and reduce cleaning after joining
• Hands-free heating that involves no operator skill for manufacturing
• Clean and controllable joints
• Produces high quality repeatable parts
https://dw-inductionheater.com/induction-brazing-steel-to-carbide.html?feed_id=249813&_unique_id=666bdf20c06c2
2020年4月18日星期六
induction brazing stainless steel to steel
High frequency magnetic induction brazing stainless steel to steel process
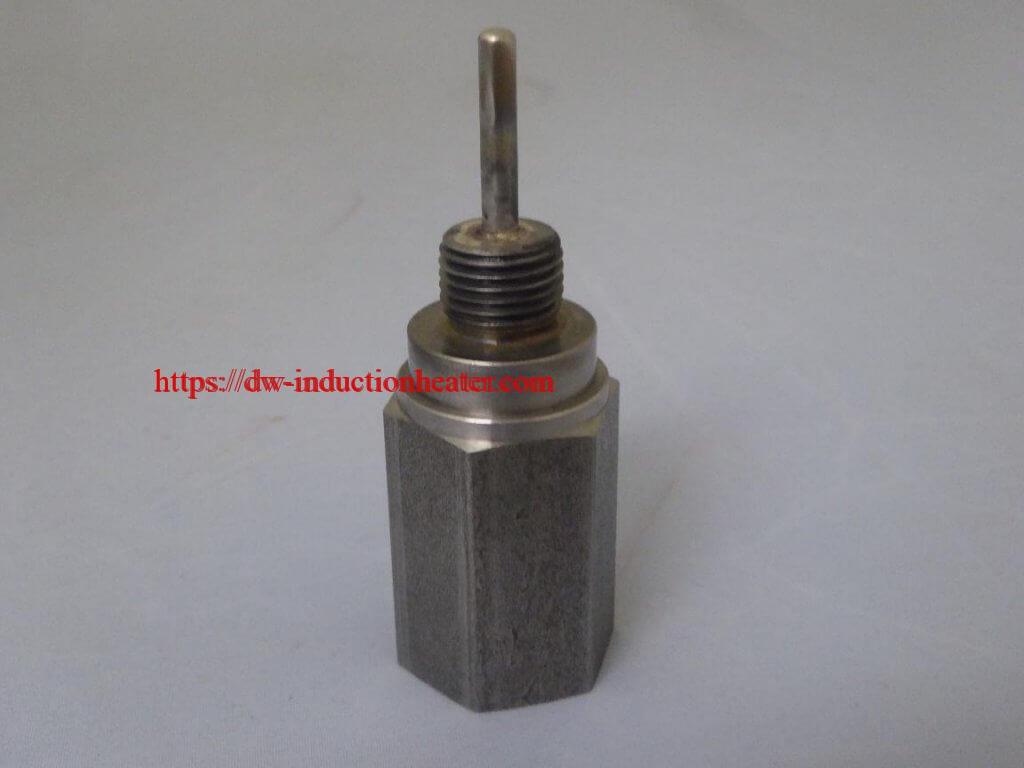
HLQ team was provided with 2 different parts to be brazed in our test laboratory.
Objective: Induction Brazing of a 0.15’’/ 3.81mm stainless steel pin to a steel base.
Equipment: DW-UHF-6KW-III handheld induction brazing system
Industry: Appliances & HVAC
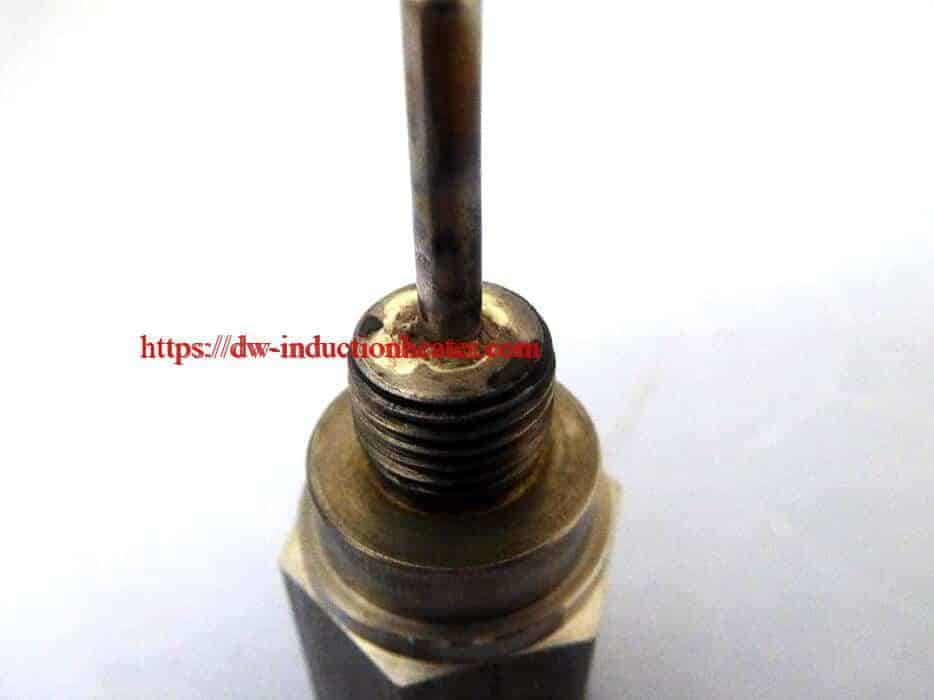
Materials:
Steel hexagon (base 1’’/ 25.4 mm diameter; 0.1’’/ 2.54 mm wall thickness)
A stainless steel pin (0.15’’/ 3.81 mm)
Other Materials:
All-purpose black brazing flux
Power: 1.43 kW
Temperature: 1400 °F/ 760°C
Time: 8 seconds
Process:
The two workpieces were carefully positioned together. All-purpose induction brazing black flux was added because it is ideal for high-temperature applications where rapid, localized heating is needed. The process of induction brazing was performed successfully within 8 seconds by using the DW-UHF-6KW-III handheld induction brazing system, producing the induction heating power of 1.43 kW at 1400 °F/ 760°C.
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-stainless-steel-to-steel-process.png?v=1587196467
https://dw-inductionheater.com/high-frequency-magnetic-induction-brazing-stainless-steel-to-steel-process.html
brazing stainless steel, brazing stainless steel to steel, HF brazing stainless steel, High Frequency Brazing steel, induction brazing, induction brazing machine, induction brazing stainless steel, induction brazing stainless steel to steel
2020年3月28日星期六
Induction Brazing Steel Parts to Tungsten Carbide Plate
Induction Brazing Steel Parts to Tungsten Carbide Plate
Objective
Induction Brazing of Steel Parts to a Tungsten Carbide Plate
Equipment
DW-UHF-6KW-III handheld induction brazing machine
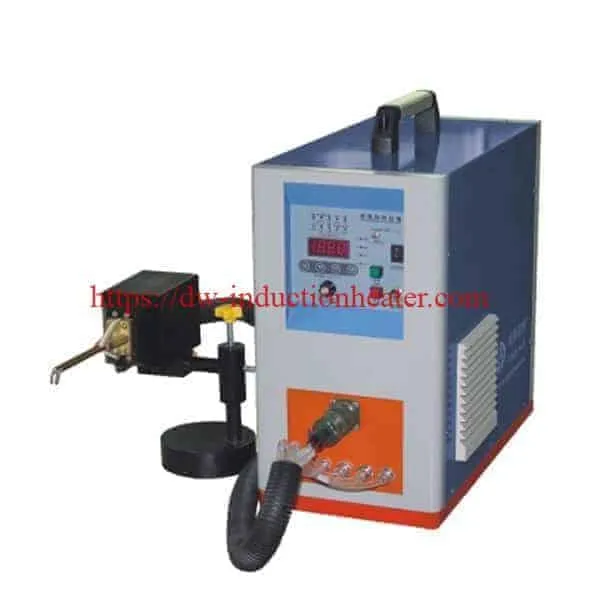
Test 1
Materials
• Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length
• Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness
• Alloy: 19.05 mm (0.75″) Brazing discs
Power: 4.0 kW
Temperature: Approximately 760° C (1400° F)
Time: 40 sec
Test 2
Materials
• Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness
• Alloy: 12.7 mm (0.50″) Brazing discs
Power: 2.36 kW
Temperature: Approximately 760° C (1400° F)
Time: 23 sec
Test 3
Materials
• Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness
• Alloy: 12.7 mm (0.50″) Brazing discs
Power: 2.36 kW
Temperature: Approximately 760° C (1400° F)
Time: 20-25 sec (Pulsing on/off)
Test 4
Materials
• Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes
• Alloy: 6.35 mm (0.25″) Brazing discs
Power: 1.96 kW
Temperature: Approximately 760° C (1400° F)

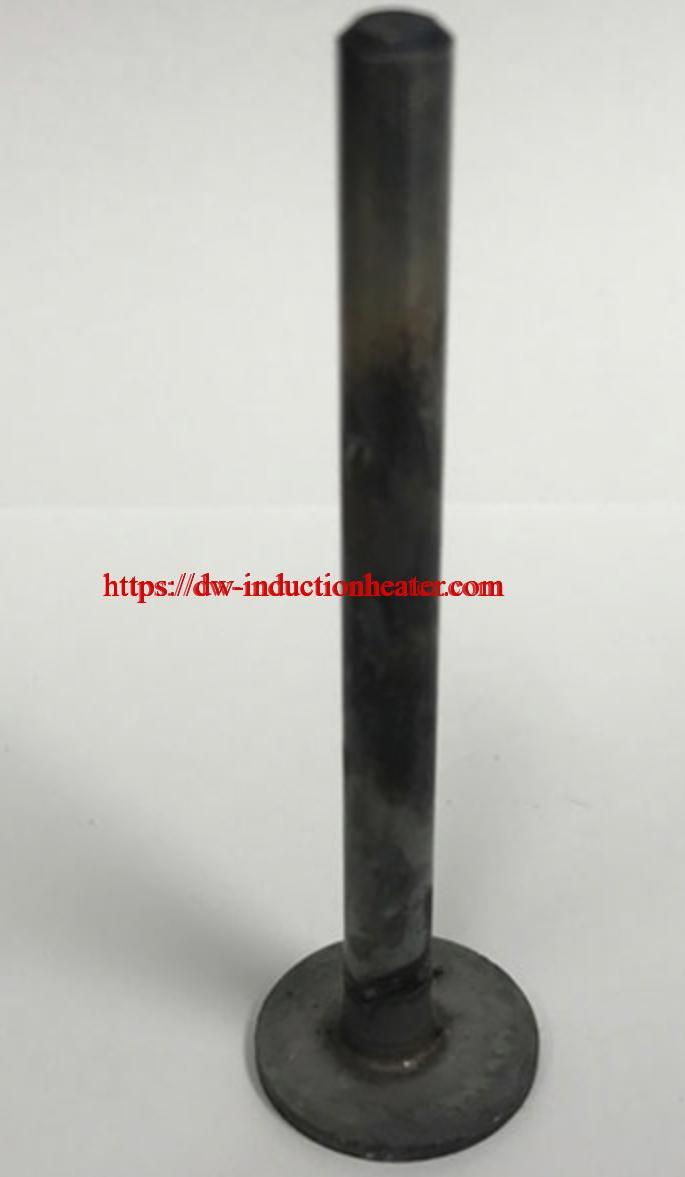
Time: 20 sec (Pulsing on/off)
Results and Conclusions:
Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
https://dw-inductionheater.com/wp-content/uploads/2020/03/4C736463-2605-4E33-8201-8092BCECA194-1024x633.jpeg
https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html
brazing carbide, brazing steel, brazing steel parts, Brazing tungsten carbide, High Frequency Brazing steel, induction brazing carbide, induction brazing steel, steel brazing
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.