 https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90
2025年2月21日星期五
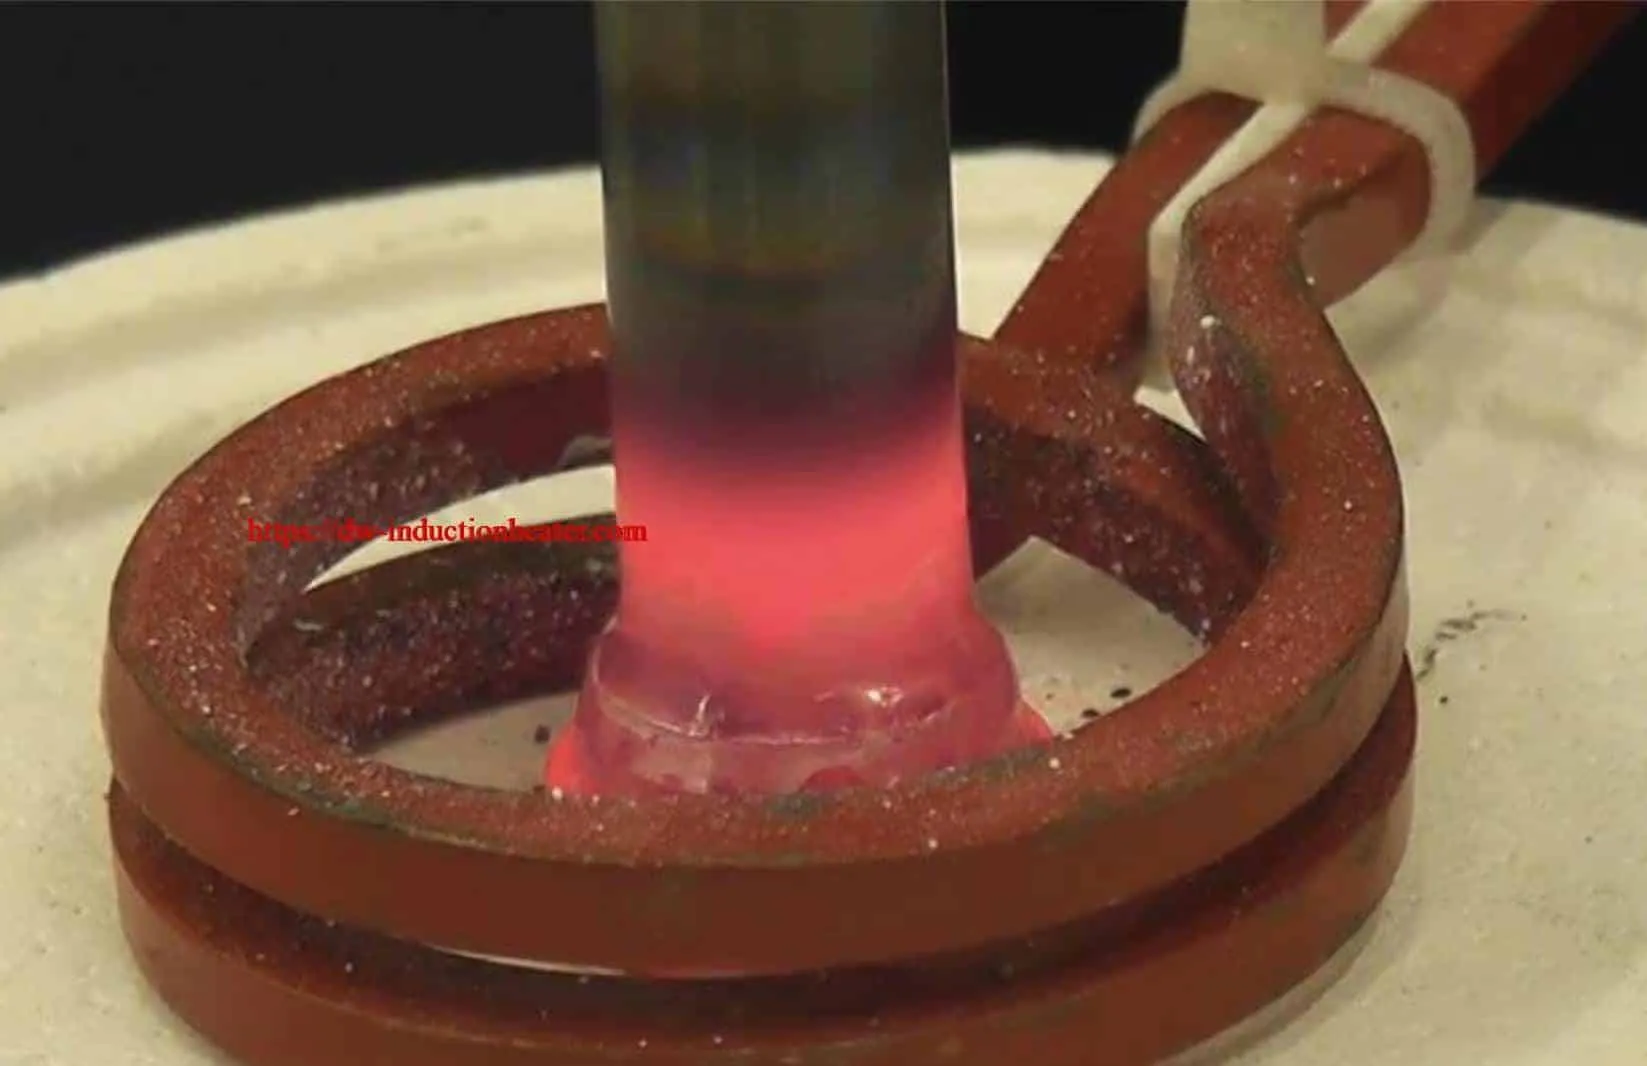
High frequency induction brazing steel tube to steel fitting
High frequency induction brazing steel tube to steel fitting
https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90
https://dw-inductionheater.com/high-frequency-induction-brazing-steel-tube-to-steel-fitting.html?feed_id=270445&_unique_id=67b9371943a90

2025年2月16日星期日
Induction Brazing Steel Parts to Tungsten Carbide Plate
Induction Brazing Steel Parts to Tungsten Carbide Plate
 https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html?feed_id=269865&_unique_id=67b24b1830232
2024年11月27日星期三
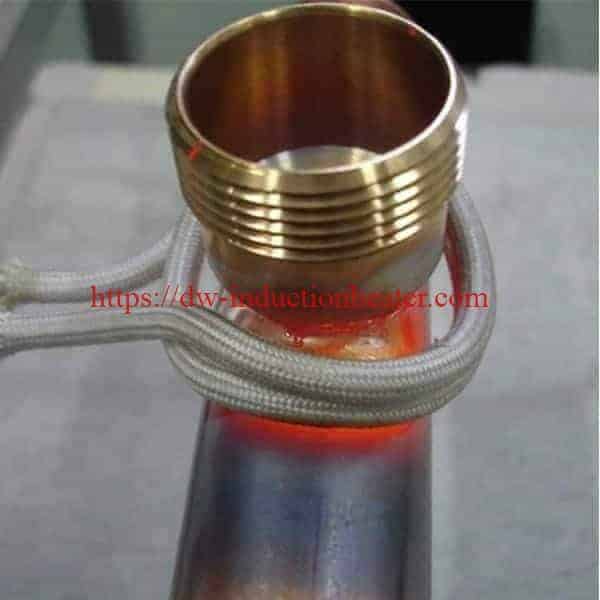
Induction Brazing Stainless Steel To Brass
Induction Brazing Stainless Steel To Brass
 https://dw-inductionheater.com/product/induction-brazing-stainless-steel-to-brass?feed_id=262006&_unique_id=674788a06f3bc
2024年7月7日星期日
Induction Brazing Steel Pipe
 Induction Brazing Steel Pipe
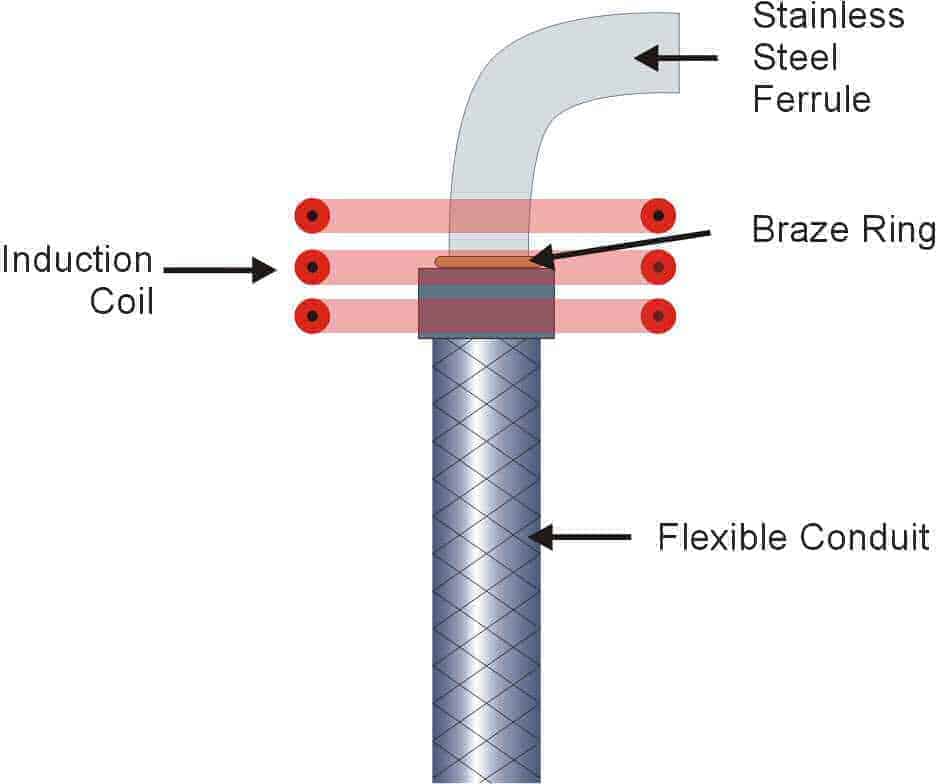
Objective: To heat a stainless steel pipe, ferrule and elbow assembly to 1400°F (760°C) within 20 seconds for brazing.
Material 6"(152.4mm)long x 0.5"(12.7mm) diameter stainless steel conduit, 0.5"(12.7mm) long x 0.5"(12.7mm) diameter ferrule, 2"(50.8mm) elbow with 0.5" (12.7mm) diameter
Temperature 1400°F (760°C)
Frequency 400 kHz
Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead • An induction heating coil designed and developed specifically for this application.
Process: A specially designed, three-turn helical coil is used to provide heat to the assembly at the braze joint area. Two small silver solder braze rings are placed at each joint; the joints are coated with black flux to insure that the braze material flows cleanly. The assembly is placed inside the coil and power is applied for 15 seconds to cause the braze to flow.
Results/Benefits: Induction heating provides: • Consistent and repeatable results • No flame process • Faster process time
https://dw-inductionheater.com/induction-brazing-steel-pipe.html?feed_id=253065&_unique_id=668a9431e0f3d
2024年6月23日星期日
Brazing Steel To Steel Pipe With Induction
 Brazing Steel To Steel Pipe With Induction
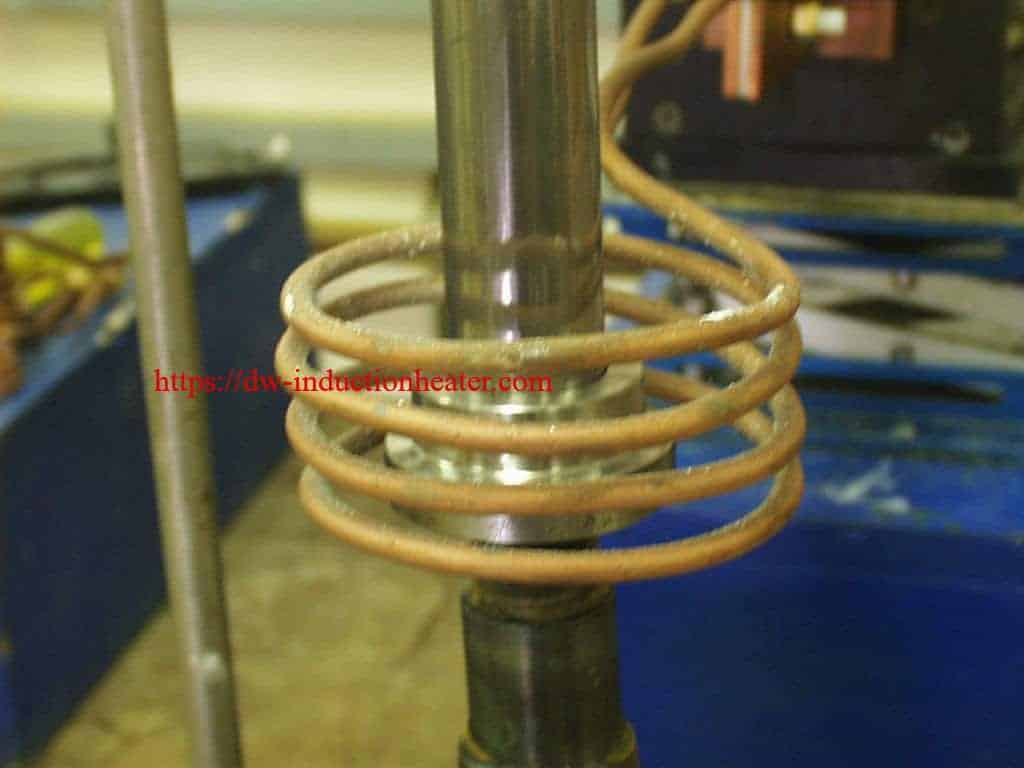
Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube.
Material
• Steel tube, 1 inch (2.54 cm) OD
• O-ring Face Seal sleeve and a male connector fittings
• Preform braze rings
• White SureFlow flux
• Steel support mandrel
Temperature 1300 ºF (704 ºC)
Frequency 200 kHz
Equipment
• DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF).
• An induction heating coil designed and developed specifically for this application.
Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows.
Results/Benefits Advantages :
• Large Inner diameter of coil allows for easy loading and unloading of parts
• With efficient energy coupling of the coil to the fittings overheating is avoided.
https://dw-inductionheater.com/brazing-steel-to-steel-pipe-with-induction.html?feed_id=251012&_unique_id=667803160f4db
2024年6月18日星期二
Brazing Golf Ball With Induction
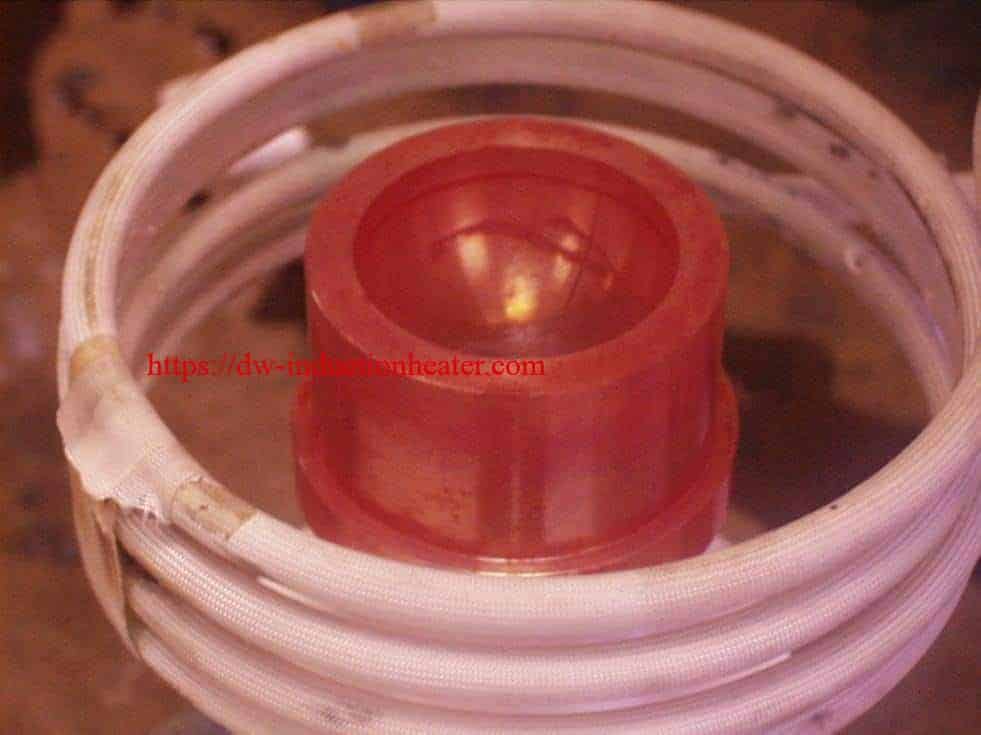 Brazing Golf Ball With Induction
Objective: Heating steel golf ball mold to brazing dimple insert
Material: Golf ball mold 2” in diameter, braze flux paste, dimple insert
Temperature: 1400 ºF (760 ºC)
Frequency: 260 kHz
Equipment • DW-UHF-10kW induction heating system, equipped with a remote workhead containing two 0.5μF capacitors for a total of 0.25 μF
• An induction heating coil designed and developed specifically for this application.
Process A four turn helical coil is used to heat the golf ball mold to 1400ºF (760 ºC) in 3 minutes and the dimple insert is brazed to the mold with braze flux paste.
Results/Benefits Induction heating provides:
• No flame process.
• Reliable, repeatable, non contact and energy efficient heat in minimal time.
• Even distribution of heating.
https://dw-inductionheater.com/brazing-golf-ball-with-induction.html?feed_id=250439&_unique_id=66724c817804f
2024年6月13日星期四
Induction Brazing Steel To Carbide Plate
 Induction Brazing Steel To Carbide Plate
Objective Brazing a steel piston valve assembly
Material Steel piston valve 4.5” dia (11.43cm), tungsten carbide plate and braze
Temperature 1350 ºF
Frequency 100 kHz
Equipment •DW-UHF-40kW induction heating system, equipped with a remote workhead containing six 1.0μF capacitors for a total of 1.5μF
• An induction heating coil designed and developed specifically for this application.
Process A five turn pancake coil is used to braze the piston valve and tungsten carbide plate. The assembly was heated for 10 minutes to flow the braze and join the two pieces.
Results/Benefits Induction heating provides:
• Rapid localized heat, which can minimize oxidation and reduce cleaning after joining
• Hands-free heating that involves no operator skill for manufacturing
• Clean and controllable joints
• Produces high quality repeatable parts
https://dw-inductionheater.com/induction-brazing-steel-to-carbide.html?feed_id=249813&_unique_id=666bdf20c06c2
2024年6月11日星期二
Induction Brazing Steel Tips
 Induction Brazing Steel Tips with Hihg Frequency Heating System
Objective To heat a steel tip and shank assembly to 1300°F (704°C) within 3 seconds for brazing with induction heating instead of torch brazing.
Material 0.1” (2.54mm) diameter steel tip & shank, 0.07” (1.78mm) diameter braze ring
Temperature 1300°F (704°C)
Frequency 800kHz
Equipment DW-UHF-4.5kW induction heating system, remote heat station containing one 1.2 microfarad capacitor.
Process A two turn helical coil is used to braze the dental parts. The braze ring is placed at the joint area of the steel tip and shank. Black flux is applied to the joint area. RF power is applied for 3 seconds to heat the parts to the established target temperature and the braze paste flows evenly and consistantly.
Results/Benefits Induction heating provides:
• Fast, accurate, repeatable heat
• Ability to heat very small areas within precise production tolerances
• Better joint quality, reduced oxidation
• Increased production rates and reduced labor costs
https://dw-inductionheater.com/induction-brazing-steel-tips.html?feed_id=249541&_unique_id=666903c7a5ab2
2020年3月28日星期六
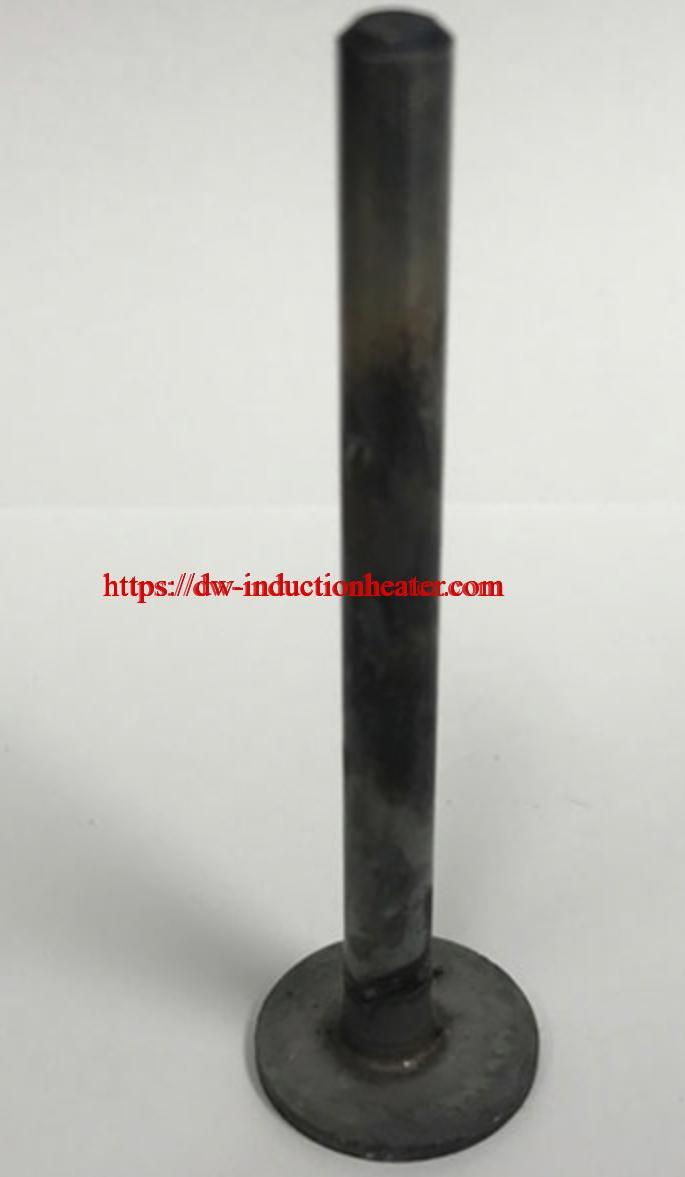
Induction Brazing Steel Parts to Tungsten Carbide Plate
Induction Brazing Steel Parts to Tungsten Carbide Plate
Objective
Induction Brazing of Steel Parts to a Tungsten Carbide Plate
Equipment
DW-UHF-6KW-III handheld induction brazing machine
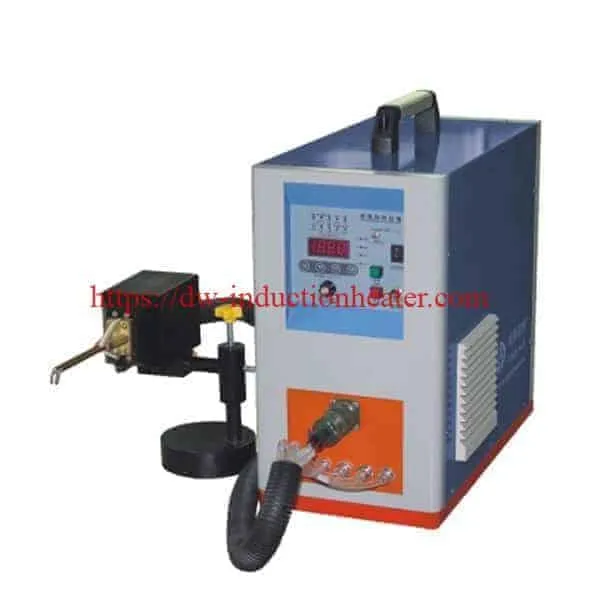
Test 1
Materials
• Steel rod: 19.05 mm (0.75″) OD, 82.55 mm (3.25″) Length
• Tungsten Carbide Plate: 38.1 mm (1.5″) OD, 10.16 mm (0.4″) Thickness
• Alloy: 19.05 mm (0.75″) Brazing discs
Power: 4.0 kW
Temperature: Approximately 760° C (1400° F)
Time: 40 sec
Test 2
Materials
• Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 19.05 mm (0.75″) OD, 6.35 mm (0.25″) Thickness
• Alloy: 12.7 mm (0.50″) Brazing discs
Power: 2.36 kW
Temperature: Approximately 760° C (1400° F)
Time: 23 sec
Test 3
Materials
• Steel rod: 12.7 mm (0.50″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 1″ OD, 1.39mm (0.055″) Thickness
• Alloy: 12.7 mm (0.50″) Brazing discs
Power: 2.36 kW
Temperature: Approximately 760° C (1400° F)
Time: 20-25 sec (Pulsing on/off)
Test 4
Materials
• Steel rod: 6.35 mm (0.25″) OD, 76.2 mm (3″) Length
• Tungsten Carbide Plate: 21.08mm (0.83″) OD, 1.65mm (0.065″) thicknes
• Alloy: 6.35 mm (0.25″) Brazing discs
Power: 1.96 kW
Temperature: Approximately 760° C (1400° F)

Time: 20 sec (Pulsing on/off)
Results and Conclusions:
Brazing of different steel parts to carbide disks is possible with one induction coil. Power was regulated by turning the heat on and off using a foot switch to prevent overheating of the carbide parts.
https://dw-inductionheater.com/wp-content/uploads/2020/03/4C736463-2605-4E33-8201-8092BCECA194-1024x633.jpeg
https://dw-inductionheater.com/induction-brazing-steel-parts-to-tungsten-carbide-plate.html
brazing carbide, brazing steel, brazing steel parts, Brazing tungsten carbide, High Frequency Brazing steel, induction brazing carbide, induction brazing steel, steel brazing
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.