 https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61
2025年2月18日星期二
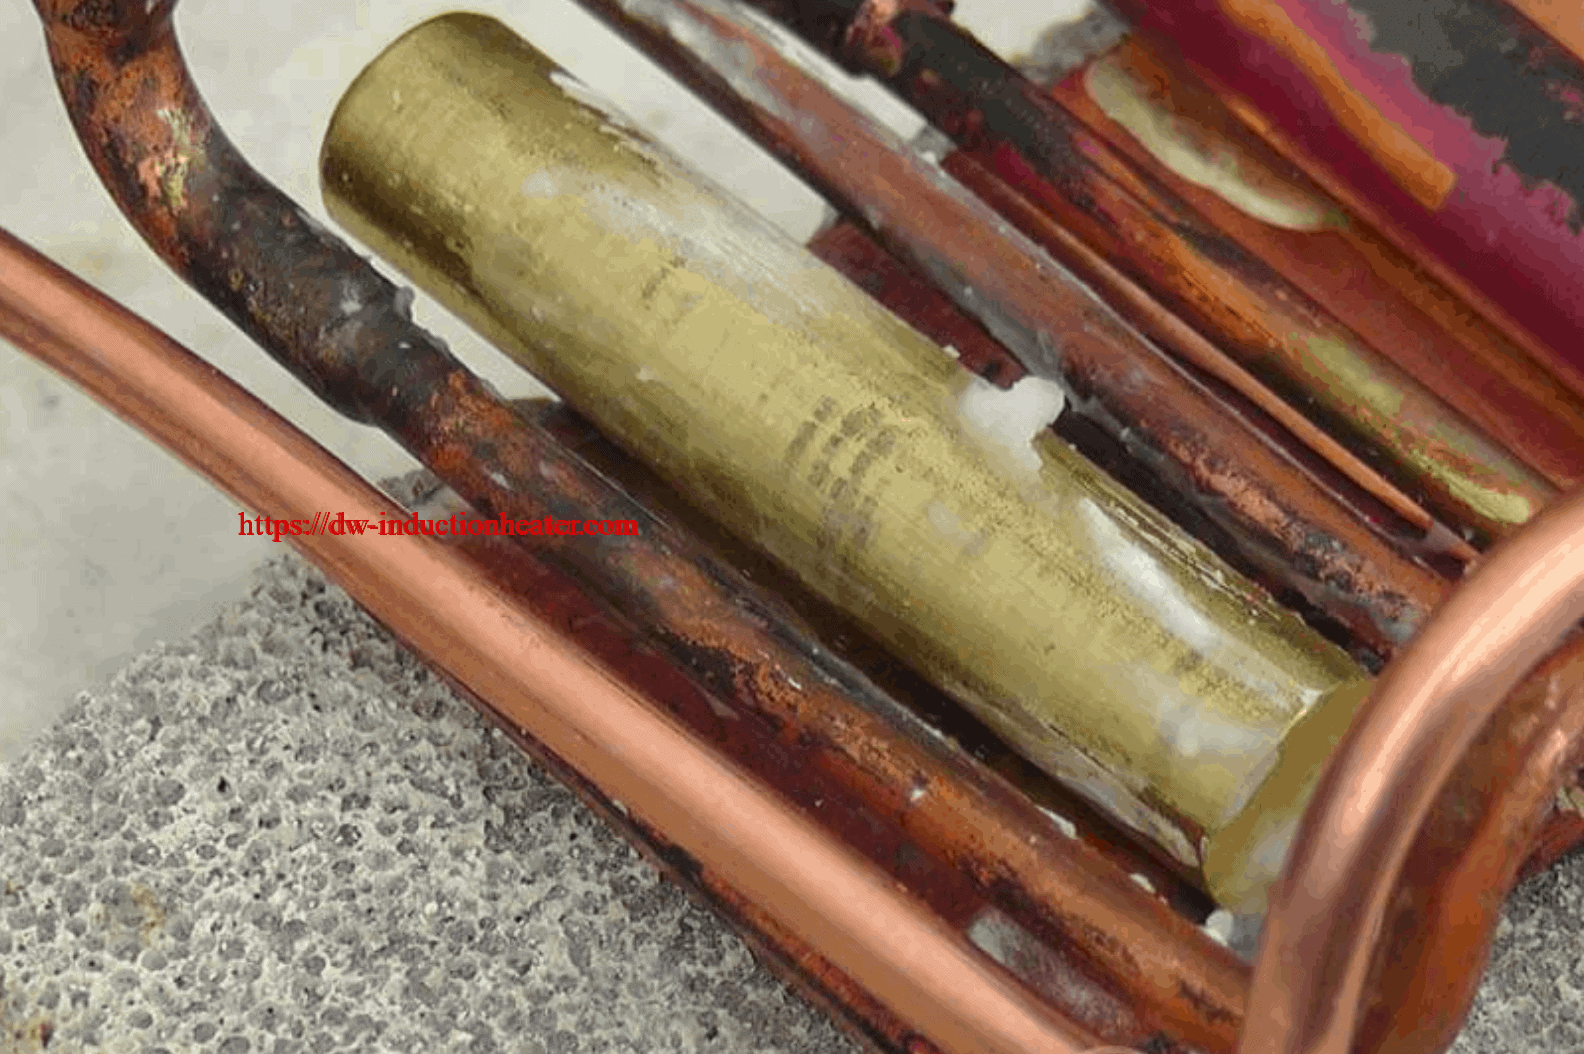
induction brazing copper and brass rods
induction brazing copper and brass rods
https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61
https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=270010&_unique_id=67b4458c8dc61

2025年1月25日星期六
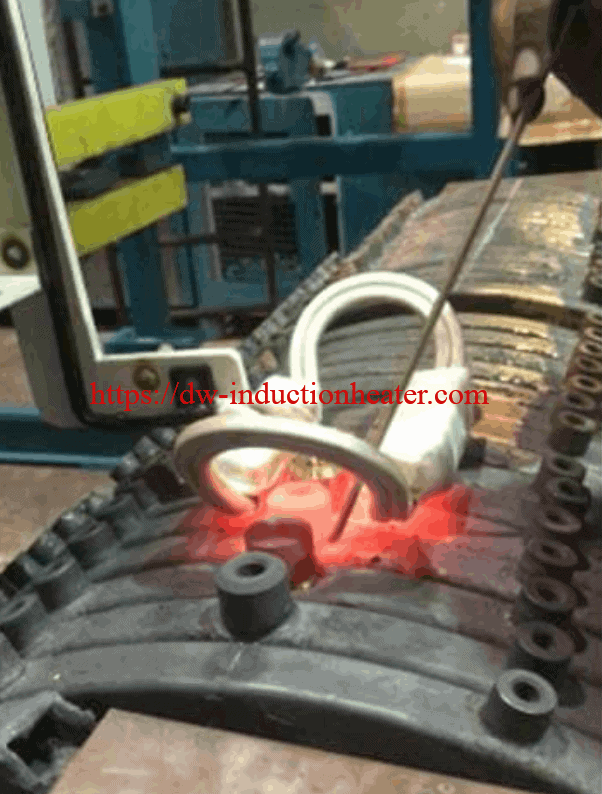
Induction Brazing Brass Studs to Copper Pipes
Induction Brazing Brass Studs to Copper Pipes
 https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html?feed_id=267748&_unique_id=67959eabde320
2025年1月17日星期五
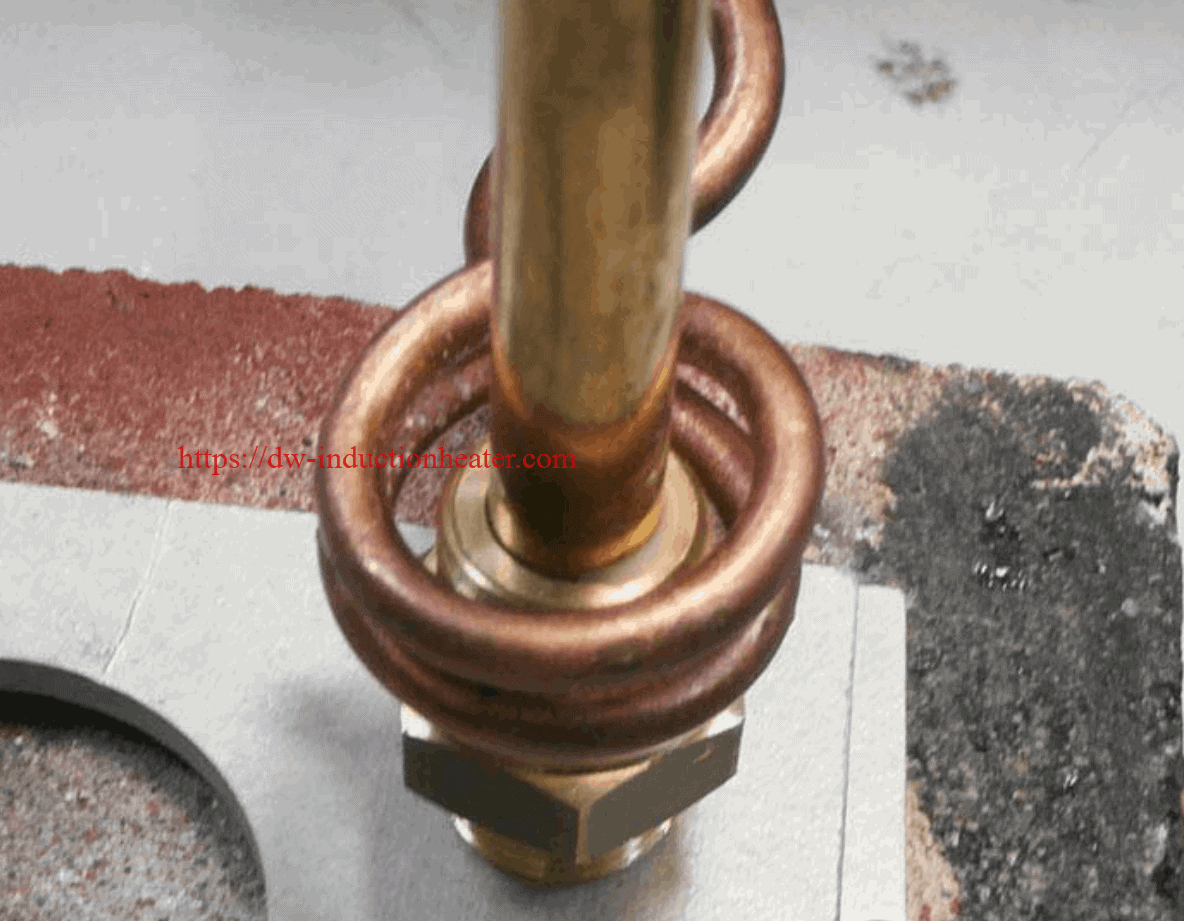
induction brazing brass pipe to brass part
induction brazing brass pipe to brass part
 https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html?feed_id=266936&_unique_id=678abe725a28b
2024年7月2日星期二
Brazing Brass Fittings With Induction
 Brazing Brass Fittings With Induction
Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm)
Material: Brass tubing Brass flange Braze rings Braze flux
Temperature :1382°F (750°C)
Frequency 200 kHz
Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application.
Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter.
Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes.
https://dw-inductionheater.com/brazing-brass-fittings-with-induction.html?feed_id=252426&_unique_id=6684ddcf51384
2024年6月26日星期三
Brazing Brass to Aluminum with Induction
 Brazing Brass to Aluminum with Induction
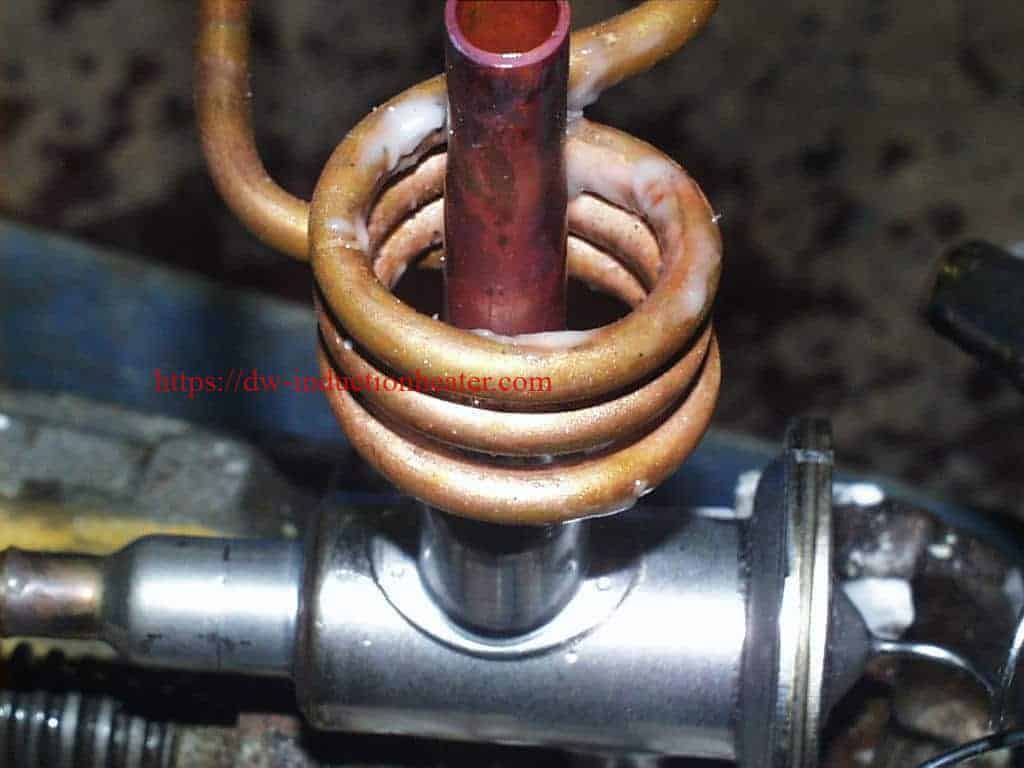
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material customer's valve copper fittings braze
Temperature 2550 ºF (1400°C)
Frequency 360 kHz
Equipment DW-UHF-10KW induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process The valve is placed inside the coil and RF power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
https://dw-inductionheater.com/brazing-brass-to-aluminum-with-induction.html?feed_id=251610&_unique_id=667c4c29db306
2024年6月13日星期四
Induction Brazing Brass Faucet
 Induction Brazing Brass Faucet
Objective Brazing two joints on a brass bathroom faucet assembly
Material Brass bathroom fittings 1” OD, brazing rings, flux
Temperature 1148 ºF (620 ºC)
Frequency 90 kHz
Equipment • DW-UHF-30 kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8.0 μF
• An induction heating coil designed and developed specifically for this application.
Process A two turn C shaped coil is used to braze the faucet assembly.
The braze rings are placed at the joint, the parts assembled and fluxed. The first braze joint is heated for 30 seconds and the braze ring flows. The assembly is rotated & the second joint is heated for 30 seconds to flow the braze ring. The two brazes are completed in 60 seconds.
Results/Benefits Induction heating provides:
• Faster, repeatable and consistent results
• Localized heat produces neat and clean joints
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
https://dw-inductionheater.com/induction-brazing-brass.html?feed_id=249745&_unique_id=666b28403ce61
2020年5月24日星期日
induction brazing brass pipe to brass part
Objective
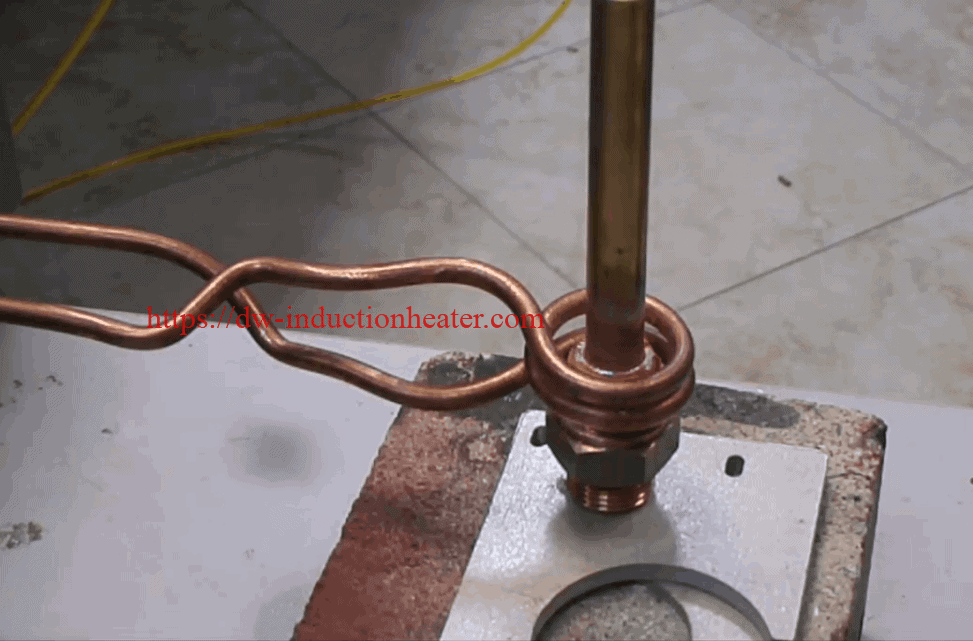
High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
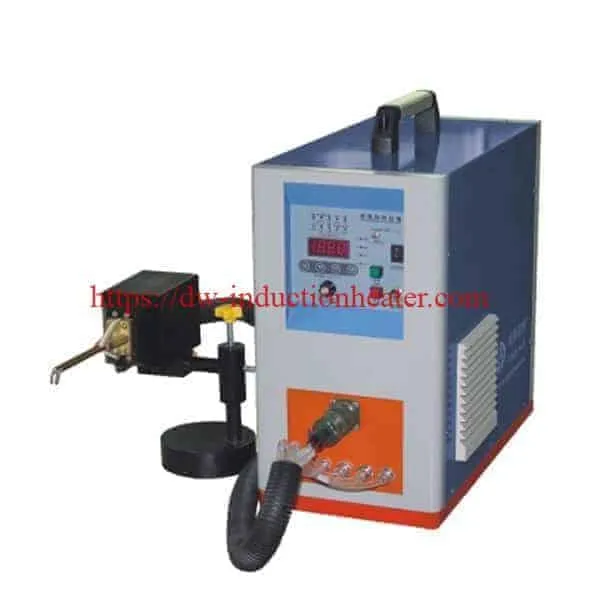
Equipment
DW-UHF-6KW-III handheld induction brazing machine
2 turns coil
Materials
• Wide brass part
• Brass pipe
• Silver-based brazing alloy, provided by customer
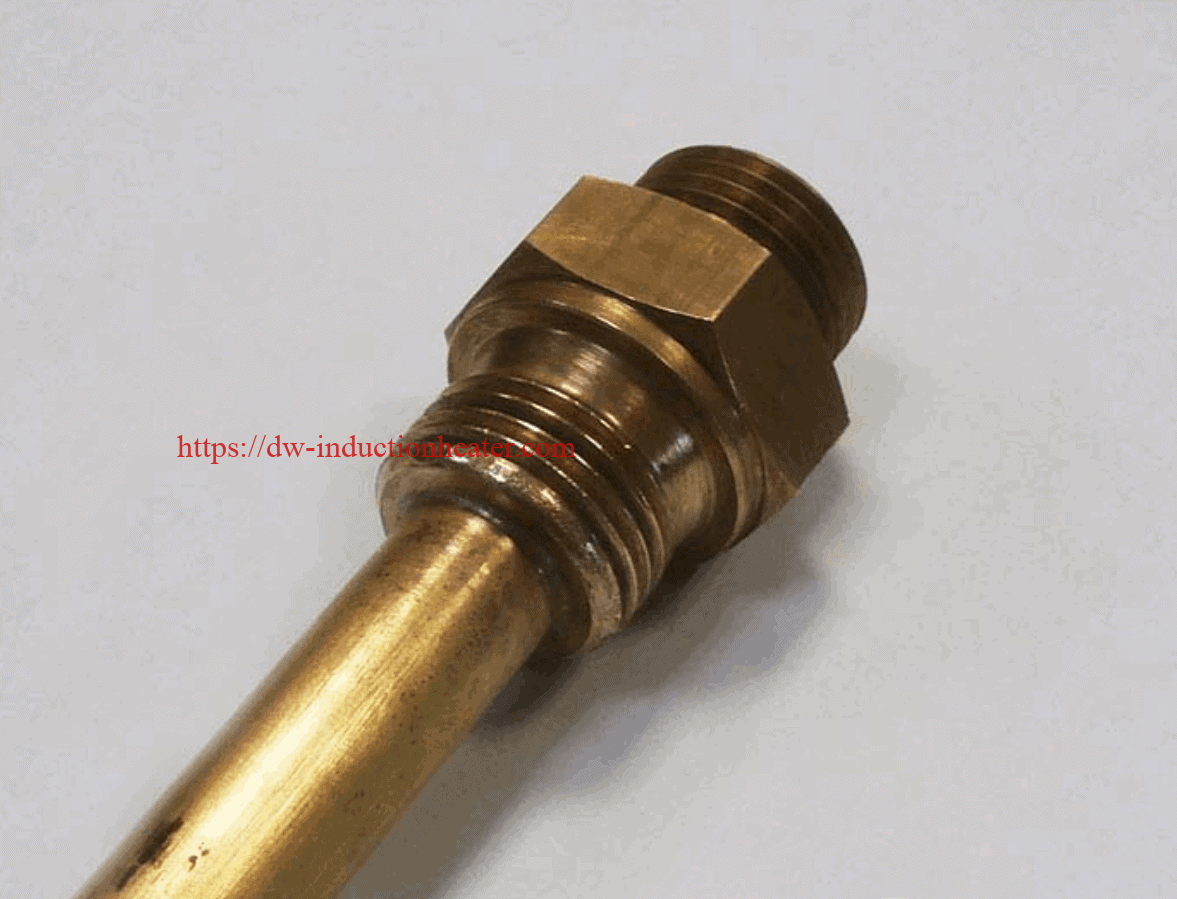
Test 1 – Pipe to wide part:
Key Parameters
Power: 4.4 kW
Temperature: Approximately 1400° F (760° C)
Time: 38 sec
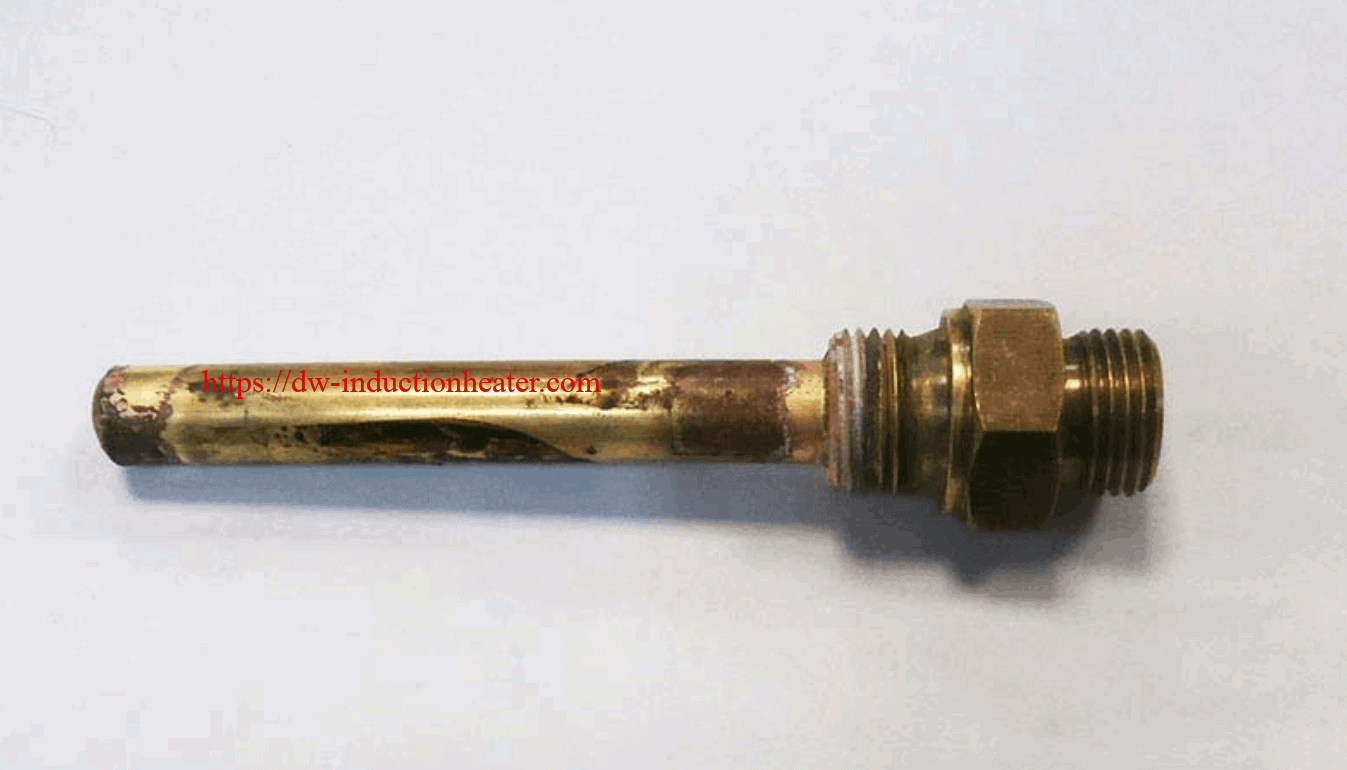
Test 2 – Pipe to tip:
Key Parameters
Power: 4.4 kW
Temperature: Approximately 1400° F (760° C)
Time: 17 sec
Process:
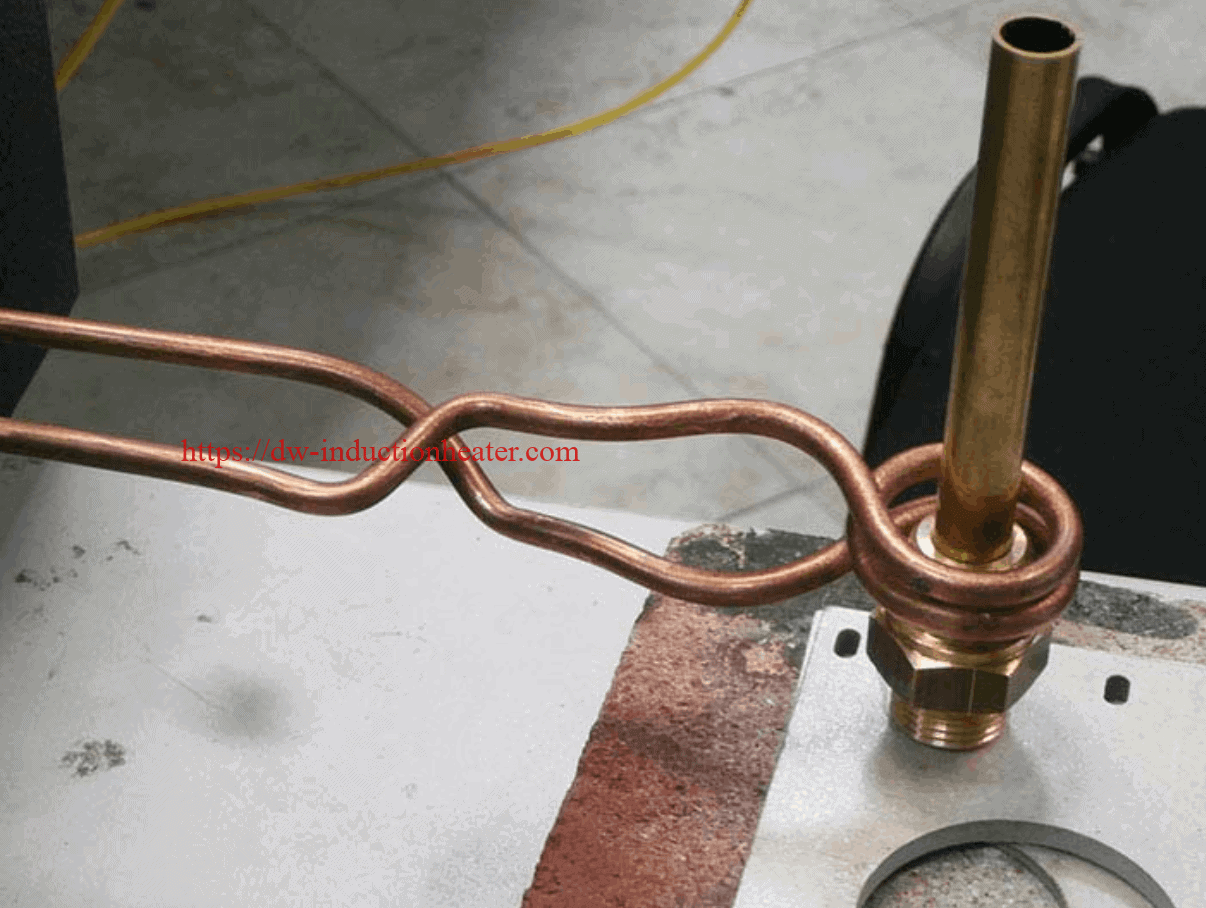
Test 1
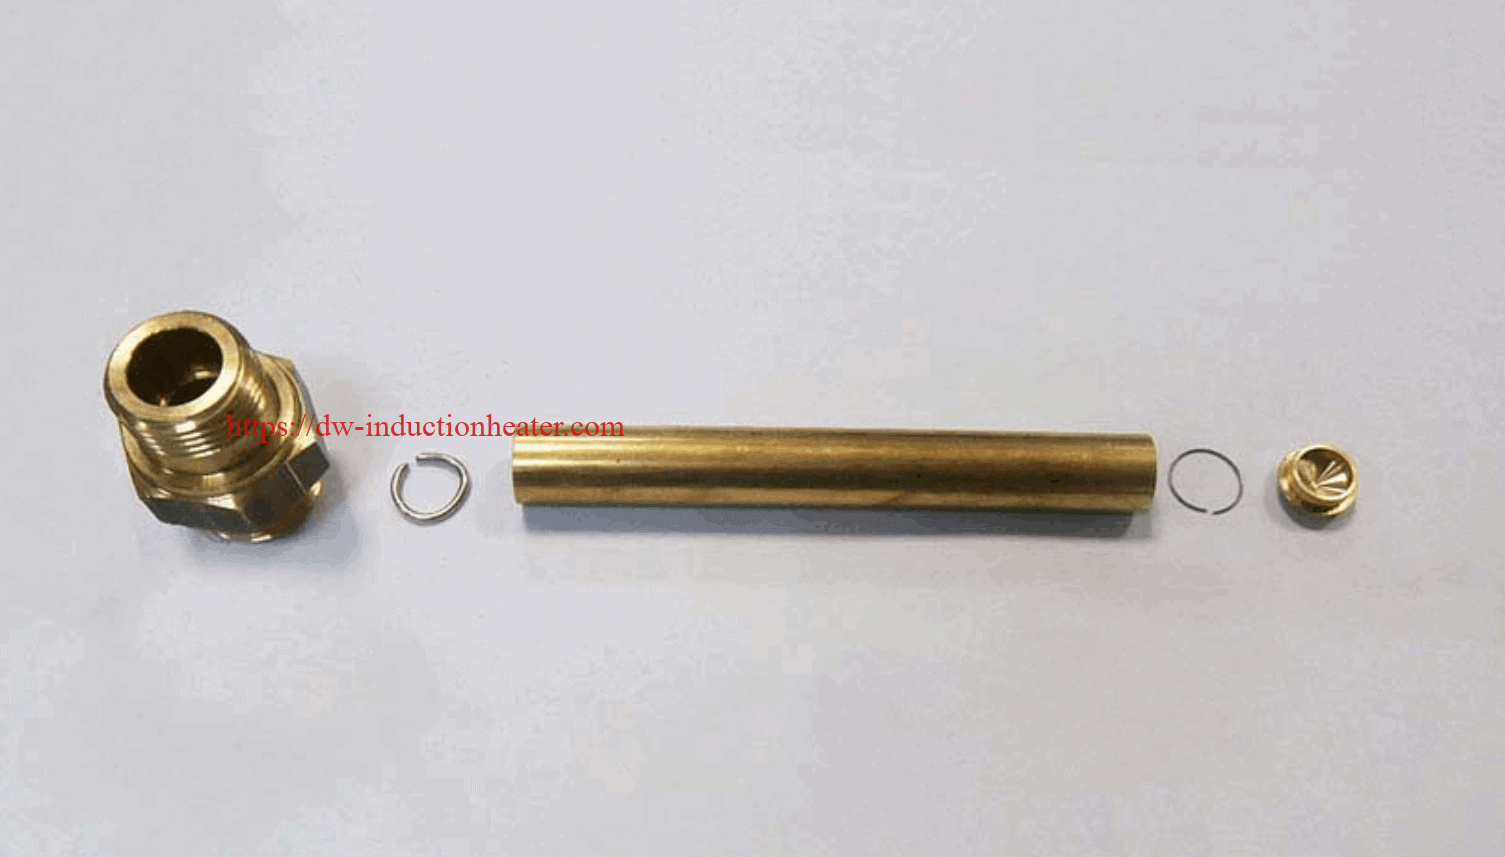
- The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
- The assembly is put inside the induction heating coil and induction heat is applied.
- The joint is completed in 38 seconds.
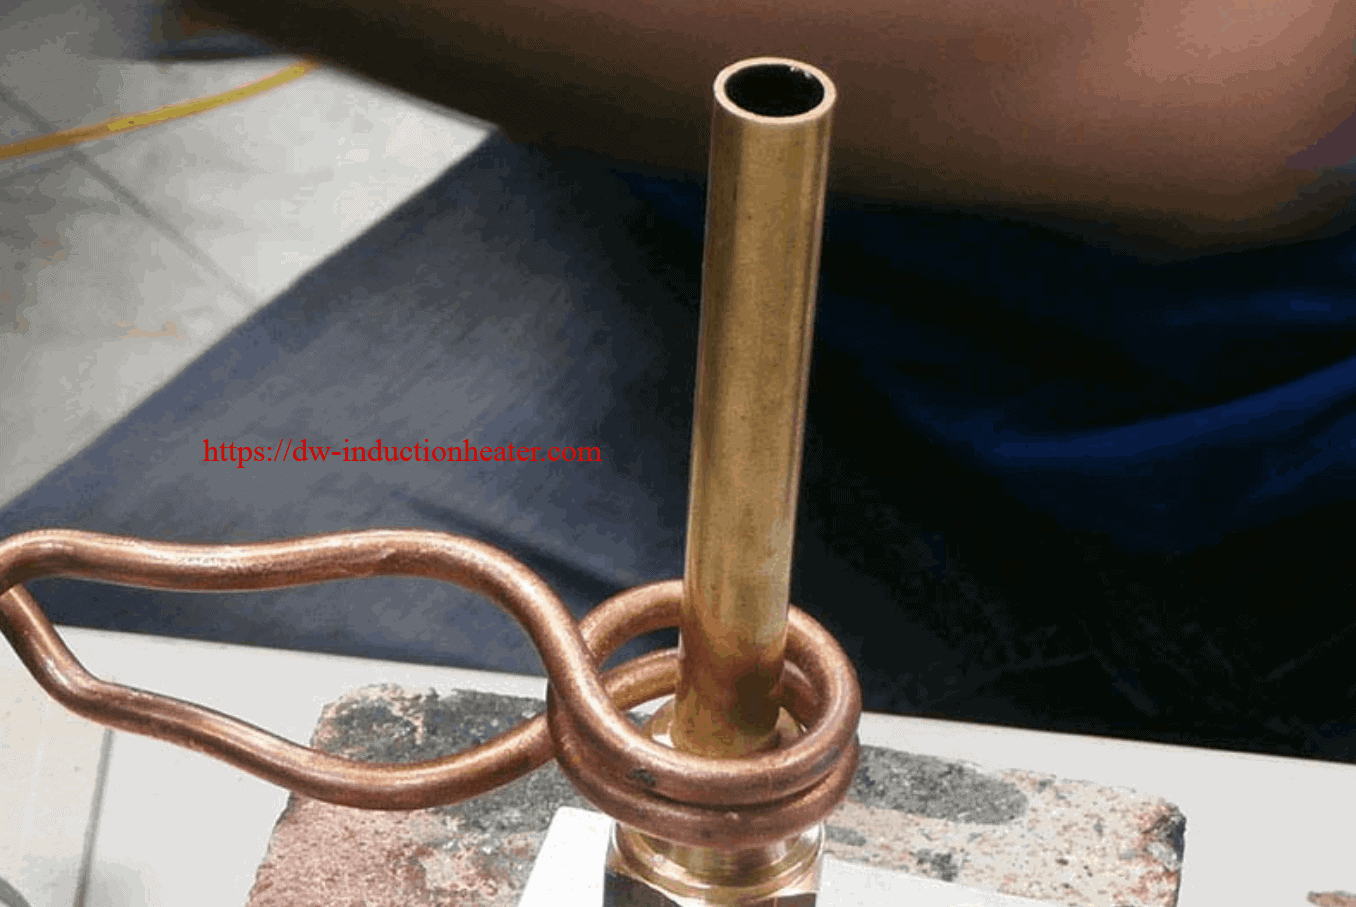
Test 2
- The tip and pipe are assembled and a brazing alloy ring is placed between them.
- The assembly is put inside the coil and induction heat is applied.
- The joint is completed in 17 seconds.
Results/Benefits:
Induction heating provides:
- Strong durable joints
- Selective and precise heat zone, resulting in less part distortion and joint stress than welding
- Less oxidation
- Faster heating cycles
- More consistent results and suitability for large volume production, without the need for batch processing
- Safer process than flame brazing
https://dw-inductionheater.com/wp-content/uploads/2020/05/induction-brazing-brass-pipe-to-brass-part3.png?v=1590326628
https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html
brazing brass, Brazing Brass pipe, brazing brass pipe machine, HF brazing brass, HF brazing brass part, HF brazing brass system, induction brass brazing, induction brazing brass, Induction Brazing Brass pipe, radio frequency brazing brass
2020年4月23日星期四
Induction Brazing Brass Studs to Copper Pipes
Induction Brazing Brass Studs to Copper Pipes
Objective:
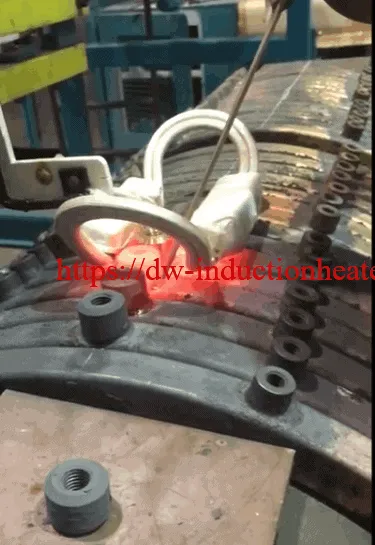
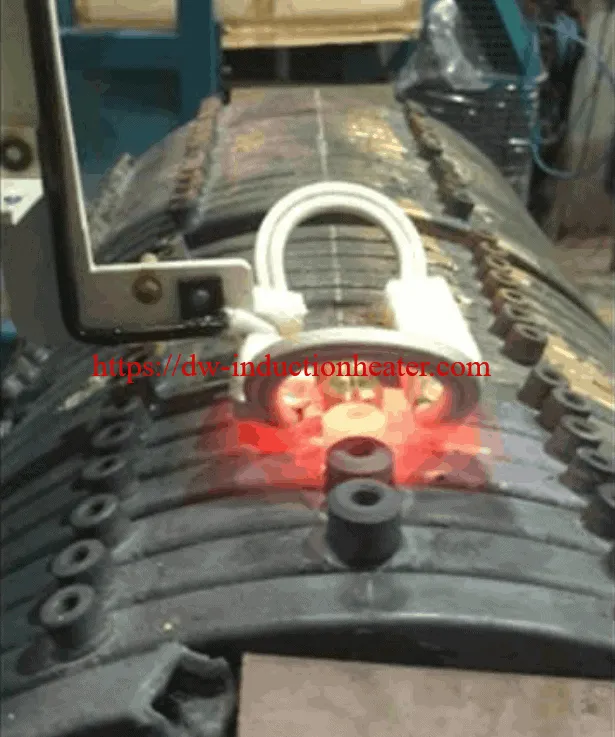
Induction brazing brass studs to copper pipes
The Client:
A manufacturer of coils for industrial heating applications.
Equipment:
DW-UHF-40KW Induction Brazing Systems – two modules.
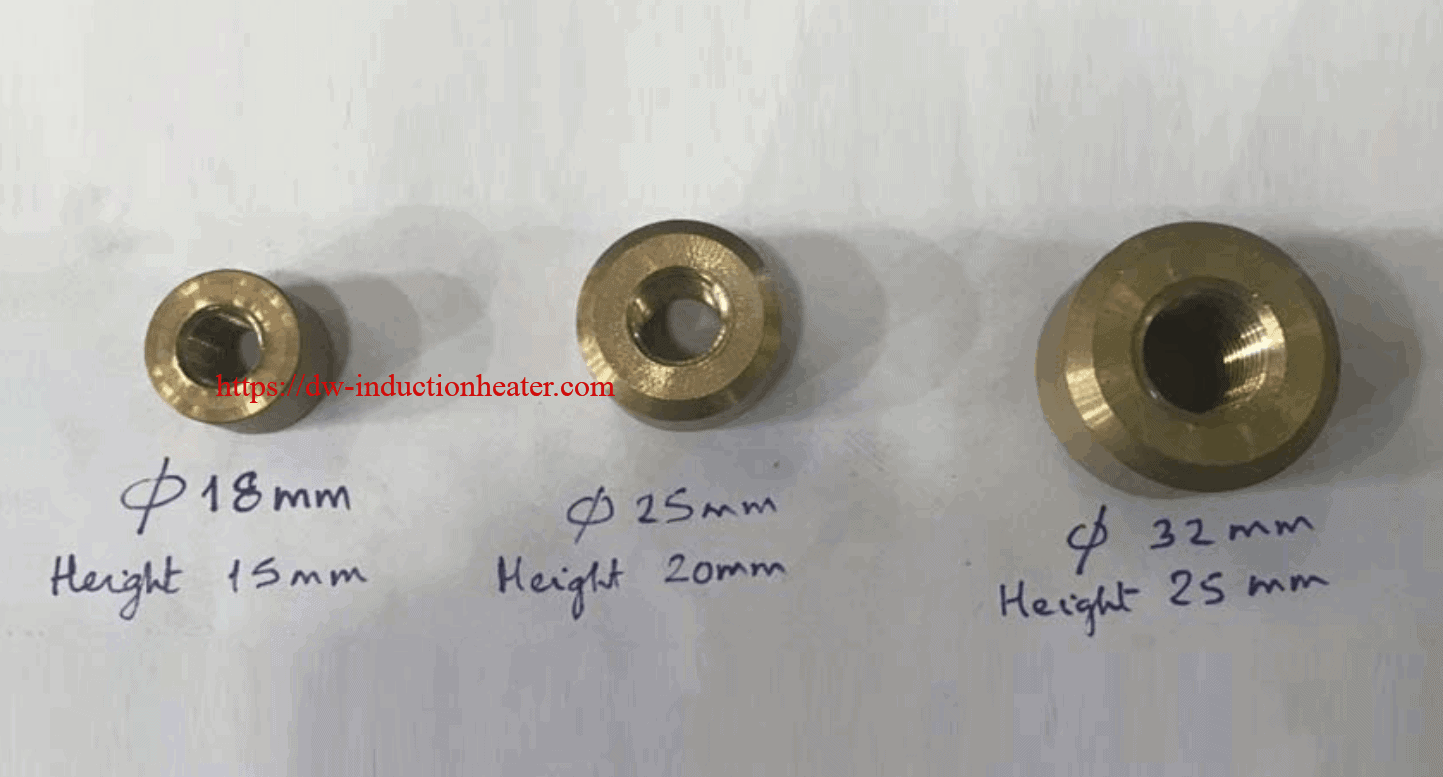
Materials: Brass stud ( size: 25mm diameter, 20 mm height )
Power: 30 kW
 The Process:
The main challenge during this induction brazing process is to ensure that the design of the coil is one that eases the technician to position it in the most convenient way. The induction coil should allow for the second stud to be pre-heated without melting the first one.
First, the electrolytic copper section is wound on a steel former by a gas torch while an equal spacing between the turns is maintained. Then, the copper turn is heated close to the required temperature and while the power is ON, the technician should make sure to manually position the brass stud with the brazing ring at the designated centre. During the process of brazing, the induction coil is moving at a speed of 58 mm per minute – 33 kW.
If the power is increased, the speed changes accordingly.
Results and Conclusions:
- A fast, clean and safe induction brazing process
- Guaranteed repeatability
- Precise control of time and temperature
https://dw-inductionheater.com/wp-content/uploads/2020/04/induction-brazing-brass-studs-to-copper.png?v=1587644202
https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html
brass studs brazing, brazing brass, brazing brass studs, brazing brass to copper, High Frequency Brazing brass, induction brazer, induction brazing brass, induction brazing copper, induction brazing copper system, induction brazing equipment, induction brazing system, induction brazing units
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.