 https://dw-inductionheater.com/brazing-aluminum-tubing-to-aluminum-parts.html?feed_id=267168&_unique_id=678db5c8dcdc1
2025年1月19日星期日
Brazing Aluminum Tubing to Aluminum Parts
Brazing Aluminum Tubing to Aluminum Parts
https://dw-inductionheater.com/brazing-aluminum-tubing-to-aluminum-parts.html?feed_id=267168&_unique_id=678db5c8dcdc1
https://dw-inductionheater.com/brazing-aluminum-tubing-to-aluminum-parts.html?feed_id=267168&_unique_id=678db5c8dcdc1

2024年6月28日星期五
Brazing Aluminum Pipes Assembly With Induction
 Brazing Aluminum Pipes Assembly With Induction
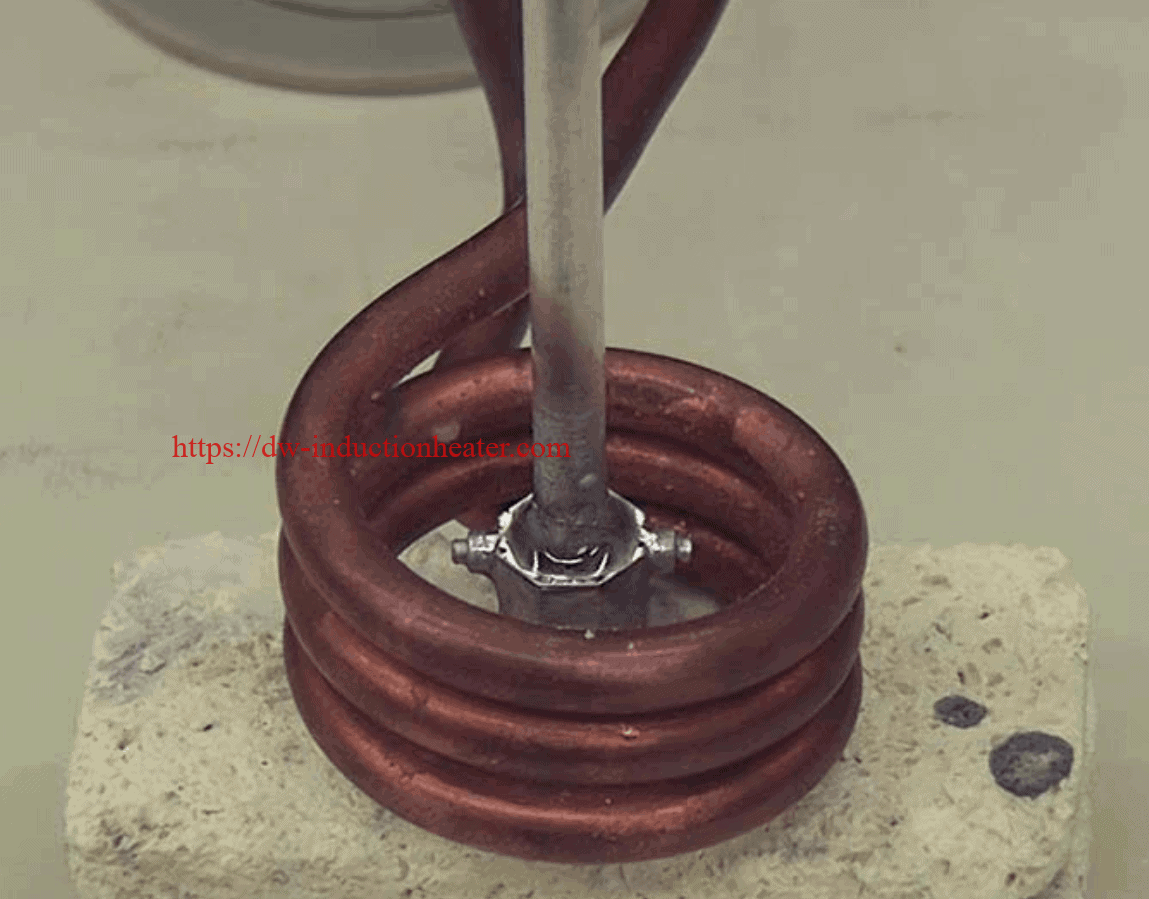
Objective: Braze an aluminum assembly to 968 ºF (520 ºC) within 20 seconds
Material : Customer supplied 1.33" (33.8 mm) O.D. aluminum tube and aluminum mating part ,Aluminum braze alloy
Temperature: 968 ºF (520 ºC)
Frequency 50 kHz
Equipment: DW-HF-35KW,30-80 kHz induction heating system equipped with a remote heat station containing one 53 μF capacitor A two-position helical induction heating coil designed and developed specifically for this application.
Process: Braze material was applied between the tubing and the mating part. The assembly was placed inside the coil and heated for approximately 40 seconds. With a two-position coil, two parts can be heated simultaneously, which means one part would be completed every 15-20 seconds. Braze material was stick fed, which created a good joint. The heating time with two parts being heated simultaneously meets the client's objective, and represents a significant improvement in regards to speed over using a torch.
Results/Benefits
- Speed: The recommended approach cut their heating time in half when compared to using a torch
- Part quality: Induction heating is a repeatable method with more consistency than a torch can generally deliver
- Safety: Induction heating is a clean, precise method that does not involve an open flame like a torch, which results in a safer work environment
Induction Aluminum Brazing Process
 Induction Aluminum Brazing Process
Induction aluminum brazing is becoming more and more common in industry. A typical example is brazing various pipes to an automotive heat exchanger body. Aluminum requires a lot of energy to heat using induction and its thermal conductivity is 60% compared to copper. Coil design and time for the heat to flow is critical in a successful induction brazing process for aluminum parts. Recent advances in lower temperature aluminum braze materials have allowed induction to effectively replace flame and furnace heating in high volume brazing of aluminum assemblies.
Successful Induction brazing of aluminum parts requires the correct braze filler material for the aluminum alloy used in the parts and the correct flux for the braze alloy. Braze filler manufacturers have their own proprietary aluminum braze alloys and flux materials that work with their alloys.
https://dw-inductionheater.com/induction-aluminum-brazing-process.html?feed_id=251814&_unique_id=667e70353f5d3
2024年6月26日星期三
Brazing Brass to Aluminum with Induction
 Brazing Brass to Aluminum with Induction
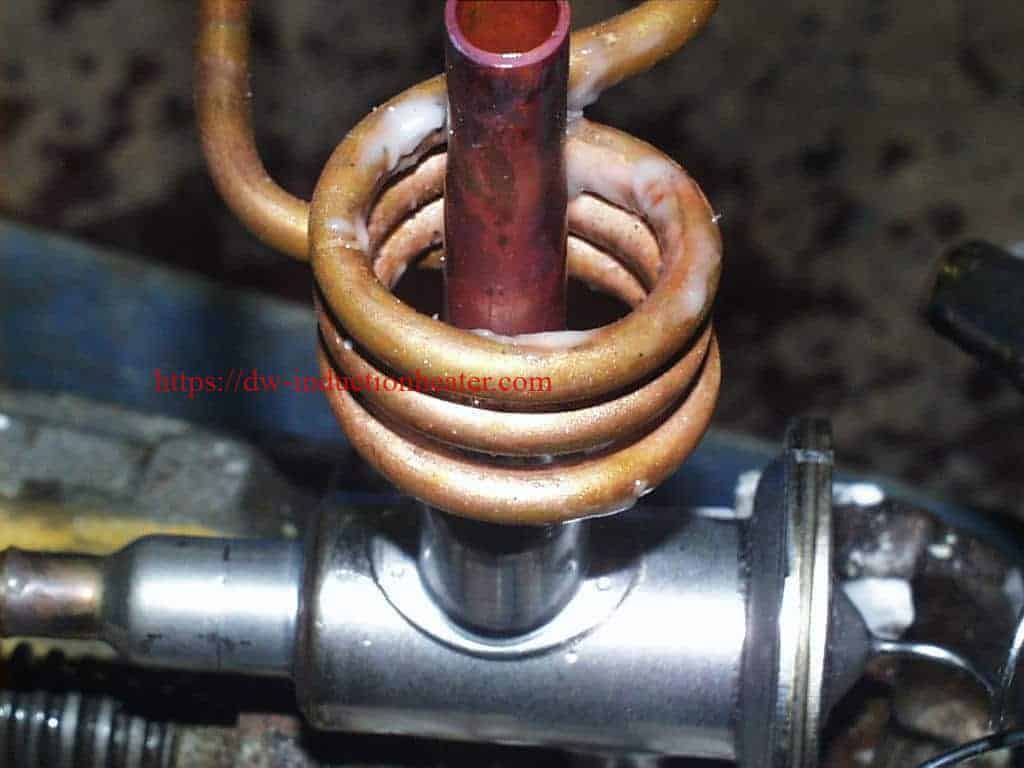
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material customer's valve copper fittings braze
Temperature 2550 ºF (1400°C)
Frequency 360 kHz
Equipment DW-UHF-10KW induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process The valve is placed inside the coil and RF power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
https://dw-inductionheater.com/brazing-brass-to-aluminum-with-induction.html?feed_id=251610&_unique_id=667c4c29db306
2020年5月17日星期日
Brazing Aluminum Tubing to Aluminum Parts
Objective
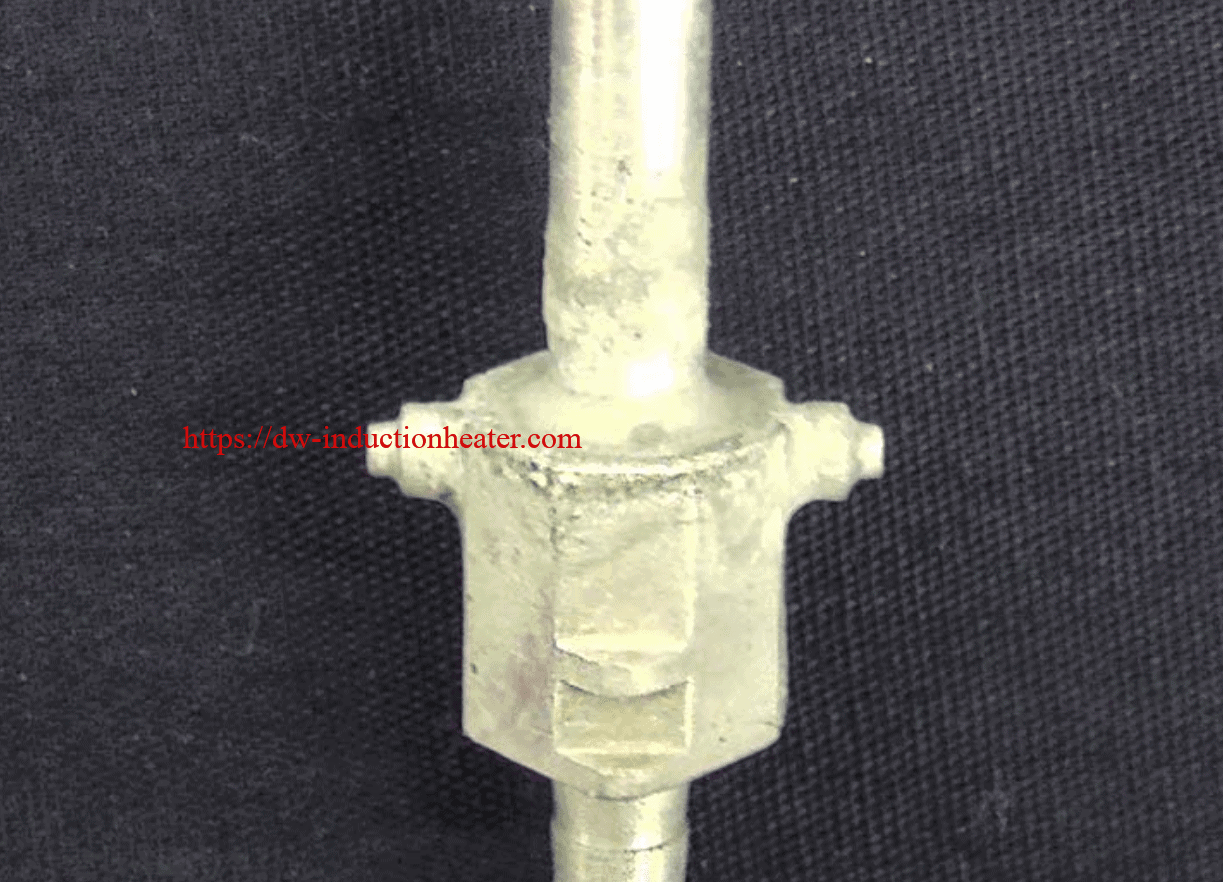
The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment
DW-HF-15kw induction heating machine
Materials
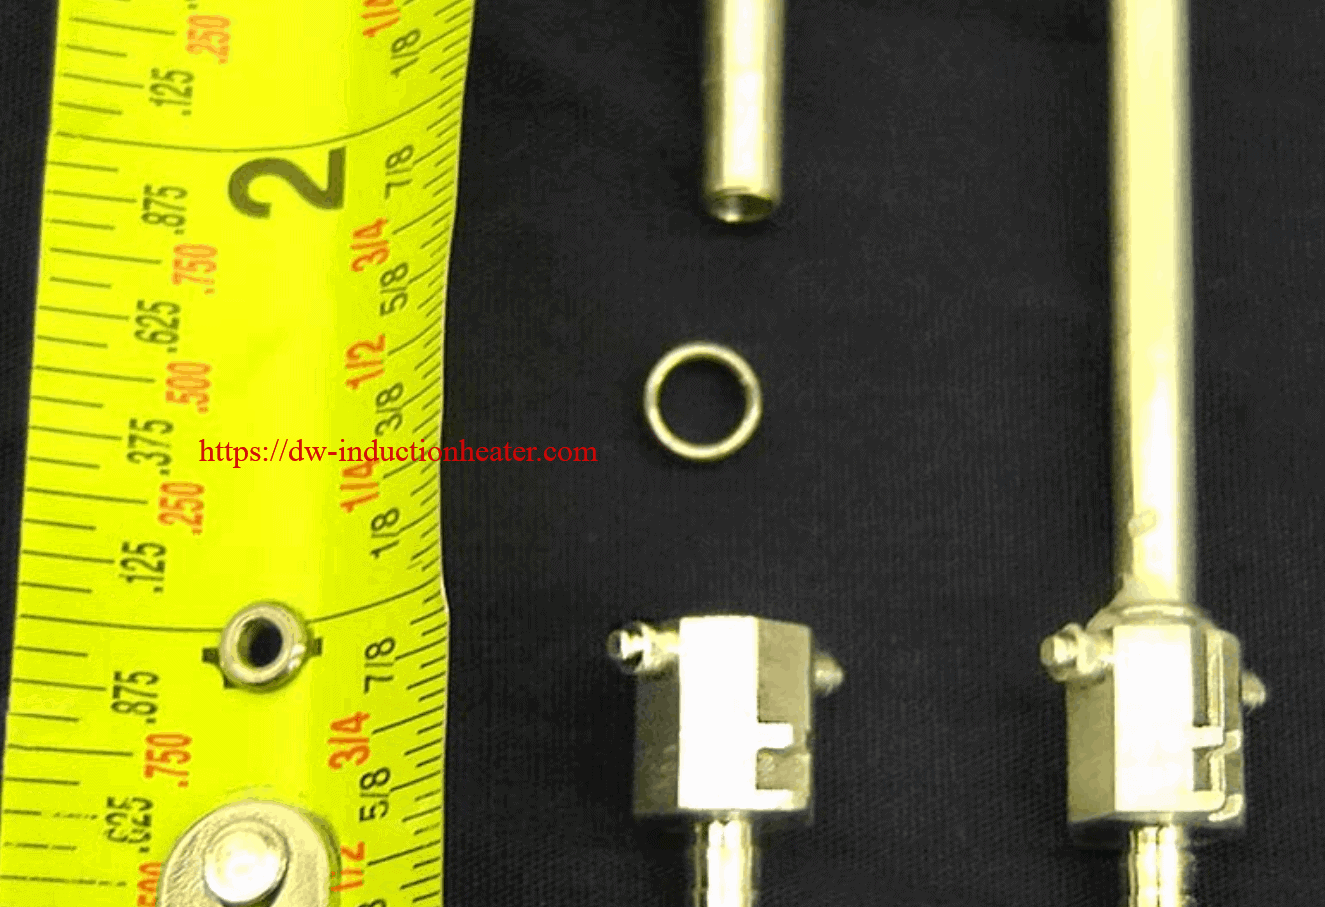
• Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID
• Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm),
chamfer at top area is 0.2375” (6.033mm) ID max
• Braze alloy in the form of two-turn alloy ring
• Flux

Key Parameters
Temperature: 1030°F (554°C)
Power: 5 kW
Time: 14 seconds
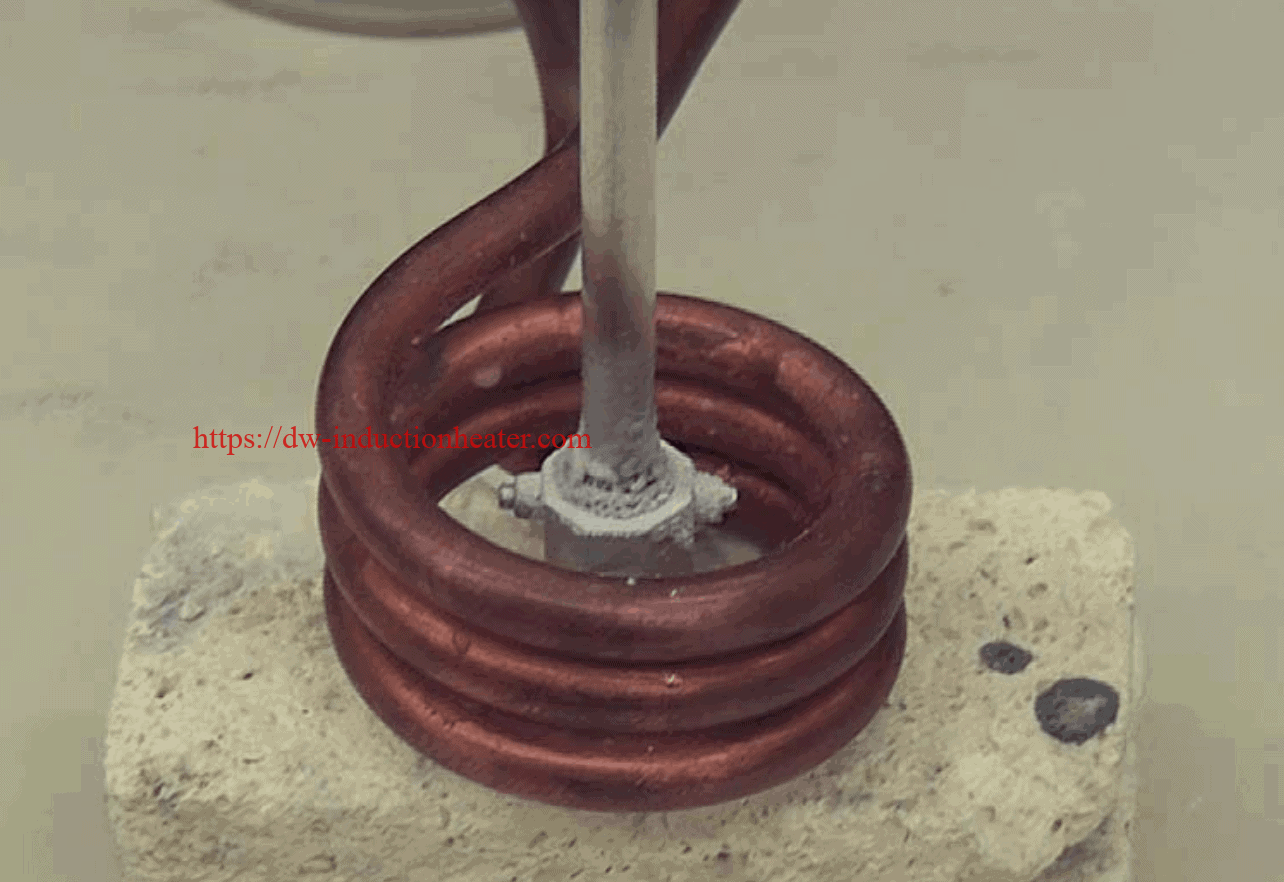
Process:
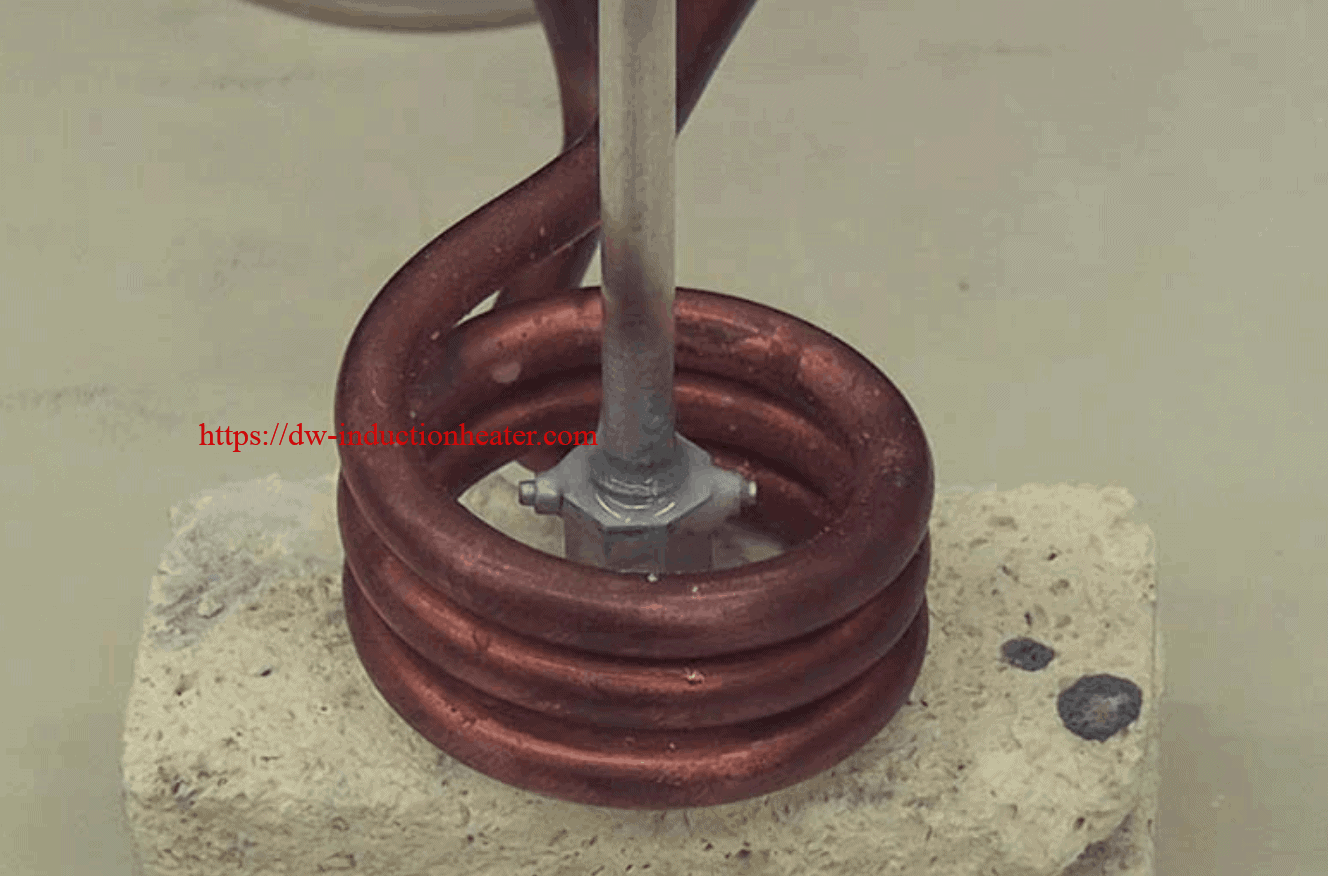
- The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
- The part was positioned in the induction coil.
- Several tests were conducted with different cycle times to confirm the heating time for a good braze.
- At 15 seconds the assembly melted.
- At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.

Results/Benefits:
The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
- Precise control of the time and temperature
- Power on demand with rapid heat cycles
- Repeatable process, not operator dependent
- Safe induction heating with no open flames
- Energy efficient heating
https://dw-inductionheater.com/wp-content/uploads/2020/05/Induction-Brazing-Aluminum-Tubing-to-Aluminum-Parts-4.png?v=1589719680
https://dw-inductionheater.com/induction-brazing-aluminum-tubing-to-aluminum-parts.html
aluminum brazing, Brazing aluminum, brazing aluminum tubing system, HF brazing aluminum tubing, high frequency brazing aluminum, high frequency brazing aluminum tubing, Induction Brazing Aluminum, induction brazing aluminum tubing, RF brazing aluminum tubing
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.