2023年9月4日星期一
Brazing Brass to Aluminum with Induction

evaporate water boiler with induction heating
evaporate water boiler with induction heating|induction steam boilers| electromagnetic induction steam generators|induction heating steam boilers
This invention relates to an induction evaporate water boiler | induction steram boiler|electromagnetic induction steam generator which operates with a low-frequency alternating current electric power source. More specifically, this invention relates to an electromagnetic induction steam boiler which is compact and highly efficient being capable of continuous operation, intermittent operation and empty-heating operation.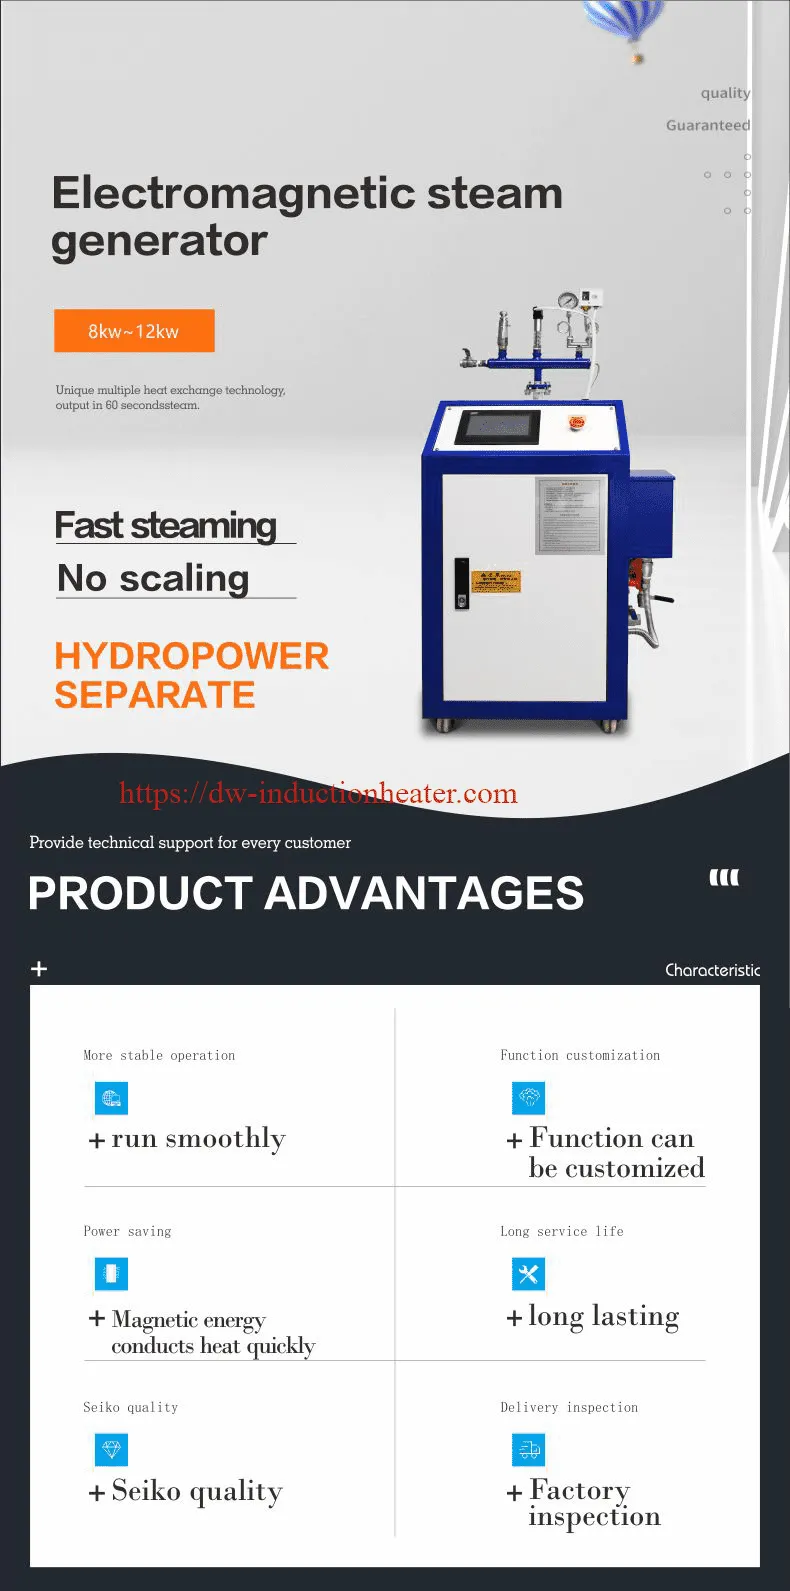

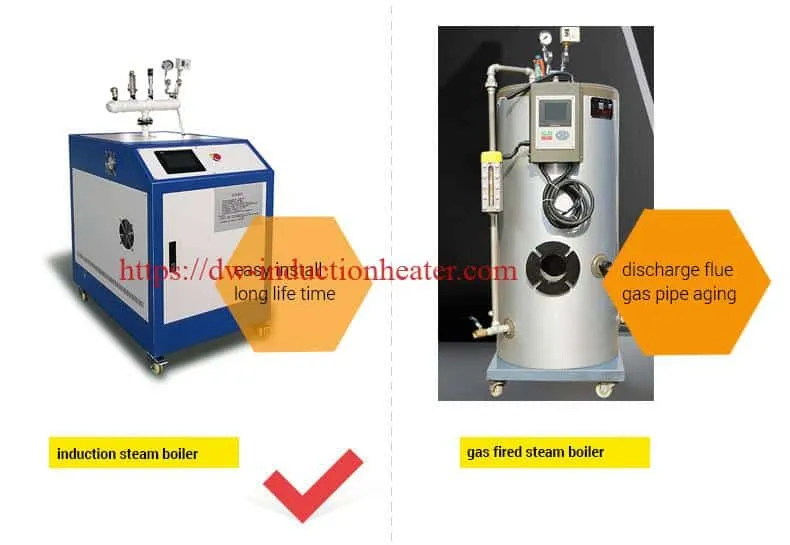
Steamers in current use, such as cooking steamers, convection ovens, cooking steam warmers, steamers for defrosting frozen food, steamers for processing tea leaves, steam baths for household use, steamers for cleaning, and steamers used in restaurants and hotels, are widely used as equipment for utilizing the steam they generate.Generally, fossil fuels (gas, petroleum, crude petroleum, coal and so forth) are burned as heat sources for large steamers in current use. This heating method, however, is not economical for compact steamers.

 Relatively compact steamers in current use commonly employ electrical resistance heaters as a heat source. Such steamers obtain steam intermittently by spraying water on an iron plate which has been heated in advance with a heater or the heater's protecting tube from inside or beneath the plate.
Energy saving rate of induction evaporate water boiler| electromagnetic induction steam boiler:
Because the iron container heats itself, the heat conversion rate is particularly high, which can reach more than 95%; the working principle of electromagnetic steam generator is that when some water enters the container, it will be heated into steam Drain, to ensure a fixed way of replenishing water, there will be continuous steam utilization.
Product Description of induction evaporate water boiler:
Industrial quality high pressure induction steamist boiler pure steam generator from china manufacturers 1) LCD Full-Automatically Intelligent Electronic Control System 2) High-quality Core Component——Electromagnetic induction heater 3) High-quality Components and Parts——Famous Brand Delixi Electrical Appliance 4) Multiple Safety Interlock Protection 5) Scientific Design and Attractive Appearance 6) Easy and Rapid Installation 7) Magnetic induction coil heat up boiling water Generate steam - Is Much More Eco-Friendly and Economical 8) Wide Application Range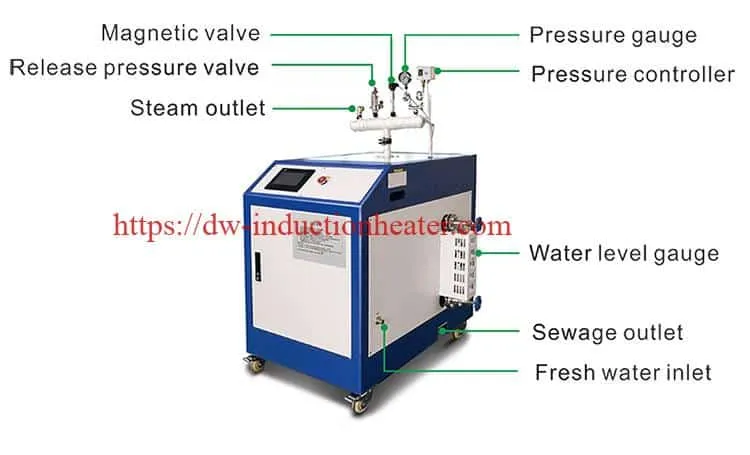
| Item content / model | Rated power (KW) | Rated steam temperature (℃) | Rated current (A) | Rated steam pressure (mpa) | Evaporation (kg/h) | Thermal efficiency (%) | Input voltage (V/HZ) | Cross section of input power cord (MM2) | Steam outlet diameter | Relief valve diameter | Inlet diameter | Drainage diameter | Overall dimensions (mm) |
| HLQ-10 | 10 | 165 | 15 | 0.7 | 14 | 97 | 380/50HZ | 2.5 | DN20 | DN20 | DN15 | DN15 | 450*750*1000 |
| HLQ-20 | 20 | 165 | 30 | 0.7 | 28 | 97 | 380/50HZ | 6 | DN20 | DN20 | DN15 | DN15 | 450*750*1000 |
| HLQ-30 | 30 | 165 | 45 | 0.7 | 40 | 97 | 380/50HZ | 10 | DN20 | DN20 | DN15 | DN15 | 650*950*1200 |
| HLQ-40 | 40 | 165 | 60 | 0.7 | 55 | 97 | 380/50HZ | 16 | DN20 | DN20 | DN15 | DN15 | 780*950*1470 |
| HLQ-50 | 50 | 165 | 75 | 0.7 | 70 | 97 | 380/50HZ | 25 | DN20 | DN20 | DN15 | DN15 | 780*950*1470 |
| HLQ-60 | 60 | 165 | 90 | 0.7 | 85 | 97 | 380/50HZ | 25 | DN20 | DN20 | DN15 | DN15 | 780*950*1470 |
| HLQ-80 | 80 | 165 | 120 | 0.7 | 110 | 97 | 380/50HZ | 35 | DN25 | DN20 | DN15 | DN15 | 680*1020*1780 |
| HLQ-100 | 100 | 165 | 150 | 0.7 | 140 | 97 | 380/50HZ | 50 | DN25 | DN20 | DN25 | DN15 | 1150*1000*1730 |
| HLQ-120 | 120 | 165 | 180 | 0.7 | 165 | 97 | 380/50HZ | 70 | DN25 | DN20 | DN25 | DN15 | 1150*1000*1730 |
| HLQ-160 | 160 | 165 | 240 | 0.7 | 220 | 97 | 380/50HZ | 95 | DN25 | DN20 | DN25 | DN15 | 1150*1000*1880 |
| HLQ-240 | 240 | 165 | 360 | 0.7 | 330 | 97 | 380/50HZ | 185 | DN40 | DN20 | DN40 | DN15 | 1470*940*2130 |
| HLQ-320 | 320 | 165 | 480 | 0.7 | 450 | 97 | 380/50HZ | 300 | DN50 | DN20 | DN50 | DN15 | 1470*940*2130 |
| HLQ-360 | 360 | 165 | 540 | 0.7 | 500 | 97 | 380/50HZ | 400 | DN50 | DN20 | DN50 | DN15 | 2500*940*2130 |
| HLQ-480 | 480 | 165 | 720 | 0.7 | 670 | 97 | 380/50HZ | 600 | DN50 | DN20 | DN50 | DN15 | 3150*950*2130 |
| HLQ-640 | 640 | 165 | 960 | 0.7 | 900 | 97 | 380/50HZ | 800 | DN50 | DN20 | DN50 | DN15 | 2500*950*2130 |
| HLQ-720 | 720 | 165 | 1080 | 0.7 | 1000 | 97 | 380/50HZ | 900 | DN50 | DN20 | DN50 | DN15 | 3150*950*2130 |

 Features of Induction Steam Generator:
1) LCD Full-Automatically Intelligent Electronic Control System
2) High-quality Core Component——Electromagnetic induction heater
3) High-quality Components and Parts——Famous Brand Electrical Appliance
4) Multiple Safety Interlock Protection
5) Scientific Design and Attractive Appearance
6) Easy and Rapid Installation
7) Magnetic induction coil heat up boiling water Generate steam - Is Much More Eco-Friendly and Economical
8) Wide Application Range

| Comparison of Different Types of Steam Generators | ||||
| Steam Generator Type | Gas Steam Generator | Resistance Wire Steam Generator | Coal Steam Generator | Electromagnetic Heating Steam Generator |
| Energy Used | Gas by Fire | Resistance Wire by Electricity | Coal by Fire | Electromagnetic Heating by Electricity |
| Heat Exchange Rate | 85% | 88% | 75% | 96% |
| Need Someone on Duty | Yes | No | Yes | No |
| Temperature Control Accuracy | ±8℃ | ±6℃ | ±15℃ | ±3℃ |
| Heating Speed | Slow | Quick | Slow | Very quick |
| Working Environment | A little pollution after fired | Clean | pollution | Clean |
| Production Risk Index | Risk of gas leakage, complicated pipelines | Risk of electricity leakage pipe inner wall easy be scaling | Risk of high temperature, heavy pollution | No risk of leakage, water & electricity separated completely |
| Operational Performance | Complicated | Simple | Complicated | Simple |
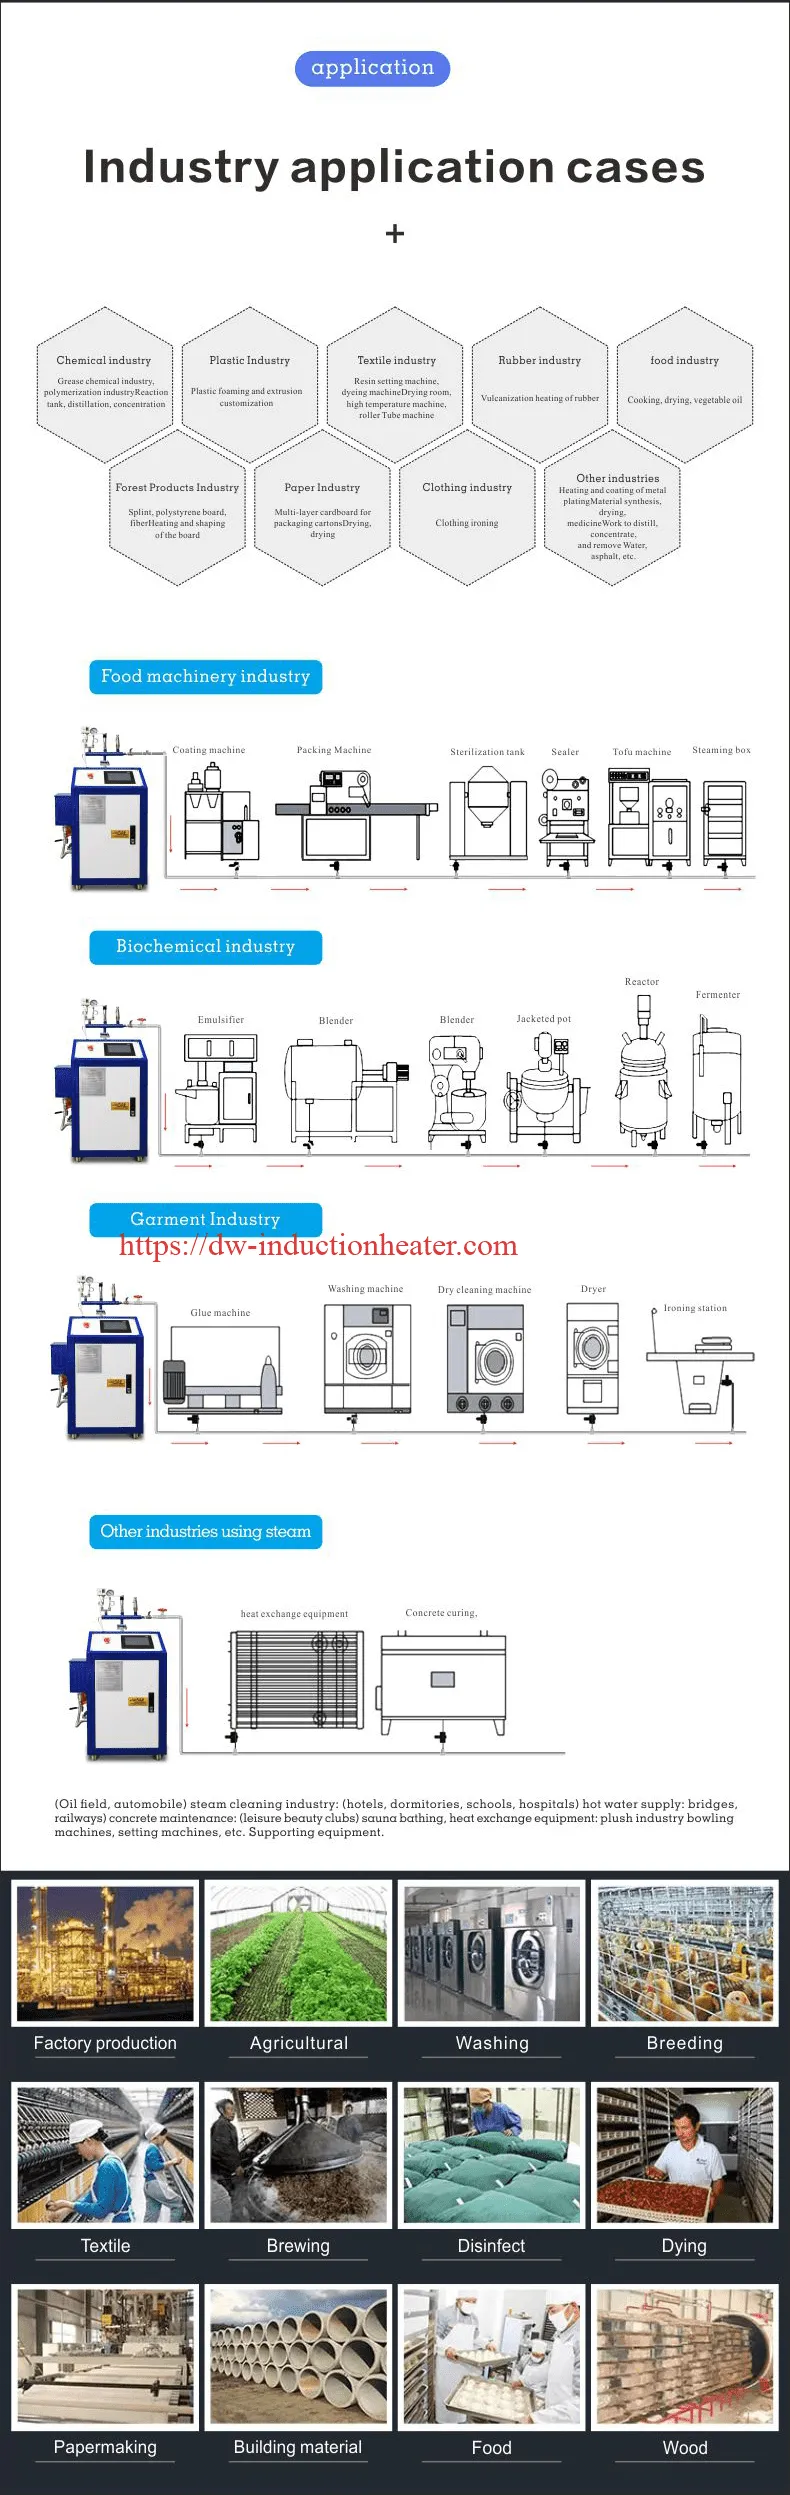
Application of induction heating steam generators|induction heating steam boilers:
Brazing copper tube to brass fitting
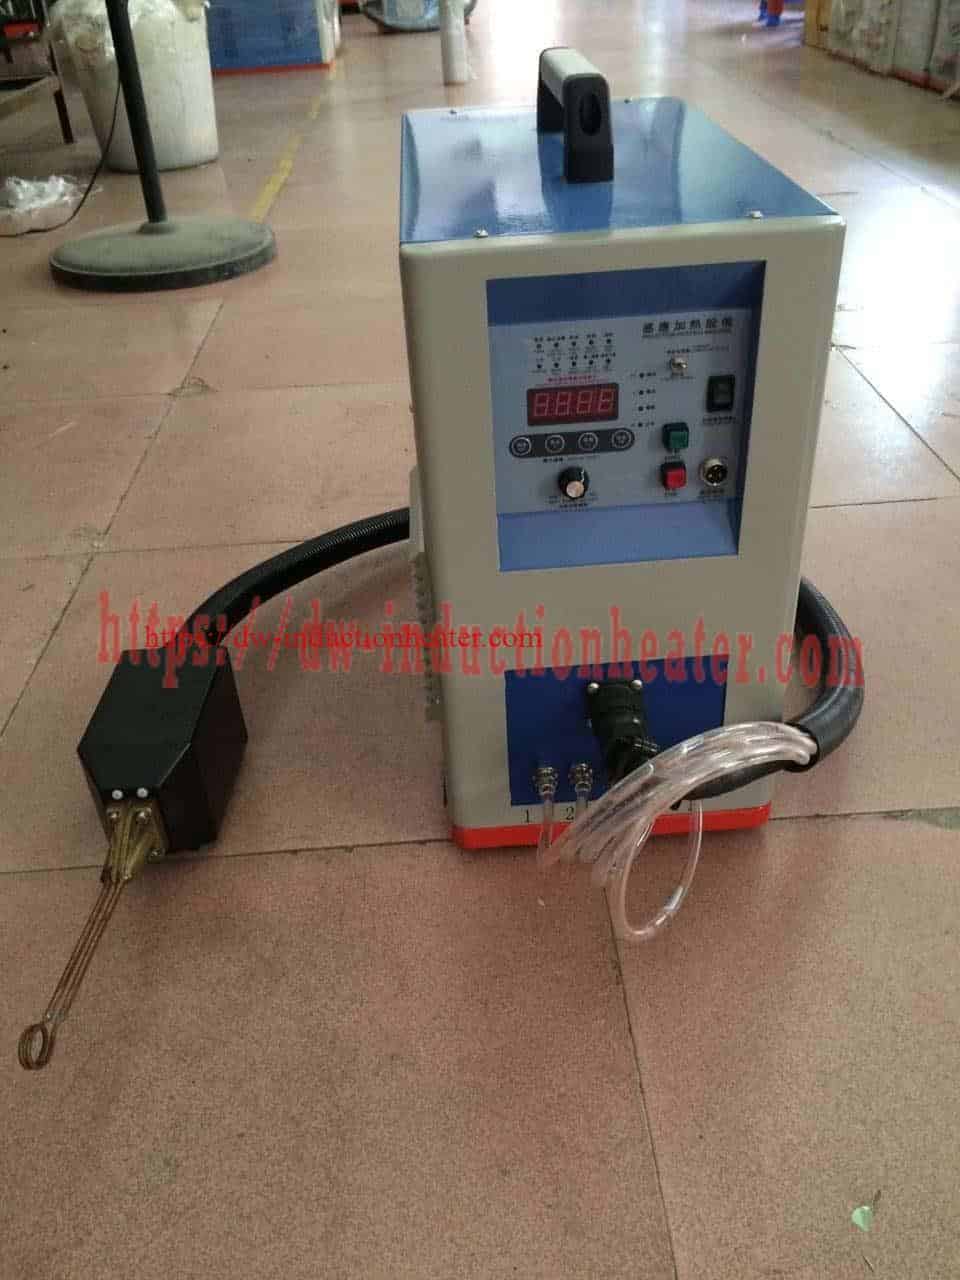
High frequency Induction brazing copper tube to brass fitting process
Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.1.DW-UHF-6KW-III handheld induction heater
2 turn helical coil
Materials
• Brass fitting
• Copper tubing
• Silver brazing alloy (pre-formed)
• Flux
Key Parameters
Temperature: Approximately 1350 °F (732°C)
- For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
- A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
- The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
- After 60 seconds in the coil, the brazing was complete.
- The material was cooled in water following the completion of brazing.
- The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
- Strong durable joints
- Selective and precise heat zone, resulting in less part distortion and joint stress than welding
- Less oxidation
- Faster heating cycles
- More consistent results and suitability for large volume production, without the need for batch processing
- Safer than flame brazing
2023年9月3日星期日
induction brazing carbide tip onto steel head teeth
high frequency induction brazing carbide tip onto steel head teeth process
 Objective
In this application test, induction brazing carbide tip onto steel working head teeth.

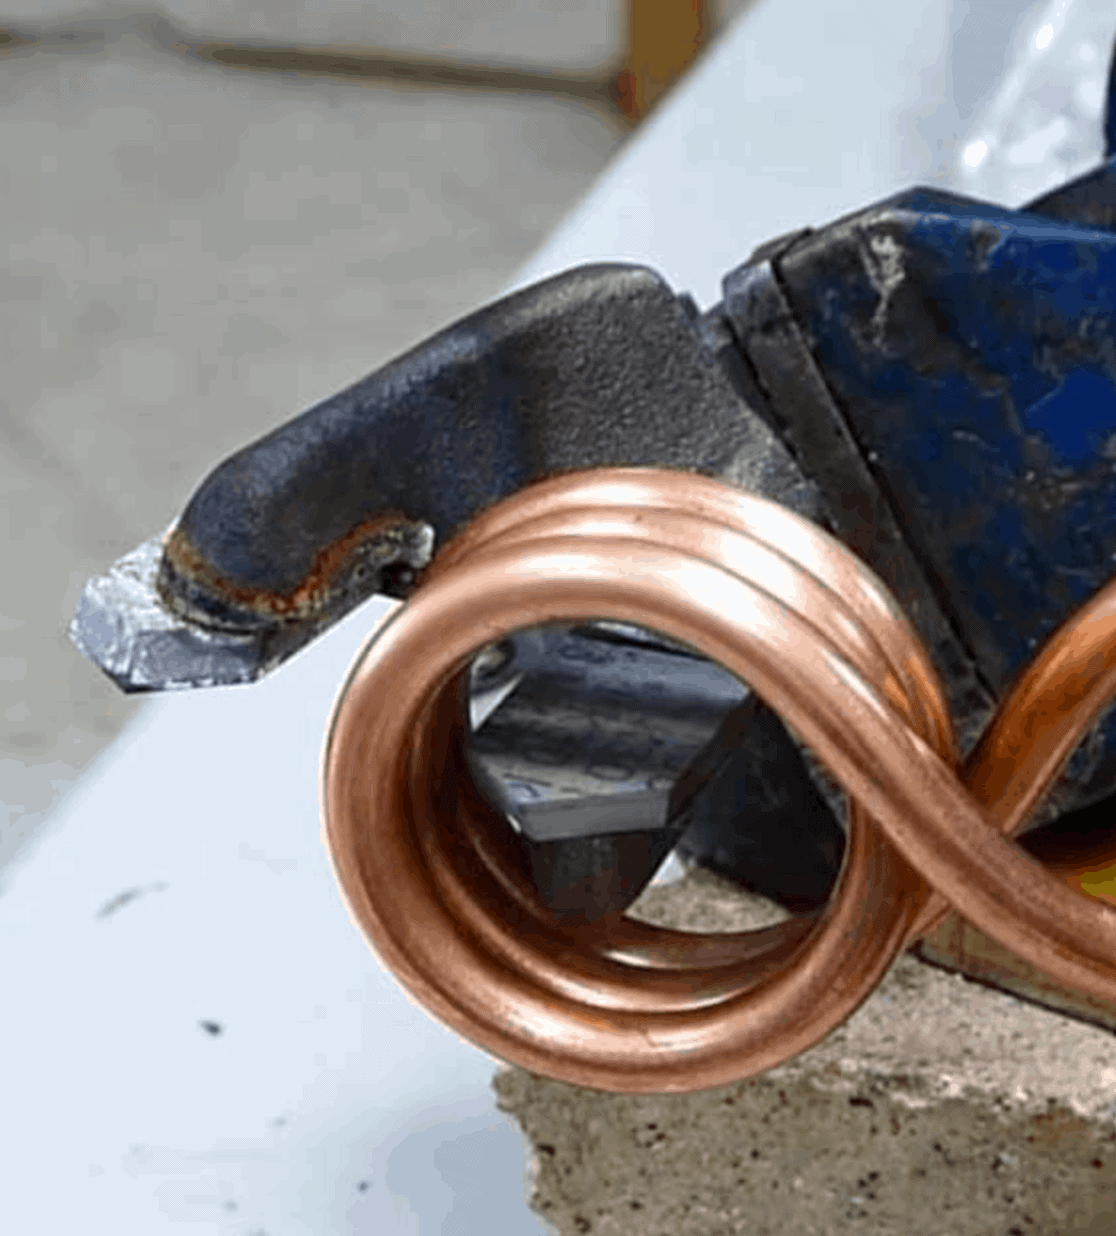
- Brazing paste is put on the tool
- The steel working head teeth are attached.
- The assembly is positioned in the three-turn coil.
- The assembly is heated.
- The joint is completed in 6 seconds.
 Results/Benefits:
- Strong durable joints
- Selective and precise heat zone, resulting in less part distortion and joint stress than welding
- Less oxidation
- Faster heating cycles
- More consistent results and suitability for large volume production
- Safer than flame brazing

Brazing stainless steel with induction
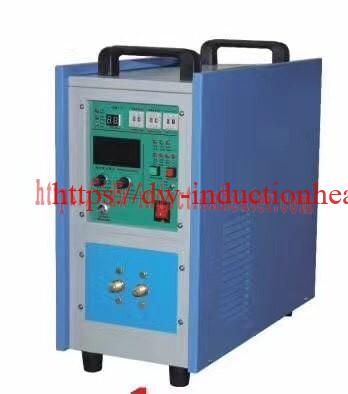
High frequency induction brazing stainless steel tube to stainless steel fitting with DW-HF-25kw-A induction heater.
Objective Brazing stainless steel tubing and stainless steel fittings Equipment DW-HF-25kw-A induction brazing machine
- Induction heating pinpoints the heat to the desired area of the part
- Improved process control for precise heating to a desired temperature
- Power on demand and rapid, consistent heat cycles
- Technology without pollution, which is both clean and safe
Induction Heating Sintering Copper Powder
Induction Shrink Fitting Assemblies

我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.