显示标签为“brazingcoppertobrass”的博文。显示所有博文

2024年4月26日星期五

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
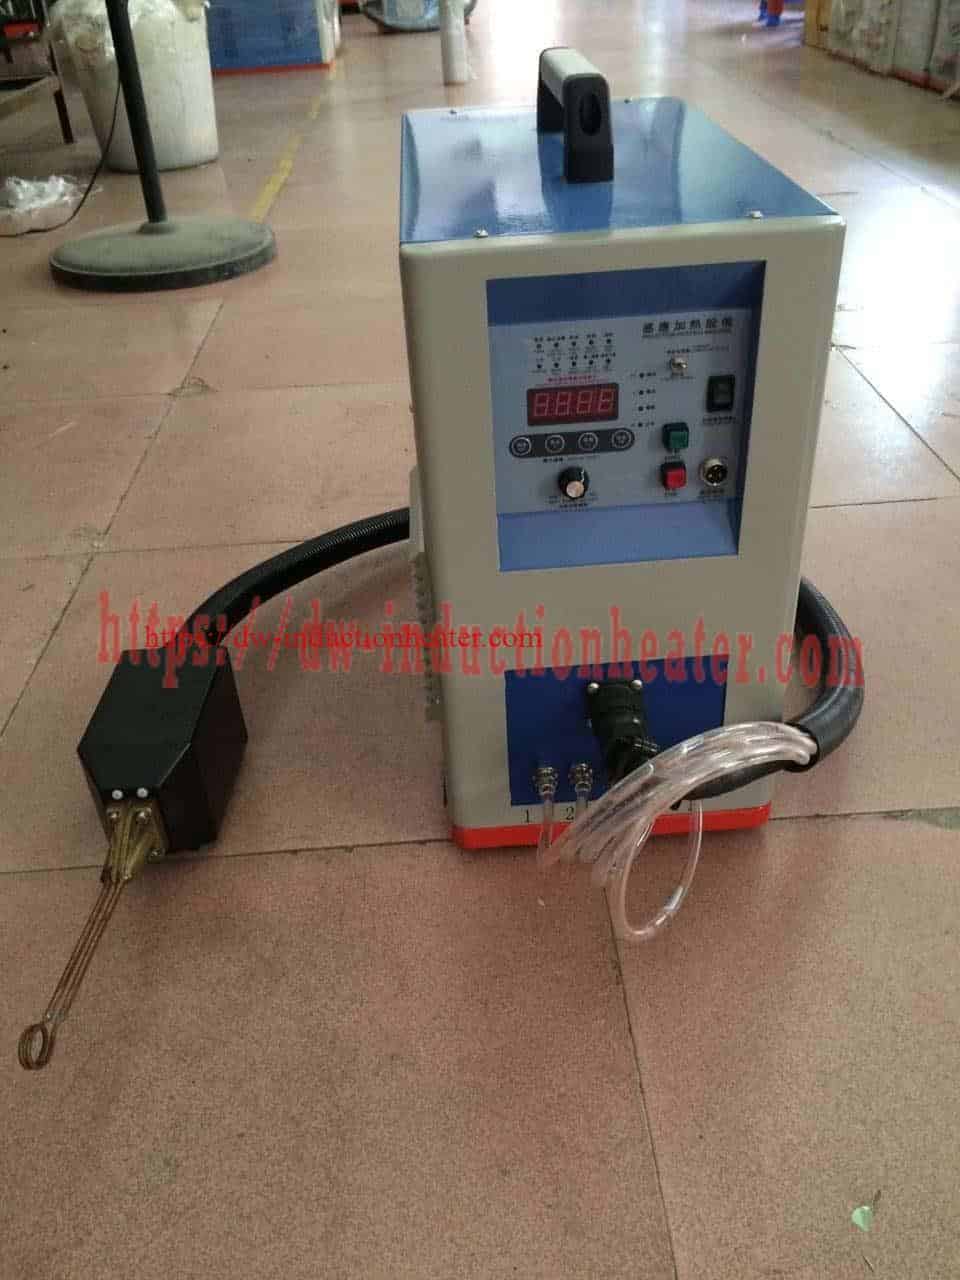
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=243162&_unique_id=662c50aa0c3fa

2023年9月4日星期一

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=226186&_unique_id=64f5aa994fcf8

2023年5月12日星期五

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2023年4月24日星期一

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2022年11月27日星期日

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2022年11月2日星期三

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2022年8月25日星期四

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2022年6月15日星期三

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2022年6月10日星期五

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

2021年11月8日星期一

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.