显示标签为“brazingcoppertube”的博文。显示所有博文

2024年4月26日星期五

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
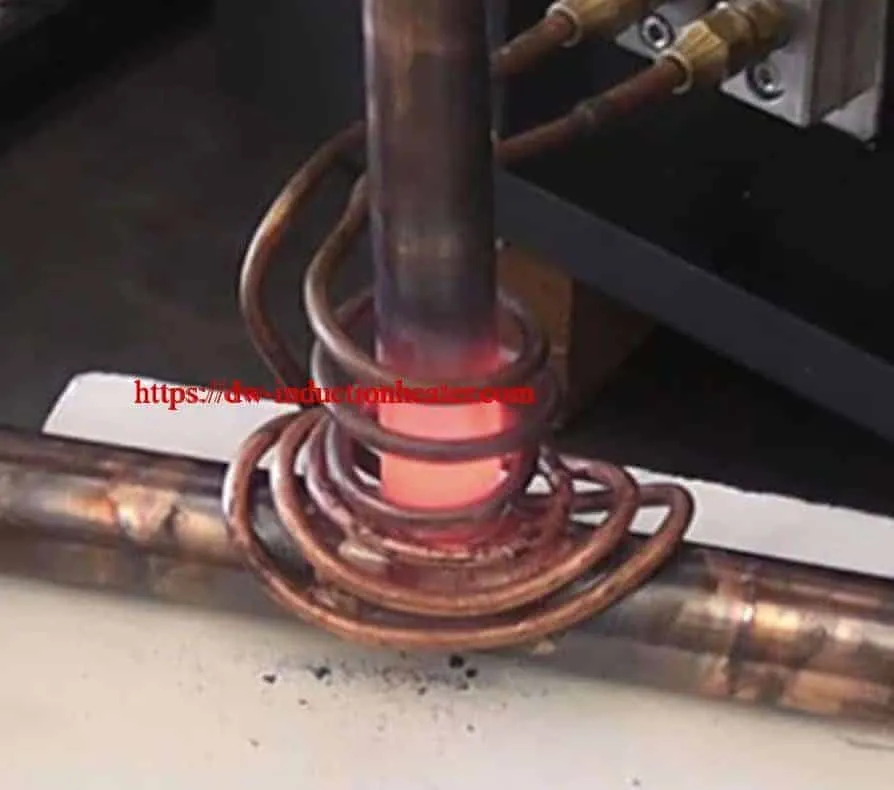
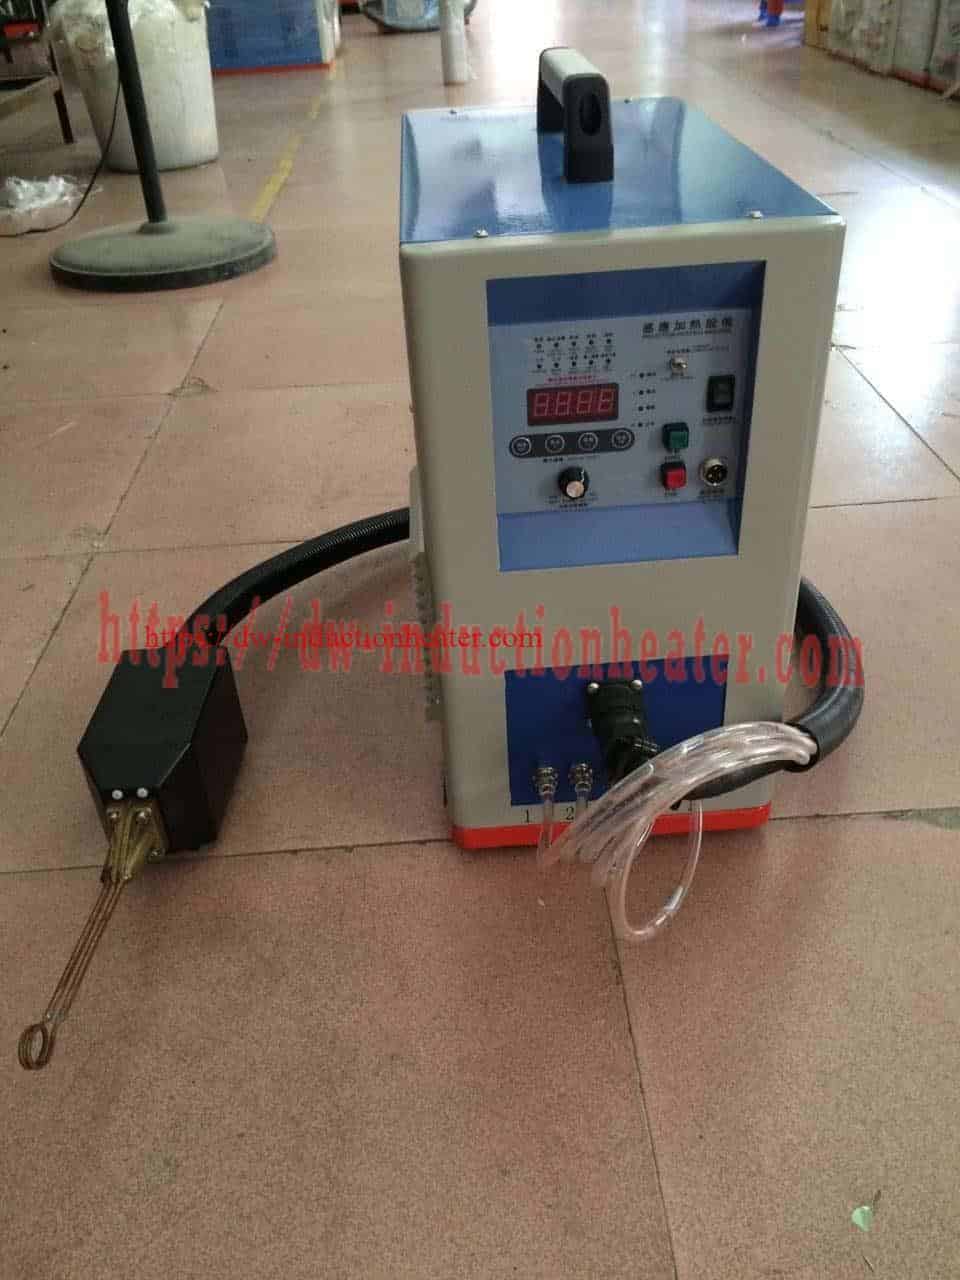
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=243162&_unique_id=662c50aa0c3fa

2024年4月13日星期六

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

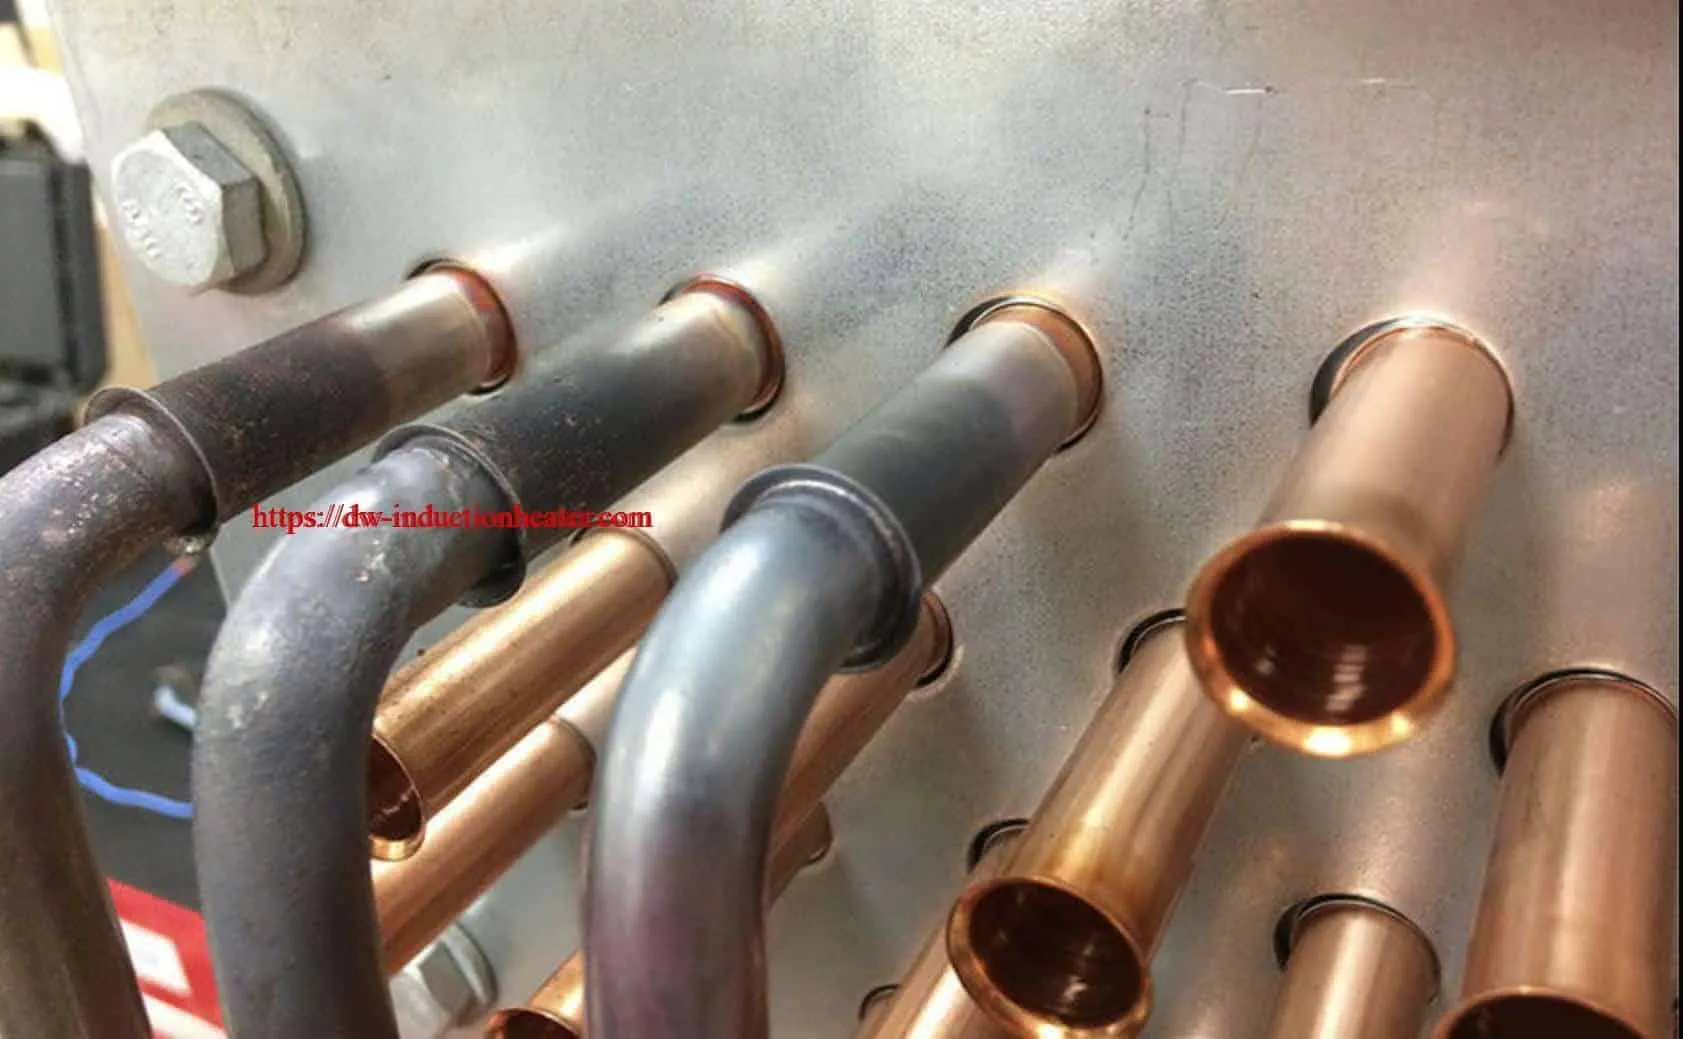
Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube
https://dw-inductionheater.com/induction-brazing-copper-tube-of-heat-exchanger.html?feed_id=241367&_unique_id=661a7699e7b00

2024年4月9日星期二

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra
https://dw-inductionheater.com/induction-brazing-copper-tube-for-refrigeration.html?feed_id=240864&_unique_id=66162da90acc5

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  
https://dw-inductionheater.com/induction-brazing-copper-t-pipe-with-induction-heating-machine.html?feed_id=240796&_unique_id=661576c3c085d

2023年10月26日星期四

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年9月19日星期二

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra

2023年9月4日星期一

Brazing copper tube to brass fitting

High frequency Induction brazing copper tube to brass fitting process

Objective Induction brazing copper to brass fitting using brazing alloy and flux within 60 seconds.
Equipment Handheld induction brazing heater1.DW-UHF-6KW-III handheld induction heater 2 turn helical coil Materials • Brass fitting • Copper tubing • Silver brazing alloy (pre-formed) • Flux Key Parameters Temperature: Approximately 1350 °F (732°C)
Process:
  1. For Induction Brazing Copper to Brass, first the copper tubing and brass fitting were assembled together.
  2. A pre-form of the silver brazing alloy was seated above the joint, and flux was added.
  3. The assembly was placed the two-turn helical coil, and positioned so the targeted joint was centered in the coil.
  4. After 60 seconds in the coil, the brazing was complete.
  5. The material was cooled in water following the completion of brazing.
  6. The joint was then cross-sectioned to validate that the induction brazing process had produced a strong, high quality joint.
Results/Benefits: Induction brazing heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting.html?feed_id=226186&_unique_id=64f5aa994fcf8

2023年8月21日星期一

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube
https://dw-inductionheater.com/induction-brazing-copper-tube-of-heat-exchanger.html?feed_id=224311&_unique_id=64e3cde37264d

2023年8月18日星期五

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra
https://dw-inductionheater.com/induction-brazing-copper-tube-for-refrigeration.html?feed_id=223711&_unique_id=64df84313d531

2023年8月3日星期四

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年6月21日星期三

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年6月9日星期五

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.