显示标签为“inductionbrazingcoppertube”的博文。显示所有博文

2024年4月13日星期六

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

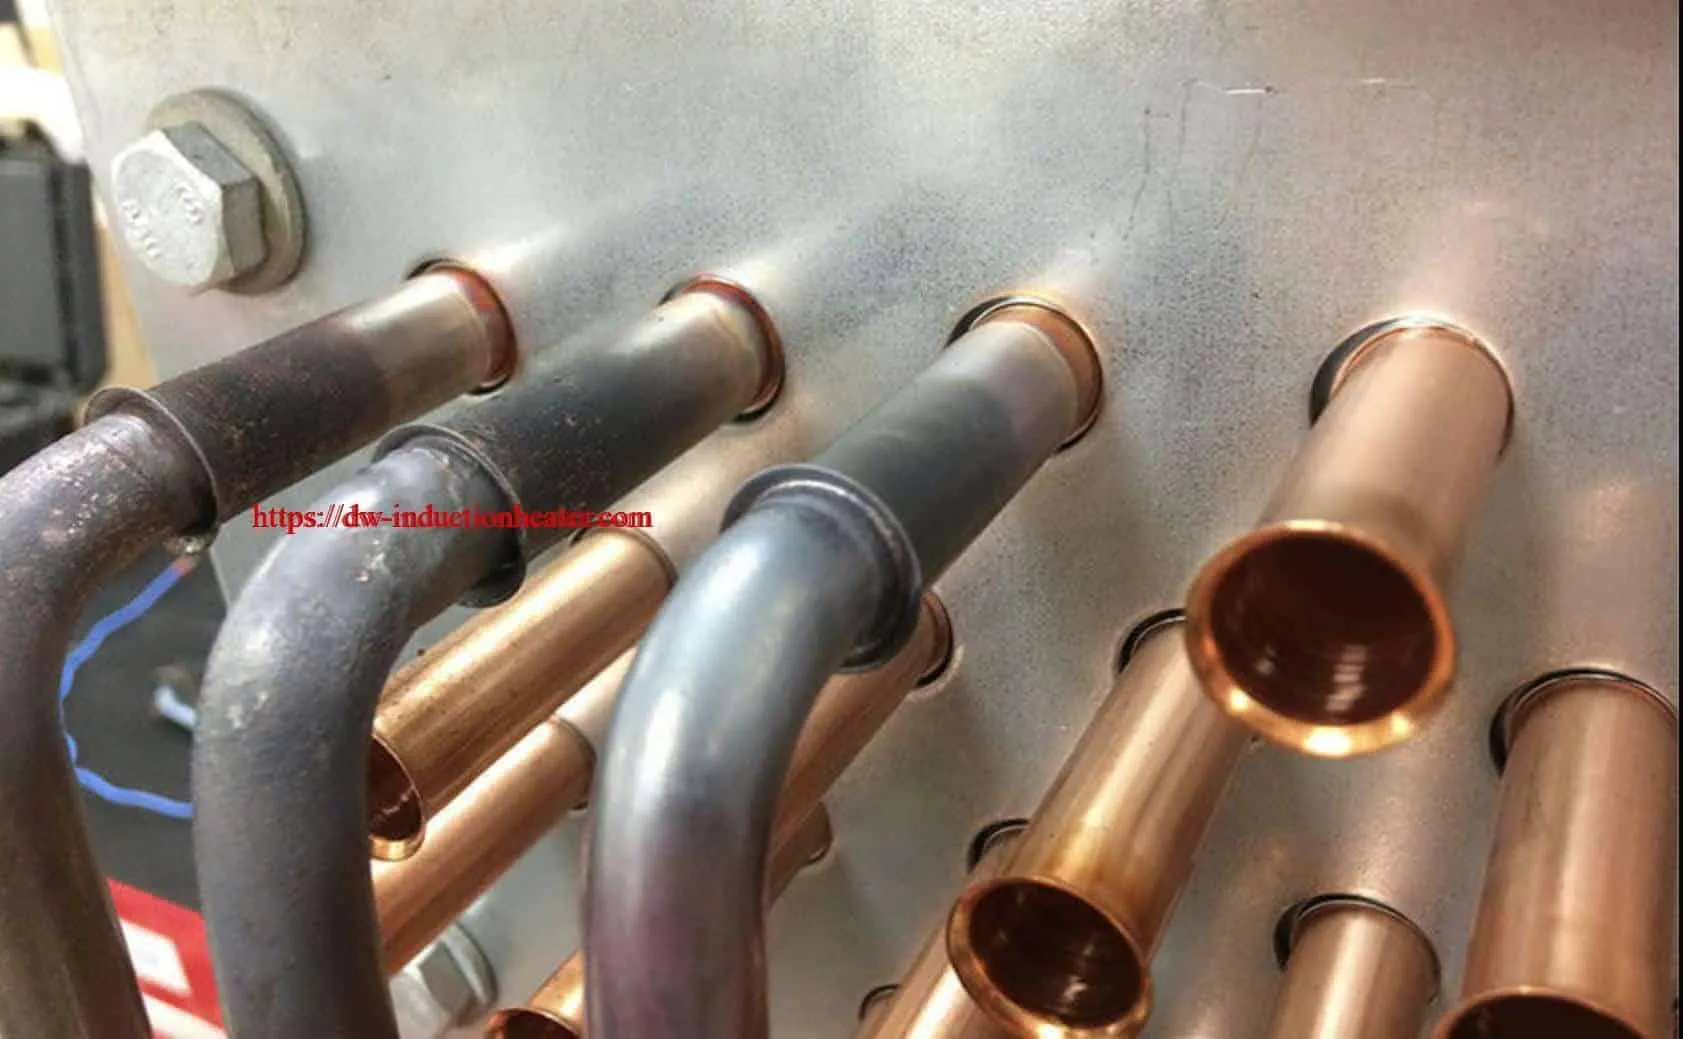
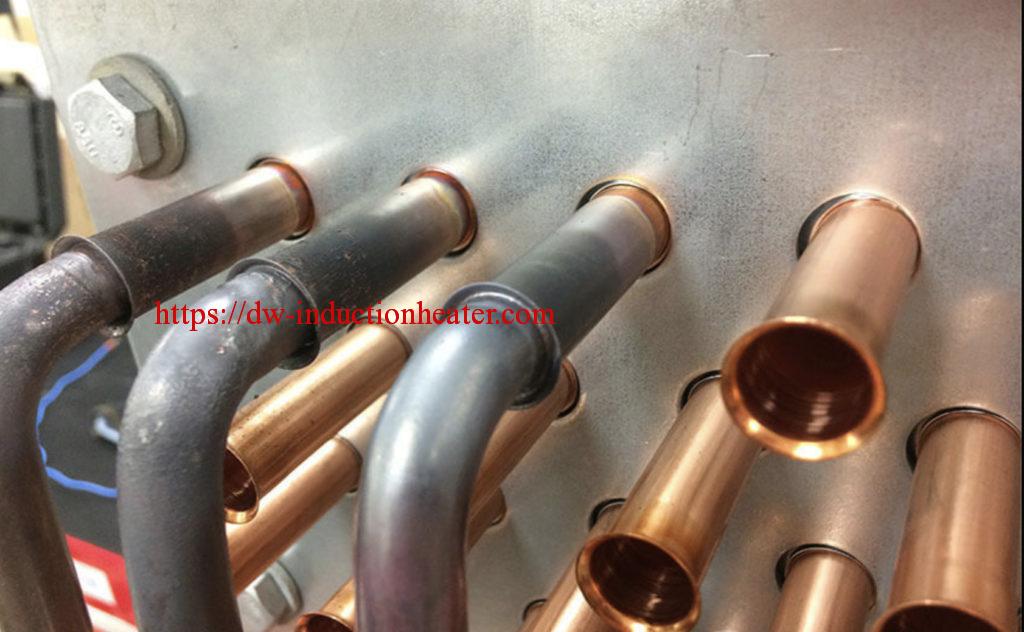
Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
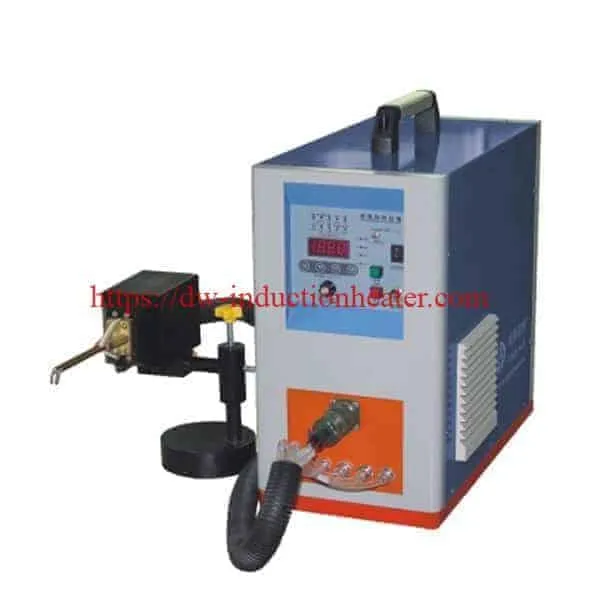
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube
https://dw-inductionheater.com/induction-brazing-copper-tube-of-heat-exchanger.html?feed_id=241367&_unique_id=661a7699e7b00

2024年4月9日星期二

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

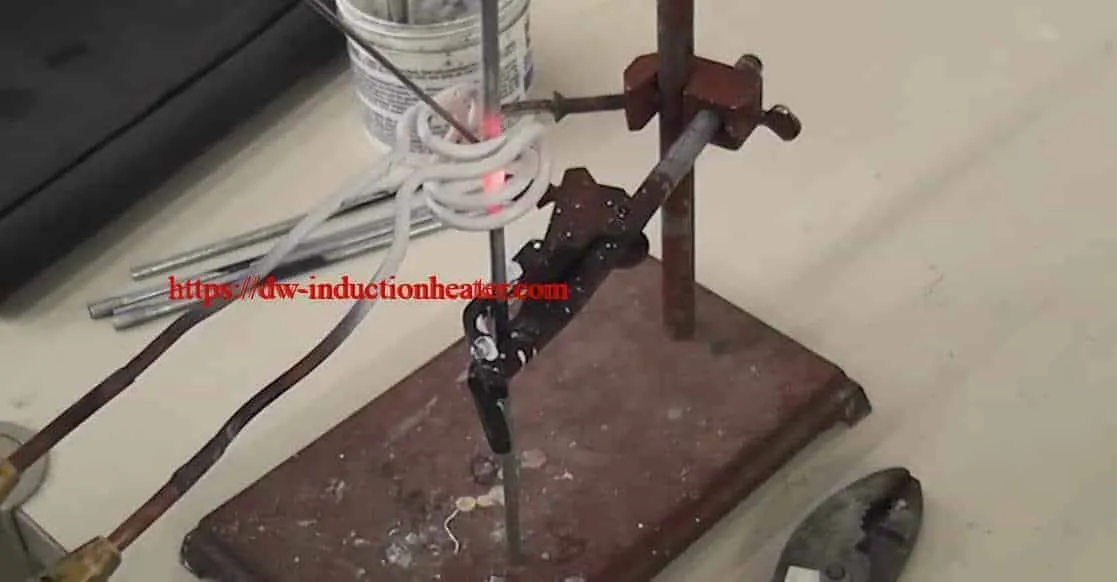
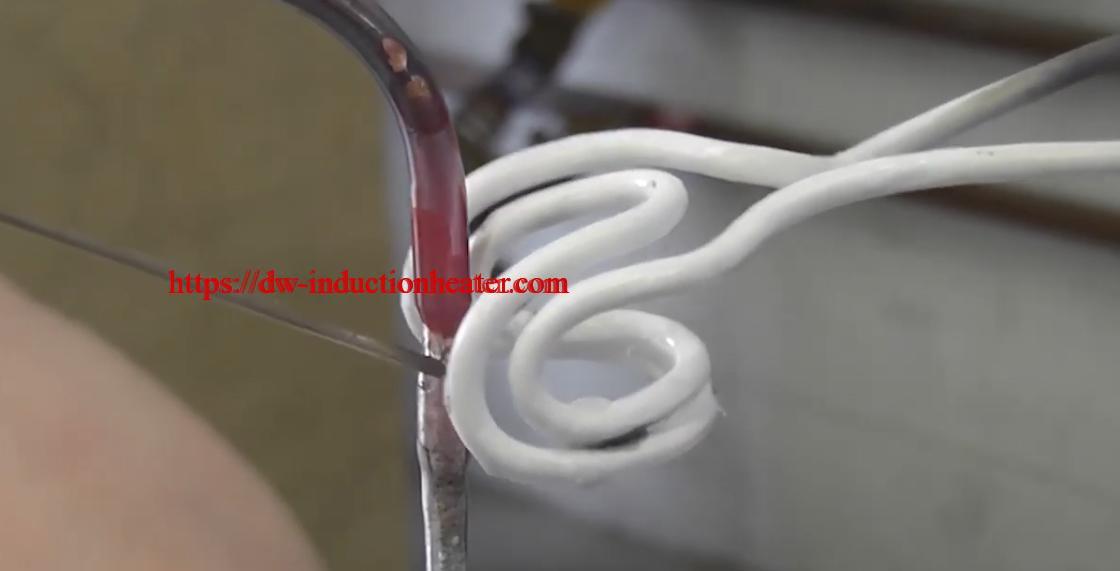
Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra
https://dw-inductionheater.com/induction-brazing-copper-tube-for-refrigeration.html?feed_id=240864&_unique_id=66162da90acc5

2024年4月8日星期一

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"] https://dw-inductionheater.com/induction-handheld-brazing-copper-to-steel-tube.html?feed_id=240602&_unique_id=661409426faca

2023年11月17日星期五

Induction Brazing Copper Pipe Fittings

Induction Brazing Copper Fittings Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve Material: customer's valve copper fittings braze Temperature: 2550 ºF (1400°C) Frequency: 585 kHz Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times. Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable https://dw-inductionheater.com/induction-brazing-copper-pipe-fittings.html?feed_id=230886&_unique_id=655782768f6d8

2023年9月21日星期四

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

2023年9月19日星期二

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra

2023年8月21日星期一

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

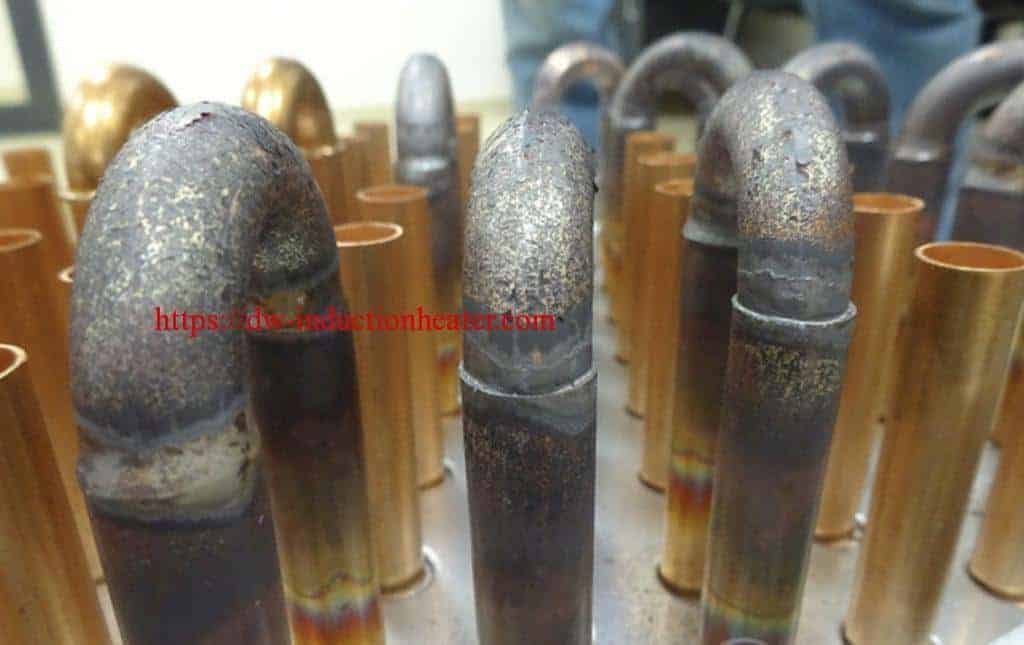
Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube
https://dw-inductionheater.com/induction-brazing-copper-tube-of-heat-exchanger.html?feed_id=224311&_unique_id=64e3cde37264d

2023年8月18日星期五

Induction Brazing Copper Tube For Refrigeration

Induction Brazing Copper Tube For Refrigeration

Objective Induction Brazing of a Copper Refrigeration Tube to Steel Tube
Equipment DW-UHF-6KW-I Handheld Induction Brazing System Materials Copper Refrigeration  to steel tube Copper tube – 0.2” (5.08mm) at the interface Steel tube Flared interface 0.25” (6.35mm) Power: 6kW Temperature: 1600°F (871°C) Time: 6 sec
Results and Conclusions:
  • Successfully braze copper to steel tube in 6 seconds
  • Strong durable joints
  • Precise control of the time and temperature
  • Reduction in defects due to overheating
  • Technology without pollution, clean and safe
Induction brazing copper tubeInduction brazing copper tubeInduction brazing copper tube  Induction brazing copper tubeBra
https://dw-inductionheater.com/induction-brazing-copper-tube-for-refrigeration.html?feed_id=223711&_unique_id=64df84313d531

2023年8月16日星期三

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"] https://dw-inductionheater.com/induction-handheld-brazing-copper-to-steel-tube.html?feed_id=223486&_unique_id=64dd5f3d3b272

2023年6月9日星期五

Induction Brazing Copper Tube of Heat Exchanger

Induction Brazing Copper Tube of Heat Exchanger

Brazing heat exchanger copper tubeObjective Brazing heat exchanger copper to copper pipes Industry Various industries Base material Copper tubes – Diameter / thickness of external tube: 12.5 x 0.35 and 16.75 x 0.4 – Type of assembly: lap joint Other materials Brazing alloy rings
Induction Brazing heat exchanger copper tubeEquipment DW-UHF-6KW-III handheld induction brazing heater Key Parameters Power: 6KW Time: ≈ 10s
Handheld induction brazing heater
Process A manufacturer of heat exchangers for various industries wanted to increase operator safety and production rate during the process of brazing. We received a sample of a heat exchanger which was a part of an actual assembly (more than 10 m long). The goal was to determine the most suitable design for a custom coil which will allow for the brazing of two joints to be performed simultaneously. HLQ team recommended using the UBraze which is a mobile induction heating solution that can be utilized as a hand-held unit or can be integrated with a robotic arm for automated production lines. Тhe performed tests matched the exact position of the heat exchanger on the production to simulate actual working conditions. We used a custom-designed elliptical coil with a positioning fixture to help the operator achieve repeatable results, as well as increase the production rate by brazing 2 joints for 10 sec. As a result, the brazed connection becomes extremely secure and leak-proof. Compared to gas torch brazing, induction heating does not produce an open flame, thus it is much safer for the operator. Fast process and repeatability are guaranteed. Heat exchangers are devices that are widely used in many industries – space heating, refrigeration, air conditioning, power stations, chemical plants, petrochemical plants, petroleum refineries, natural gas processing, and sewage treatment. Benefits
  • Safe heating with no open flame
  • Precise control over time and temperature resulting in improved quality and consistent result
  • A repeatable process, not operator dependent
  • Energy efficient heating
Induction brazing copper tubeInduction brazing heat exchanger copper tube

2023年5月11日星期四

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.