 Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
https://dw-inductionheater.com/induction-brazing-copper-pipe-fittings.html?feed_id=230886&_unique_id=655782768f6d8
2023年11月17日星期五
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
https://dw-inductionheater.com/induction-brazing-copper-pipe-fittings.html?feed_id=230886&_unique_id=655782768f6d8

2023年11月11日星期六
Brazing Copper Tube to Brass Fitting With Induction
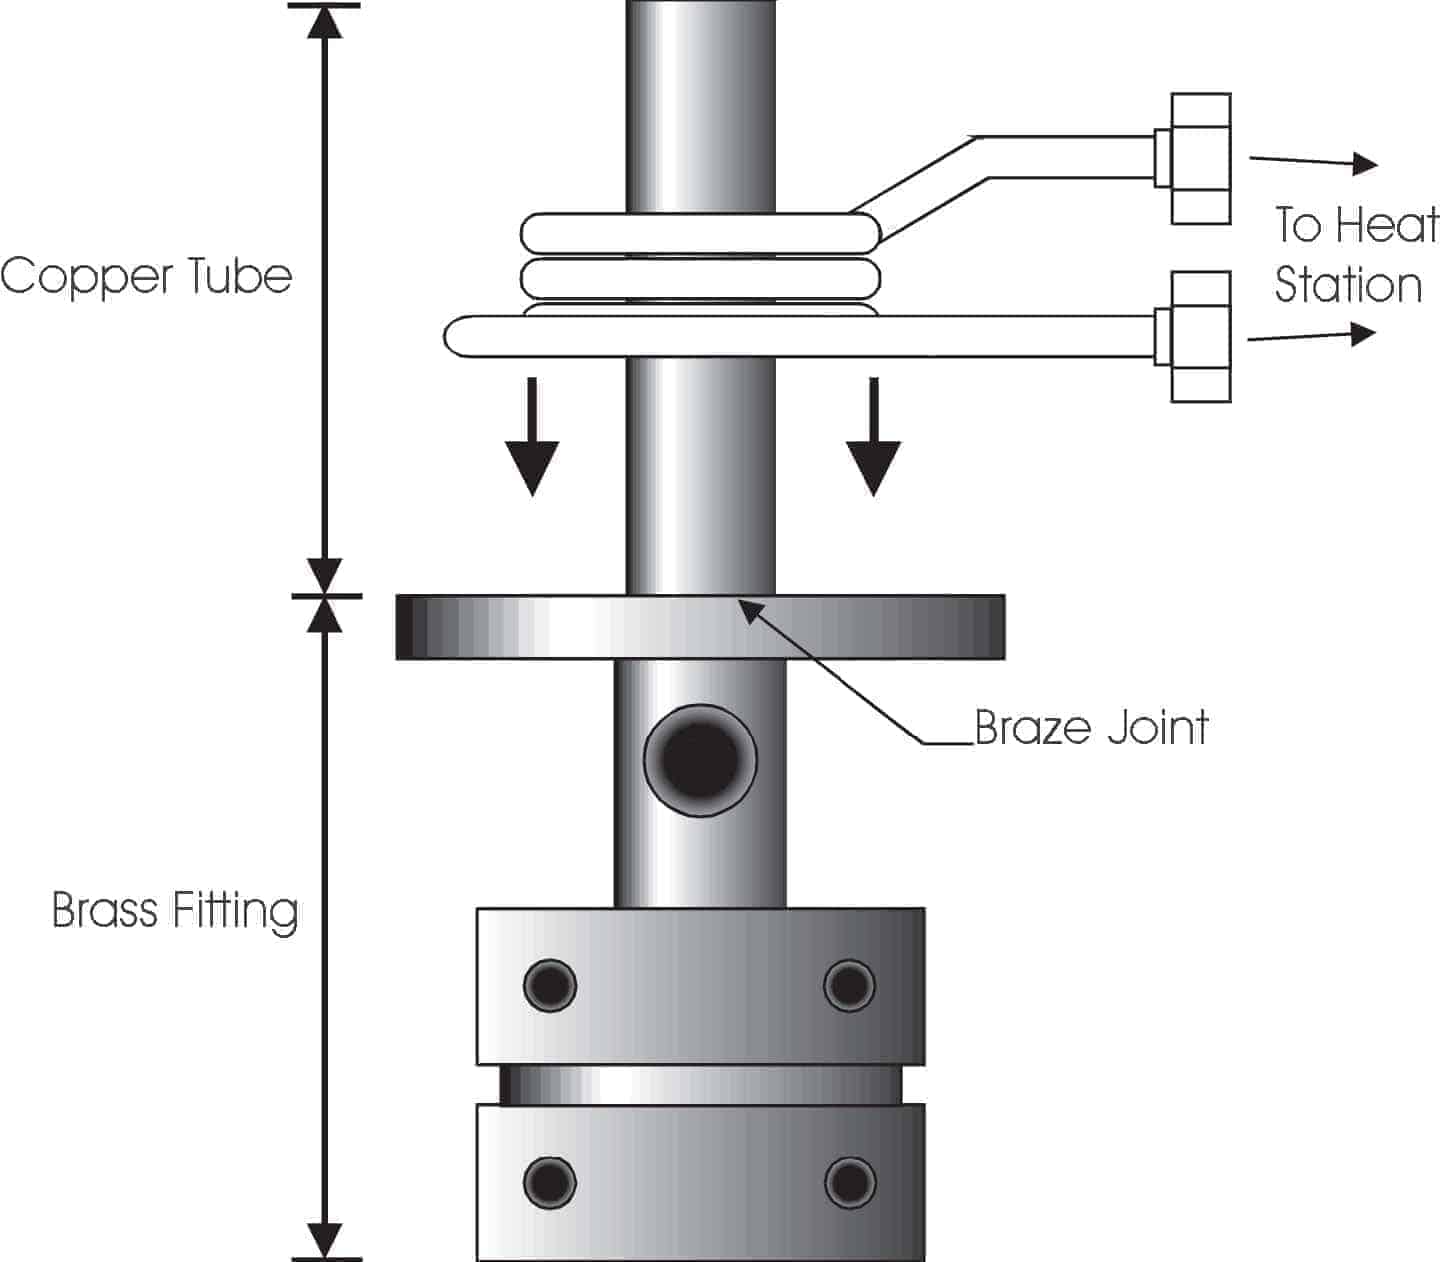 Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=230586&_unique_id=65505e7426754
2023年8月1日星期二
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年3月29日星期三
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年3月27日星期一
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2023年2月15日星期三
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2023年2月2日星期四
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年1月31日星期二
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2023年1月6日星期五
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年11月11日星期五
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年11月1日星期二
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2022年10月31日星期一
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年10月16日星期日
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年9月22日星期四
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年8月12日星期五
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2022年6月6日星期一
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年4月24日星期日
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
2022年4月9日星期六
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年3月20日星期日
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年1月26日星期三
Induction Brazing Copper Pipe Fittings
Induction Brazing Copper Fittings
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material: customer's valve copper fittings braze
Temperature: 2550 ºF (1400°C)
Frequency: 585 kHz
Equipment: DW-UHF-10kw induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process: The valve is placed inside the coil and RF induction heating power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction heating system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.