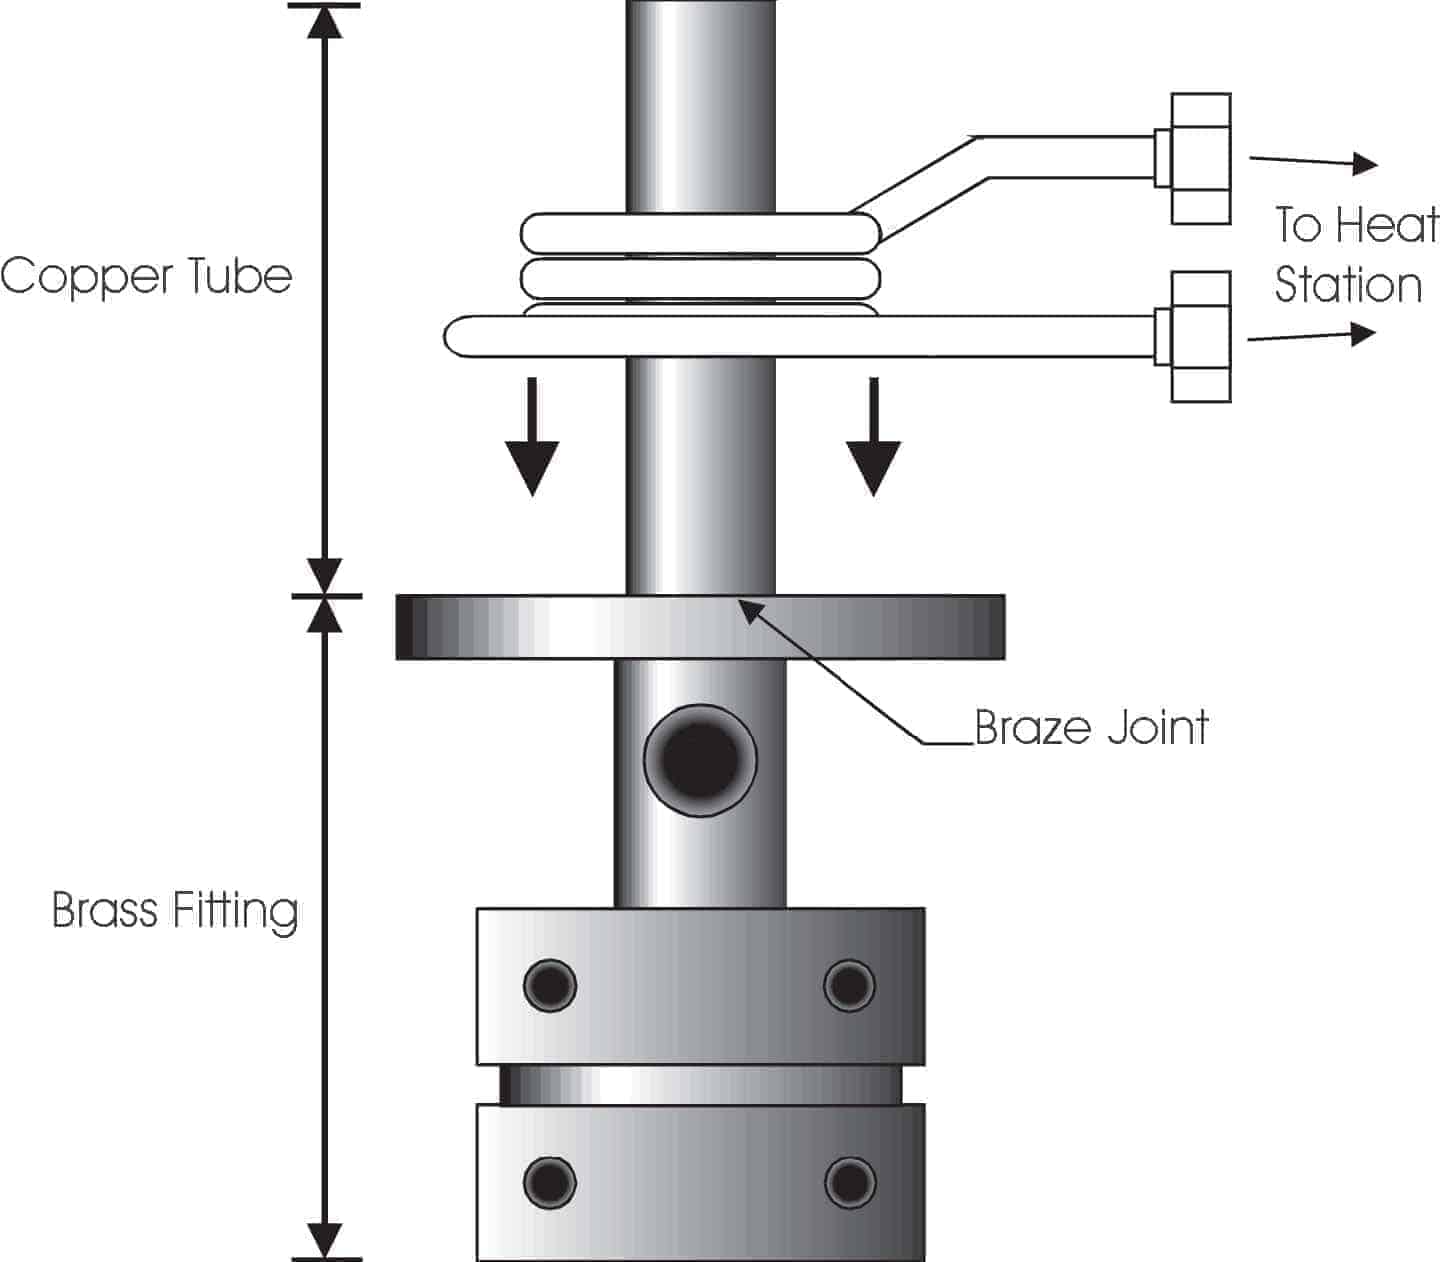
 Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=230586&_unique_id=65505e7426754
2023年11月11日星期六
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
https://dw-inductionheater.com/brazing-copper-tube-to-brass-fitting-with-induction.html?feed_id=230586&_unique_id=65505e7426754

2023年8月1日星期二
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年3月29日星期三
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年2月2日星期四
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2023年1月6日星期五
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年11月11日星期五
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年10月31日星期一
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年10月16日星期日
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年9月22日星期四
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年6月6日星期一
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年4月9日星期六
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2022年3月20日星期日
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
2021年12月23日星期四
RF Brazing Copper System
RF Brazing Copper System With Induction
Applications
*Quick quenching *Hardening for small depth *Brazing for tiny workpiece *Heating tiny workpiece *Diamond blade brazing to segments, carbon steel blade brazing, PCBN blade brazing etc.*Glasses steel alloys frame brazing, small bearings quenching, annealing etc.
*Jewelries brazing, watchcase annealing and clock outer quenching.
*Electronics products brazing/welding/heating: fine and expensive products like bulb filaments etc.
*Precise mechanical parts brazing/heating.
*Stainless steel strip annealing etc.
|
Model |
DW-UHF-30KW |
|
|
Input Voltage |
3 phases,380V±10%,50/60Hz |
|
|
Output Power |
30KW |
|
|
Oscillate frequency |
50-200KHz |
|
|
Max Input Current |
45A |
|
|
Cooling Water |
>0.2 MPa, 5 L/Min, |
|
|
Weight |
55KG |
|
|
Size |
Main |
590X300X530mm |
|
Head |
520X255X380mm |
|
Main characteristics:
1. With high frequency up to 50-250KHz.the quenching thickness can be controlled lower than 1mm ,and very tiny parts can be easily heated. 2. IGBT and inverting technologies of third generation been used, higher reliability and lower maintenance cost. 3. 100% duty cycle, continuous working is allowed at Max power output. 4. Light weight,55KG only. Small and portable.
5. Constant current or constant power status can be selected accordingly to achieve higher heating efficiency.
[wpforms id="3947"]
2021年11月22日星期一
Brazing Copper Tube to Brass Fitting With Induction
Brazing Copper Tube to Brass Fitting With Induction
Objective: To use induction heating to braze a copper tube to a brass fitting using a preform braze wire. Processing is to occur under an atmosphere of Nitrogen and 4% Hydrogen gas. The braze preforms melt at 1190°F, but the parts need to be kept below 1300°F. The parts need to be processed at a rate of 175 to 200 per hour which translates into 18 seconds of heating time per part.
Material Copper Tubing Measuring 0.5" OD and 2" Long, Brass fitting, Braze Preform, No Flux.
Temperature Above 1190°F but not to exceed 1300°F
Frequency :300 kHz
Equipment: DW-UHF-10KW output solid state induction heating power supply with three (3) busses, eight (8) capacitors totaling 0.66 μF, and a unique four turn helical coil. Process The DW-UHF-10KW output solid state power supply along with a unique four turn helical coil were used to achieve the following results.
Results • The requested atmosphere was provided under a bell jar by supplying 95% Nitrogen/5%Hydrogen at a rate of 25-30 cfh. • A heating cycle of only 10 seconds was necessary to attain sufficient braze flow which surpasses the required limit of 18 seconds.
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.