显示标签为“brazingtubes”的博文。显示所有博文

2024年4月8日星期一

Induction Handheld Brazing Copper To Steel Tube
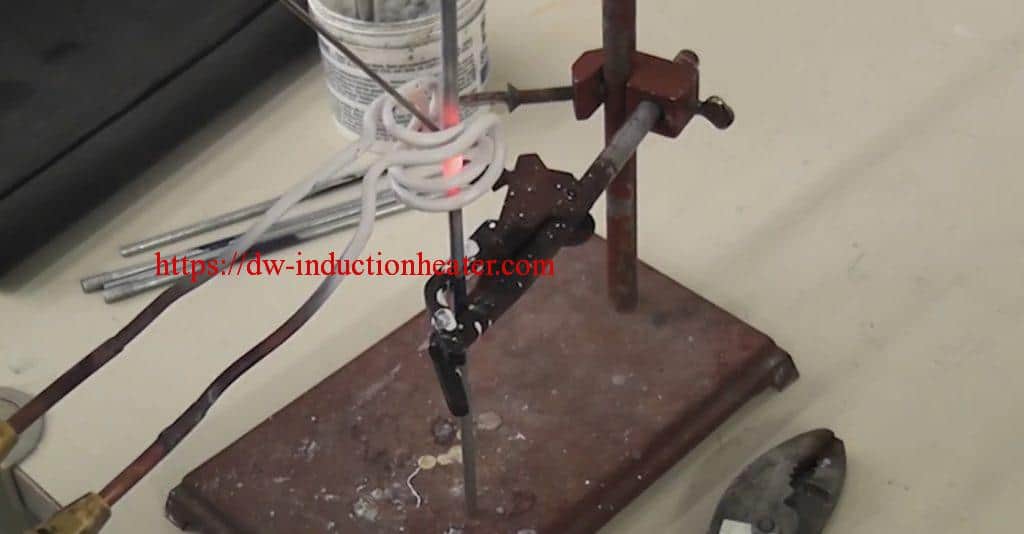
Induction Handheld Brazing Copper To Steel Tube

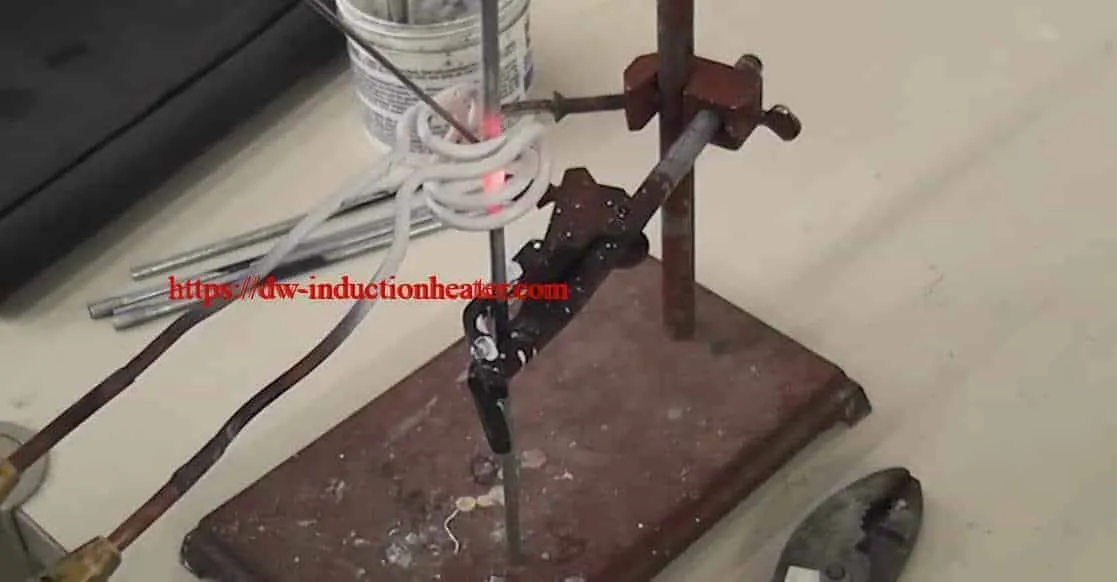
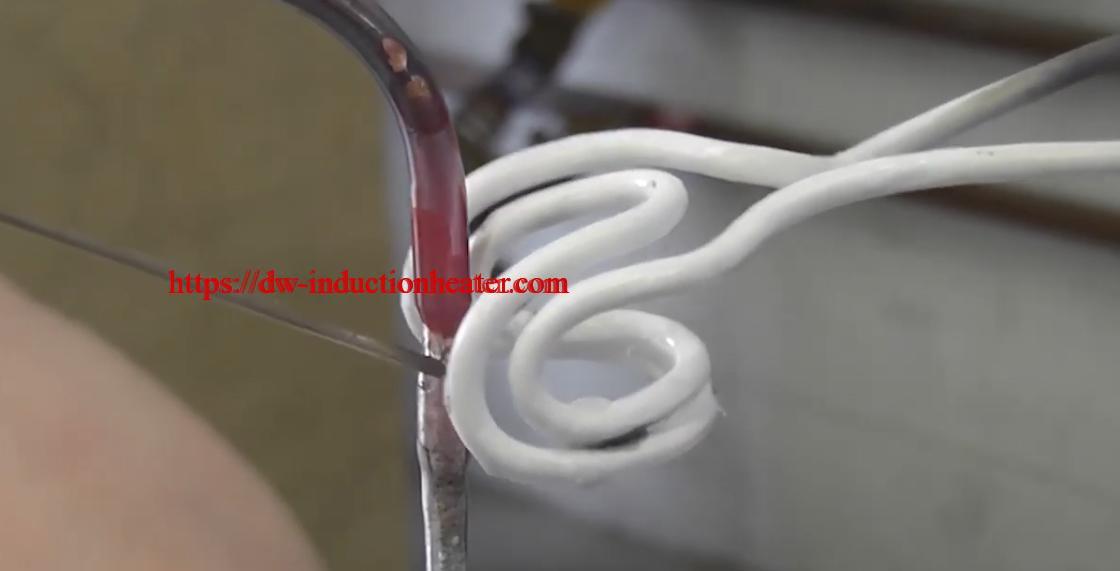
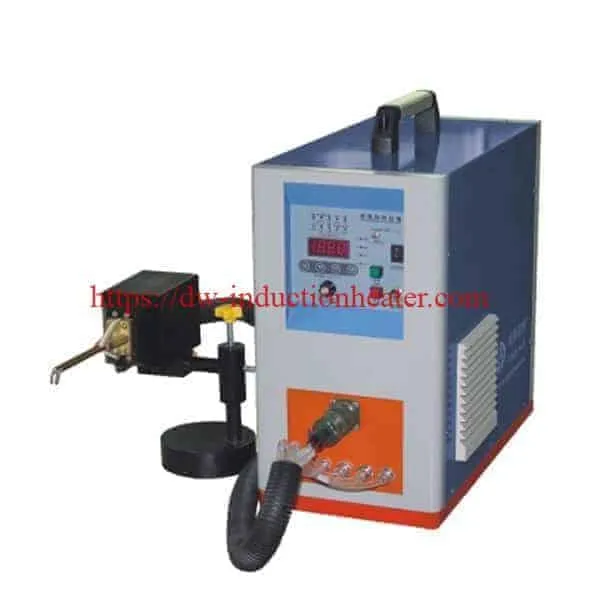
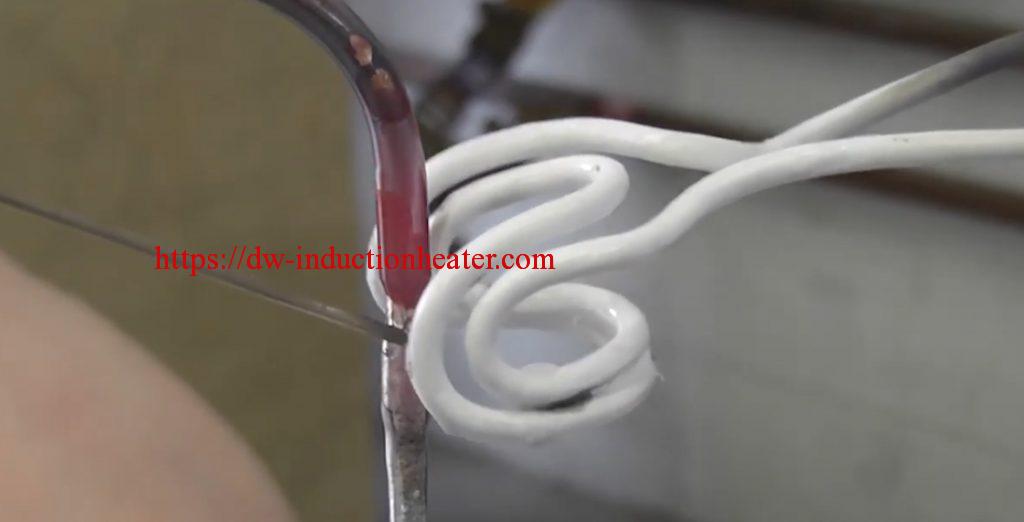
Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"] https://dw-inductionheater.com/induction-handheld-brazing-copper-to-steel-tube.html?feed_id=240602&_unique_id=661409426faca
2023年9月21日星期四

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

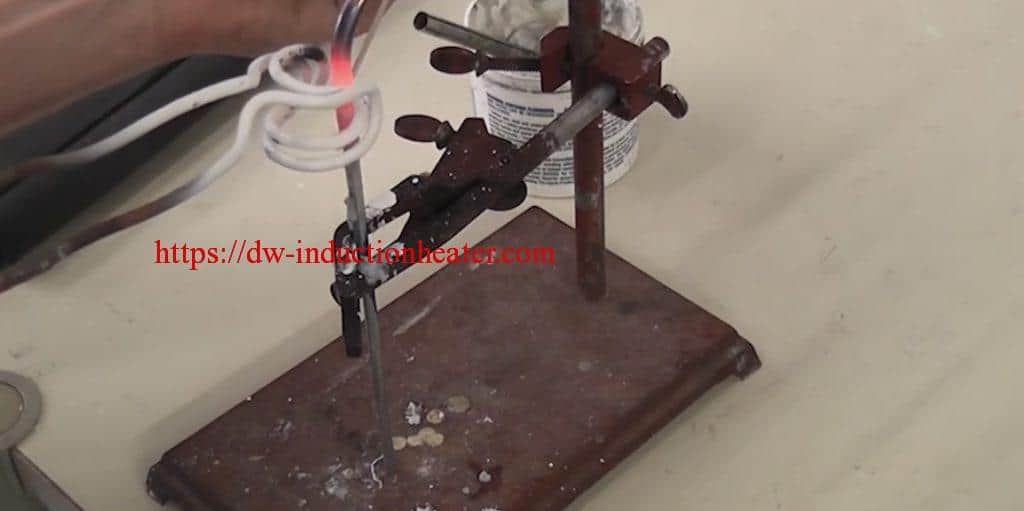
Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]
2023年8月16日星期三

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"] https://dw-inductionheater.com/induction-handheld-brazing-copper-to-steel-tube.html?feed_id=223486&_unique_id=64dd5f3d3b272

2023年5月11日星期四

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

2023年4月26日星期三

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

2023年2月9日星期四

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

2022年10月17日星期一

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

2022年9月30日星期五

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube

Induction Handheld Brazing Copper To Steel Tube Objective Braze copper cylinders, copper wires, and steel tubes in under 20 seconds using the DW-UHF-6KW-III handheld induction heating system. Equipment DW-UHF-6KW-III handheld induction heating system Test 1 Materials • Copper cylinder to copper wire. Power: 6.6kW Temperature: 871° C (1600° F) Time: 20 sec Test 2 Materials • Copper cylinder to steel tube. Power: 10 kW Temperature: 871° C (1600° F) Time: 10 to 11 sec Results and Conclusions: It is recommended to use brazing alloy preforms / rings instead of a brazing rod. This allows the user to use both hands to hold the U-Braze. It also improves the quality of the braze and repeatability by distributing the correct amount of alloy all around the braze joint every time. When brazing copper to steel, it is best to preheat the copper to avoid overheating the steel piece since the copper is harder to heat.   Handheld Brazing Copper To Steel Tube Induction Handheld Brazing Copper To Steel Tube [wpforms id="3947"]

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.