显示标签为“highfrequencybrazingcopperpipe”的博文。显示所有博文

2024年4月9日星期二

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  
https://dw-inductionheater.com/induction-brazing-copper-t-pipe-with-induction-heating-machine.html?feed_id=240796&_unique_id=661576c3c085d

2023年11月13日星期一

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing https://dw-inductionheater.com/induction-brazing-steel-tube.html?feed_id=230676&_unique_id=655282f3806fa

2023年10月26日星期四

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
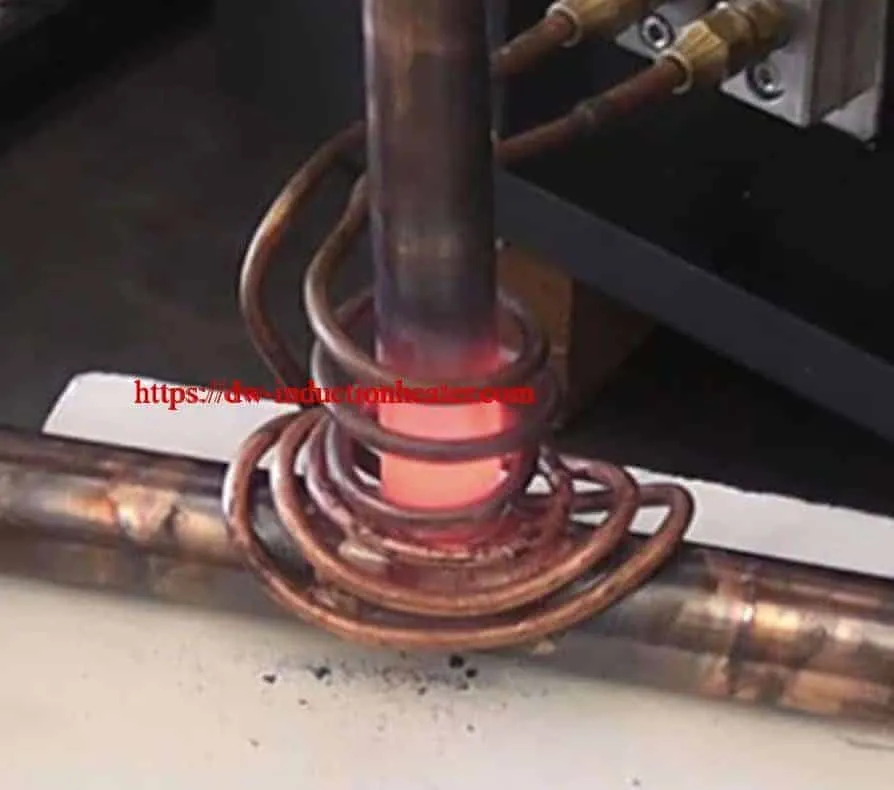
Induction brazing copper pipe  

2023年8月3日星期四

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年6月21日星期三

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年5月4日星期四

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2023年4月8日星期六

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2023年3月27日星期一

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2023年2月21日星期二

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2023年2月8日星期三

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2023年2月3日星期五

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2022年11月14日星期一

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2022年8月25日星期四

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2022年6月22日星期三

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2022年6月11日星期六

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2022年3月5日星期六

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

2022年1月31日星期一

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2022年1月26日星期三

Induction Brazing Steel Tube

Induction Brazing Steel Tube Objective: To heat an oil suction assembly (steel tubing and filter cap) to 1,850°F (1010°C) within 15 seconds for a brazing application. Material 0.125" (3.2mm) diameter steel tube and filter cap assembly, high temperature brazing flux, copper ring. Temperature 1850°F(1010°C) Frequency 500 kHz Equipment • DW-UHF-6KW-I induction heating system equipped with a remote workhead containing 0.66 μF capacitors • An induction heating coil designed and developed specifically for this application. Process A two-turn, specially-contoured helical induction coil is used to heat the tube assembly near the joint area. A copper ring and high temperature flux are then applied to the joint area. Power is applied for 15 seconds until the braze flows. Results/Benefits Induction heating provides: • Easy loading and unloading of parts • Heat very precise areas within production tolerances • Hands free heating that involves minimal operator skill for manufacturing

2021年11月10日星期三

Induction Brazing Copper T Pipe With Induction Heating Machine

Induction Brazing Copper T Pipe With Induction Heating Machine

High frequency Induction brazing copper pipe
Objective Evaluate replacing of flame copper t pipe brazing with induction brazing. Equipment DW-HF-25kw high frequency induction heating machine
Materials
• Copper main tube – 1.13” (28.7 0mm) OD 1.01” (25.65 mm) ID • Riser tube copper – 0.84” (21.33 0mm)  OD,  0.76” (19.30 0mm)  ID Power: Power manually reduced from max output of 10kW to 15kW to provide even heat distribution on the assembly with the modified test coil. NOTE: Heat time can be improved with custom coil design. Temperature:  Approximately 704° C (1300° F) Time: 25sec
Process Steps: Induction brazing copper pipeThe copper tubes were cleaned and assembled. Two preformed alloy rings were made from available alloy in lab for the demonstration.  The wire used measured 0.787mm (0.031”) in diameter  Both the riser an base copper tubes were pre-fluxed with white braze flux. The assembly was placed in the test coil per the video bellow and the alloy flowed to form a joint at the “T” interface in 30seconds. Results and Conclusions: The target heat time for the smallest T joint assembly is 20 seconds . Using a lab test coil, we were able to effect a braze in the interface section of the tubes (copper) in 30 seconds. Induction brazing copper pipe  
Induction brazing copper pipe  

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.