induction brazing copper and brass rods
Objective
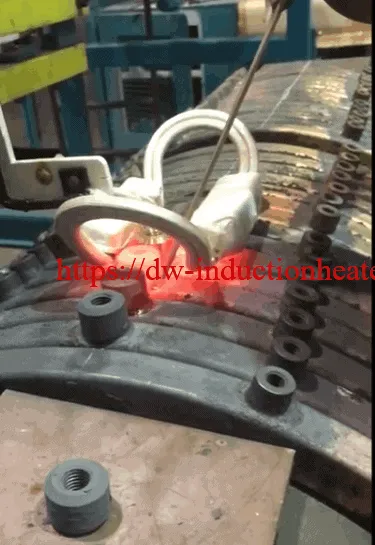
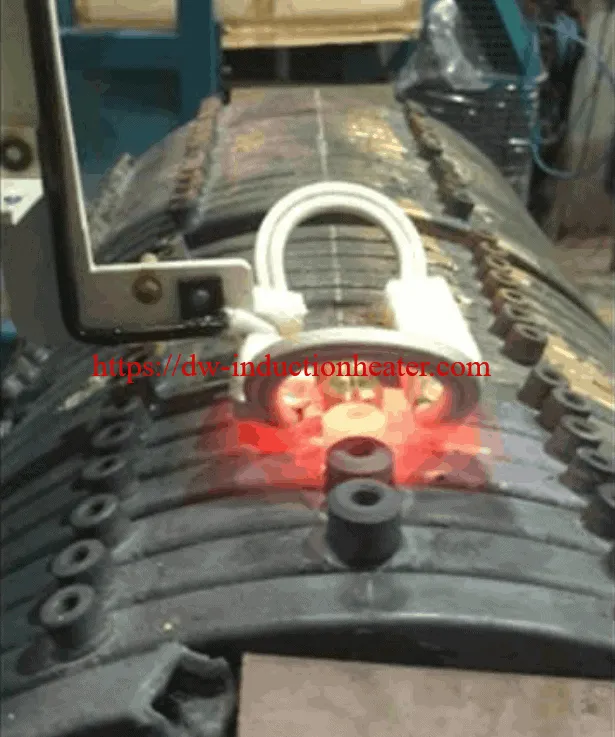
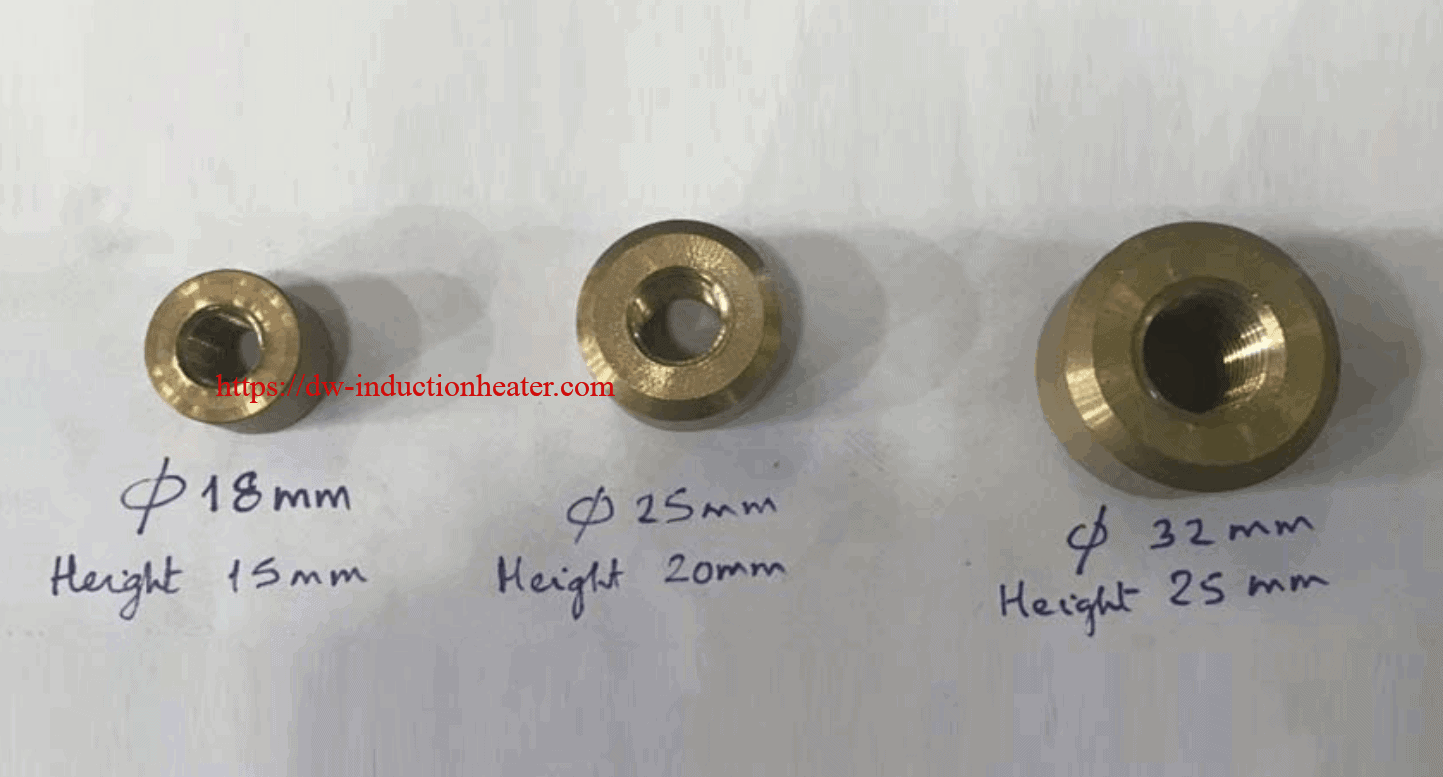
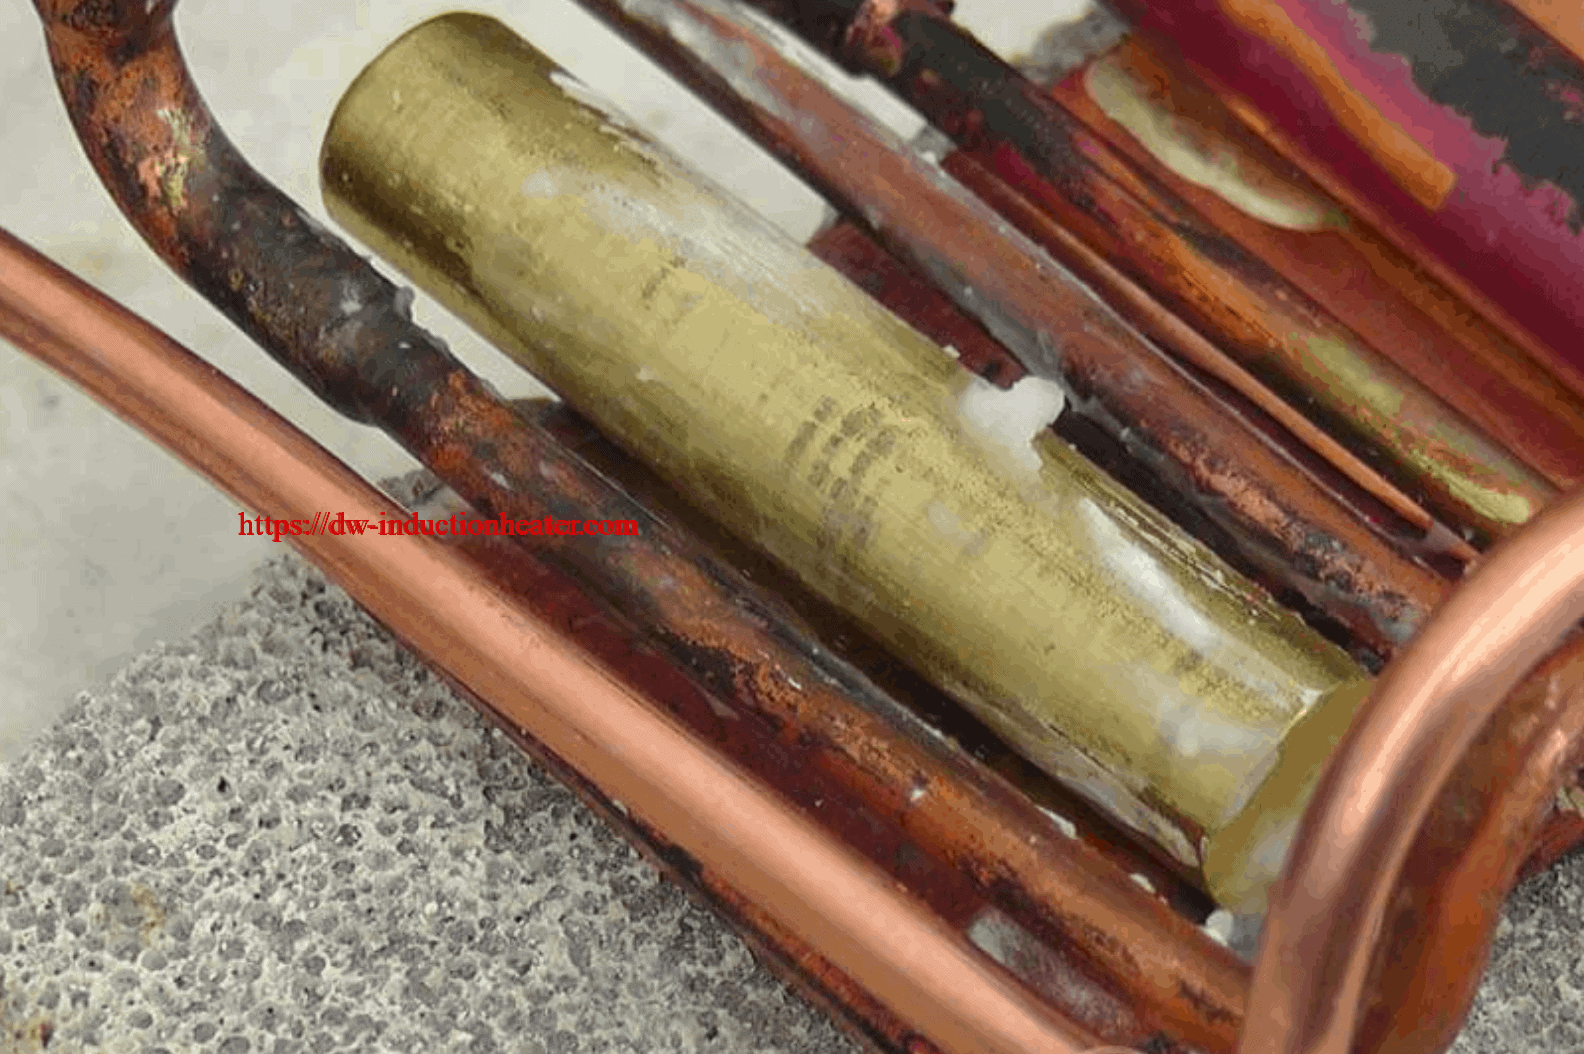
Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation.
Equipment
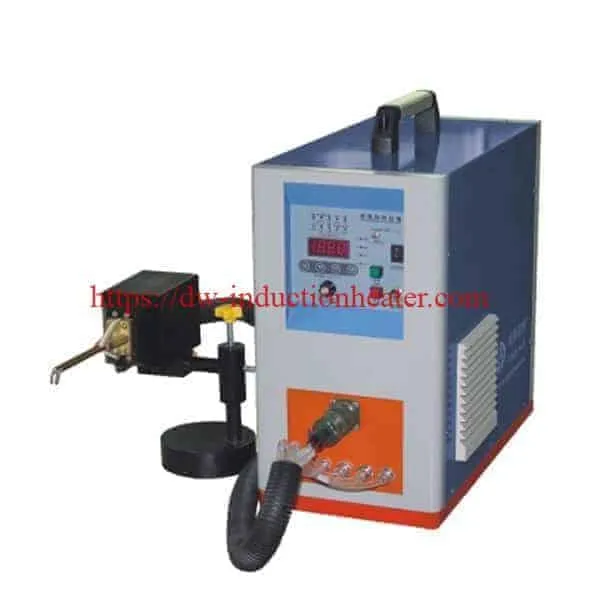
DW-UHF-40KW high frequency induction brazing machine
Two turn open end conveyor coil
Materials
• Copper coupon plate and copper rod
• Braze wire – EZ Flo 45
• Braze alloy – 45% Silver, 1/32 DIA
TEST
Power: 30 kW
Temperature: Approximately 1350° F (732° C)
Time: Average time – 25 seconds
Process and Results:
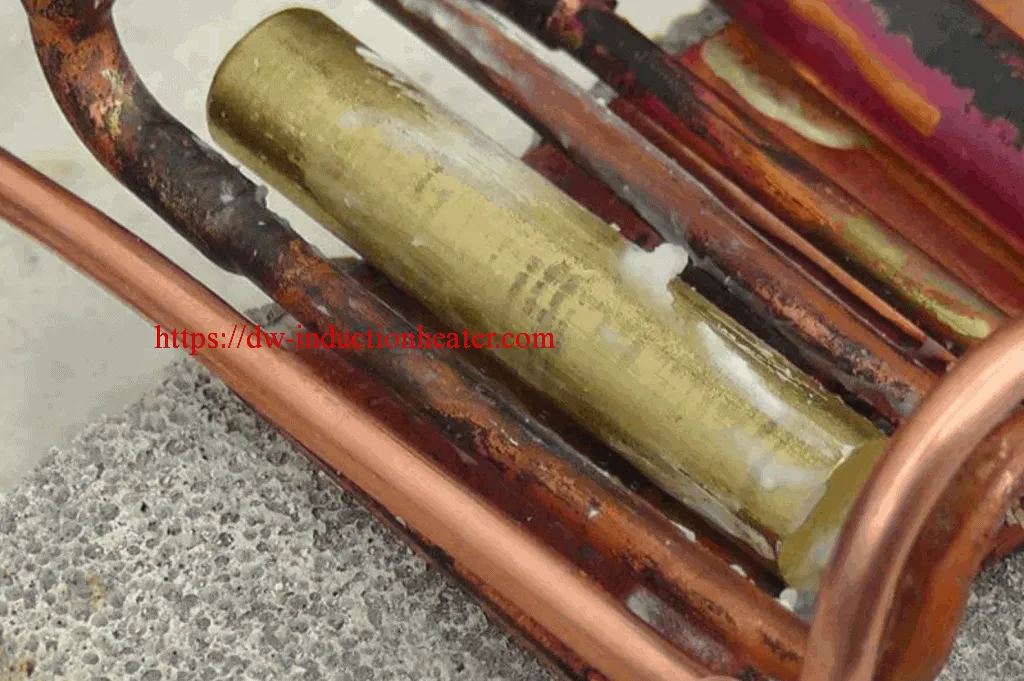
For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze.
Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate.
Results/Benefits:
- Strong durable joints
- Selective and precise heat zone, resulting in less part distortion and joint stress than welding
- Less oxidation
- Faster heating cycles
- More consistent results and suitability for large volume production, without the need for batch processing
- Safer than flame brazing
 [wpforms id="3947"]
https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=240534&_unique_id=6613527647eb1

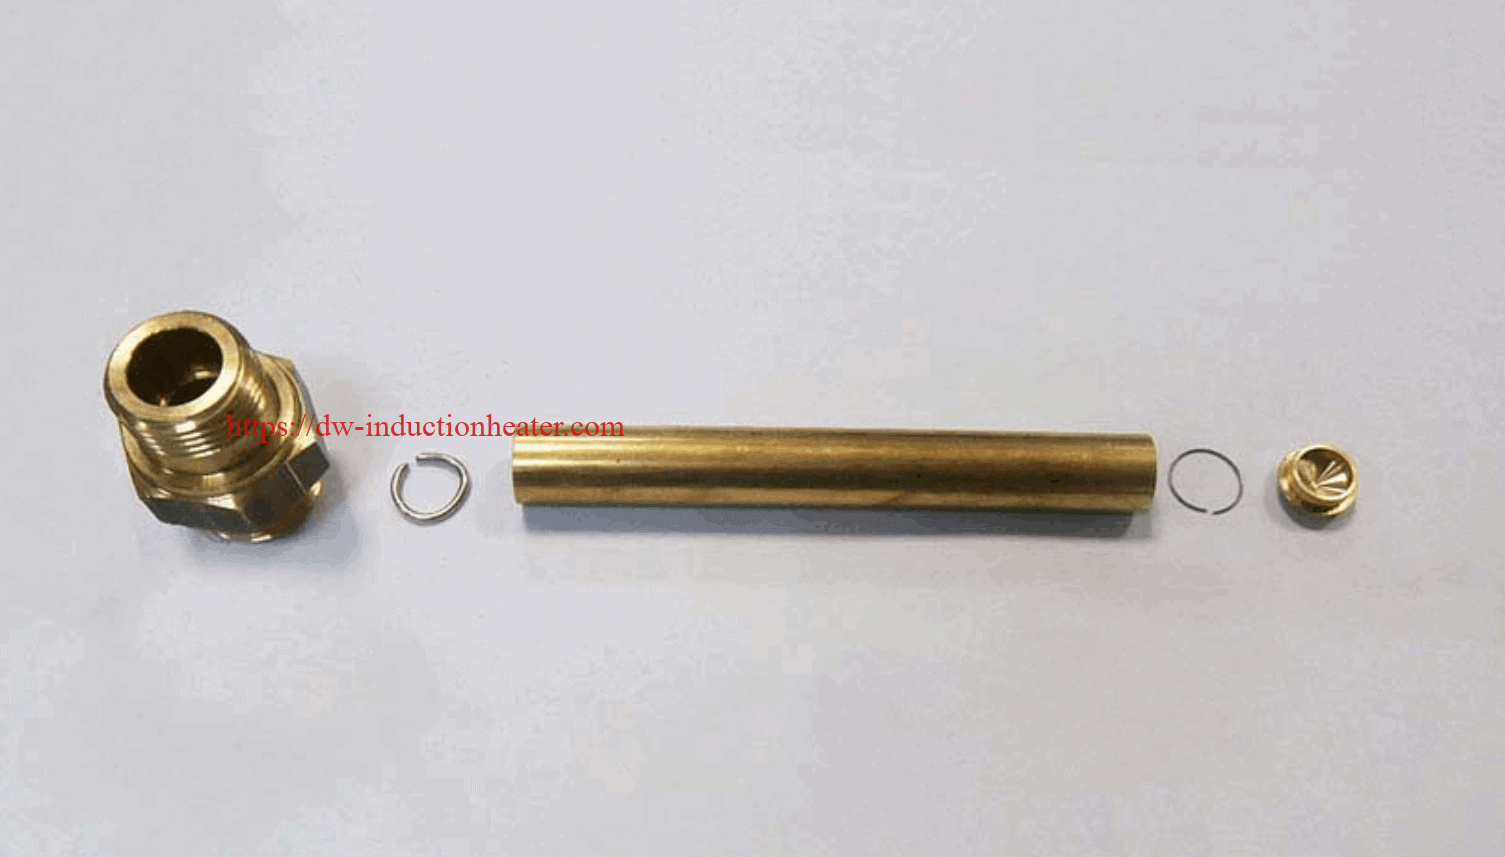
 Brazing Brass Fittings With Induction
Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm)
Material: Brass tubing Brass flange Braze rings Braze flux
Temperature :1382°F (750°C)
Frequency 200 kHz
Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application.
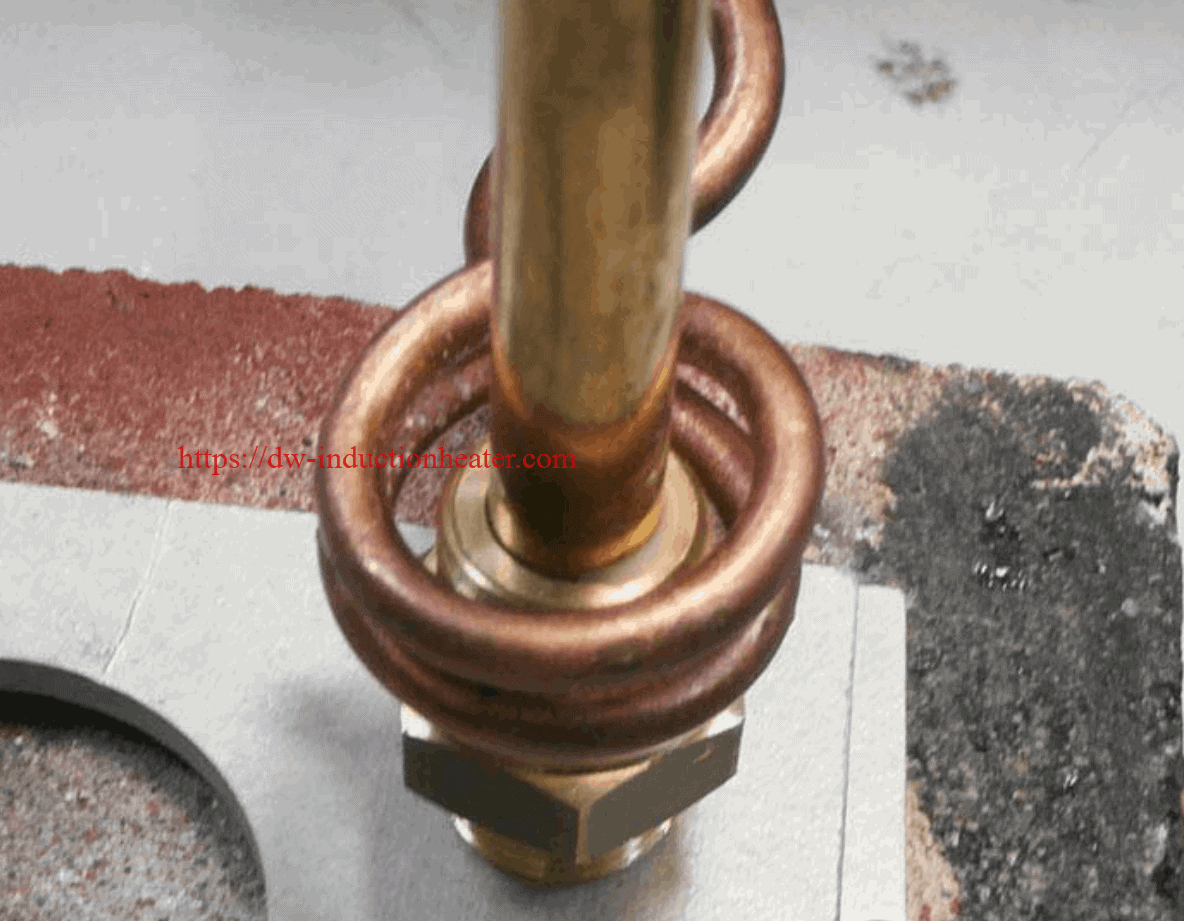
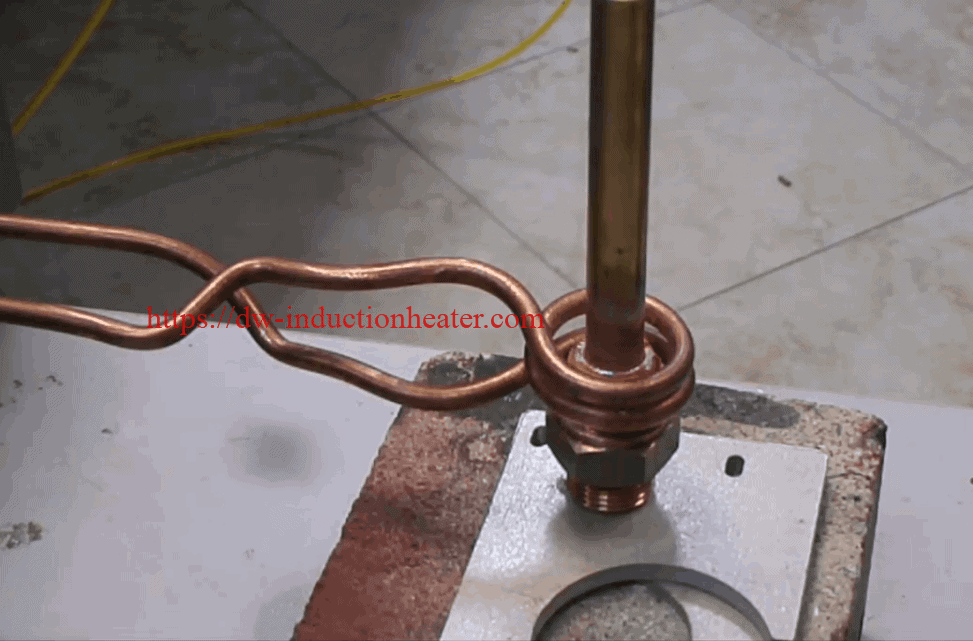
Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter.
Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes.
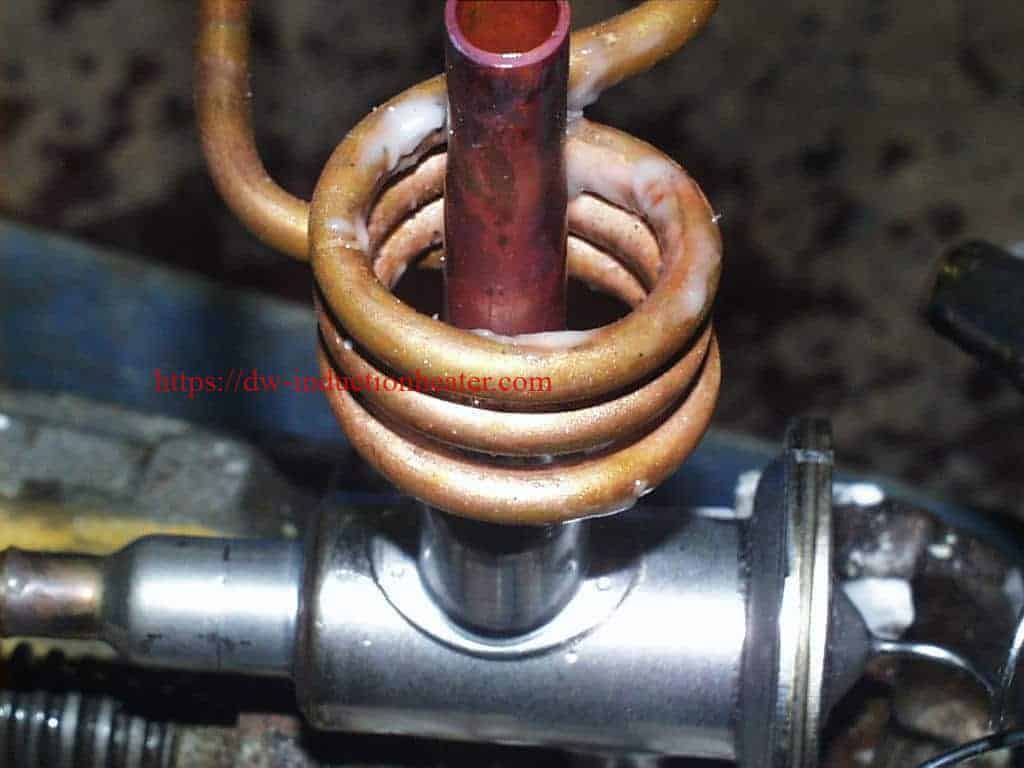 Brazing Brass to Aluminum with Induction
Objective: Copper 'tees' and 'ells' are to be brazed to the aluminum body of a refrigeration valve
Material customer's valve copper fittings braze
Temperature 2550 ºF (1400°C)
Frequency 360 kHz
Equipment DW-UHF-10KW induction heating system including a workhead containing two 1.5μF capacitors (total 0.75μF) and a three-turn helical coil
Process The valve is placed inside the coil and RF power is applied until the part is heated to the required temperature and the braze is seen to flow into the joint. Two tube sizes were run using the same induction system settings with differing cycle times.
Results/Benefits • energy is applied only to the zone to be heated • heating of the joint/braze is uniform and repeatable
 Induction Brazing Brass Faucet
Objective Brazing two joints on a brass bathroom faucet assembly
Material Brass bathroom fittings 1” OD, brazing rings, flux
Temperature 1148 ºF (620 ºC)
Frequency 90 kHz
Equipment • DW-UHF-30 kW induction heating system, equipped with a remote workhead containing eight 1.0 μF capacitors for a total of 8.0 μF
• An induction heating coil designed and developed specifically for this application.
Process A two turn C shaped coil is used to braze the faucet assembly.
The braze rings are placed at the joint, the parts assembled and fluxed. The first braze joint is heated for 30 seconds and the braze ring flows. The assembly is rotated & the second joint is heated for 30 seconds to flow the braze ring. The two brazes are completed in 60 seconds.
Results/Benefits Induction heating provides:
• Faster, repeatable and consistent results
• Localized heat produces neat and clean joints
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
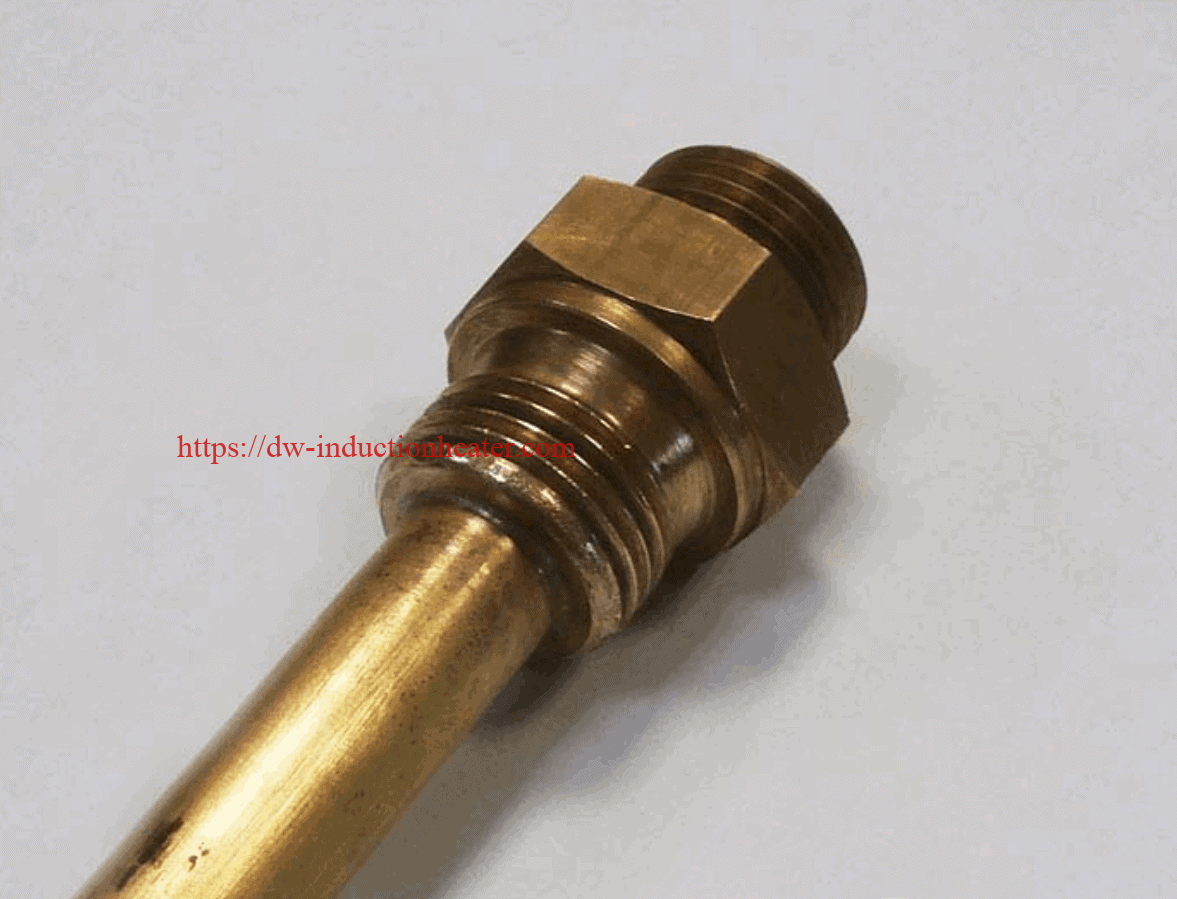
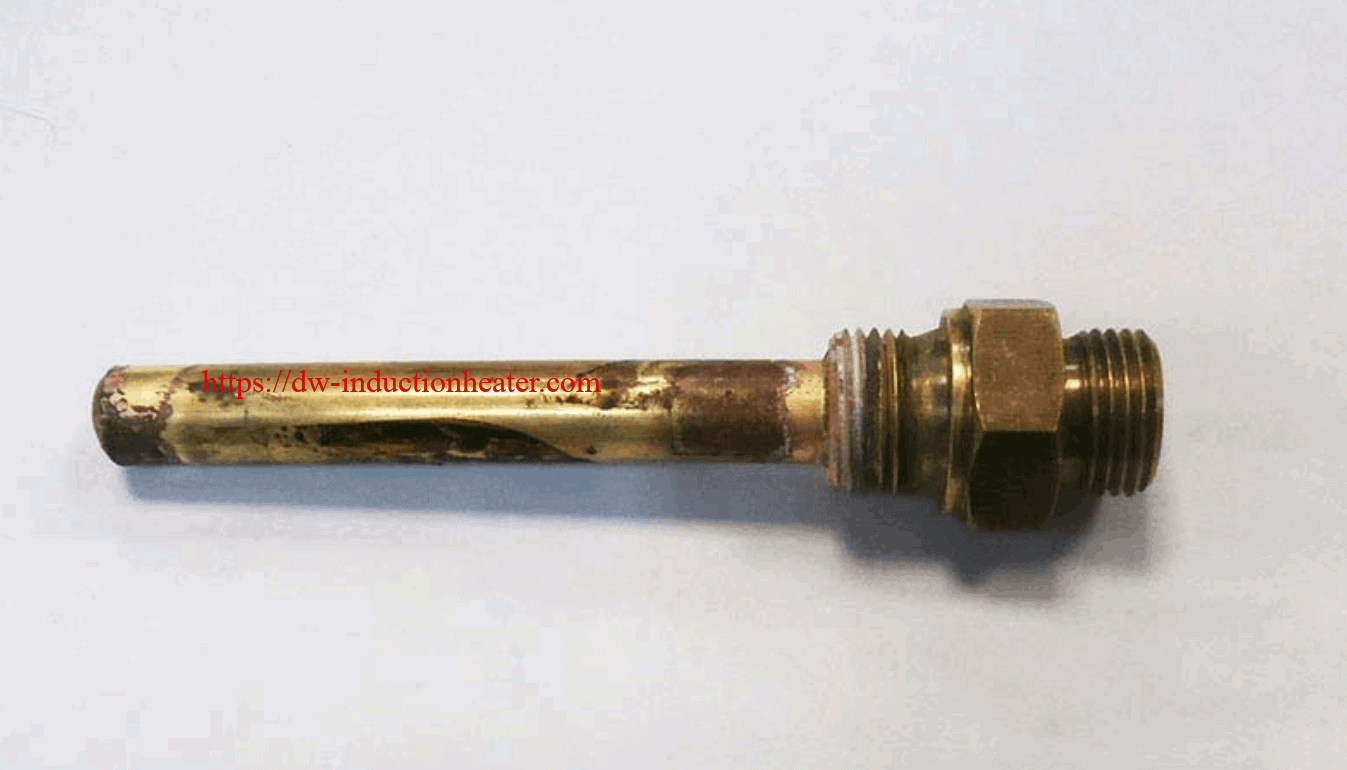
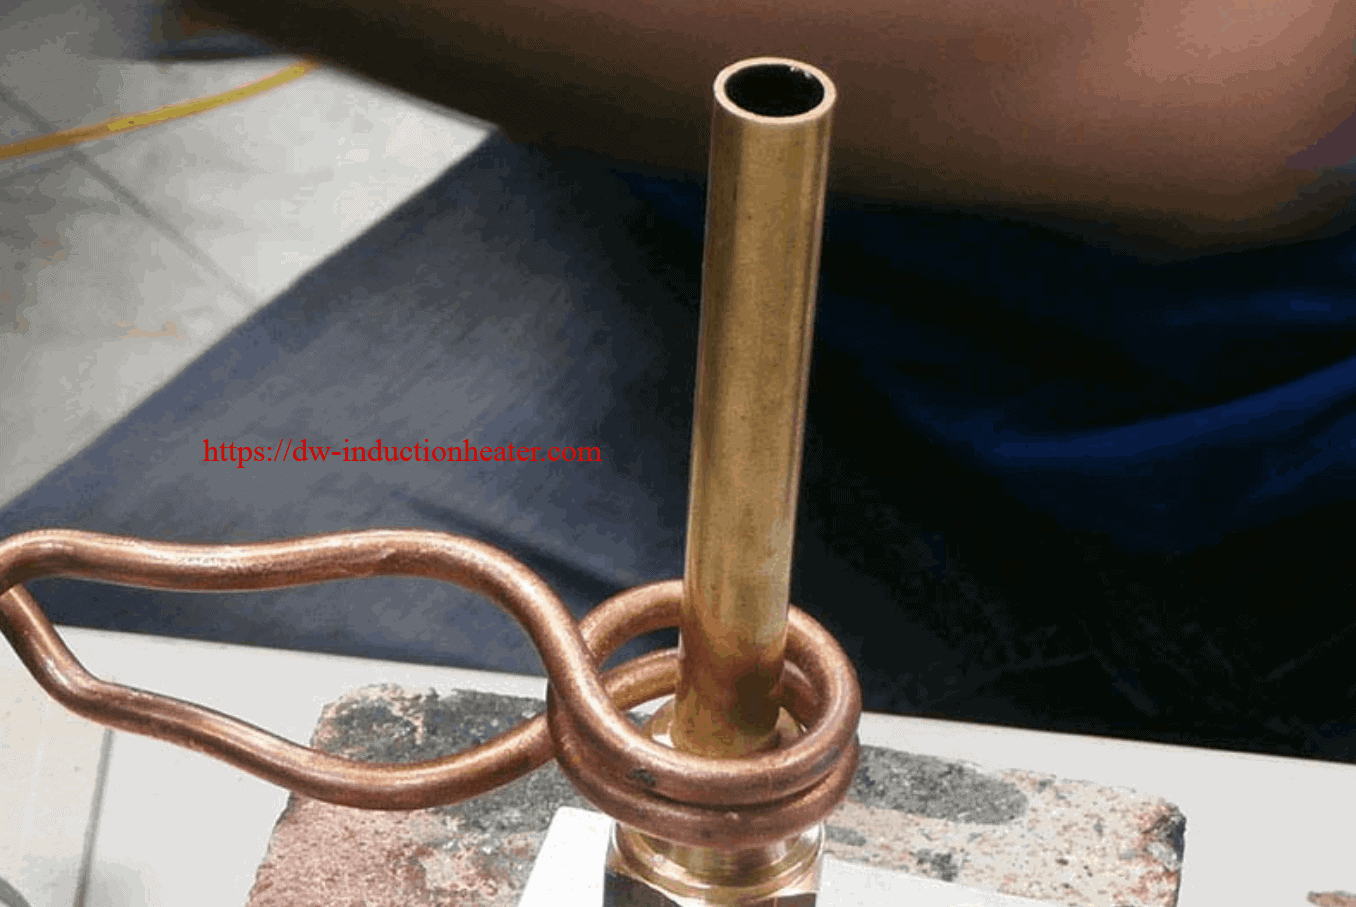
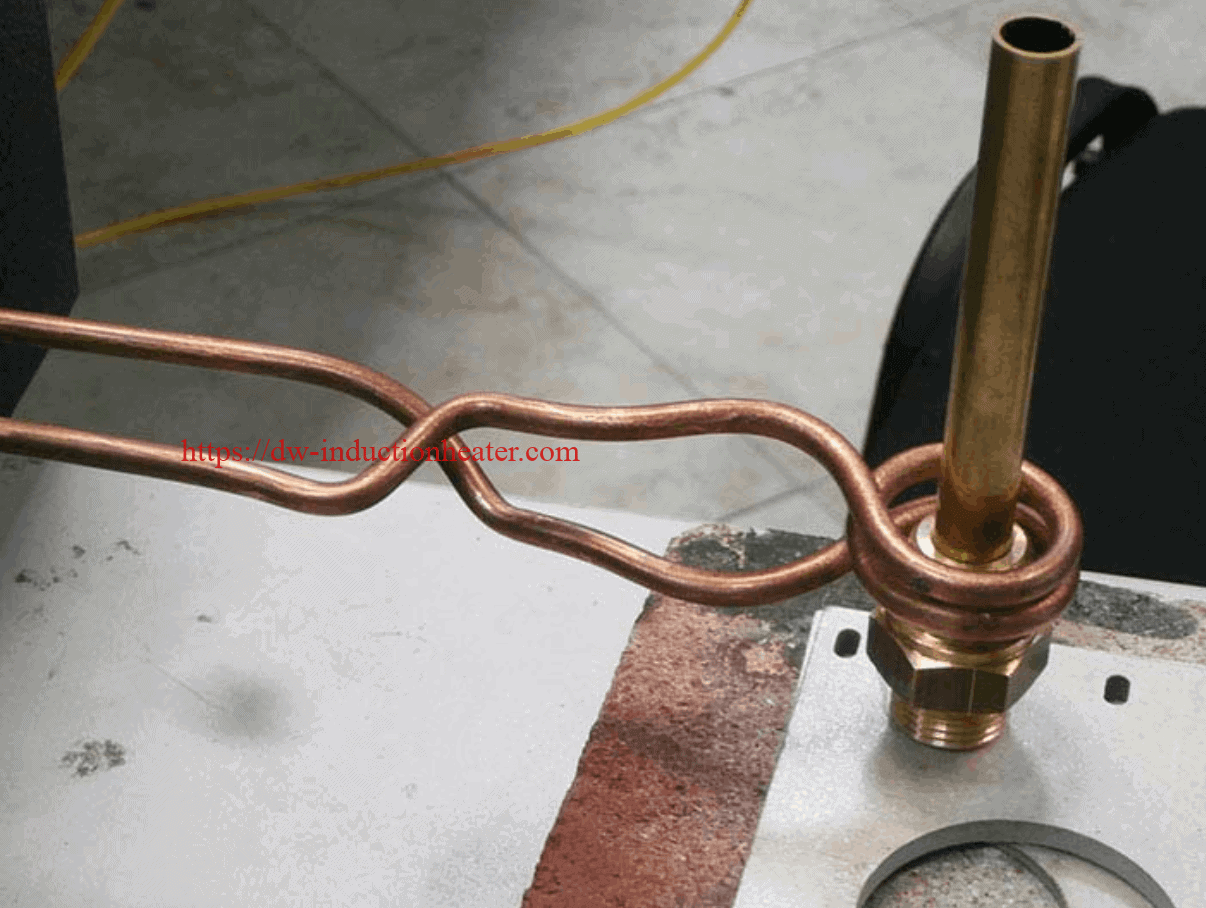
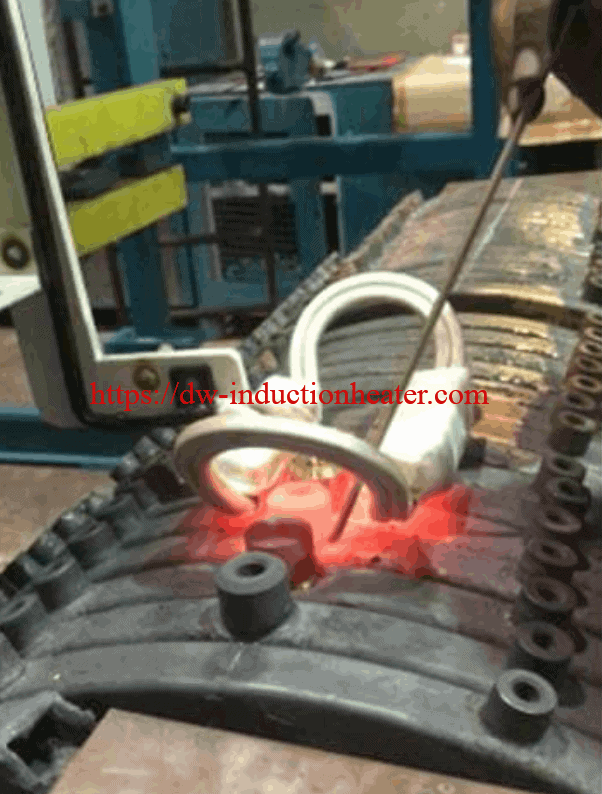 Induction Brazing Brass Studs to Copper Pipes