显示标签为“brazingbrass”的博文。显示所有博文

2024年4月7日星期日

induction brazing copper and brass rods

induction brazing copper and brass rods

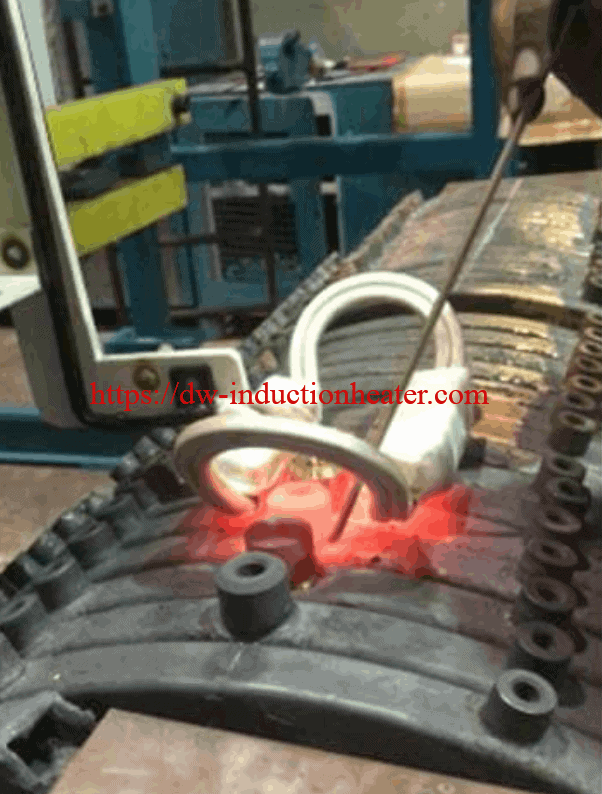
Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
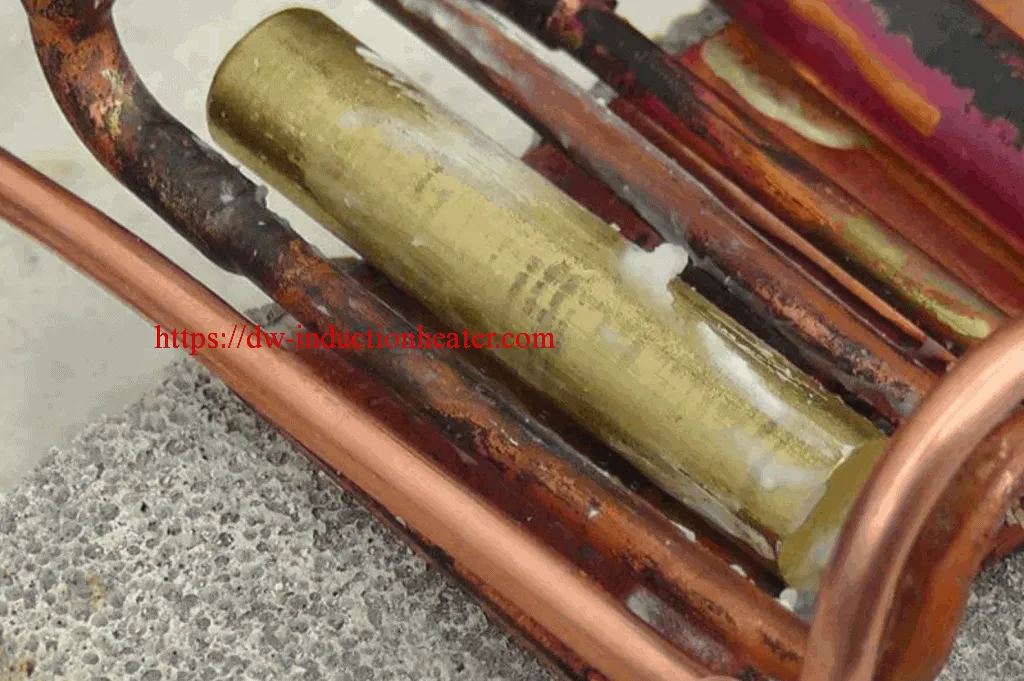
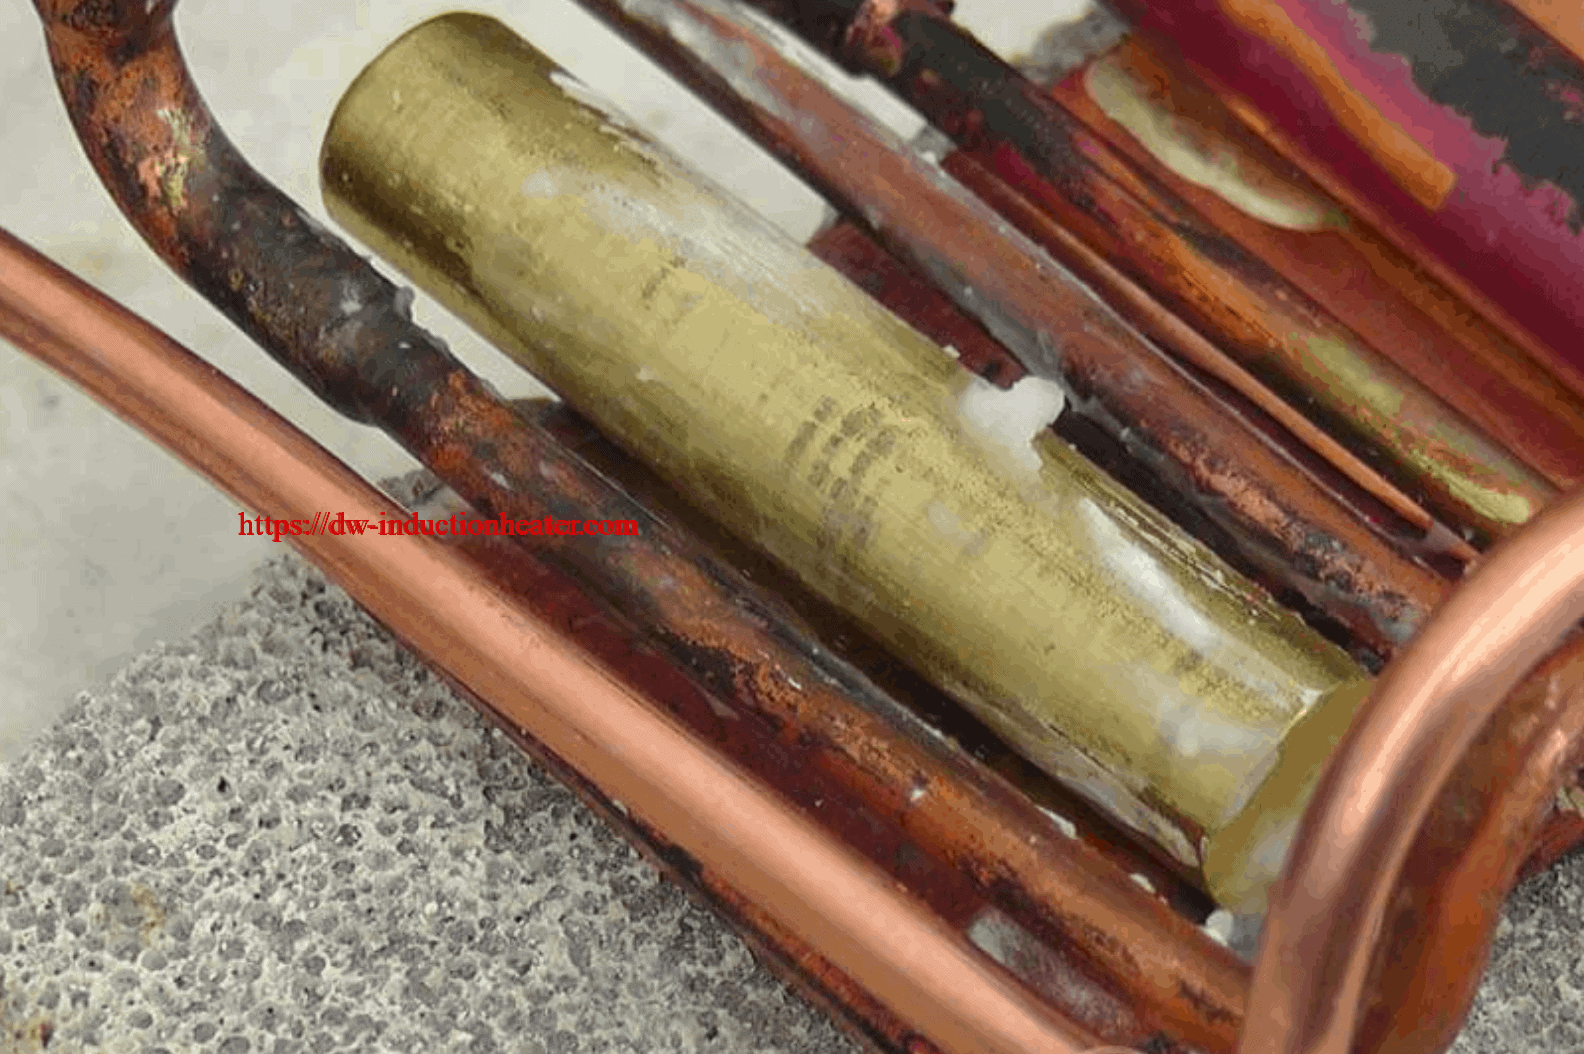
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=240534&_unique_id=6613527647eb1

2024年3月16日星期六

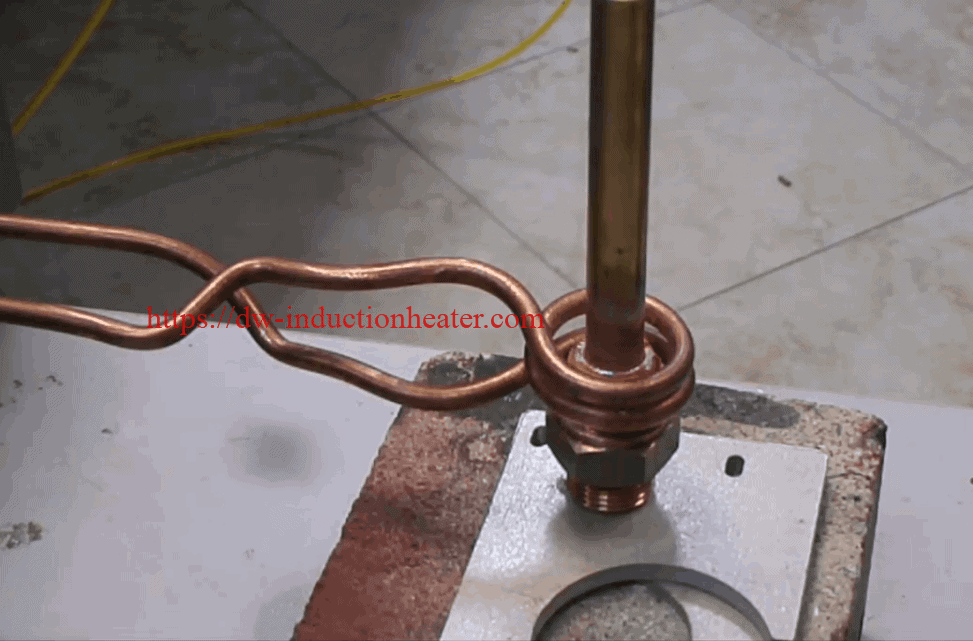
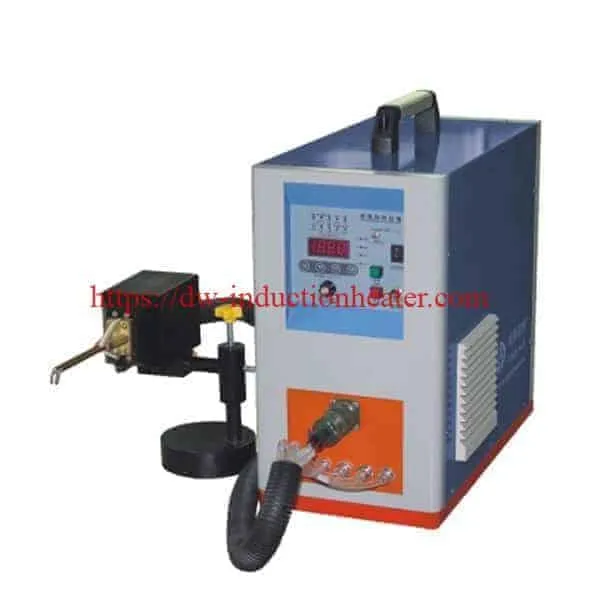
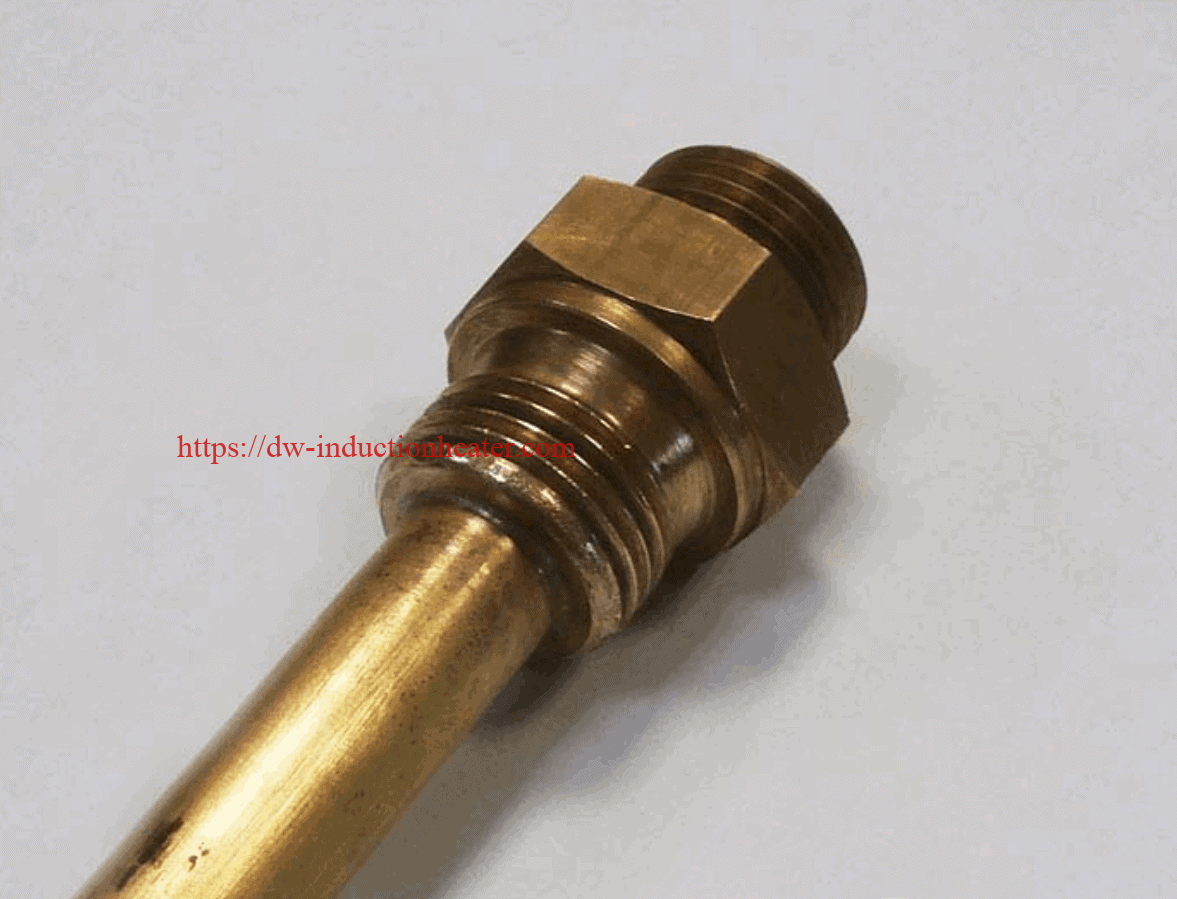
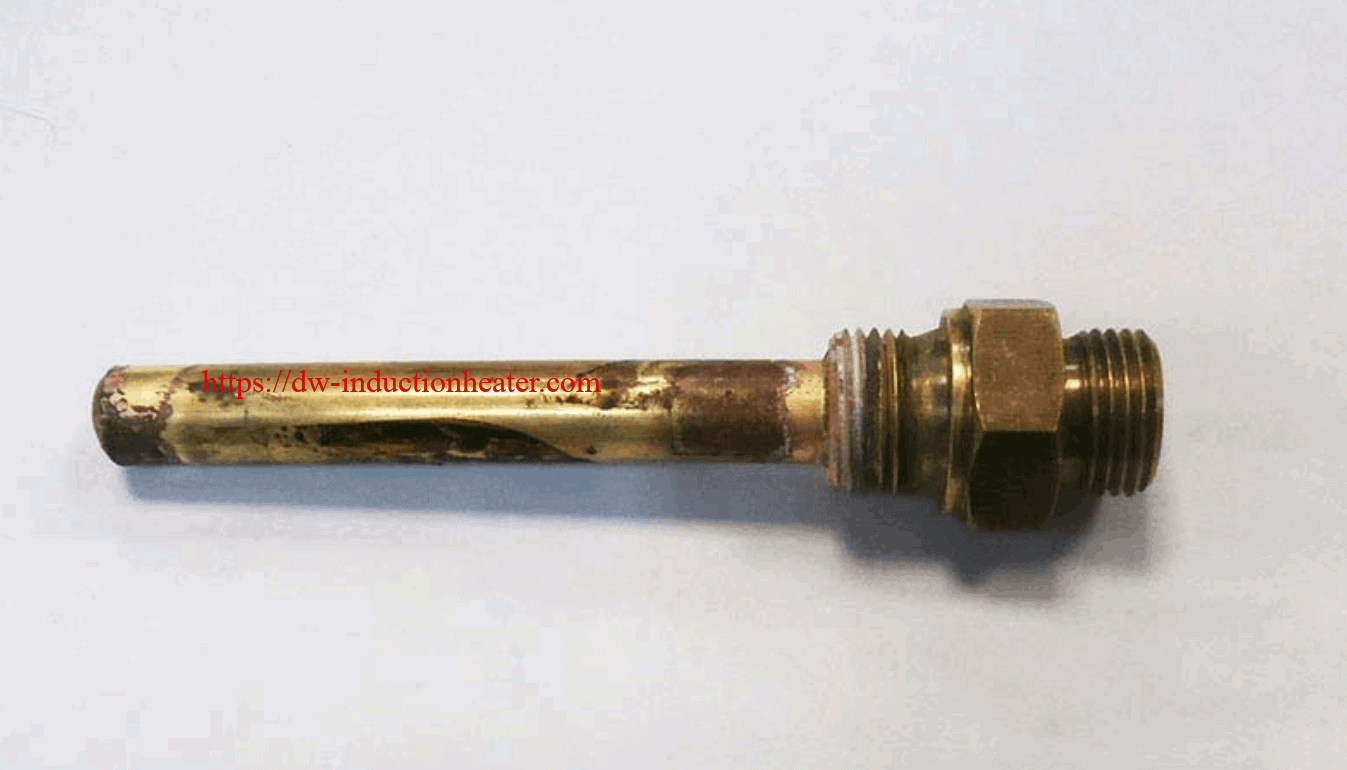
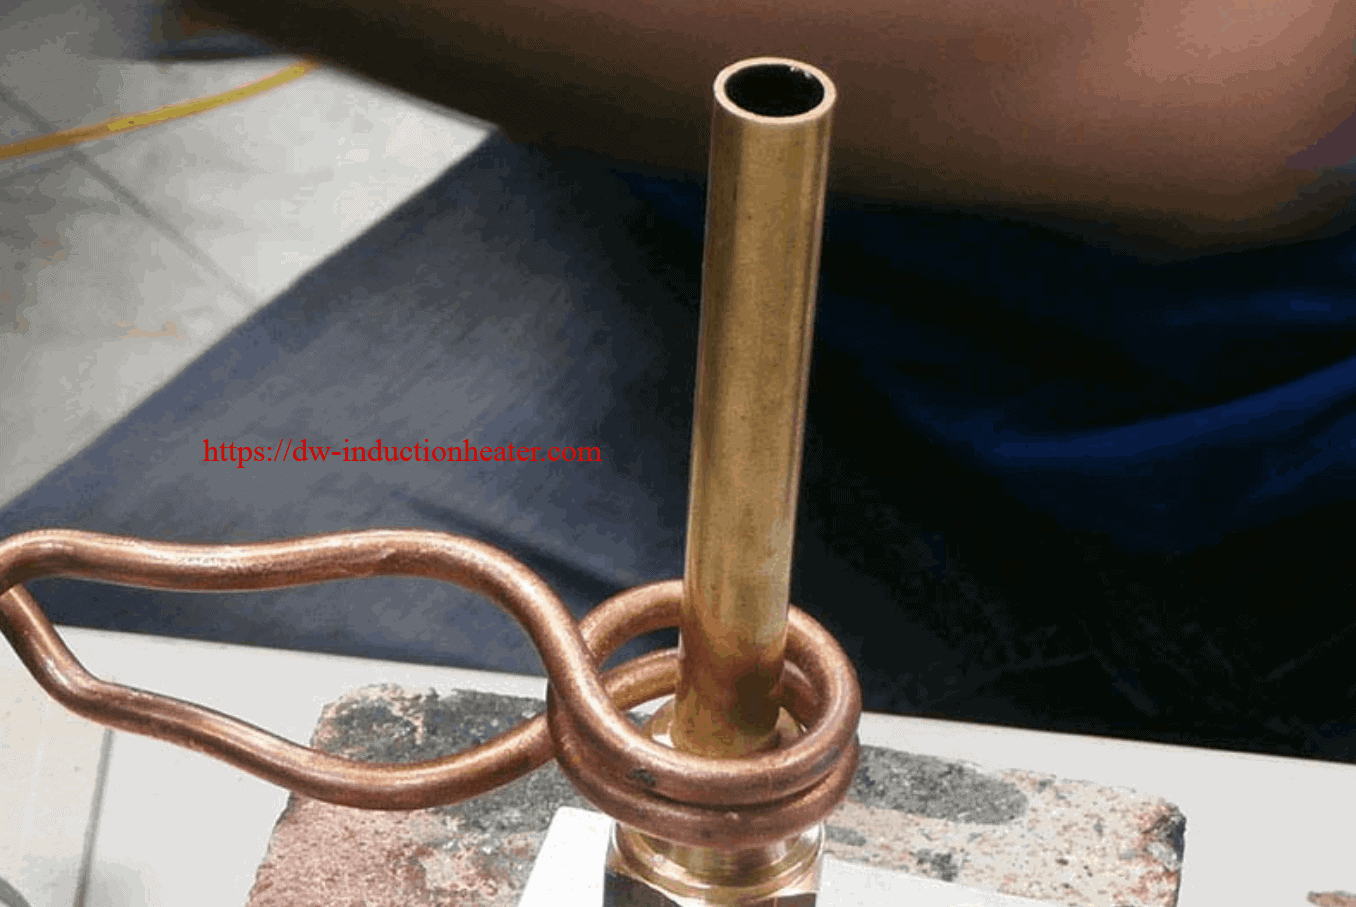
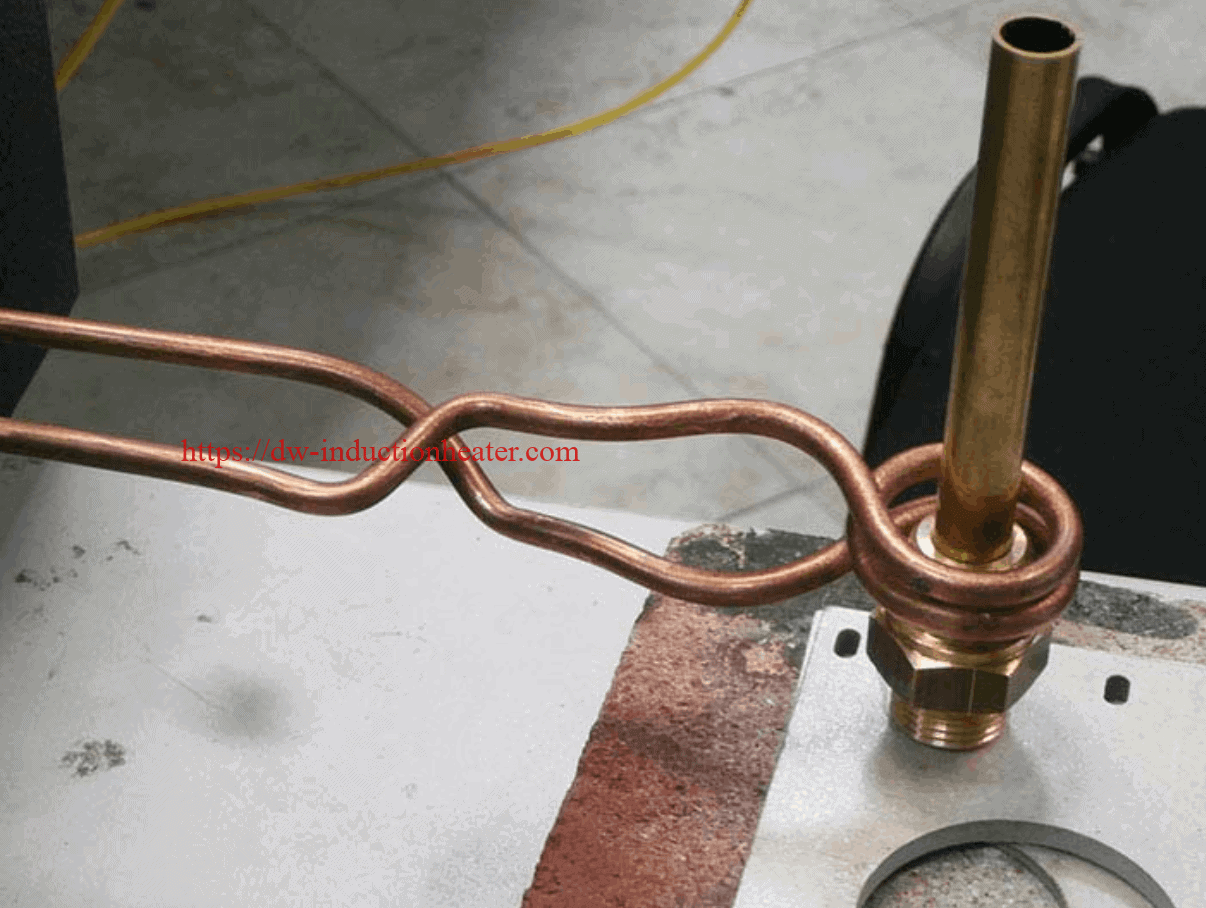
induction brazing brass pipe to brass part

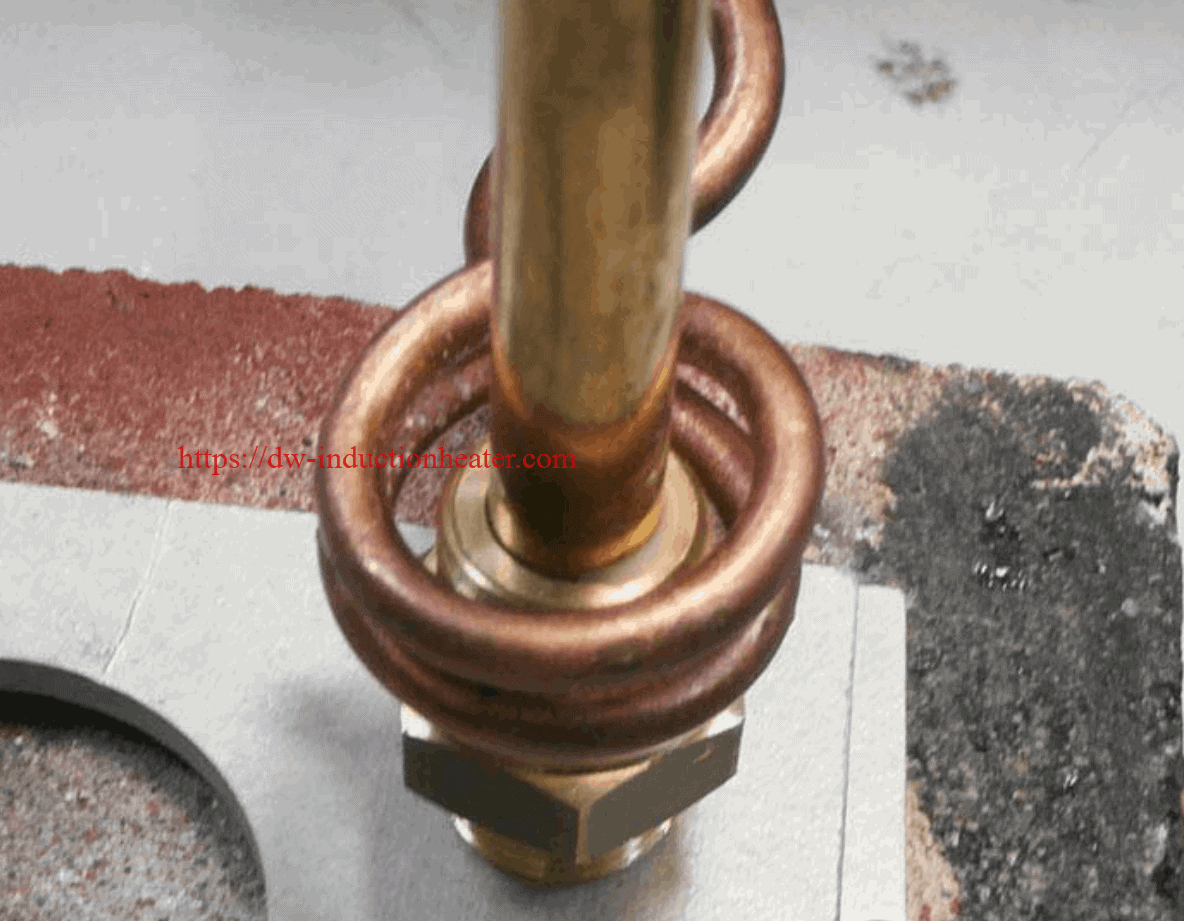
Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
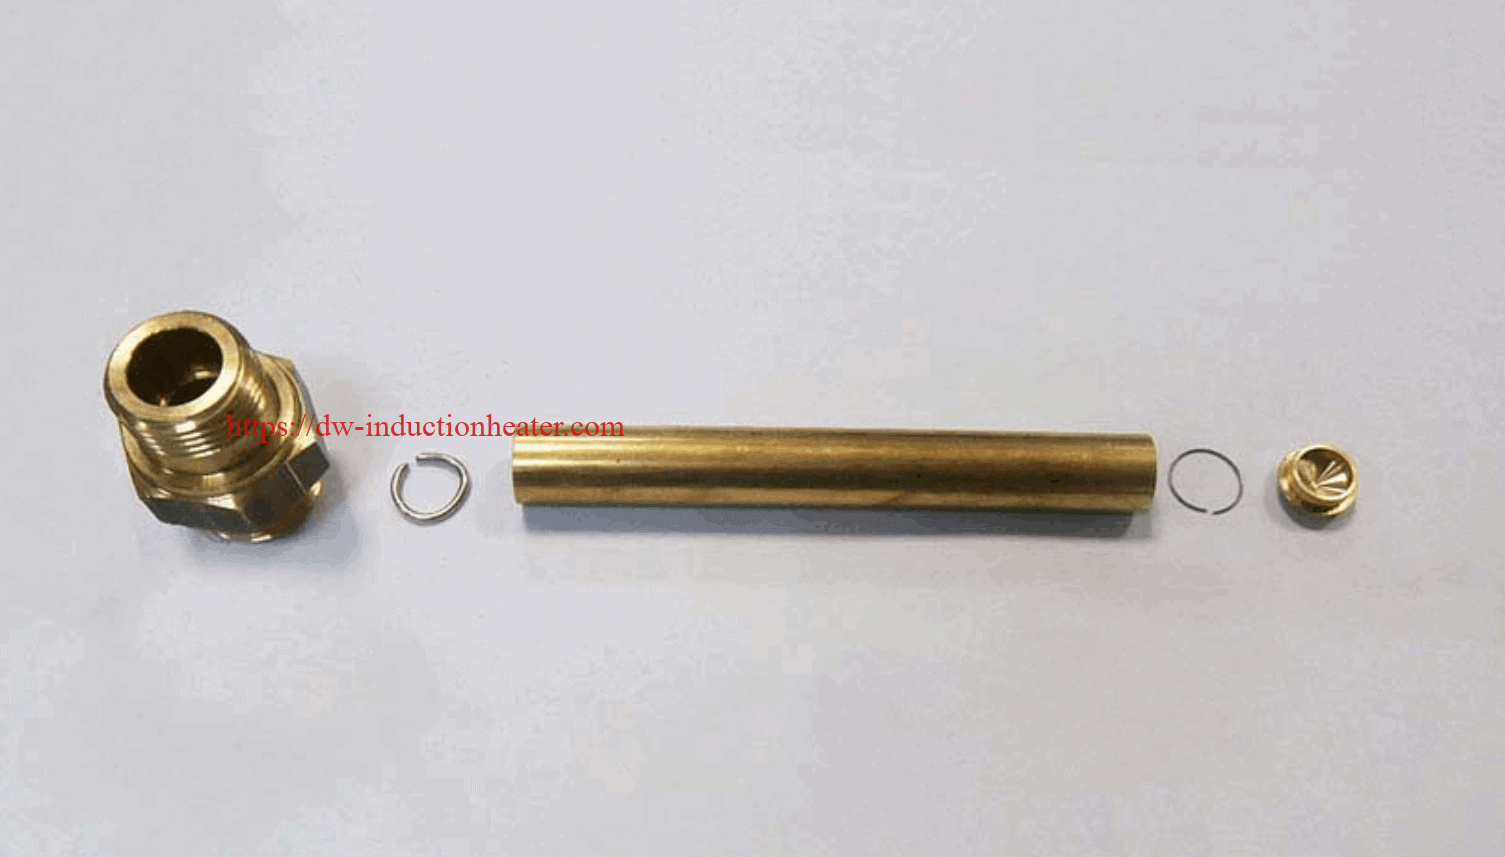
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing
https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html?feed_id=236860&_unique_id=65f555b095631

2023年8月19日星期六

induction brazing copper and brass rods

induction brazing copper and brass rods

Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"]

2023年8月18日星期五

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing

2023年8月16日星期三

induction brazing copper and brass rods

induction brazing copper and brass rods

Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"] https://dw-inductionheater.com/induction-brazing-copper-and-brass-rods.html?feed_id=223411&_unique_id=64dca846dfa63

2023年7月29日星期六

Induction Brazing Brass Studs to Copper Pipes
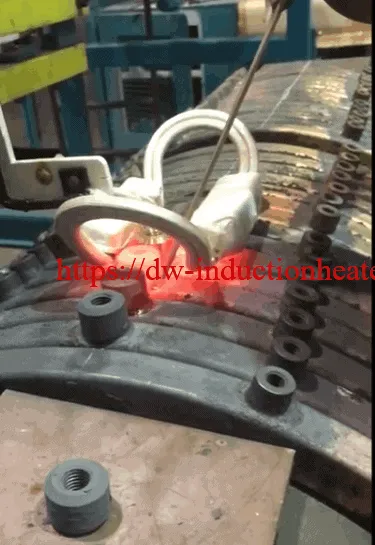
Induction Brazing Brass Studs to Copper Pipes
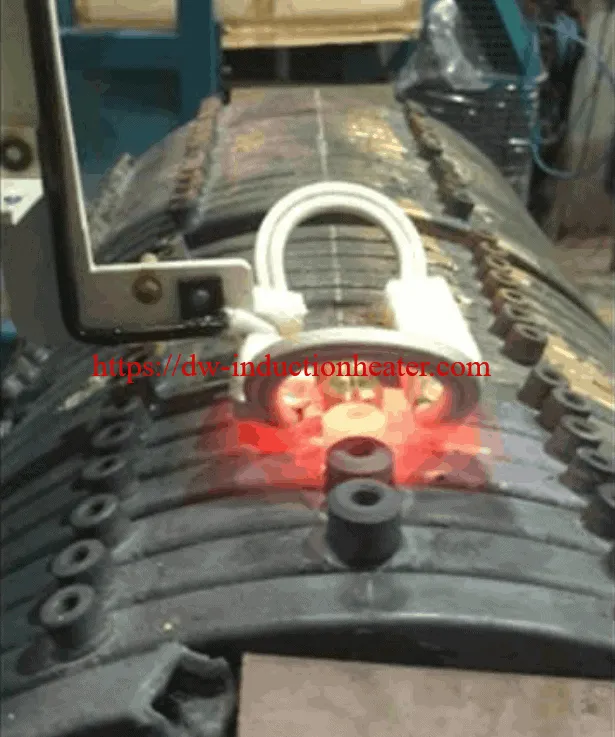
Objective:

Induction brazing brass studs to copper pipes

The Client:

A manufacturer of coils for industrial heating applications.

Equipment:

DW-UHF-40KW Induction Brazing Systems – two modules.

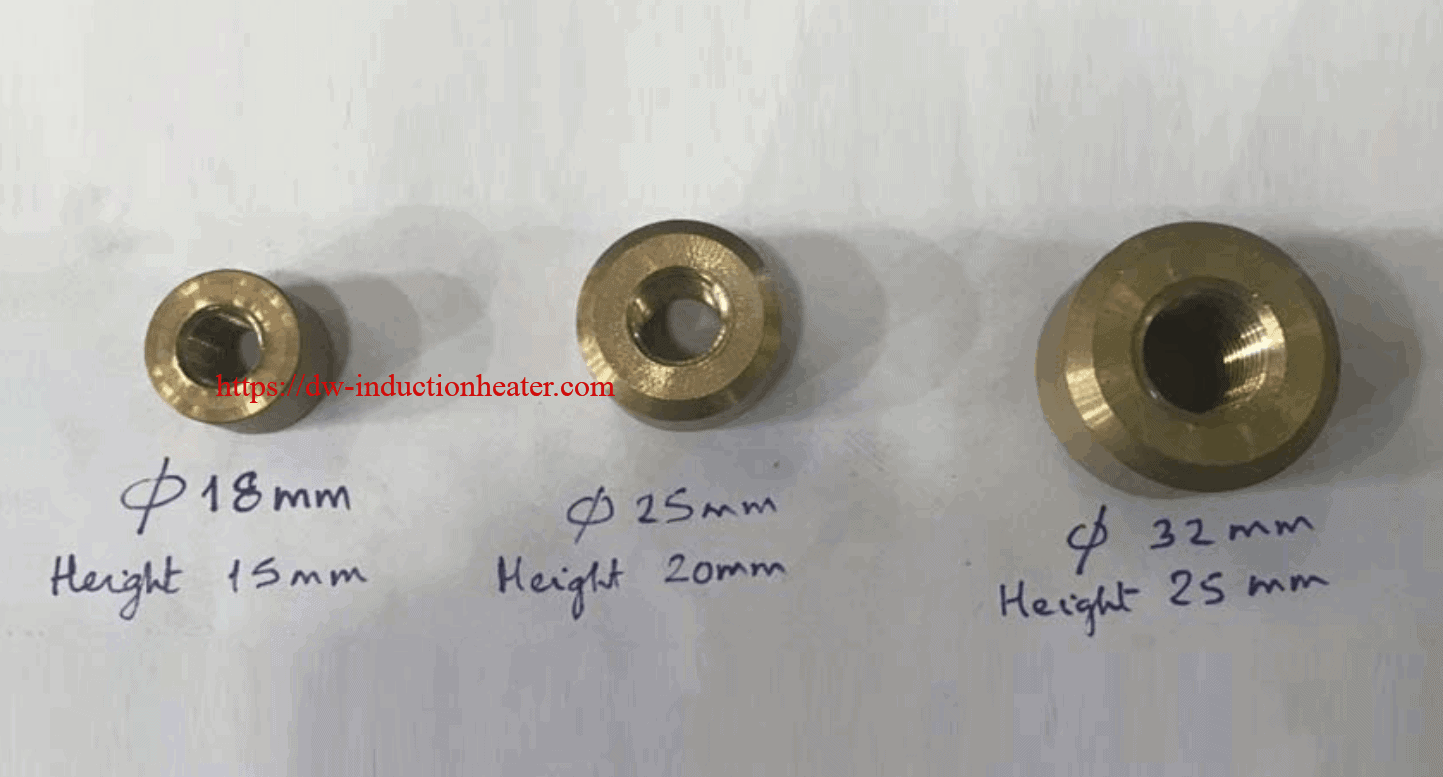
Materials: Brass stud ( size:  25mm diameter, 20 mm height ) Power: 30 kW
The Process:  The main challenge during this induction brazing process is to ensure that the design of the coil is one that eases the technician to position it in the most convenient way. The induction coil should allow for the second stud to be pre-heated without melting the first one. First, the electrolytic copper section is wound on a steel former by a gas torch while an equal spacing between the turns is maintained. Then, the copper turn is heated close to the required temperature and while the power is ON, the technician should make sure to manually position the brass stud with the brazing ring at the designated centre. During the process of brazing, the induction coil is moving at a speed of 58 mm per minute – 33 kW. If the power is increased, the speed changes accordingly. Results and Conclusions:
  • A fast, clean and safe induction brazing process
  • Guaranteed repeatability
  • Precise control of time and temperature
https://dw-inductionheater.com/induction-brazing-brass-studs-to-copper-pipes.html?feed_id=221086&_unique_id=64c5bde9f35f8

2023年7月23日星期日

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing
https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html?feed_id=220186&_unique_id=64bde142a19f8

2023年5月17日星期三

induction brazing copper and brass rods

induction brazing copper and brass rods

Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"]

2023年4月24日星期一

induction brazing copper and brass rods

induction brazing copper and brass rods

Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"]

2023年4月18日星期二

induction brazing copper and brass rods

induction brazing copper and brass rods

Objective Induction Brazing copper and brass rods and strips to replace torch operation. The current torch process results in excessive contaminants on the assembly, and requires extensive rework after the brazing operation. induction brazing brass copper
Equipment DW-UHF-40KW high frequency induction brazing machine Two turn open end conveyor coil Materials • Copper coupon plate and copper rod • Braze wire – EZ Flo 45 • Braze alloy – 45% Silver, 1/32 DIA TEST Power: 30 kW Temperature: Approximately 1350° F (732° C) Time: Average time – 25 seconds Process and Results: For Induction braze copper coupon plate and copper rod,, EZ Flo 45 braze wire was cut into 2” lengths and placed in the interface area. In a production situation, EZ Flo 45 brazing paste is recommended. The assemblies were set up (see photographs) and heated for an average time of 25s to flow the alloy and achieve the braze. Due to the metal resistance differential between copper and brass, the brass bar heat preferentially. The coil designed to braze the bars to the plate section heats the rods and the heat is transferred to the plate more by conduction than induction causing the bars to initially reach temperature prior to the plate. If the materials are the same (cooper to copper or brass to brass, this is not a problem. If the bar is copper and the plate is brass there are not issues – only when the bar is brass and the plate is copper. This requires the power to be reduced to allow tie for heat transfer from the brass rod to the copper plate. Results/Benefits:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
   
induction copper and brass induction brazing brass copper [wpforms id="3947"]

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.