显示标签为“inductionbrazingbrasspipe”的博文。显示所有博文

2024年3月16日星期六

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
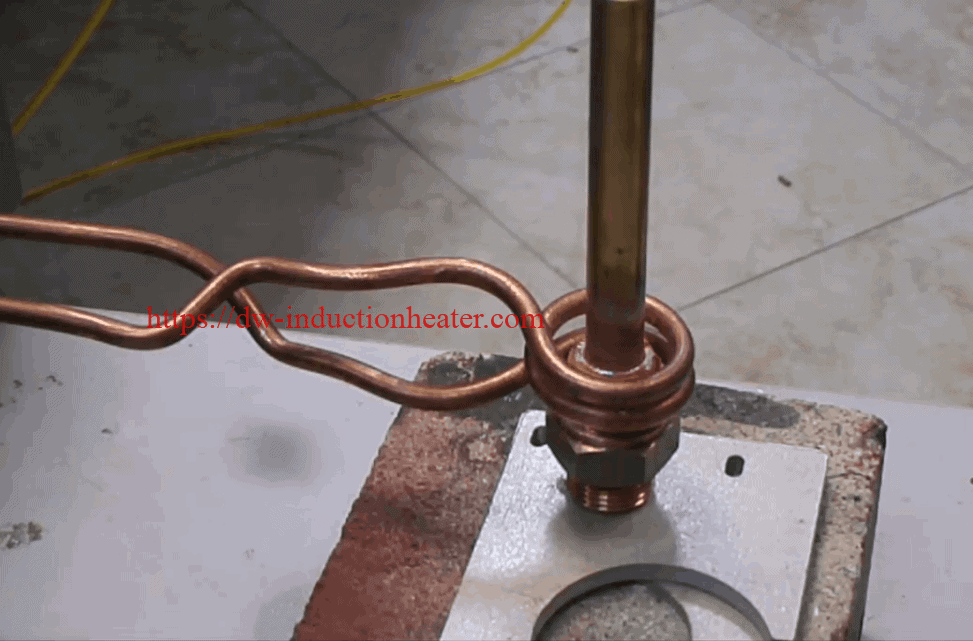
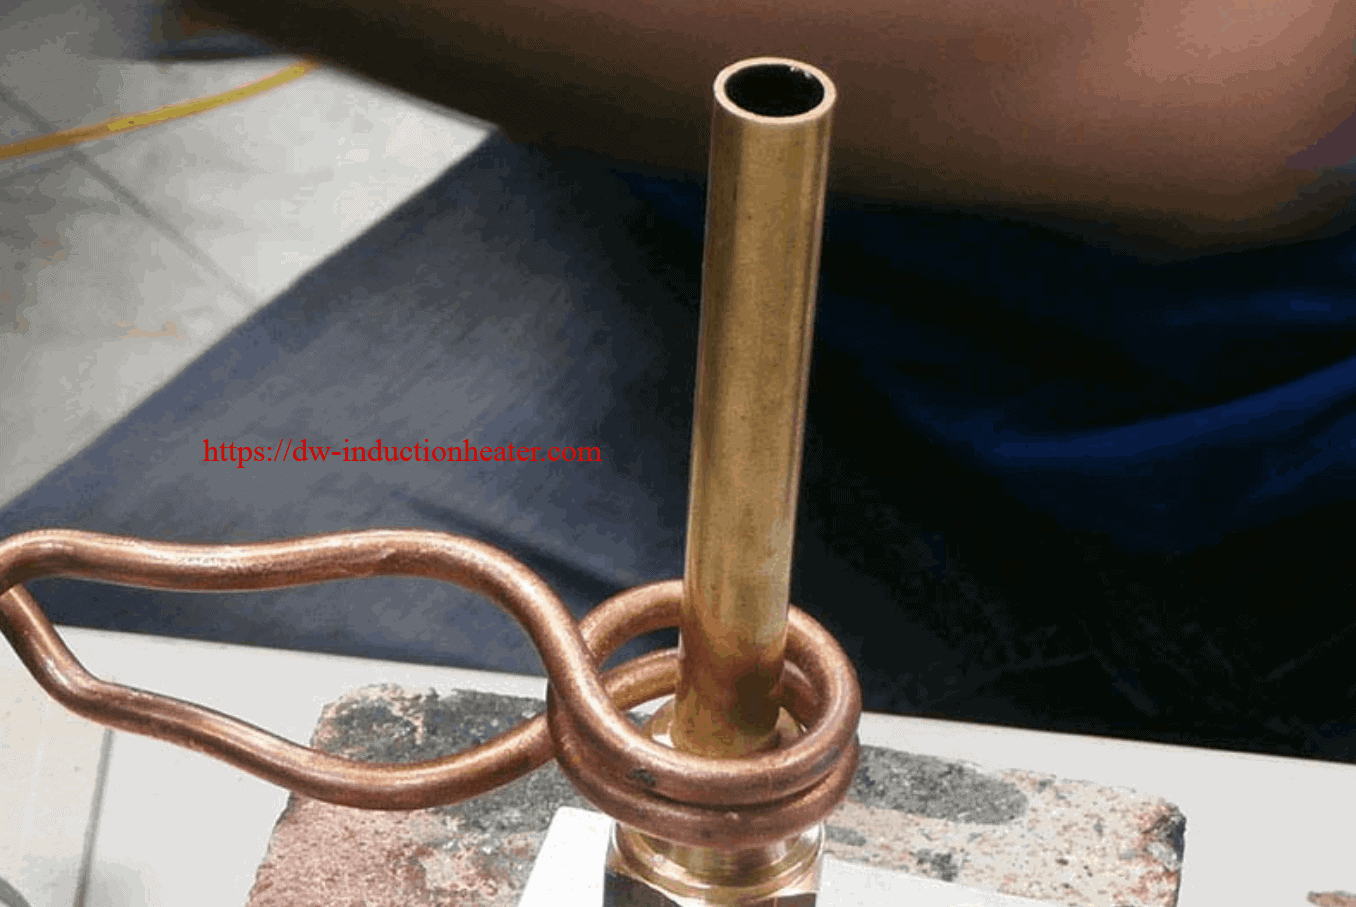
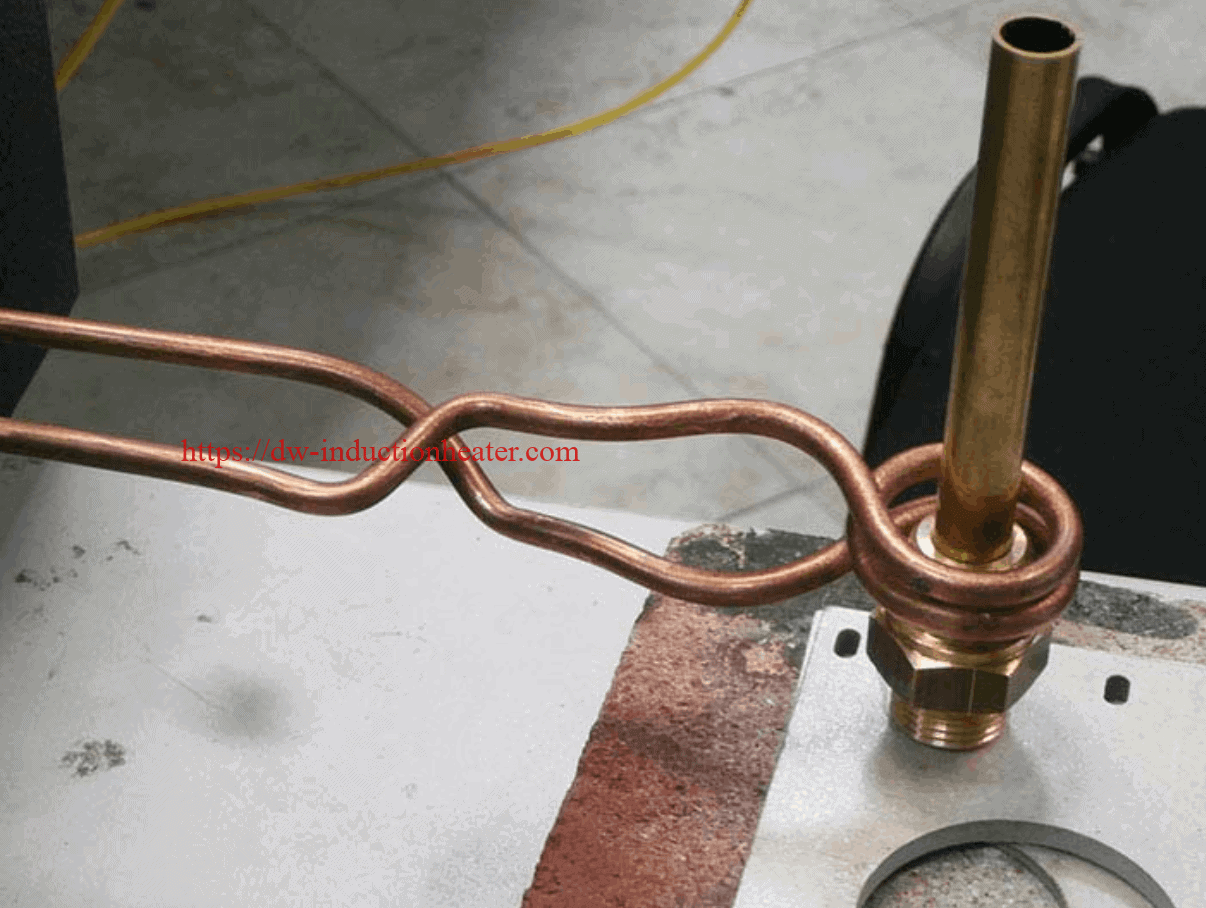
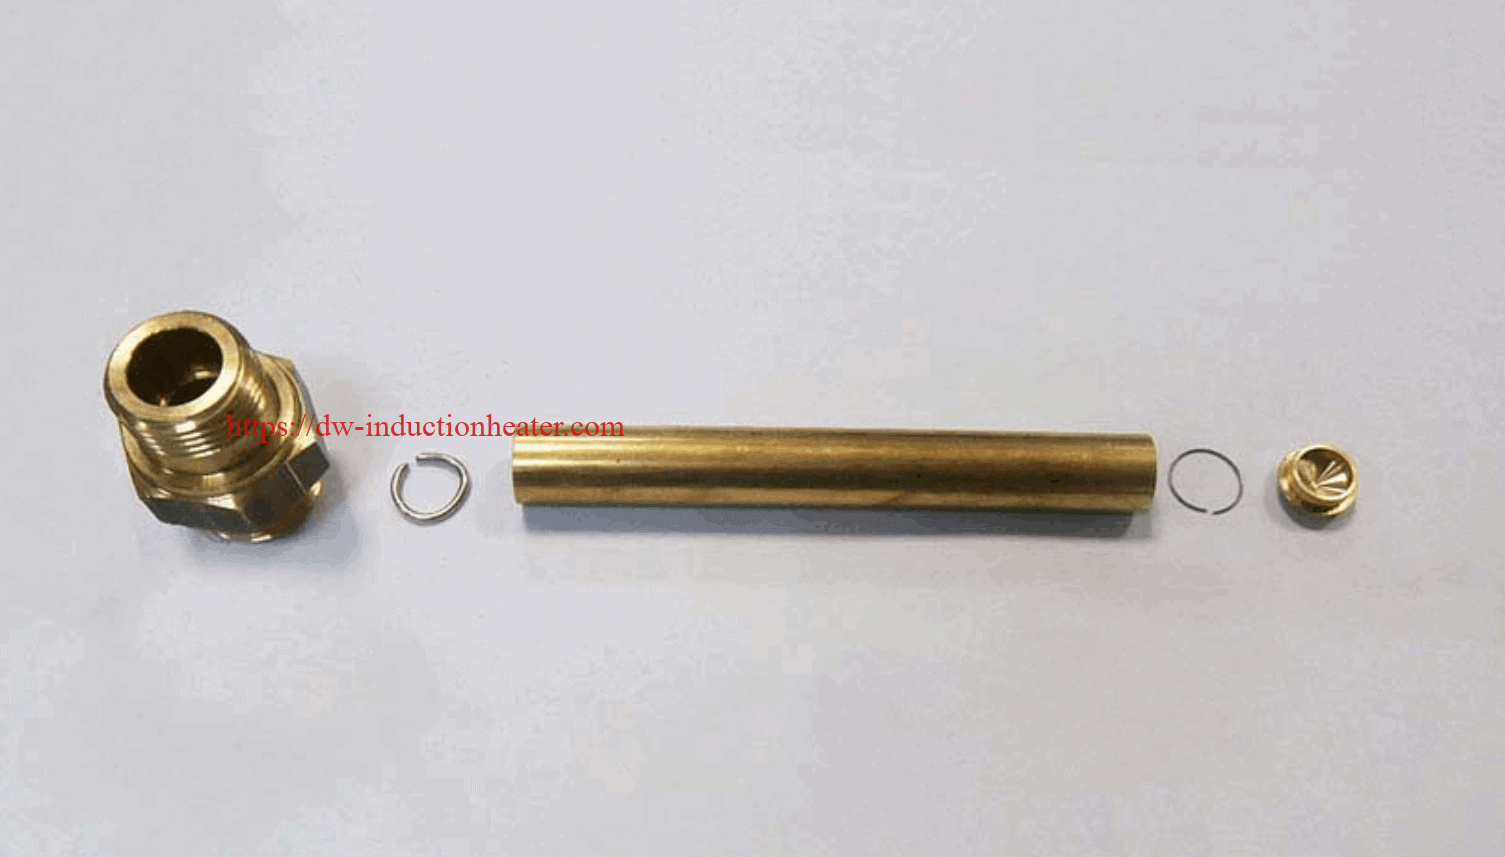
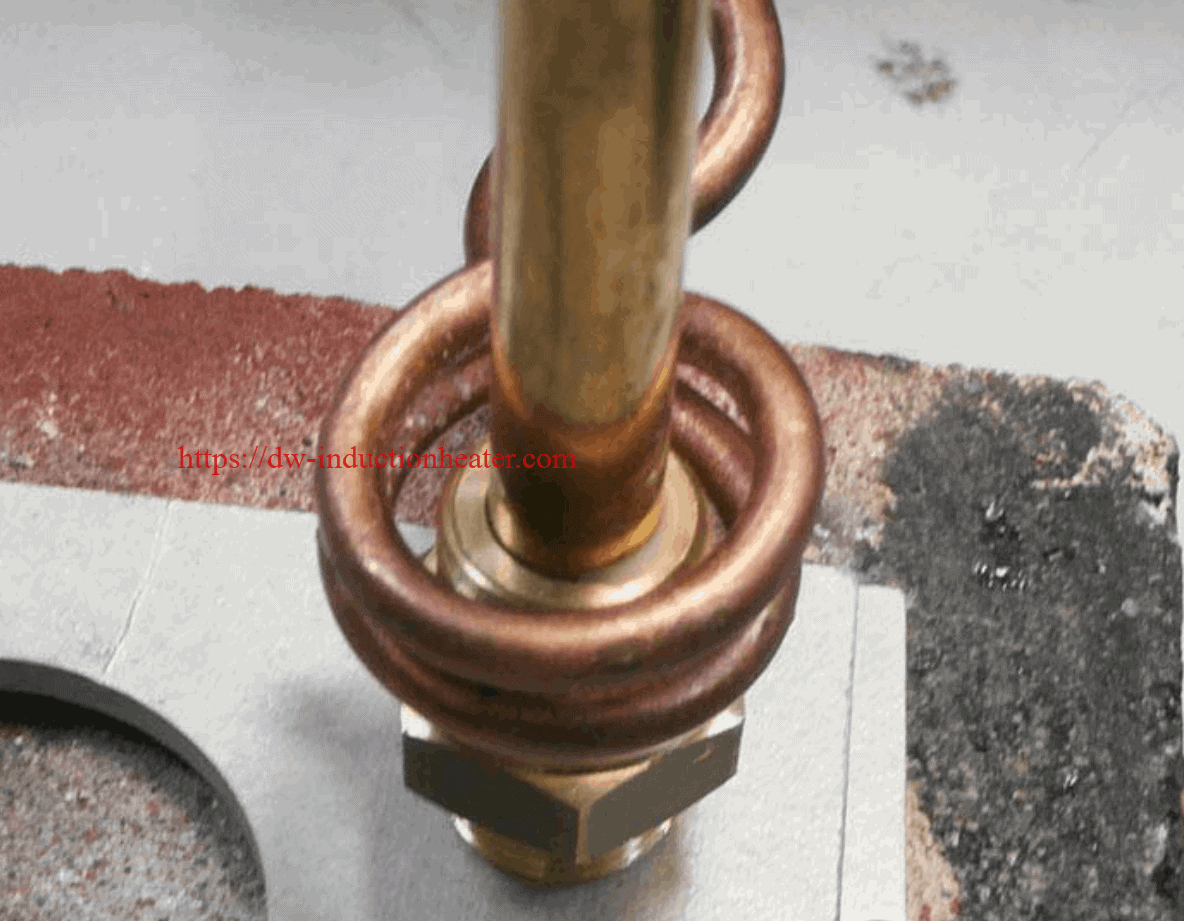
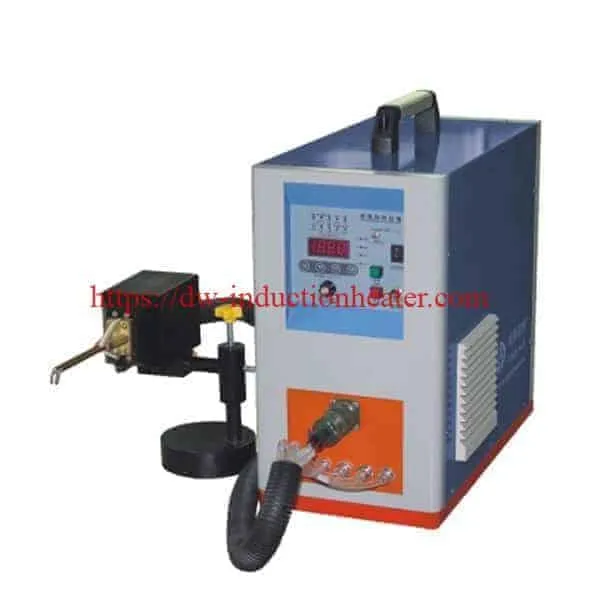
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
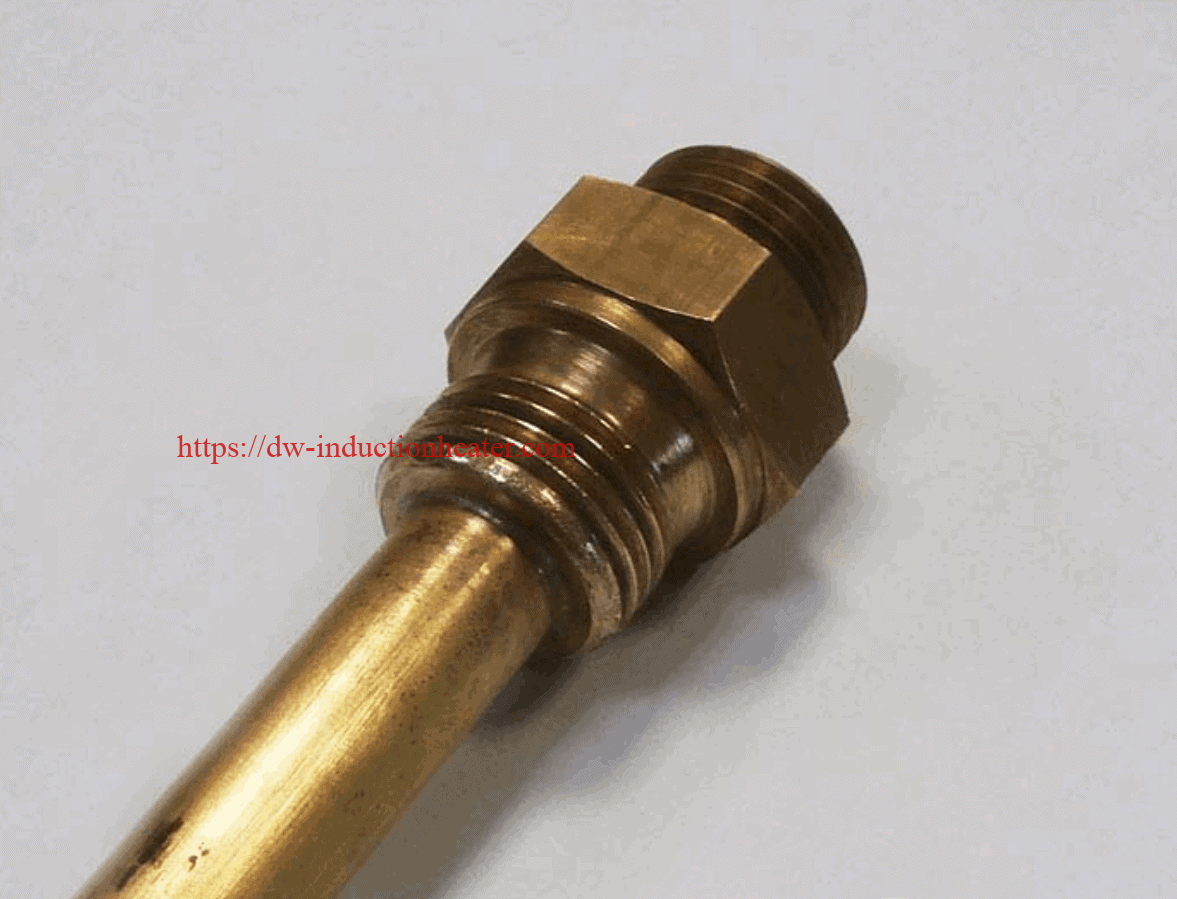
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
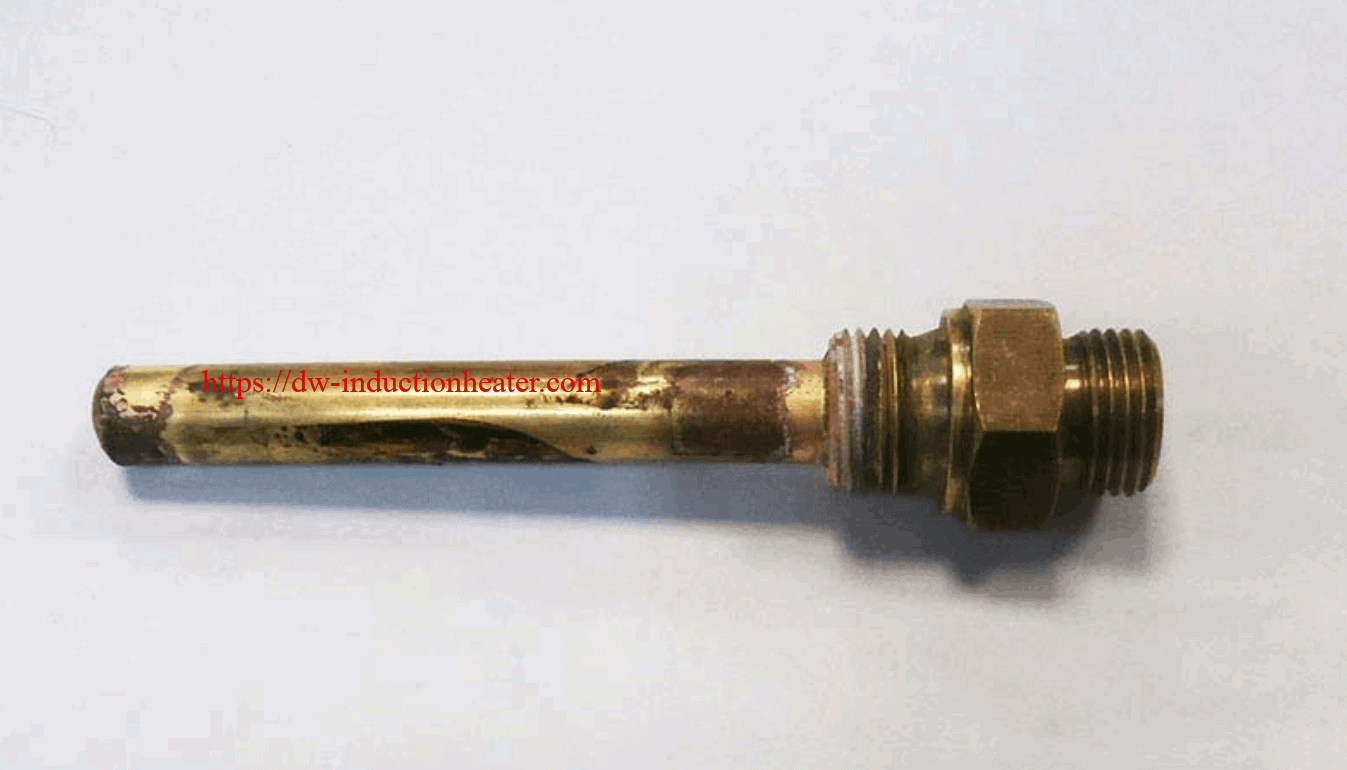
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
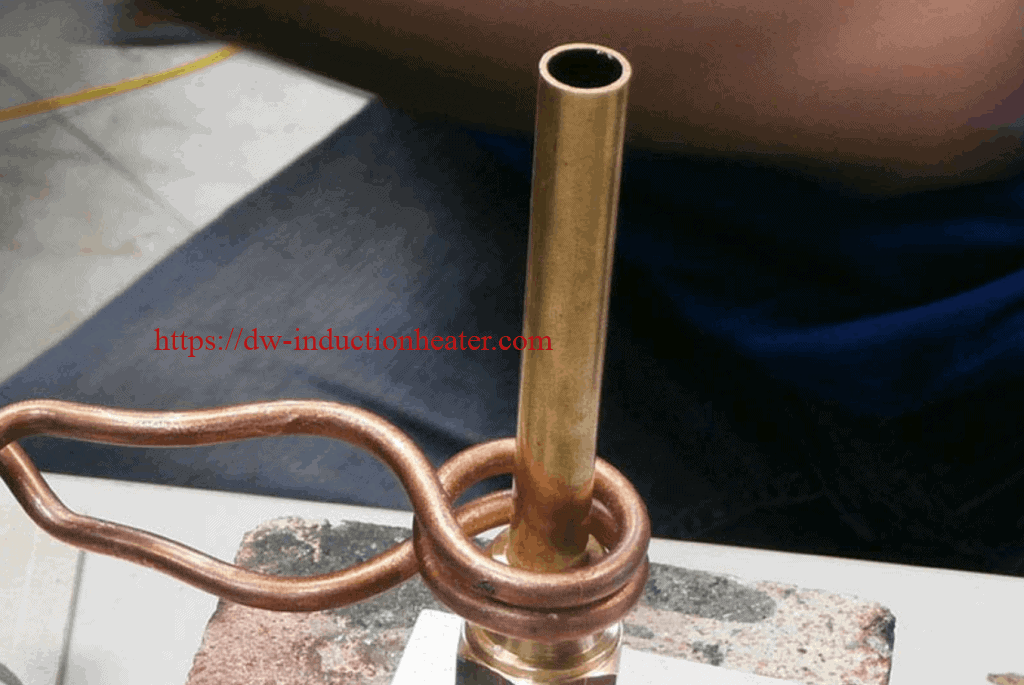
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
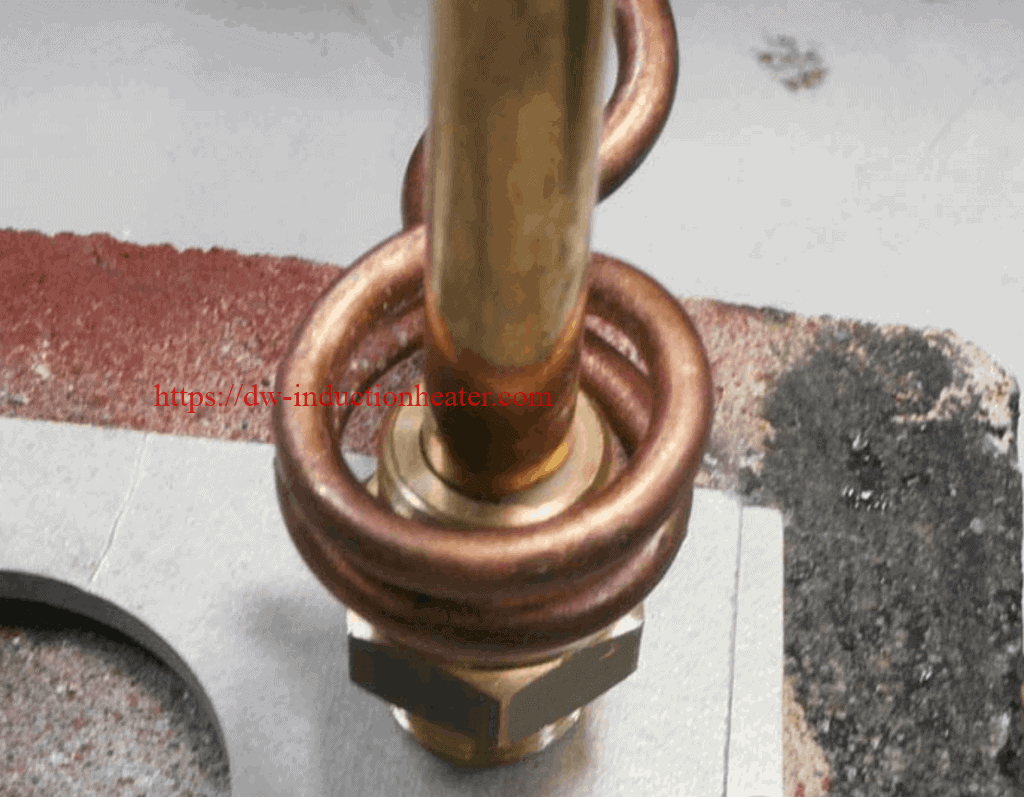
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing
https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html?feed_id=236860&_unique_id=65f555b095631

2023年11月10日星期五

Brazing Brass Fittings With Induction

Brazing Brass Fittings With Induction Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm) Material: Brass tubing Brass flange Braze rings Braze flux Temperature :1382°F (750°C) Frequency 200 kHz Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application. Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter. Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes. https://dw-inductionheater.com/brazing-brass-fittings-with-induction.html?feed_id=230496&_unique_id=654e39f56072c

2023年8月18日星期五

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
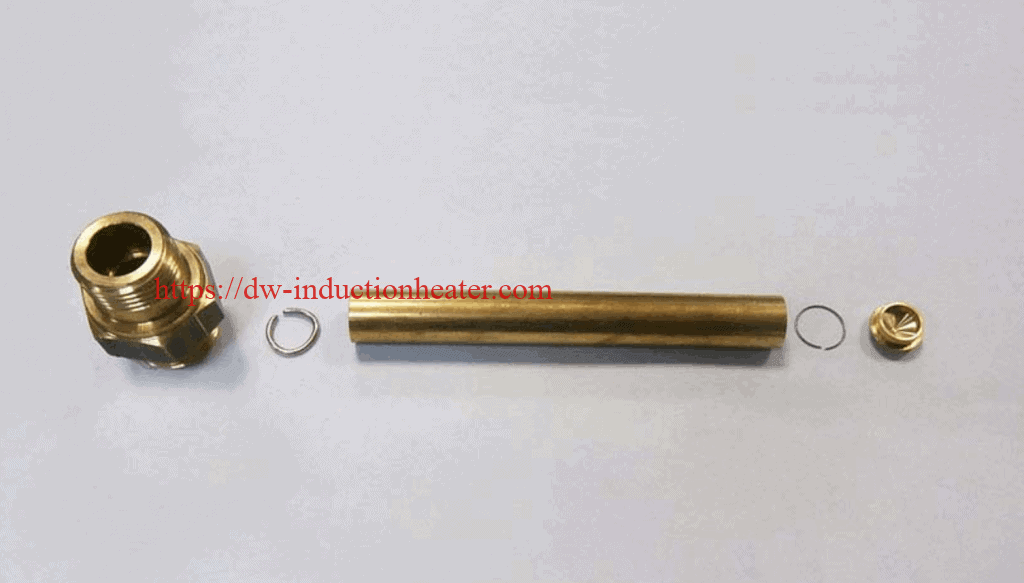
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing

2023年7月23日星期日

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing
https://dw-inductionheater.com/induction-brazing-brass-pipe-to-brass-part.html?feed_id=220186&_unique_id=64bde142a19f8

2023年7月15日星期六

Brazing Brass Fittings With Induction

Brazing Brass Fittings With Induction Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm) Material: Brass tubing Brass flange Braze rings Braze flux Temperature :1382°F (750°C) Frequency 200 kHz Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application. Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter. Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes.

2023年4月1日星期六

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing

2023年2月2日星期四

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing

2022年12月24日星期六

Brazing Brass Fittings With Induction

Brazing Brass Fittings With Induction Objective :To heat brass tubing assemblies to 750°C for a brazing application. The tubing diameter varies from 3 to 8 inches (76.2 to 203.2 mm) Material: Brass tubing Brass flange Braze rings Braze flux Temperature :1382°F (750°C) Frequency 200 kHz Equipment DW-UHF-20KW, 150-500 kHz induction heating power supply, equipped with a remote heat station containing eight 1.0 μF capacitors (total 2.0 μF). A multi-turn helical coil induction heating coil designed and developed specifically for this application. Process The parts are disassembled. All connections are cleaned and braze flux is applied to the entire surface of the assembly. Before assembling the parts an induction coil is slipped over the tube. The brass coupling is placed over the brass tubes. The flux on the parts is allowed to dry before heating. The induction heating power is applied until the braze flows well at the joint. The assembly heats well to 1382°F (750°C) and melts the braze alloy all around the tube. Heating time is several minutes depending on flange diameter. Results/Benefits The coil allows heating at the best possible efficiency which reduces the cycle time and the conducted heat along the brass tubes.

2022年11月29日星期二

induction brazing brass pipe to brass part

Objective High Frequency Induction Brazing brass pipe to brass part and a brass tip in under one minute using induction.
Equipment DW-UHF-6KW-III handheld induction brazing machine handheld inductino heater 2 turns coil Materials • Wide brass part • Brass pipe • Silver-based brazing alloy, provided by customer
Test 1 – Pipe to wide part: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 38 sec
Test 2 – Pipe to tip: Key Parameters Power: 4.4 kW Temperature: Approximately 1400° F (760° C) Time: 17 sec
Process: Test 1
  • The wide part and brass pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the induction heating coil and induction heat is applied.
  • The joint is completed in 38 seconds.
Test 2
  • The tip and pipe are assembled and a brazing alloy ring is placed between them.
  • The assembly is put inside the coil and induction heat is applied.
  • The joint is completed in 17 seconds.
Results/Benefits: Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress than welding
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer process than flame brazing

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.