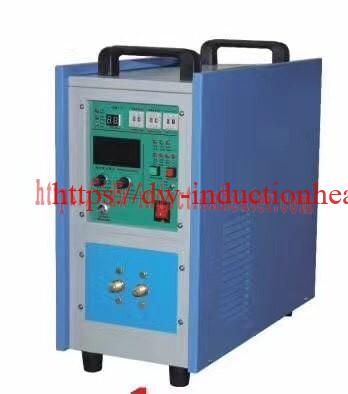
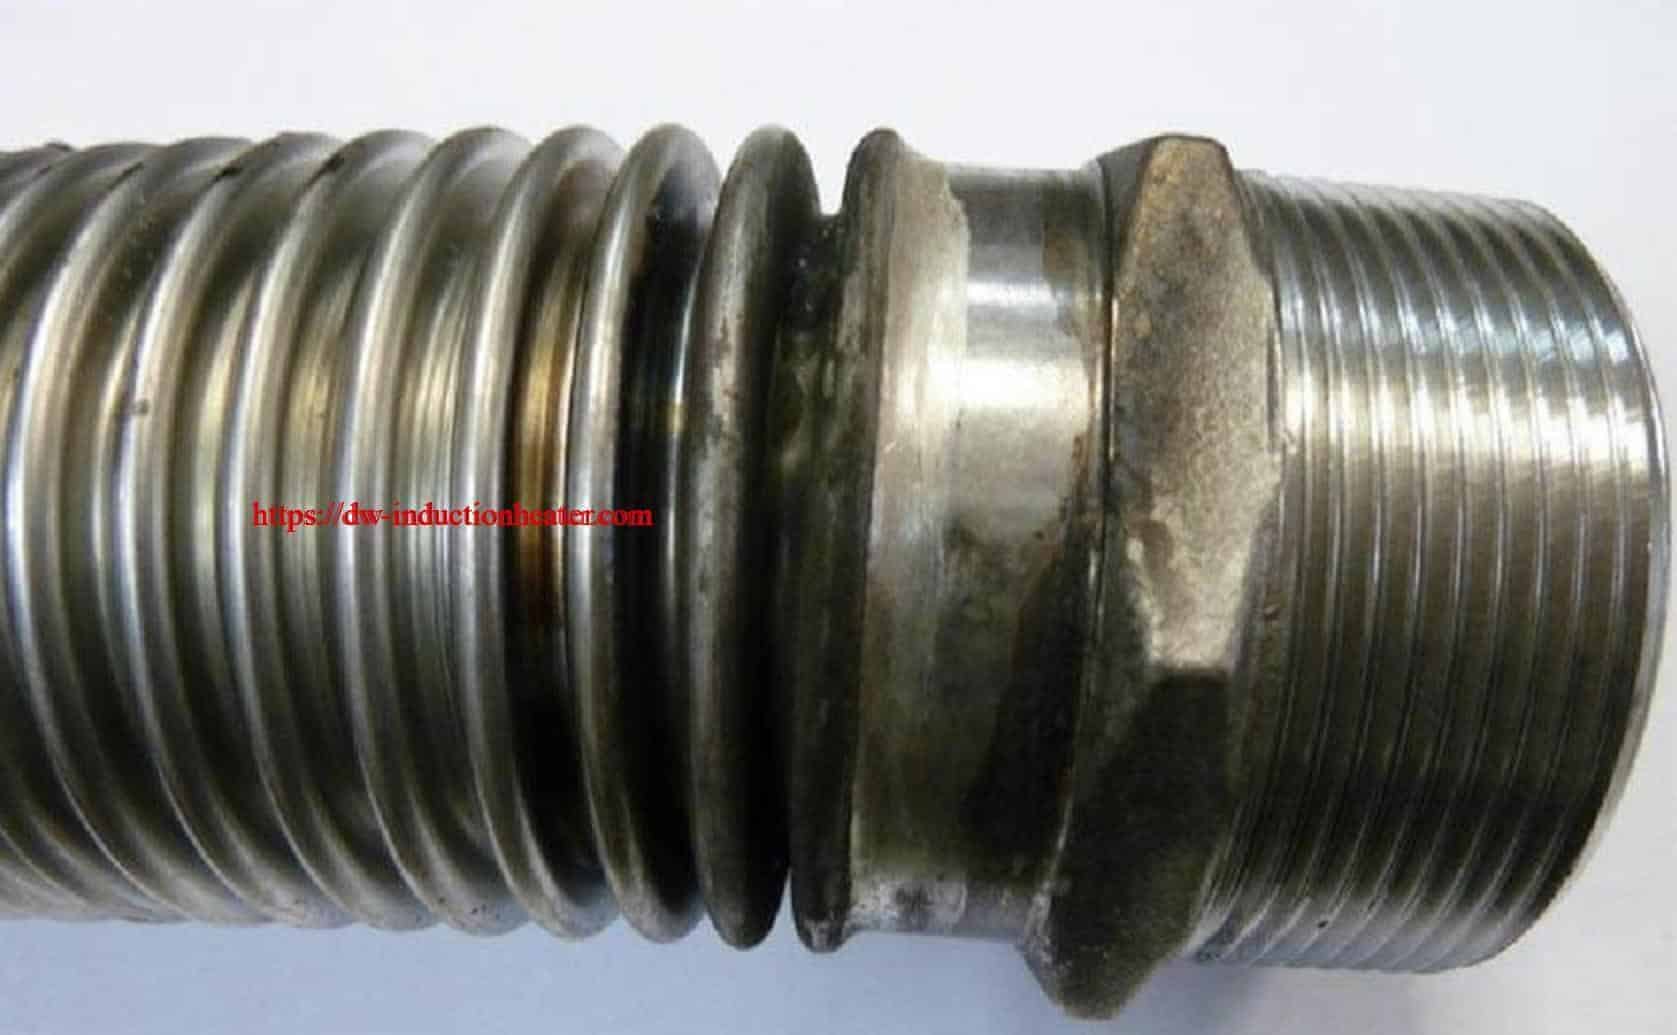
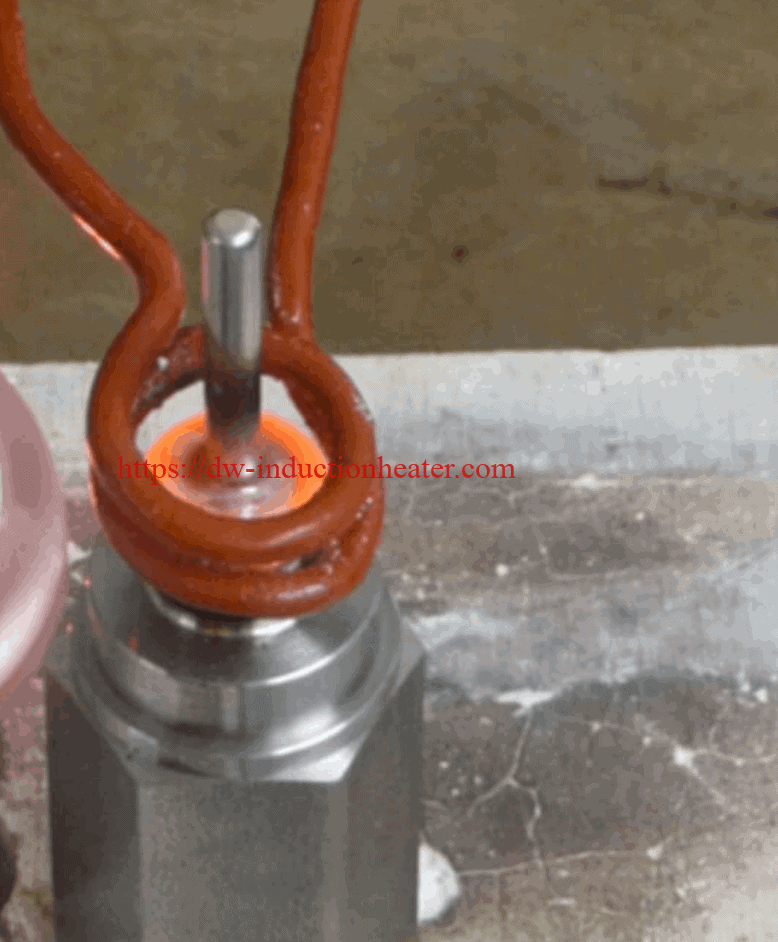
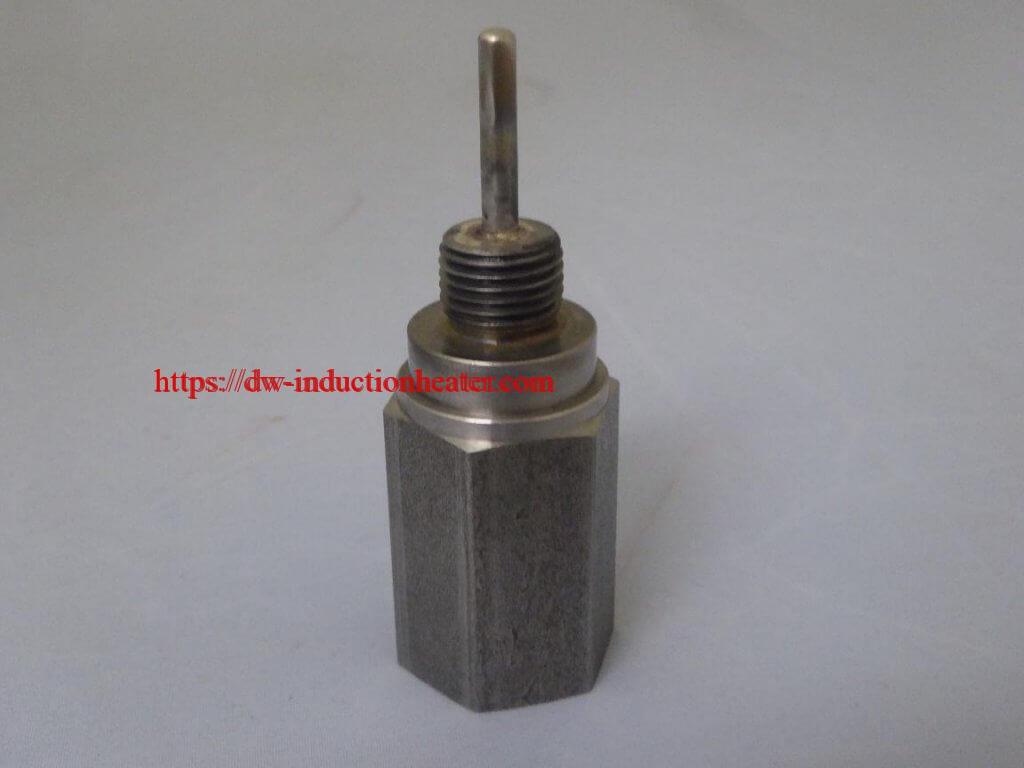
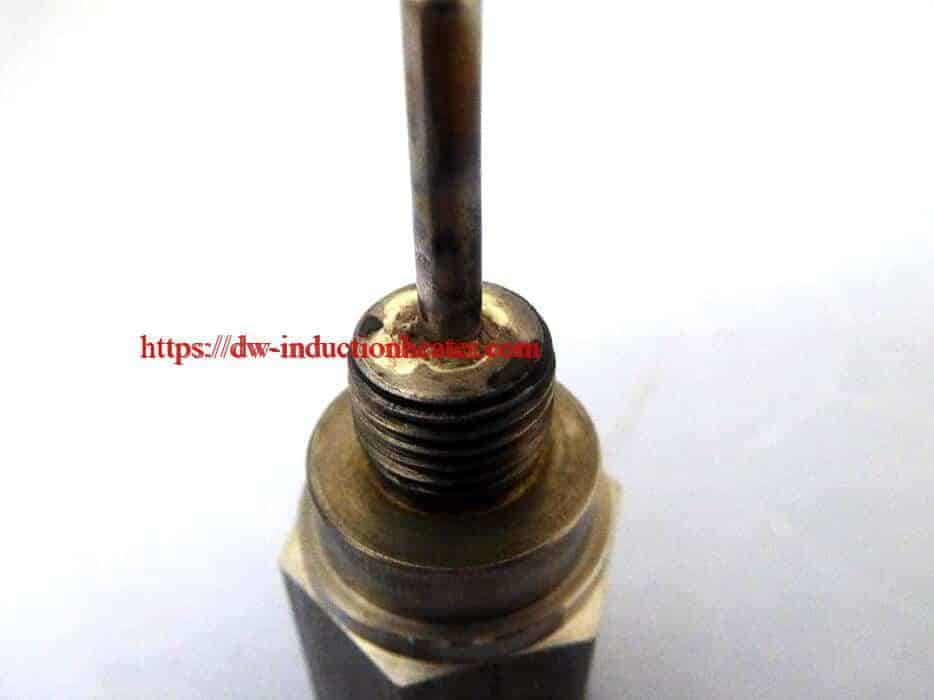
High frequency induction brazing stainless steel tube to stainless steel fitting with DW-HF-25kw-A induction heater.
Objective Brazing stainless steel tubing and stainless steel fittings Equipment DW-HF-25kw-A induction brazing machine
Materials
1.75″(44.45mm) Hexagon fitting
Power: 10.52 kW
Temperature: 1300°F (704°C)
Time: 30 seconds
Results and Conclusions:
- Induction heating pinpoints the heat to the desired area of the part
- Improved process control for precise heating to a desired temperature
- Power on demand and rapid, consistent heat cycles
- Technology without pollution, which is both clean and safe



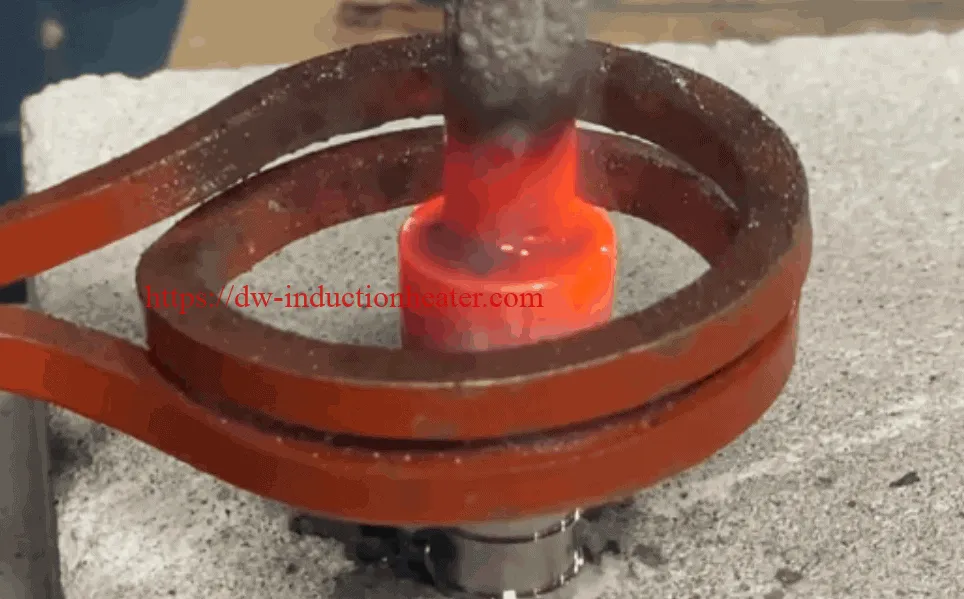
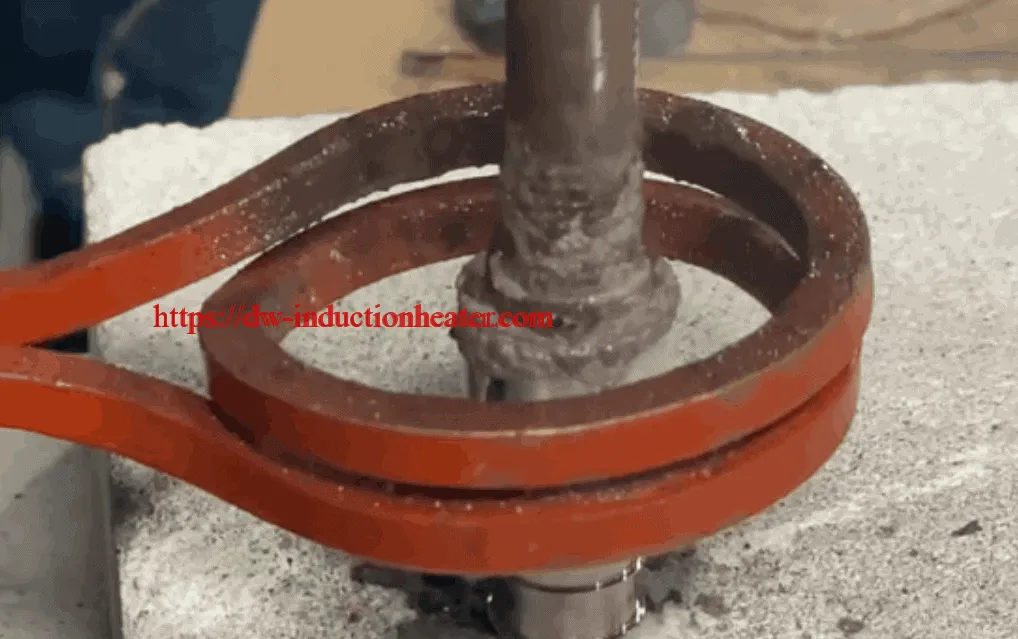
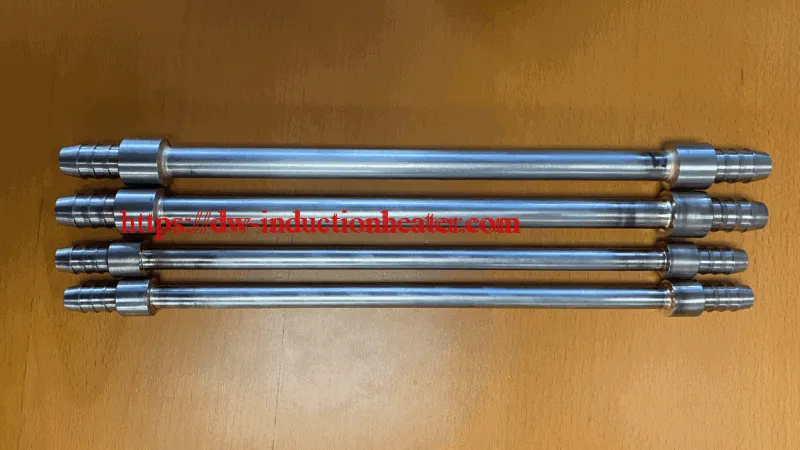
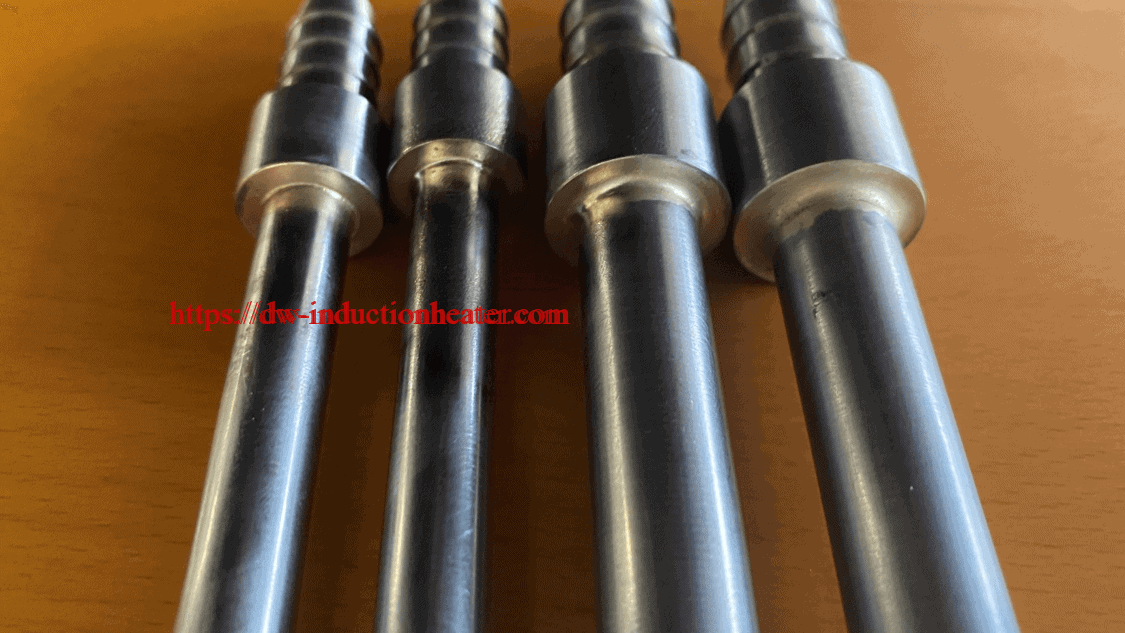

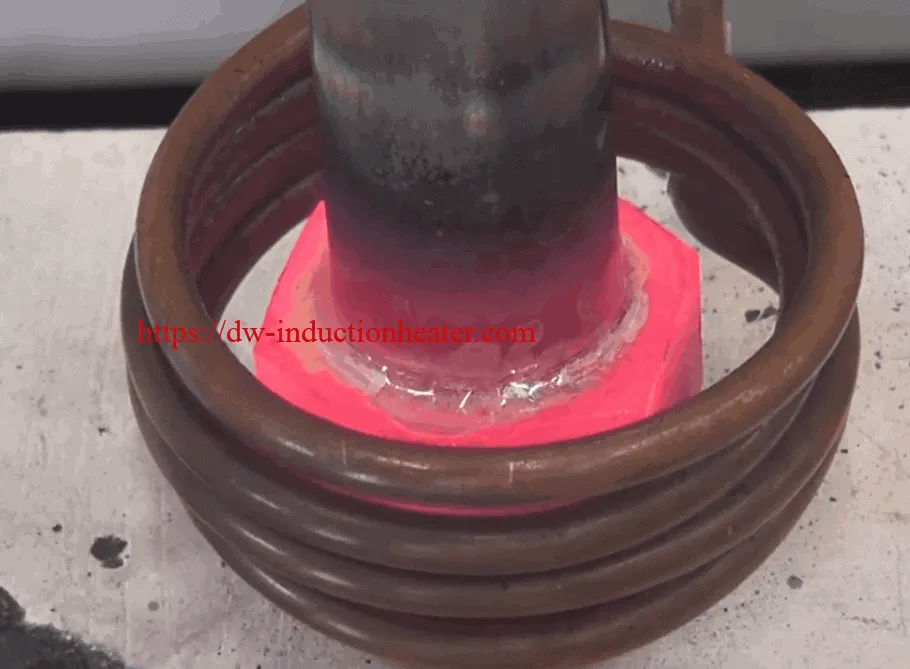



 Induction Brazing Stainless Steel Car grill
Objective Braze an end plug on a stainless steel car grill before powder coating application
Material Stainless steel car grill 0.5” x 0.19” (12.7mm x 4.8mm), end plugs and braze ring
Temperature: 1350 ºF (732°C)
Frequency:400 kHz
Equipment •DW-UHF-6kW-III induction heating system, equipped with a remote workhead containing one 0.66μF capacitor.
• An induction heating coil designed and developed specifically for this application.
Process A three turn square shaped helical coil is used to heat the end of the grill. End plugs are inserted into the grill and the assembly is inserted into the coil for 30 seconds. The braze flows to create a neat and clean leak-proof joint.
Results/Benefits Induction heating provides:
• Rapid localized heat to joint area only
• Minimized oxidation reduces cleaning time
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating
