显示标签为“stainlesssteel”的博文。显示所有博文

2024年5月19日星期日

Induction Soldering Stainless Steel Tubing

Induction Soldering Stainless Steel Tubing with IGBT Soldering Heating Units Objective Heat a.125” (3.175mm) diameter stainless steel tube to a 1” diameter cylinder 1” (25.4mm) tall for a soldering application Material Stainless steel cylinder and tube Temperature indicating paint Lead free solder preform rings Temperature 300-400 ºF (150-205 ºC) Frequency 235 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 0.66 μF capacitors (total 1.32 μF). A three-turn pancake coil induction heating coil designed and developed specifically for this application. Process Initial tests without solder ensured that the metal reaches the required temperature and the heating pattern on the part.Solder preform rings are placed onto the tube at the joint. The part is placed inside the induction-heating coil heated until the solder melts. Results/Benefits Programmable and adjustable heating ramp rates achieve the desired heat profile. Too fast a heat profile does not conduct the heat through the joint and too slow a heat cycle vaporizes or dries the flux causing poor solder flow. soldering stainless steel tubing https://dw-inductionheater.com/induction-soldering-stainless-steel-tubing.html?feed_id=246208&_unique_id=664a4eef2e83a

2024年5月15日星期三

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires https://dw-inductionheater.com/induction-soldering-stainless-steel-to-wire.html?feed_id=245732&_unique_id=66454f2a79866
2024年4月7日星期日

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

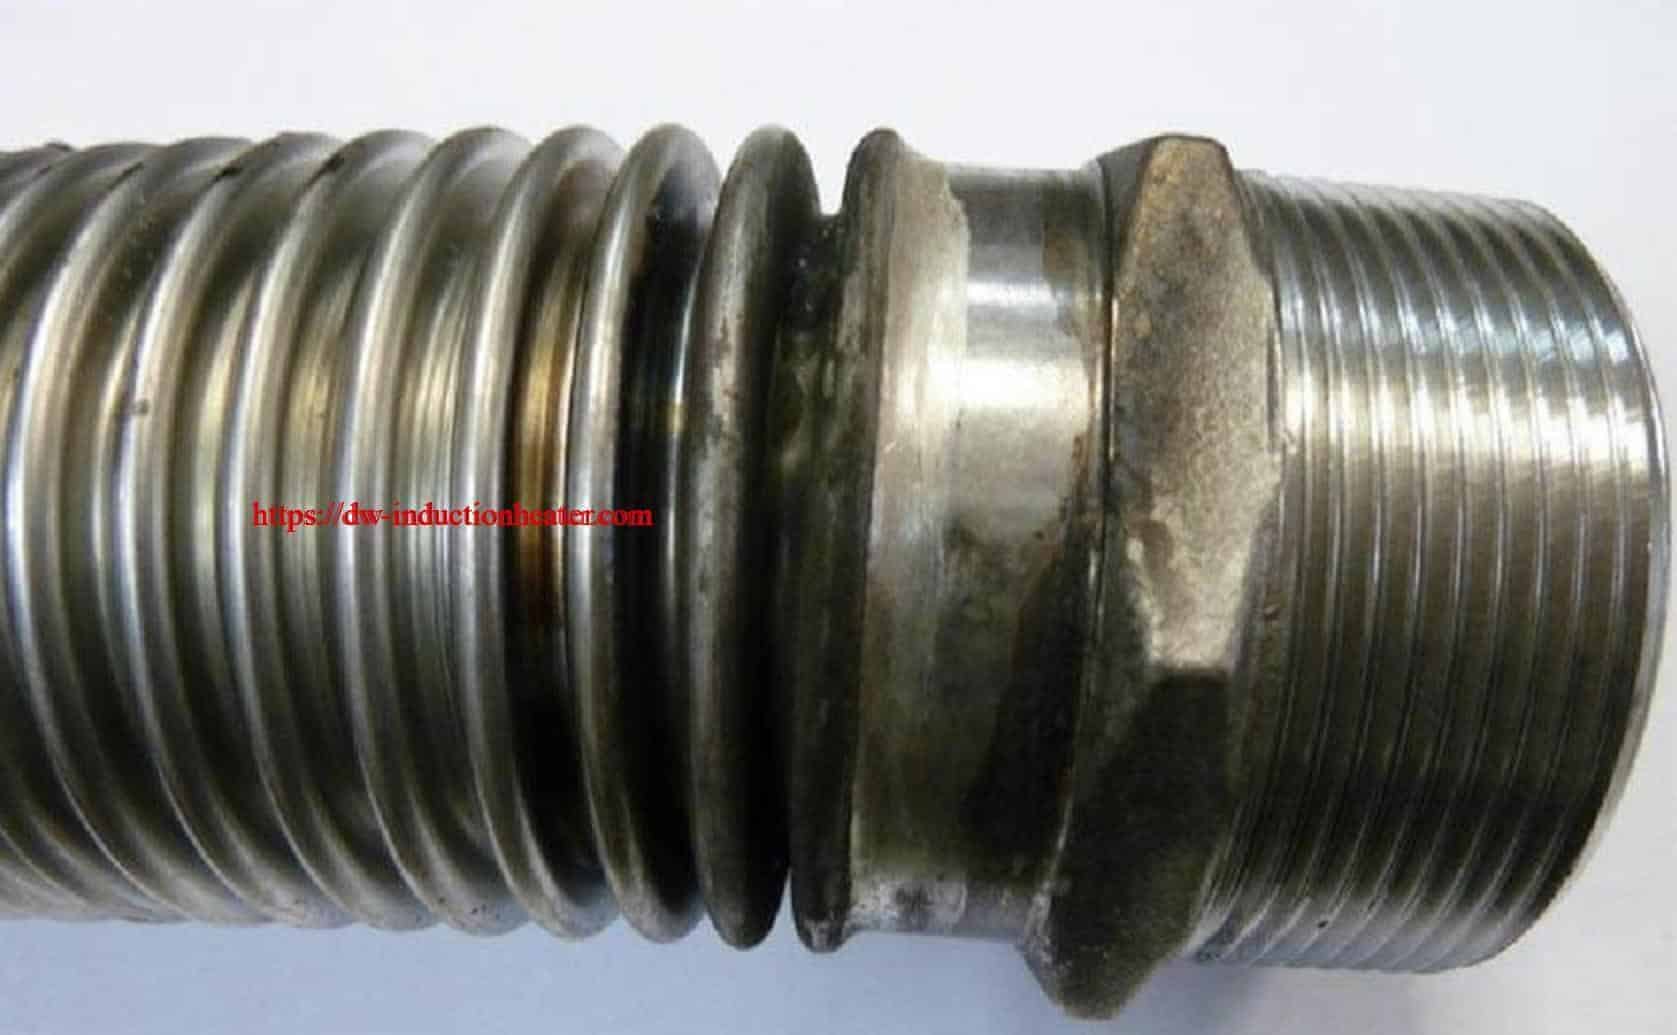
Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"] https://dw-inductionheater.com/high-frequency-brazing-stainless-steel-fittings-machine.html?feed_id=240466&_unique_id=66129ba5d669a

2023年9月29日星期五

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires
2023年9月23日星期六

Induction Soldering Stainless Steel To Wire

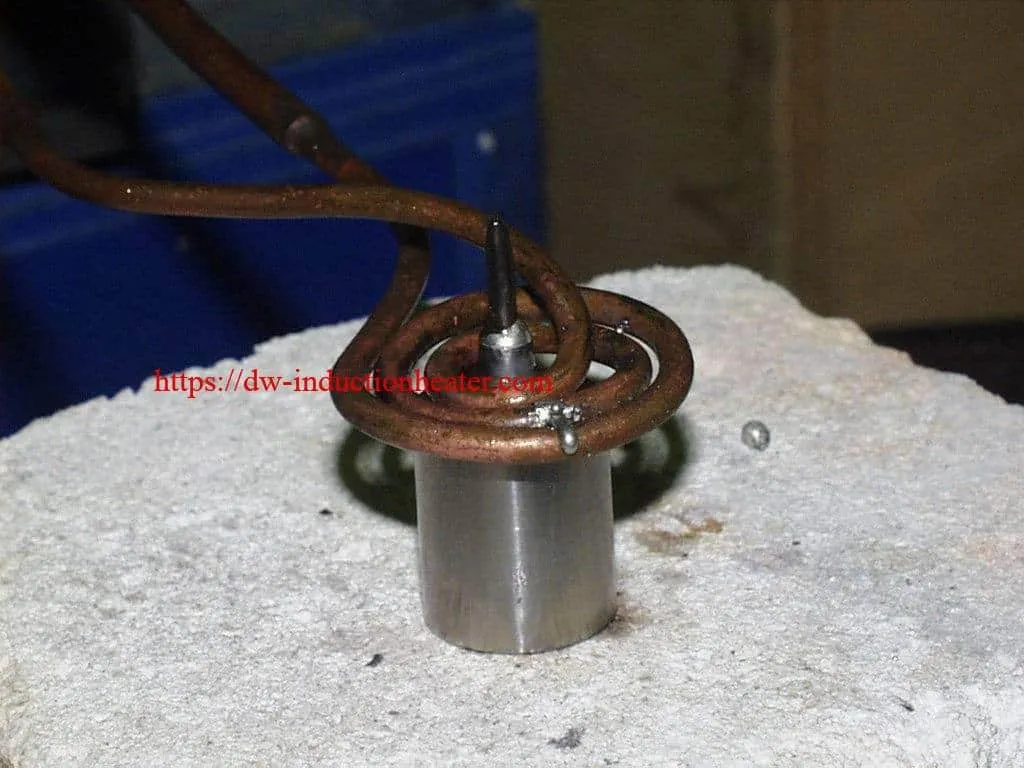
Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires https://dw-inductionheater.com/induction-soldering-stainless-steel-to-wire.html?feed_id=227771&_unique_id=650eabb6a2db5
2023年8月15日星期二

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"] https://dw-inductionheater.com/high-frequency-brazing-stainless-steel-fittings-machine.html?feed_id=223336&_unique_id=64dbf151f27e9

2023年6月27日星期二

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"]

2023年6月24日星期六

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"]

2023年6月23日星期五

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires

2023年6月14日星期三

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"]

2023年5月30日星期二

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings

Objective High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints. Induction Brazing stainless steel Equipment DW-UHF-10KW induction brazing machine Materials • Flexible metal hose • Ag45Sn brazing alloy
Test 1 Key Parameters Flexible metal hose with ID 1.575in (40mm) Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 7kW Time: 28seconds
Test 2 Key Parameters Flexible metal hose with ID 2.913in (74mm) Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn Temperature: approximately 1382°F (750°C) Power: Pre-curie – 8 kW Time: 1 minute 20 seconds
Process:
  1. Hose and fittings are prepared with borax flux paste in the surface area.
  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.
  3. The hose and the fittings are placed into the coil.
  4. Induction heating is applied to the area until the braze is completed.
Results/Benefits:
  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.
  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.
  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.
Induction heating provides:
  • Strong durable joints
  • Selective and precise heat zone, resulting in less part distortion and joint stress
  • Less oxidation
  • Faster heating cycles
  • More consistent results and suitability for large volume production, without the need for batch processing
  • Safer than flame brazing
Induction Brazing stainless steel Induction Brazing stainless steel
  [wpforms id="3947"]

2023年5月14日星期日

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires

2023年4月10日星期一

Induction Soldering Stainless Steel Tubing

Induction Soldering Stainless Steel Tubing with IGBT Soldering Heating Units Objective Heat a.125” (3.175mm) diameter stainless steel tube to a 1” diameter cylinder 1” (25.4mm) tall for a soldering application Material Stainless steel cylinder and tube Temperature indicating paint Lead free solder preform rings Temperature 300-400 ºF (150-205 ºC) Frequency 235 kHz Equipment DW-UHF-4.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 0.66 μF capacitors (total 1.32 μF). A three-turn pancake coil induction heating coil designed and developed specifically for this application. Process Initial tests without solder ensured that the metal reaches the required temperature and the heating pattern on the part.Solder preform rings are placed onto the tube at the joint. The part is placed inside the induction-heating coil heated until the solder melts. Results/Benefits Programmable and adjustable heating ramp rates achieve the desired heat profile. Too fast a heat profile does not conduct the heat through the joint and too slow a heat cycle vaporizes or dries the flux causing poor solder flow. soldering stainless steel tubing

2023年3月13日星期一

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires

2023年3月2日星期四

Induction Soldering Stainless Steel Tubing

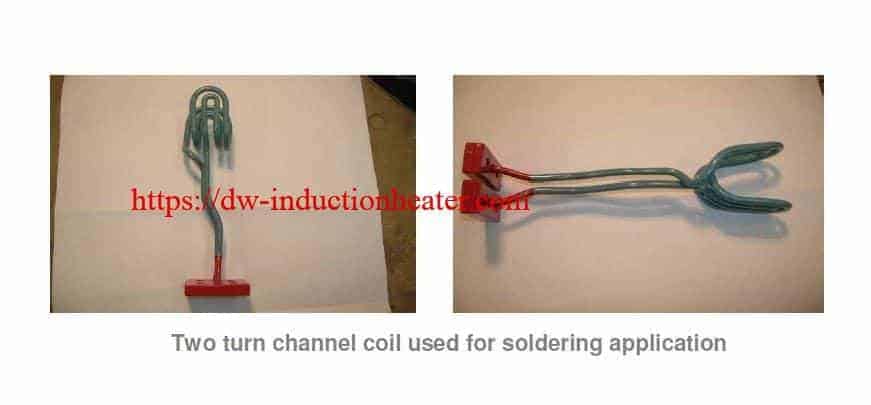
Induction Soldering Stainless Steel Tubing with IGBT Soldering Heating Units

Objective Heat a.125” (3.175mm) diameter stainless steel tube to a 1” diameter cylinder 1” (25.4mm) tall for a soldering application
Material Stainless steel cylinder and tube
Temperature indicating paint
Lead free solder preform rings
Temperature 300-400 ºF (150-205 ºC)
Frequency 235 kHz
Equipment DW-UHF-4.5 kW, 150-400 kHz induction power supply, equipped with a remote heat station containing two 0.66 μF capacitors (total 1.32 μF).
A three-turn pancake coil induction heating coil designed and developed specifically for this application.
Process Initial tests without solder ensured that the metal reaches the required temperature and the heating pattern on the part.Solder preform rings are placed onto the tube at the joint. The part is placed inside the induction-heating coil heated until the solder melts.
Results/Benefits Programmable and adjustable heating ramp rates achieve the desired heat profile. Too fast a heat profile does not conduct the heat through the joint and too slow a heat cycle vaporizes
or dries the flux causing poor solder flow.

soldering stainless steel tubing

2023年2月25日星期六

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires

2023年2月23日星期四

High Frequency Brazing Stainless Steel Fittings

High Frequency Brazing Stainless Steel Fittings


Objective
High Frequency Brazing stainless steel fittings to corogated (SS) hoses. The hoses are with sizes ID 1.575in (40mm) and ID 2.99in (76 mm).  The customer has never used induction heating before and is not familiar with the induction process. The goal of this test is to prove the strength of the joints.

Induction Brazing stainless steel

Equipment


DW-UHF-10KW induction brazing machine

Materials
•
Flexible metal hose
• Ag45Sn brazing alloy


Test 1
Key Parameters
Flexible metal hose with ID 1.575in (40mm)
Equipment: DW-UHF-10KW induction brazing heater, custom coil – ID 1.654in (42mm), 1 turn
Temperature: approximately 1382°F (750°C)
Power: Pre-curie – 7kW
Time: 28seconds


Test 2
Key Parameters
Flexible metal hose with ID 2.913in (74mm)
Equipment: DW-UHF-10kw induction brazing heater, custom coil – ID 2.992in (76mm), 1 turn
Temperature: approximately 1382°F (750°C)
Power: Pre-curie – 8 kW
Time: 1 minute 20 seconds


Process:

  1. Hose and fittings are prepared with borax flux paste in the surface area.

  2. Brazing rod is prepared in form of a ring fitting around the diameter of the joint.

  3. The hose and the fittings are placed into the coil.

  4. Induction heating is applied to the area until the braze is completed.


Results/Benefits:

  1. Power supply DW-UHF-10KW induction brazing machine meets the requirements for this process.

  2. For better performance for bigger diameter joints, we recommend power supply DW-UHF-10KW  induction brazing heater.A special custom coil can be designed as well.

  3. For the tests, static induction was used (see video), but flexible leads and coil or our DW-UHF series are also recommended.


Induction heating provides:

  • Strong durable joints

  • Selective and precise heat zone, resulting in less part distortion and joint stress

  • Less oxidation

  • Faster heating cycles

  • More consistent results and suitability for large volume production, without the need for batch processing

  • Safer than flame brazing


Induction Brazing stainless steel Induction Brazing stainless steel


[wpforms id="3947"]

2023年2月11日星期六

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units

Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing
Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder
Temperature 392 ºF (200 ºC)
Frequency 352 kHz
Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor.
• An induction heating coil designed and developed specifically for this application.
Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to
fill just the top of the connector.
Results/Benefits Induction heating provides:
• By precisely heating the metal, the plastic shroud is not directly heated
• Reduced production cost
• Faster process time, reduced production cost
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating

induction soldering coil


soldering stainless steel to wires

2022年12月24日星期六

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires
2022年11月8日星期二

Induction Soldering Stainless Steel To Wire

Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder Temperature 392 ºF (200 ºC) Frequency 352 kHz Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor. • An induction heating coil designed and developed specifically for this application. Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to fill just the top of the connector. Results/Benefits Induction heating provides: • By precisely heating the metal, the plastic shroud is not directly heated • Reduced production cost • Faster process time, reduced production cost • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating induction soldering coil         soldering stainless steel to wires

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.