2023年2月25日星期六
Brazing Steel To Steel Pipe With Induction
Brazing Steel To Steel Pipe With Induction
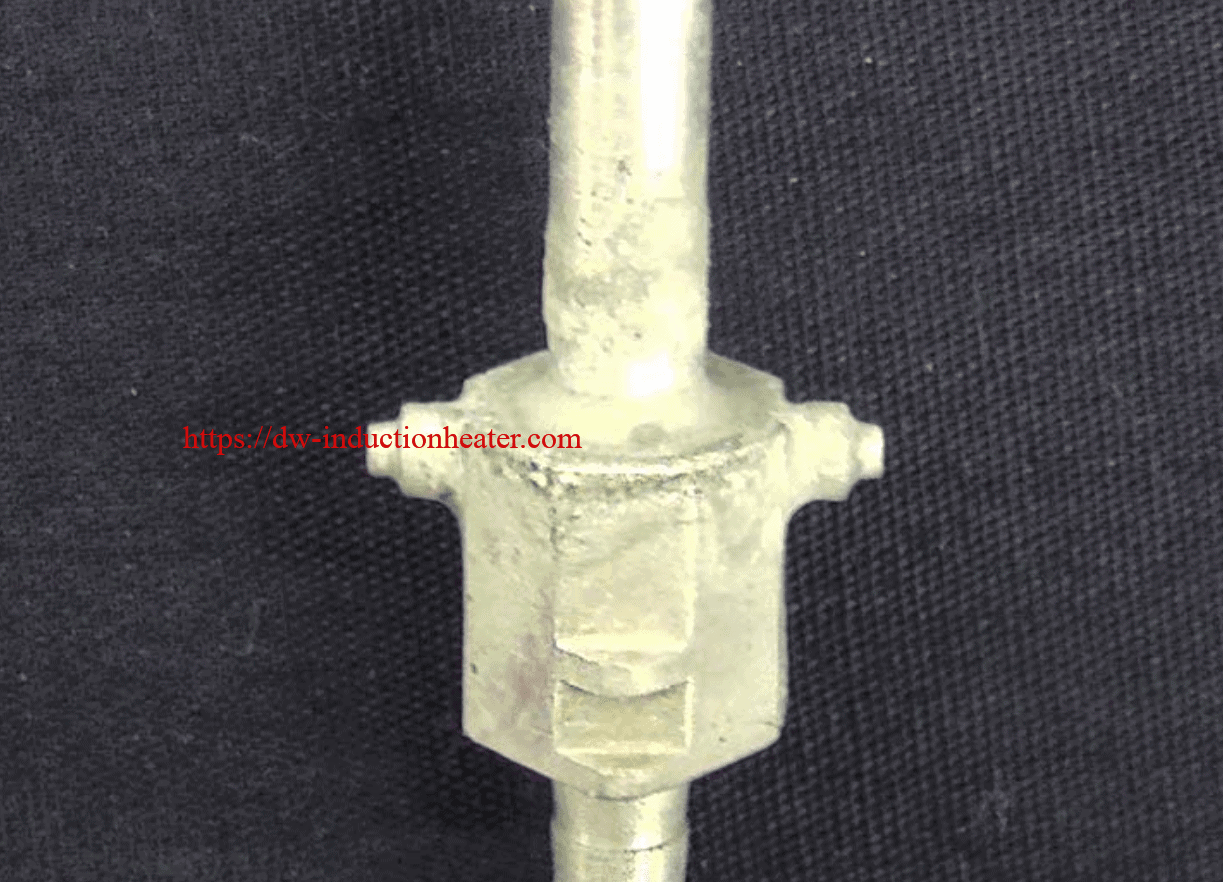
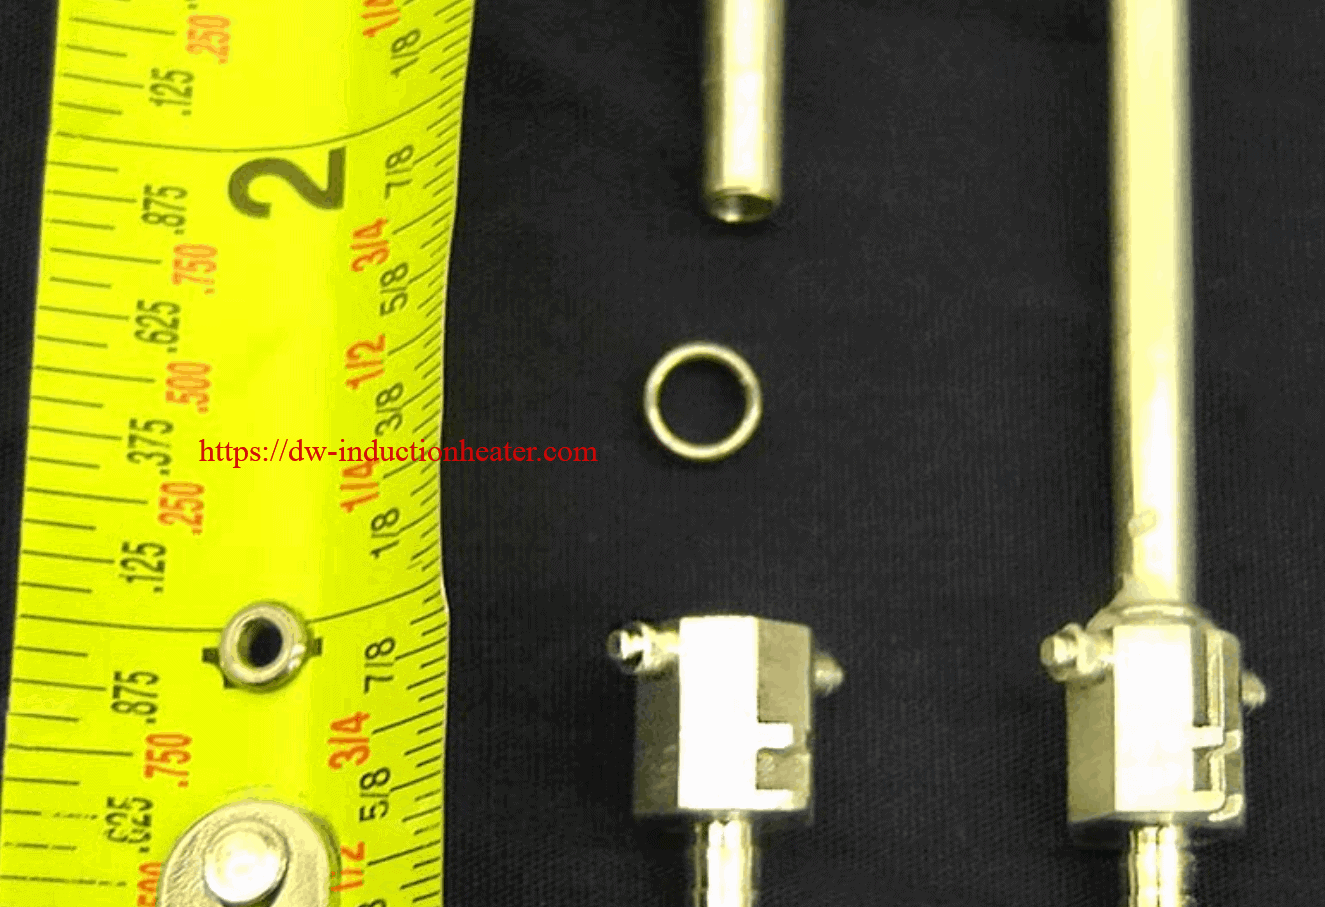
Objective: To braze O-ring Face (ORFS) sleeve or male connector to a steel tube.
Material
• Steel tube, 1 inch (2.54 cm) OD
• O-ring Face Seal sleeve and a male connector fittings
• Preform braze rings
• White SureFlow flux
• Steel support mandrel
Temperature 1300 ºF (704 ºC)
Frequency 200 kHz
Equipment
• DW-UHF-20KW induction heating system, equipped with a remote workhead containing two (2) 1.5 μF capacitors (for a total of 0.75 μF).
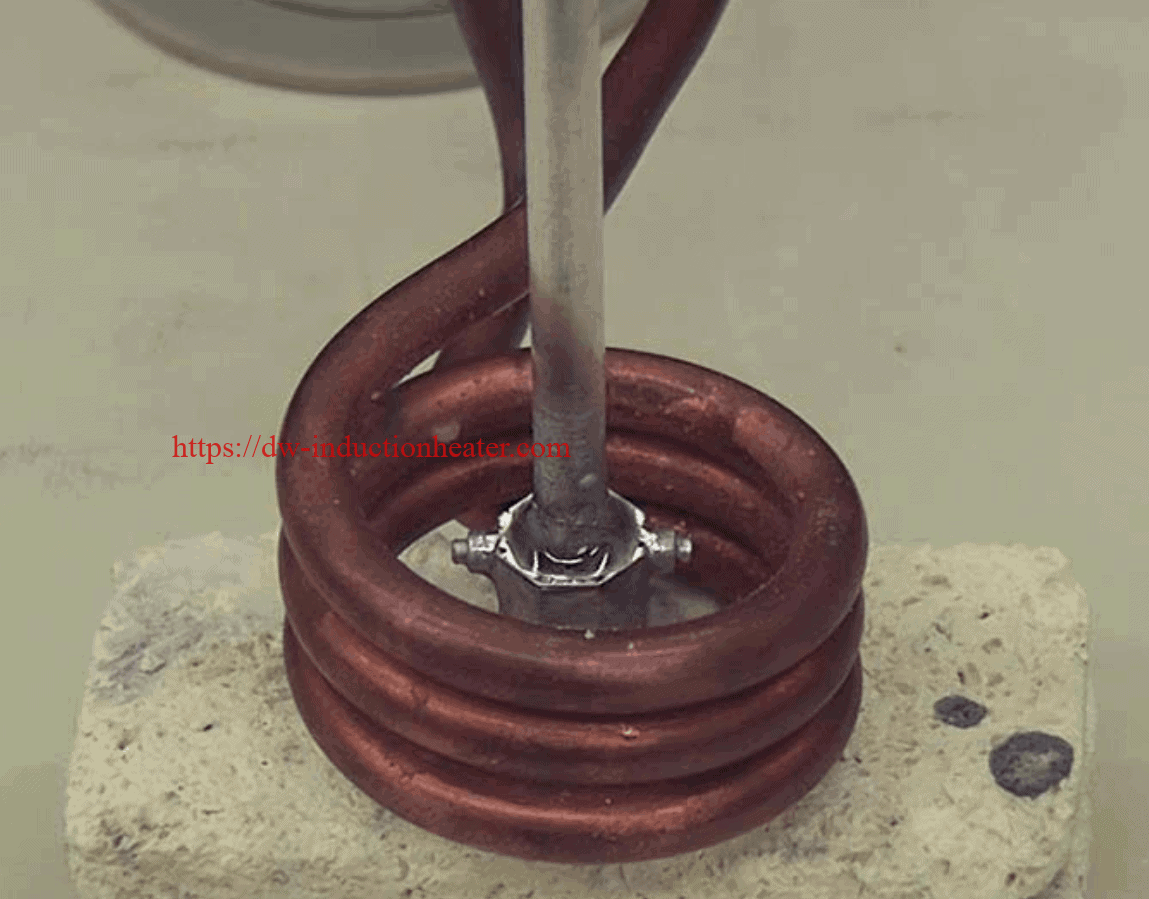
• An induction heating coil designed and developed specifically for this application.
Process A four-turn 2.75 inch (7.0 cm) ID helical coil is used for heating both the steel tube and the ORFS sleeve or the ORFS male connector. This coil is designed to braze either the sleeve or male connector to the tube. The parts to be brazed are assembled with flux and heated for 45 seconds. Pressure is applied to the tube to make sure it is inserted fully into the fittings as the braze ring flows.
Results/Benefits Advantages :
• Large Inner diameter of coil allows for easy loading and unloading of parts
• With efficient energy coupling of the coil to the fittings overheating is avoided.

Brazing Copper Tube with Induction
Brazing Copper Tube with Induction
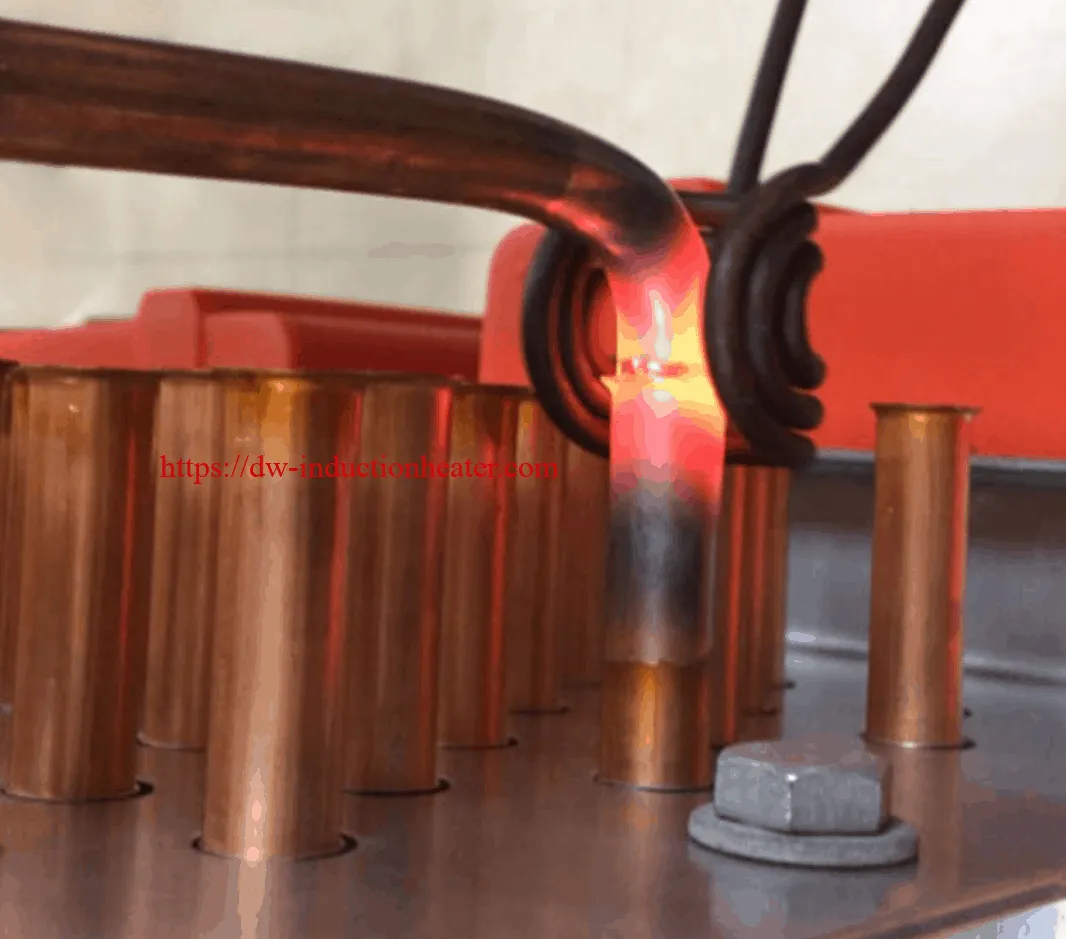
Objective: To braze a copper tube ( 3/8" OD by 2-4" long) into a 3/8" fitting in less than 10 seconds. Heating must take place in a channel type coil to allow for easy loading of parts.
Material Copper Tubing and Fitting with Braze and Stay Silv White Flux
Temperature 1300°F
Frequency 215 kHz
Equipment DW-UHF-10kw output solid state induction power supply equipped with a standard heat station containing eight 0.33 μF capacitors for a total of 0.66μF, a step down transformer, and a specifically designed induction heating coil.
Process DW-UHF-10kw solid state induction power supply was setup to achieve the following results: · 2.0 kW of power was directly loaded into the copper tube resulting in a heating time of 7.2 seconds to reach the necessary 13000F for brazing.
Results& Processing ease was achieved through the design of a unique channel type coil comprised of three turns of 1/8" copper.
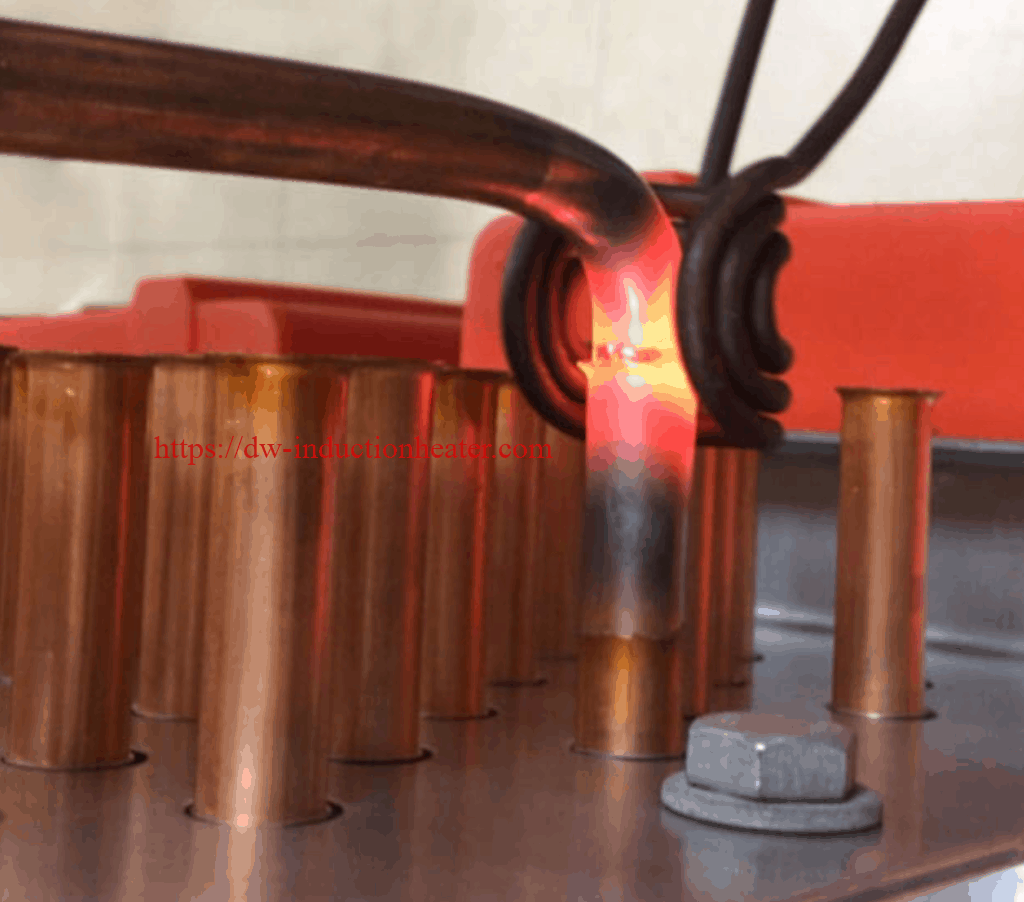
Objective: To braze a copper tube ( 3/8" OD by 2-4" long) into a 3/8" fitting in less than 10 seconds. Heating must take place in a channel type coil to allow for easy loading of parts.
Material Copper Tubing and Fitting with Braze and Stay Silv White Flux
Temperature 1300°F
Frequency 215 kHz
Equipment DW-UHF-10kw output solid state induction power supply equipped with a standard heat station containing eight 0.33 μF capacitors for a total of 0.66μF, a step down transformer, and a specifically designed induction heating coil.
Process DW-UHF-10kw solid state induction power supply was setup to achieve the following results: · 2.0 kW of power was directly loaded into the copper tube resulting in a heating time of 7.2 seconds to reach the necessary 13000F for brazing.
Results& Processing ease was achieved through the design of a unique channel type coil comprised of three turns of 1/8" copper.
Melting Aluminum Tilting Crucible Induction Furnace
Melting Aluminum Tilting Crucible Induction Furnace
 HLQ Induction Equipment Co has a complete line of Tilting Crucible Melting Induction Furnaces to melt Aluminum, aluminum alloy, etc. Melting Furnaces are provided for temperature ranges from 600℃ to 900℃ by air cooled (max 1700℃ by water cooled ).
Application Range:
Aluminum melting induction furnace is widely used for the melting and keep warm process of the Low melting point non-ferrous metals, such as aluminum, copper, zinc, lead, tin, cadmium and other alloys. Suitable for all kinds of aluminum alloy castings, die castings, piston, engine block, automotive aluminum wheels, etc Our Crucible Melting Furnaces are provided for temperature ranges from 600℃ to 900℃ not water cooled.Product Features:
HLQ Induction Equipment Co has been designing, engineering, and manufacturing Tilting Crucible Melting Induction Furnaces since 1996.
Tilting type aluminum melting induction furnace, it unload liquid aluminum through diversion trench, also can be used to cast aluminum. It safe and reliable pouring used 2 hydraulic cylinders with end bearing dampers on tilting frame. The furnaces are using ultra save energy structure of ceramic fiber insulation. Very low heat loss due to excellent thermal insulation. Thermally efficient multi layered lining, insulated refractory lining, Longer crucible life, Fast, easy installation. High quality crucible, fast crucible thermal conductivity, high thermal efficiency, long service life. Designed for hand or robotic ladling directly to the die or mold or pressurized for low pressure die casting. HLQ Induction Equipment Co provides aluminum liquid holding furnace, which is mainly used for heat preservation, let stand, degassing and refining of melted aluminum alloy.Benefits:
- High efficiency and energy saving
- High thermal efficiency
- Stable and reliable operation


Annealing Metal Stamp With Induction
Annealing Metal Stamp With Induction
Objective: Induction Heating the opposite end of a metal stamp so that it mushrooms instead of cracks/splits when struck by a hammer.
Material S-7 steel of varying rectangular cross sectional sizes
Temperature 1400-1800 ºF (760-982) ºC
Frequency 300 kHz
Equipment DW-UHF-10KW, induction heating system, equipped with a remote heat station containing two 1.5 μF capacitors for a total of 0.75 μF and three different induction heating coils designed and developed specifically for this application.
Process One five-turn and two four-turn helical coils are used to heat the end of stamps to the required temperature. Two part sizes can be run in each of coils, using the same machine settings except for cycle time. Cycle rates dependent upon the crosssection size. The 3/8" (0.9525 cm) square size is has a rate of below 10 seconds. The rate for the middle size, ½" – 1 ½ " (1.27 - 3.81 cm) is 30 to 60 seconds. A 1" (2.54 cm) square part takes approximately two minutes. Fixturing can influence the length of the cycle time required. For shorter heat times a larger power supply may be used.
Results/Benefits Precise heat only to the area that needs annealing is more efficient and repeatable than heating with a torch.
Objective: Induction Heating the opposite end of a metal stamp so that it mushrooms instead of cracks/splits when struck by a hammer.
Material S-7 steel of varying rectangular cross sectional sizes
Temperature 1400-1800 ºF (760-982) ºC
Frequency 300 kHz
Equipment DW-UHF-10KW, induction heating system, equipped with a remote heat station containing two 1.5 μF capacitors for a total of 0.75 μF and three different induction heating coils designed and developed specifically for this application.
Process One five-turn and two four-turn helical coils are used to heat the end of stamps to the required temperature. Two part sizes can be run in each of coils, using the same machine settings except for cycle time. Cycle rates dependent upon the crosssection size. The 3/8" (0.9525 cm) square size is has a rate of below 10 seconds. The rate for the middle size, ½" – 1 ½ " (1.27 - 3.81 cm) is 30 to 60 seconds. A 1" (2.54 cm) square part takes approximately two minutes. Fixturing can influence the length of the cycle time required. For shorter heat times a larger power supply may be used.
Results/Benefits Precise heat only to the area that needs annealing is more efficient and repeatable than heating with a torch.
Annealing Metal Stamp With Induction
Annealing Metal Stamp With Induction
Objective: Induction Heating the opposite end of a metal stamp so that it mushrooms instead of cracks/splits when struck by a hammer.
Material S-7 steel of varying rectangular cross sectional sizes
Temperature 1400-1800 ºF (760-982) ºC
Frequency 300 kHz
Equipment DW-UHF-10KW, induction heating system, equipped with a remote heat station containing two 1.5 μF capacitors for a total of 0.75 μF and three different induction heating coils designed and developed specifically for this application.
Process One five-turn and two four-turn helical coils are used to heat the end of stamps to the required temperature. Two part sizes can be run in each of coils, using the same machine settings except for cycle time. Cycle rates dependent upon the crosssection size. The 3/8" (0.9525 cm) square size is has a rate of below 10 seconds. The rate for the middle size, ½" – 1 ½ " (1.27 - 3.81 cm) is 30 to 60 seconds. A 1" (2.54 cm) square part takes approximately two minutes. Fixturing can influence the length of the cycle time required. For shorter heat times a larger power supply may be used.
Results/Benefits Precise heat only to the area that needs annealing is more efficient and repeatable than heating with a torch.
Objective: Induction Heating the opposite end of a metal stamp so that it mushrooms instead of cracks/splits when struck by a hammer.
Material S-7 steel of varying rectangular cross sectional sizes
Temperature 1400-1800 ºF (760-982) ºC
Frequency 300 kHz
Equipment DW-UHF-10KW, induction heating system, equipped with a remote heat station containing two 1.5 μF capacitors for a total of 0.75 μF and three different induction heating coils designed and developed specifically for this application.
Process One five-turn and two four-turn helical coils are used to heat the end of stamps to the required temperature. Two part sizes can be run in each of coils, using the same machine settings except for cycle time. Cycle rates dependent upon the crosssection size. The 3/8" (0.9525 cm) square size is has a rate of below 10 seconds. The rate for the middle size, ½" – 1 ½ " (1.27 - 3.81 cm) is 30 to 60 seconds. A 1" (2.54 cm) square part takes approximately two minutes. Fixturing can influence the length of the cycle time required. For shorter heat times a larger power supply may be used.
Results/Benefits Precise heat only to the area that needs annealing is more efficient and repeatable than heating with a torch.
Induction Soldering Stainless Steel To Wire
Induction Soldering Stainless Steel To Wire With IGBT High Frequency Heating Units
Objective Heat Stainless steel connector for soldering application in automotive wire harness manufacturing
Material Stainless steel connector 1.57” (40mm) long, 0.6” (15mm) OD & 0.4” (10mm) thick. Lead free solder
Temperature 392 ºF (200 ºC)
Frequency 352 kHz
Equipment • DW-UHF-6kW induction heating system, equipped with a remote workhead containing one 1 μF capacitor.
• An induction heating coil designed and developed specifically for this application.
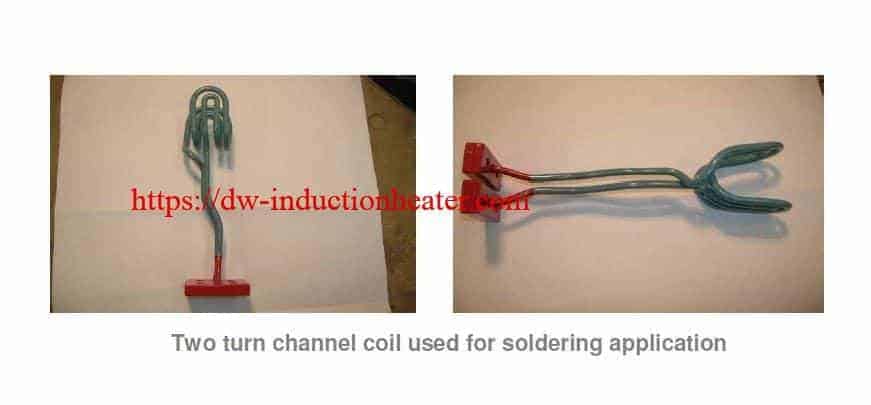
Process A two turn channel coil is used for soldering the connector to the wire harness. The stainless steel connector and wire harness are placed in the coil for 20 seconds for the solder to
fill just the top of the connector.
Results/Benefits Induction heating provides:
• By precisely heating the metal, the plastic shroud is not directly heated
• Reduced production cost
• Faster process time, reduced production cost
• Hands-free heating that involves no operator skill for manufacturing
• Even distribution of heating

2023年2月24日星期五
Brazing Aluminum Tubing to Aluminum Parts
Objective
The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment
DW-HF-15kw induction heating machine
[caption id="attachment_97" align="alignnone" width="267"]
 induction heating machine HF-15[/caption]
Induction heating coil
Materials
• Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID
• Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm),
chamfer at top area is 0.2375” (6.033mm) ID max
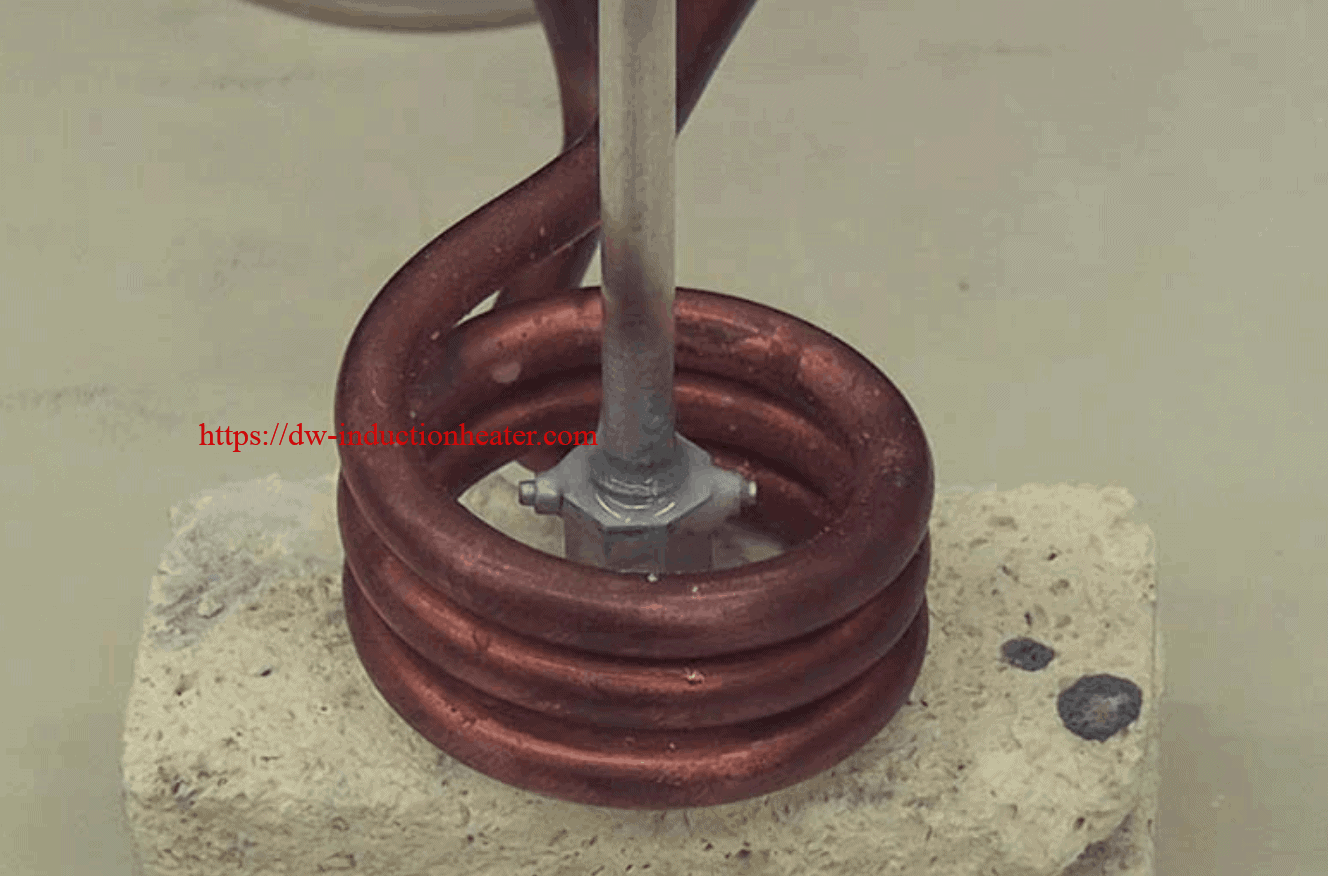
• Braze alloy in the form of two-turn alloy ring
• Flux

Key Parameters
Temperature: 1030°F (554°C)
Power: 5 kW
Time: 14 seconds
Process:
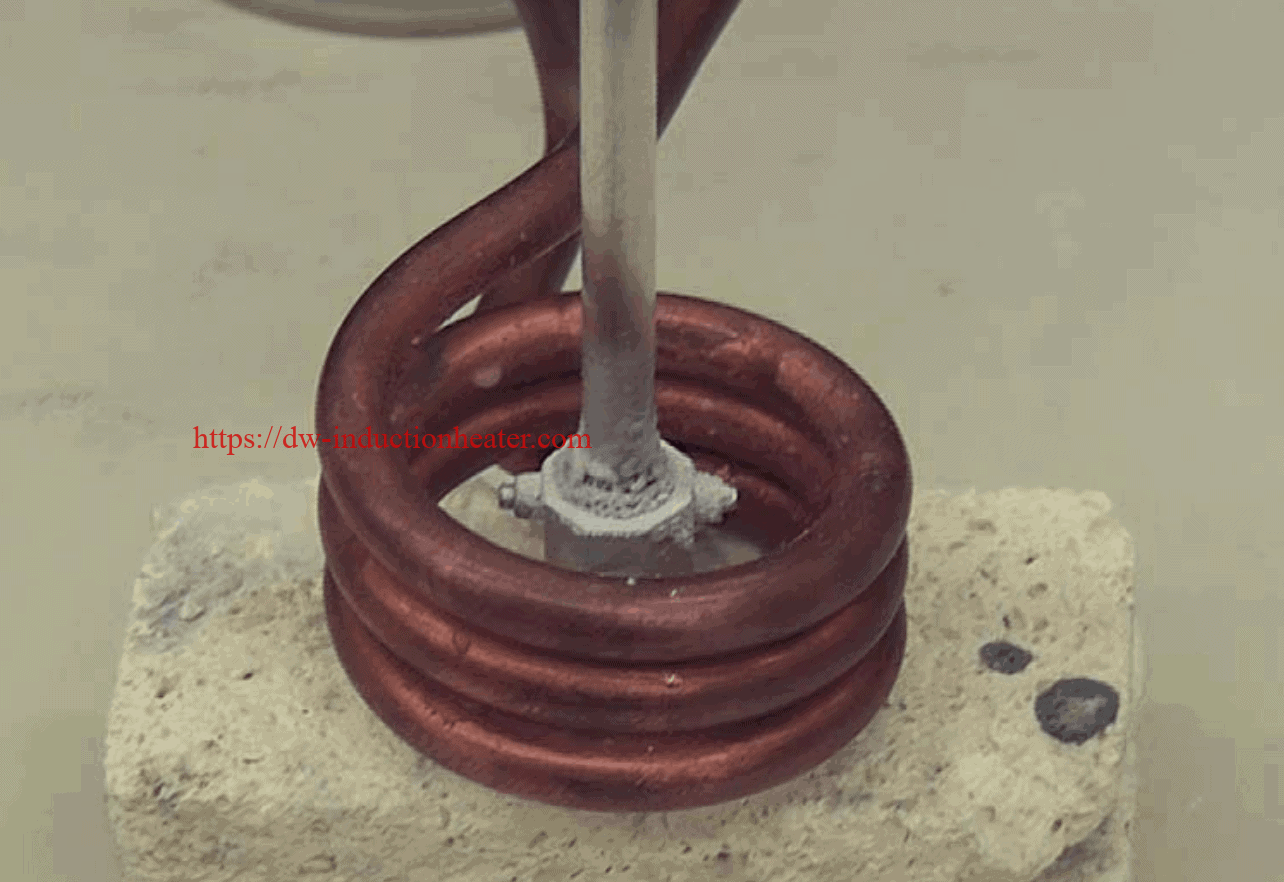
- The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
- The part was positioned in the induction coil.
- Several tests were conducted with different cycle times to confirm the heating time for a good braze.
- At 15 seconds the assembly melted.
- At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.

Results/Benefits:
The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
- Precise control of the time and temperature
- Power on demand with rapid heat cycles
- Repeatable process, not operator dependent
- Safe induction heating with no open flames
- Energy efficient heating
订阅:
博文 (Atom)
我的简介

- HLQ induction heating machine
- HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.