显示标签为“InductionBrazingAluminum”的博文。显示所有博文

2024年3月17日星期日

Brazing Aluminum Tubing to Aluminum Parts

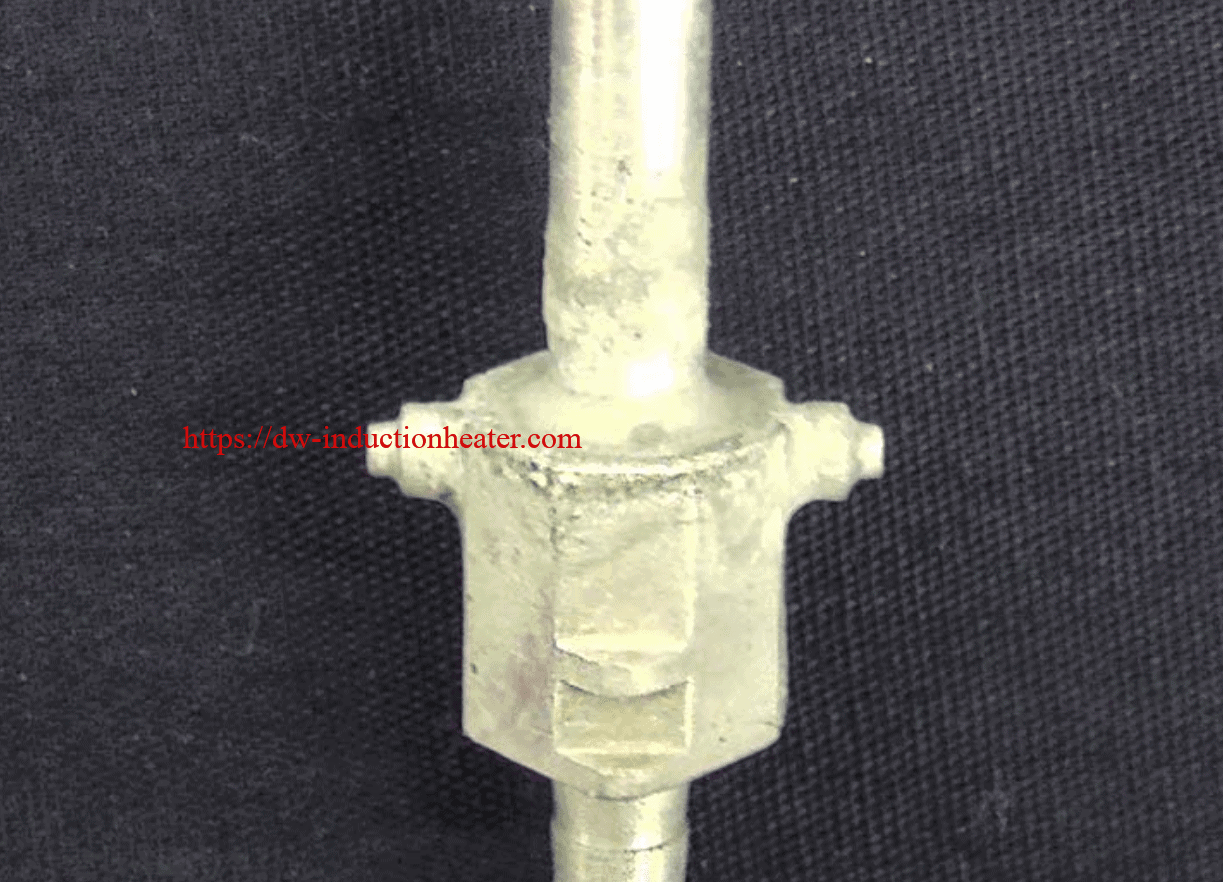
Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
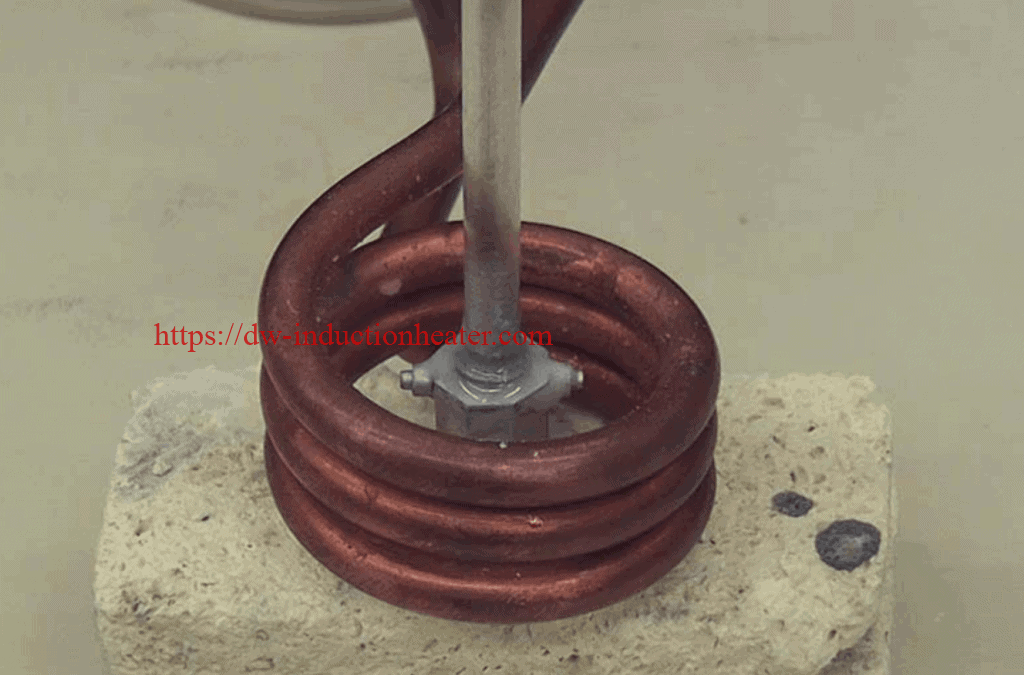
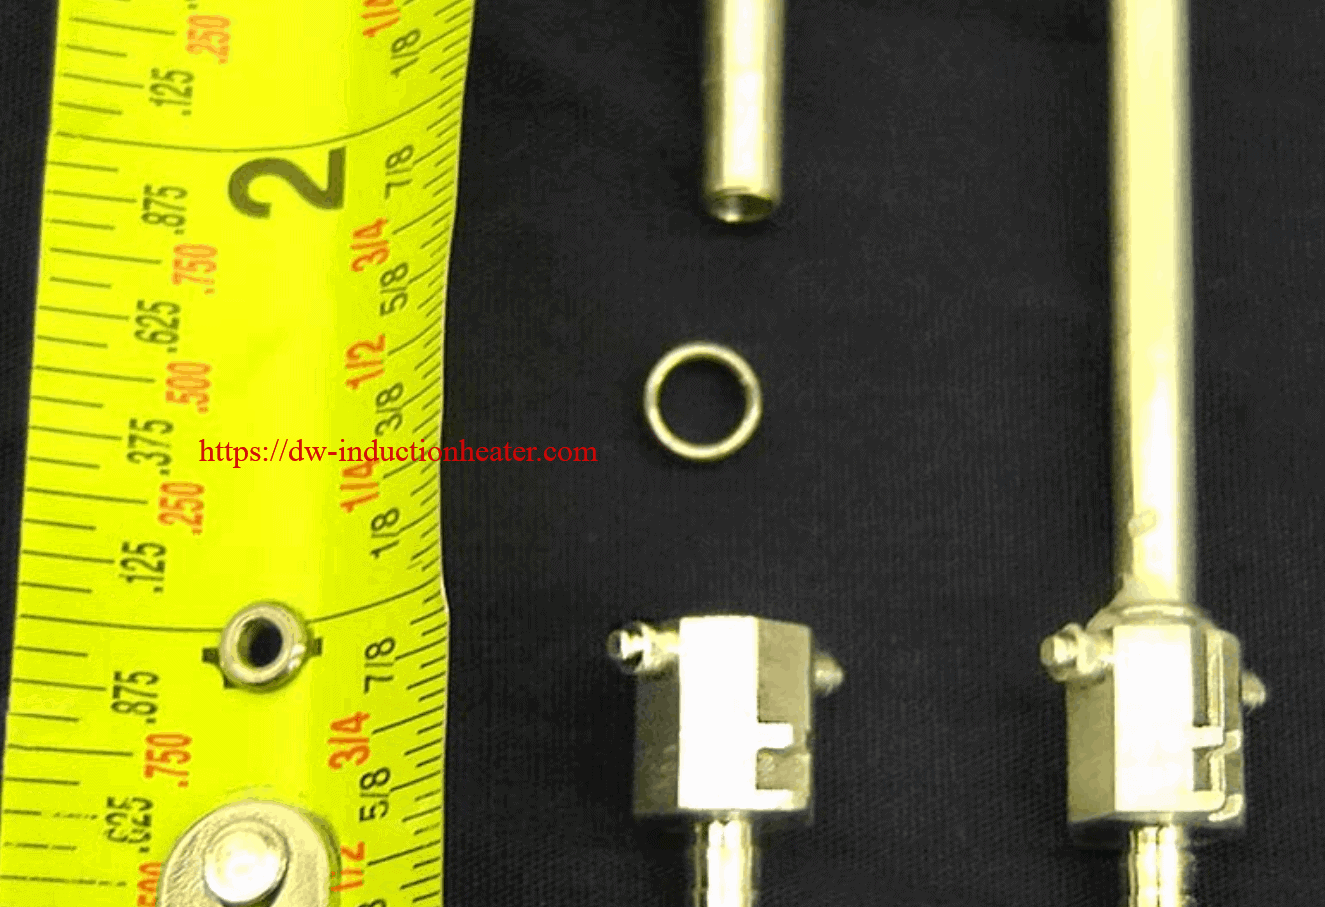
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
Process:
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
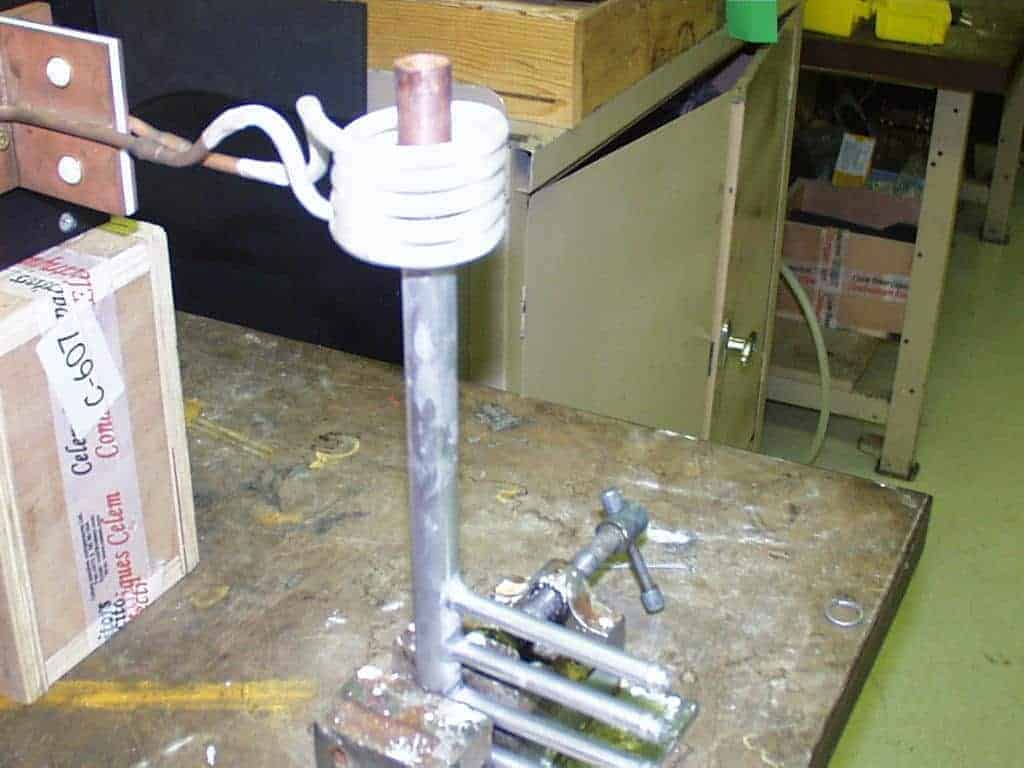
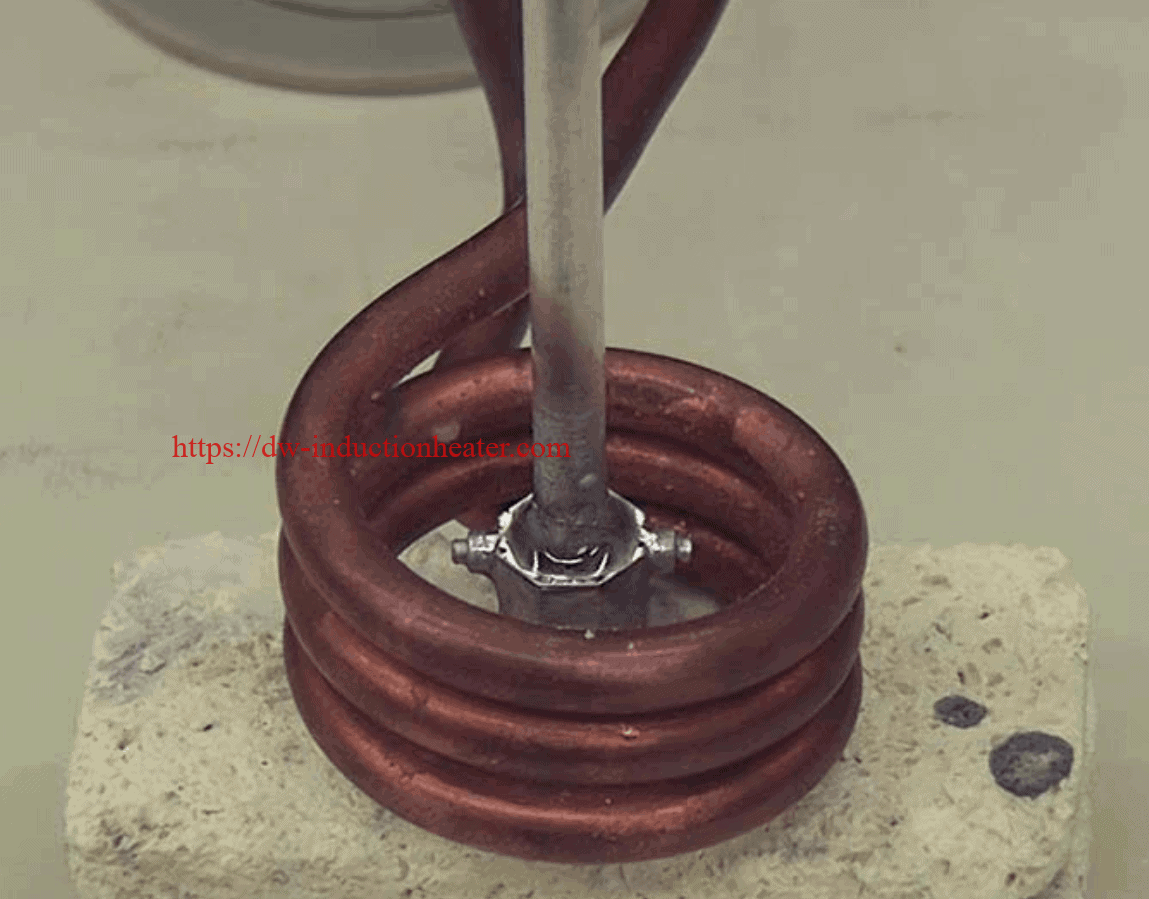
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating
https://dw-inductionheater.com/brazing-aluminum-tubing-to-aluminum-parts.html?feed_id=237093&_unique_id=65f7790bc0f47

2023年11月7日星期二

Induction Brazing Aluminum Pipes

Induction Brazing Aluminum Pipes Objective: Brazing two aluminum pipes simultaneously to an aluminum evaporator core Material 2 aluminum pipes 0.72" (18.3mm) diameter, evaporator core 9.88" x 10.48" x 1.5" thick (251mm x 266.3mm x 38mm), braze rings Temperature 610 ºF (321 ºC) Frequency 250 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A four turn helical pancake coil is used to heat the 2 pipes simultaneously. Three braze rings are placed on each joint and power is applied for 90-100 seconds to create a leak proof joint on both pipes. Narrative • Customer is requiring a 40 seconds heat time for both brazes. In order to meet this requirement 3 units will be utilized to braze 2 joints each for a total of 6 joints in 90-100 seconds. The customer is currently using a flame process which can burn away the thin flange at the joint area and create scrap parts. By switching to induction for this application the customer is decreasing their scrap parts and also increasing their quality and production rate. Results/Benefits Induction heating provides: • Repeatable leak free joints • Increased part quality, less scrap • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating

Induction Brazing Aluminum Pipes

Induction Brazing Aluminum Pipes Objective: Brazing two aluminum pipes simultaneously to an aluminum evaporator core Material 2 aluminum pipes 0.72" (18.3mm) diameter, evaporator core 9.88" x 10.48" x 1.5" thick (251mm x 266.3mm x 38mm), braze rings Temperature 610 ºF (321 ºC) Frequency 250 kHz Equipment • DW-UHF-20KW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A four turn helical pancake coil is used to heat the 2 pipes simultaneously. Three braze rings are placed on each joint and power is applied for 90-100 seconds to create a leak proof joint on both pipes. Narrative • Customer is requiring a 40 seconds heat time for both brazes. In order to meet this requirement 3 units will be utilized to braze 2 joints each for a total of 6 joints in 90-100 seconds. The customer is currently using a flame process which can burn away the thin flange at the joint area and create scrap parts. By switching to induction for this application the customer is decreasing their scrap parts and also increasing their quality and production rate. Results/Benefits Induction heating provides: • Repeatable leak free joints • Increased part quality, less scrap • Hands-free heating that involves no operator skill for manufacturing • Even distribution of heating https://dw-inductionheater.com/induction-brazing-aluminum-pipes.html?feed_id=230316&_unique_id=6549f1063f4ea

2023年11月6日星期一

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
  https://dw-inductionheater.com/brazing-aluminum-to-copper-tubes-with-induction.html?feed_id=230286&_unique_id=65493a353009e

2023年10月30日星期一

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年10月17日星期二

Brazing Aluminum Tubing to Aluminum Parts

Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
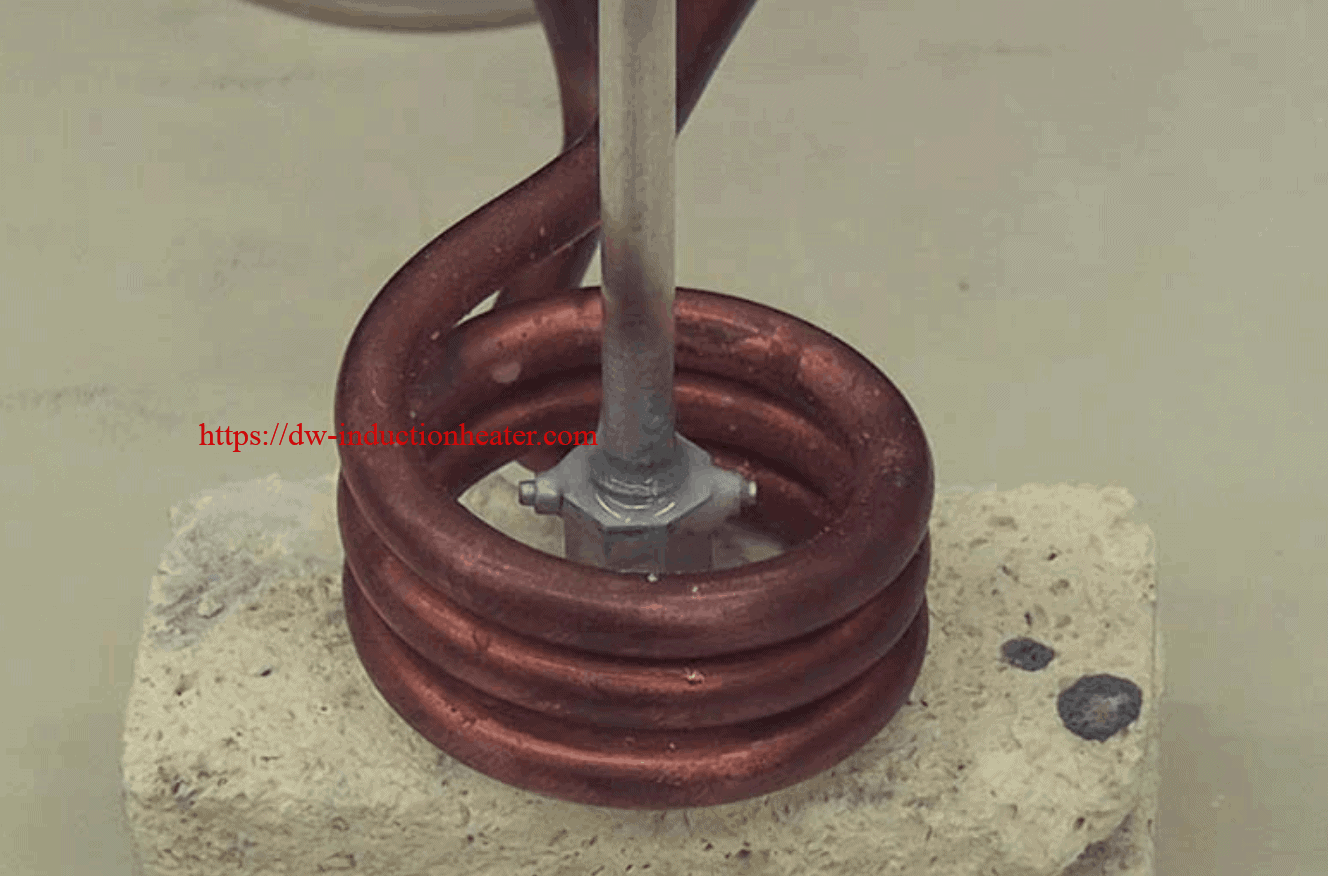
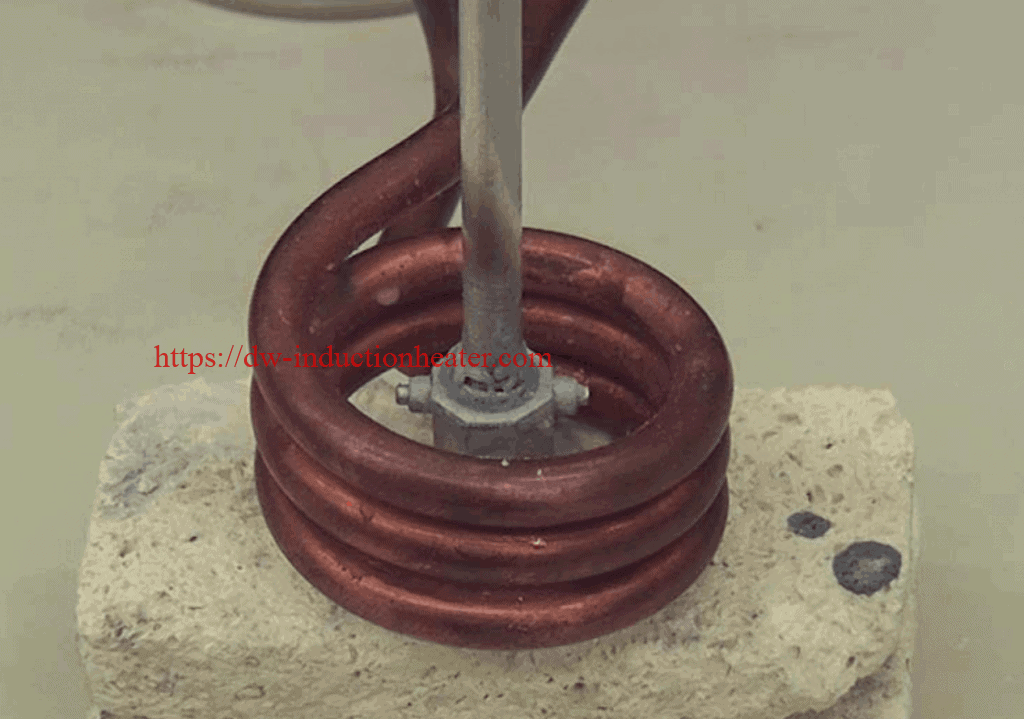
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
Process:
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating

2023年9月24日星期日

Induction Brazing Aluminum Automotive

Induction Brazing Aluminum Automotive  Objective: Heat aluminum for an automotive brazing application Material: Aluminum tubing 0.50 (12.7mm) dia, an aluminum boss 1” (25.4mm) long, flux filled braze rings Temperature: 1200 ºF (649 ºC) Frequency: 370 kHz Equipment • DW-UHF-10KW induction heating system, equipped with a remote workhead containing one 1.0μF capacitors for a total of 1.0 μF • An induction heating coil designed and developed specifically for this application. Process A multi turn pancake coil is used to heat the joint between the aluminum tubing and boss. The joint heats to temperature in 1.5 minutes and the braze ring melts forming a clean brazed joint. Results/Benefits Induction heating provides: • Hands-free heating that involves minimal operator skill for manufacturing • Flameless application • Reliable, repeatable aesthetically pleasing braze joint • Even distribution of heating

2023年8月8日星期二

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年7月25日星期二

Brazing Aluminum Tubing to Aluminum Parts

Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
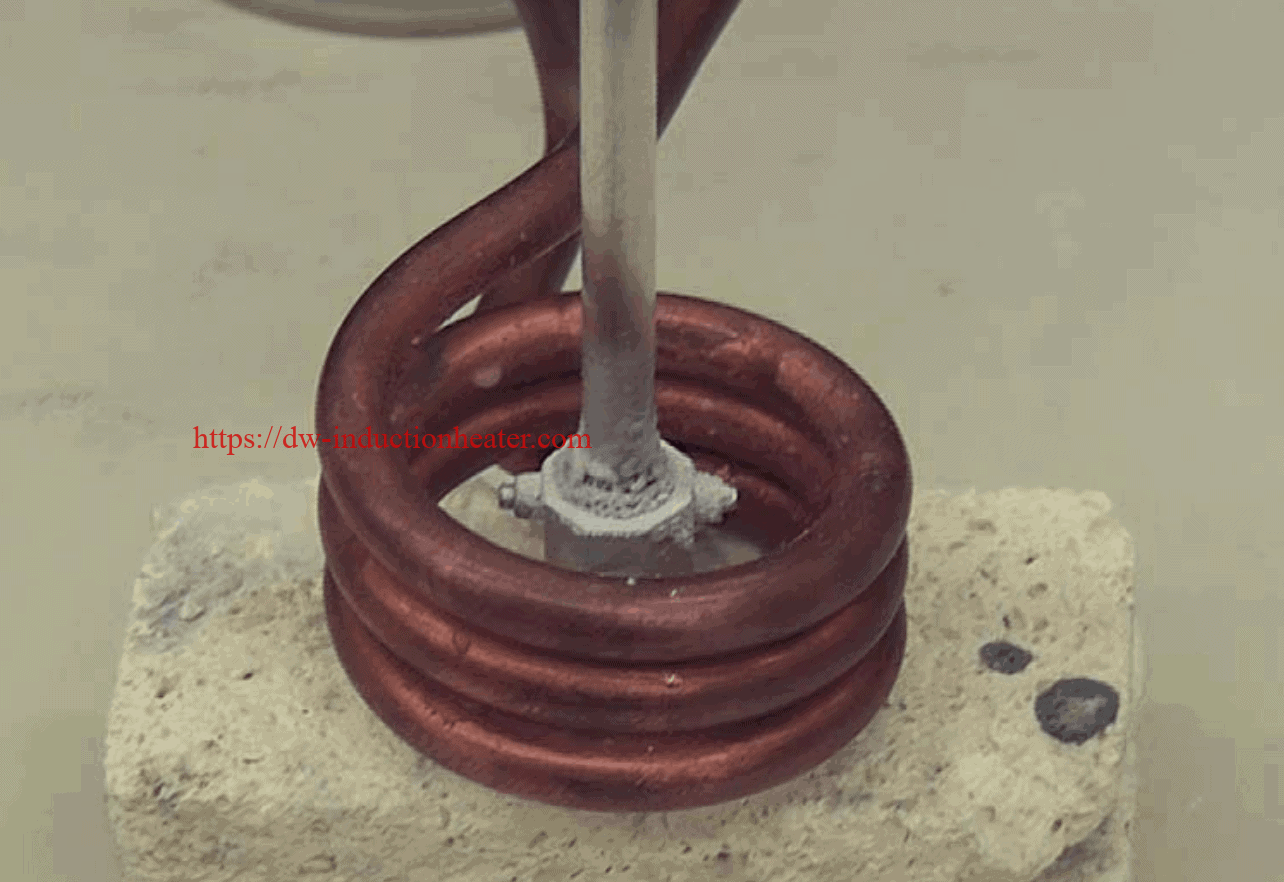
Process:
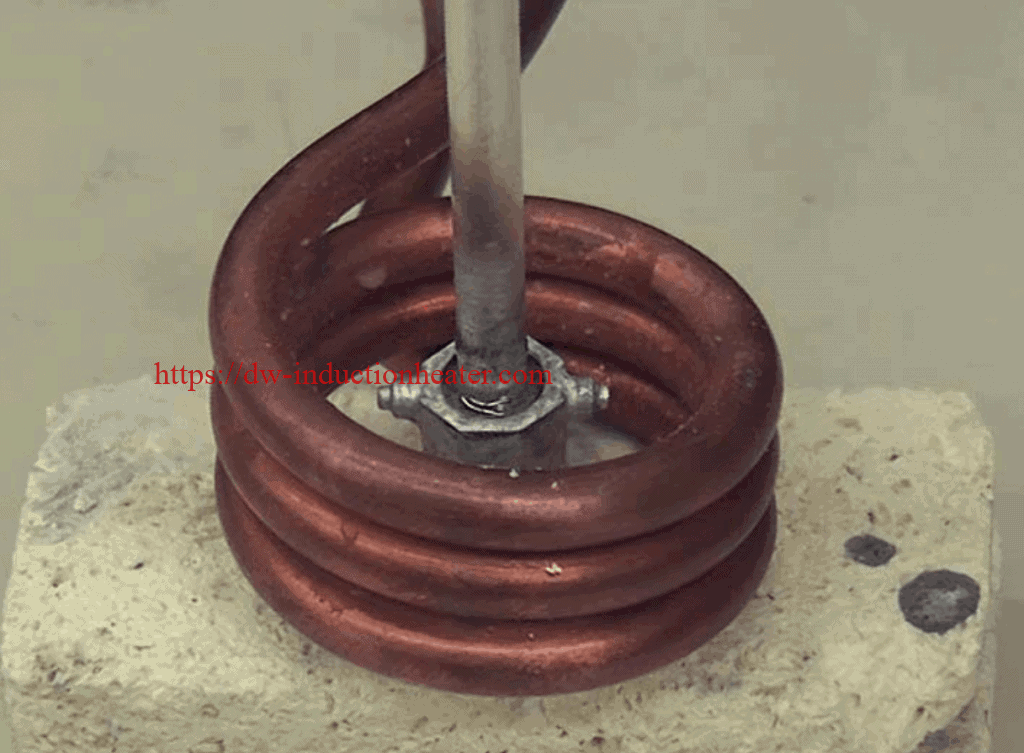
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating
https://dw-inductionheater.com/brazing-aluminum-tubing-to-aluminum-parts.html?feed_id=220411&_unique_id=64c00640be5d9

2023年7月21日星期五

Brazing Aluminum Tubing to Aluminum Parts

Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
Process:
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
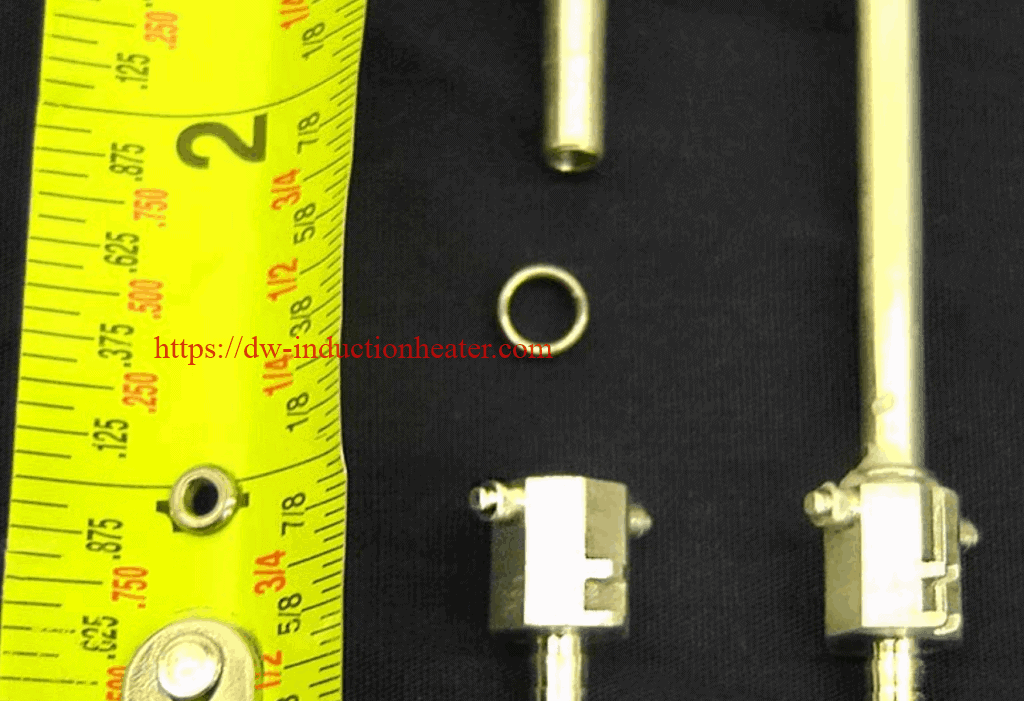
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating

2023年7月6日星期四

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年6月8日星期四

Brazing Aluminum Tubing to Aluminum Parts

Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
Process:
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
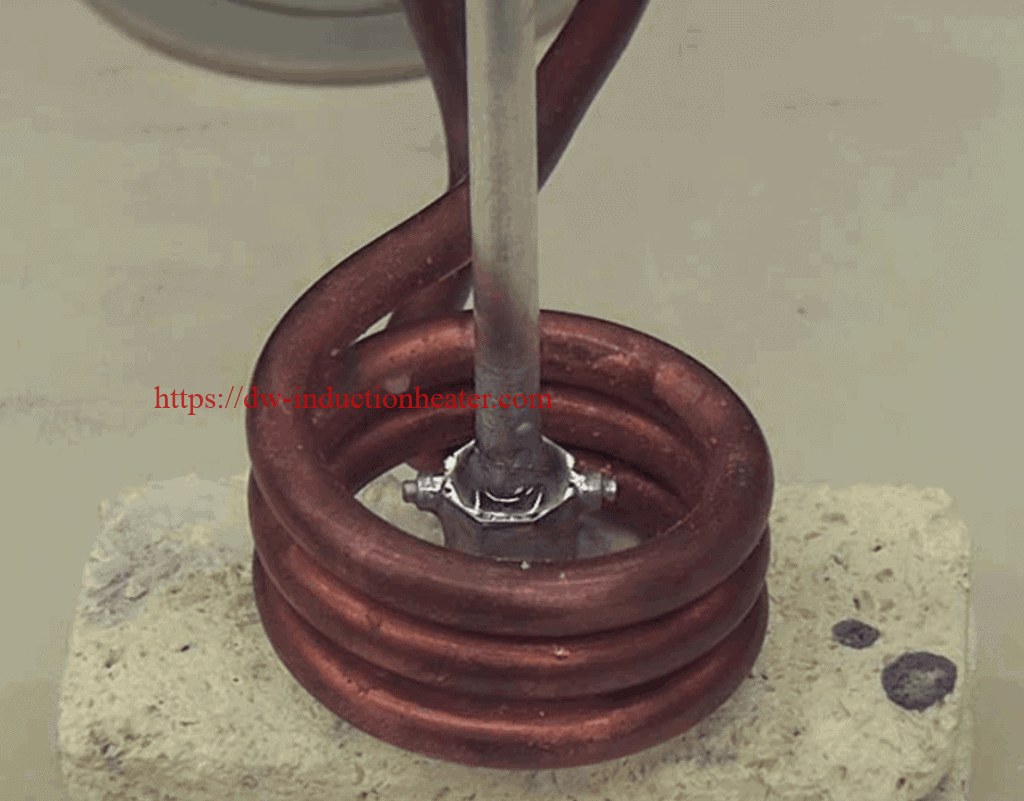
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating

2023年5月19日星期五

Brazing Aluminum Tubing to Aluminum Parts

Objective The objective of the application test is induction brazing aluminum tubing to aluminum parts in less than 15 seconds. We have aluminum tubing and an aluminum “receiver”. The brazing alloy is an alloy ring, and has a flow temperature of 1030°F (554°C).
Equipment DW-HF-15kw induction heating machine   [caption id="attachment_97" align="alignnone" width="267"]induction heating units HF-15 induction heating machine HF-15[/caption] Induction heating coil Materials • Aluminum tube: 0.167” (4.242mm) OD, 0.108” (2.743mm) ID • Aluminum component: ID .1675” (4.255mm), depth .288” (7.315mm), chamfer at top area is 0.2375” (6.033mm) ID max • Braze alloy in the form of two-turn alloy ring • Flux Key Parameters Temperature: 1030°F (554°C) Power: 5 kW Time: 14 seconds
Process:
  1. The Aluminum component and tube were assembled together with the alloy ring. Flux was added.
  2. The part was positioned in the induction coil.
  3. Several tests were conducted with different cycle times to confirm the heating time for a good braze.
  4. At 15 seconds the assembly melted.
  5. At 14 seconds, we had success for brazing aluminum to aluminum, and a good quality braze joint was achieved.
Results/Benefits: The 5 kW induction heating system requested by the customer, will meet the customer’s time requirements for induction brazing.
  • Precise control of the time and temperature
  • Power on demand with rapid heat cycles
  • Repeatable process, not operator dependent
  • Safe induction heating with no open flames
  • Energy efficient heating

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.