显示标签为“inductionheatingaluminum”的博文。显示所有博文

2024年5月28日星期二

Induction Heating Aluminum Pipe

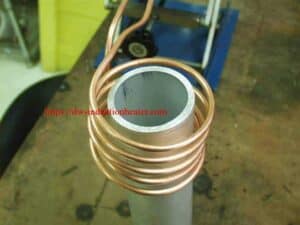
Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe https://dw-inductionheater.com/induction-heating-aluminum-pipe.html?feed_id=247678&_unique_id=665672a46957a
2024年5月11日星期六

Induction Heating Aluminum Catheter Tipping

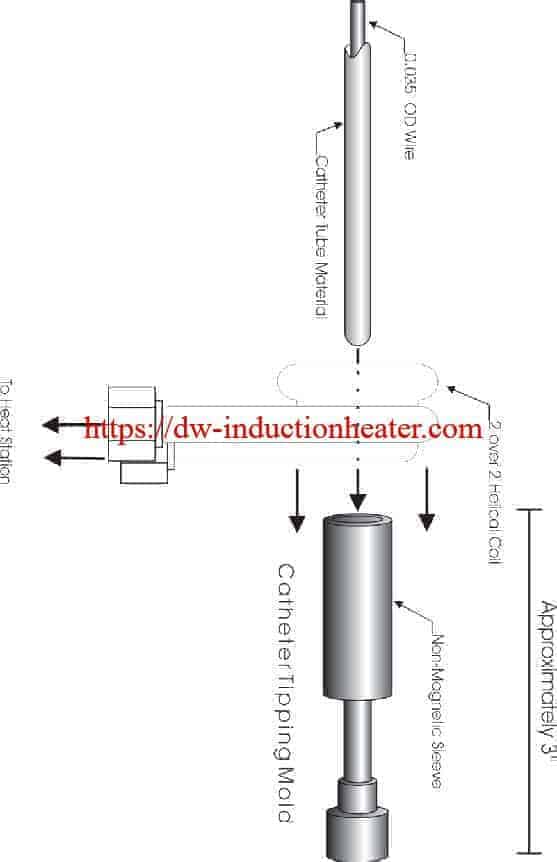
Induction Heating Aluminum Catheter Tipping With IGBT Heating Units Objective: To heat an aluminum catheter tipping die to above 2850F within 2 to 5 seconds for the forming of catheter material. Presently, heating is performed in 15 seconds with older induction equipment. The customer would like to use solid state induction equipment to reduce the heating times and develop a more efficient process. Material: Aluminum catheter tipping die measuring 3/8" OD and 2" long with a nonmagnetic sleeve over the heat zone. The catheter material was described as being similar to polyurethane plastic. Also, a 0.035" diameter steel wire was inserted into the catheter tube to prevent collapsing. Temperature: 5000F Application: The DW-UHF-4.5kW solid state induction power supply was determined to most efficiently produce the following results: A heating time of 3.3 seconds to reach 5000F and form the catheter was achieved through the use of a two (2) over two (2) turn helical coil. A quality catheter was formed by pressing 1/2" of the polyurethane tube into the mold while retaining shape through the use of a 0.035" wire to prevent collapsing of the tube. Laboratory results show that a substantial time decrease was accomplished which will allow for a significant increase in production while not sacrificing quality. Equipment: DW-UHF-4.5kW solid state induction power supply including a remote heat station containing one (1) capacitor totalling 1.2 μF. Frequency: 287 kHz Induction Heating Aluminum Catheter Tipping https://dw-inductionheater.com/induction-heating-aluminum-catheter-tipping.html?feed_id=245256&_unique_id=66404f89b277f

2023年11月6日星期一

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
  https://dw-inductionheater.com/brazing-aluminum-to-copper-tubes-with-induction.html?feed_id=230286&_unique_id=65493a353009e

2023年10月30日星期一

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年10月16日星期一

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe

2023年10月6日星期五

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe https://dw-inductionheater.com/induction-heating-aluminum-pipe.html?feed_id=228491&_unique_id=651fcf111ae0c

2023年9月19日星期二

Induction Heating Aluminum Catheter Tipping

Induction Heating Aluminum Catheter Tipping With IGBT Heating Units Objective: To heat an aluminum catheter tipping die to above 2850F within 2 to 5 seconds for the forming of catheter material. Presently, heating is performed in 15 seconds with older induction equipment. The customer would like to use solid state induction equipment to reduce the heating times and develop a more efficient process. Material: Aluminum catheter tipping die measuring 3/8" OD and 2" long with a nonmagnetic sleeve over the heat zone. The catheter material was described as being similar to polyurethane plastic. Also, a 0.035" diameter steel wire was inserted into the catheter tube to prevent collapsing. Temperature: 5000F Application: The DW-UHF-4.5kW solid state induction power supply was determined to most efficiently produce the following results: A heating time of 3.3 seconds to reach 5000F and form the catheter was achieved through the use of a two (2) over two (2) turn helical coil. A quality catheter was formed by pressing 1/2" of the polyurethane tube into the mold while retaining shape through the use of a 0.035" wire to prevent collapsing of the tube. Laboratory results show that a substantial time decrease was accomplished which will allow for a significant increase in production while not sacrificing quality. Equipment: DW-UHF-4.5kW solid state induction power supply including a remote heat station containing one (1) capacitor totalling 1.2 μF. Frequency: 287 kHz Induction Heating Aluminum Catheter Tipping https://dw-inductionheater.com/induction-heating-aluminum-catheter-tipping.html?feed_id=227561&_unique_id=6509ab9f54bbb

2023年8月8日星期二

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年7月6日星期四

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年6月13日星期二

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe
2023年5月10日星期三

Induction Heating Aluminum Catheter Tipping

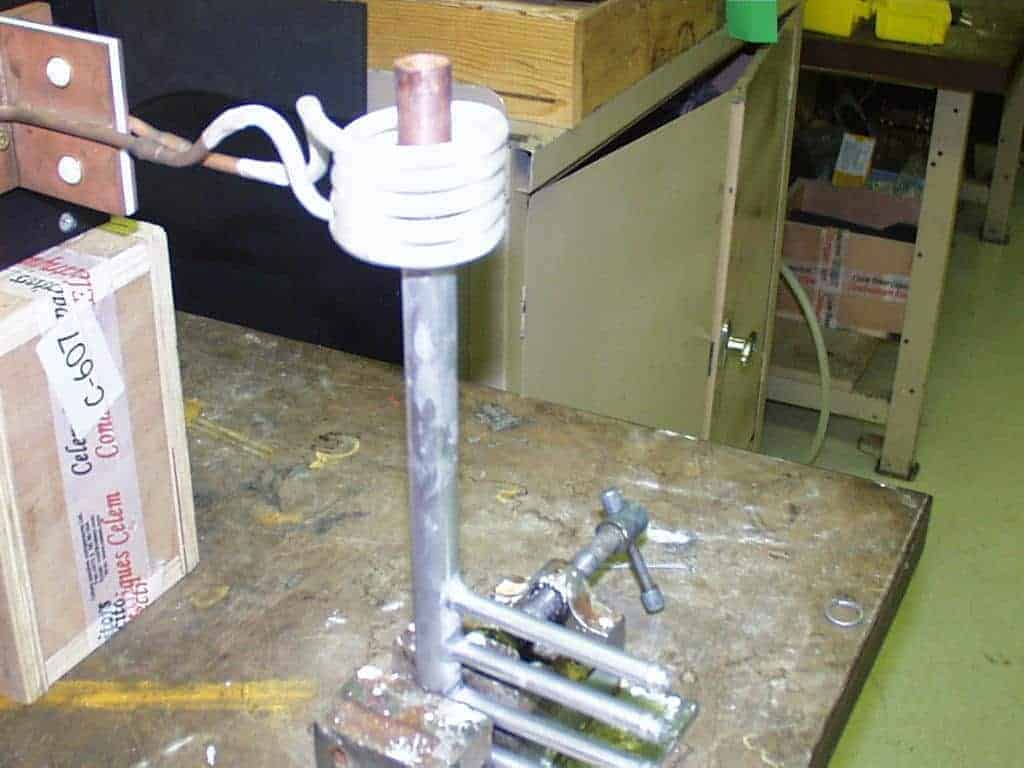
Induction Heating Aluminum Catheter Tipping With IGBT Heating Units Objective: To heat an aluminum catheter tipping die to above 2850F within 2 to 5 seconds for the forming of catheter material. Presently, heating is performed in 15 seconds with older induction equipment. The customer would like to use solid state induction equipment to reduce the heating times and develop a more efficient process. Material: Aluminum catheter tipping die measuring 3/8" OD and 2" long with a nonmagnetic sleeve over the heat zone. The catheter material was described as being similar to polyurethane plastic. Also, a 0.035" diameter steel wire was inserted into the catheter tube to prevent collapsing. Temperature: 5000F Application: The DW-UHF-4.5kW solid state induction power supply was determined to most efficiently produce the following results: A heating time of 3.3 seconds to reach 5000F and form the catheter was achieved through the use of a two (2) over two (2) turn helical coil. A quality catheter was formed by pressing 1/2" of the polyurethane tube into the mold while retaining shape through the use of a 0.035" wire to prevent collapsing of the tube. Laboratory results show that a substantial time decrease was accomplished which will allow for a significant increase in production while not sacrificing quality. Equipment: DW-UHF-4.5kW solid state induction power supply including a remote heat station containing one (1) capacitor totalling 1.2 μF. Frequency: 287 kHz Induction Heating Aluminum Catheter Tipping
2023年4月7日星期五

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2023年4月4日星期二

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe

2023年3月18日星期六

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe

2023年2月18日星期六

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater

Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve
Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness
Temperature 700 ºF (371 ºC)
Frequency 71 kHz
Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF
• An induction heating coil designed and developed specifically for this application.
Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC).
Results/Benefits Induction heating provides:
• Uniform through heating
• Fast, energy-efficient heat
• Fast, controllable and repeatable process
• Hands-free heating that involves no operator skill for manufacturing

induction heating aluminum pipe

2023年2月17日星期五

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2022年12月30日星期五

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2022年12月15日星期四

Brazing Aluminum to Copper Tubes with Induction

Brazing Aluminum to Copper Tubes with Induction Objective: To heat an aluminum manifold to 1050 ºF (566 ºC) for a brazing application: Material :
  • Cu tubes (3/4"/19mm)
  • Cu tubes (5/8"/15.8mm)
  • AI tubes (3/8"/9.5mm)
  • AI manifold (5/8"/15.8mm)
  • AI manifold (3/4"/19mm)
  • Lucas-Milhaupt Handy One alloy 30-832
  • Braze wire
Temperature 1050 ºF (566 ºC) Frequency 260 kHz Equipment DW-UHF-10KW 150-500 kHz induction heating system equipped with a remote heat station containing two 1.5 μF capacitors.
  • A two-turn oval helical induction heating coil designed and developed specifically for the aluminum assembly
  • A five-turn helical induction heating coil designed and developed specifically for brazing the Cu tubes to AI joint assembly
Process Braze : pre-forms were designed to fit the aluminum tubes. Then the four aluminum tubes were placed into the manifold and the assembly was inserted into the coil. The assembly was heated for approximately 70 seconds, at which point it reached the targeted temperature and braze flowed. For the Cu tubes, a braze pre-form was also designed for them, wound around the tubes, and the assembly was placed inside the coil. The heating cycle time was approximately 100 seconds. Some joints required stick feeding of braze to fill the entire joint area due to the braze wire size. If the cycle time was lengthened, the need for stick feeding would be eliminated. Results/Benefits: Precise, repeatable heating:
  • The client wanted more precise and repeatable heating than a torch could deliver, which induction was able to achieve .
  • Temperature control: Induction allows for superior temperature control when compared to other methods, including a torch, which the client desired
 

2022年10月21日星期五

Induction Heating Aluminum Catheter Tipping

Induction Heating Aluminum Catheter Tipping With IGBT Heating Units Objective: To heat an aluminum catheter tipping die to above 2850F within 2 to 5 seconds for the forming of catheter material. Presently, heating is performed in 15 seconds with older induction equipment. The customer would like to use solid state induction equipment to reduce the heating times and develop a more efficient process. Material: Aluminum catheter tipping die measuring 3/8" OD and 2" long with a nonmagnetic sleeve over the heat zone. The catheter material was described as being similar to polyurethane plastic. Also, a 0.035" diameter steel wire was inserted into the catheter tube to prevent collapsing. Temperature: 5000F Application: The DW-UHF-4.5kW solid state induction power supply was determined to most efficiently produce the following results: A heating time of 3.3 seconds to reach 5000F and form the catheter was achieved through the use of a two (2) over two (2) turn helical coil. A quality catheter was formed by pressing 1/2" of the polyurethane tube into the mold while retaining shape through the use of a 0.035" wire to prevent collapsing of the tube. Laboratory results show that a substantial time decrease was accomplished which will allow for a significant increase in production while not sacrificing quality. Equipment: DW-UHF-4.5kW solid state induction power supply including a remote heat station containing one (1) capacitor totalling 1.2 μF. Frequency: 287 kHz Induction Heating Aluminum Catheter Tipping

2022年9月3日星期六

Induction Heating Aluminum Pipe

Induction Heating Aluminum Pipe For End Forming With High Frequency Induction Heater Objective Through heating the top 2” (50.8mm) of aluminum oxygen tank to form a rounded end with a hole for oxygen valve Material Aluminum oxygen tank with open end 2.25” (57.15mm) diameter, 0.188” (4.8mm) wall thickness Temperature 700 ºF (371 ºC) Frequency 71 kHz Equipment • DW-HF-45kW induction heating system, equipped with a remote workhead containing two 1.5μF capacitors for a total of 0.75μF • An induction heating coil designed and developed specifically for this application. Process A five turn helical coil is used to heat the open end of the oxygen tank. The tank is heated for 24 seconds to reach 700ºF (371 ºC). Results/Benefits Induction heating provides: • Uniform through heating • Fast, energy-efficient heat • Fast, controllable and repeatable process • Hands-free heating that involves no operator skill for manufacturing induction heating aluminum pipe

关注者

我的简介

我的照片
HLQ induction heating machine manufacturer provides the service of induction brazing,melting,hot forming,hardening surface,annealing,shrink fitting,PWHT,etc.